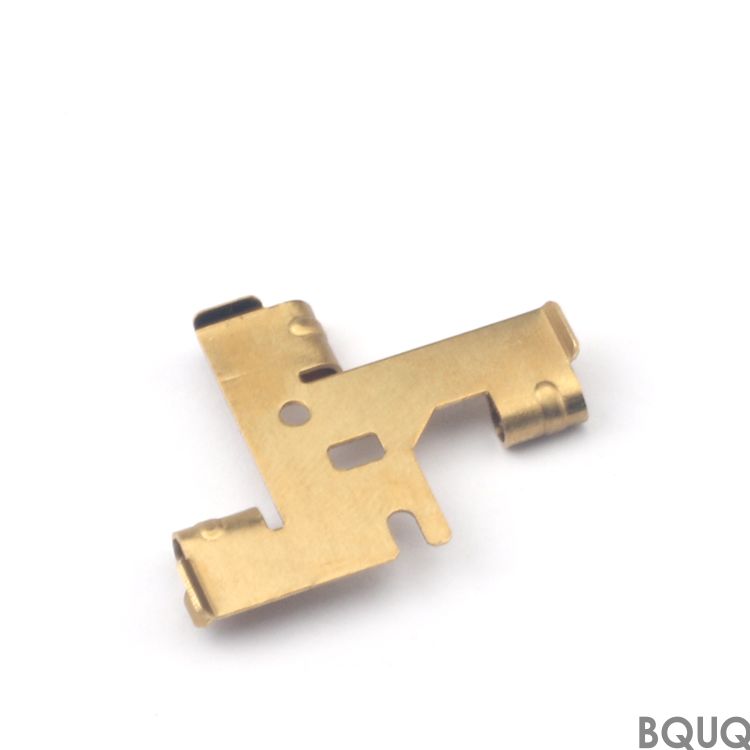
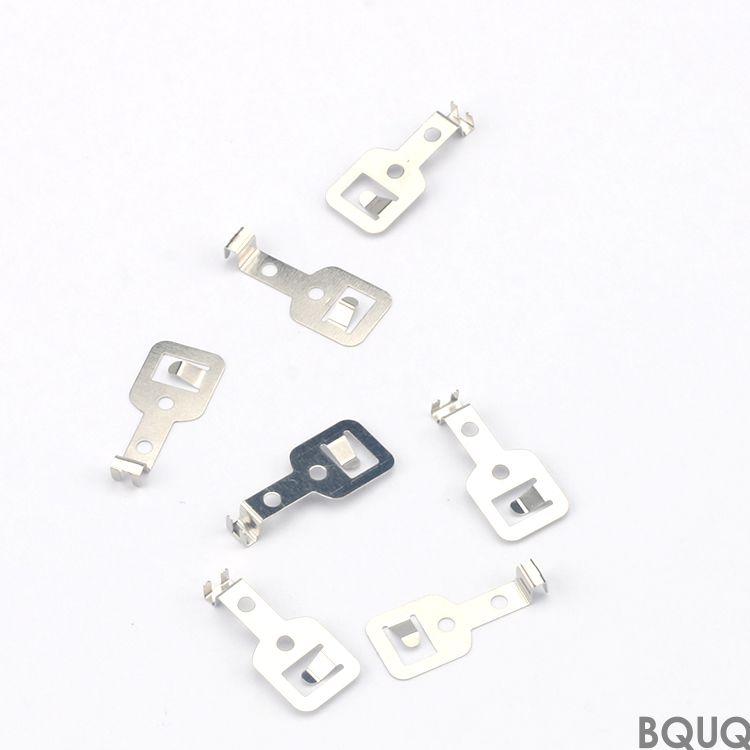
BQUQ Energy Storage Battery Connectors Collection | Precision Metal Stamping
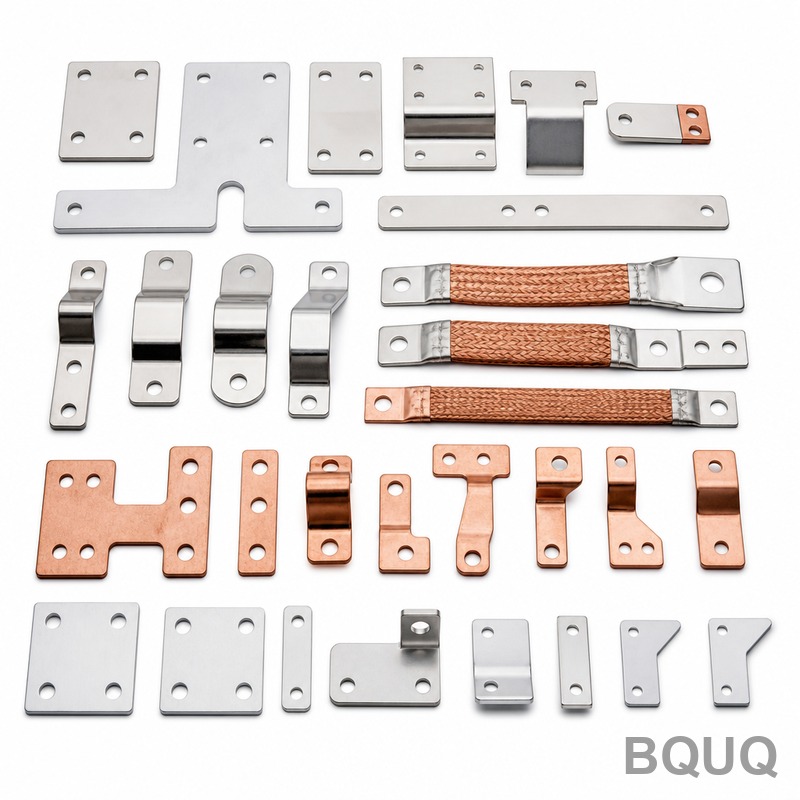
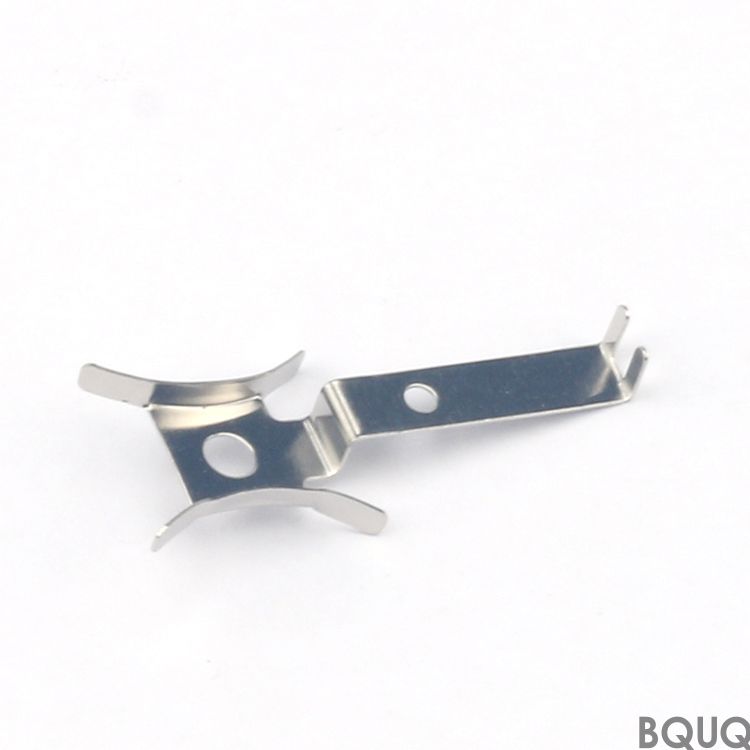
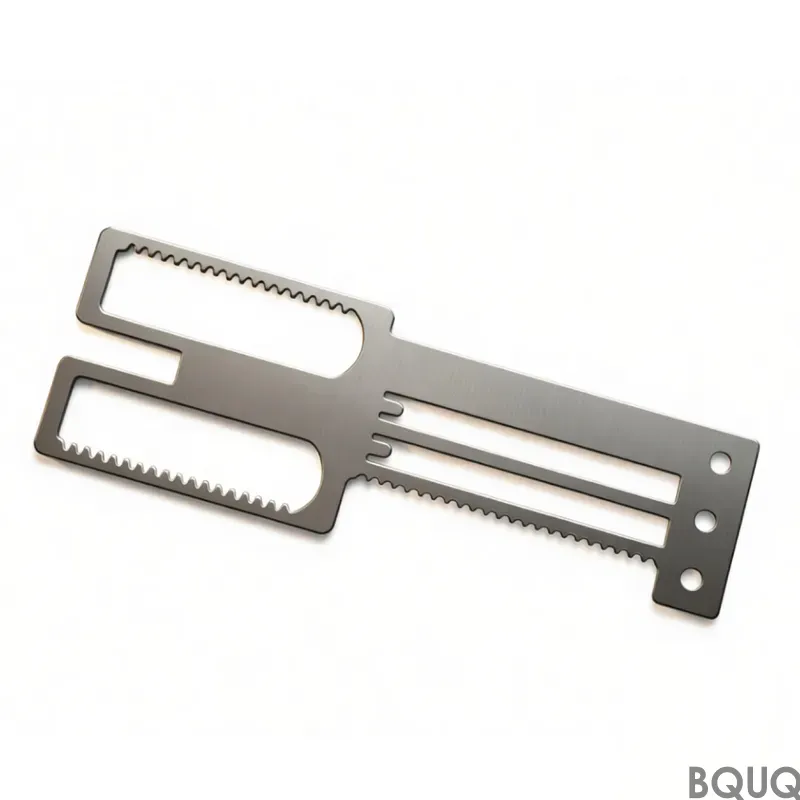
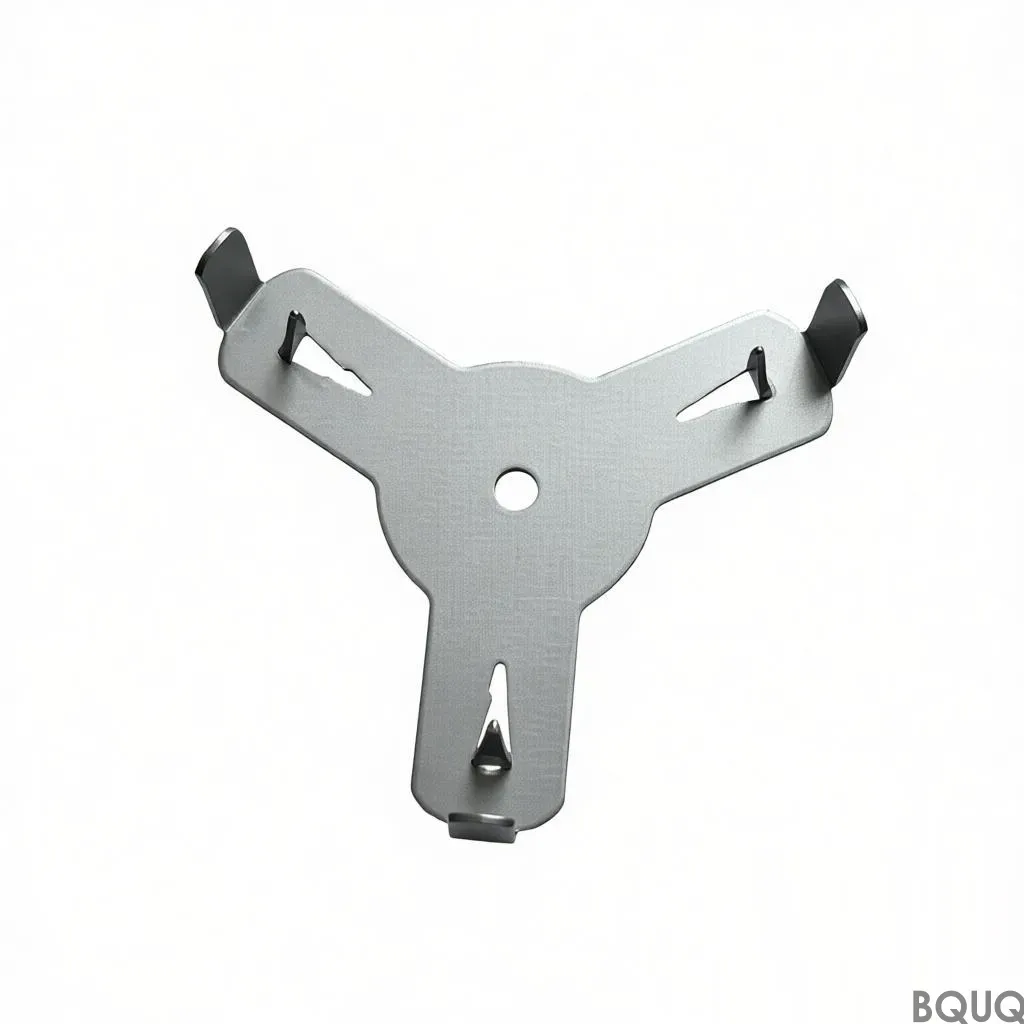
This is a collection of metal-stamped connectors built specifically for energy storage battery packs—busbar links, terminal lugs, cell-to-cell interconnect plates, and high-current contact tabs. Each
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
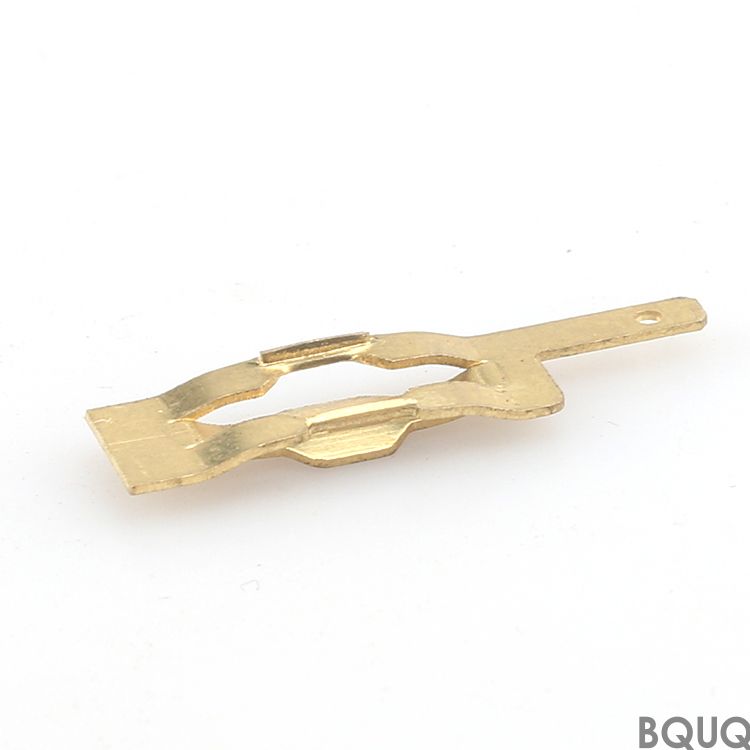
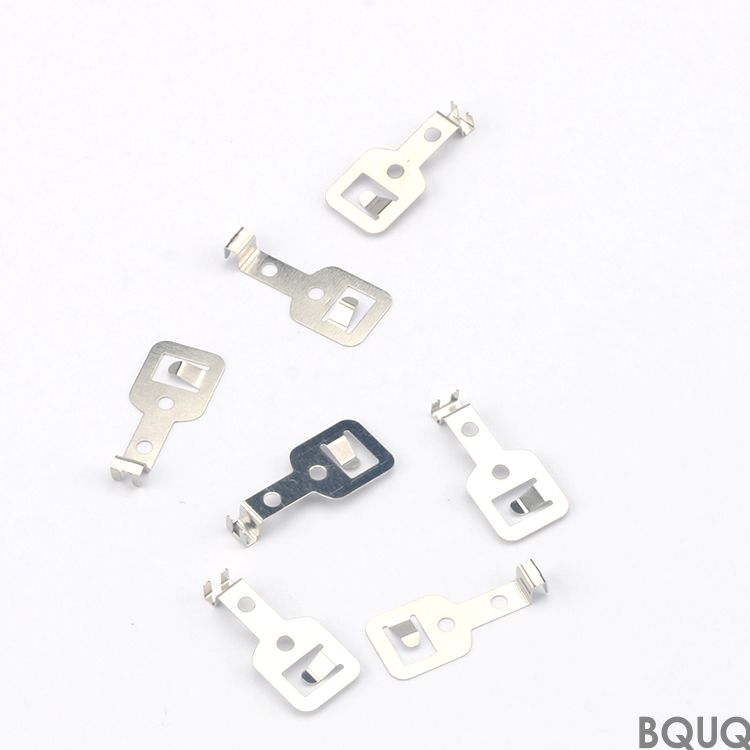
This is a collection of metal-stamped connectors built specifically for energy storage battery packs—busbar links, terminal lugs, cell-to-cell interconnect plates, and high-current contact tabs. Each part is stamped from certified copper or aluminum alloy, then plated and formed to a dimensional tolerance of ±0.01 mm, with a maximum burr of 0.05 mm and surface finish of Ra 0.8. This gives you repeatable low-contact resistance, consistent mating force, and a stamped part that drops into your assembly without secondary rework. We are a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining and stamping experience—and we ship most connector orders within 15 working days.
How Our Progressive Dies Control Contact Resistance and Flatness
Contact resistance in a battery connector is a function of surface area and pressure. Our progressive dies are built with a die clearance of 4–6% of material thickness, which produces a clean shear zone and minimizes the burnished area that causes hot spots. We hold flatness within 0.02 mm across the entire contact face, so when you bolt two stamped connectors together, the full surface carries current. Unlike a laser-cut or machined part, a stamped connector has a work-hardened edge that improves spring retention in tab-to-cell connections—this is critical for vibration-prone stationary storage racks.
Materials and Heat Treatment We Use for High-Cycle Flexing
We stock four primary alloys for this collection: C11000 copper (ETP), C5191 phosphor bronze, 6061-T6 aluminum, and 301 stainless steel. For connectors that must flex—like battery disconnect tabs—we use C5191 in a half-hard temper, achieving a hardness of 90–100 HRB, which gives you 40,000+ flex cycles without cracking. For high-current busbars, we use C11000 with a minimum conductivity of 101% IACS. If your design requires a spring element, we can selectively heat-treat the formed area to 380–420 HV using a localized induction process, leaving the rest of the part soft for forming. No secondary annealing is needed on our stampings; the grain structure is controlled at the coil stage.
Surface Finish and Plating Options for Corrosive Environments
Bare copper oxidizes fast in a battery room. We offer three standard plating options: tin plating (2–4 µm, matte finish), silver plating (3–5 µm, for high-cycle sliding contacts), and nickel plating (1–3 µm, for high-temperature areas near the cell vents). Each plating is applied after stamping, so there is no edge exposure—a common failure point when plating pre-cut sheet. We measure average surface roughness at Ra 0.8 on the contact face and Ra 1.6 on the body. If you need a lower Ra for a gasket seal, we can add a coining step that brings the surface down to Ra 0.2. Every lot is tested for salt spray resistance (24 hours minimum per ASTM B117).
Parameter
Specification / Range
Available Materials
C11000, C5191, 6061-T6, 301 Stainless
Material Thickness
0.1 mm – 3.0 mm
Hardness (as stamped)
90–100 HRB (bronze), 80–90 HRB (copper)
Dimensional Tolerance
±0.01 mm
Flatness
0.02 mm max over 100 mm length
Burr Height
0.05 mm max
Surface Finish Ra
0.8 µm standard, 0.2 µm with coining
Plating Thickness
Sn 2–4 µm, Ag 3–5 µm, Ni 1–3 µm
Max Current Rating (typical)
Up to 600 A per connector (based on cross-section)
Lead Time (standard)
15 working days
MOQ
No MOQ (1 piece for prototyping)
Burr Control and Deburring Process Before Plating
A burr on a stamped connector is not just a cosmetic defect—it creates a high-resistance point and can puncture heat-shrink insulation. Our dies are maintained with a cutting edge radius under 0.01 mm, and we run a two-step deburring process: a mechanical tumbling step (for parts under 50 mm) followed by an electrolytic polishing step that removes micro-burrs down to 0.01 mm. We measure burr height on every 5th part using a digital microscope with 100x magnification, and we record the results on the inspection report that ships with your box. If a burr exceeds 0.05 mm, the entire lot is rejected and re-run—we do not sort, we re-stamp.
Inspection Before Every Shipment—A 9-Point Check
Every order, regardless of quantity, goes through a 9-point inspection before we issue the packing list. We check: 1) outer dimensions with a CMM (accuracy ±0.002 mm), 2) flatness with a granite surface plate and feeler gauge, 3) burr height, 4) plating thickness with an X-ray fluorescence gauge, 5) hardness with a micro-Vickers tester, 6) contact resistance with a micro-ohmmeter (target under 0.5 mΩ for a 10 mm² cross-section), 7) salt spray test on a sample part, 8) visual inspection for scratches or die marks, and 9) packaging integrity for anti-static and moisture barrier. We also send you a digital copy of the inspection report within 24 hours of shipment. This is part of our standard service—no extra charge.
Tooling Maintenance and Die Life for Long-Run Consistency
If you are ordering in high volume, consistency matters more than the first sample. Our progressive dies for battery connectors are built with tungsten carbide inserts, and we run a preventive maintenance schedule: after every 50,000 strokes, we stop the press, measure the punch tip wear, and re-polish if the radius exceeds 0.02 mm. This keeps your part dimensions stable across a 500,000-piece run. We have seen die life exceed 2 million strokes on simple busbar shapes. For your first order, we can build a prototype die in 7 days using a wire-cut EDM, then transfer to a production die once the design is frozen. If you are still designing, we also offer soft tooling (aluminum dies) for 100–1,000 piece validation runs at a lower upfront cost.
Is there a minimum order quantity for the Energy Storage Battery Connectors Collection?
No MOQ—we accept a single prototype piece for testing, and we only ask that you cover the tooling or setup fee for small quantities.
Can you customize the connector shape or plating for our battery pack design?
Yes, we can modify any die or plating option; send us your 2D or 3D drawing and we will suggest material thickness and plating based on your current and temperature requirements.
How do you guarantee quality on a large production run?
We use in-line SPC monitoring on critical dimensions (flatness and hole position) and perform a full 9-point inspection on a sample from every 500-piece batch, not just the first article.
What is the lead time for a custom stamped connector?
Standard parts ship in 15 working days; custom dies add 7–10 days for prototyping, and production runs of 10,000+ pieces typically ship within 20 working days after your approval of the sample.
For a firm quote on the Energy Storage Battery Connectors Collection, send your drawing and quantity to sc@bquq.com or WhatsApp +86 13713157787. We reply with a firm quote within 12 hours—no vague estimates. If you are still choosing a material or plating, read our CNC cutting tool selection guide for edge quality tips, or check the CNC machining tolerances guide to compare stamped vs. machined tolerances. Precision manufacturing, made in China, with a 20-year track record—send your drawing today.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.