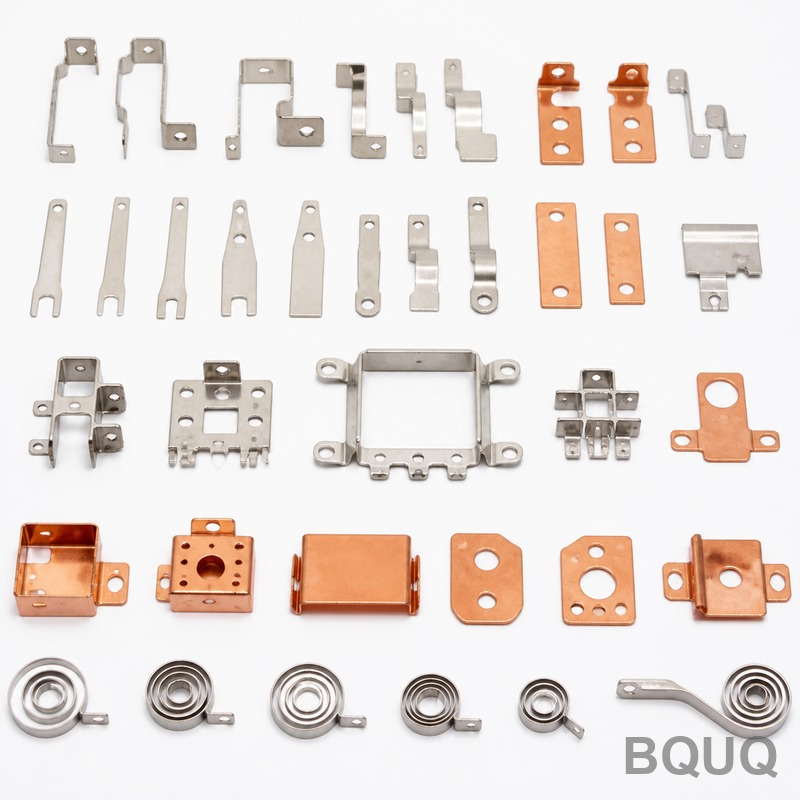
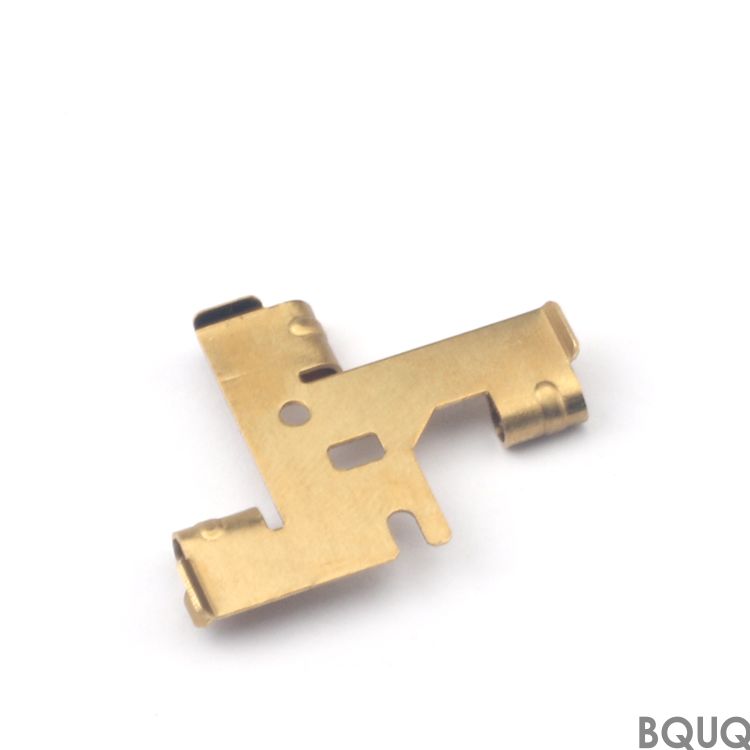
This is our EV High Voltage Contactor Parts Collection — a set of precision metal stampings for the internal current path, spring carriers, and arc chamber terminals of DC contact
EV High Voltage Contactor Parts Collection | Precision Stamping by BQUQ
This is our EV High Voltage Contactor Parts Collection — a set of precision metal stampings for the internal current path, spring carriers, and arc chamber terminals of DC contactors rated 100A to 60
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is our EV High Voltage Contactor Parts Collection — a set of precision metal stampings for the internal current path, spring carriers, and arc chamber terminals of DC contactors rated 100A to 600A. You get flatness within 0.03mm, burr height under 0.05mm, and a consistent hardness of 40–45 HRC on copper and steel parts, with a standard lead time of 10 working days after drawing approval.
Why the Current Path Needs Sub-0.05mm Burr Control
In a high voltage contactor, a burr on the stamped edge acts as a stress riser. At 750V DC and 300A continuous current, that tiny imperfection creates localized heating and can initiate micro-arcing. Our stamping dies are wire-cut to a clearance of 5% of material thickness, which holds burr height under 0.05mm across the entire EV High Voltage Contactor Parts Collection. You do not have to deburr manually before assembly.
Materials That Match Your Sealed Contactor Design
We stock three material families for this collection. First, C1100 copper and C17200 beryllium copper for the main contact bridges and flexible shunt connectors. Second, AISI 304 stainless steel for the moving spring seats and return spring guides. Third, cold-rolled steel (SPCC) with tin plating for the arc chamber terminals. Each material is certified with a mill test certificate, and we keep 2-ton coils of each in our Dongguan warehouse so your lead time does not wait on material procurement.
How We Hold Runout Under 0.02mm on Multi-Stage Forming
A contactor terminal has two or three bends in different planes. If the second bend shifts even 0.03mm, the contact gap becomes uneven, and the switching lifetime drops. We use a progressive die with 9 to 14 stations, and each station has a precision guide bushing with a clearance of 0.008mm. The result: hole-to-bend positional tolerance of ±0.02mm, and total runout on the assembled terminal face under 0.02mm across a 15mm width. This is verified on a CMM after every 500th part, not just at setup.
Heat Treatment and Surface Finishing for 10,000-Cycle Life
Beryllium copper parts are age-hardened at 315°C for 2 hours to reach 42–45 HRC. Stainless steel spring carriers are annealed to 35 HRC to avoid cracking under cyclic load. Copper parts get a silver plating of 4–6 microns to keep contact resistance below 0.5 milliohm. Steel parts receive a bright tin finish of 3–5 microns for corrosion resistance in high humidity. Every surface finish is tested with an XRF thickness gauge; we do not ship parts without a coating report.
Inspection Before Every Shipment: CMM and Pull-Test Data
We do not rely on in-process checks alone. Before packing your EV High Voltage Contactor Parts Collection, we run a final batch inspection: 10 parts from each production lot are measured on a Zeiss CMM for critical dimensions, a pull test verifies weld or crimp strength if you request sub-assemblies, and a roughness tester confirms Ra 0.8µm on sealing surfaces. You receive a PDF inspection report with the actual measured values, not a generic certificate of conformance.
Making Your Custom Contact Bridge Without a Minimum Order
Our stamping press line runs from 25 tons to 300 tons. For your custom bridge or terminal, we only need a 2D drawing or a 3D STEP file. Tooling design takes 3 days, tool build takes 7–10 days, and first articles are shipped within 24 hours of approval. There is no MOQ. You can order 50 pieces for a prototype batch or 100,000 pieces for production. The unit price drops predictably: tooling is amortized over the first 5,000 parts, so your cost per piece falls quickly.
Sealing and Plating Options for IP67-Rated Housings
Many of our clients use these parts inside a sealed contactor housing. For that, we offer a stamped dimple pattern on the terminal flat that locks into a molded rubber gasket. We also provide selective plating — silver on the contact area only, leaving the mounting hole unplated for a secure screw connection. This is done with a masking process that holds the plating boundary within ±0.2mm, so you do not get creep corrosion on the thread.
Before you finalize your drawing, check two of our engineering guides: the CNC cutting tool selection guide for choosing the right die material, and the CNC machining tolerances guide for understanding how bend radius and grain direction affect your final dimensions.
Silver 4–6µm, Tin 3–5µm, Selective plating available
Lead Time
10 working days (standard), 5 days (prototype)
MOQ
No MOQ
What is your minimum order quantity for a custom part?
No MOQ — we accept 50 pieces for a prototype run and scale from there, with tooling cost amortized over the first 5,000 units.
Can you match my existing contactor part dimensions exactly?
Yes, send your drawing or a physical sample, and we will reverse-engineer the dimensions to ±0.01mm and quote within 12 hours.
How do you control quality for high-voltage contactor parts?
We use a 9–14 station progressive die with 0.008mm guide bushing clearance, plus CMM inspection on every 500th part and a final 10-piece lot check with a PDF report.
What is the typical lead time for a first article?
Tooling build is 7–10 days, first articles ship within 24 hours after your approval, and production orders ship in 10 working days from drawing sign-off.
Get a firm quote within 12 hours. Email your drawing to sc@bquq.com or send it via WhatsApp to +86 13713157787. We are a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining and stamping experience. Send your drawing — we will reply with a price and DFM feedback today.