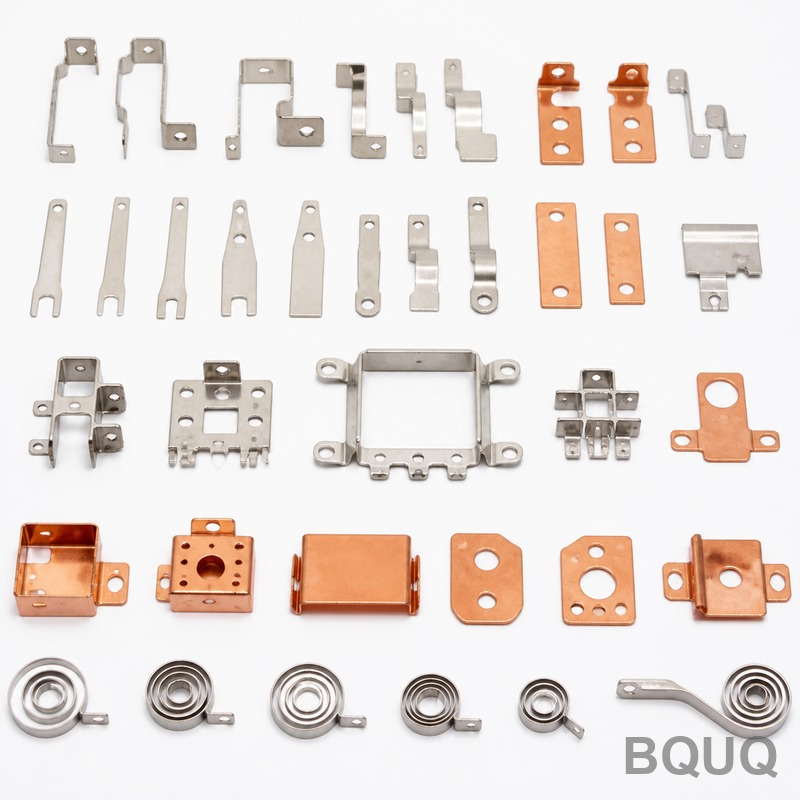
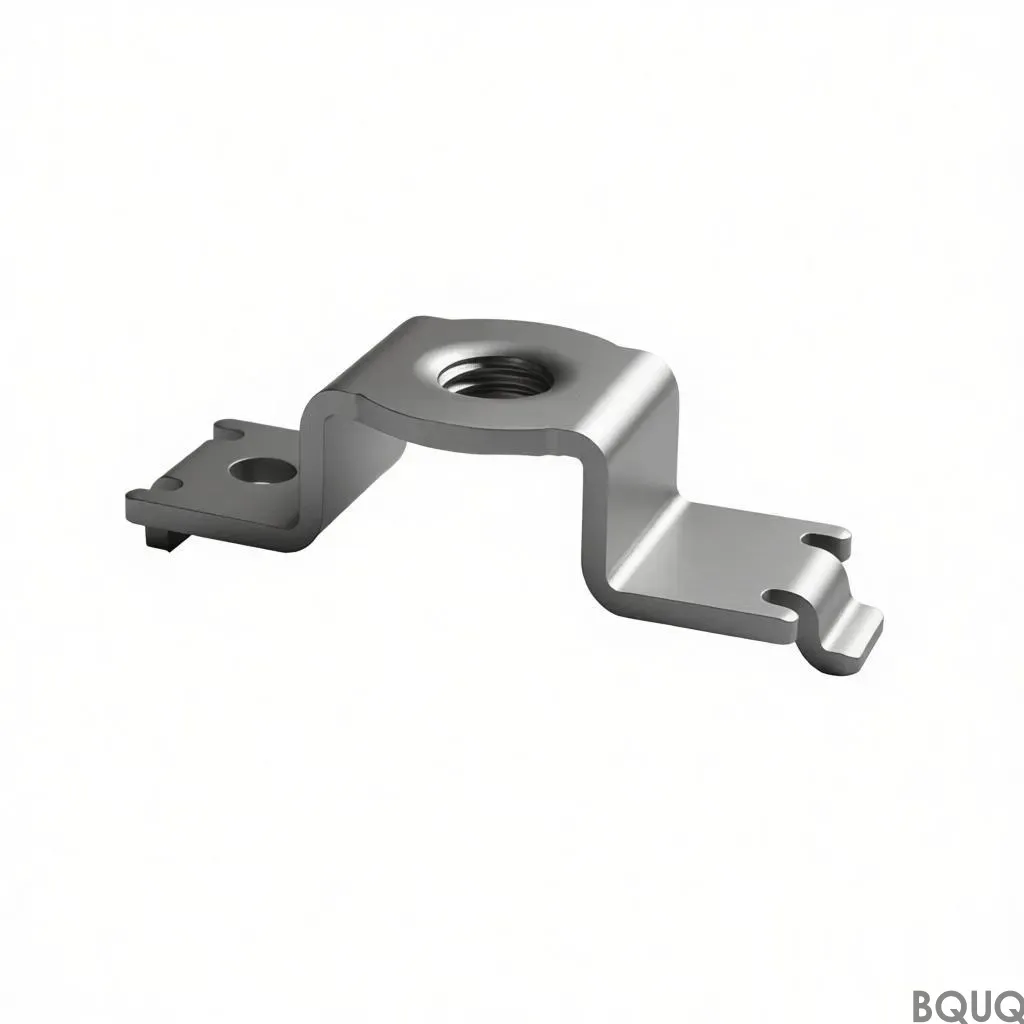
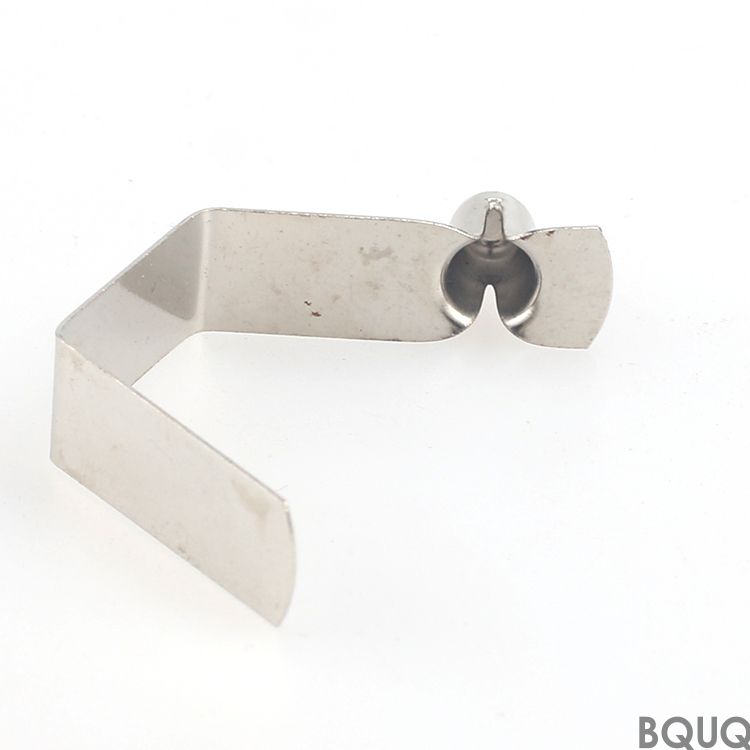
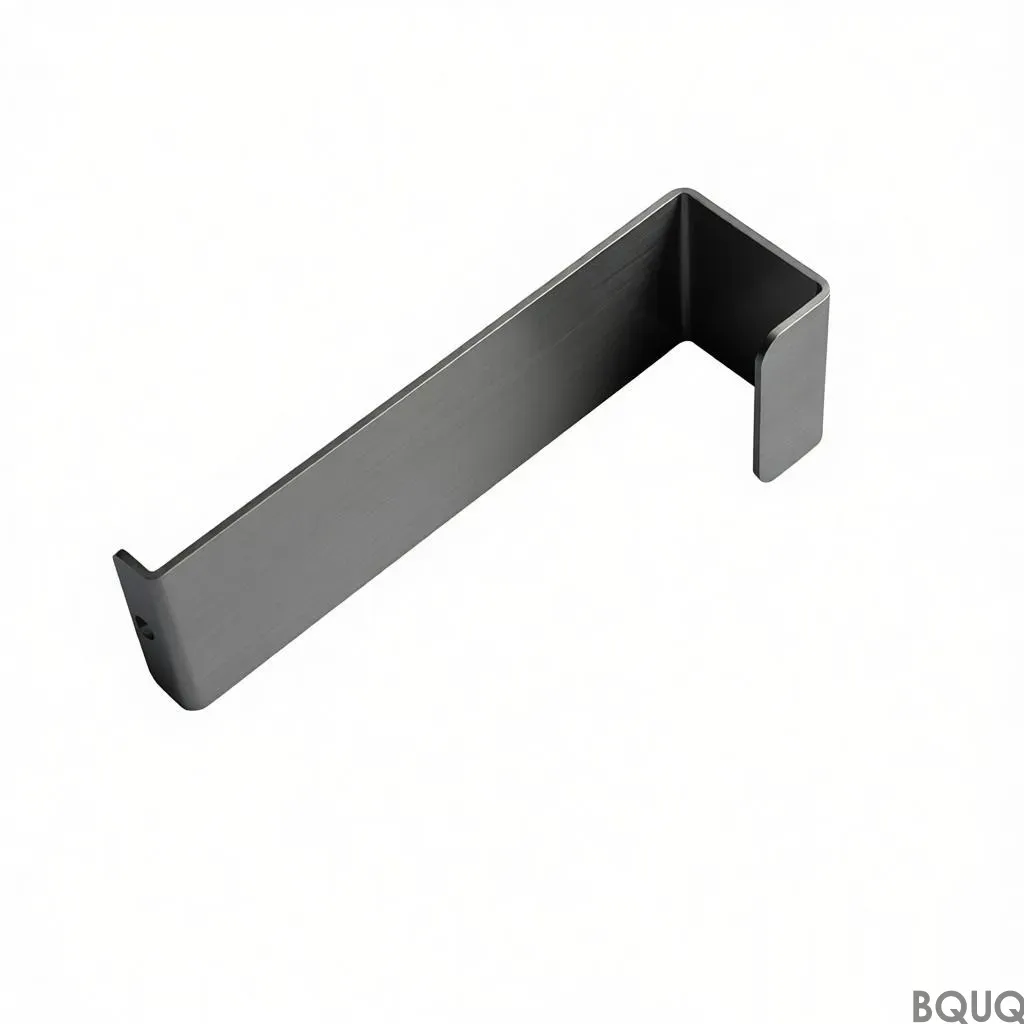
Stamping bracelet holder is a single-stroke SUS304 1.0 mm part with hot-dip galvanize 60 µm as standard. At ΔT = 60 K, tooling runs with repeatability, and hole position carries across the batch. Low fin gauge at pitch gives more surface per cubic millimetre, so medical enclosure volume programs stay repeatable without sacrificing fin density.
Stamping bracelet holder is a single-stroke SUS304 1.0 mm part with hot-dip galvanize 60 µm as standard. At ΔT = 60 K, tooling runs with repeatability, and hole position carries across the batch. Low fin gauge at pitch gives more surface per cubic millimetre, so medical enclosure volume programs stay repeatable without sacrificing fin density.
Running at , this stamping bracelet holder is pressed on tooling with repeatability. SUS304 1.0 mm gives at ΔT = 60 K, and hot-dip galvanize 60 µm is applied as standard.
Design Approach and Process
A single stroke forms the whole stamping bracelet holder, so part cost stops scaling with complexity. Tooling runs , and the cycle feeds a line.
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
One supplier now covers to fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor.
Pressing SUS304 1.0 mm keeps the stamping bracelet holder light, from depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
Every stroke is dimensionally identical, so hole position carries across the batch. That is what makes medical enclosure volume programs repeatable.
The standard material is SUS304 1.0 mm, supplied with hot-dip galvanize 60 µm. For applications where medical enclosure exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Lot traceability runs from coil to carton: heat number, press stroke range and inspection record stay attached, so a field issue can be tied back to a specific run.
Final containment is . Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
medical enclosure packaging and vibration rules push toward one-piece construction. A stamped stamping bracelet holder has no adhesive to creep, which is the usual failure mode in two-part coolers.
Designers working on medical enclosure ask for flatness before they ask for thermal data, because medical enclosure assembly is automated and a non-flat base stops the line.
medical enclosure designs often run a 2.0 m/s forced-air path. at means medical enclosure can hold its target with fan power below the acoustic limit.
For medical enclosure prototypes, covers drawing review and first article. Production lots move to 25 working days once the capability is signed off.
Specifications
Parameter
Value / Range
Material
SUS304 1.0 mm
Surface finish
hot-dip galvanize 60 µm
MOQ (prototype)
100 pcs
MOQ (production)
5000 pcs
Lead time (production)
25 working days
Tooling lead time
30 working days
FAQ: Your Questions Before Ordering
How does this compare to an extruded stamping bracelet holder?
Extrusion is cheaper above roughly 500,000 pieces per year and gives a smoother profile. Stamping wins below that and wherever fin gauge drops below 0.5 mm, because extrusion cannot hold consistently. For medical enclosure prototypes, tooling cost usually decides it.
We test at and report . That is a steady-state figure, not a transient: for medical enclosure first-power-on behaviour you need a different test, and we can run it on request.
Do you make the stamping bracelet holder in different sizes?
The family covers , with unit weights from . Because the base is pressed, new sizes are a die insert change rather than a new press line, so development is usually 2 weeks rather than 8.
The key is avoiding a second metal at the wet contact area. We recommend hot-dip galvanize 60 µm and, where the part touches an aluminium chassis, an isolating washer. Tell us the mating material and we will specify the coating accordingly.
Can you help with thermal simulation before sampling?
Yes. Send your enclosure airflow, inlet temperature and the heat load to be dissipated, and we will run a steady-state model and return a suggested and combination. That usually saves one tooling iteration.
How We Manufacture and Ship
The factory holds ISO9001 and can ship RoHS and REACH documentation with the . Third-party SGS inspection is arranged on request before the container is sealed.
Production runs on cycles with in-line vision on . That is what keeps a commitment credible in peak season.
Hole position carries across batch; fin gauge and pitch per tooling
Lead time
Not stated in excerpt; tooling change rather than new vendor for thermal redesign
MOQ
Not stated in excerpt; volume programs supported
Capacity
Single-stroke press line; one supplier covers fin gauges from same press family
Selection / comparison
Option
Best for
Trade-off
SUS304 1.0 mm + hot-dip galvanize 60 µm
Standard stamping bracelet holder
Standard corrosion protection; not passivated route
Passivated route
Medical enclosure exposure concern
Alternative finish route; may differ from standard galvanize
Low fin gauge at pitch
More surface per cubic millimetre
Requires tooling change for thermal redesign
Single-stroke stamping
Part cost stops scaling with complexity
Dimensional identity depends on tooling repeatability
Same press family fin gauges
Thermal redesign as tooling change
Avoids new vendor but still requires tooling change
Process / inspection
Stage
Control
Record
Pressing
Single stroke forms whole stamping bracelet holder
Every stroke dimensionally identical
Tooling
Tooling runs with repeatability
Hole position carries across the batch
Material
SUS304 1.0 mm
Standard material specification
Surface finish
Hot-dip galvanize 60 µm standard
Passivated route for medical enclosure exposure
Inspection
Inspection before every shipment
Batch repeatability for medical enclosure volume programs
Frequently Asked Questions
What material is the stamping bracelet holder made from?
The standard material is SUS304 1.0 mm. It is supplied with hot-dip galvanize 60 µm as standard. For medical enclosure exposure concerns, we recommend the passivated route. Pressing SUS304 1.0 mm keeps the part light while maintaining fin density where airflow path length is fixed.
A single stroke forms the whole stamping bracelet holder on tooling that runs with repeatability. The cycle feeds a line, and every stroke is dimensionally identical, so hole position carries across the batch. Low fin gauge at pitch gives more surface per cubic millimetre than machined or extruded profiles.
What tolerance can I expect on hole position?
Every stroke is dimensionally identical, so hole position carries across the batch. This repeatability is what makes medical enclosure volume programs repeatable. Tolerance classes you can specify are covered under the Tolerance Classes You Can Specify section. Exact numerical tolerance values are not stated in the excerpt.
What surface finish options are available?
Hot-dip galvanize 60 µm is applied as standard. For applications where medical enclosure exposure is a concern, we recommend the passivated route. The standard material is SUS304 1.0 mm. Surface finish selection depends on corrosion exposure and whether the part is used in a medical enclosure.
Can the stamping bracelet holder be redesigned for different thermal performance?
Yes. One supplier now covers fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor. Low fin gauge at pitch gives more surface per cubic millimetre than a machined or extruded profile of the same envelope. This supports airflow path length fixed by the enclosure.
Where is this stamping bracelet holder used?
It is used where airflow path length is already fixed by the enclosure, and in medical enclosure volume programs. The repeatable hole position across the batch makes it suitable for those volume programs. The Where This Part Is Used section covers additional applications. Fin density matters where the envelope is constrained.
How is the stamping bracelet holder inspected before shipment?
Inspection before every shipment is a standard step. Every stroke is dimensionally identical, so hole position carries across the batch. This supports repeatability for medical enclosure volume programs. The Inspection Before Every Shipment section covers the specific checks. Records are kept per the process inspection table.
Key Specifications and Selection Guide
Spec comparison
Parameter
Value / Range
Material
SUS304 1.0 mm
Tolerance
Hole position carries across batch; repeatability at ΔT = 60 K
Lead time
Not specified in excerpt
MOQ
Not specified in excerpt
Capacity
Single-stroke press; one supplier covers fin gauges from same press family
Selection / comparison
Option
Best for
Trade-off
Stamping bracelet holder
Medical enclosure volume programs needing repeatable fin density
Requires tooling change for thermal redesign
Machined profile
Complex geometries outside stamping envelope
Lower surface per cubic millimetre at same envelope
Extruded profile
Continuous lengths with uniform cross-section
Lower fin density than stamped low fin gauge at pitch
SUS304 1.0 mm
Lightweight parts with fixed airflow path length
Material thickness fixed by envelope
Hot-dip galvanize 60 µm
Standard corrosion protection
Adds thickness; not for tight tolerance interfaces
Frequently Asked Questions
What material and thickness is the stamping bracelet holder made from?
The stamping bracelet holder is made from SUS304 stainless steel at 1.0 mm thickness. This material provides corrosion resistance and formability for single-stroke pressing. Hot-dip galvanize 60 µm is applied as standard for additional protection.
What is the standard surface finish for this stamped part?
Hot-dip galvanize 60 µm is the standard surface finish. This coating provides corrosion resistance for medical and industrial enclosure applications. It is applied after stamping and before final inspection.
How does stamping compare to machining for fin density?
Stamping wins at low fin gauge: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope. This means better thermal performance in a fixed volume, which matters for medical enclosure volume programs.
Can I change the fin gauge without switching suppliers?
Yes. One supplier now covers fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor. This reduces lead time and keeps quality consistent across iterations.
What is the tooling repeatability at ΔT = 60 K?
At ΔT = 60 K, tooling runs with repeatability, and hole position carries across the batch. This ensures consistent part-to-part performance for assembly and thermal contact.
Is the stamping bracelet holder suitable for medical enclosures?
Yes. Low fin gauge at pitch gives more surface per cubic millimetre, so medical enclosure volume programs stay repeatable without sacrificing fin density. The SUS304 1.0 mm construction keeps weight low while maintaining fin density.
What inspection is performed before shipment?
Inspection before every shipment includes verification of hole position, coating thickness for hot-dip galvanize 60 µm, and overall dimensions. Records are kept for traceability. This ensures batch-to-batch consistency.