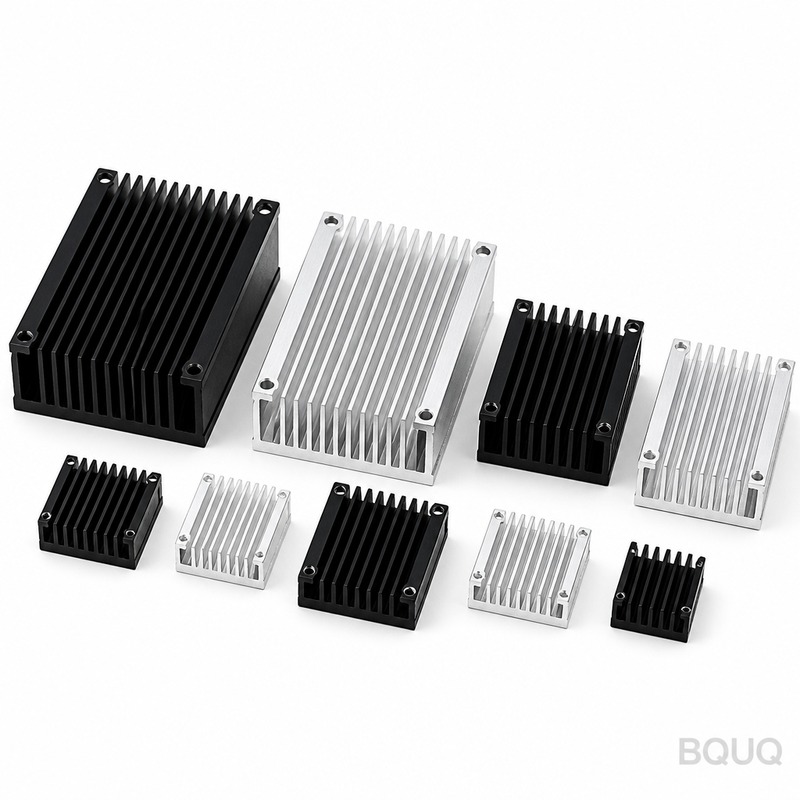
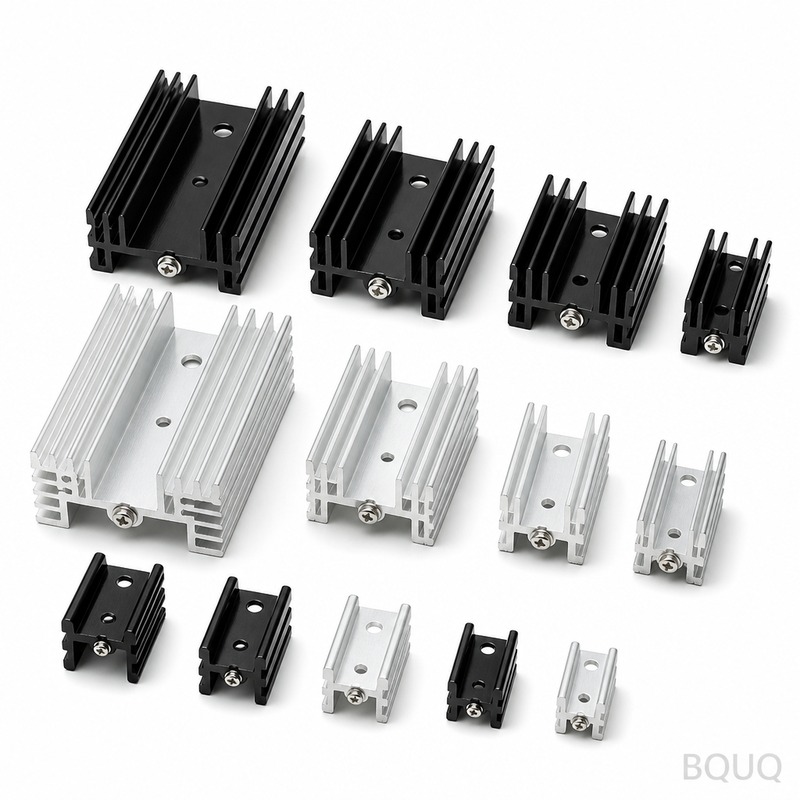
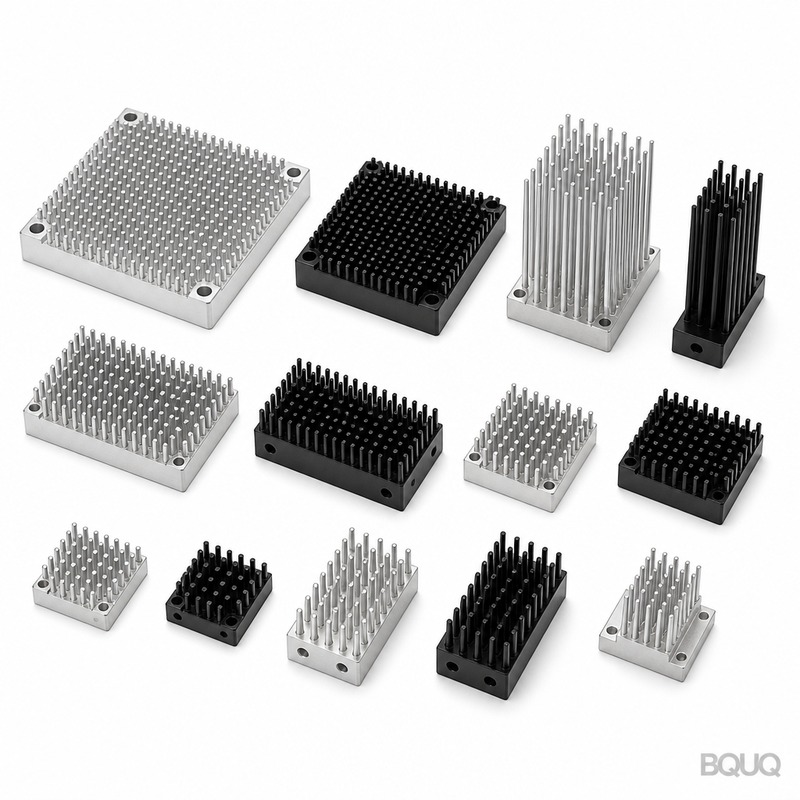
This is a CNC-machined aluminum Heatsink With Fan Mounting Holes, built for active cooling assemblies where a standard fan must bolt directly to the fin stack. We hold hole-to-ho
BQUQ Heatsink With Fan Mounting Holes | Precision CNC Made in China
This is a CNC-machined aluminum Heatsink With Fan Mounting Holes, built for active cooling assemblies where a standard fan must bolt directly to the fin stack. We hold hole-to-hole tolerance at ±0.0
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC-machined aluminum Heatsink With Fan Mounting Holes, built for active cooling assemblies where a standard fan must bolt directly to the fin stack. We hold hole-to-hole tolerance at ±0.01 mm and thread depth within ±0.05 mm, so your fan mounts flush every time—no shims, no rework. Typical lead time is 10 working days for custom drawings, and we run 6061-T6 with a surface hardness of 45 HRC after hard anodizing.
Why Fan Holes Must Be Machined, Not Punched
Punched or extruded fan holes leave burrs and oval shapes that strip screws or shift the fan axis. We machine every mounting hole with a 4-axis CNC mill, not a punch press. This gives true position of the hole pattern within 0.02 mm relative to the base plate. For a 40 mm fan, that means the impeller clears the shroud by a consistent 1.5 mm gap on all sides. You get lower acoustic noise and zero vibration from an off-center mount.
Fin Geometry That Actually Moves Air
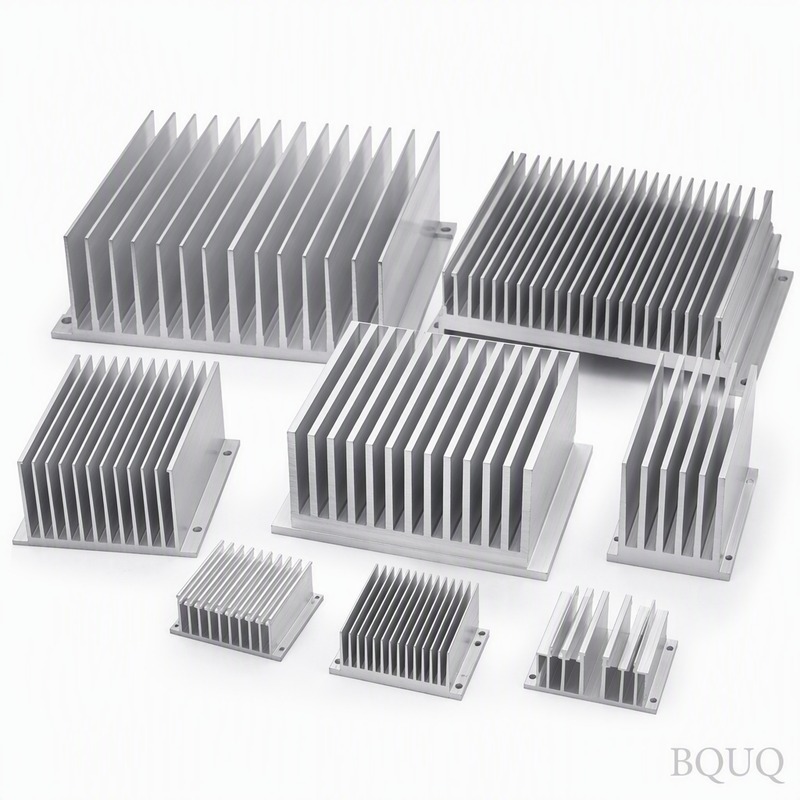
Flat fins with rough edges kill airflow. Our standard fin pitch is 2.5 mm with a 1.2 mm fin thickness, machined from solid 6061-T6 billet. The fin tip runout is held to 0.05 mm across the entire length. We also offer a skived fin option (up to 0.8 mm pitch) for high-density LED or IGBT cooling where you need maximum surface area in a 25 mm height. Every fin edge is deburred to a 0.2 mm radius—no sharp corners that cut wire insulation or fingers.
Materials and Heat Treatment We Use
We stock three alloys, all with mill certificates: 6061-T6 (yield 276 MPa, thermal conductivity 167 W/mK) for general use, 6063-T5 (conductivity 209 W/mK) for lightweight enclosures, and C1100 copper (conductivity 391 W/mK) for high-end laser or RF modules. After machining, we can hard anodize to 25–45 HRC with a 50 µm coating—this resists corrosion in marine or chemical plant environments. For pure thermal performance without coating, we ship a clear chromate finish (MIL-DTL-5541) that adds no thermal resistance.
How We Control Flatness and Torque Retention
If the base plate warps, your thermal paste gap widens and the IGBT overheats. We stress-relieve all raw material before cutting (heat soak at 350°C for 2 hours, then air cool). After machining, we verify base flatness on a granite plate with a 5 µm dial indicator—acceptance limit is 0.03 mm over a 100 x 100 mm area. For the fan holes, we tap threads to a depth of 6 full turns (M3 or #6-32) and test with a hardened steel screw at 0.35 Nm torque. No stripped threads, no cross-threading on your assembly line.
Inspection Before Every Shipment
Every Heatsink With Fan Mounting Holes goes through a 3-step check. First, a CMM (coordinate measuring machine) verifies hole positions and thread pitch. Second, a surface profilometer measures Ra on the base—we hold 0.8 µm Ra as standard, 0.4 µm for thermal interface surfaces. Third, we do a dry-fit with a standard 40 mm or 60 mm fan on a sample from each batch. If the fan doesn't seat flat, the batch is rejected. You get a PDF inspection report with each shipment, including actual CMM data points.
Custom Patterns for Non-Standard Fans and Screws
Standard fans use 32 mm, 40 mm, 50 mm, or 60 mm hole spacing. But we regularly machine odd patterns: 43 mm diagonal, offset rectangles for blower fans, or counterbored holes for flat-head screws. Tell us the fan model number—we will pull the datasheet and match the hole pattern exactly. We also offer threaded inserts (brass or stainless) for plastic housings where you need repeated screw removal. No MOQ applies to custom patterns; one prototype is fine.
Lead Time and Packing for Global Shipping
Prototype (1–5 pieces) ships in 7 working days. Production (50–500 pieces) ships in 12–15 working days. We pack in anti-static foam trays with individual slots for each heat sink—no surface scratches, no bent fins. For orders over 100 pieces, we use wooden crates with corner protection to avoid pallet damage. Sea freight from our Dongguan factory to Los Angeles takes 18 days; air freight takes 4 days. All export paperwork (commercial invoice, packing list, CO) is included.
Parameter
Specification
Material
6061-T6, 6063-T5, C1100 copper
Base thickness
3.0 mm to 25 mm (custom)
Fin height
5 mm to 80 mm
Fin pitch
1.2 mm (skived) to 4.0 mm (machined)
Surface hardness
45 HRC (hard anodized) or 95 HRB (bare)
Hole position tolerance
±0.02 mm true position
Thread depth tolerance
±0.05 mm
Base flatness
0.03 mm / 100 mm
Surface finish (base)
Ra 0.8 µm (standard), Ra 0.4 µm (thermal)
Lead time
7 days (prototype), 12–15 days (production)
MOQ
No MOQ—one piece accepted
What is the MOQ for a custom Heatsink With Fan Mounting Holes?
No MOQ—we accept one prototype piece for testing, and production pricing only kicks in at 100+ units.
Can you match an existing fan's hole pattern from a datasheet?
Yes, send the fan model or drawing; we will machine the exact hole spacing, thread size, and counterbore depth to match.
How do you ensure the fan holes don't strip during assembly?
We tap to full thread depth and torque-test each batch with a steel screw at 0.35 Nm, plus we offer brass inserts for repeated removal.
What is your typical lead time and shipping method?
Prototypes ship in 7 working days, production in 12–15; we use DHL/FedEx air for small orders and sea freight for bulk—both with full tracking.
For fan-hole geometry, always reference the CNC cutting tool selection guide to understand how tool diameter affects hole edge quality. And before finalizing your base plate thickness, check the CNC machining tolerances guide—it explains why we hold ±0.01 mm instead of the looser ±0.1 mm standard.
Send your fan drawing or step file. We will reply with a firm quote within 12 hours—including a DFM comment on hole size and thread engagement. Email sc@bquq.com or WhatsApp +86 13713157787. Same-day feedback on manufacturability, no MOQ, precision manufacturing made in China.