Decorative Craft Springs Collection 02 | Custom Precision by BQUQ
What This Collection Ships With: Exact Numbers, Not Promises Decorative Craft Springs Collection 02 is a series of custom-formed springs engineered for visible, tactile applications — think luxury pac
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Collection Ships With: Exact Numbers, Not Promises
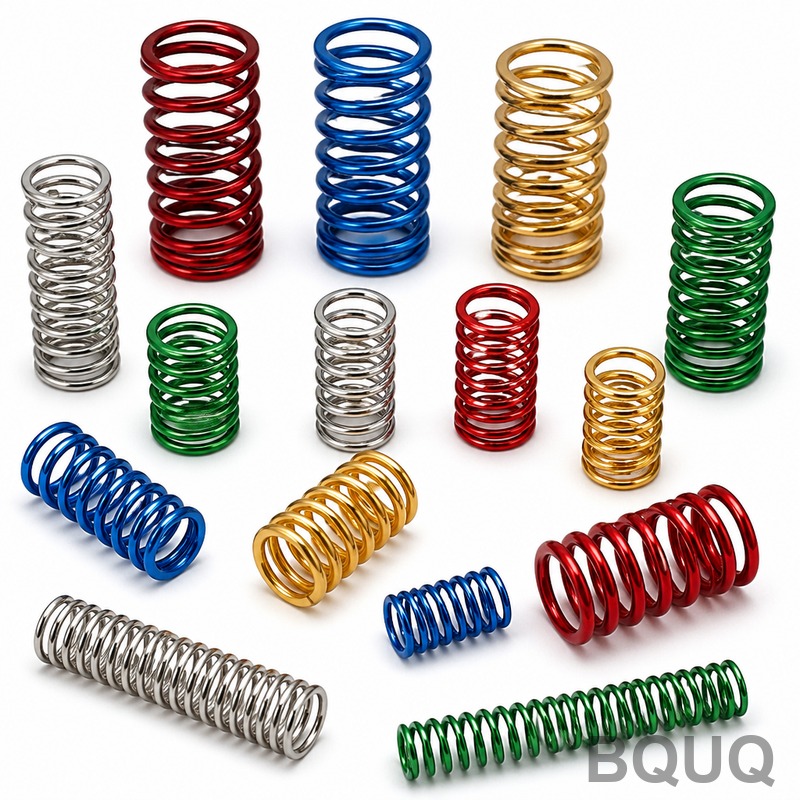
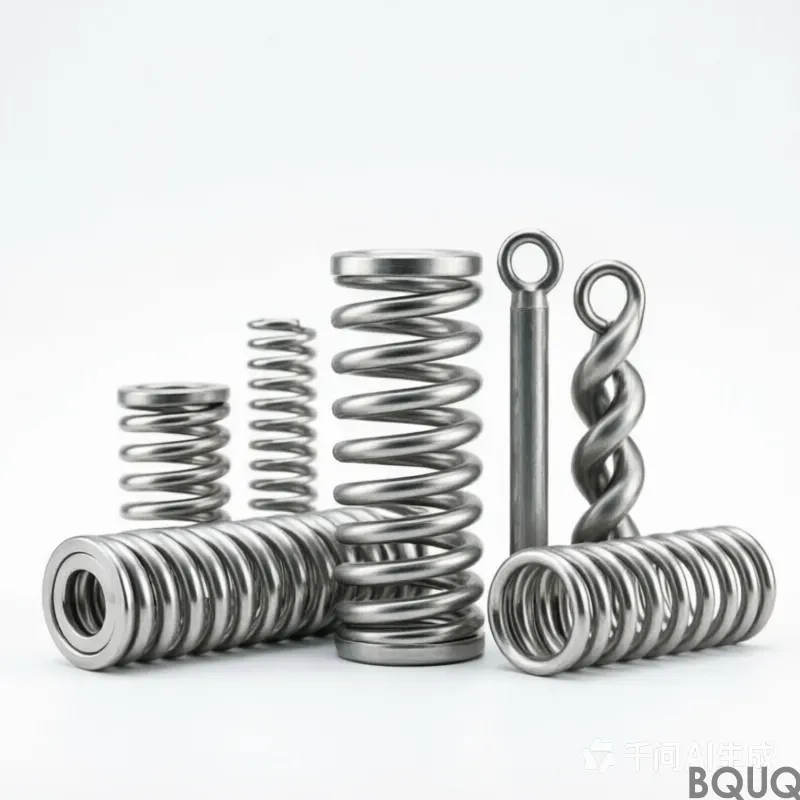
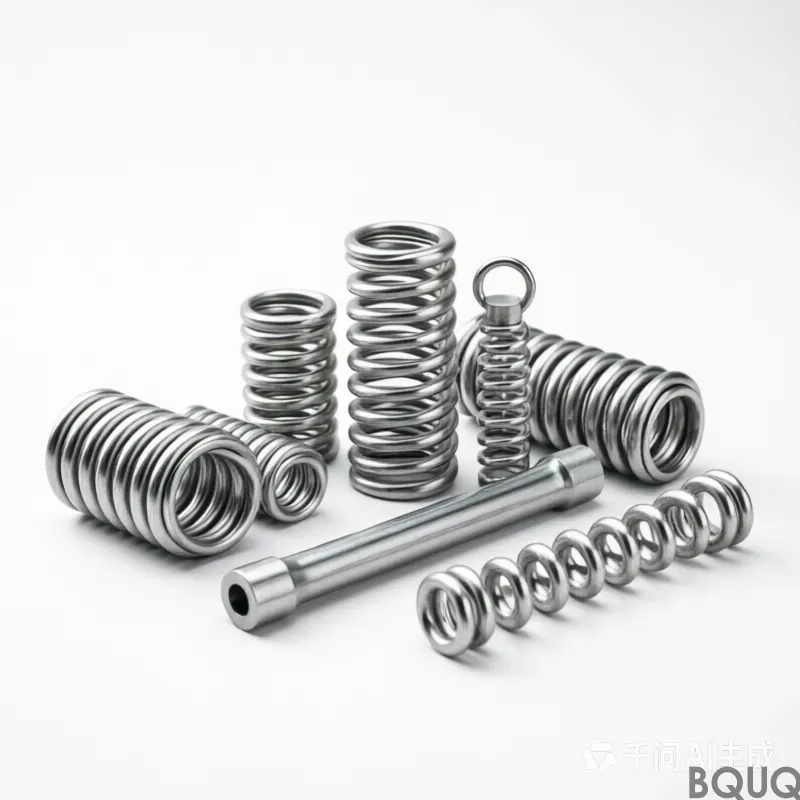
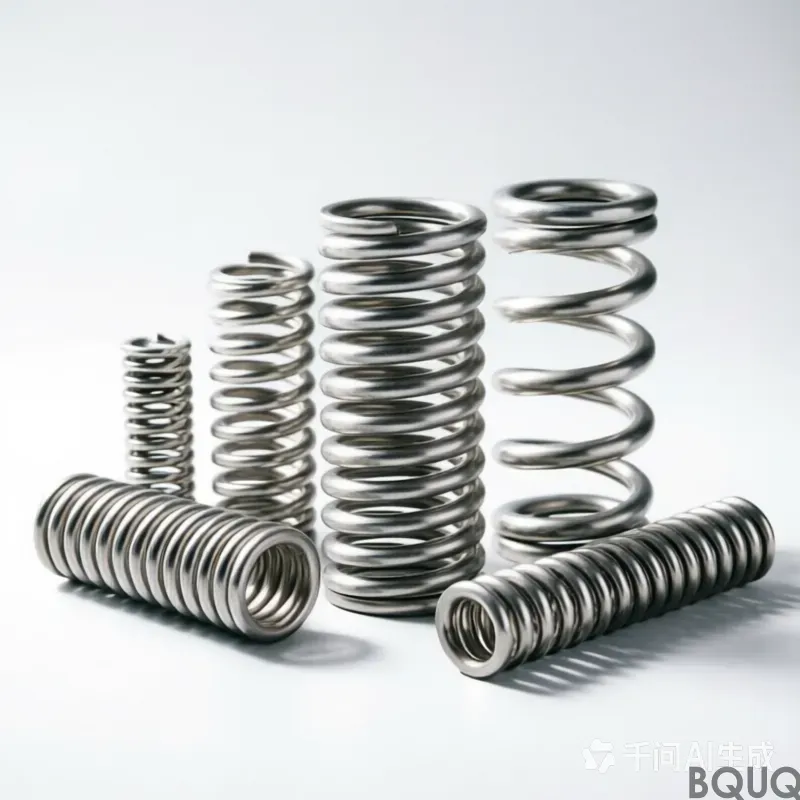
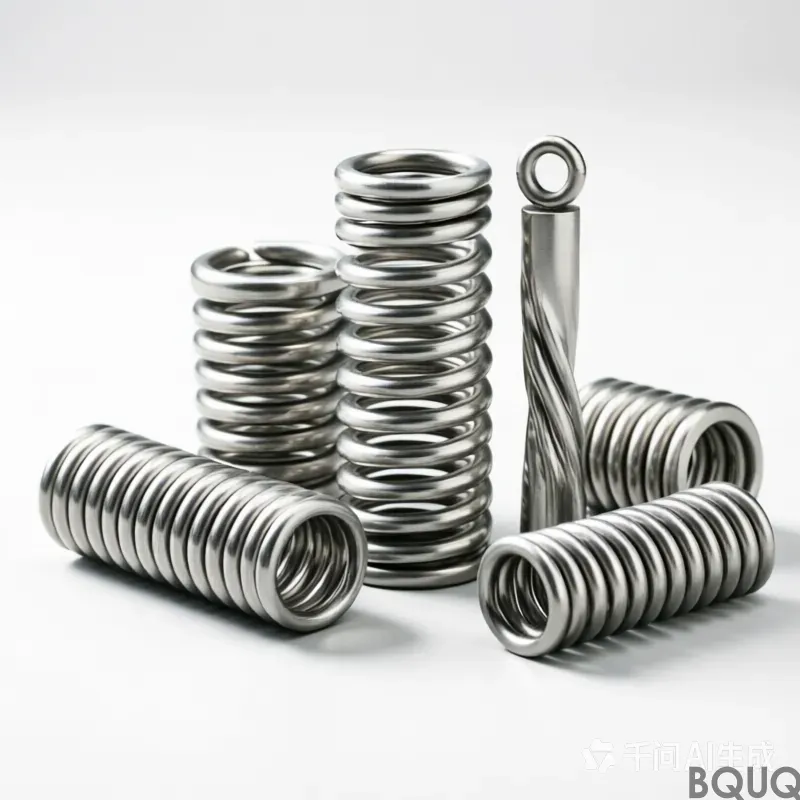
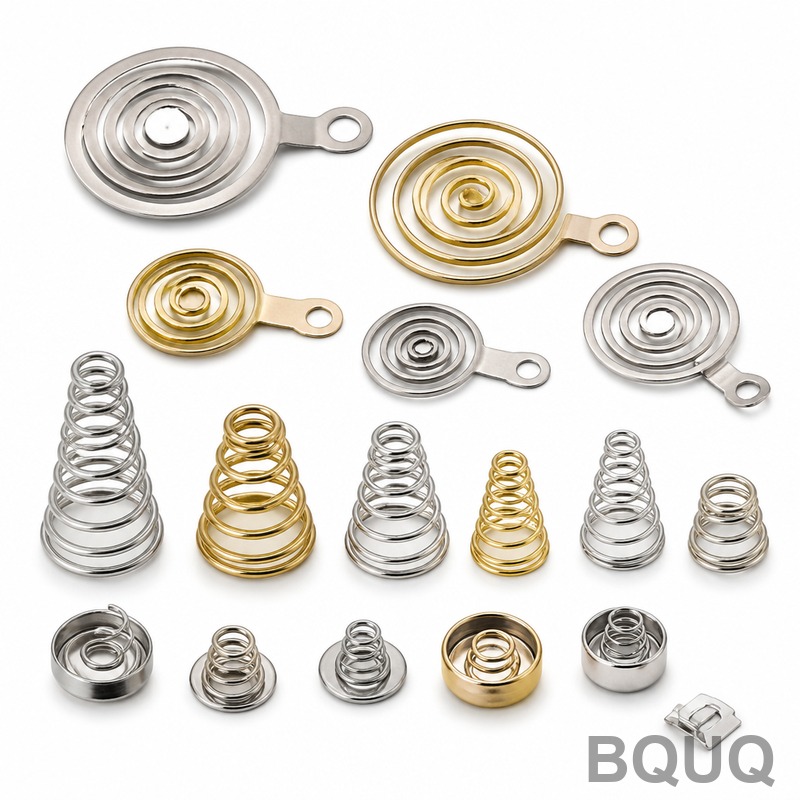
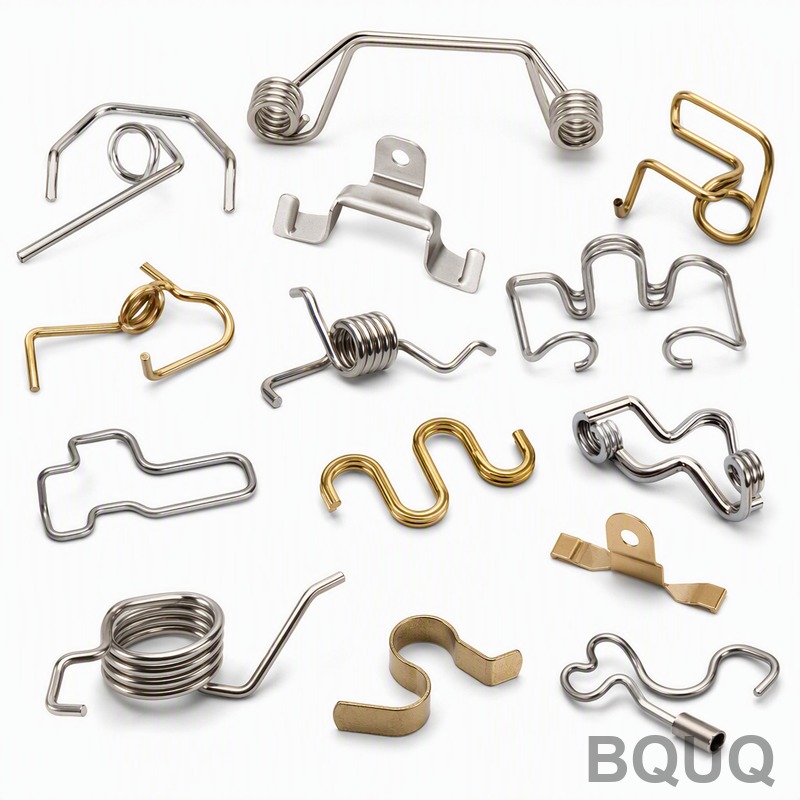
Decorative Craft Springs Collection 02 is a series of custom-formed springs engineered for visible, tactile applications — think luxury packaging hinges, jewelry clasps, cosmetic compact closures, and architectural model mechanisms. Every spring in this collection is made in China at our Dongguan factory, with 20 years of CNC machining and stamping precision behind it. You get wire diameter accuracy of ±0.02mm, coil pitch tolerance of ±0.05mm, and surface finish of Ra0.4 or better. Hardness is held at 48-52 HRC for most alloys, with a standard lead time of 7 days for prototypes and 15 days for production runs.
No MOQ applies to any item in this collection. If you need 5 pieces for a hand-built sample or 50,000 for a production line, the same tolerance and inspection protocol applies. This is not a catalog of stock parts — every spring is wound, heat-treated, and finished to your exact drawing.
Why Decorative Springs Demand Tighter Runout Than Functional Springs
A functional spring can tolerate 0.1mm runout because it is hidden inside a mechanism. A decorative spring is seen, touched, and often plated. Runout — the deviation from a perfect circular path when the spring rotates — shows up as a wavy gap between coils or an uneven gap at the spring ends. In Decorative Craft Springs Collection 02, we hold total runout to ≤0.05mm on outer diameter and ≤0.03mm on end closure. This is achieved by using CNC coiling machines with servo-controlled wire feed, not conventional cam-driven winders. The result is a spring that looks machined from a solid piece, not wound from wire.
For comparison, our standard industrial springs run at 0.1mm runout. This collection halves that number because the visual gap between coils is the first thing an inspector checks. If you are plating or PVD-coating these springs, runout below 0.05mm also ensures uniform coating thickness — no thin spots on one side, no buildup on the other.
Materials and Heat Treatment We Use for This Collection
Decorative Craft Springs Collection 02 is not limited to music wire. We offer five material families, each with a specific visual and mechanical profile:
Closed and ground, closed not ground, or open per drawing
Lead time
7 days prototype, 15 days production
MOQ
No MOQ — 1 piece accepted
Heat treatment is controlled in-house. We use vacuum furnaces for stainless grades to prevent surface oxidation — critical for decorative parts where a dull grey oxide layer would ruin the finish. Music wire and 17-7PH are tempered in a continuous belt furnace with nitrogen atmosphere. After heat treatment, every spring goes through a double-pass barrel polishing with ceramic media, then a vibratory finishing step with walnut shell for a matte-to-semi-bright surface. If you need mirror polish, we add a third step with stainless steel shot.
How We Eliminate Coil Interference in Tight-Pitch Decorative Springs
Decorative springs often have tight pitch — coils nearly touching — to create a dense, metallic look. The problem is that during compression, coils can rub, causing scratching and a squeaking sound. In Decorative Craft Springs Collection 02, we apply a dry film lubricant (molybdenum disulfide or PTFE) before heat treatment, not after. This bakes the lubricant into the metal surface, reducing friction coefficient to 0.08 versus 0.15 for untreated steel. This means no audible squeak, no visible scratch marks on the coil flanks, and a longer cycle life — up to 100,000 compressions at 80% of maximum deflection without visible wear.
For springs that will be plated (gold, nickel, black oxide), we use a different approach. The plating process itself can cause hydrogen embrittlement, which makes the spring brittle. We counter this by baking the plated springs at 190°C for 4 hours immediately after plating. This is a standard step in aerospace, but most decorative spring shops skip it. We do not. Every plated spring in this collection passes a 24-hour load relaxation test — we compress it to 50% of its free length, hold it for 24 hours, and measure the load loss. Acceptable loss is under 2%. If it exceeds that, the batch is rejected and re-heat-treated.
Inspection Before Every Shipment: 100% Dimensional + Visual
No sampling. Every spring in Decorative Craft Springs Collection 02 is individually inspected. We use an optical comparator for OD, free length, and coil count — three measurements per spring. For runout, we place each spring on a precision mandrel and rotate it 360 degrees under a dial indicator. The maximum deviation is recorded. For surface finish, we use a profilometer on three random coils of each spring — reading must be ≤0.4μm Ra. Visual inspection is done under a 5x magnifying lamp by two separate operators. They check for scratches, pits, discoloration, and edge burrs on the cut ends.
Each spring is then packaged in an anti-static foam insert inside a rigid box. No loose springs rattling in a poly bag — that causes micro-scratches in transit. For plated springs, we add a layer of anti-tarnish paper. Every box includes a certificate of conformance with actual measured values, not just "within spec". This certificate lists the wire lot number, heat treatment batch, and the exact runout and hardness measurements for your reference.
Why This Collection Uses CNC Coiling, Not Traditional Spring Winders
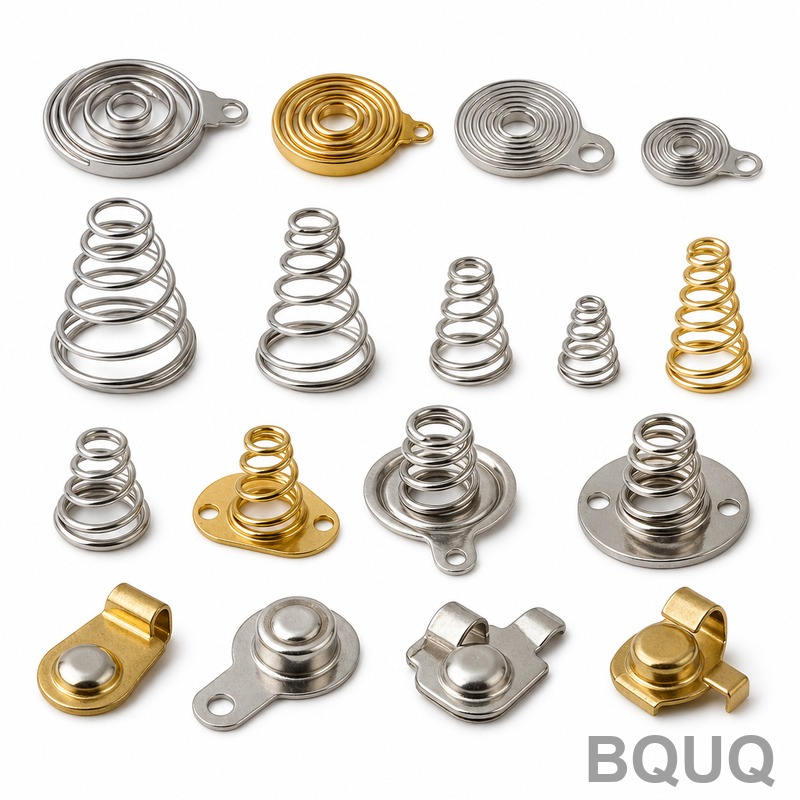
Traditional spring winders use a fixed mandrel and a tool that pushes the wire. This is fast but limited in shape — you cannot make variable pitch, conical, or torsion springs with tight end geometry. Decorative Craft Springs Collection 02 uses CNC coiling machines with 6-axis servo control. This allows us to program pitch changes mid-coil, create closed ends with a specific gap, and form hooks or loops at the ends without secondary bending operations. The tolerance benefit is direct: a CNC-coiled spring holds pitch consistency of ±0.02mm across 50 coils, while a traditional winder holds ±0.08mm. For a decorative spring that is 80mm long, that is the difference between a uniform visual helix and a spring that looks hand-made in a bad way.
CNC coiling also lets us handle materials that are difficult to wind, like beryllium copper and 17-7PH, which have high springback. The servo system compensates for springback in real time, adjusting the coiling angle by fractions of a degree. This means we can produce a 1.0mm wire diameter spring with a 6mm OD and get a consistent gap of 0.5mm between coils — every time. If you are designing a spring for a visible mechanism, this precision is what makes the product look premium.
Design Rules for Decorative Springs: What We Recommend You Specify
When you send your drawing for Decorative Craft Springs Collection 02, include these five data points: wire diameter, outside diameter, free length, number of active coils, and end style (closed and ground, closed not ground, open). Also specify surface finish target (Ra0.4 is standard, Ra0.2 available) and whether plating is required. If you do not specify, we default to closed and ground ends with Ra0.4 and no plating. For torsion springs, specify the arm length and the angle between arms in free position. For conical springs, specify the small OD, large OD, and the pitch transition rate.
One common mistake: engineers specify a load at a compressed length but forget the solid height — the length when all coils are touching. For decorative springs, we recommend you keep the solid height at least 15% below your minimum working height. This prevents coil interference and maintains the visual gap. If you are unsure, send us your drawing and our engineers will flag any issue within 12 hours. We have seen thousands of spring drawings — we can tell you if your design is manufacturable at the tolerance you want.
Can I order just one piece to test the look and feel?
Yes, no MOQ applies to Decorative Craft Springs Collection 02 — a single piece is accepted, and you will pay only for the material and setup time, with prototype lead time of 7 days.
What is the maximum wire diameter you can coil in this collection?
8.0mm is the maximum wire diameter, but for decorative springs above 5mm we recommend a ground-end finish to ensure the spring stands perfectly flat on a table.
How do you ensure plated springs do not flake or crack?
We bake all plated springs at 190°C for 4 hours to relieve hydrogen embrittlement, then load-test each spring for 24 hours at 50% deflection — flaking is eliminated by this process.
What if my drawing has tolerances tighter than ±0.02mm?
Send it anyway — our CNC coiling and grinding processes can achieve ±0.01mm on wire diameter under 2mm, but we will quote a longer lead time of 20 days for that level.
Get a Firm Quote Within 12 Hours — Send Your Drawing Today
Send your 2D drawing or 3D model for Decorative Craft Springs Collection 02 and receive a firm quote with exact pricing, lead time, and tolerance confirmation within 12 business hours. Our engineers review your file and respond with a detailed breakdown — no vague estimates. For design advice, read our CNC cutting tool selection guide to understand how we machine any mating components, and our CNC machining tolerances guide to see how spring tolerances align with overall assembly precision.
Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. We are BQUQ — precision manufacturing in Dongguan, China, since 2005. No MOQ, no minimum order headaches, just exactly what you specified.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.