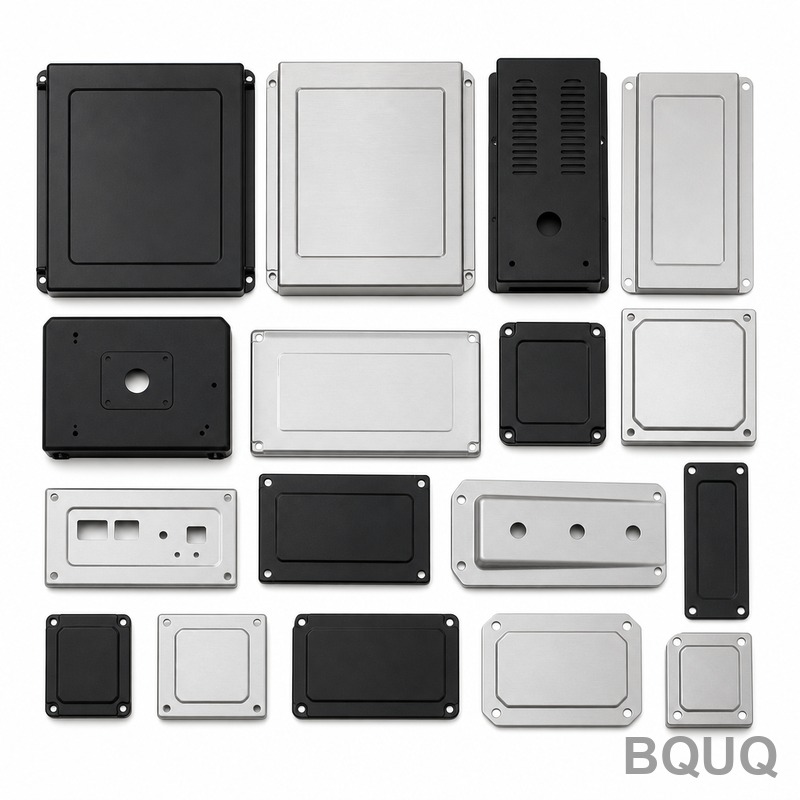
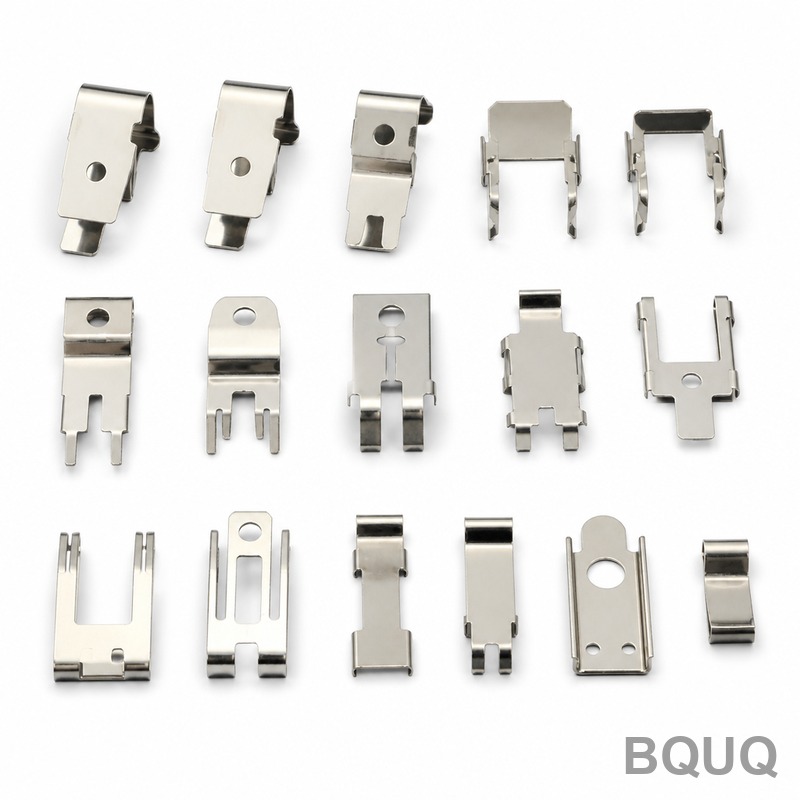
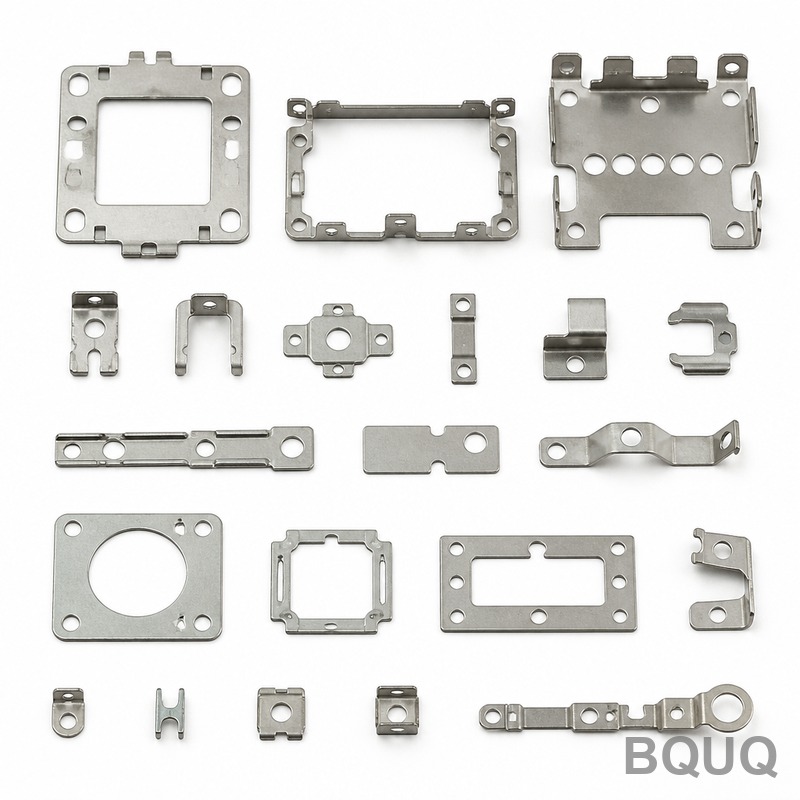
This is our Stamped Sheet Metal Enclosures Covers Collection — a series of precision-formed steel and aluminum covers designed to protect electronics, sensors, and mechanical assem
BQUQ Stamped Sheet Metal Enclosures Covers Collection | Precision Manufacturing
This is our Stamped Sheet Metal Enclosures Covers Collection — a series of precision-formed steel and aluminum covers designed to protect electronics, sensors, and mechanical assemblies in demanding i
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is our Stamped Sheet Metal Enclosures Covers Collection — a series of precision-formed steel and aluminum covers designed to protect electronics, sensors, and mechanical assemblies in demanding industrial environments. Each part ships with a guaranteed tolerance of ±0.05 mm, surface finish down to Ra 0.8, and a standard lead time of 10 working days from drawing approval. You get enclosures that fit your mating components without rework, made in China under strict BQUQ process control.
How Our Progressive Dies Hold ±0.05 mm Over 50,000 Hits
We use progressive dies with hardened tool steel inserts (62 HRC) and a four-post guide frame that keeps punch-to-die clearance uniform. This setup eliminates the progressive drift you see with cheaper tooling, especially on parts longer than 150 mm. Runout on flanged covers stays under 0.03 mm. For high-volume runs, we carbide-coat the wear surfaces, which extends die life to 1.2 million strokes before any dimensional change is detectable.
Materials and Heat Treatment We Use for Enclosure Covers
We stock SPCC cold-rolled steel (0.5–3.0 mm), SECC electro-galvanized steel, and 5052-H32 aluminum as standard options. For stainless requirements, we use SUS304 and SUS316L in thicknesses from 0.4 mm to 2.5 mm. When your cover needs extra stiffness or wear resistance, we offer induction hardening on selective edges up to 48 HRC. All raw coils come with mill certificates and are tested for yield strength before we commit them to production.
Deburring and Surface Finish: Ra 0.8 Without Secondary Op Costs
Every stamped cover goes through a two-stage deburring line — first a vibratory tumbler with ceramic media, then a dry abrasive belt pass. This removes all micro-burrs on the cut edges and flanges, giving you a safe-to-handle part rated to Ra 0.8 on visible surfaces. For cosmetic finishes, we offer brushed, bead-blasted, or powder-coated surfaces (60–120 micron thickness) in any RAL color. No secondary deburring is needed on your side.
Forming and Bending Accuracy for Flanged Covers and Lipped Enclosures
Our press brakes are equipped with CNC backgauges and angle-sensing lasers that hold bend angles to ±0.5 degrees. Flange heights are controlled within ±0.1 mm, and we use a coining step on all critical bend radii to eliminate spring-back variation. For deep-drawn covers (depth > 40 mm), we simulate the draw in-house using AutoForm software, which reduces die try-out time and ensures consistent wall thickness distribution.
Inspection Before Every Shipment: CMM and Height Gauge Verification
Every batch of Stamped Sheet Metal Enclosures Covers Collection parts is inspected on a coordinate measuring machine (CMM) with a resolution of 0.5 microns. We check all critical dimensions, hole positions, and flatness per your drawing. Additionally, we perform a 100% visual inspection on all visible surfaces for scratches, dents, or discoloration. A full dimensional report is included with each shipment, so you can skip incoming QC if your system allows.
Packaging and Anti-Rust Protection for Ocean or Air Freight
All covers are individually separated with VCI (vapor corrosion inhibitor) paper and then packed in export-grade corrugated boxes with foam inserts. For aluminum parts, we use a neutral pH paper to prevent any oxidation. If you are shipping by sea, we add a desiccant pack and a heat-sealed PE bag for each unit. This keeps your parts rust-free for up to 12 months in warehouse conditions.
Cost Reduction Through In-House Tooling and Secondary Operations
Our tool room builds all progressive and compound dies internally, which cuts tooling costs by 30–40% compared to outsourced tooling. We also perform tapping, countersinking, and riveting in-house, so you do not pay for separate suppliers. This integration is what allows us to offer no MOQ — even a single prototype cover is produced on the same line as a 10,000-piece order, with the same quality checks.
Specification
Value / Range
Material Options
SPCC, SECC, SUS304, SUS316L, 5052-H32
Thickness Range
0.4 mm – 3.0 mm
Maximum Part Size
600 mm x 400 mm
Hardness (Steel)
As-rolled 90 HRB; edge hardened up to 48 HRC
Dimensional Tolerance
±0.05 mm on critical features
Bend Angle Tolerance
±0.5 degrees
Surface Finish (Ra)
0.8 µm standard; 0.4 µm on request
Flatness (after forming)
≤ 0.1 mm per 100 mm length
Lead Time (prototype)
5 working days
Lead Time (production)
10 working days
MOQ
No MOQ — 1 piece accepted
Do you require a minimum order quantity?
No MOQ — we accept single-piece orders for prototypes and ramp up to high-volume production without any price penalty.
Can you customize a cover from my existing CAD model?
Yes, send us your STEP or IGES file, and our engineers will verify formability, add bend reliefs, and suggest material thickness changes within 24 hours.
How do you ensure quality on a small batch?
We follow the same CMM inspection and visual checks on a 1-piece lot as we do on a 10,000-piece run, and you get the dimensional report with the shipment.
What is the typical production lead time?
For stamped covers without custom tooling, we ship in 10 working days; if a new die is required, add 15 days for tool build and sample approval.
Send your drawing today for a firm quote within 12 hours. Email us at sc@bquq.com or reach us on WhatsApp at +86 13713157787. We will confirm material cost, tooling needs, and delivery date before you commit.