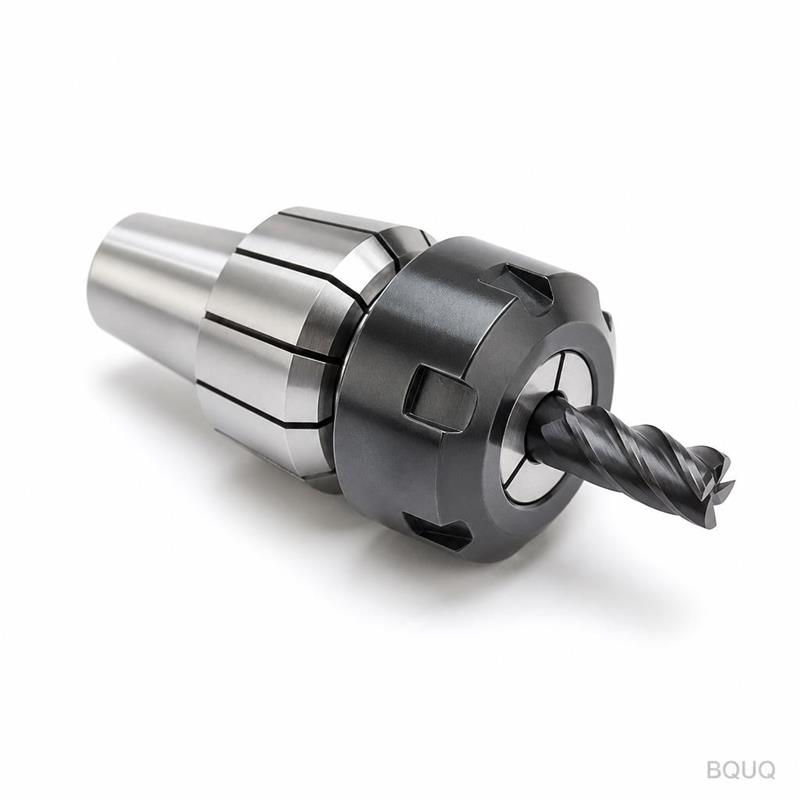
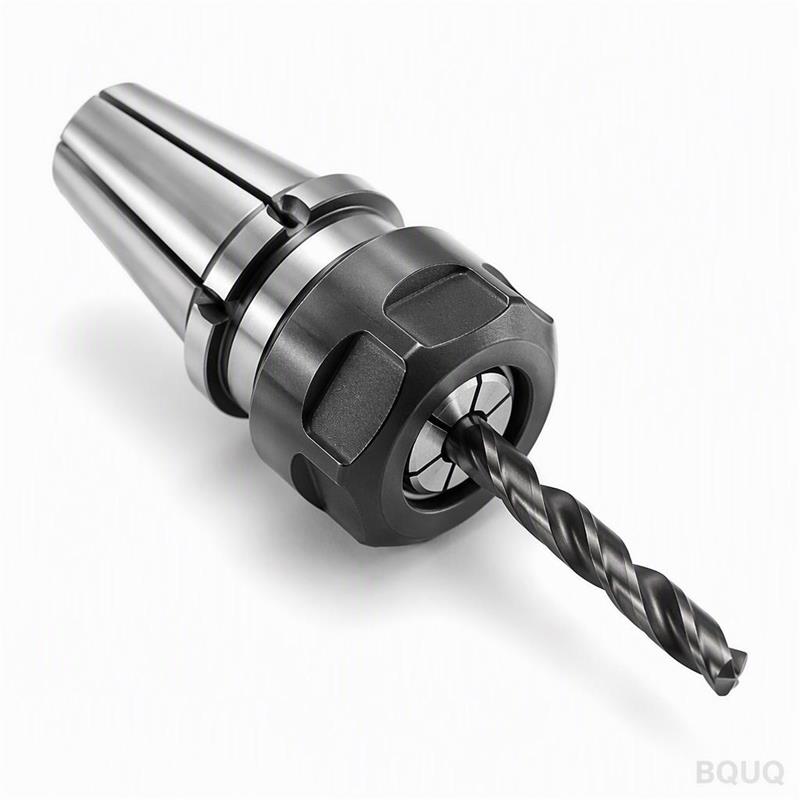
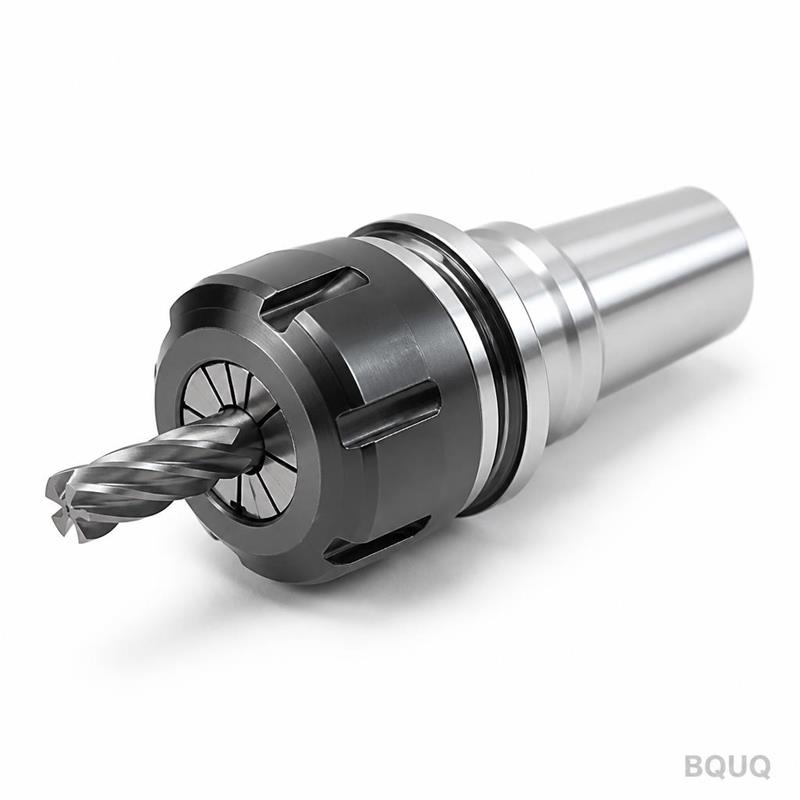
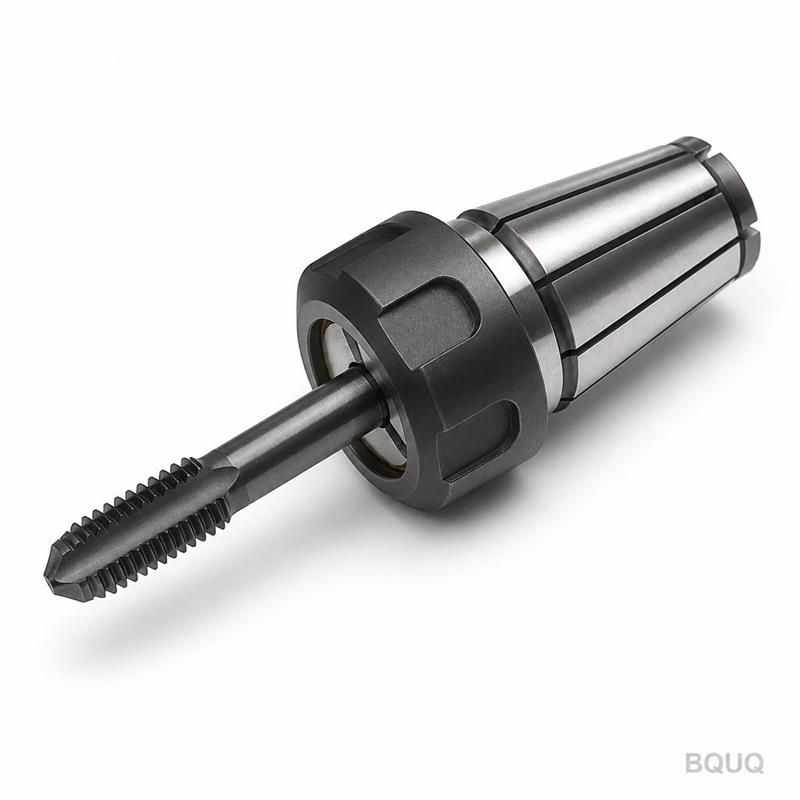
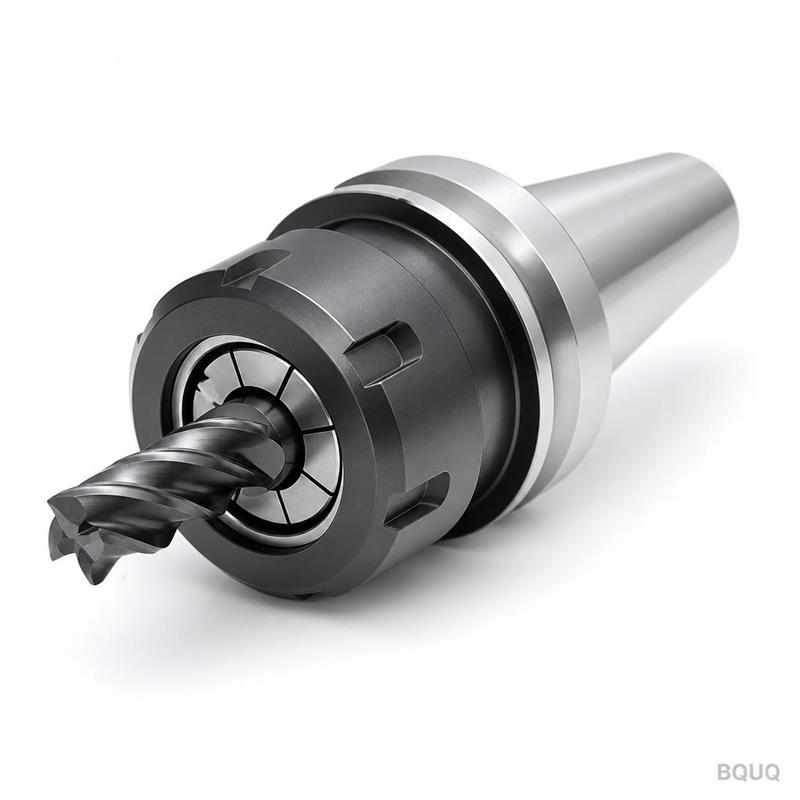
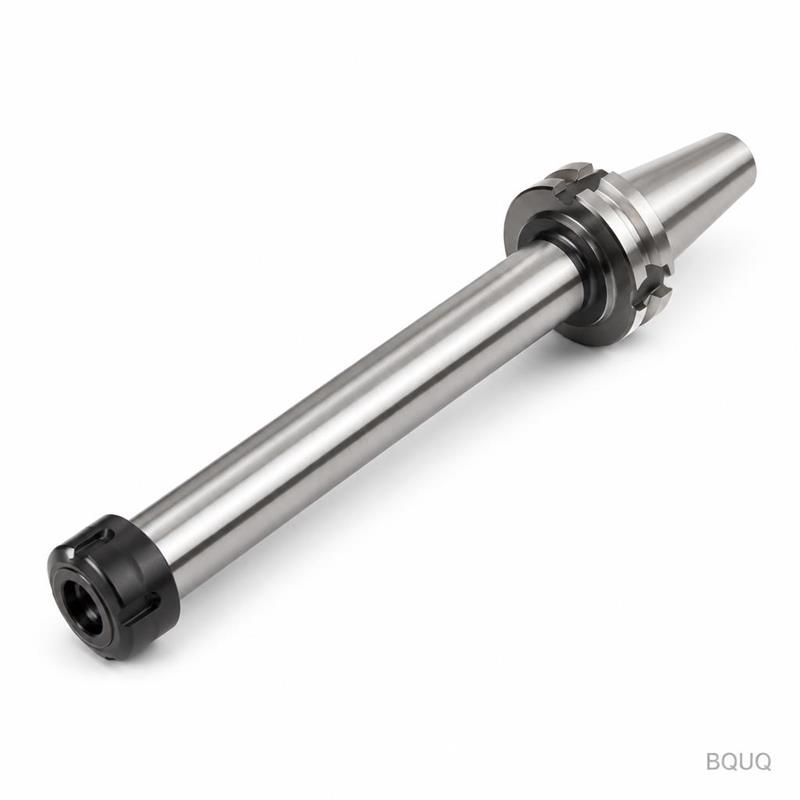
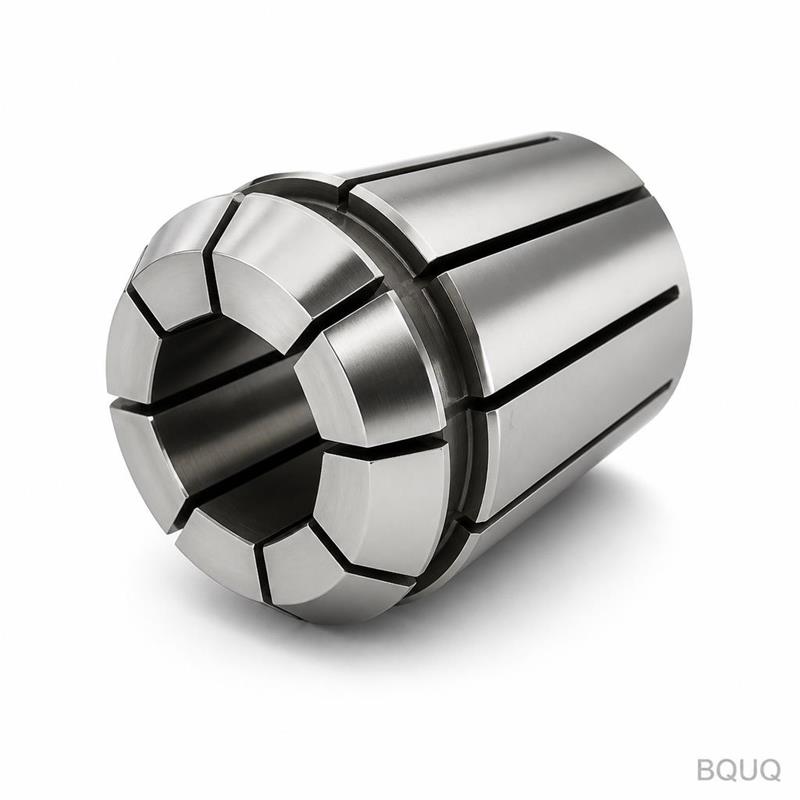
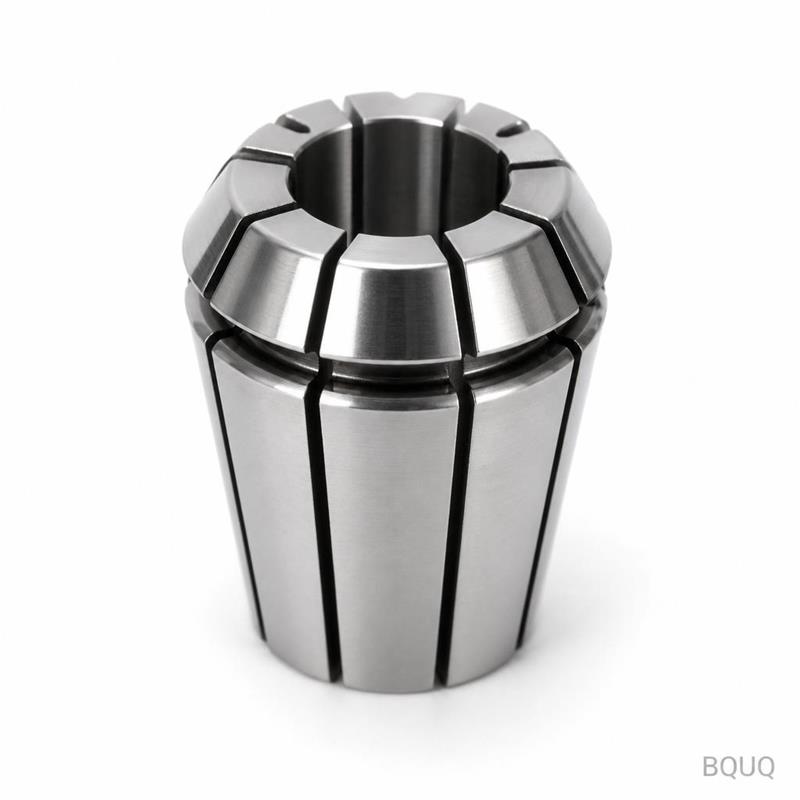
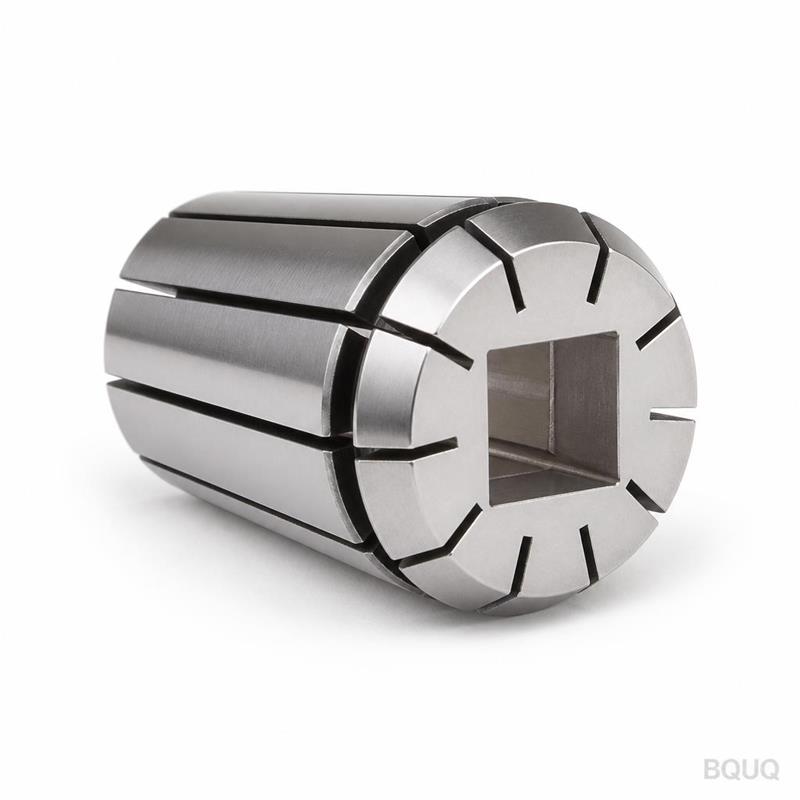
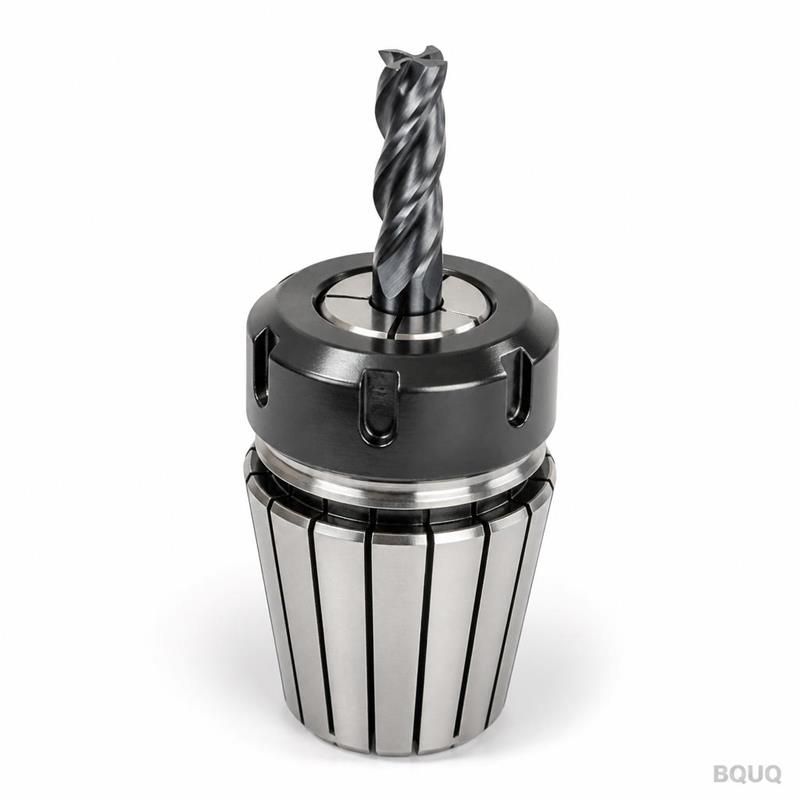
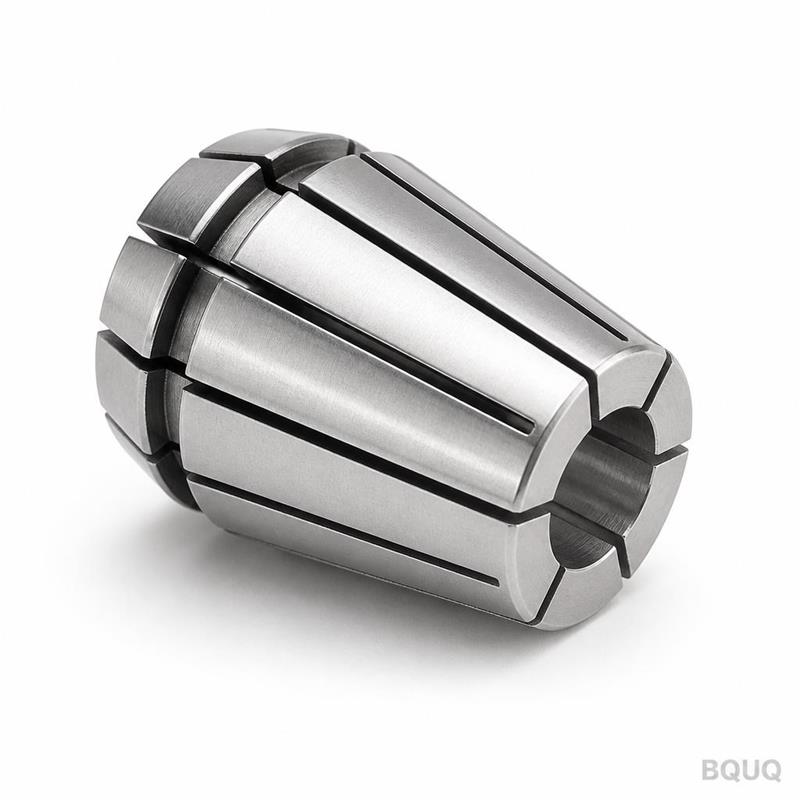
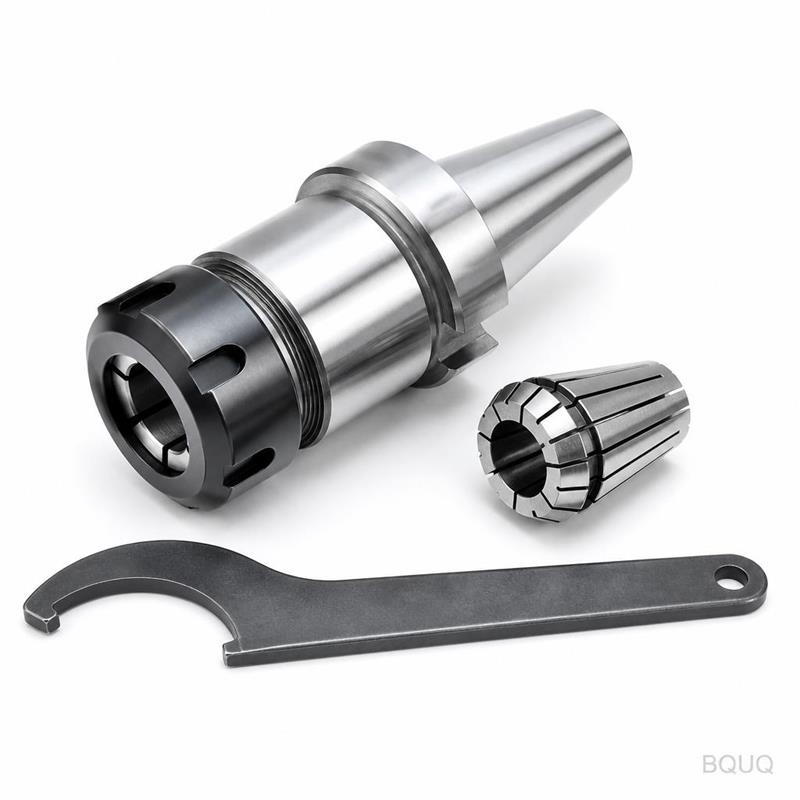
Custom CNC Machined ER20 Collet Chuck with Carbide End Mill
OpeningWe machine your ER20 spring collet chuck to your drawing, not to a stock catalog. Every chuck is verified for runout and taper fit before it leaves our floor. You send the print, we handle the
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
We machine your ER20 spring collet chuck to your drawing, not to a stock catalog. Every chuck is verified for runout and taper fit before it leaves our floor. You send the print, we handle the rest.
At a glance: ER20 taper tolerance within 0.005 mm, concentricity ≤ 0.01 mm TIR, lead time 7–12 days, no MOQ, made in China.
Laser engraving per your spec (part number, date code, logo)
We use 5-axis CNC mills and cylindrical grinders for the taper seat. Heat treatment is done in-house with a vacuum furnace for consistent hardness. Each batch gets a full dimensional report, not a sample check.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Every chuck gets a unique batch number. We keep material certificates, heat treatment records, and inspection data for 5 years. If a problem shows up in your assembly line, we trace it back to the exact heat and machine shift.
2. Inspection report per batch. You get a PDF with actual measured values for taper angle, runout, hardness, and surface finish. We do not send a generic "passed" sheet. The report shows the numbers, and you can verify them with your own gauge.
3. One factory for CNC + stamping + springs + heatsinks. Your collet chuck is not an orphan part. If your assembly needs a spring, a stamped retainer, or a heat sink for the spindle motor, we machine all of them under one roof. One purchase order, one quality system, one shipping point. No third-party coordination.
Where these parts are used
Custom CNC collet chucks with ER20 tapers are used in:
CNC milling spindles – holding carbide end mills for aluminum and steel cutting, where runout directly affects tool life and surface finish.
Automatic tool changers – on machining centers that require a repeatable grip force for high-speed tool swaps.
Engraving and PCB drilling machines – where the small ER20 size fits tight spindle noses and needs low vibration at 20,000+ RPM.
Robotic deburring cells – holding carbide burrs with a rigid, short projection to reduce deflection.
Inspection fixtures – as a precision reference for holding round parts during CMM measurement.
The ER20 size is common because it balances grip range (1–13 mm) with a compact body. When you pair it with a carbide end mill, the chuck's concentricity determines whether your tool cuts true or wobbles.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototype validation and scale to thousands. The unit price drops as quantity increases, but the quality standard stays the same.
Q: How do you guarantee taper and runout tolerance?
A: We grind the taper after heat treatment, not before. Then we check every chuck with a calibrated taper gauge and a dial indicator at the collet seat. The inspection report lists the actual measured runout, typically under 0.01 mm TIR.
Q: What is the lead time for a custom design?
A: 7 days for a prototype after drawing approval. Production batches take 12 days. If you need faster, tell us your deadline and we will schedule your job on the right machine.
Q: Do you provide material certificates?
A: Yes. Every batch comes with a mill certificate for the raw material, heat treatment report, and our dimensional inspection report. All documents are in English and traceable to the batch number.
Send your drawing
Email your PDF or STEP file to sc@bquq.com. We reply with a firm quote within 12 hours, including unit price, tooling cost (if any), and delivery date. For urgent questions, WhatsApp +86 13713157787. We are a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining experience. Your drawing is safe with us – we sign NDAs on request.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.