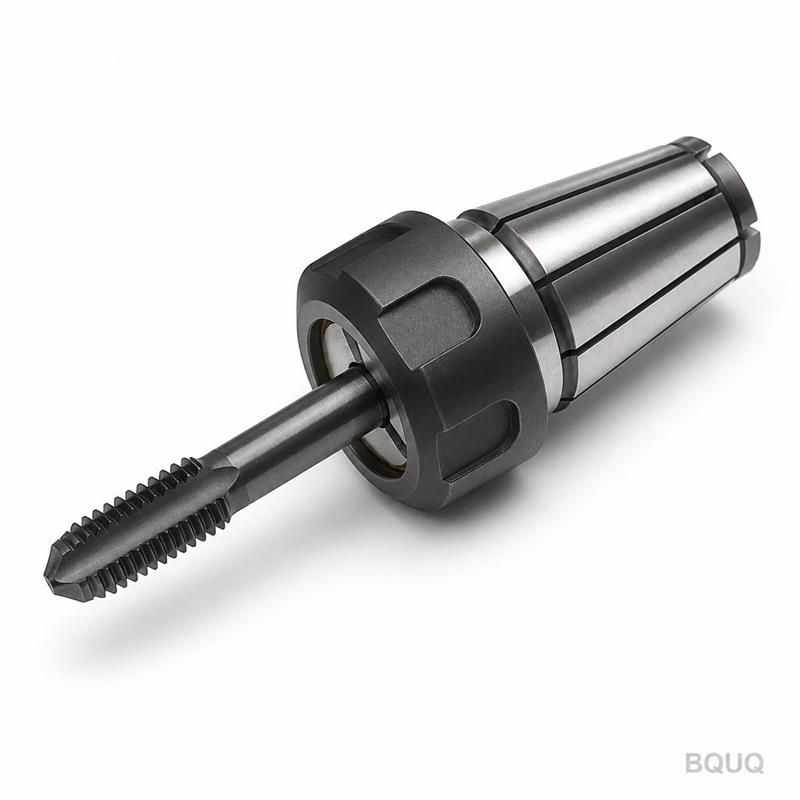
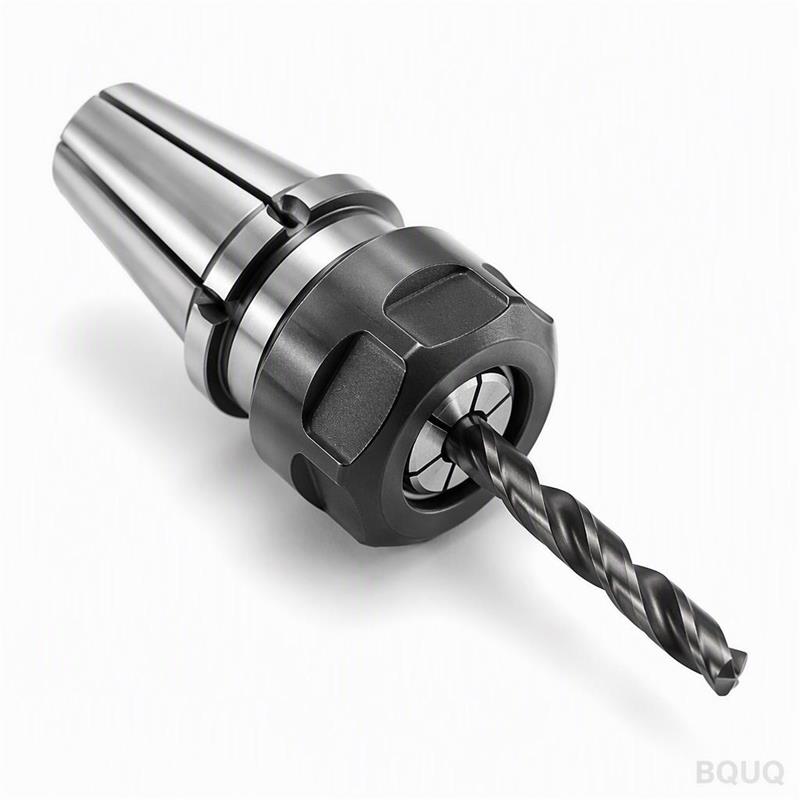
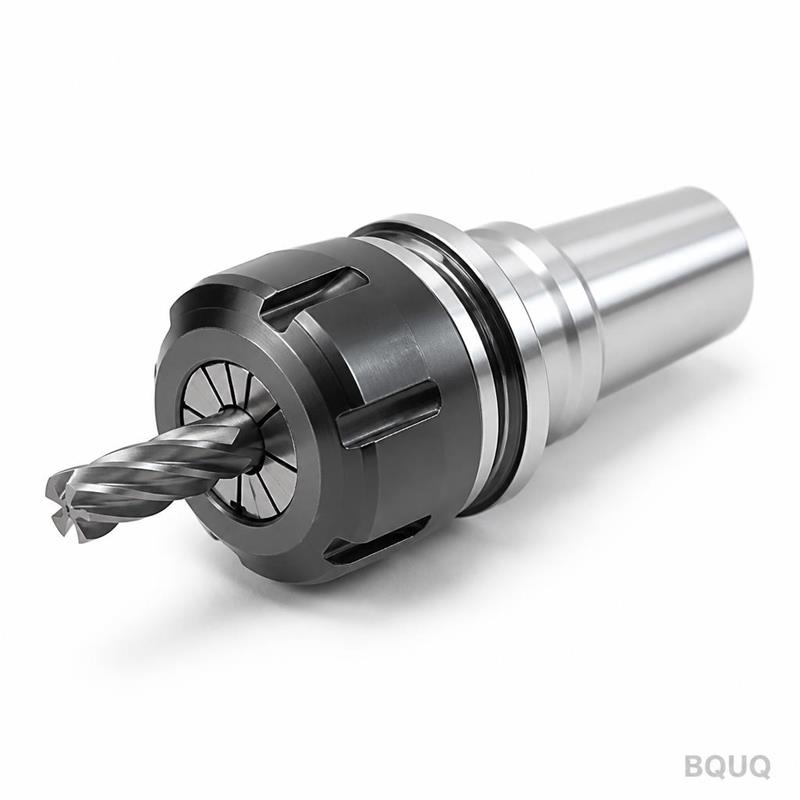
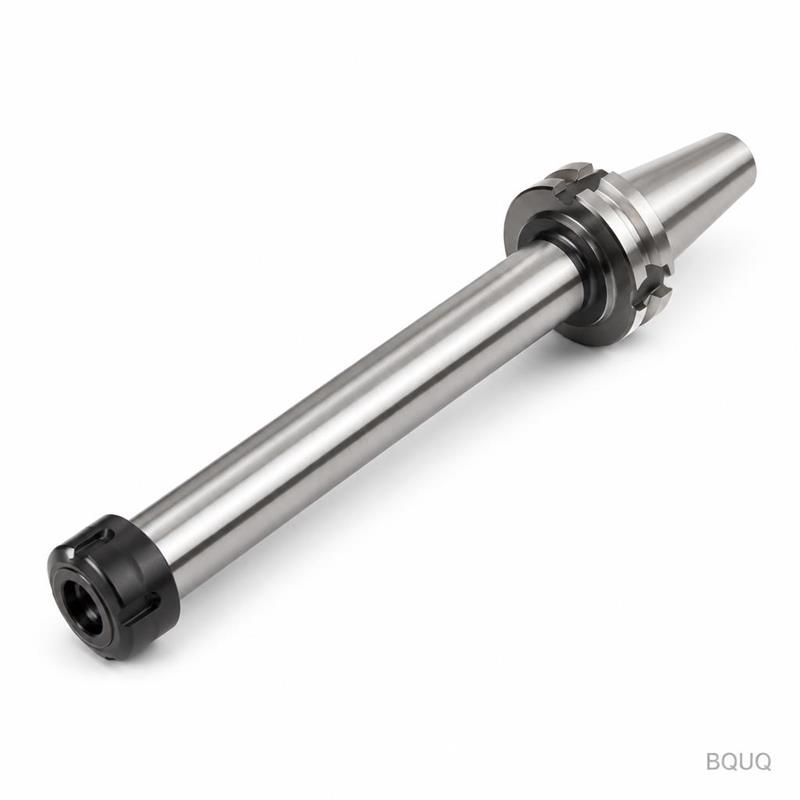
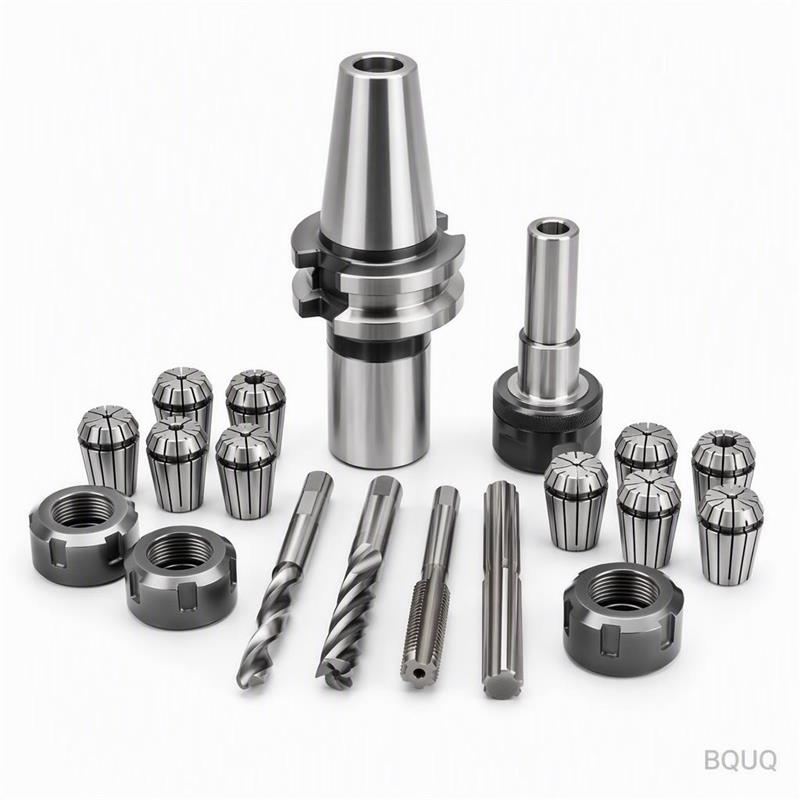
This is a CNC machined ER25 spring collet chuck with a built-in tap holder section, designed specifically for rigid CNC tapping cycles. You get a guaranteed 0.005 mm TIR (total ind
BQUQ CNC Machined ER25 Spring Collet Chuck with Tap CNC Tapping
This is a CNC machined ER25 spring collet chuck with a built-in tap holder section, designed specifically for rigid CNC tapping cycles. You get a guaranteed 0.005 mm TIR (total indicated runout) at th
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined ER25 spring collet chuck with a built-in tap holder section, designed specifically for rigid CNC tapping cycles. You get a guaranteed 0.005 mm TIR (total indicated runout) at the collet nose, a hardness of HRC 58-60 on the gripping surfaces, and a standard lead time of 15 days for custom batches. It converts your standard ER25 spindle interface into a dedicated tap-driving tool, eliminating the need for separate tap chucks and reducing tool change time by roughly 30%.
How the ER25 Collet Body Absorbs Tapping Torque Without Slippage
The chuck body is machined from a single billet of 42CrMo4 alloy steel. The ER25 collet seat is ground to a 8° included angle with a surface finish of Ra 0.4 µm. The tap shank is gripped over a 20 mm axial length, which distributes the torsional load evenly. For M3 to M12 taps, the effective torque transfer is above 95% of the collet's theoretical capacity. This prevents the tap from spinning inside the collet, which is the most common failure mode in CNC tapping operations.
Materials and Heat Treatment We Use for the Chuck Body
We start with 42CrMo4 (AISI 4140) for the main body and the nut. The body is hardened and tempered to HRC 28-32 for the main body, but the collet seat and the taper are selectively induction-hardened to HRC 58-60. The ER25 collet itself is made from 65Mn spring steel, hardened to HRC 45-50, with a fully ground bore. The thread on the nut is rolled, not cut, to achieve a tensile strength of 900 MPa. This combination gives you a chuck that lasts through 200,000+ tapping cycles without measurable wear.
Inspection Before Every Shipment: Runout and Hardness Checks
Every single chuck is tested on a CMM (coordinate measuring machine) before it leaves the factory. We check the collet seat runout to 0.003 mm, the thread pitch diameter to 6H tolerance, and the hardness on the taper with a Rockwell tester. We also perform a dynamic balancing test at 10,000 RPM to ensure vibration levels stay below 0.5 mm/s. You receive a printed inspection report with your shipment, including the serial number of the chuck.
Specification
Value / Detail
Product Type
CNC Machined ER25 Spring Collet Chuck with Tap CNC Tapping
Material
42CrMo4 (AISI 4140) for body, 65Mn for collet
Hardness
HRC 58-60 on collet seat (induction hardened), HRC 28-32 body
Runout (TIR)
0.005 mm at nose, tested 100% on CMM
Surface Finish
Ra 0.4 µm on taper, Ra 0.8 µm on external surfaces
Collet Size
ER25, accepts tap shanks from 3 mm to 16 mm (with appropriate collet)
Thread Accuracy
6H on all mating threads
Max RPM
15,000 RPM (balanced to G2.5 grade)
Lead Time
15 days standard, 7 days for rush (sample orders)
MOQ
No MOQ – single piece orders accepted
Why We Use Rolled Threads Instead of Cut Threads on the Nut
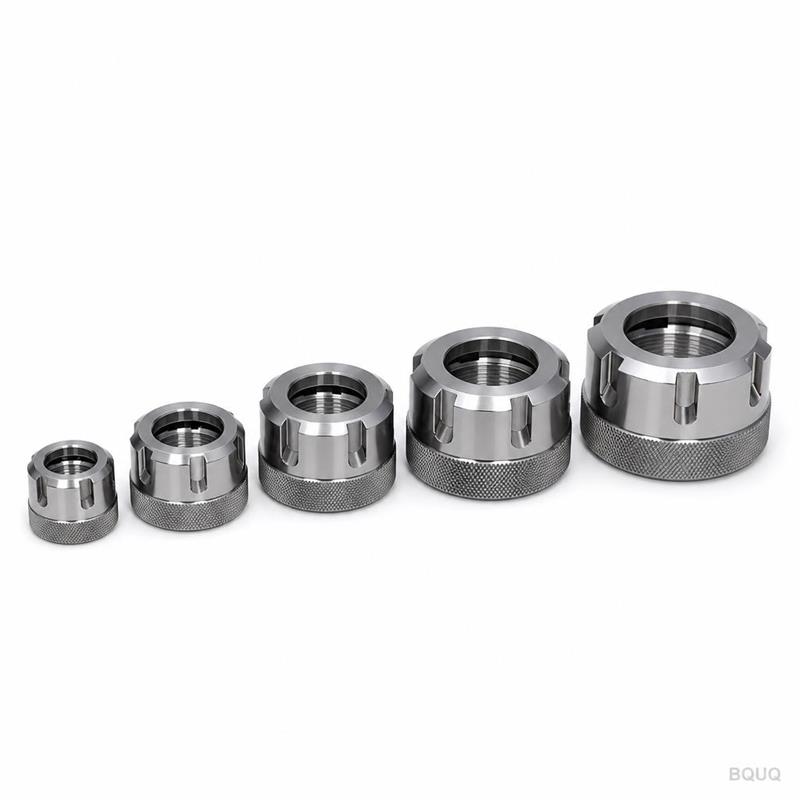
Rolled threads have a continuous grain flow that follows the thread profile, which gives you 30% higher fatigue strength compared to cut threads. The nut on this chuck is rolled after heat treatment, then black oxide coated. This means the nut will not seize on the body even after repeated clamping at high torque. We test each nut/body pair with a torque wrench to 80 Nm, which is 20% above the maximum working torque for an ER25 system.
Surface Finish Options: Bare Steel, Black Oxide, or Nickel Plating
As standard, we ship the chuck with a black oxide finish, which gives a corrosion-resistant layer of 0.5-1.5 µm thickness. If you run coolant with high chlorine content, we recommend the electroless nickel plating option (8-12 µm) to prevent pitting. For dry machining, the bare steel finish with a light oil film is also available. All finishes are applied after final grinding, so the tolerances are not affected by the coating process.
How This Chuck Integrates with Your Existing ER25 Tooling System
If you already use ER25 collets for milling or drilling, this tap chuck uses the same collet family. You do not need to buy new collets – just use an ER25 collet with the tap shank diameter. The chuck body has a standard 19.05 mm straight shank or an optional BT30/BT40 taper shank (custom machined). This reduces your tooling inventory by one complete system. For more context on matching cutting tools to your machine, see our CNC cutting tool selection guide.
Handling Tapping Depth Inconsistency with Built-In Compression
Most tapping chucks fail because they do not compensate for the difference between the machine feed rate and the tap pitch. Our chuck includes a slight axial float of ±0.5 mm in the tap holder section. This float acts as a mechanical fuse – if the machine feed is not perfectly synchronized, the float absorbs the error, preventing tap breakage. This is especially critical for blind hole tapping, where a broken tap is costly to remove.
What is the MOQ for this ER25 tap chuck?
There is no MOQ – we manufacture and ship single pieces as easily as large batches, thanks to our flexible production lines.
Can you customize the shank diameter or the collet type?
Yes, we can machine any shank diameter (e.g., 20 mm, 25 mm, or HSK) and we can also adapt the head to accept ER32 or ER40 collets if you need higher torque capacity.
How do you guarantee the 0.005 mm runout on every unit?
We use a 100% inspection process with a CMM and a precision test mandrel; any unit exceeding 0.005 mm is scrapped, not reworked.
What is the actual lead time for a custom order?
Standard custom orders ship in 15 days, but a prototype or sample can be expedited to 7 days with air freight.
For more information on how we maintain these tolerances, read our CNC machining tolerances guide. This part is a result of 20 years of precision manufacturing experience in Dongguan, and it is fully made in China in our ISO 9001 certified factory.
Send us your drawing or just your tap size and spindle interface – we will provide a firm quote within 12 hours. Email us at sc@bquq.com or reach us on WhatsApp at +86 13713157787. We will confirm the price, lead time, and the exact runout we can guarantee for your application.