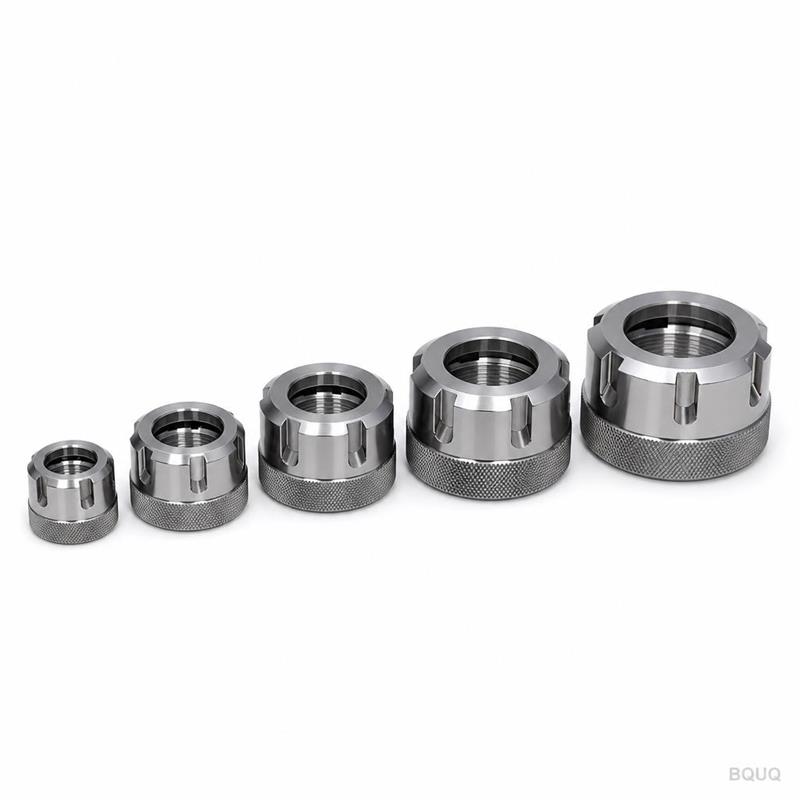
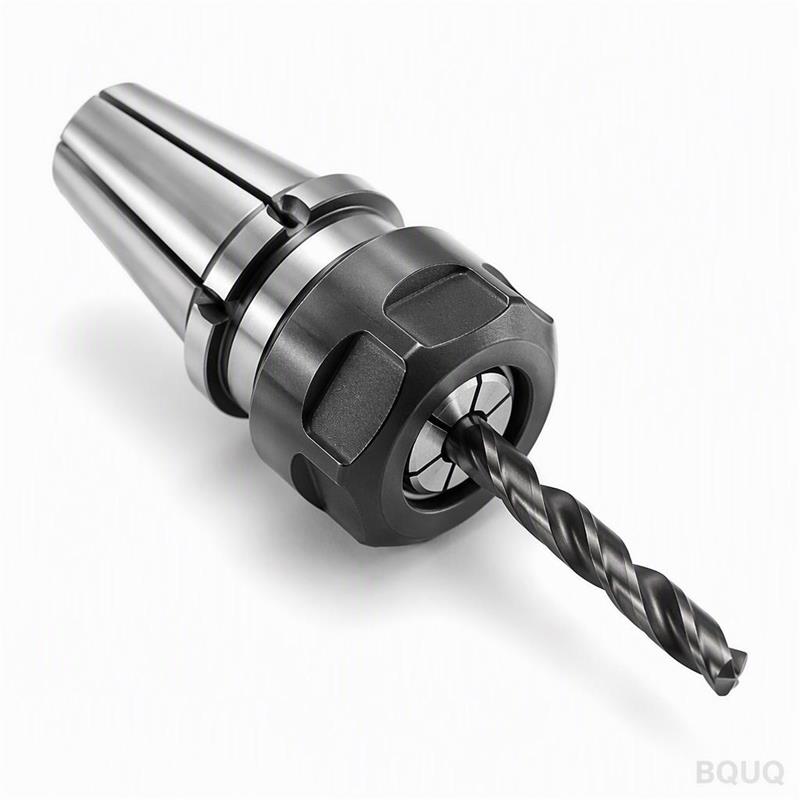
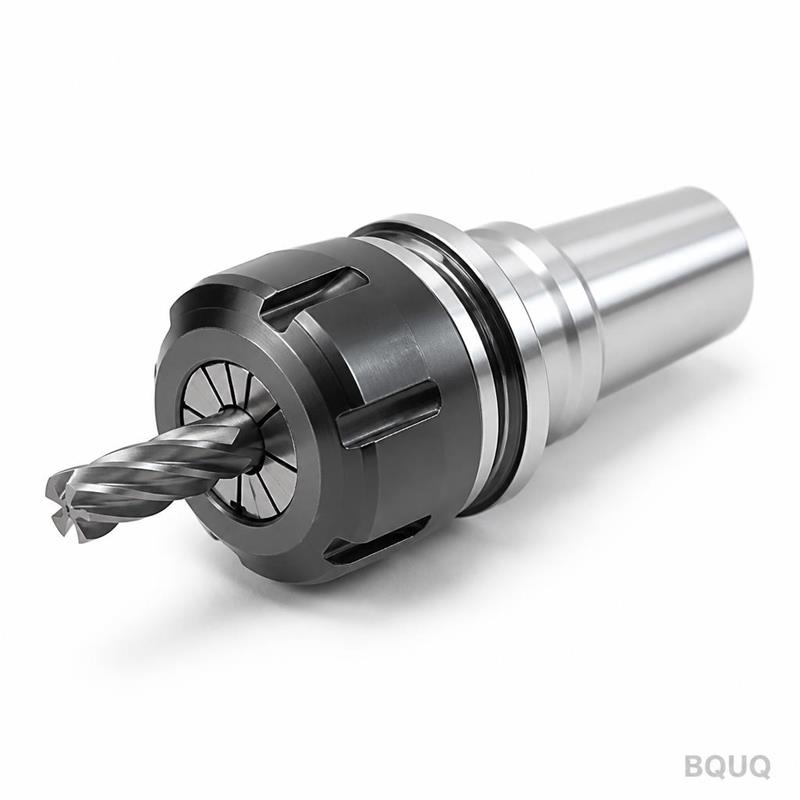
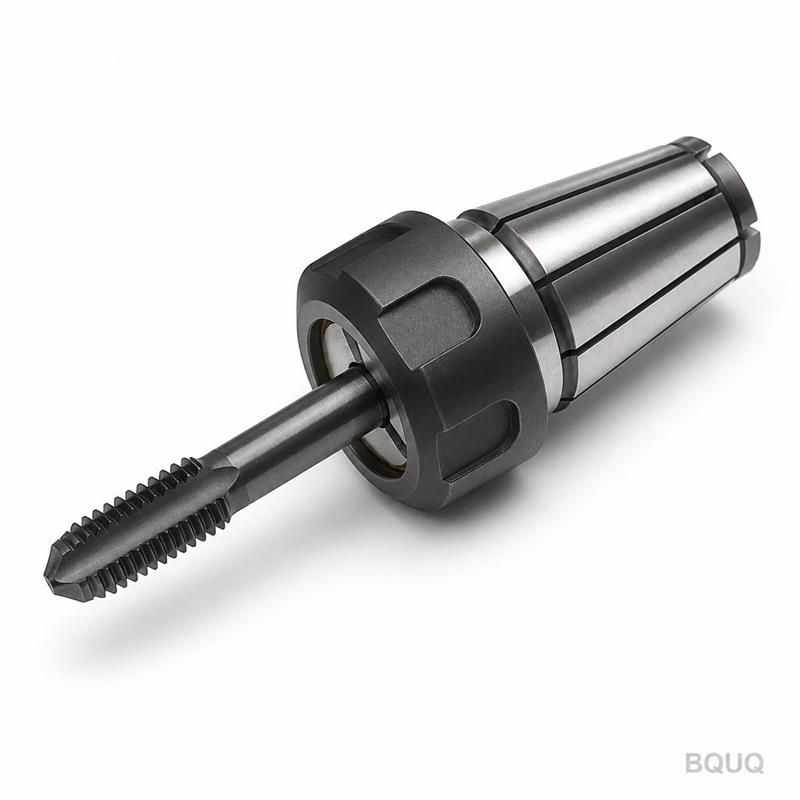
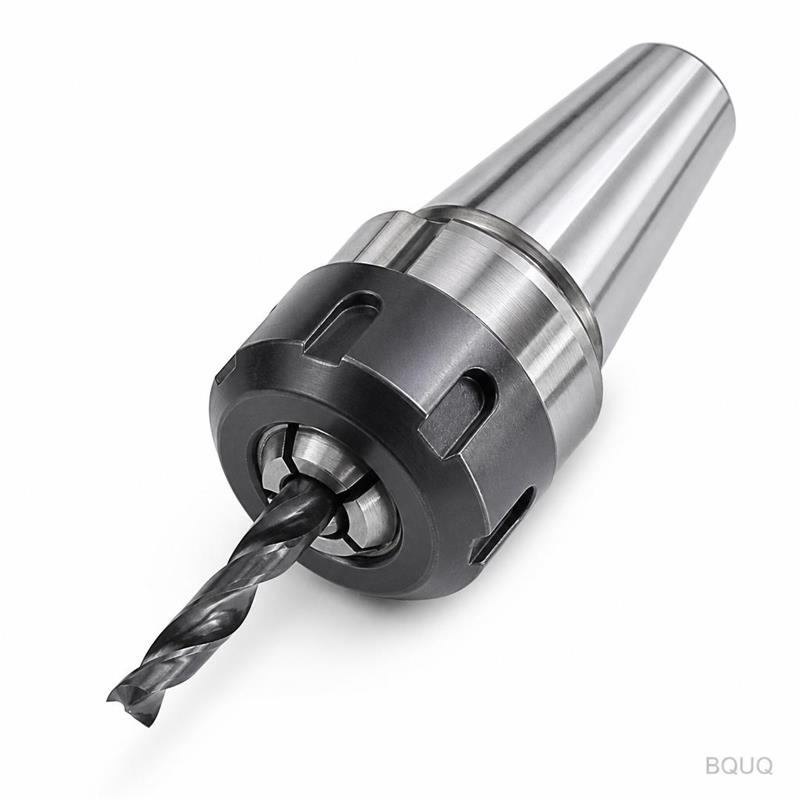
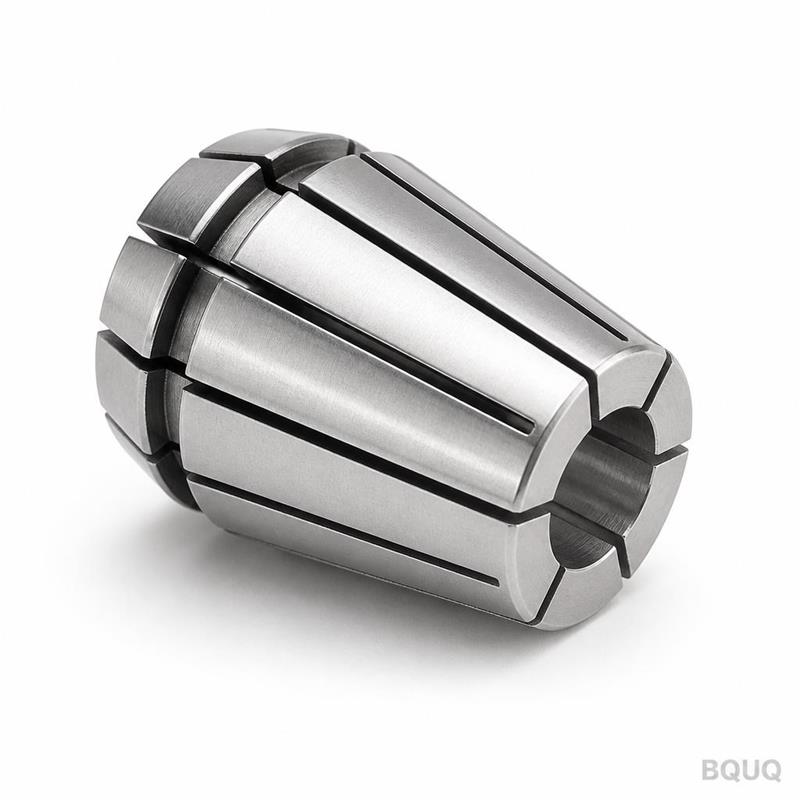
This is a complete CNC machined ER collet nut set in various sizes, built for holding tool shanks firmly in CNC spindles and collet chucks. You get a guaranteed runout of 0.005mm o
BQUQ CNC Machined ER Collet Nut Set Various Sizes Precision Tooling
This is a complete CNC machined ER collet nut set in various sizes, built for holding tool shanks firmly in CNC spindles and collet chucks. You get a guaranteed runout of 0.005mm or less, a surface fi
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a complete CNC machined ER collet nut set in various sizes, built for holding tool shanks firmly in CNC spindles and collet chucks. You get a guaranteed runout of 0.005mm or less, a surface finish of Ra 0.4µm, and a nut hardness of 45HRC—so your tooling stays centered under heavy cuts, not wobbling at 15,000 RPM. Every set is made in China at our Dongguan factory with 20 years of precision manufacturing experience, and we ship standard sizes within 7 days with no MOQ.
How ER Collet Chucks Grip Tooling Without Runout
An ER collet nut set works by compressing a slotted collet inward onto the tool shank. The nut’s internal taper angle (exactly 8 degrees for ER series) matches the collet’s external taper, creating a uniform radial force around the entire circumference. This is what keeps runout at 0.005mm—not luck, but geometry. The threads on our nuts are rolled, not cut, to eliminate stress risers and maintain concentricity between the nut and the collet seat. When you torque the nut to the recommended 80-100 Nm (for ER32), the collet closes evenly, gripping the tool shank across its full length, not just at the mouth.
Materials and Heat Treatment We Use
We machine the nuts from 4140 alloy steel, not cheap 12L14. The collets themselves are made from 65Mn spring steel. For the nut body, we harden to 42-45HRC, which resists galling when you repeatedly tighten and loosen it. The threads are precision ground after heat treatment, so the pitch diameter stays within 0.02mm. Collets get a spring temper of 44-48HRC, allowing them to flex open and closed over thousands of cycles without taking a permanent set. We finish everything with a black oxide coating to prevent corrosion. No coating flakes off inside your spindle—it’s a chemical conversion layer, not paint.
Inspection Before Every Shipment
Every single nut and collet goes through a 100% inspection, not a batch sample. We check the taper angle on a CMM with a resolution of 0.001mm—if the taper is off by more than 0.005mm, it’s scrapped. Runout is measured at the nose of the collet with a test bar, and we record the actual value on the packing slip. Thread fit is verified with a go/no-go gauge. Hardness is spot-checked on a Rockwell tester, one sample per heat treatment batch. If you ask for our inspection report, we send it with the shipment, signed by the QC lead. We don’t ship a set unless every piece passes.
Size Range and Fit for Common Spindles
We stock ER11, ER16, ER20, ER25, ER32, and ER40 nut sets. Each set includes the nut and the matching collet sizes—from 1mm up to 26mm gripping range depending on the series. The ER32 set covers tool shanks from 2mm to 20mm; the ER40 set goes up to 26mm. Threads match standard spindle noses: ER11 uses M14x0.75, ER16 uses M16x1.0, ER20 uses M20x1.0, ER25 uses M25x1.5, ER32 uses M32x1.5, ER40 uses M40x1.5. If you use a BT, CAT, or HSK holder, the nut thread is the same—it’s the holder taper that changes. We can also machine custom thread pitches for non-standard spindles, but that adds 3-5 days to lead time.
Specification
Value
Material (Nut)
4140 Alloy Steel
Material (Collet)
65Mn Spring Steel
Nut Hardness
42-45 HRC
Collet Hardness
44-48 HRC
Runout (TIR)
≤0.005mm
Surface Finish
Ra 0.4µm
Thread Tolerance
6H (internal)
Available Sizes
ER11, ER16, ER20, ER25, ER32, ER40
Gripping Range
1mm to 26mm (by series)
Lead Time (Standard)
7 days
MOQ
No MOQ
Coating
Black Oxide
Why Torque Consistency Matters for Tool Life
If you under-torque the nut, the collet doesn’t close fully, and the tool pulls out during a cut. Over-torque deforms the collet slots permanently, and you lose grip. We machine a hex-shaped drive surface on the nut so a torque wrench engages cleanly, not slipping off. The nut’s outer diameter is sized to clear standard spindle noses, so you don’t need a special socket. For ER32, the recommended torque is 80-100 Nm; for ER40, it’s 100-120 Nm. Use a torque wrench every time—your tool life improves by up to 30% compared to hand-tightening, because the cutting edge stays where you set it. The nut set itself won’t fix a worn spindle, but it will eliminate the variable of loose tooling.
Custom Options for Non-Standard Tool Holders
If you run a proprietary spindle or a modified holder, we can adjust the nut’s thread pitch, outer diameter, or drive slot configuration. Send us a drawing or a sample nut, and we’ll reverse-engineer it within 48 hours. We can also change the coating—for example, electroless nickel for chemical resistance, or a dry-film lubricant for high-temperature cutting. If you need a longer nut to clear a deep counterbore, we’ll machine it from bar stock, not modify a standard blank. Because we CNC machine everything in-house, there’s no tooling cost for custom parts—just a slightly longer lead time of 10-12 days. We’ve done custom ER nuts for automotive, aerospace, and medical device manufacturers who use non-catalog spindles.
Packaging and Traceability for Every Set
Each nut and collet is individually wrapped in anti-rust paper, then placed in a foam-lined plastic box that prevents contact between parts. The box is labeled with the part number, batch number, and inspection date. If you order 50 sets, they come in a single carton with a packing list that matches the batch numbers. This traceability means if you ever have a quality issue, we can pull the exact heat treatment records and inspection logs for that batch. We’ve been doing this for 20 years, and we keep records for 5 years. You don’t get a generic bag of parts—you get a documented set that meets the tolerances we advertise.
Before you pick a collet system, check our CNC cutting tool selection guide to see how the ER nut fits with your other tooling. And if you’re setting tolerances on a new part, our CNC machining tolerances guide explains what’s achievable in practice, not just on paper.
What is the minimum order quantity for the ER collet nut sets?
There is no MOQ—order one set or a thousand, the unit price only drops slightly at 50+ sets because we save on setup time.
Can you customize the thread pitch or nut dimensions for my spindle?
Yes, send us a drawing or sample, and we’ll machine a custom nut in 10-12 days, including any thread pitch or outer diameter change.
How do you guarantee the 0.005mm runout on every set?
We measure each assembled nut-and-collet set with a test bar on a CMM, and the actual runout value is written on the inspection report included with your shipment.
What is the typical lead time for standard ER collet nut sets?
Standard sizes ship in 7 days from our Dongguan factory; custom sizes take 10-12 days depending on the complexity of the modification.
Get a firm quote within 12 hours. Email your drawing or your required sizes to sc@bquq.com, or message us on WhatsApp at +86 13713157787. We’ll confirm the price, lead time, and specs before you commit.