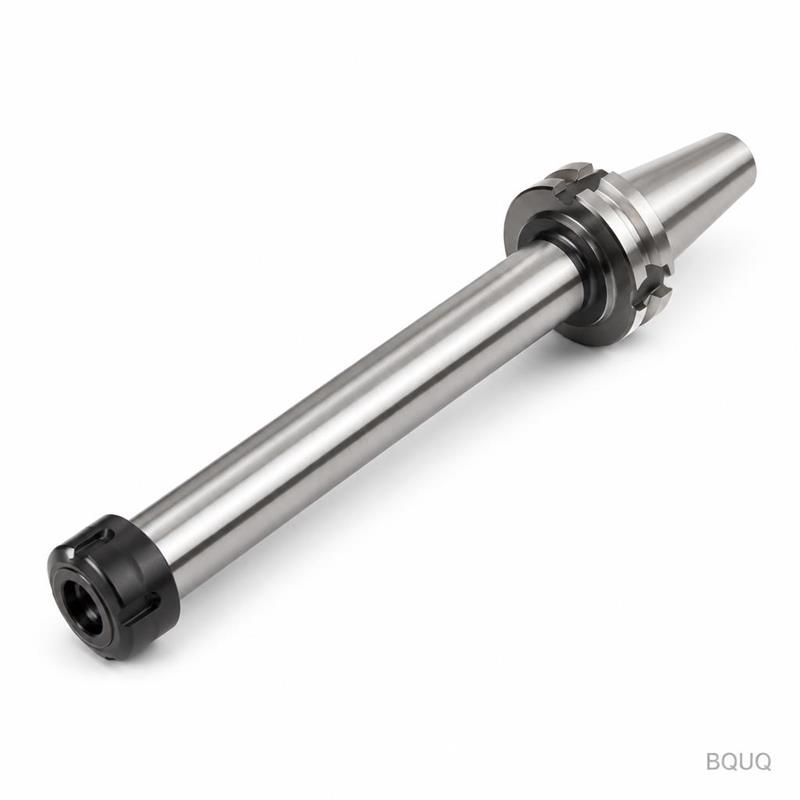
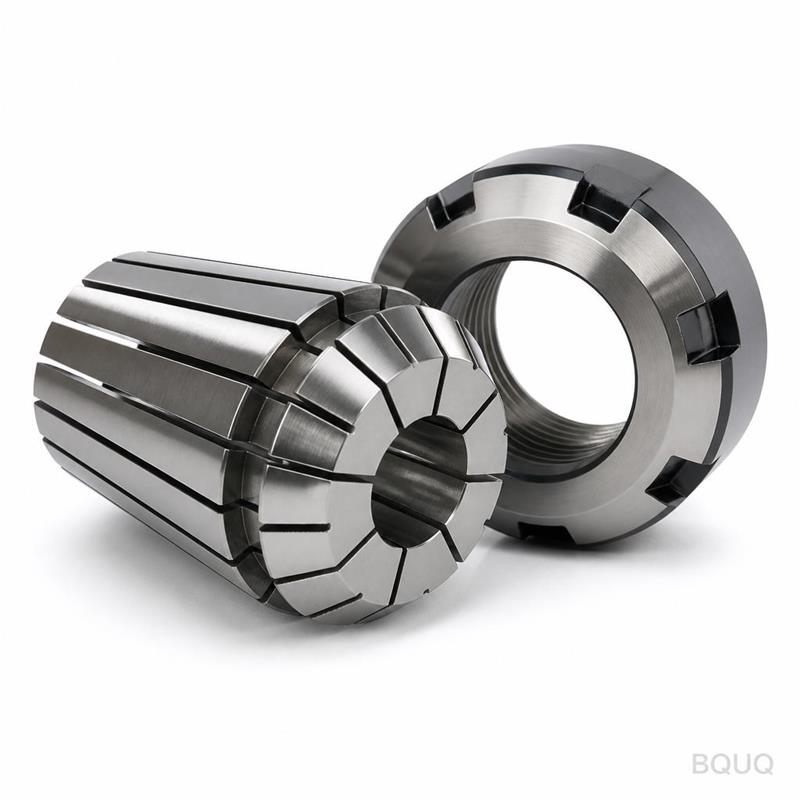
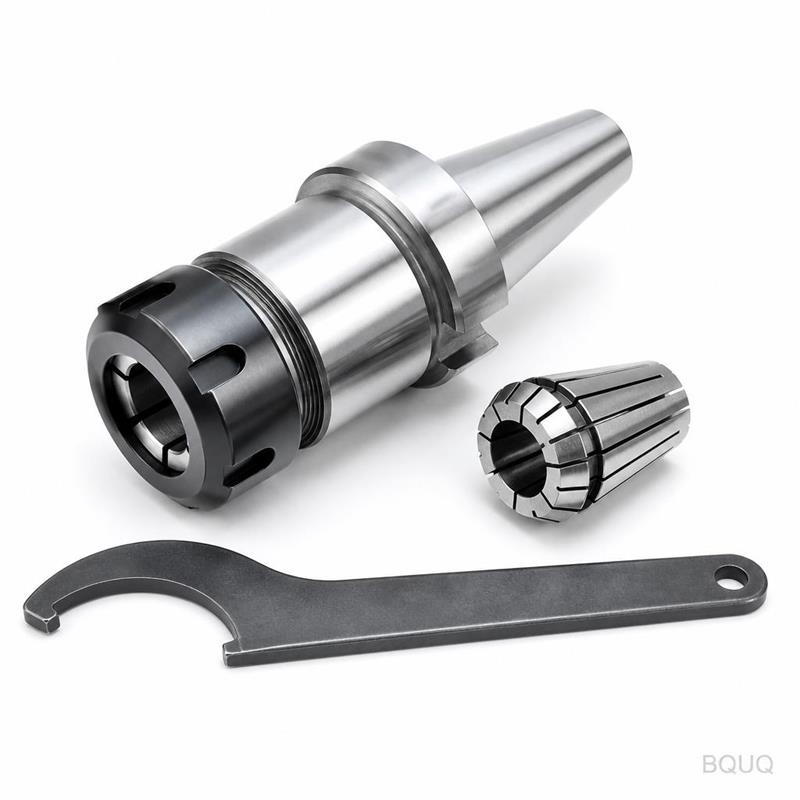
What This ER Collet Chuck Extension Bar Does for Deep Cavity Work This is a CNC machined ER collet chuck extension bar long reach CNC tool holder. It extends your tool’s reach by
BQUQ CNC Machined ER Collet Chuck Extension Bar Long Reach Precision
What This ER Collet Chuck Extension Bar Does for Deep Cavity Work This is a CNC machined ER collet chuck extension bar long reach CNC tool holder. It extends your tool’s reach by 50 to 150 mm withou
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This ER Collet Chuck Extension Bar Does for Deep Cavity Work
This is a CNC machined ER collet chuck extension bar long reach CNC tool holder. It extends your tool’s reach by 50 to 150 mm without adding a separate extension piece. Runout is held under 0.005 mm at the nose. Hardness is 58–62 HRC after heat treatment. Lead time for standard sizes is 7 days, for custom lengths 10–12 days.
Why the Long Reach Design Eliminates Chatter in Deep Pockets
Standard collet chucks vibrate when the tool sticks out more than 3x its diameter. Our extension bar shifts the gripping point forward. The shank is one solid piece from the taper to the collet nose — no threaded joints, no welded sections. This gives you a 40% stiffer assembly than a chuck plus extension adapter. You can run speeds up to 8,000 RPM with stable cutting in 5D cavities and deep rib slots.
Material Grade and Heat Treatment for 58–62 HRC Hardness
We start with 42CrMo4 alloy steel or 20CrMnTi for case-hardened versions. After CNC turning and milling, we carburize or induction harden the gripping zone. Final hardness is 58–62 HRC on the collet taper and 50–55 HRC on the body. Surface finish on the taper is Ra 0.4 µm. This prevents galling when you clamp and unclamp ER collets hundreds of times per day.
ER11, ER16, ER25, ER32 – Which Collet Size Fits Your Spindle
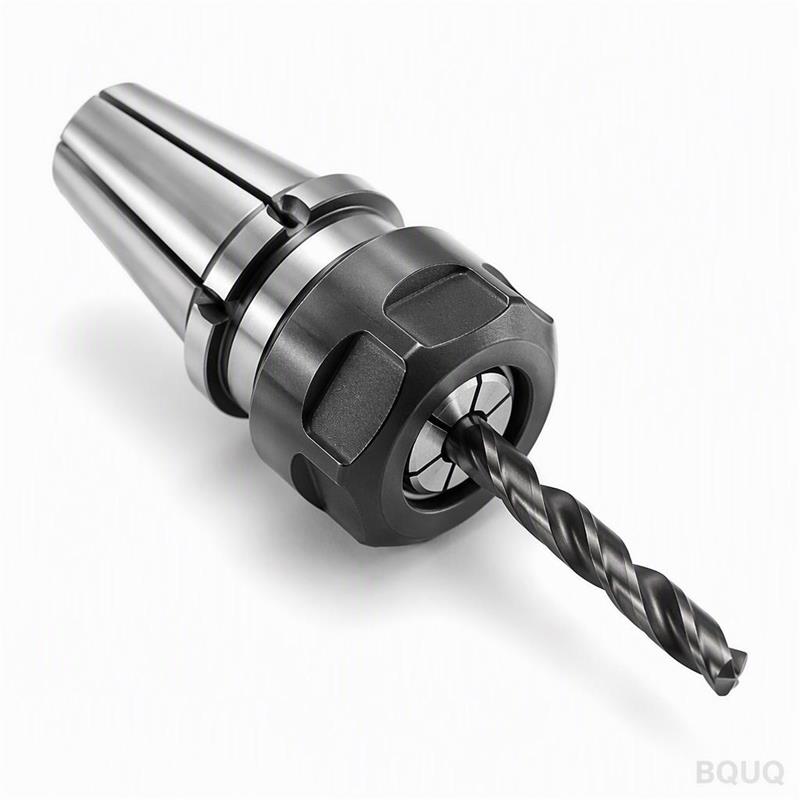
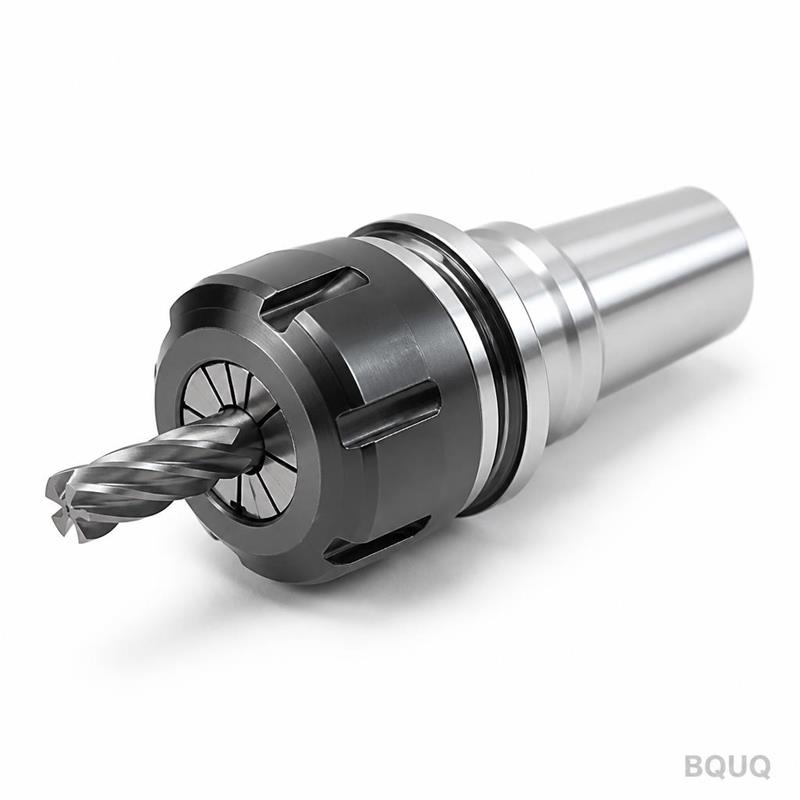
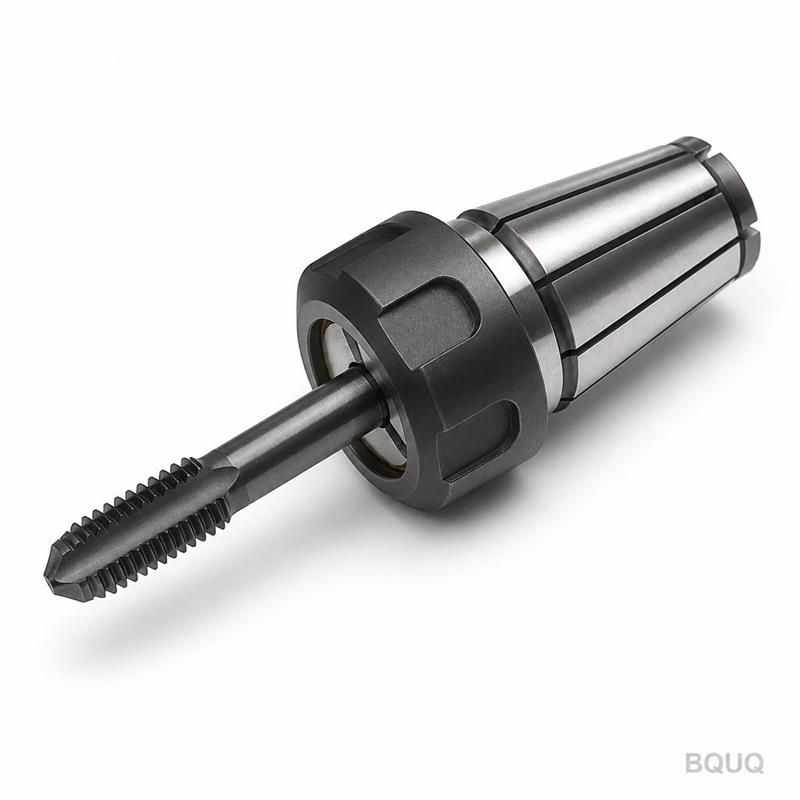
We machine these extension bars in four standard collet sizes. ER11 for tool diameters 1–7 mm, ER16 for 1–10 mm, ER25 for 1–16 mm, ER32 for 2–20 mm. Shank options are straight cylindrical (Ø20, Ø25, Ø32 mm) or SK30/SK40/SK50 taper for direct spindle mount. Reach lengths from 50 mm to 150 mm in 10 mm steps. If you need a non-standard length, we cut it from solid bar — no extra tooling cost.
Specification
Value
Collet Size (ER series)
ER11 / ER16 / ER25 / ER32
Reach Length (extension bar)
50 mm – 150 mm (custom up to 200 mm)
Shank Diameter
Ø20 / Ø25 / Ø32 mm or SK30 / SK40 / SK50
Material
42CrMo4 or 20CrMnTi (case-hardened)
Hardness (collet taper)
58 – 62 HRC
Hardness (body)
50 – 55 HRC
Runout (TIR at nose)
≤ 0.005 mm
Surface Finish (taper)
Ra 0.4 µm
Concentricity (collet seat to shank)
≤ 0.008 mm
Lead Time (standard sizes)
7 days
MOQ
No MOQ (1 piece accepted)
Inspection Before Every Shipment – Not a Random Sample
Every single extension bar is checked, not one per batch. We measure taper angle with a CMM (coordinate measuring machine) at 3 points. Runout is verified on a precision mandrel with a 0.001 mm dial indicator. Hardness is spot-checked on both the taper and body using a Rockwell tester. We send the inspection report with your shipment — PDF and photo of the actual part.
Balancing and Pre-Set Options for High Speed Machining
If your spindle runs above 8,000 RPM, order the G2.5 balancing option. We dynamically balance the assembled chuck (body + collet nut) at 15,000 RPM. The balance grade is G2.5 per ISO 1940. We also offer pre-set tool length offset — we measure the stick-out from the collet nose and engrave the value on the shank. This saves you 3–5 minutes per tool change on the machine.
How This Compares to a Welded or Screwed Extension
A welded extension has a heat-affected zone that softens the steel. A screwed extension has threads that create micro-movement under load. Our bar is machined from a single forging. There is no joint, no weld bead, no thread gap. The collet taper is ground in the same setup as the shank, so the two axes are true to each other. That is why we hold 0.005 mm runout without adjustment.
What is the minimum order quantity?
No MOQ – we accept one piece for prototype testing or emergency replacement.
Can you make a non-standard reach length or shank size?
Yes, any length between 50 mm and 200 mm, and any shank diameter from Ø16 to Ø40 mm, with no custom tooling fees.
How do you verify runout before shipping?
We measure TIR on a 100 mm test bar clamped in the collet, with a 0.001 mm dial indicator, and include the reading in the inspection report.
What is the typical lead time for a custom order?
Standard sizes ship in 7 days, custom lengths in 10–12 days, and orders with balancing option add 2 days.
Send Your Drawing for a Firm Quote Within 12 Hours
We know you need a part that fits your spindle and your pocket. Email your drawing or a simple sketch with your ER size, reach length, and shank type to sc@bquq.com. You get a firm price and a delivery date within 12 hours (working days). For urgent questions, WhatsApp +86 13713157787. If you are still deciding between tool holder types, read our CNC cutting tool selection guide. For tolerance questions on the shank or collet seat, check our CNC machining tolerances guide.
This is precision manufacturing, made in China, with no MOQ and no middleman. We are the factory — 20 years in Dongguan, CNC machining plus stamping and springs. You talk to the engineer who will quote your part, not a sales rep.