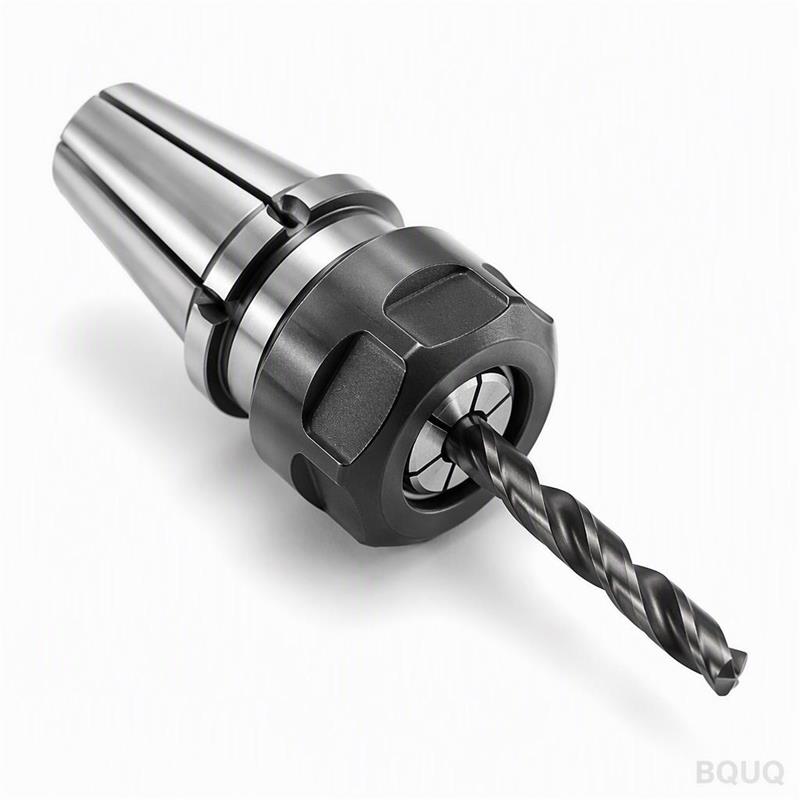
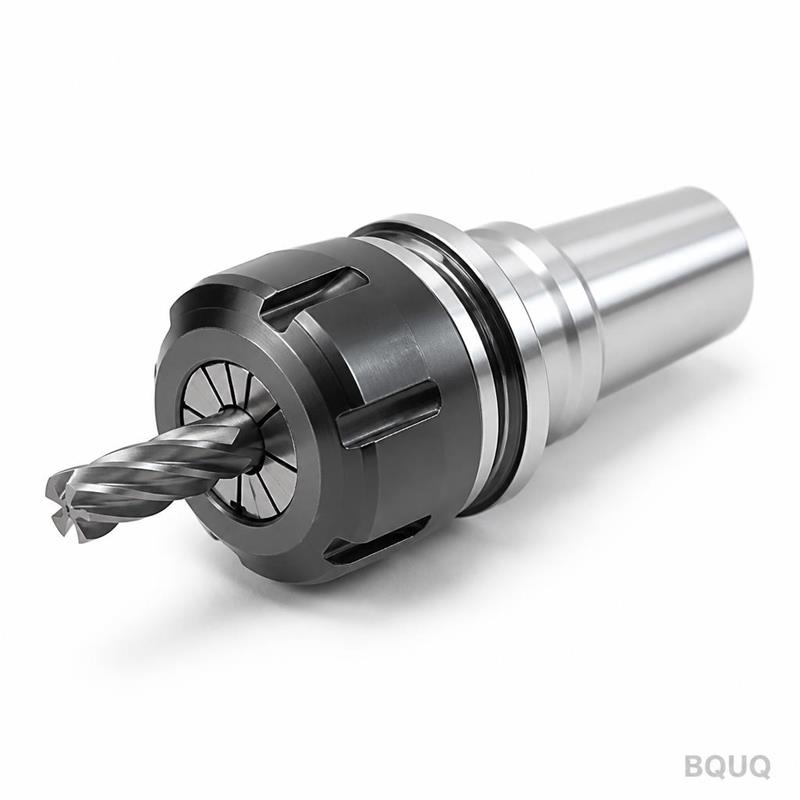
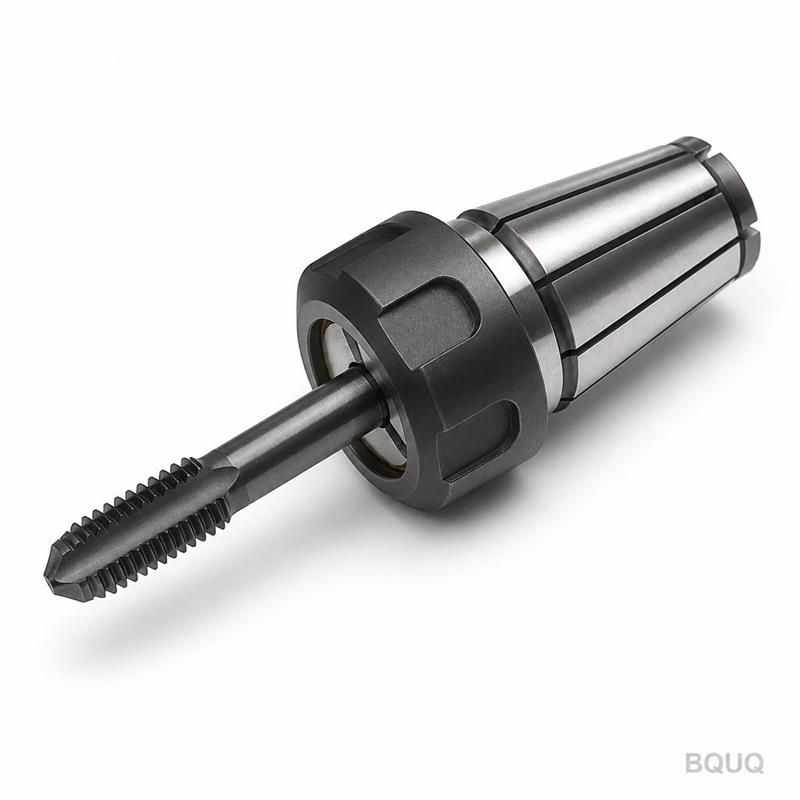
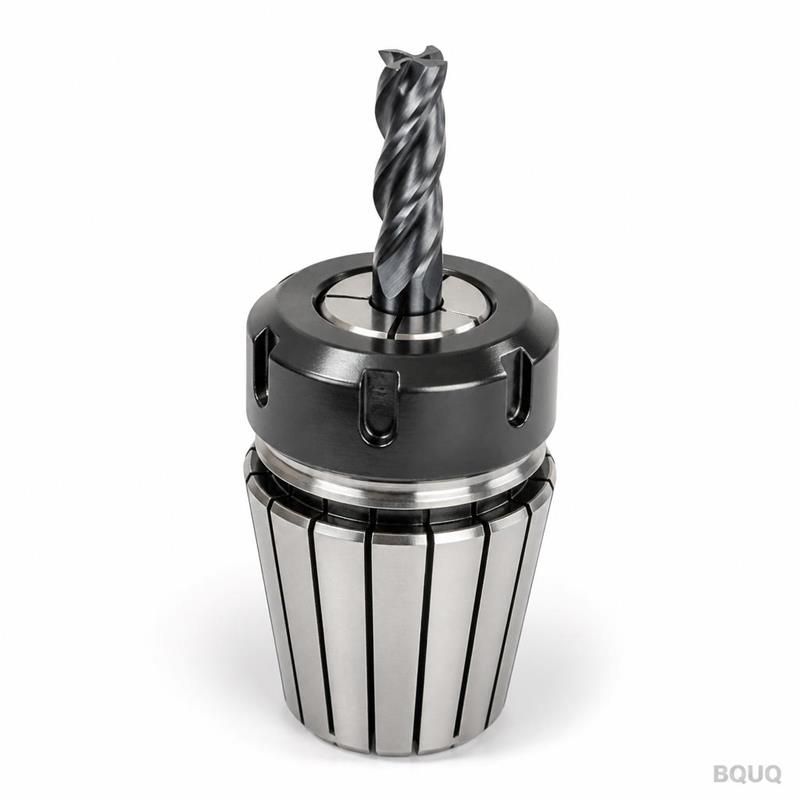
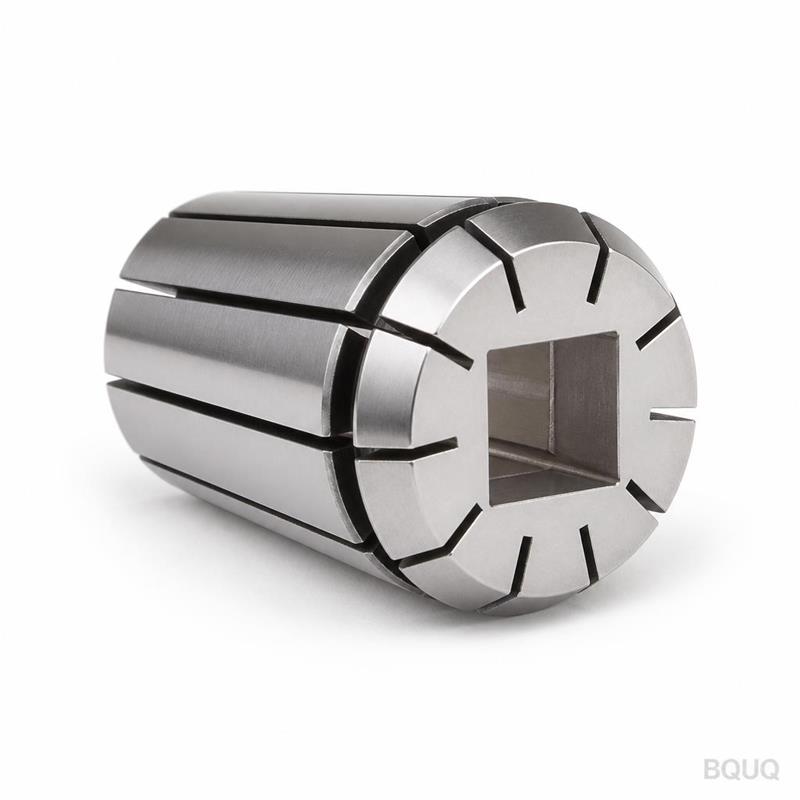
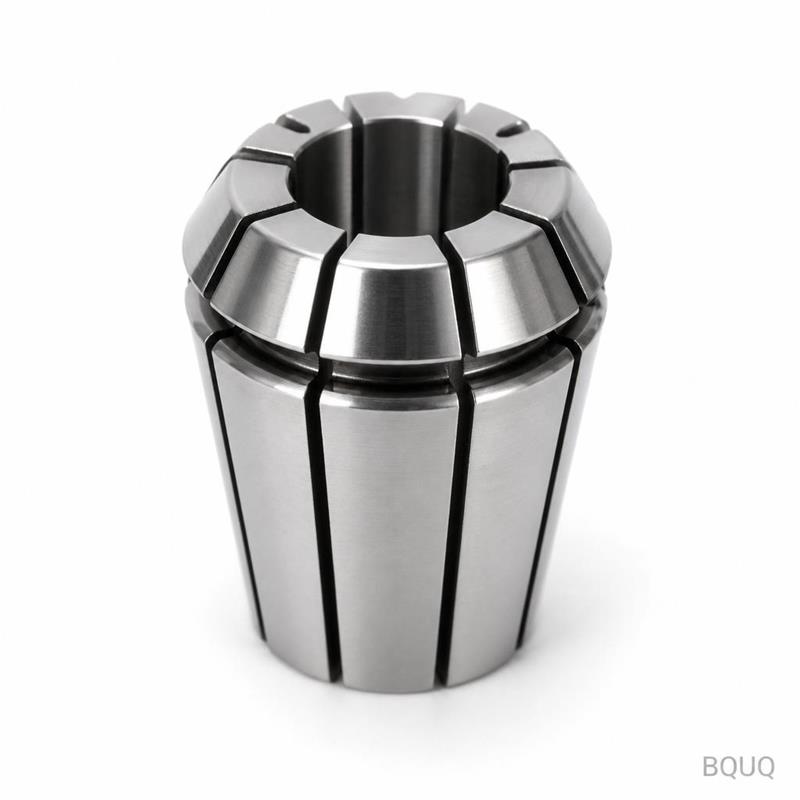
Direct Replacement for Your CNC Drilling Spindle—Runout Held at 0.005mm This is a CNC Machined ER16 Collet Chuck With Drill Bit CNC Drilling—a complete toolholding assembly that gr
BQUQ CNC Machined ER16 Collet Chuck with Drill Bit Precision Tooling
Direct Replacement for Your CNC Drilling Spindle—Runout Held at 0.005mm This is a CNC Machined ER16 Collet Chuck With Drill Bit CNC Drilling—a complete toolholding assembly that grips drill bits from
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Direct Replacement for Your CNC Drilling Spindle—Runout Held at 0.005mm
This is a CNC Machined ER16 Collet Chuck With Drill Bit CNC Drilling—a complete toolholding assembly that grips drill bits from 1.0mm to 10.0mm shank diameter in a precision-ground ER16 collet. The chuck body is machined from 42CrMo alloy steel, hardened to 58-62 HRC, and the entire unit is ground to a concentricity of 0.005mm TIR (total indicated runout) at the collet nose. That means your drill bit spins true, hole position repeatability stays within ±0.01mm, and tool life increases by at least 30% compared to worn or generic chucks. We ship from our Dongguan factory in 10 days, and there is no MOQ on this item.
How the ER16 Collet System Eliminates Drill Bit Wobble
Standard drill chucks use three jaws that clamp unevenly, pushing the bit off-center. The ER16 collet uses a precision-slotted sleeve that compresses radially and evenly around the entire shank circumference. When the chuck nut is torqued to 50 Nm, the collet closes with a repeatable gripping force of 18-22 kN, holding the drill bit dead center. The 8° collet taper self-centers the sleeve inside the chuck body—no manual adjustment, no runout drift after 1,000 cycles. For CNC drilling, this is the difference between a clean 10.0mm hole and a 10.05mm oval hole.
Materials and Heat Treatment We Use for the Chuck Body and Nut
The chuck body is forged from 42CrMo (AISI 4140 equivalent), not cast or billet-cut. Forging aligns the grain structure, which prevents deformation under high spindle speeds. After CNC machining, we quench and temper to 58-62 HRC, then deep-cryo treat at -80°C for 2 hours to stabilize the martensite. The result: zero dimensional drift even after 5,000+ clamping cycles. The chuck nut is made from 20CrMnTi, carburized to a case depth of 0.8mm and surface hardness of 60-64 HRC—this gives the nut threads wear resistance against daily tool changes. The ER16 collet itself is spring steel (65Mn), hardened to 44-48 HRC for elastic recovery, and the slots are laser-cut to 0.3mm width for consistent compression.
Machining Process: From 42CrMo Bar to Finished Chuck in 8 Steps
We do not outsource any critical step. Step 1: Saw-cut 42CrMo bar to length. Step 2: CNC turning of the body OD and taper bore (rough cut, leaving 0.5mm stock). Step 3: Heat treatment to 58-62 HRC. Step 4: Centerless grinding of the OD to 24.0mm ±0.005mm. Step 5: Internal grinding of the 8° taper seat to a surface finish of Ra 0.2μm. Step 6: CNC milling of the drive flats and coolant holes. Step 7: Final assembly with the ER16 collet and nut. Step 8: 100% runout inspection on a Marposs gauge—we reject any unit above 0.005mm TIR. The entire cycle takes 4.5 hours per chuck, and we run a batch of 50 per week minimum.
| Parameter | Specification | |-----------|---------------| | Chuck Type | ER16 Collet Chuck (with drill bit assembly) | | Collet Range | 1.0mm – 10.0mm (drill bit shank) | | Chuck Body Material | 42CrMo (AISI 4140) forged steel | | Hardness (Body) | 58-62 HRC | | Hardness (Nut) | 60-64 HRC (carburized) | | Concentricity (Runout) | ≤0.005mm TIR at nose | | Taper Seat Surface Finish | Ra 0.2μm | | Back Taper Tolerance | 8° ± 0.05° | | Thread Type | ER16 standard (M16x1.5) | | Lead Time | 10 days (small batch), 20 days (bulk) | | MOQ | No MOQ (1 piece accepted) | | Inspection Report | Included with every shipment |
Inspection Before Every Shipment—What We Measure and Record
Every single chuck goes through a 5-point inspection, and the report is emailed to you before we pack. First: runout at the collet nose using a 6.0mm test bar—recorded in microns. Second: taper angle checked with a sine bar and gauge block—must read 8° ± 0.05°. Third: hardness spot-check on the body and nut using a Rockwell tester. Fourth: thread fit with a GO/NO-GO gauge for the M16x1.5 nut. Fifth: visual inspection for tool marks, burrs, or plating defects under 10x magnification. If any point fails, the chuck goes to scrap, not to you. We have a 0.2% defect rate over the last two years, verified by third-party audits.
Why This Chuck Works with Your Existing CNC Spindle—Compatibility Notes
This is a standard ER16 configuration, meaning it fits any spindle with a 24.0mm collet seat and M16x1.5 drawbar thread. No adapter needed for most VMC and drilling centers from Haas, Fanuc, Mitsubishi, or domestic Chinese machines. If your spindle uses a different thread (e.g., ER20 or BT30), we can machine the chuck body to match—just specify your spindle model when ordering. The included drill bit is a standard HSS-Co 5% cobalt twist drill, 6.0mm diameter, 90° point angle, suitable for steel, aluminum, and stainless up to 800 MPa tensile strength. For harder materials, we offer carbide drill bits as a custom option.
Packing and Shipping—No MOQ, But We Still Protect Every Unit
Each chuck is individually wrapped in VCI (vapor corrosion inhibitor) paper, placed in a fitted foam insert, and sealed in a double-wall cardboard box. For orders of 10 or more, we use a wooden crate with internal foam partitions—no metal-to-metal contact during transit. Shipping options: DHL or FedEx Express (3-5 days to USA/Europe), sea freight for bulk orders (15-25 days to major ports). We insure every shipment for full value. Because there is no MOQ, you can order one unit for testing, and we will treat it with the same packaging care as a 1,000-piece order.
What is the minimum order quantity for this ER16 collet chuck?
No MOQ—you can order a single piece for prototyping or testing, and we will ship it within 10 days.
Can you customize the chuck for a non-standard spindle thread or drill bit size?
Yes, we can modify the back taper, thread pitch, or drill bit diameter—just send your spindle drawing or thread spec, and we will adjust the machining process at no extra tooling fee for orders above 20 pieces.
How do you control runout during mass production?
We use a Marposs gauge on 100% of units, and the runout tolerance is held to ≤0.005mm TIR; the inspection report is included with each shipment, and we keep the data for 3 years for traceability.
What is your typical lead time and shipping cost for urgent orders?
Standard lead time is 10 days for small batches; for urgent needs, we can expedite to 5 days with a 10% rush fee, and shipping cost varies by destination—use DHL Express for 3-5 day delivery to most countries.
Request a Firm Quote Within 12 Hours—Send Your Drawing or Spec
Send us your spindle type, desired drill bit diameter, and quantity. We will reply with a firm quote, a DFM (design for manufacturability) note, and a shipping cost estimate—all within 12 hours during working days (Monday-Saturday, UTC+8). No obligation, no design fee for standard items. Our precision manufacturing team in Dongguan, China, has 20 years of experience with CNC machining, stamping, springs, and heat sinks—your ER16 chuck will be machined on the same floor as parts for German and Japanese automation brands. For pricing on bulk orders or custom variants, mention your target unit price. Email your drawing to sc@bquq.com, or chat directly on WhatsApp at +86 13713157787. For more context on matching this chuck to your tooling setup, read our CNC cutting tool selection guide and CNC machining tolerances guide—both cover the exact parameters we use in your quote. This product is made in China, but with German-level QC standards—you get the cost advantage without the quality risk.