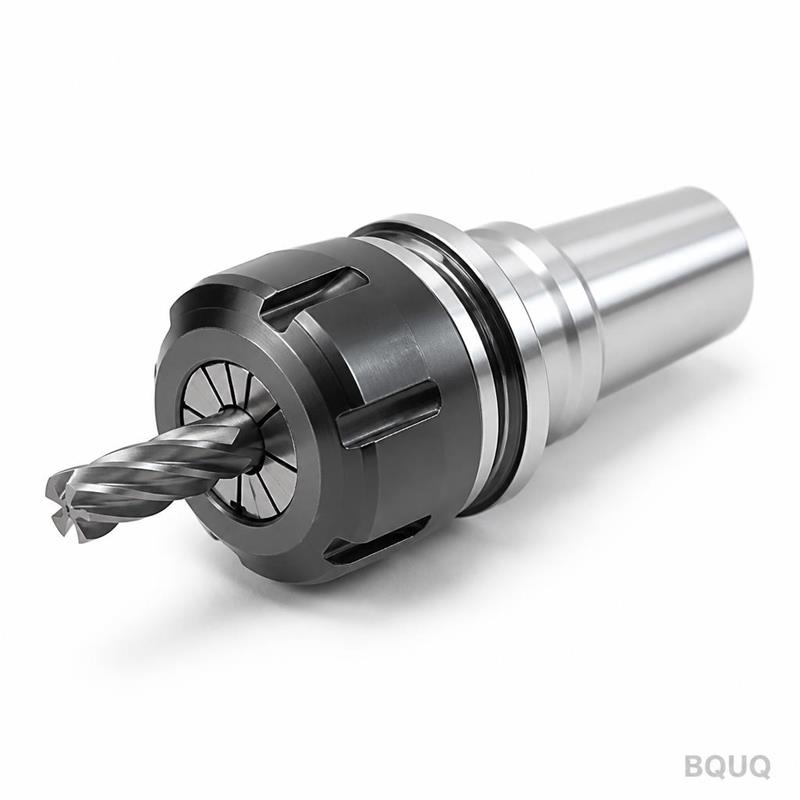
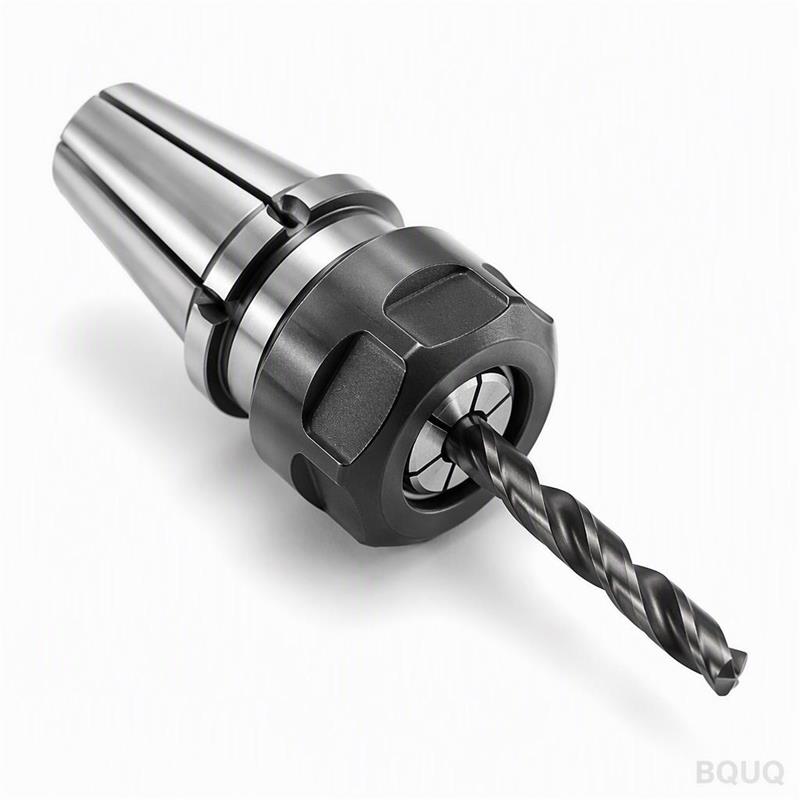
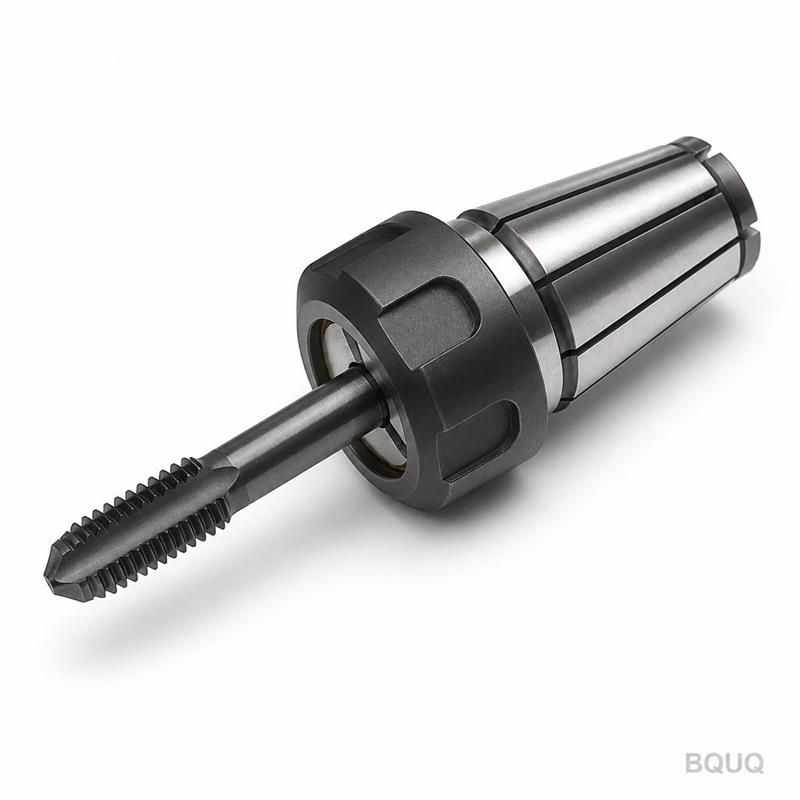
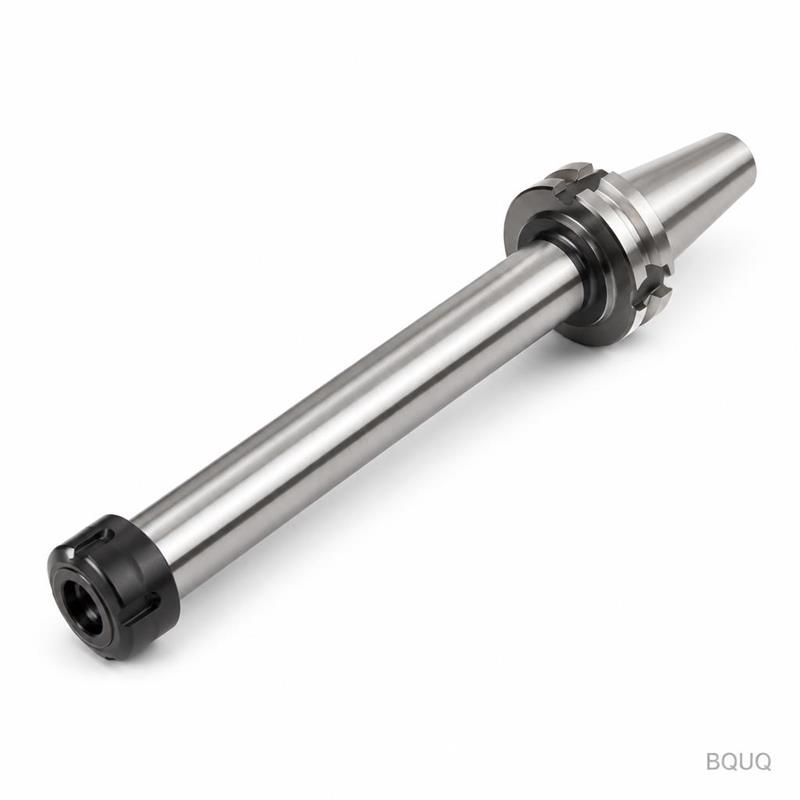
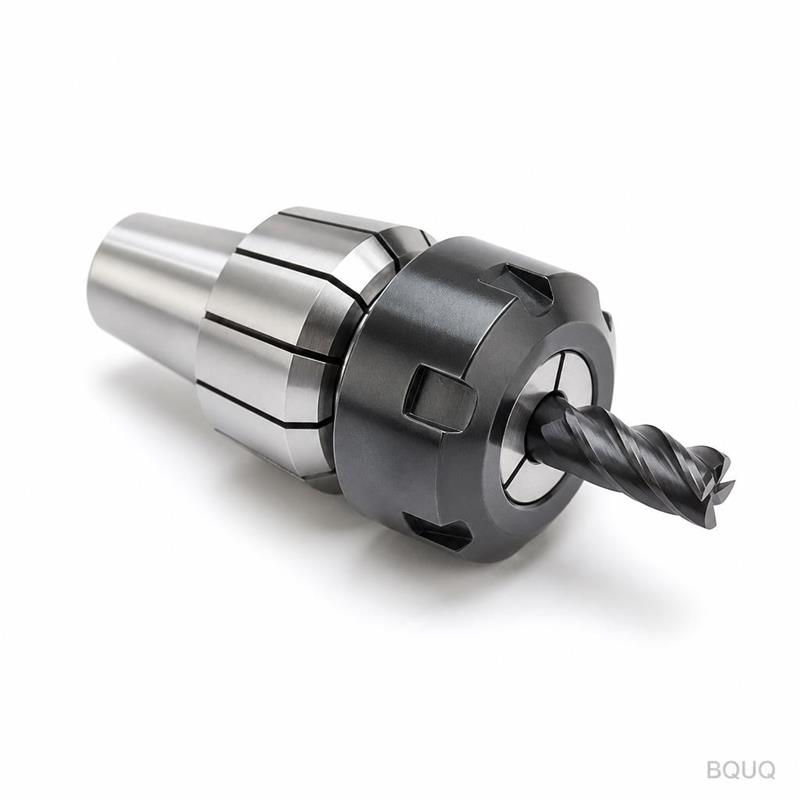
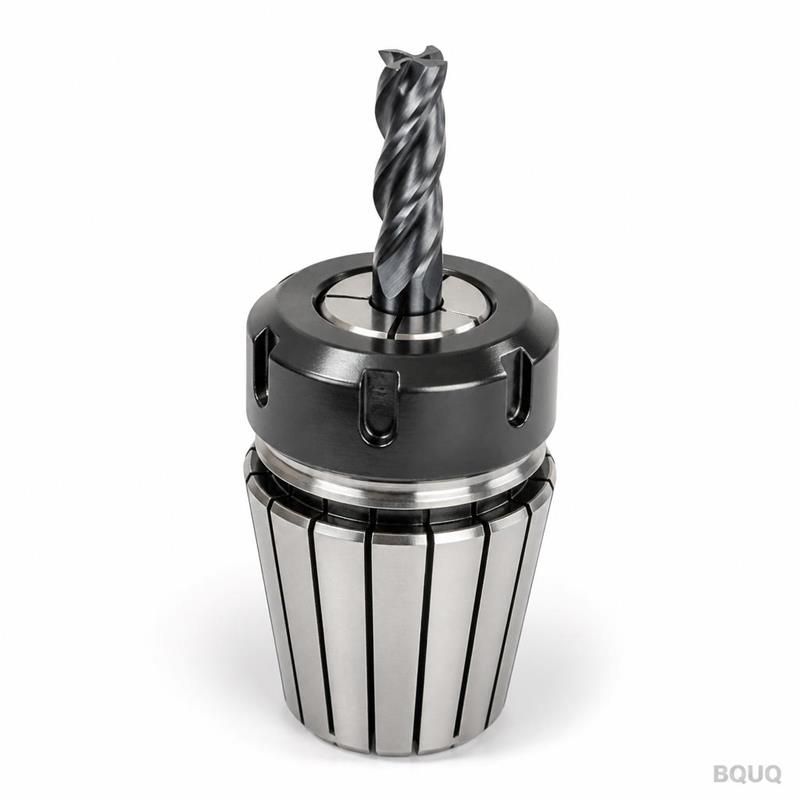
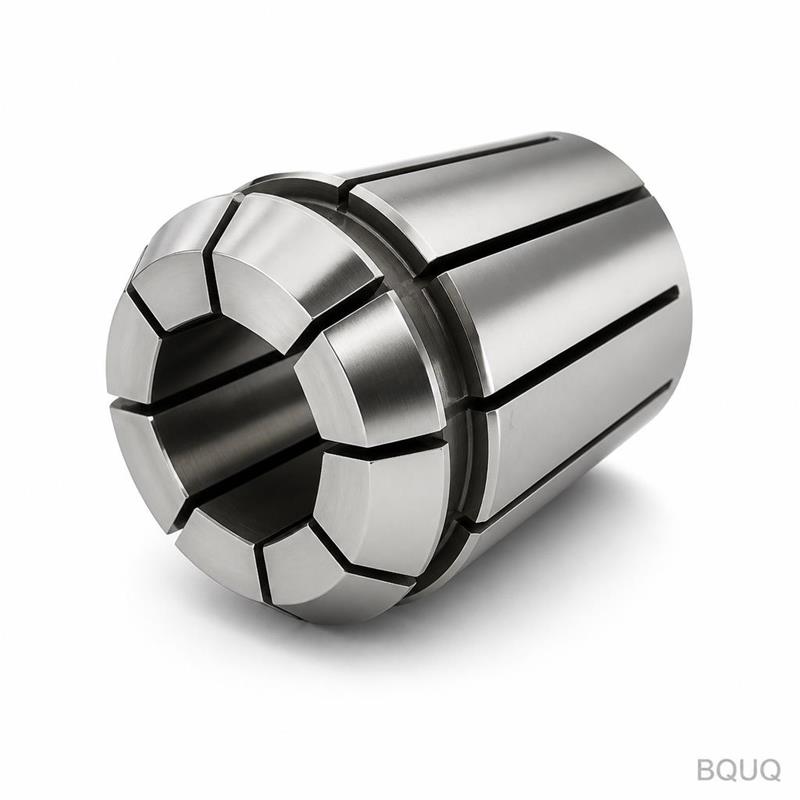
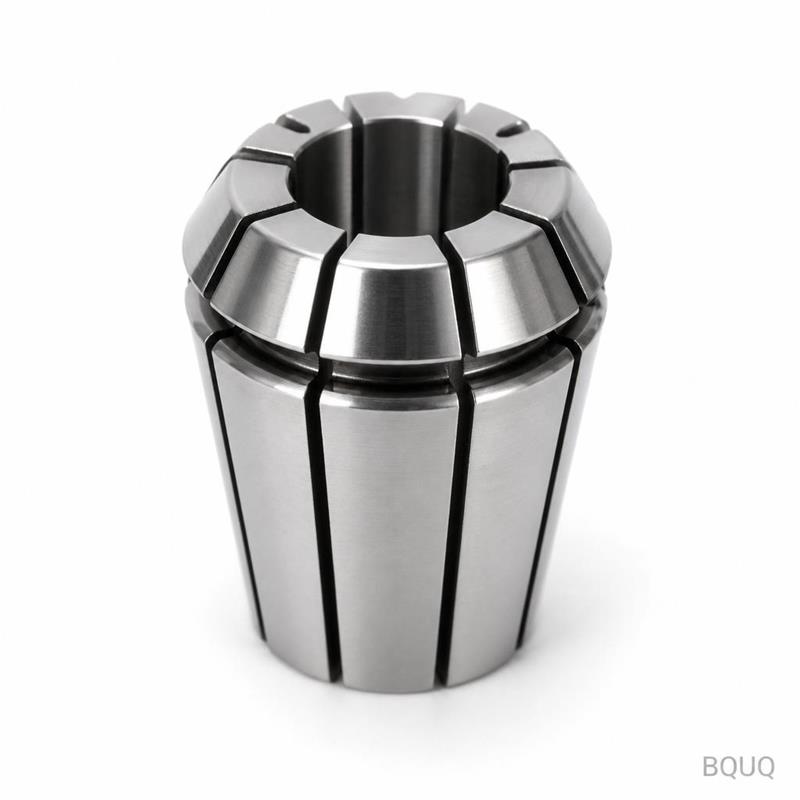
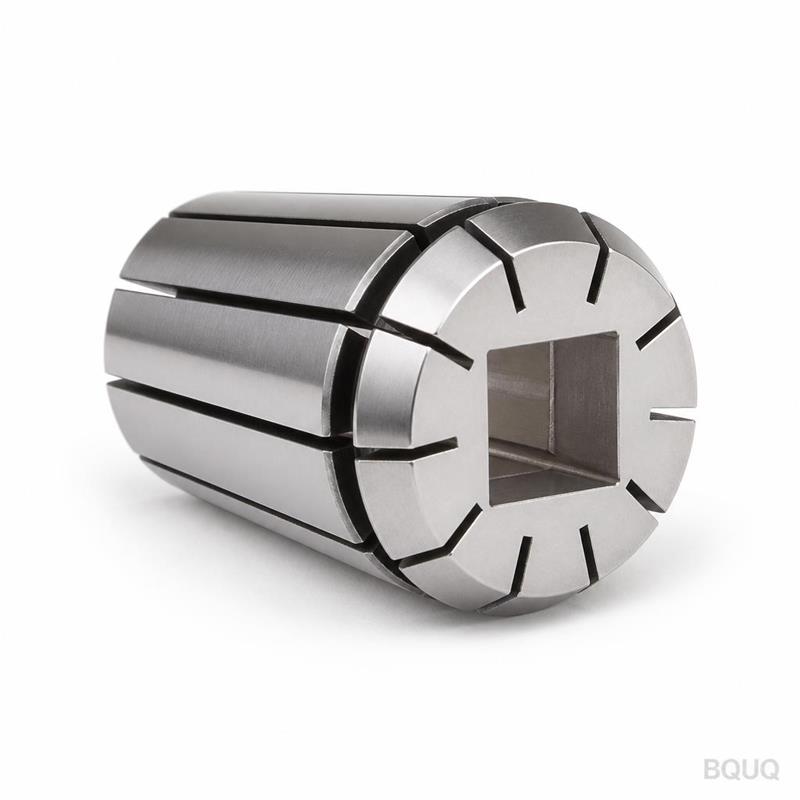
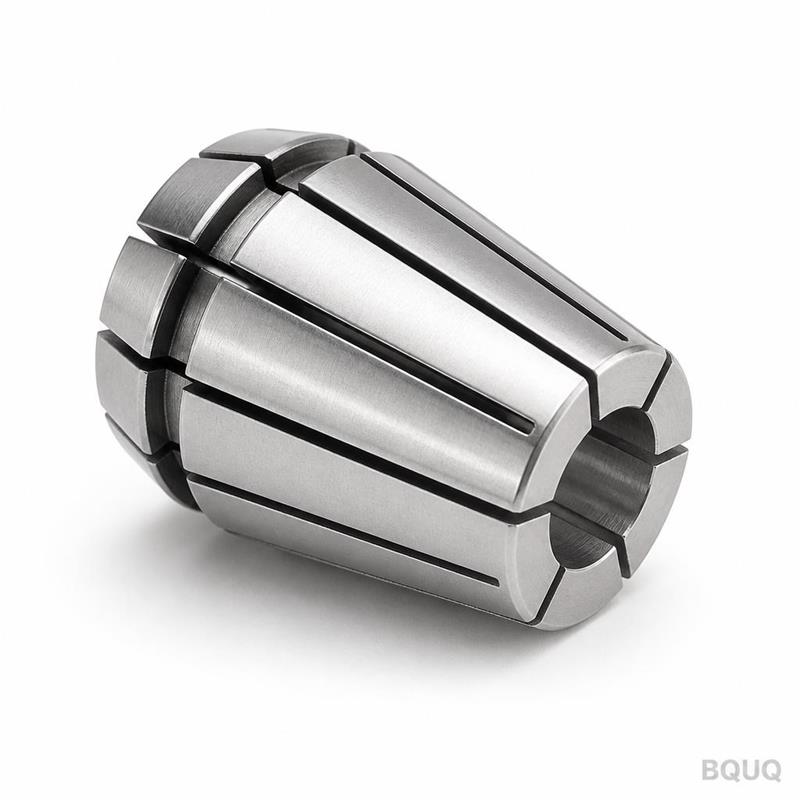
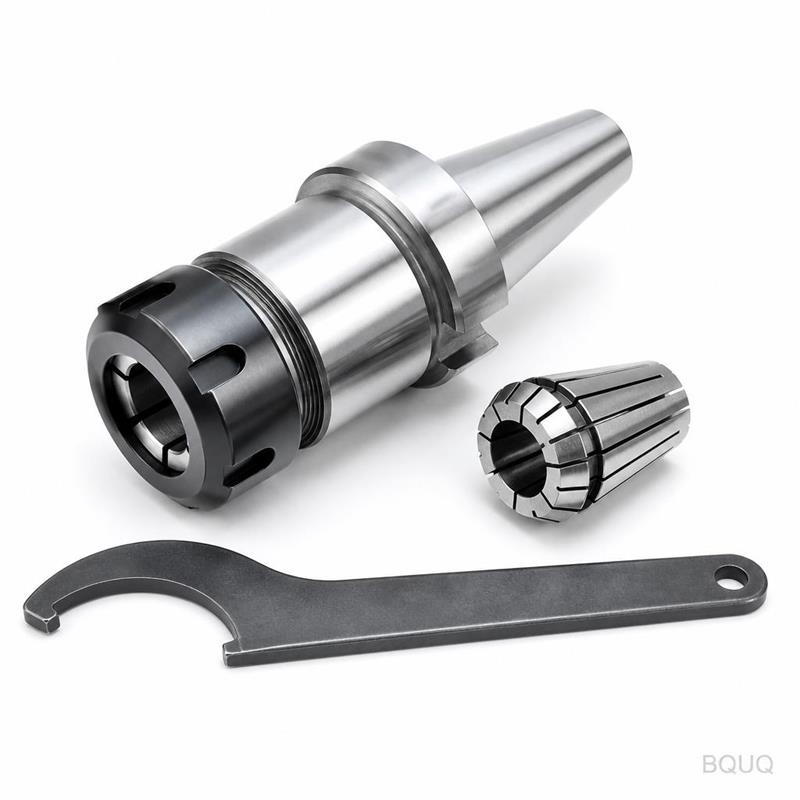
Custom CNC Machined ER32 Spring Collet Chuck for Reaming | BQUQ
OpeningYou need a collet chuck that holds a reamer true. Not a generic off-the-shelf part. You need one made to your drawing, with your bore size, your shank geometry, and your runout limits.We machin
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
You need a collet chuck that holds a reamer true. Not a generic off-the-shelf part. You need one made to your drawing, with your bore size, your shank geometry, and your runout limits.
We machine it from solid bar or forging. We verify it before shipment. Every unit is checked for concentricity and taper fit. If it does not pass, it does not ship.
We grind the internal taper after heat treatment. That is where the accuracy comes from. We do not skip stress relieving. We do not cut corners on the collet seat.
Three Reasons Buyers Send Us Their Drawings
1. Batch-traceable quality.
Every heat number is recorded. Every batch gets a unique code. If you have a problem six months later, we trace it back to the exact machine, operator, and material lot. No guesswork.
2. Inspection report per batch.
You get a full dimensional report with every shipment. Runout, taper angle, hardness, surface finish – all measured and documented. Not a generic certificate. Real numbers from our CMM and hardness tester.
3. One factory for CNC, stamping, springs, and heat sinks.
Your collet chuck is not an island. You may also need a spring for the release mechanism, a stamped washer, or a heat sink for the spindle motor. We make all of them under one roof. One purchase order, one shipping point, one quality standard.
Where These Parts Are Used
Our custom CNC collet chucks are not for hobby mills. They go into production environments where a 0.01 mm error costs money.
Automotive: Reaming valve guides and dowel holes in cylinder heads. High volume, tight cycle times.
Aerospace: Reaming fastener holes in aluminum and titanium assemblies. Material is expensive, scrap is not an option.
Medical devices: Reaming bone screws and implant drill guides. Surface finish and concentricity are critical.
Hydraulics: Reaming spool bores in valve bodies. A bad bore means leakage and warranty claims.
General machining: Any CNC lathe or mill where you need a rigid, accurate holder for a reamer or boring tool.
If you are reaming with a floating holder and getting taper or bell-mouth, the problem is often the chuck, not the reamer. A rigid, true-running collet chuck fixes that.
Q: Do you have a minimum order quantity?
A: No. We run one-piece prototypes and 10,000-piece production runs on the same machines. You pay a small setup fee for the first piece, but the unit price drops immediately with quantity.
Q: What tolerance can you actually hold on the taper and runout?
A: We hold AT3 taper accuracy per DIN 6499. Runout at the nose is ≤ 0.005 mm TIR with a master collet. If your drawing requires tighter, we can lap the taper to AT2 – but that adds 2–3 days and cost.
Q: What is your lead time for a custom design?
A: 7 working days for standard materials like 20CrMnTi. 12 working days if you need stainless steel or a special heat treatment cycle. We do not quote 3 weeks to buy time. We quote what we can deliver.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. We supply mill certificates for raw material and a heat treatment report with hardness curves. All documents are in English and can be notarized if your customer requires it.
Send Your Drawing
Stop guessing. Send us your 2D drawing or 3D model. We check it for manufacturability and send you a firm quote within 12 hours.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Include your target quantity, material, and required runout. We will confirm price, lead time, and inspection plan. No obligation, no pressure. Just a straight answer from a precision manufacturing shop in Dongguan.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.