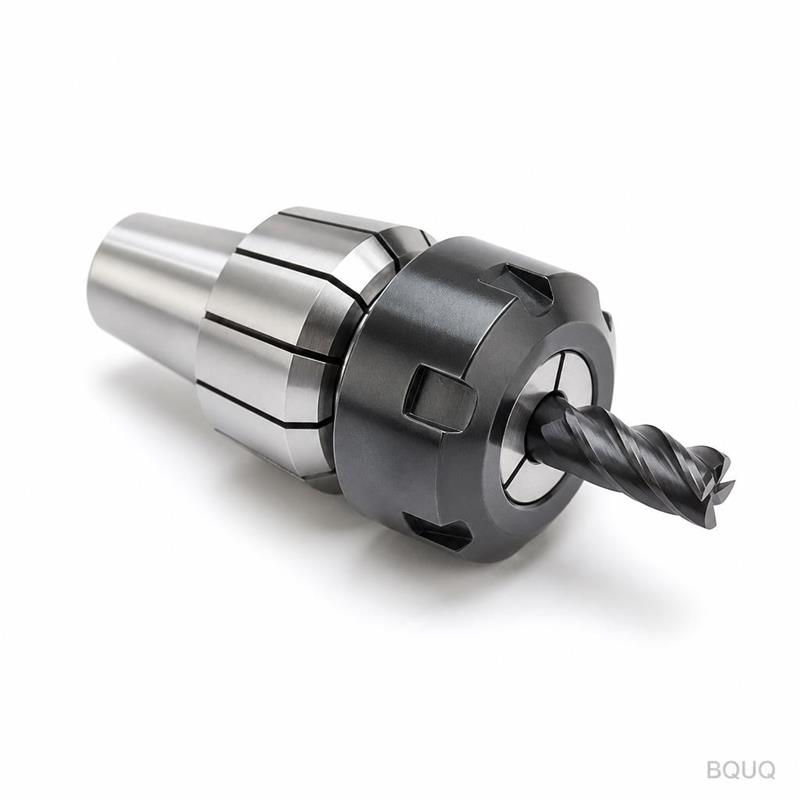
Product details
## Opening
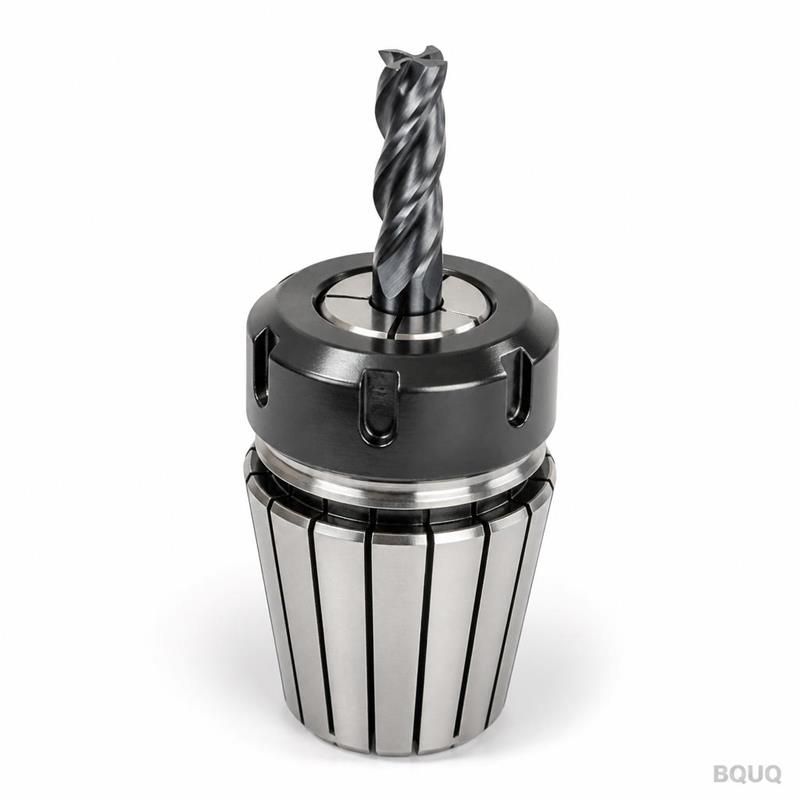
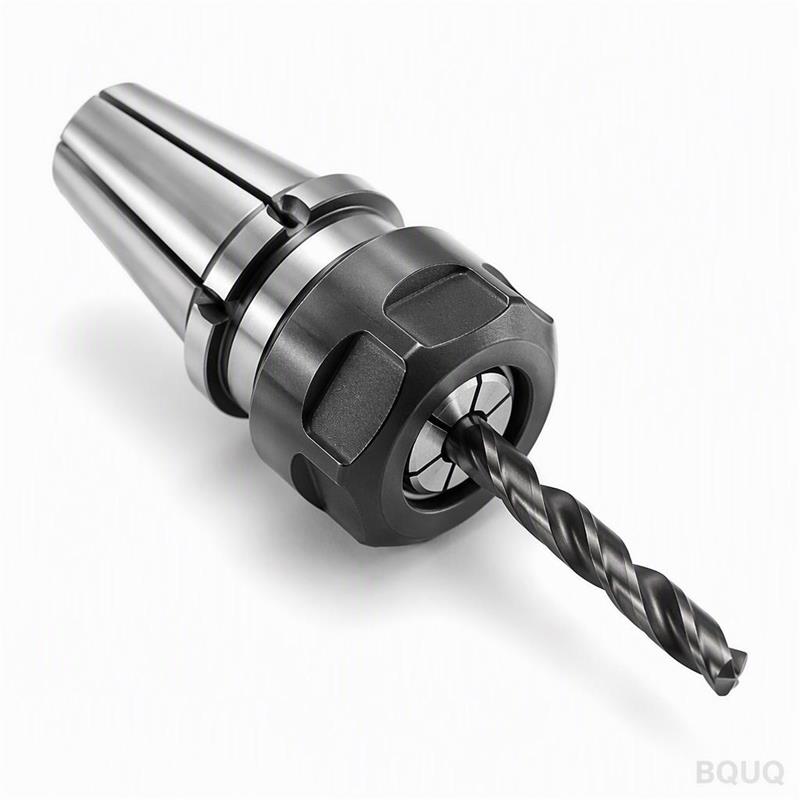
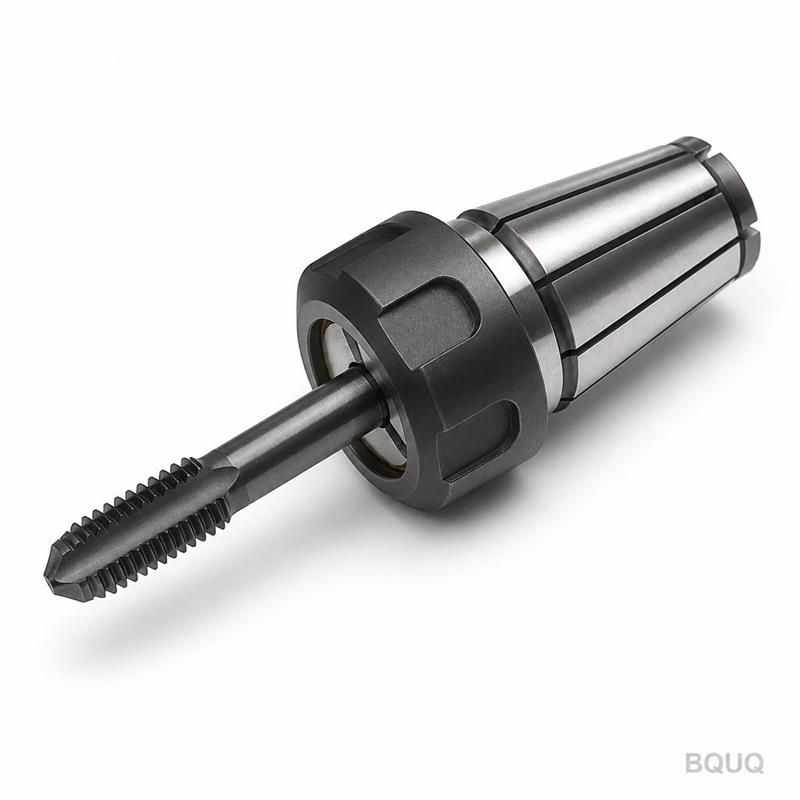
Your drawing becomes a finished ER25 collet chuck with runout held to 0.005 mm. We machine it from solid steel or stainless, harden it, and verify the taper and thread before it leaves our Dongguan factory. Every unit is measured, not sampled. You get the inspection report with the shipment.
- Tolerance: ±0.005 mm on critical diameters, 0.005 mm TIR on taper
- Lead time: 7–12 working days for prototypes, 15–20 days for production runs
- No MOQ: order one piece or ten thousand
- Material certs: EN 10204 3.1 available for every batch
- Made in China, shipped worldwide via DHL/UPS/FedEx
## Specifications
We build collet chucks on 5-axis CNC lathes and machining centers. The process is the same whether you need one prototype or a full production batch.
| Parameter | Value |
|---|
| Material options | 20CrMnTi, 40Cr, 65Mn, 304/316 stainless, A2 tool steel |
| Hardness | 58–62 HRC (case-hardened), 48–52 HRC (through-hardened) |
| Taper accuracy | AT3 or better per DIN 6499 / ISO 15488 |
| Runout (TIR) | ≤0.005 mm at nose, ≤0.010 mm at 4× diameter |
| Surface finish | Ra 0.4 µm on taper, Ra 0.8 µm on body |
| Threads | Ground after hardening, class 6H/6g |
| Slots | Wire-cut, width ±0.02 mm, no burrs |
| Coating options | Black oxide, TiN, or no coating as specified |
| Inspection | 100% taper gauge check, CMM report for critical dimensions |
| Batch size | 1 to 50,000 pieces, no tooling charge for standard sizes |
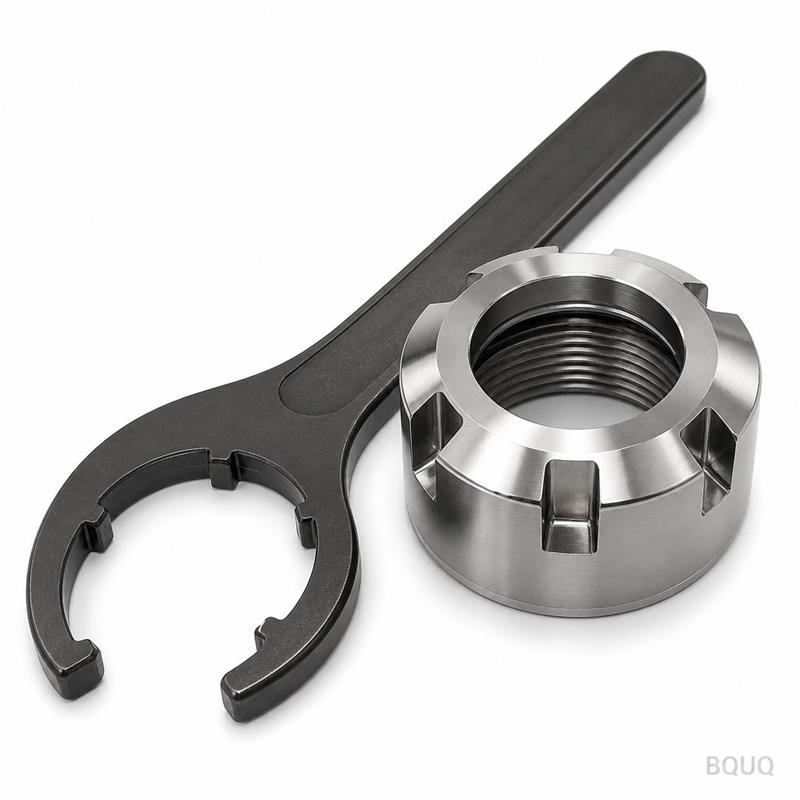
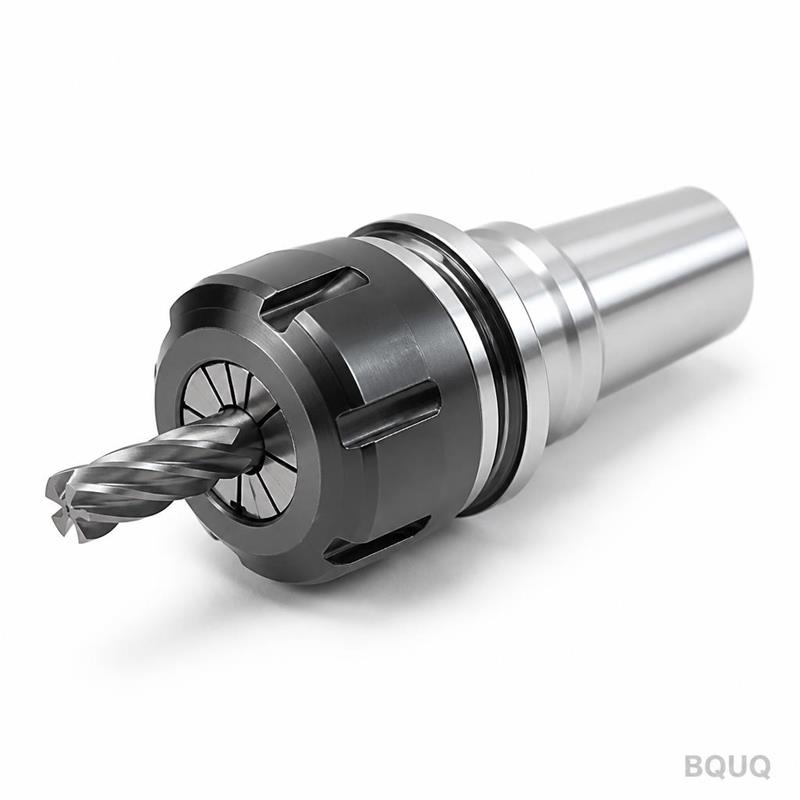
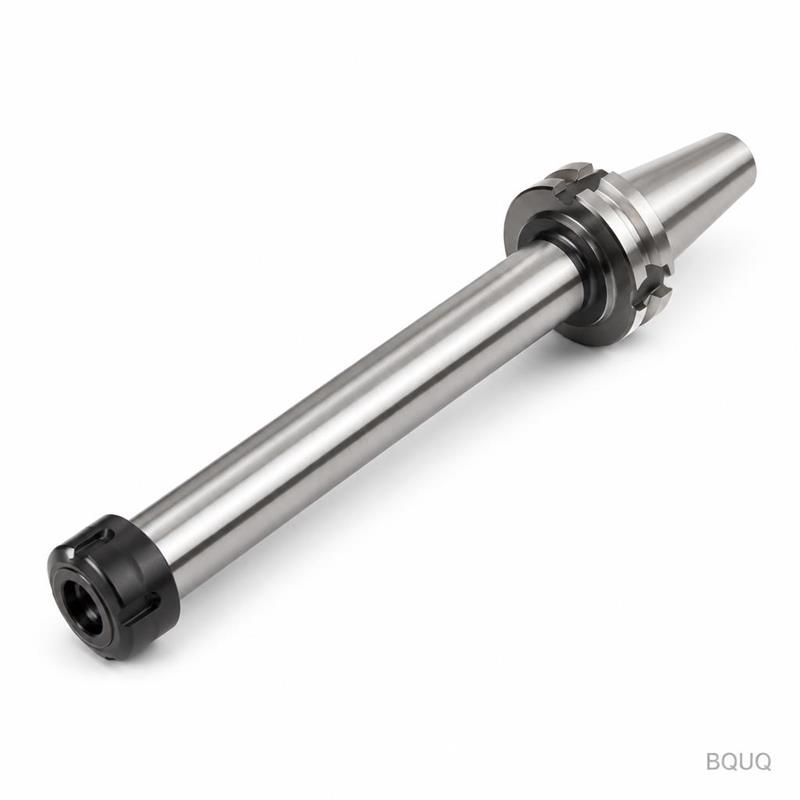
We also make the mating end mill holders and retention knobs. If you need a complete set, send the assembly drawing. We will match the pull stud thread and flange dimensions to your spindle.
## Three reasons buyers send us their drawings
1. Batch-traceable quality. Each collet chuck gets a unique serial number. The heat treatment furnace log, grinding wheel specs, and final inspection data are stored by that number. If a problem appears in your shop six months later, we pull the record and tell you exactly what was done. This is precision manufacturing you can audit.
2. Inspection report per batch. You do not have to trust our word. Every batch ships with a dimensional report: taper contact area, runout values, hardness readings, and thread pitch checks. For high-volume orders, we include SPC charts. Your incoming QC can verify our numbers in minutes.
3. One factory for CNC + stamping + springs + heat sinks. Your collet chuck is not the only part you need. We also run stamping presses, spring coiling machines, and heat sink extrusion lines. Send us a full BOM. We will quote the entire assembly, manage the tolerances between parts, and ship one consolidated order. Fewer vendors, fewer handoffs, fewer errors.
## Where these parts are used
ER25 collet chucks are not limited to end mills. Our customers use them in these real applications:
- CNC milling spindles – holding carbide end mills, drills, and reamers for aluminum and steel machining
- Automatic tool changers – with retention knobs for BT, CAT, or HSK spindles
- EDM and wire-cut machines – precise electrode holding where runout directly affects part geometry
- Robotic deburring cells – holding rotary burrs at high RPM, where balance matters
- Prototype shops – quick tool changes between operations, one chuck for multiple tool diameters
- Aerospace and medical contract manufacturing – where a 0.01 mm runout error scrapes a $500 part
The ER25 size covers tool shanks from 1 mm to 16 mm. That range makes it the most common collet system in job shops. We also make ER16, ER20, ER32, and ER40 to the same standards.
## Questions buyers ask before ordering
Q: What is the minimum order quantity?
A: No MOQ. We machine one piece for prototypes and small batches. For production, we offer tiered pricing – the unit price drops at 100, 500, and 1,000 pieces. Tooling is free for standard ER collet chuck designs. Custom designs may have a one-time setup fee, which we quote upfront.
Q: How do you guarantee tolerance and quality?
A: We grind the taper and bore after heat treatment. That removes distortion from hardening. Then we check every piece with a calibrated taper gauge and a CMM. The runout is measured at the nose and at 4× diameter. If any dimension is out of spec, the part is scrapped – not reworked. You receive the inspection report with the shipment.
Q: What is the lead time for custom CNC collet chucks?
A: Prototypes (1–5 pieces) ship in 7–12 working days. Production batches (100+ pieces) ship in 15–20 working days. For urgent orders, we can split the batch – ship the first 10 pieces in 5 days, the rest in 15 days. We will confirm the exact date when you send the drawing.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. We supply EN 10204 3.1 material certificates for steel and stainless. Heat treatment reports include hardness curves and furnace time-temperature charts. For aerospace or medical orders, we also provide full traceability documentation at no extra cost.
## Send your drawing
Email your PDF or STEP file to sc@bquq.com. Include the material, hardness, and any coating requirements. We will reply with a firm quote in 12 hours or less. For urgent discussions, message us on WhatsApp at +86 13713157787. We will review the design for manufacturability, point out any tolerance that is too tight for the application, and suggest a more cost-effective alternative if possible. No MOQ, no obligation, no marketing games – just a clear quote from a factory that has been doing this for 20 years.
Looking for a different part? We also machine Custom CNC Machined ER20 Collet Chuck with Carbide End Mill in the same Dongguan factory.
Related Products
parameter
| Parameter | Capability |
|---|
| Materials | AL6061/7075, SUS303/304/316, 45# steel, T2 copper, H59 brass, POM, PEEK, nylon |
| Tolerance | ±0.005mm standard, ±0.003mm on request |
| Machines | 3/4/5-axis CNC, turn-mill, Swiss lathe |
| Surface | Anodizing, nickel, zinc, passivation, sandblast, polish |
| Size Range | Max 400 x 300 x 200 mm |
| Prototype | 72 hours, no MOQ on samples |
| Inspection | Full report per batch, CMM data on request |