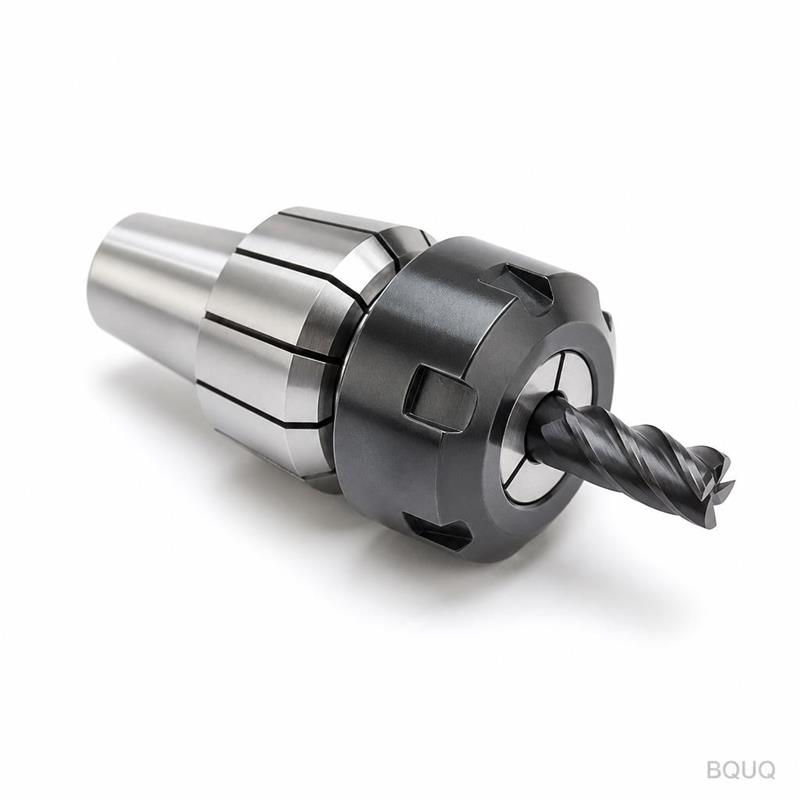
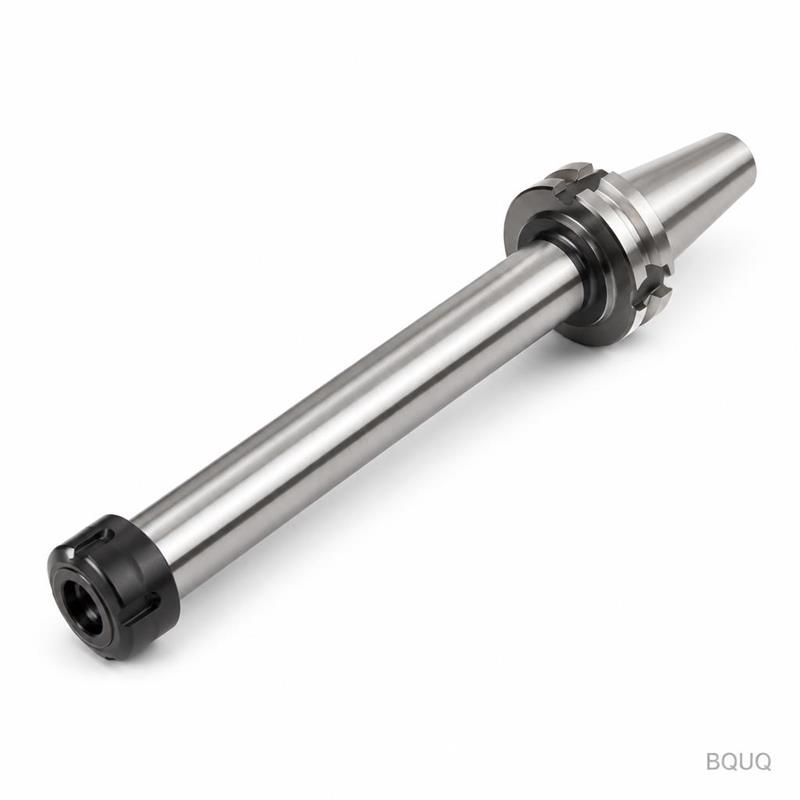
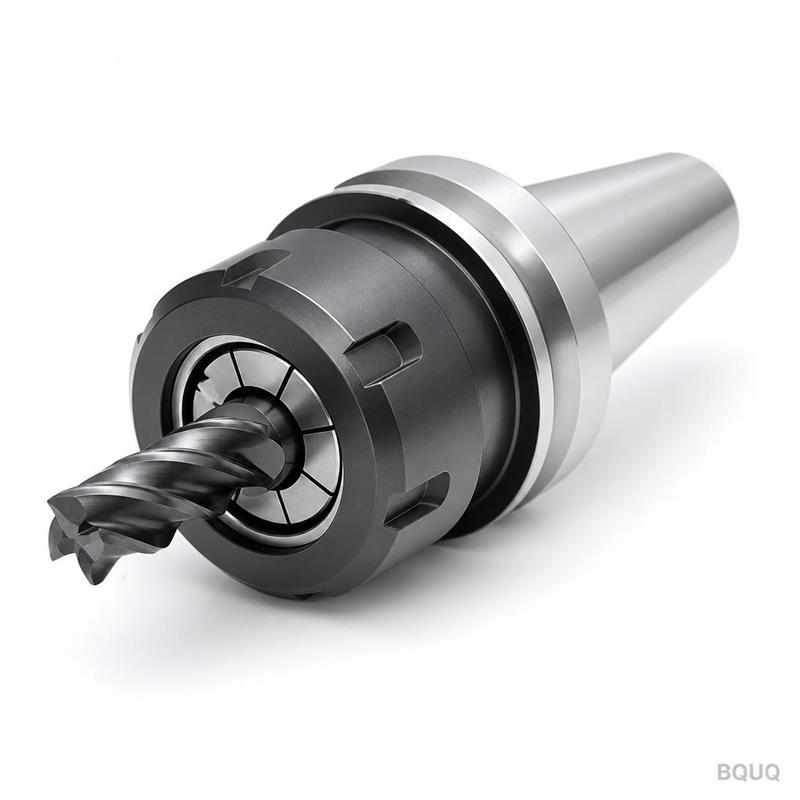
OpeningYour ER32 collet nut is not a shelf item. It is made to your drawing, with your thread pitch, your relief angles, and your hex or round profile. We machine it from bar stock
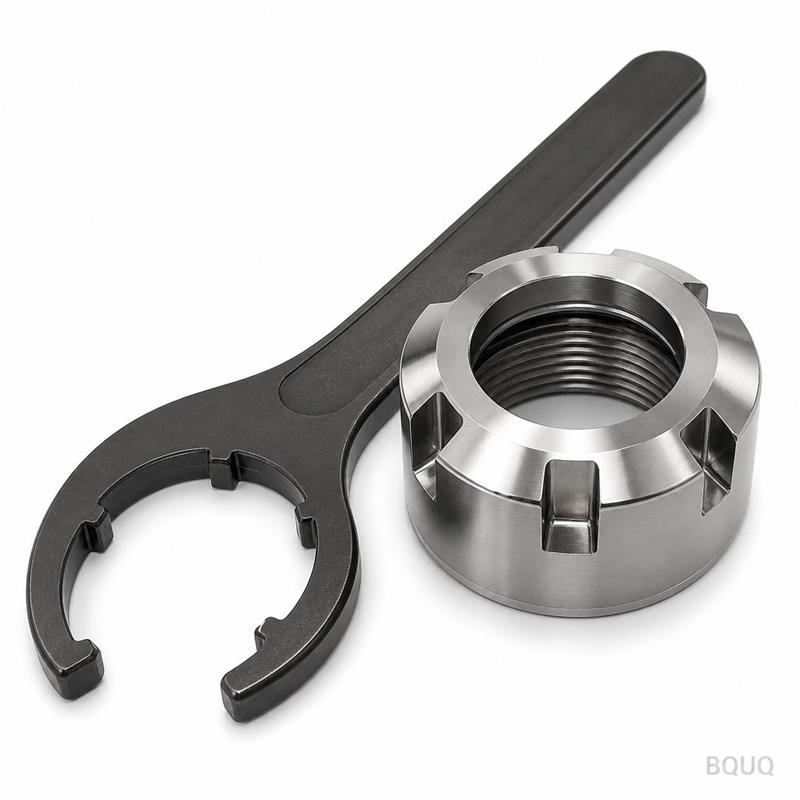
Custom CNC Machined ER32 Collet Nut with Spanner Wrench Tooling
OpeningYour ER32 collet nut is not a shelf item. It is made to your drawing, with your thread pitch, your relief angles, and your hex or round profile. We machine it from bar stock, verify the thread
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your ER32 collet nut is not a shelf item. It is made to your drawing, with your thread pitch, your relief angles, and your hex or round profile. We machine it from bar stock, verify the thread fit with a calibrated ER32 collet gauge, and check the wrench slot depth before it leaves the floor.
At a glance: Tolerance ±0.005 mm on thread pitch diameter, surface finish Ra 0.8 µm on sealing faces, lead time 7–10 days for standard steel, no MOQ—order one piece or one thousand.
We are a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining experience. You send the drawing. We send back a part that fits your spindle, not a compromise.
CNC turning, milling, drilling, broaching for wrench slots
Tolerance
±0.005 mm on thread pitch diameter, ±0.01 mm on wrench flats
Surface finish
Ra 0.8 µm on sealing faces, Ra 1.6 µm on wrench surfaces
Hardness (steel)
28–32 HRC for 4140, case-hardened 12L14 to 55 HRC on request
Wrench type
C-type spanner, pin spanner, or hex nut—per your tooling setup
Batch size
1 to 10,000 pieces, no MOQ, same process control
Inspection
100% thread gauge check, CMM report on request per batch
Lead time
7 days for standard steel, 10 days for stainless or hardened
We run these on Citizen sliding-head lathes and Fanuc-controlled turning centers. For high-volume runs, we switch to CNC multi-spindle machines. Every batch is traceable to the raw material lot number.
Three Reasons Buyers Send Us Their Drawings
1. Batch-traceable quality, not a lucky first piece.
Each heat number is recorded. Each batch gets a dimensional report. If you need to trace a failure back to the material, we can tell you the exact supplier and melt date. That matters when your spindle is running 20,000 RPM.
2. Inspection report per batch, included with every shipment.
You get a PDF with thread pitch diameter measurements, wrench slot width, and surface finish readings. No extra charge. No request needed. We do this because a collet nut that fails on the machine costs you more than the part itself.
3. One factory for CNC, stamping, springs, and heat sinks.
Your ER32 collet nut is a machined part. But your tooling package might also include a stamped retainer plate, a spring-loaded detent, or a heat sink for the spindle motor. We make all of those in the same building. One purchase order, one quality system, one shipping address. That reduces your supplier management time to zero.
Where These Parts Are Used
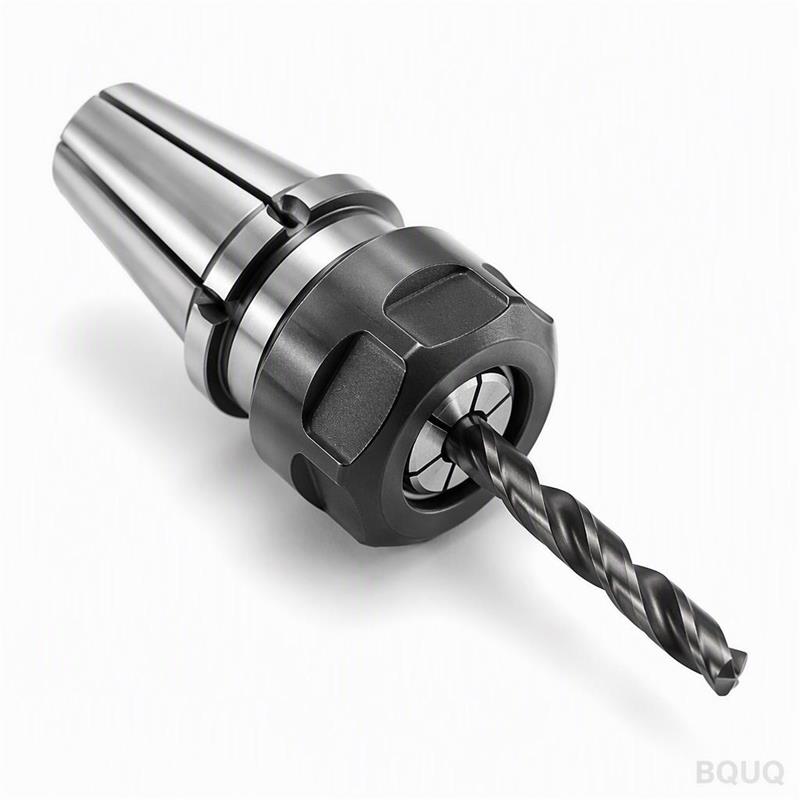
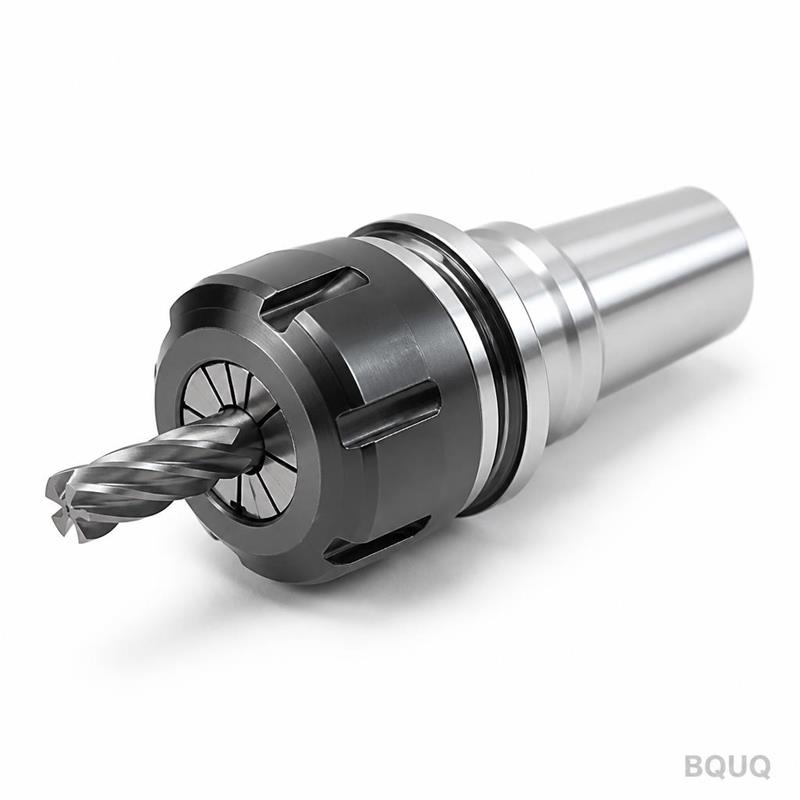
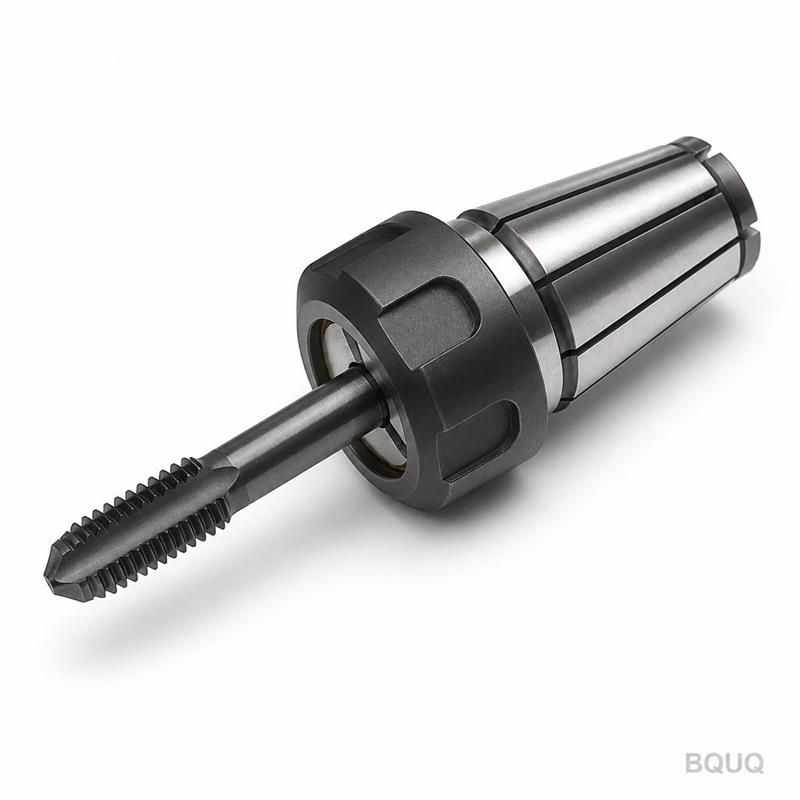
Our custom CNC collet chucks and ER32 collet nuts go into:
CNC milling spindles for tool clamping in vertical and horizontal machining centers.
CNC lathe live tooling where a compact collet nut is needed for clearance.
Automatic tool changers in high-volume production lines, where the nut must survive 100,000+ cycles without wear.
Precision grinding fixtures where runout below 0.005 mm is required for bearing seats.
Robotic deburring cells that use ER32 collets to hold end mills and deburring tools.
In each case, the nut is not a commodity. It is a precision interface between the spindle taper and the cutting tool. If the thread is off by a few microns, the tool pulls out. If the wrench slot is too shallow, the nut rounds off. We machine both features to your exact spec, so you do not have to think about them again.
Q: Do you really have no MOQ?
A: Yes. We machine one prototype for a tooling engineer testing a new spindle design, and we machine 10,000 pieces for a machine builder’s annual production. The setup time is the same. The price per piece drops with volume, but the quality standard does not.
Q: What tolerance can you hold on the thread and wrench flats?
A: Standard is ±0.005 mm on the pitch diameter, which is a class 4H fit for ER32. Wrench flats are ±0.01 mm. If you need tighter, we can grind the thread after turning to reach ±0.002 mm, but that adds 3 days to lead time.
Q: What is your typical lead time for a custom CNC collet chuck?
A: For a standard steel ER32 nut with a spanner wrench, 7 days from drawing approval to shipment. Stainless or hardened steel takes 10 days. If you need a rush, we can do 3 days for a small batch, but you pay a 20% expedite fee.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. Every batch ships with a mill certificate for the raw material and a heat treatment report if you specify hardening. We also include a dimensional inspection report per batch. All documents are in English and PDF format.
Send Your Drawing
Stop guessing whether a standard nut will fit your spindle. Send us your drawing, and we will machine an ER32 collet nut that fits exactly.
Firm quote in 12 hours. We reply with price, lead time, and process notes. No hidden fees, no surprises.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing, made in China, with no MOQ and full traceability. Your drawing is the only thing we need to start.