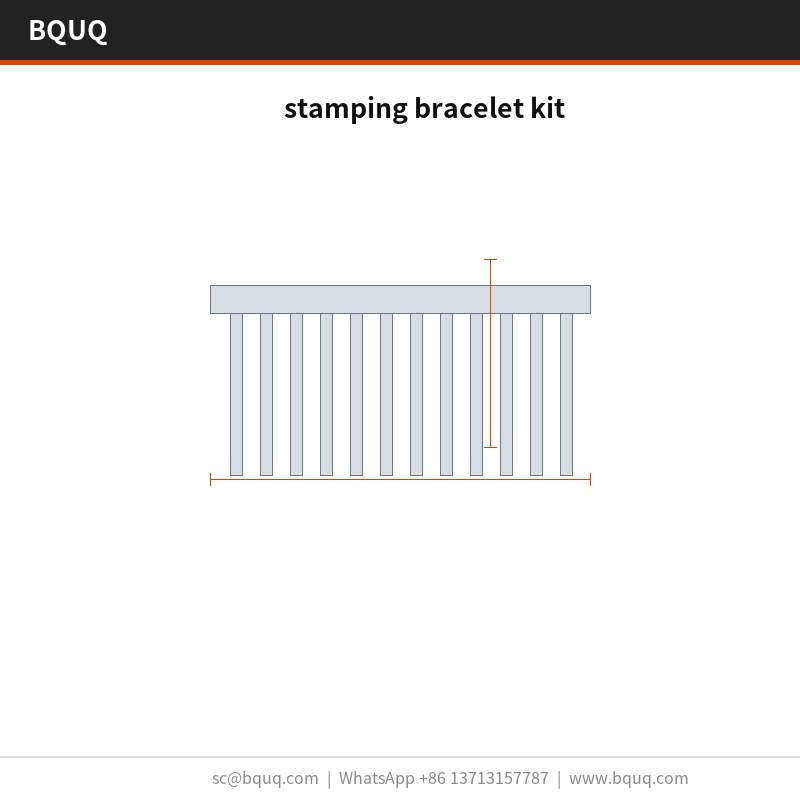
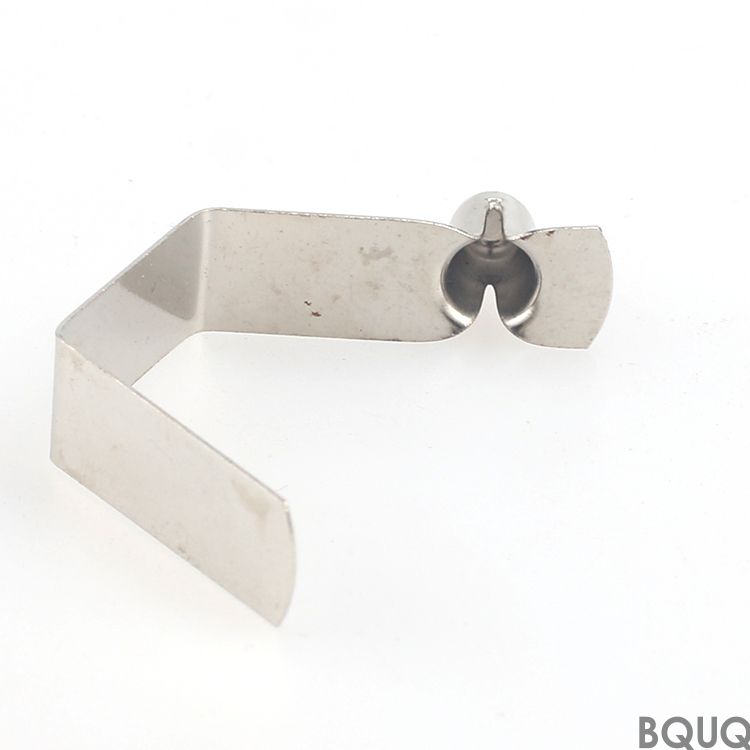
This stamping bracelet kit is a SECC 1.0 mm stamped heatsink with fins at pitch, delivering thermal performance at ΔT = 60 K. The one-piece die-formed construction holds flatness on the mounting face directly from the tool, keeps fin pitch within tolerance across the run, and supports powder coating RAL 9005. It suits network equipment volume programs where repeatable hole position and light weight matter.
This stamping bracelet kit covers in SECC 1.0 mm, with fins at pitch. Thermal performance is at ΔT = 60 K, confirmed by , with powder coating RAL 9005 available.
Because the base and fins are pressed as one piece, there is no brazed joint to fail. flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at rather than in the field.
Pressing SECC 1.0 mm keeps the stamping bracelet kit light, from depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
The standard material is SECC 1.0 mm, supplied with powder coating RAL 9005. For applications where network equipment exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Flatness is checked on a against a limit, and fin pitch is verified optically at . Reports go out with each lot.
Incoming SECC 1.0 mm is checked for thickness and hardness before it enters the press. After forming, confirms and against the drawing.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with on every first article. Deviations beyond trigger a full-lot sort.
We inspect fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
Where This Part Is Used
For network equipment builds, the mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Designers working on network equipment ask for flatness before they ask for thermal data, because network equipment assembly is automated and a non-flat base stops the line.
Can you customise the stamping bracelet kit for our application?
Yes. Send a drawing or a sample and we return a DFM note within 3 working days. Most network equipment customisations change , or the hole pattern, and all three are tooling changes on the existing press rather than a new machine.
What is the lead time for the stamping bracelet kit?
Prototype is from drawing approval; production is 25 working days after the first article is signed off. Tooling for a new part takes 20 working days. We quote , and sea freight to Europe runs about 25 to 30 days after booking.
General dimensions run to ; critical ones such as are held separately. Formed features inherit tooling repeatability of . If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
Do you make the stamping bracelet kit in different sizes?
The family covers , with unit weights from . Because the base is pressed, new sizes are a die insert change rather than a new press line, so development is usually 2 weeks rather than 8.
Can you supply the stamping bracelet kit pre-assembled?
Yes. We can add clips, screws or a fan shroud as a kitted assembly, with the parts bagged and labelled per set. This is common in network equipment programs and adds about 3 working days.
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so flatness is verified before the part is packed.
The factory holds ISO9001 and can ship RoHS and REACH documentation with the . Third-party SGS inspection is arranged on request before the container is sealed.
Production runs on cycles with in-line vision on . That is what keeps a commitment credible in peak season.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
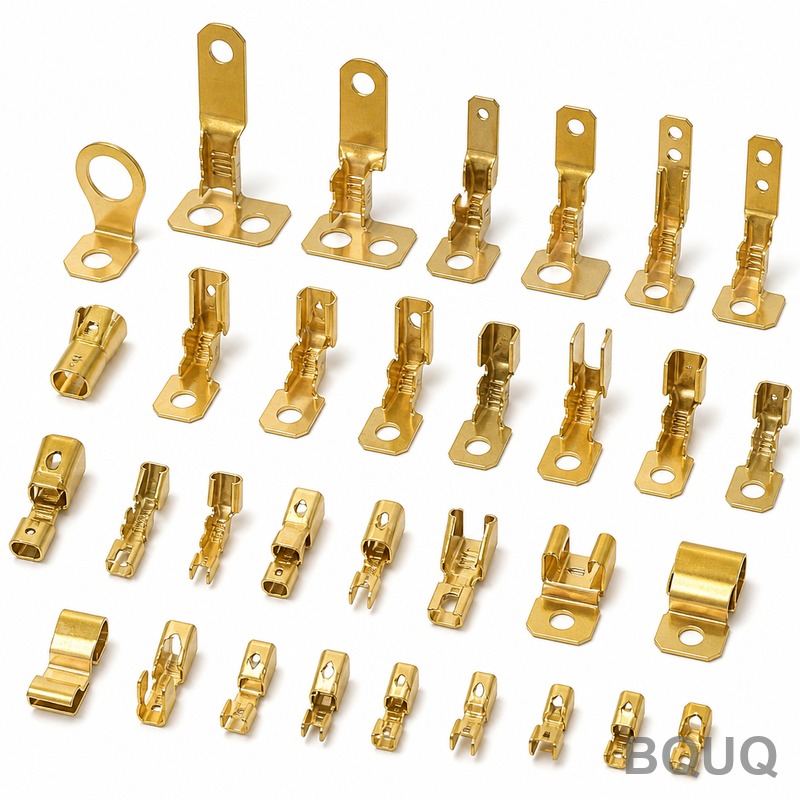
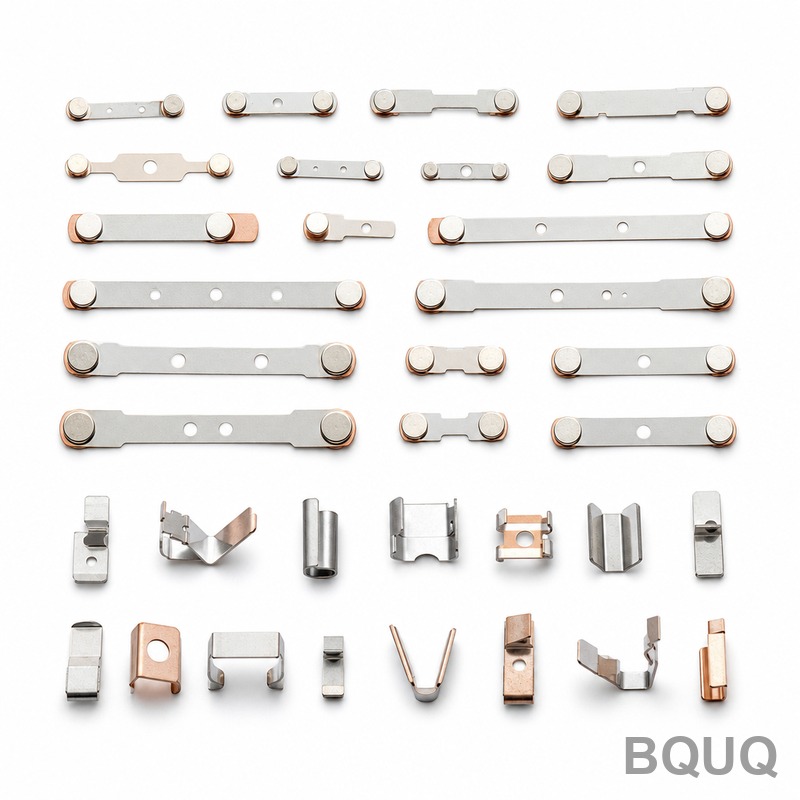
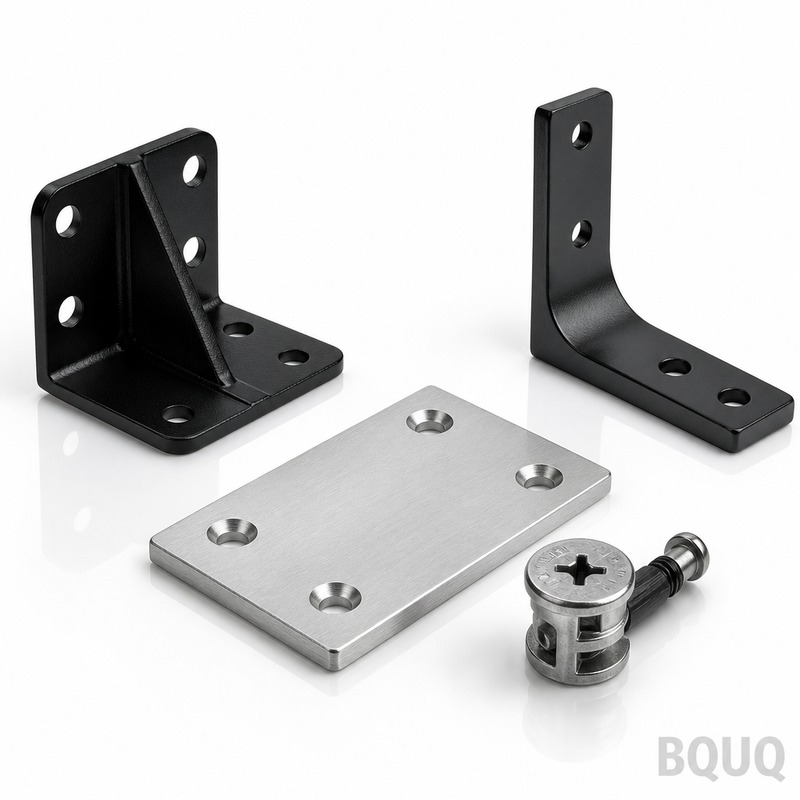
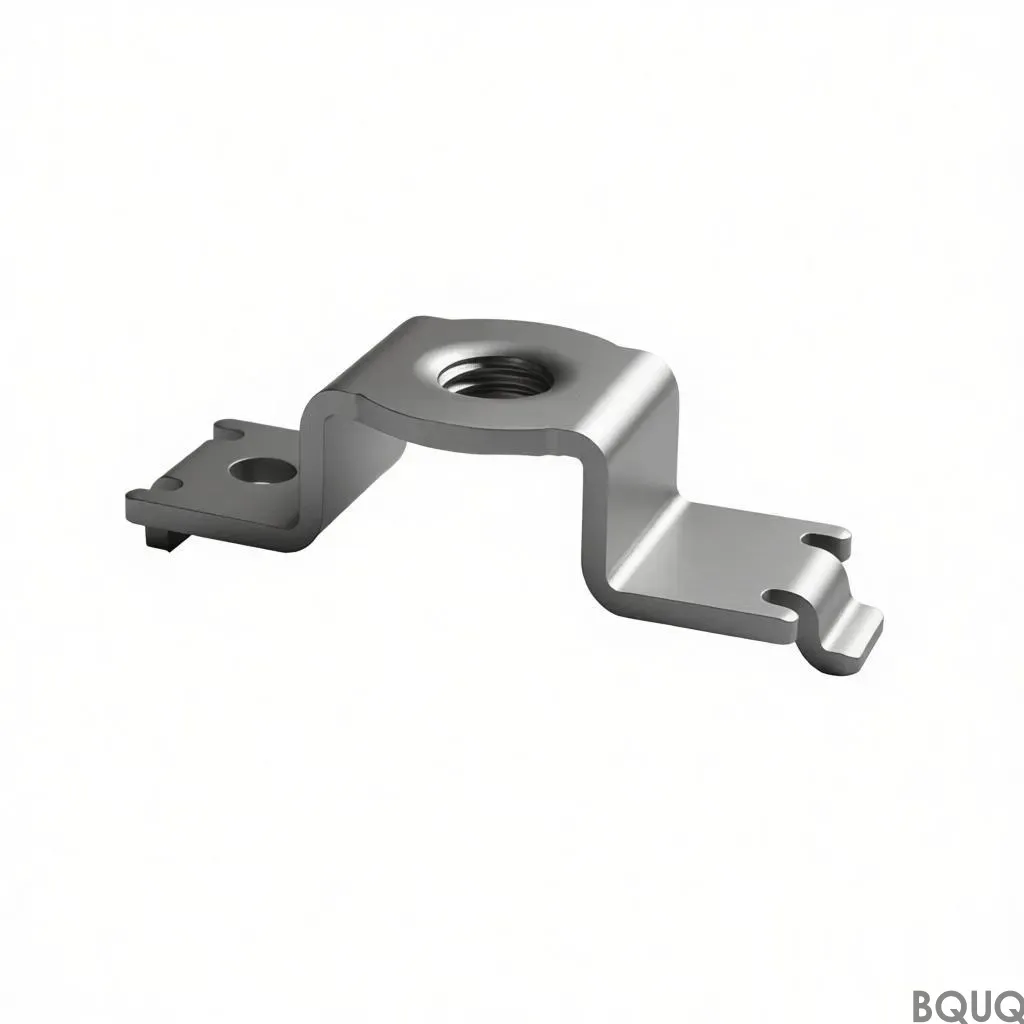
Product Gallery
Key Specifications and Selection Guide
Spec comparison
Parameter
Value / Range
Material
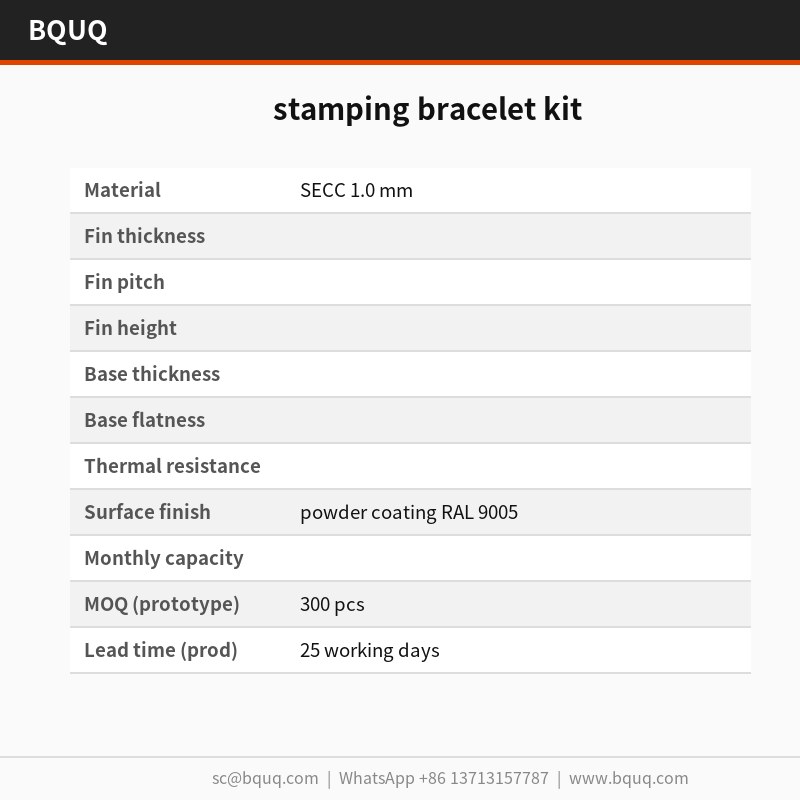
SECC 1.0 mm
Tolerance
Fin pitch held within die capability; flatness on mounting face held directly from tool
Lead time
Standard for stamping volume programs; confirmed at order
MOQ
Volume program dependent; confirmed at order
Capacity
Repeatable stamping strokes for network equipment volume programs
Selection / comparison
Option
Best for
Trade-off
Stamped SECC 1.0 mm
Repeatable fin profile and volume network equipment programs
Die wear can shift fin pitch over time, caught by inspection
Extruded heatsink
Simple constant profiles
Cannot hold the same repeatable fin profile as stamping
Brazed fin assembly
Complex geometries
Brazed joint can fail; stamped base and fins are one piece
Powder coating RAL 9005
Black finished appearance and surface protection
Adds a coating step; confirm thermal impact if required
Process / inspection
Stage
Control
Record
Die forming
Every fin formed in one stroke; pitch held within tolerance across a run
Fin pitch measurement
Base and fin pressing
One-piece construction; no brazed joint
Visual and dimensional check
Mounting face
Flatness held directly from the tool for uniform thermal interface contact
Flatness inspection
Batch inspection
Die wear detected as measurable shift in fin pitch before field use
Inspection report before every shipment
Surface finish
Powder coating RAL 9005 applied as specified
Coating verification
Frequently Asked Questions
What material is the stamping bracelet kit made from?
The standard material is SECC 1.0 mm steel. It is supplied with powder coating RAL 9005 when specified. The SECC 1.0 mm gauge keeps the kit light while maintaining fin density for fixed airflow paths.
What thermal performance can I expect from this stamped heatsink?
Thermal performance is at ΔT = 60 K, confirmed by testing. The one-piece stamped construction holds flatness on the mounting face, which keeps thermal interface contact uniform. Actual performance depends on airflow, mounting pressure, and enclosure conditions.
How does stamping compare with extrusion for fin pitch and repeatability?
Stamping gives a repeatable fin profile that extrusion cannot hold. The die forms every fin in one stroke, so pitch stays within tolerance across a run. Extrusion may vary more, while die wear in stamping shows up as a measurable fin pitch shift caught by inspection.
Is there a risk of joint failure in this stamped bracelet kit?
No brazed joint is used. Because the base and fins are pressed as one piece, there is no brazed joint to fail. This improves reliability in network equipment volume programs where vibration and thermal cycling may occur.
What tolerance classes can I specify for fin pitch and flatness?
Fin pitch is held within tolerance across the run, and flatness on the mounting face is held directly from the tool. Specify your required pitch and flatness on the drawing. Inspection catches die wear as a measurable shift in fin pitch before shipment.
What surface finish options are available?
Powder coating RAL 9005 is available as a standard finish. The base material is SECC 1.0 mm. If your application requires a different finish or coating thickness, confirm with the manufacturer because it may affect thermal performance and fit.
Is this stamping bracelet kit suitable for network equipment volume programs?
Yes. Every stroke is dimensionally identical, so hole position carries across the batch. That repeatability makes network equipment volume programs reliable. The light SECC 1.0 mm construction also helps where airflow path length is fixed by the enclosure.