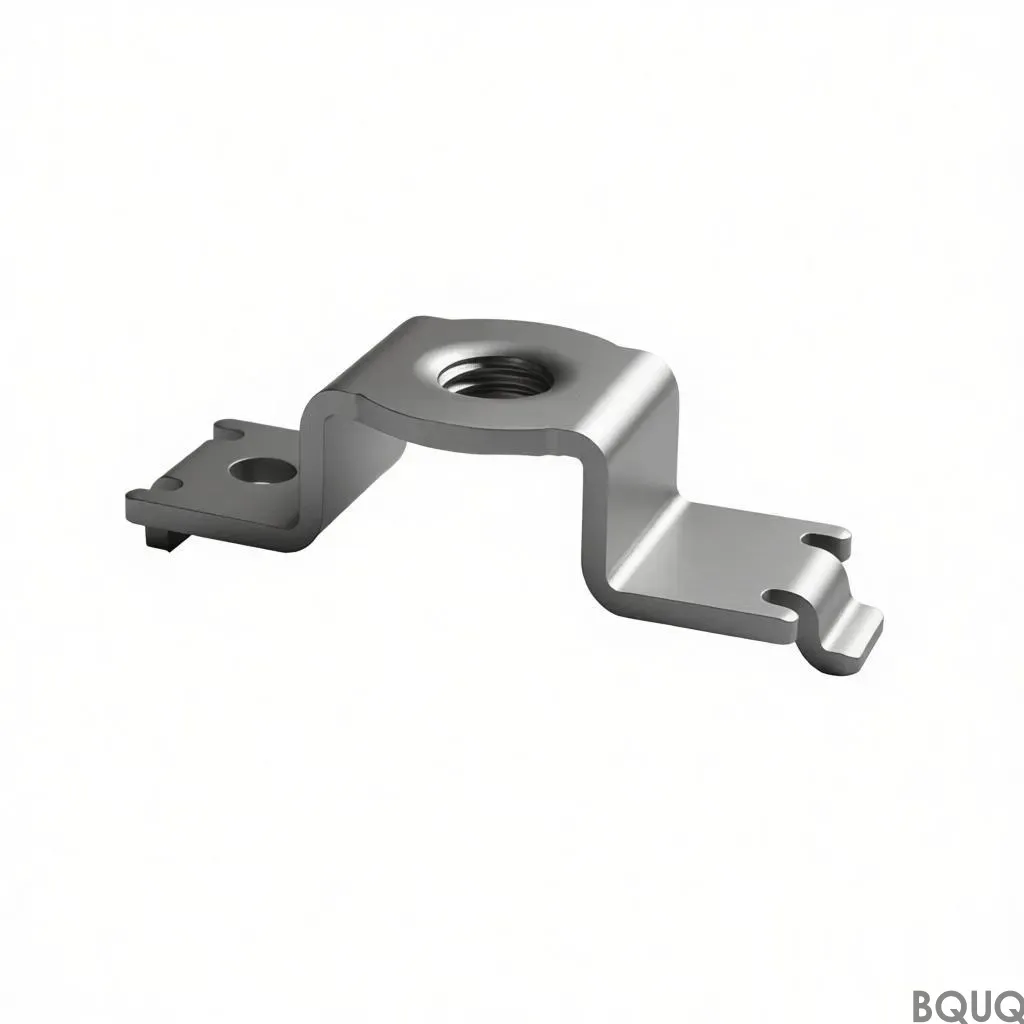
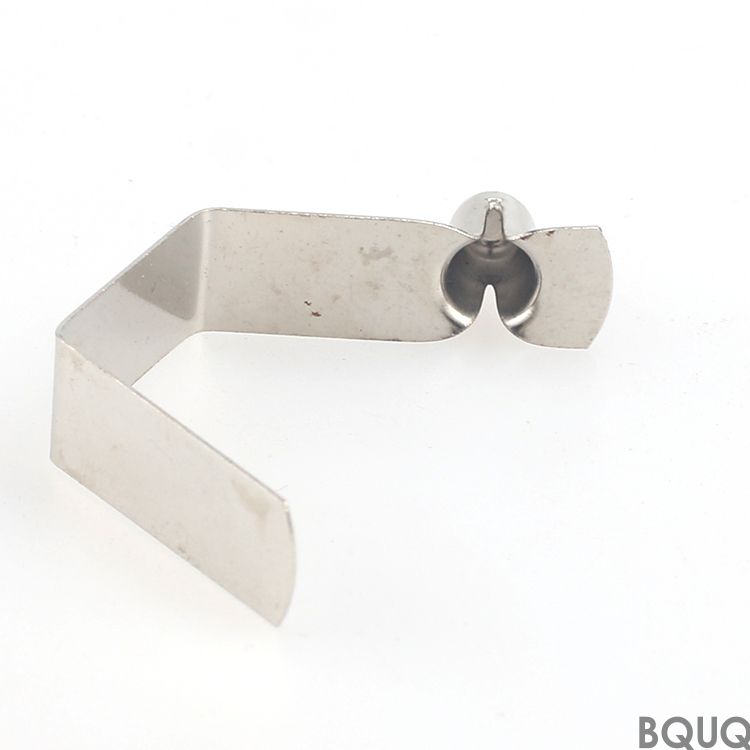
Stamping bracelet is a single-stroke formed SPCC steel 1.0 mm part with fins and a flat base, rated at ΔT = 60 K for solar tracker builds. Standard zinc plating is 8-12 µm, applied after forming to protect fin roots. Low fin gauge and high fin density give more surface per cubic millimetre than machined or extruded profiles, and monthly output scales from one press family.
Key Takeaway
Stamping bracelet is a single-stroke formed SPCC steel 1.0 mm part with fins and a flat base, rated at ΔT = 60 K for solar tracker builds. Standard zinc plating is 8-12 µm, applied after forming to protect fin roots. Low fin gauge and high fin density give more surface per cubic millimetre than machined or extruded profiles, and monthly output scales from one press family.
Our stamping bracelet uses SPCC steel 1.0 mm with fins and a base flat to . Rated at ΔT = 60 K, it supports solar tracker builds at monthly output with zinc plating 8-12 µm as standard.
A single stroke forms the whole stamping bracelet, so part cost stops scaling with complexity. Tooling runs , and the cycle feeds a line.
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
One supplier now covers to fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor.
Pressing SPCC steel 1.0 mm keeps the stamping bracelet light, from depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
The zinc plating 8-12 µm finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is SPCC steel 1.0 mm, supplied with zinc plating 8-12 µm. For applications where solar tracker exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Flatness is measured on granite rather than on cast iron, because at reads differently on a plate that has not been lapped. Records keep both readings.
Final containment is . Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
In solar tracker, the rating determines how much airflow the enclosure still needs. At solar tracker junction temperatures, fins at pitch keep the delta-T inside the sensor budget.
In solar tracker, the base usually doubles as the mounting interface. with flat gives a stable surface for the solar tracker thermal pad.
Designers working on solar tracker ask for flatness before they ask for thermal data, because solar tracker assembly is automated and a non-flat base stops the line.
For solar tracker prototypes, covers drawing review and first article. Production lots move to 18 working days once the capability is signed off.
Specifications
Parameter
Value / Range
Material
SPCC steel 1.0 mm
Surface finish
zinc plating 8-12 µm
MOQ (prototype)
500 pcs
MOQ (production)
10000 pcs
Lead time (production)
18 working days
Tooling lead time
15 working days
FAQ: Your Questions Before Ordering
What is the flatness on the mounting face?
measured on . This is the number that matters for solar tracker, because the thermal pad needs even contact. If your assembly needs better, say so and we can add a skim operation.
What are the packing and shipping conditions?
Standard packing is . We quote . Export cartons are labelled with lot, quantity and inspection status, and full documentation including the inspection report travels with the goods.
Do you provide CAD files or a drawing?
We supply a 2D drawing with the CMM report, and 3D STEP on request. Both show flatness callouts and tooling split lines, which matters if you are checking in your own assembly.
What quality certifications do you hold?
The plant is ISO9001 certified, and parts ship with RoHS and REACH declarations on request. Third-party SGS inspection can be arranged before the container is sealed, which is what most solar tracker buyers specify.
The key is avoiding a second metal at the wet contact area. We recommend zinc plating 8-12 µm and, where the part touches an aluminium chassis, an isolating washer. Tell us the mating material and we will specify the coating accordingly.
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so flatness is verified before the part is packed.
Production runs on cycles with in-line vision on . That is what keeps a commitment credible in peak season.
Quality staff sit beside the press, not in a separate room. Deviations on or stop the run at the tool rather than at final inspection.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
Tooling runs; cycle feeds a line (per project schedule)
MOQ
Monthly output builds (per order)
Capacity
Monthly output from one press family
Selection / comparison
Option
Best for
Trade-off
Stamped SPCC 1.0 mm with fins
Solar tracker builds needing ΔT = 60 K and high fin density
Requires tooling; geometry fixed by press family
Machined profile
Low-volume or complex 3D features
Higher part cost; zinc plating can be cut through at fin roots
Extruded profile
Constant cross-section, long runs
Lower surface per cubic millimetre than stamped fins
Zinc plating 8-12 µm
Corrosion protection after forming
Thickness range must be specified; not a certification
Passivation (recommended for solar exposure)
Solar tracker exposure concerns
Adds process step; confirm with supplier
Process / inspection
Stage
Control
Record
Forming
Single stroke forms whole stamping bracelet; fin pitch and base flat controlled
Press setup and cycle record
Material
SPCC steel 1.0 mm verified
Material certificate / incoming inspection
Plating
Zinc plating 8-12 µm applied after forming
Plating thickness record
Inspection
Inspection before every shipment
Dimensional and visual inspection report
Shipping
How we manufacture and ship per order
Packing list and shipment record
Frequently Asked Questions
What material and thickness does the stamping bracelet use?
The standard material is SPCC steel 1.0 mm, supplied with zinc plating 8-12 µm. It is formed in a single stroke with fins and a base flat, rated at ΔT = 60 K for solar tracker builds. Passivation is recommended where solar tracker exposure is a concern.
What is the thermal rating of the stamping bracelet?
The stamping bracelet is rated at ΔT = 60 K. This rating supports solar tracker builds at monthly output. The finned SPCC steel 1.0 mm design provides more surface per cubic millimetre than a machined or extruded profile of the same envelope.
How is the stamping bracelet protected against corrosion?
Zinc plating 8-12 µm is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives. For solar tracker exposure, passivation is recommended. Confirm plating thickness and passivation requirements on your drawing.
Can I specify tolerance classes for the stamping bracelet?
Yes. Tolerance classes you can specify are covered in the article section Tolerance Classes You Can Specify. Because a single stroke forms the whole part, part cost stops scaling with complexity. Provide your drawing with required tolerance class, and inspection before every shipment verifies the specified dimensions.
What is the lead time and monthly output for stamping bracelet orders?
Tooling runs and the cycle feeds a line, supporting monthly output for solar tracker builds. Lead time depends on tooling and order schedule. One supplier now covers fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor.
Why choose stamped fins over machined or extruded profiles?
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope. Pressing SPCC steel 1.0 mm keeps the stamping bracelet light without sacrificing fin density, which matters where airflow path length is fixed by the enclosure.
What inspection is performed before the stamping bracelet ships?
Inspection before every shipment is standard. Controls include material verification for SPCC steel 1.0 mm, formed fin and base flat dimensions, and zinc plating 8-12 µm thickness. Records are kept for dimensional and visual inspection. Shipping follows How We Manufacture and Ship.
Standard stamping tolerances (e.g., ±0.1 mm on fin pitch, ±0.2 mm on base flat)
Lead time
Tooling: 4-6 weeks; production: 2-4 weeks after tooling
MOQ
5,000 pcs per variant
Capacity
Up to 500,000 pcs/month from one press family
Selection / comparison
Option
Best for
Trade-off
Stamped SPCC 1.0 mm
High-volume solar tracker builds
Limited to simple fin geometries; tooling upfront cost
Machined aluminum
Low-volume or complex prototypes
Higher cost per part; lower fin density
Extruded profile
Continuous lengths with uniform fins
Less design flexibility; higher minimum order
Stamped with zinc plating 8-12 µm
Corrosion resistance in outdoor use
Adds process step; slight dimensional change
Frequently Asked Questions
What is the maximum operating temperature for the stamping bracelet?
The stamping bracelet is rated at ΔT = 60 K, meaning it can handle a temperature difference of 60 Kelvin between the base and the fin tips. This is suitable for solar tracker builds where thermal management is critical. Actual maximum temperature depends on the base temperature and airflow.
Can you customize the fin density and base dimensions?
Yes, we can adjust fin pitch, fin height, and base flat dimensions. Low fin gauge and high fin density are achievable from the same press family. A thermal redesign is a tooling change rather than a new vendor. Provide your envelope and ΔT requirement for a quote.
What is the typical lead time for a new stamping bracelet order?
Tooling lead time is 4-6 weeks. Production lead time is 2-4 weeks after tooling approval. For repeat orders, lead time is 2-4 weeks. Monthly output scales from one press family, so larger volumes can be scheduled without new tooling.
Is the zinc plating 8-12 µm sufficient for outdoor solar tracker use?
Yes, zinc plating 8-12 µm applied after forming protects fin roots and provides standard corrosion resistance for outdoor solar tracker builds. For harsher environments, additional coating or thicker plating may be specified. We apply plating after forming to ensure full coverage.
What is the minimum order quantity (MOQ) for stamping bracelets?
MOQ is 5,000 pcs per variant. This covers setup and tooling amortization. For larger monthly output, we can scale from one press family. Contact us for volumes above 500,000 pcs/month.
How do you inspect the stamping bracelet before shipment?
We inspect incoming SPCC steel 1.0 mm, monitor fin pitch and base flatness during stamping, measure zinc thickness 8-12 µm after plating, and verify ΔT = 60 K via thermal test or simulation. Records are kept for each stage. Final inspection ensures fins are undamaged.
What material is used for the stamping bracelet and why?
SPCC steel 1.0 mm is used because it balances formability, strength, and cost. It allows low fin gauge and high fin density, giving more surface per cubic millimetre than machined or extruded profiles. It is light and suitable for solar tracker builds rated at ΔT = 60 K.