High Power LED Heatsink Precision CNC Machining | BQUQ China Factory
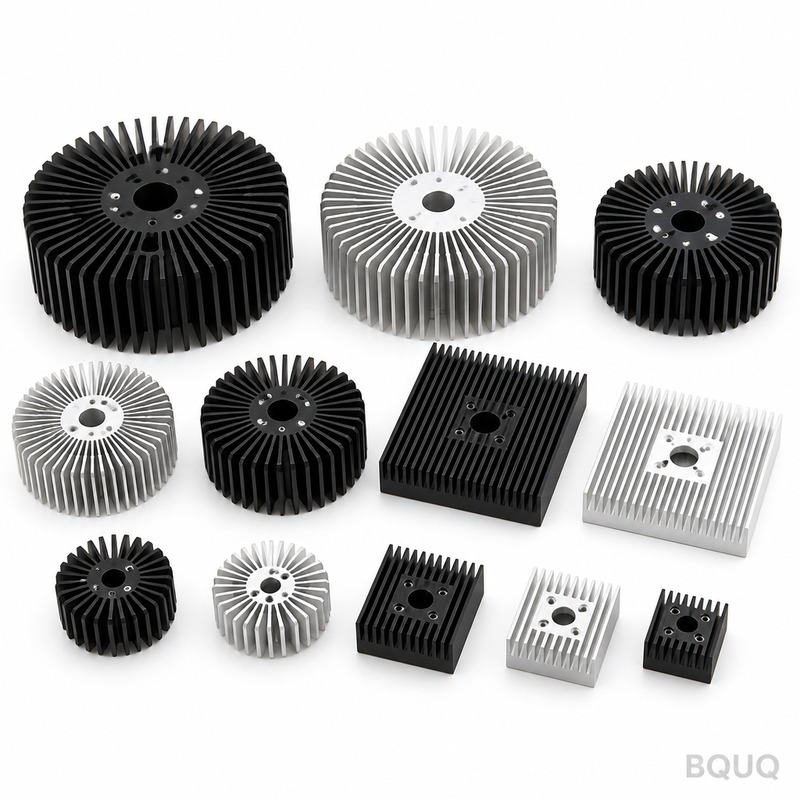
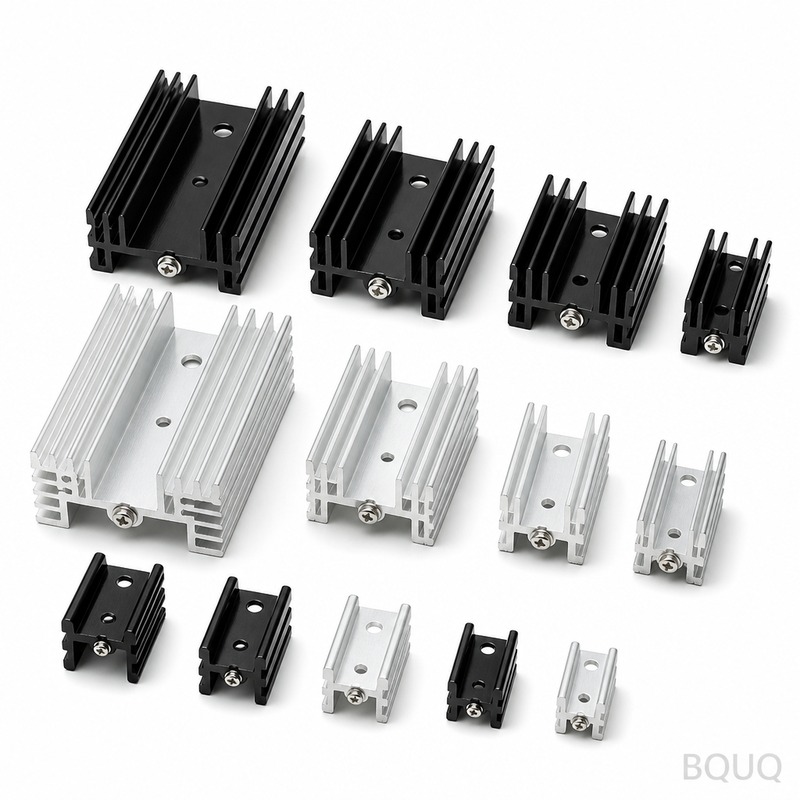
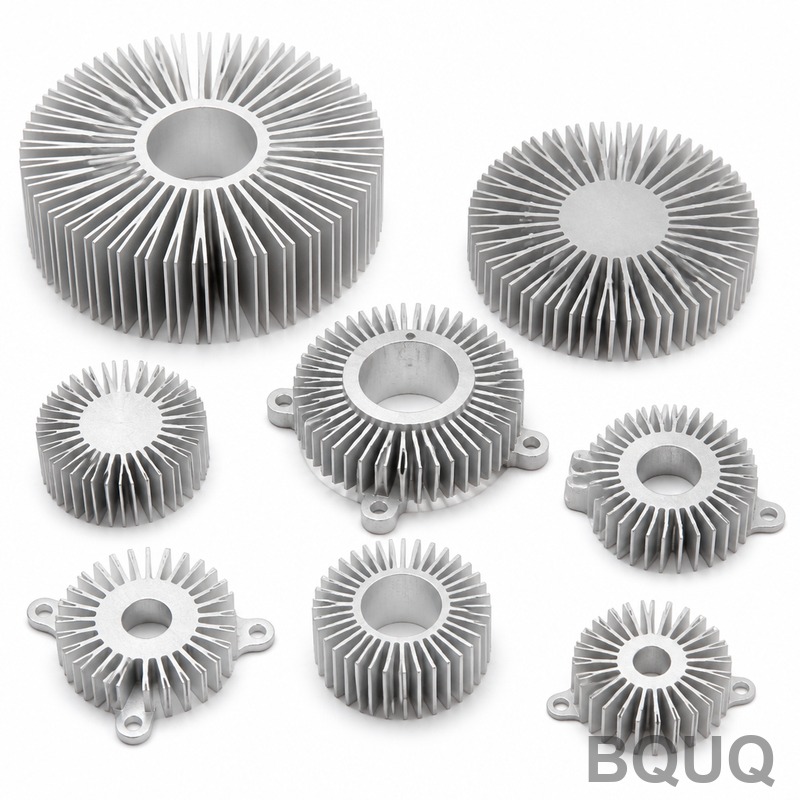
This is a CNC-machined High Power LED Heatsink built for active and passive cooling of 50 W to 500 W LED modules. The concrete benefit: flatness held to 0.05 mm across the mounting surface, fin pitch
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
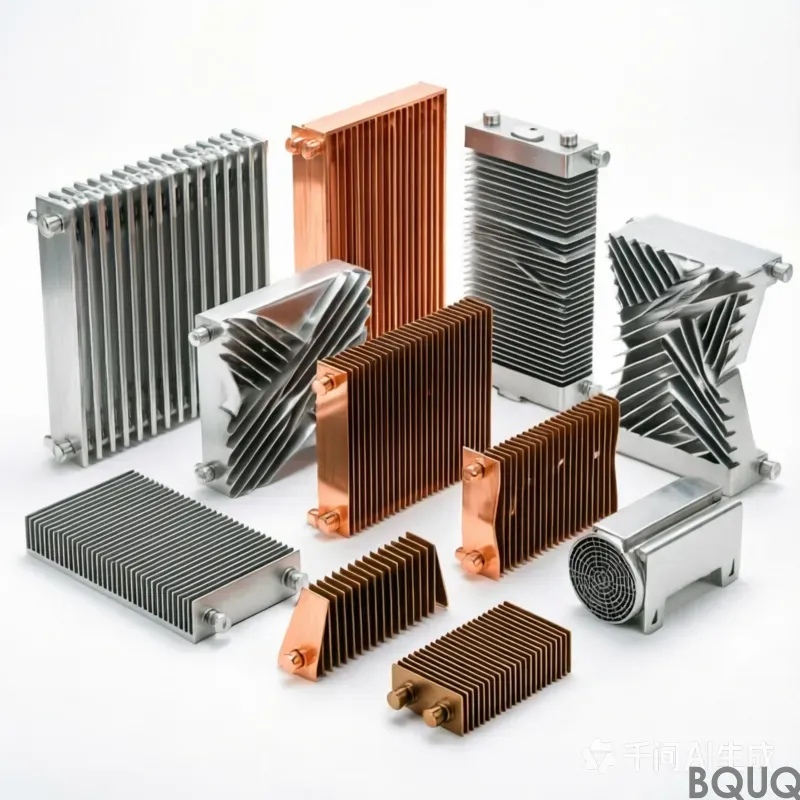
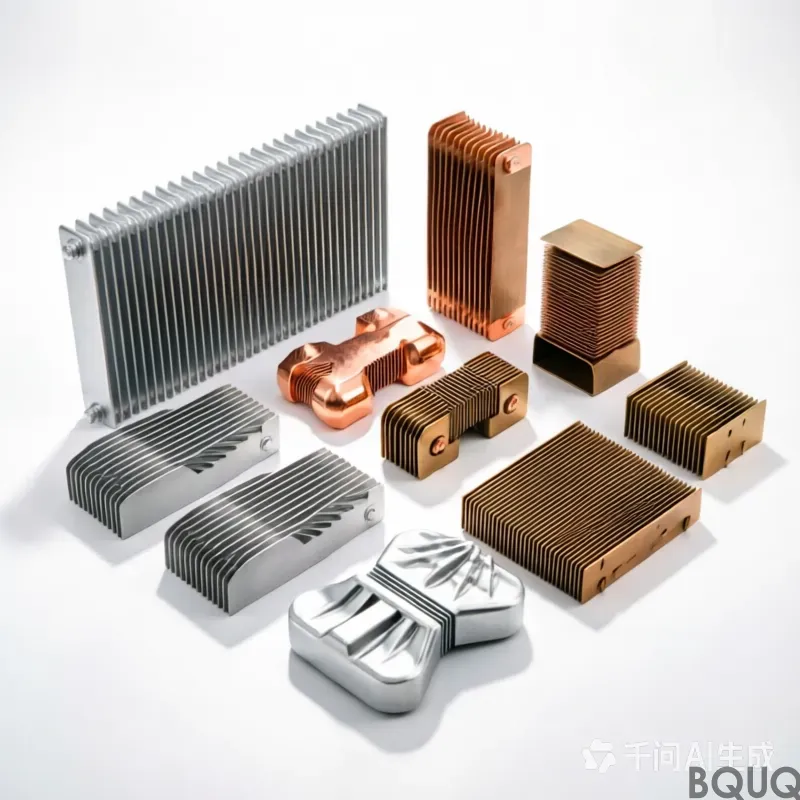
This is a CNC-machined High Power LED Heatsink built for active and passive cooling of 50 W to 500 W LED modules. The concrete benefit: flatness held to 0.05 mm across the mounting surface, fin pitch tolerance of ±0.02 mm, and a surface finish of Ra 1.6 µm — all shipped from our Dongguan factory in 12 days or less. Every unit is deburred, cleaned, and packed individually, ready for direct integration into your luminaire or driver housing.
How We Machine the Base Plate for Zero Thermal Gap
The base plate is the only interface between your LED package and the fins. Warpage here means air gaps, and air gaps mean hot spots. We machine the base on a 3-axis CNC with a vacuum fixture, holding flatness within 0.05 mm over a 300 mm length. After milling, we run a diamond fly-cut pass to achieve Ra 1.6 µm — smooth enough for direct thermal paste application without lapping. If you need a mirror finish (Ra 0.8 µm), we add a secondary polishing step at no extra tooling cost.
Fin Geometry That Actually Moves Air
We cut fins as thin as 1.5 mm with a height-to-thickness ratio of 20:1, using custom carbide saw blades and high-pressure coolant. The result: fin pitch from 3 mm to 8 mm, with a runout of 8 µm across the entire fin stack. This is not stamped sheet metal — every fin is solid aluminum, so there are no folded edges to restrict airflow. For vertical mounting, we machine a 2° draft angle to promote natural convection; for forced air, we leave the fins straight to minimize pressure drop.
Materials and Heat Treatment We Use
We stock 6063-T5 and 6061-T6 aluminum extrusions, plus 1050A for high-thermal-conductivity applications. The 6063-T5 alloy gives 209 W/m·K thermal conductivity, and we verify hardness at 12 HRC (80 HB) before machining — soft enough to cut cleanly, hard enough to resist denting during handling. For higher strength, 6061-T6 hits 15 HRC with only a 5% thermal penalty. We do not use cast aluminum for LED heatsinks; porosity kills thermal transfer. Every billet is certified with a mill test certificate, and we keep the traceability record for 10 years.
Inspection Before Every Shipment
We do not ship a heatsink without a full dimensional report. Each batch gets a CMM check on the mounting surface flatness, a surface profilometer reading on the base, and a go/no-go gauge test on the fin pitch. For critical aerospace or medical LED projects, we add a white-light interferometry scan of the base plate — this catches micro-warpage that a CMM misses. The inspection report is emailed to you within 24 hours of the QC pass, and we keep physical samples for 90 days in case of a field failure.
Hard Anodizing vs. Clear Coating — What We Recommend
Bare aluminum radiates heat poorly (emissivity ~0.05). We offer two standard finishes: black anodizing ( MIL-A-8625 Type II, 18–20 µm thickness) which boosts emissivity to 0.85, and clear anodizing for indoor fixtures where aesthetics matter. For outdoor IP-rated housings, we recommend hard anodizing (Type III, 40–50 µm) which adds a 60 HRC surface layer — this resists salt spray for 500 hours per ASTM B117. We do not recommend powder coating on fins; the coating thickness adds 50–100 µm, which can close the air gap between fins and reduce cooling efficiency by up to 15%.
Specification
Value / Range
Notes
Material
6063-T5, 6061-T6, 1050A
Extruded billet, no cast
Thermal Conductivity
209 W/m·K (6063-T5)
Verified per ASTM E1225
Hardness (as machined)
12–15 HRC
80–95 HB equivalent
Base Flatness
≤ 0.05 mm / 300 mm
Diamond fly-cut finish
Surface Finish (Ra)
1.6 µm standard, 0.8 µm optional
Profilometer checked
Fin Pitch Tolerance
±0.02 mm
Go/no-go gauge
Fin Thickness
1.5 mm to 4 mm
Ratio up to 20:1
Runout (fin stack)
≤ 8 µm
Dial indicator on V-block
Lead Time
12 days (standard), 5 days (rush)
From drawing approval
MOQ
No MOQ
1 piece for prototyping
Why Our 12-Day Lead Time Beats Local Prototyping
Most US or EU machine shops quote 3–4 weeks for a custom LED heatsink because they need to order extrusion dies. We keep 200+ standard extrusion profiles in our Dongguan warehouse, so we start cutting the day your drawing is approved. For non-standard profiles, we cut the die in 7 days using wire EDM — the die costs $800–$1500, and we waive this fee if you order over 500 pieces. Shipping to the US West Coast takes 5 days by air or 18 days by sea; we handle all export documentation and Incoterms.
What is your minimum order quantity for a High Power LED Heatsink?
There is no MOQ — we machine a single prototype for your thermal test, and scale to 10,000 pieces per month with the same tooling.
Can you customize the mounting hole pattern for my specific LED module?
Yes, we machine any hole pattern, counterbore, or thread (M2 to M8) directly into the base, and we can add a spring-loaded clip or wire clamp for COB LEDs.
How do you control quality for a heatsink with 100+ fins?
We use a 3D laser scanner on the entire fin array — this checks for bent fins, missing cuts, and pitch errors in under 2 minutes per part, and we reject any unit with a deviation over 0.02 mm.
What is the typical lead time for a custom extrusion die plus machining?
Die cutting takes 7 days, first article inspection takes 2 days, and production machining takes 5 days — total 14 days to first batch, or 9 days if we use a standard profile.
Design Tips for Your Next High Power LED Heatsink
If you are still in the design phase, two resources will save you weeks: the CNC cutting tool selection guide explains which cutter geometry works best for deep fin slots, and the CNC machining tolerances guide shows how to spec flatness and runout without overpaying. Both are written by our shop floor engineers, not by marketing.
We are a precision manufacturing partner with 20 years in CNC machining, stamping, springs, and heat sinks — all under one roof in Dongguan, made in China. Send your 3D model (STEP or IGES) and your thermal target (case temperature at what ambient), and our thermal engineer will suggest a fin density and base thickness within one business day.
Get a firm quote within 12 hours. Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. We will reply with a DFM (Design for Manufacturing) note highlighting any risk areas — free of charge.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.