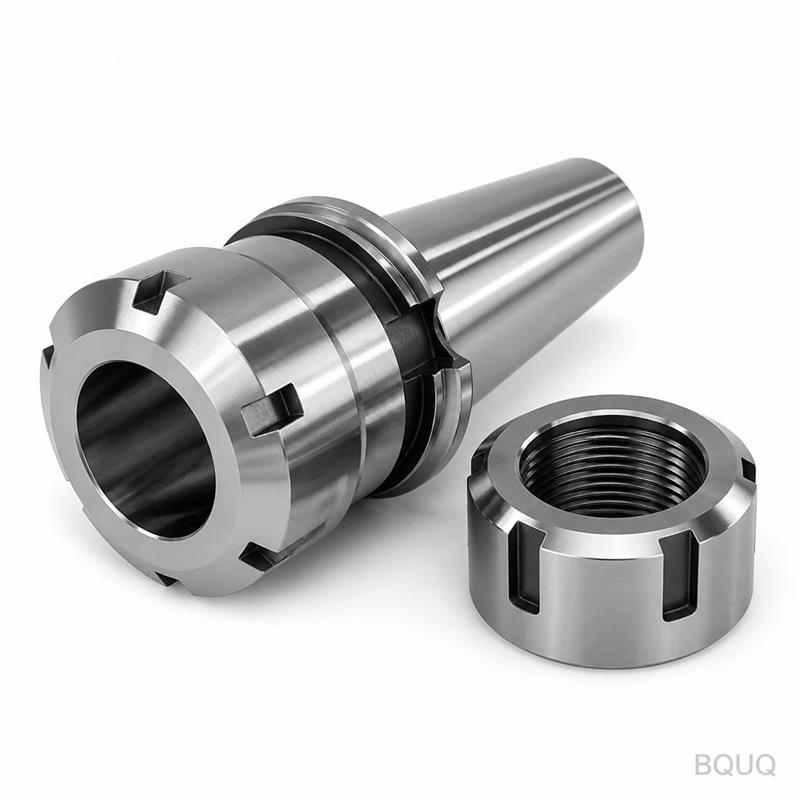
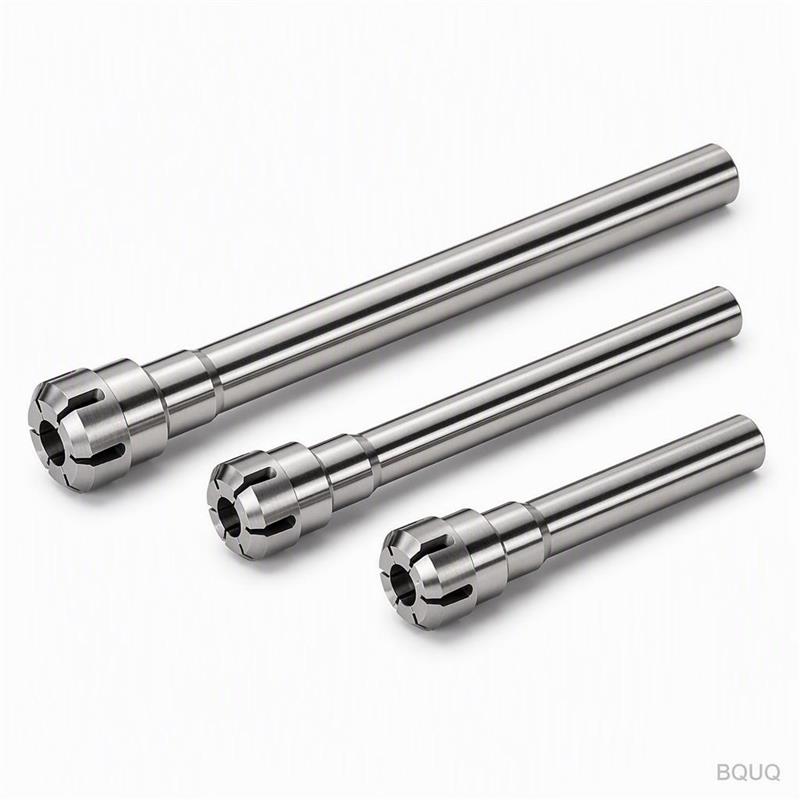
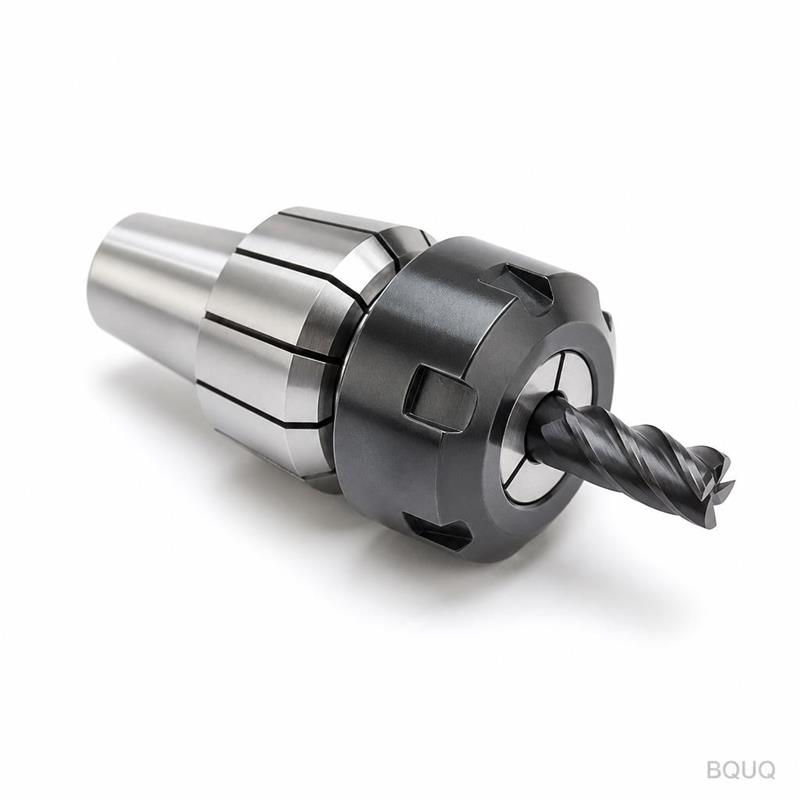
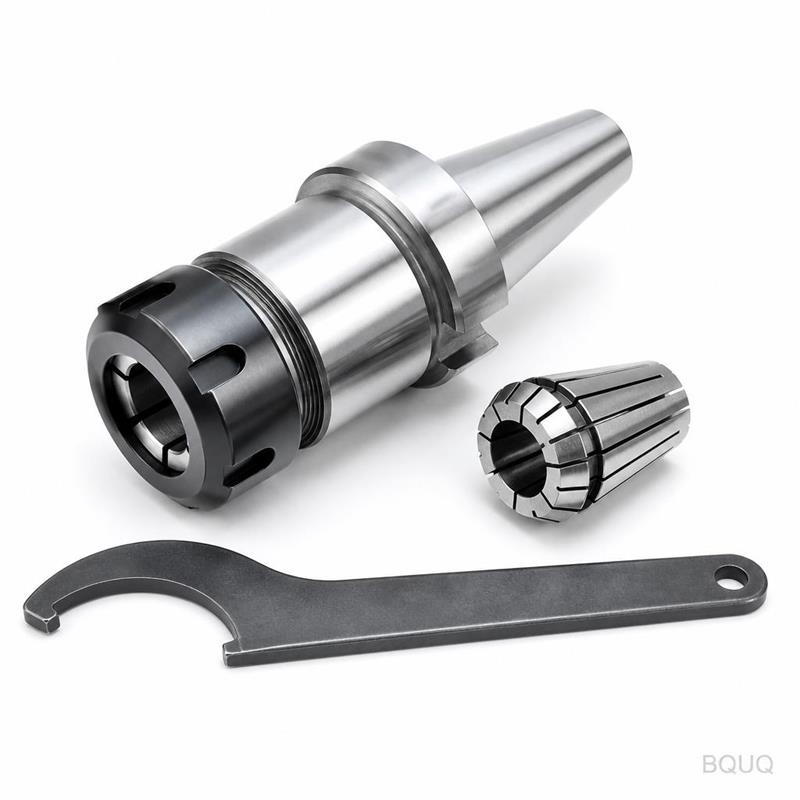
OpeningYour drawing defines the tolerances. Our job is to hit them exactly. We machine your ER50 spring collet chuck and collet nut from solid bar stock, not from cast blanks with
Custom CNC Collet Chuck ER50 Heavy Duty Precision Made in China
OpeningYour drawing defines the tolerances. Our job is to hit them exactly. We machine your ER50 spring collet chuck and collet nut from solid bar stock, not from cast blanks with hidden porosity. Eve
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
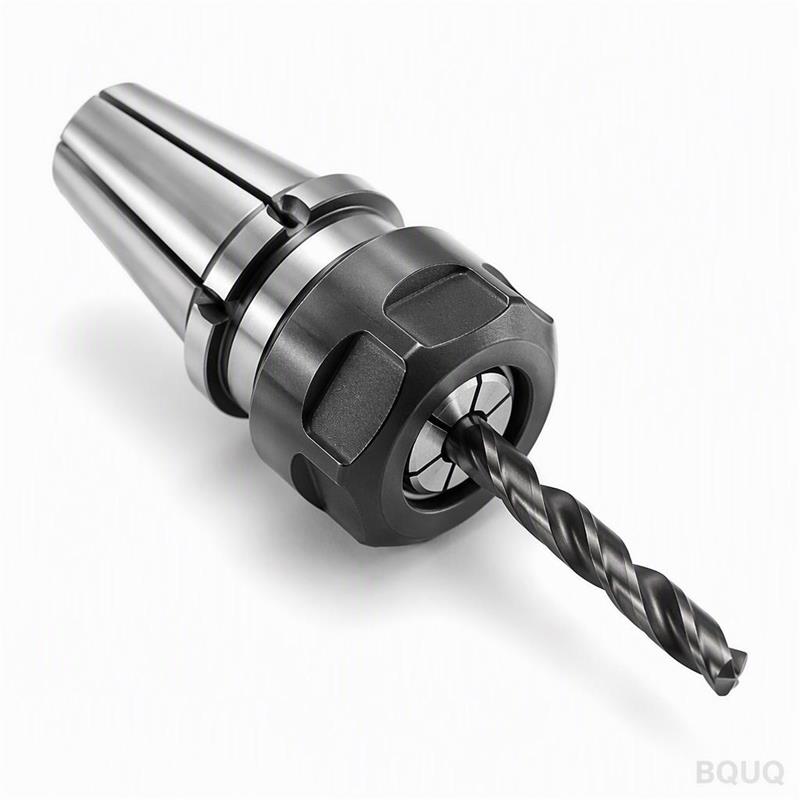
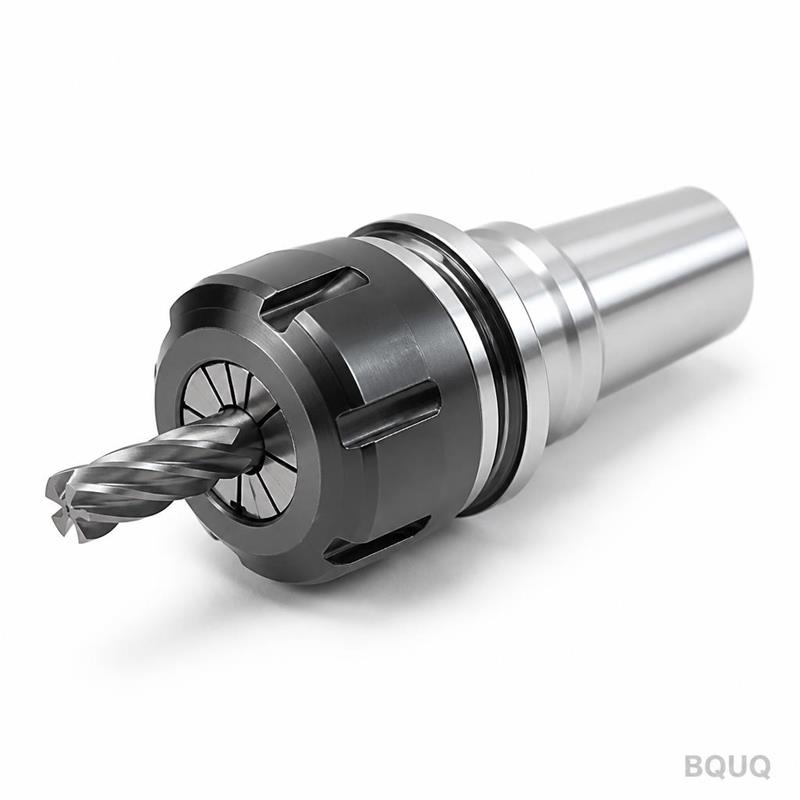
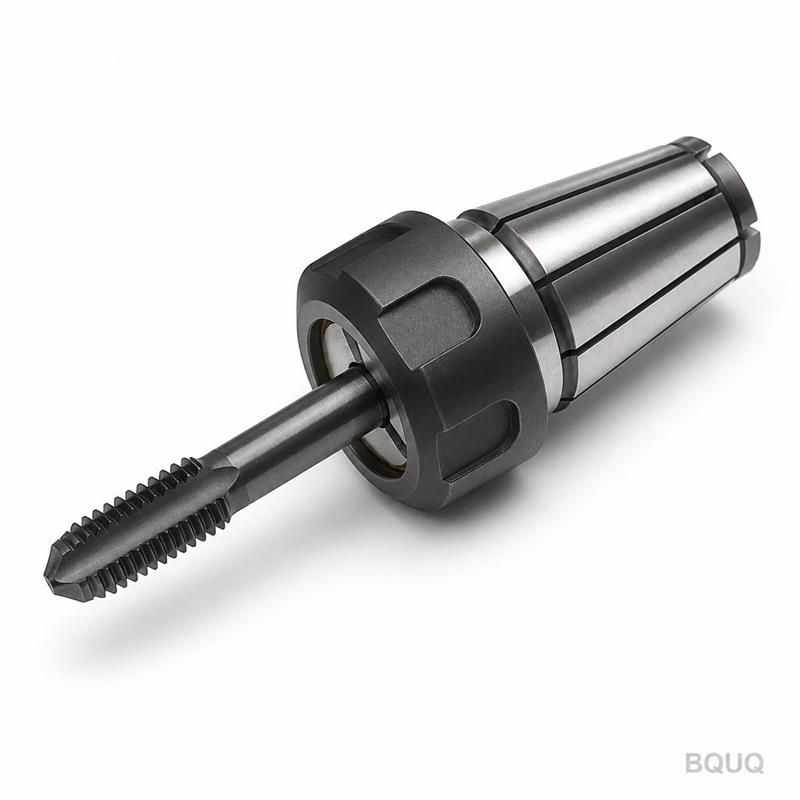
Your drawing defines the tolerances. Our job is to hit them exactly. We machine your ER50 spring collet chuck and collet nut from solid bar stock, not from cast blanks with hidden porosity. Every thread is cut, every taper is ground, and every concentricity is verified before the part leaves our floor.
We do not ship parts we would not mount on our own spindles. If the print says it, we measure it. If the print does not say it, we ask first.
Concentricity: ≤ 0.005 mm TIR at nose
Thread pitch accuracy: 6H / 6g class
Surface finish: Ra 0.4 µm on taper and bore
Lead time: 15-20 working days for custom batches
No MOQ – one piece or one thousand, same process control
Optional G2.5 at 20,000 RPM (dynamic balance report available)
Batch size
1 to 10,000 pieces
Inspection
100% critical dimensions, CMM report per batch
Country of origin
Made in China, Dongguan factory
We use Mazak and Doosan CNC lathes with live tooling for the body, then finish the taper on a Studer internal grinder. Threads are cut on a CNC thread grinder, not chased with a die. This is the difference between a collet chuck that grips true and one that wobbles.
Three Reasons Buyers Send Us Their Drawings
1. Batch-traceable quality
Each batch gets a unique heat number and work order. We record material certs, machine settings, and operator initials. If a problem appears in your assembly line six months later, we can trace it back to the exact shift and tool insert. You cannot do that with a trading company.
2. Inspection report per batch
You get a dimensional report with every shipment. It lists measured values for taper angle, thread pitch, concentricity, and hardness. We do not just say "it is within tolerance." We show you the numbers. For critical aerospace or medical runs, we include CMM point-cloud data on request.
3. One factory for CNC + stamping + springs + heatsinks
Your collet chuck is not an island. It works with a drawbar spring, a stamped retainer plate, or a heatsink in a high-speed spindle housing. We make all of those in the same building. You send one drawing package, we coordinate the processes, and you receive one consolidated shipment. Fewer vendors, fewer excuses, fewer delays.
Where These Parts Are Used
Our custom CNC collet chucks are running in production environments that punish cheap tooling:
Swiss-type lathes for medical bone screws and dental implants – where 0.005 mm runout means the difference between a passing and failing part.
Multi-spindle automatics in automotive fuel injector lines – ER50 collets hold bar stock up to 34 mm diameter through high-cycle gripping.
Tool presetters and grinding fixtures – the collet nut must repeat to the same position every clamp, so we grind the thread flanks to a consistent lead.
Robotic deburring cells – a heavy-duty chuck body with a keyed slot prevents rotation under side load.
High-speed spindle rebuild shops – they replace worn OEM chucks with our version, machined to the original drawing but with better steel.
If your application involves gripping round stock, pushing coolant through the bore, or spinning at 10,000+ RPM, this is the part.
Q: What is your MOQ?
A: No MOQ. We machine one prototype for you to test, then scale to 5,000 pieces when you are confident. The per-piece price drops with quantity, but the quality process does not change.
Q: How do you guarantee tolerance and quality?
A: We grind the taper and bore on the same setup to eliminate stacking errors. Every chuck is checked on a Marposs gauge for taper angle and concentricity. We send the inspection report with the shipment. If any dimension is out, we replace the part at our cost.
Q: What is the lead time?
A: Standard custom batch is 15-20 working days from drawing approval. If you need a sample for fit testing, we can rush one in 7 days. Production repeat orders are faster because we keep your tooling and program files on file.
Q: Can you provide material certificates?
A: Yes. We supply mill test certificates for the raw material, heat treatment reports, and hardness test results. For stainless or high-alloy steel, we can also provide a chemical composition analysis from an independent lab.
Send Your Drawing
Stop guessing if a standard catalog chuck will fit your spindle. Send us your drawing and we will tell you exactly what we can hold, what it costs, and when you will have it.
Firm quote within 12 hours – including tooling cost, piece price, and lead time
DFM feedback – if your design has a sharp internal corner or a tight tolerance that is expensive to hit, we will tell you before you pay
No MOQ, no hidden fees – the quote you get is the invoice you pay
Email your PDF or STEP file to sc@bquq.com
Or message us directly on WhatsApp: +86 13713157787
Precision manufacturing is not a slogan. It is a measurement. Send us the drawing and we will prove it.