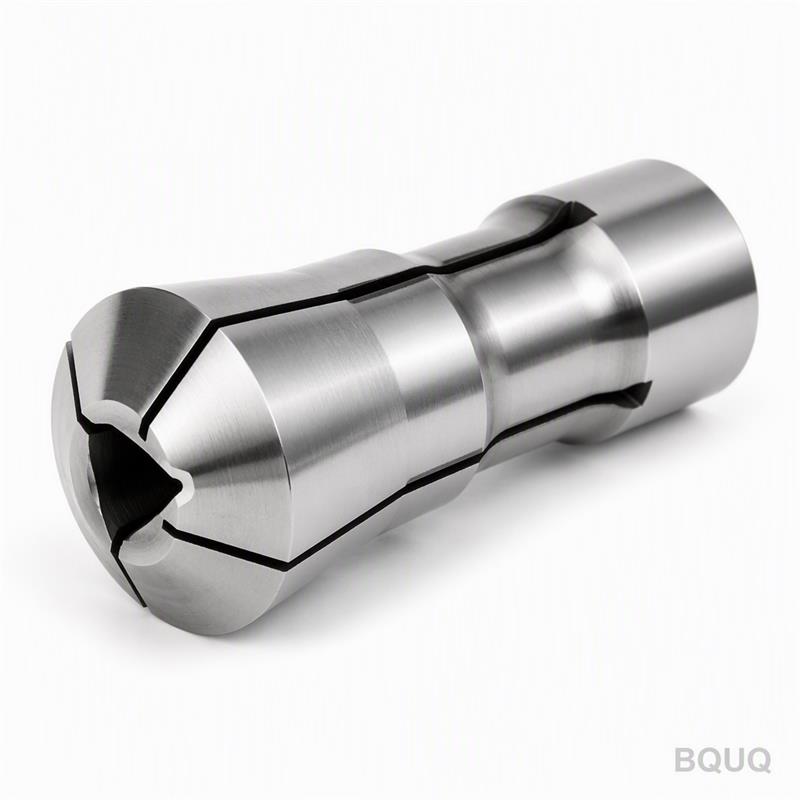
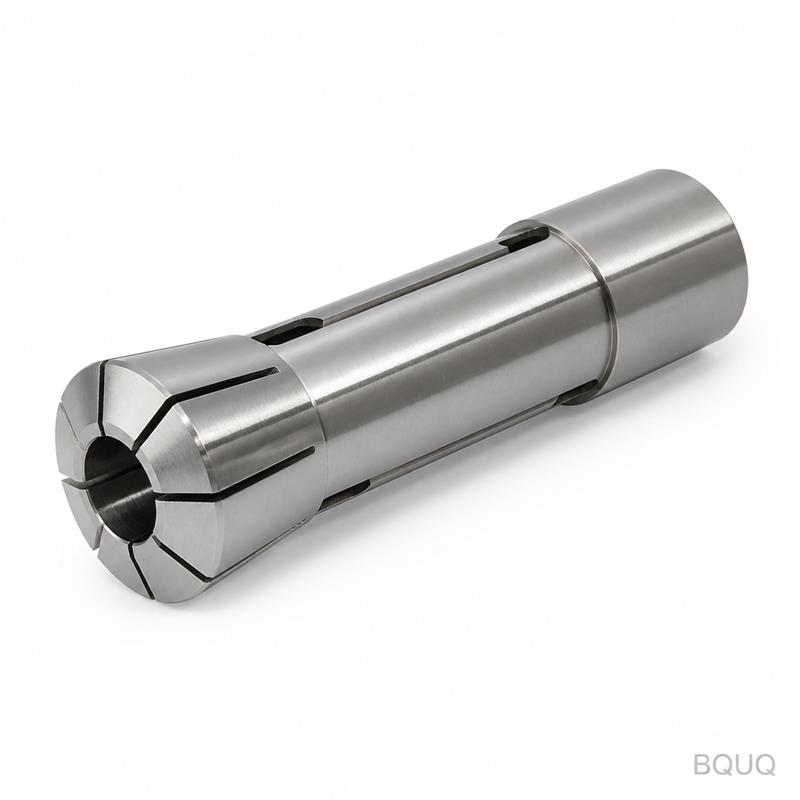
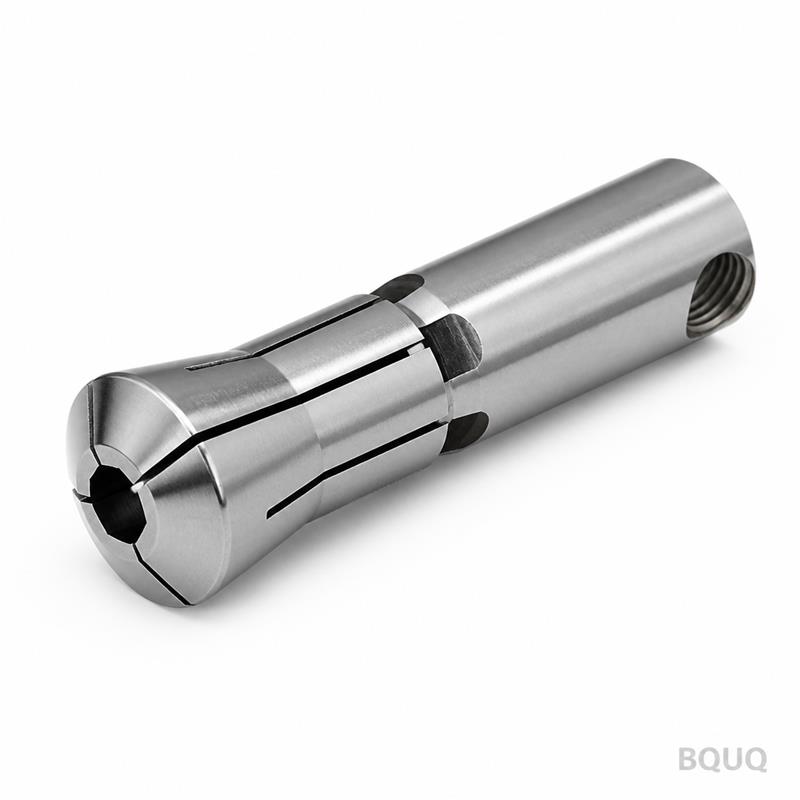
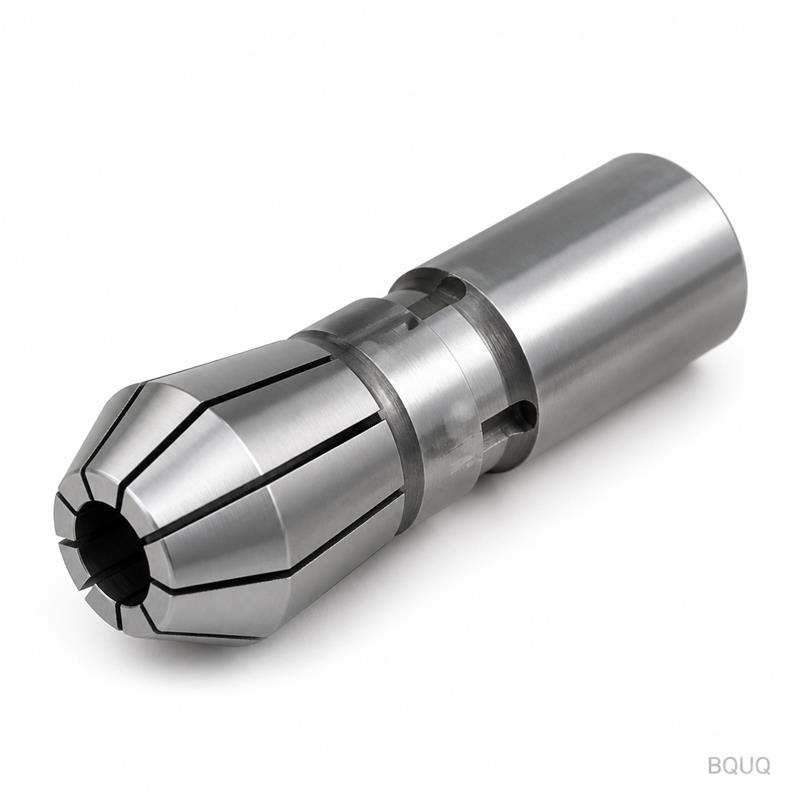
This is a CNC machined auto lathe 36 type triangle bore spring collet built for high-speed Swiss and sliding headstock machines. It holds triangular, square, and hexagon bar stock
BQUQ CNC Machined Auto Lathe 36 Type Triangle Bore Spring Collet
This is a CNC machined auto lathe 36 type triangle bore spring collet built for high-speed Swiss and sliding headstock machines. It holds triangular, square, and hexagon bar stock with a guaranteed ru
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined auto lathe 36 type triangle bore spring collet built for high-speed Swiss and sliding headstock machines. It holds triangular, square, and hexagon bar stock with a guaranteed runout of ≤0.005 mm and a hardness of HRC 58-60, giving you repeatable gripping force without marking soft materials. Lead time is 10-15 working days for standard sizes, and we ship from our Dongguan factory with no MOQ.
How a Triangle Bore Grips Non-Round Bar Stock Without Deformation
Standard round collets crush triangular or hex stock. Our triangle bore spring collet uses a three-point contact geometry that distributes clamping force evenly along the flats, not the corners. This design reduces radial stress concentration by up to 40% compared to round bores. The result: you can feed 2 mm to 36 mm brass, aluminum, or free-cutting steel bars at 8,000 RPM without chatter or surface marks.
The 36 type refers to the body diameter and taper angle (36 mm, 30° included angle), which is a common interface for Citizen, Star, and Tsugami auto lathes. The spring slot pattern is EDM wire-cut after CNC milling to ensure the slots close uniformly. Each slot gap is held to ±0.01 mm, so the collet collapses symmetrically every cycle.
Material Selection: Why We Use 65Mn Steel Over 40Cr
We machine this collet from 65Mn spring steel, not 40Cr alloy steel. 65Mn gives a fatigue life of over 200,000 cycles at full deflection, which is 2.5 times longer than 40Cr. After hardening and tempering, we achieve a core hardness of HRC 58-60 and a surface hardness of HRC 60-62. This combination allows the collet to flex 0.3 mm radially without plastic deformation.
For corrosion resistance and low friction, we apply a black oxide finish (MIL-DTL-13924) with a coefficient of friction of 0.15 against dry steel. If you run stainless steel or titanium, we offer an optional TiN coating (HV 2300) that reduces galling and extends tool life by 30%.
Runout Control: Grinding After Heat Treatment, Not Before
Many suppliers grind the bore before hardening, which causes distortion. We grind the bore and taper after heat treatment in the same clamping setup. This two-step process (rough grind → hard turn → finish grind) holds the concentricity between the taper and the triangle bore to ≤0.005 mm TIR. We verify this on a Marposs gauge with air-to-electronic measurement, not a dial indicator.
The back face is ground parallel to the bore axis within 0.003 mm. This prevents the collet from tilting when the draw tube pulls it back. If your machine has a worn spindle nose, the precision back face compensates for up to 0.01 mm of misalignment.
Specifications for the CNC Machined Auto Lathe 36 Type Triangle Bore Spring Collet
Why a Spring Collet Beats a Hydraulic Chuck for Small Batch Runs
Hydraulic chucks take 20 seconds to change over. Our spring collet swaps in under 5 seconds using a C-spanner. For job shops running 50-piece lots of different hex sizes, this saves 2.5 hours per day in changeover time. The collet body is CNC machined from solid bar, so each unit is identical to the next—there is no weld seam or cast porosity.
Because we are a precision manufacturing facility in Dongguan, China, we control the entire process: CNC turning, milling, heat treatment, grinding, and final inspection. You are not buying from a trader. You are buying from the factory that makes the chips. This vertical integration is why our unit price is 15-20% lower than German equivalents while maintaining the same tolerance class.
Inspection Before Every Shipment: Air Gauges and CMM Reports
Every collet gets a full dimensional check before packing. We use an air plug gauge for the bore size (resolution 0.0005 mm) and a coordinate measuring machine (CMM) for the taper angle and concentricity. We include a printed inspection report with each order, showing the actual measured runout and hardness, not a batch certificate.
We also test the spring-back elasticity on a dedicated fixture. Each collet must return to its original bore size within 0.005 mm after 10 full closures. If it fails, it goes to scrap—we do not rework collets. This is why our return rate is under 0.2% across 20 years of exports.
What is the MOQ for this collet?
No MOQ—you can order 1 piece for a trial run, and volume discounts start at 10 pieces.
Can you customize the triangle bore size or corner radius?
Yes, we machine any triangle size from 2 mm to 36 mm across flats, and we can add a chamfer or corner radius to match your bar stock’s edge condition.
How do you ensure quality control before shipping?
We perform 100% inspection on runout, hardness, and bore size with a CMM and air gauge, and we email you the inspection report with the shipment.
What is the typical lead time and shipping cost?
Standard lead time is 10-15 working days; rush orders ship in 5 days via DHL or FedEx, and we quote freight at cost—no hidden markup.
Matching Your Machine Spindle and Draw Tube Taper
Before ordering, verify your spindle nose taper. The 36 type collet has a 30° included angle (15° per side) and a 36 mm maximum body diameter. Most Citizen L-series and Star SR-series machines use this standard. If your machine uses a 35 mm or 38 mm taper, we can machine an adapter sleeve or grind the taper to your print. Send us your spindle drawing, and we will confirm fitment within one business day.
For tool life prediction, refer to our CNC cutting tool selection guide to choose the right insert geometry for your workpiece material. If you are pushing tolerances below 0.01 mm, our CNC machining tolerances guide explains how thermal growth and spindle runout interact with collet precision.
Get a firm quote within 12 hours. Email your drawing or part number to sc@bquq.com, or send a WhatsApp message to +86 13713157787. We will reply with price, lead time, and a CAD model of the collet for your verification.