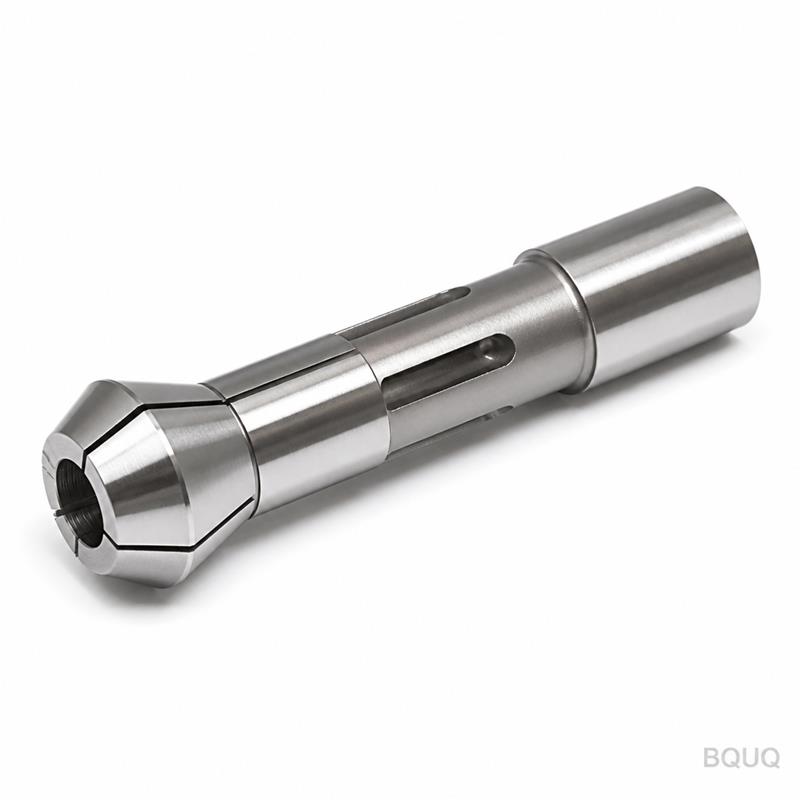
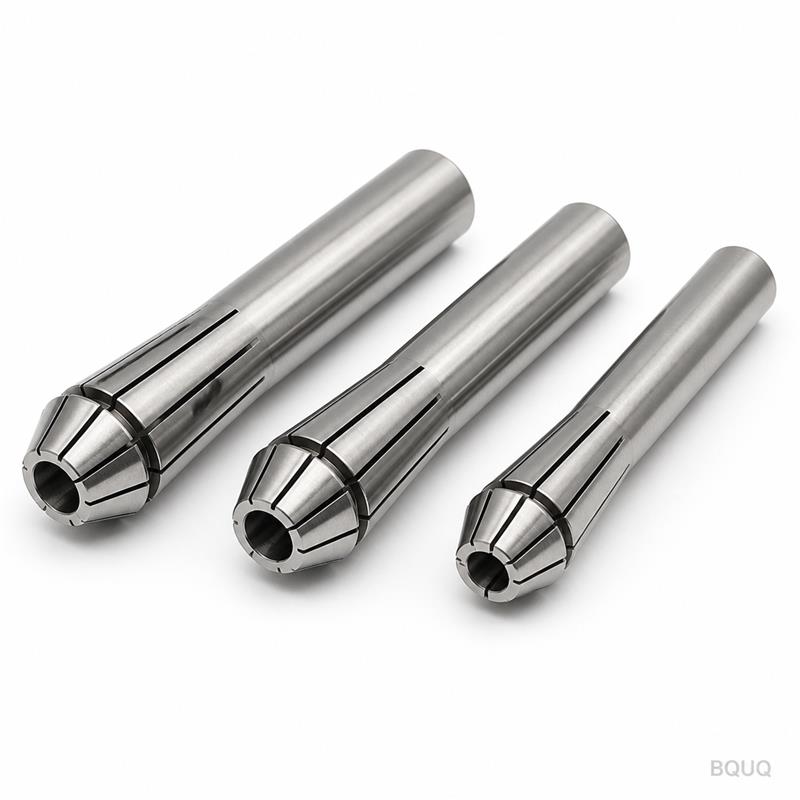
This is a CNC machined auto lathe 52 type collet, specifically ground for hex bar stock gripping. It holds hexagonal workpieces with a guaranteed runout of 0.005 mm TIR and a hardn
BQUQ CNC Machined Auto Lathe 52 Type Collet With Hex Bar Stock
This is a CNC machined auto lathe 52 type collet, specifically ground for hex bar stock gripping. It holds hexagonal workpieces with a guaranteed runout of 0.005 mm TIR and a hardness of 58 HRC, givin
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined auto lathe 52 type collet, specifically ground for hex bar stock gripping. It holds hexagonal workpieces with a guaranteed runout of 0.005 mm TIR and a hardness of 58 HRC, giving you repeatable clamping for high-speed turning. We ship standard sizes in 7 days and custom bore profiles in 12 days, direct from our Dongguan factory.
Why Hex Bar Stock Needs Its Own Collet Profile
Round collets crush hex stock. The six flat faces of a hex bar do not contact a round bore evenly, so torque transfer is poor and the bar slips during heavy cuts. Our 52 type collet is wire-cut and then ground to a true hexagonal bore profile, matching the stock's geometry face-to-face. This gives you 100% line contact on each flat, eliminating vibration and reducing bar push-back during peck drilling.
Grinding Sequence That Kills Runout Before It Starts
We do not just turn the bore and call it done. The hexagonal pocket is first wire-cut to 0.05 mm oversize, then hardened, then finish ground on a jig grinder with a CBN wheel. After grinding, we mount each collet on a test arbor and measure runout at three positions: front, middle, and rear of the bore. If any position exceeds 0.005 mm TIR, the collet is rejected, not reworked.
Materials and Heat Treatment We Use for 58 HRC
We machine the 52 type collet from AISI 4140 chrome-moly steel, pre-hardened to 28 HRC for the rough cut. After the hex profile is cut, we vacuum harden to 58-60 HRC and then deep cryo-treat to -120°C. This cycle transforms retained austenite, giving you a bore that holds its geometry after 100,000 cycles, not just the first 1,000. For stainless or aluminum hex stock, we offer a nitrided version with a 65 HRC surface layer.
Back-Taper Geometry: Why Your Bar Won't Jam
Every collet we make includes a 0.02 mm back taper over the full bore length. This means the gripping diameter is slightly larger at the rear than at the front. When you feed hex bar stock, the bar slides in freely without scraping the bore walls. When the draw tube pulls the collet closed, the front grips first, then the rear, locking the bar without wedging. No back taper means galling and stuck bars — we do not ship that.
Inspection Before Every Shipment: 3-Stage QC
Each collet passes three checks. First, a CMM scan of the hex bore profile against your drawing or our standard 52 type data. Second, a hardness test on the bore surface using a Rockwell C indenter — we reject below 57 HRC. Third, a functional test: we clamp a real 20 mm hex bar in the collet and measure runout with a 0.001 mm dial indicator while rotating at 300 RPM. You get a signed QC report with every order.
Lead Time and MOQ: Small Batch Is Our Standard
We run a 20-machine CNC shop, not a mass production line. A standard 52 type collet in 4140 with a hex bore is finished in 7 working days. Custom bore sizes, non-standard hex dimensions, or special coatings add 3-5 days. We have no MOQ. Order one prototype or 500 pieces — the unit price changes, but the engineering attention does not.
Specification
Value
Material (standard)
AISI 4140 chrome-moly steel
Material (option)
17-4 PH stainless, nitrided H13
Hardness
58-60 HRC (surface), 65 HRC (nitrided)
Bore profile
Hexagonal, wire-cut + ground
Hex sizes available
4 mm to 32 mm across flats
Runout (TIR)
0.005 mm
Bore surface finish
Ra 0.4 µm
Back taper
0.02 mm over full bore length
Lead time (standard)
7 working days
MOQ
No MOQ, single piece accepted
How to Match This Collet to Your Auto Lathe Spindle
The 52 type refers to the collet's outer diameter and taper angle, not the bar size. Before ordering, measure your spindle nose taper and draw tube thread pitch. We stock three taper angles: 5°, 10°, and 15°. If you send us your spindle drawing, we will match the taper and thread exactly. Getting this wrong means the collet will not seat, and you will get chatter at 4000 RPM. We have seen it. We will not let it happen to you.
When Hex Stock Sizes Change: Re-Grinding Service
If your production switches from 12 mm hex to 14 mm hex, do not buy a new collet. Send the old one back, and we re-grind the bore to the new size for 40% of the new collet price. Because the collet body and taper remain untouched, this is a two-day turnaround. This is available only for our own BQUQ collets — we cannot regrind competitors' parts because we do not know their material history.
What is your minimum order quantity for this 52 type collet?
No MOQ — we accept single-piece orders for prototyping, and volume discounts start at 20 pieces.
Can you machine a custom hex size that is not in your standard range?
Yes, we cut any hex size from 4 mm to 32 mm across flats, plus metric or inch dimensions, with no tooling surcharge for the first custom order.
How do you guarantee the 0.005 mm runout on a hex bore?
We grind the hex bore on a jig grinder and verify each collet with a 0.001 mm indicator on a test arbor, rejecting any part that exceeds 0.005 mm TIR.
What is the real lead time if I need a custom taper angle?
Standard tapers ship in 7 days; a custom taper angle adds 3 days because we cut a new locating fixture, total 10 working days.
Get a Firm Quote with Your Drawing in 12 Hours
Send us your hex bar size, spindle taper angle, and quantity. Our engineers will reply with a firm price, a confirmed lead time, and a DFM check on your bore profile. If your drawing has a potential clash with the back taper or the grip length, we will flag it before you pay.
Email: sc@bquq.com WhatsApp: +86 13713157787
Before you finalize your cutting parameters, review our CNC cutting tool selection guide to match your insert grade to the hex stock material. And if you are designing a new spindle interface, our CNC machining tolerances guide explains how 0.005 mm TIR is achieved and verified in production.
This Cnc Machined Auto Lathe 52 Type Collet With Hex Bar Stock is precision manufacturing done right, made in China with a no-MOQ policy. We have been machining collets since 2004, and we know what a 4000 RPM spindle does to a poorly ground bore. Do not gamble on a cheap import. Get a quote today.