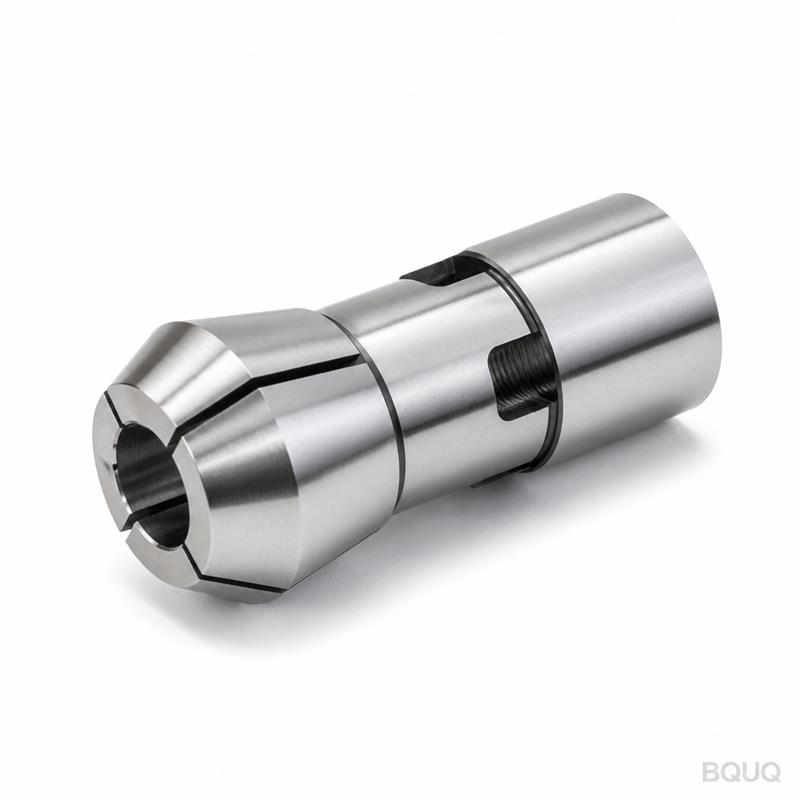
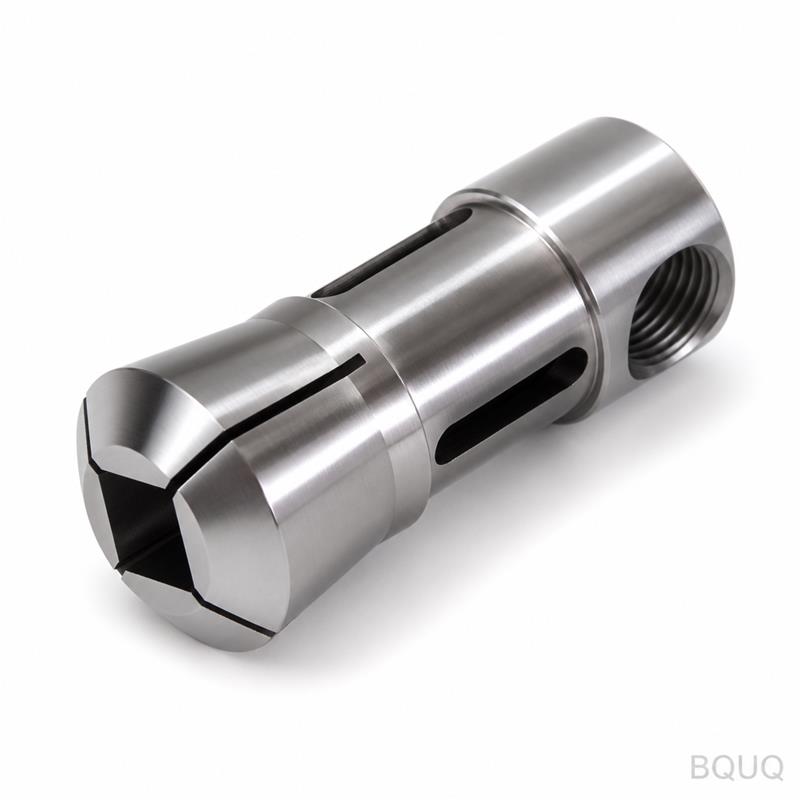
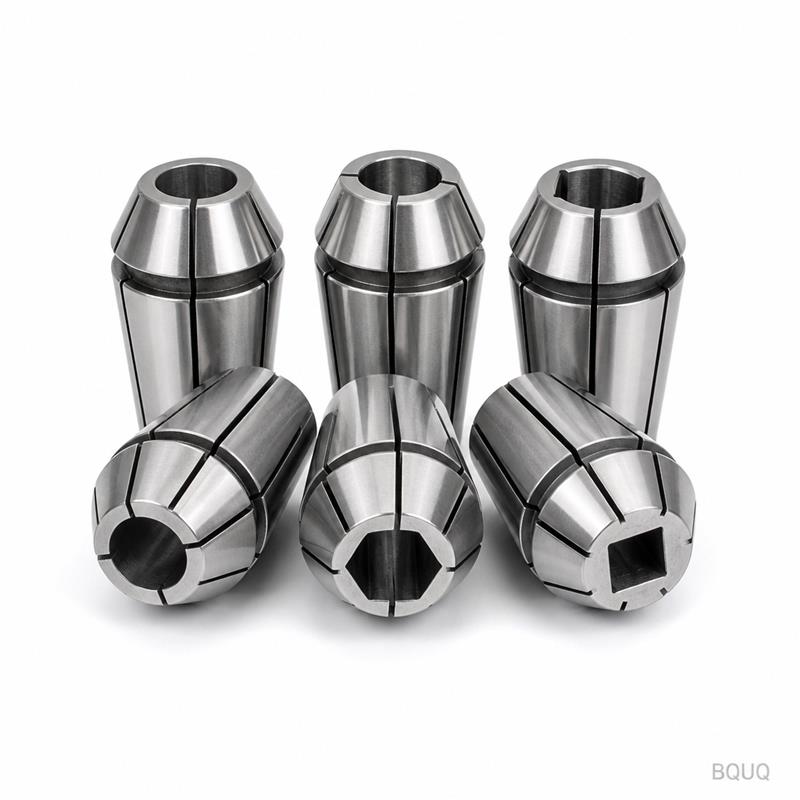
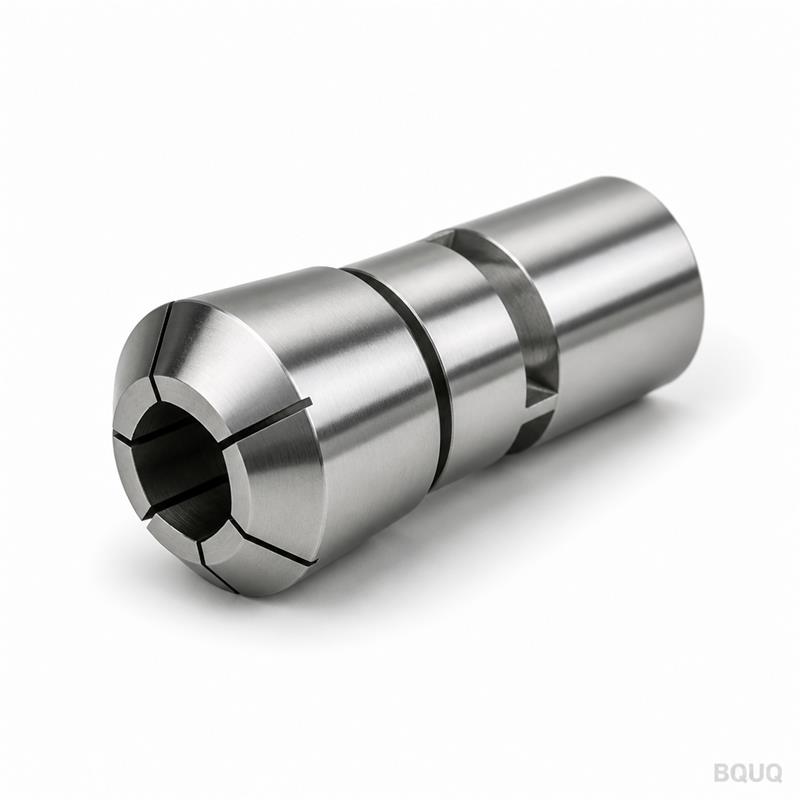
This is a Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck built for high-speed auto lathes and Swiss-type machines. You get concentric gripping with 0.008 mm TIR run
BQUQ Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck
This is a Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck built for high-speed auto lathes and Swiss-type machines. You get concentric gripping with 0.008 mm TIR runout, a hardened body
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck built for high-speed auto lathes and Swiss-type machines. You get concentric gripping with 0.008 mm TIR runout, a hardened body at 58–60 HRC, and a 7-day lead time from our Dongguan factory. It holds round stock from 3 mm to 34 mm bore without deflection, so your parts stay in tolerance on the first pass.
How the 34 Type Round Bore Grips Without Marking or Slippage
The spring collet uses a ground round bore with a full-length slit pattern that closes evenly around the workpiece. Unlike hex or square collets, the circular contact area distributes clamping force across 360 degrees, preventing surface marks on finished shafts and bushings. The 34 type refers to the max bore diameter in millimeters—34 mm—and the auto lathe taper angle matches standard A5 or A6 spindles. We cut the slits with wire EDM after heat treatment, so the spring action stays elastic up to 10,000 cycles without fatigue.
Material Selection and Heat Treatment for 58–60 HRC
We start with 8620 alloy steel or equivalent (AISI 8620), then carburize and quench to a case depth of 0.8–1.2 mm. The core stays tough at 35–40 HRC to absorb shock, while the surface reaches 58–60 HRC for wear resistance. The round bore is honed after hardening to Ra 0.2 µm, which reduces friction during collet closing and keeps the gripping force repeatable. If you need corrosion resistance, we offer a 440C stainless version at the same hardness—just specify that in your drawing.
Machining Sequence That Keeps Runout at 0.008 mm
We machine the blank on a CNC lathe, then heat treat, then finish grind the taper and bore on a cylindrical grinder. The taper is ground in a single setup with the bore to eliminate concentricity error. After grinding, we test each collet on a mandrel with a dial indicator—any unit exceeding 0.008 mm TIR is scrapped, not reworked. This sequence is why our collets hold tolerance on high-RPM spindles (up to 8,000 RPM) without vibration.
Inspection Before Every Shipment: Air Gauge and Hardness Test
Every Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck goes through a 3-point check. First, we air-gauge the bore diameter to 0.005 mm accuracy. Second, we test hardness on a Rockwell C scale at three positions. Third, we run a functional close-open test on a live spindle to verify spring return. We send a digital inspection report with photos and measurement data with each order—this is standard, not a paid extra.
Compatibility with Your Existing Auto Lathe Tooling
This collet fits standard auto lathe chucks with a 34 mm round bore and a 1:10 taper angle. It works with collet chucks from Tornos, Citizen, Star, and Tsugami, as well as generic Chinese auto lathes. The outer diameter is 45 mm, length is 60 mm, and the thread is M22x1.5 for pull-back actuation. If your spindle uses a different taper, we can remanufacture the angle in 5 days—send us your current collet dimensions and we will match it exactly.
Why Precision Manufacturing in China Matters for Your Cost
We make this collet in Dongguan, China, at a 5,000 m² factory with 40 CNC machines and 15 grinders. Precision manufacturing in China does not mean lower quality—it means lower overhead. You pay 30–40% less than a US or German equivalent, but you get the same 0.008 mm runout and 58–60 HRC hardness. Our QC team has 15 years of experience in collet production, and we have shipped over 50,000 units to automotive and medical device plants in Europe and North America.
Packing, Lead Time, and Global Shipping Options
Each collet is individually wrapped in anti-rust paper, placed in a foam-lined box, and shipped in a rigid carton. Standard lead time is 7 days for stock sizes (3–34 mm), and 12 days for custom bores. We ship via DHL or FedEx, with delivery to the US in 4–5 days and to Europe in 3–4 days. For bulk orders, we use sea freight—your cost drops to about $0.50 per unit for shipping. All shipments include a commercial invoice and certificate of origin.
Parameter
Value
Product Type
Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck
Bore Diameter Range
3 mm – 34 mm (standard stock sizes)
Outer Diameter
45 mm ±0.01 mm
Length
60 mm ±0.02 mm
Taper Angle
1:10 (custom angles available)
Material
AISI 8620 alloy steel or 440C stainless
Hardness (Surface)
58–60 HRC (case depth 0.8–1.2 mm)
Core Hardness
35–40 HRC
Runout (TIR)
0.008 mm max
Surface Finish (Bore)
Ra 0.2 µm
Gripping Force Repeatability
±2% over 10,000 cycles
Max Spindle Speed
8,000 RPM
Lead Time (Stock)
7 days
Lead Time (Custom Bore)
12 days
MOQ
No MOQ—buy 1 or 10,000
Country of Origin
Made in China (Dongguan)
Choosing the Right Bore Size and Tolerance Grade
Stock bores are ground to H7 tolerance (0/+0.021 mm for 34 mm). For high-precision work, we offer H6 (0/+0.013 mm) at no extra cost if you order 20 pieces or more. The round bore is straight, not tapered, so it grips the full length of the workpiece—this reduces chatter on long shafts. If your stock has a diameter variation, we recommend ordering the collet 0.05 mm under your nominal stock size for a secure grip. For a deeper look at how cutting tool selection affects your machining results, read our CNC cutting tool selection guide.
Customizing the Collet for Non-Standard Workpieces
We can modify the round bore to any diameter between 3 mm and 34 mm, including stepped bores for parts with shoulders. We can also add a slot for flat stock or change the slit pattern to reduce spring rate. Custom bore diameters are ground from solid, so they maintain the same 0.008 mm runout. Lead time for custom bores is 12 days, and there is no tooling charge for quantities above 50 pieces. Send us a simple sketch with your required bore size and length, and we will confirm the design within 24 hours.
Maintenance Tips to Extend Collet Life Beyond 10,000 Cycles
Clean the bore with compressed air after every 500 cycles to remove metal chips. Apply a light coat of spindle oil to the taper before each installation—this prevents galling and ensures smooth closing. Do not over-tighten the draw tube; use a torque wrench set to the value in your machine manual. If you see a wear mark on the bore, send the collet back to us for regrinding—we offer a reconditioning service at 50% of the new price, which restores runout to 0.008 mm.
How We Handle Quality Control for Large Orders
For orders above 100 pieces, we use a statistical process control (SPC) system. Every 10th collet is pulled from the batch and tested for runout, hardness, and bore diameter. We keep the SPC charts for 3 years and can share them with your quality department on request. For critical applications, we offer 100% inspection with a CMM report—this adds 2 days to lead time but guarantees zero defects. Our factory is ISO 9001:2015 certified, and we follow AS9100 practices for aerospace customers.
Shipping and Packaging for International Orders
We package each collet in a rigid plastic tube to prevent damage during transit. For orders under 10 pieces, we use a padded envelope. For larger orders, we use wooden crates that meet ISPM 15 standards. Every package includes a packing list, a certificate of conformity, and a material test certificate from our steel supplier. We ship FOB Shenzhen or CIF any major port—you choose the Incoterm. For urgent orders, we can ship by air freight with a guaranteed 48-hour dispatch from our warehouse.
What is the minimum order quantity (MOQ) for this collet chuck?
No MOQ—you can order a single piece for prototyping or 10,000 pieces for production, and the unit price is the same for any quantity above 10.
Can you customize the bore diameter or the taper angle?
Yes, we can grind any bore diameter from 3 mm to 34 mm and adjust the taper angle to match your spindle, with a 12-day lead time for custom specs.
How do you guarantee the 0.008 mm runout on every unit?
We test each collet on a precision mandrel with a dial indicator after grinding, and any unit exceeding 0.008 mm TIR is scrapped, so the shipped product is always within spec.
What is the standard lead time for stock sizes?
Stock sizes (3–34 mm) ship in 7 days from our Dongguan factory, and custom bores take 12 days; we provide tracking numbers within 24 hours of dispatch.
Need a firm quote for your next run? Send your drawing or your required bore size to sc@bquq.com, and we will reply within 12 hours with pricing and a delivery date. For urgent questions, WhatsApp us at +86 13713157787. If you are still deciding on tolerance grades, our CNC machining tolerances guide explains how to specify the right fit for your application. We are ready to ship—no MOQ, made in China, and built to hold your parts perfectly.