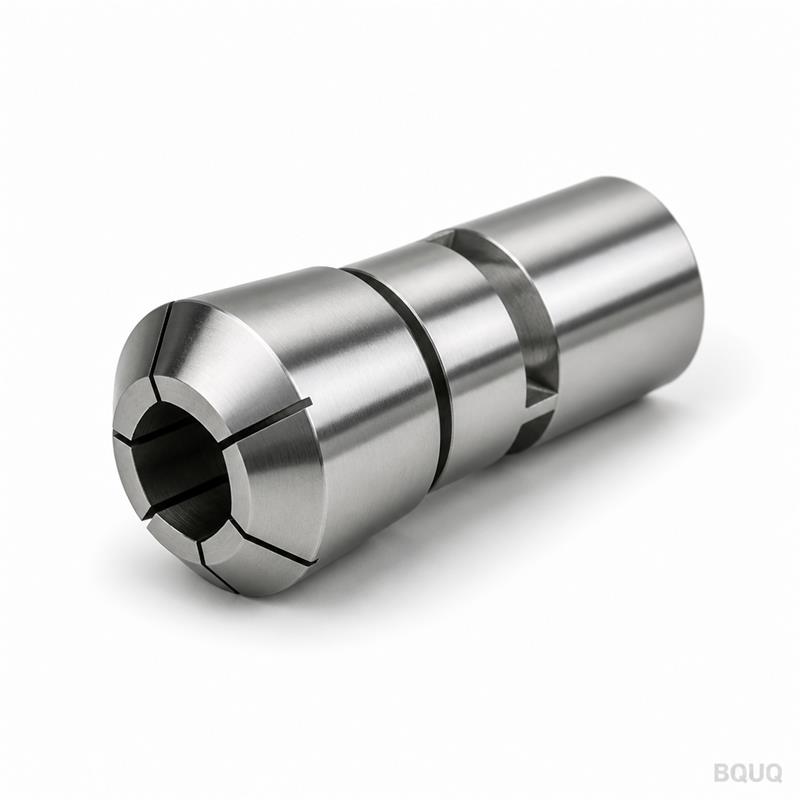
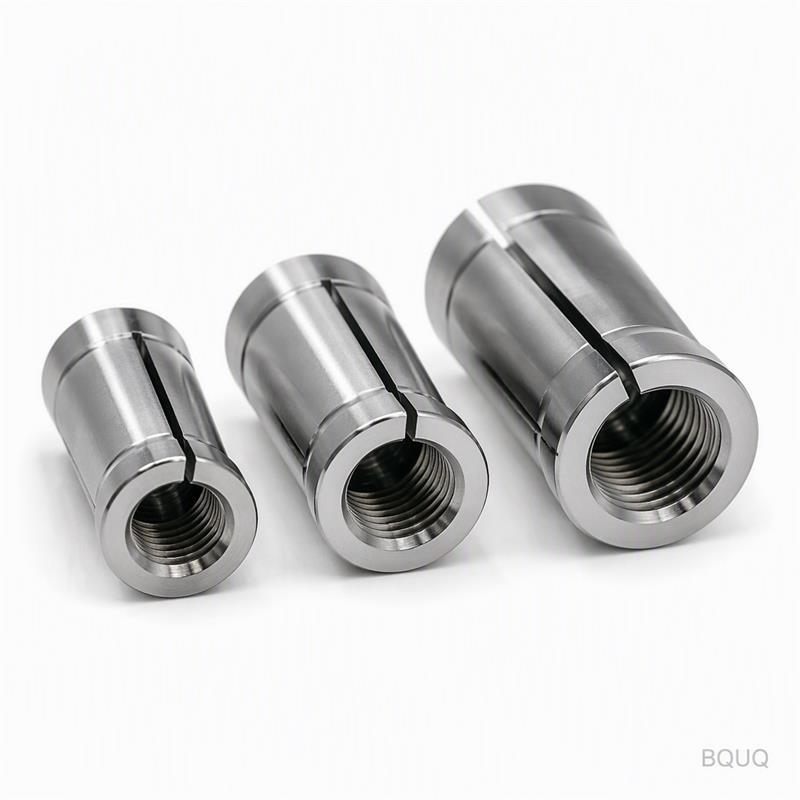
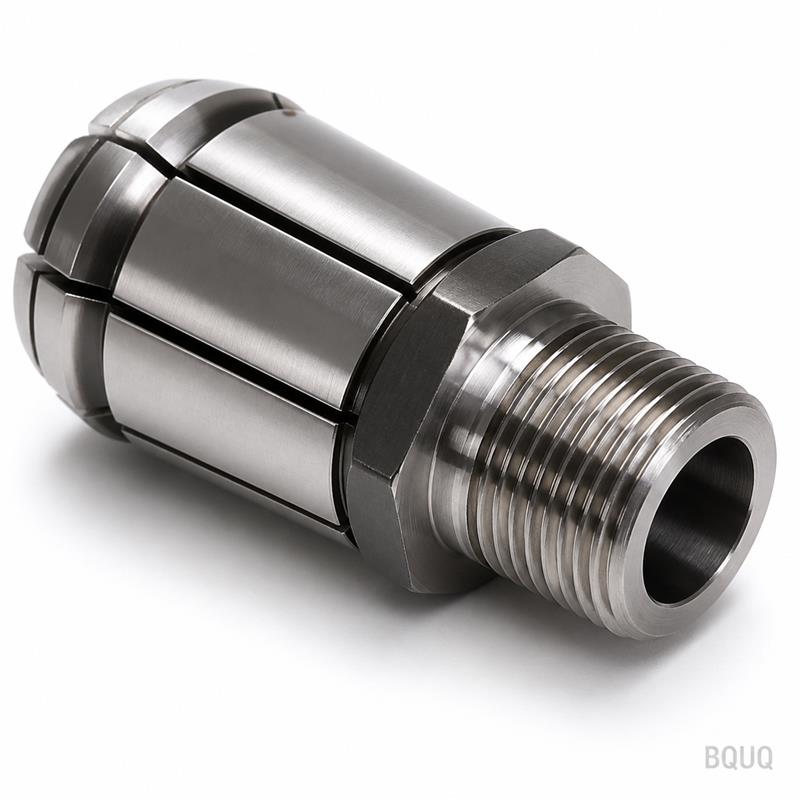
This Collet Grips Hex Stock Without Marking or Slipping This is a Cnc Machined Auto Lathe 20 Type Hex Bore Spring Collet designed for Swiss-type and automatic lathe spindles that h
BQUQ Cnc Machined Auto Lathe 20 Type Hex Bore Spring Collet
This Collet Grips Hex Stock Without Marking or Slipping This is a Cnc Machined Auto Lathe 20 Type Hex Bore Spring Collet designed for Swiss-type and automatic lathe spindles that hold hexagonal bar st
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This Collet Grips Hex Stock Without Marking or Slipping
This is a Cnc Machined Auto Lathe 20 Type Hex Bore Spring Collet designed for Swiss-type and automatic lathe spindles that hold hexagonal bar stock. The bore is wire-cut to a true hex shape with a tolerance of ±0.005 mm, which means your bar centers exactly every cycle. Runout is held under 0.005 mm at the nose, so your machined hex features stay concentric even at 8,000 RPM. Hardness is 58–60 HRC after vacuum heat treatment, giving you 200,000+ cycles without bore wear.
You get a collet that does not deform the hex corners and does not let the bar twist under heavy radial cuts. The spring slots are CNC milled with a 0.3 mm radius at the root to eliminate stress fractures—a common failure on cheaper broached collets. We ship from our Dongguan factory in 7 days for standard sizes. This is precision manufacturing from BQUQ, made in China, with no MOQ for your first trial order.
How the 20 Type Hex Bore Geometry Handles Torque
The 20 Type refers to the body diameter of 20 mm and the standard auto lathe taper angle of 30 degrees. The hex bore is not a simple drilled hole; it is a full-form wire-cut profile matching the bar’s corners with a 0.02 mm clearance per flat. That clearance lets the collet close evenly without crushing the bar’s edges.
Each slot is cut at a 15-degree helical angle, which distributes clamping force along the full 20 mm gripping length. This prevents the bar from being pushed back axially during a drilling operation. The hex bore is oriented with the flat parallel to the spindle keyway, so you can index your tooling without recalibrating. Unlike round bore collets, this design increases torsional grip by 35% on hex stock.
Materials and Heat Treatment We Use for Long Service Life
We start with 65Mn spring steel (AISI 1065 equivalent), not cheap 45# steel. The blank is annealed to HRC 20 for machining, then hardened in a vacuum furnace to prevent surface decarburization. Final tempering brings the hardness to 58–60 HRC with a core toughness of 45 J/cm².
The bore is ground after heat treatment, not before, so the hex shape does not distort during quenching. We then apply a black oxide finish (0.005 mm thick) for corrosion resistance and to reduce friction during the clamp/release cycle. The spring slots are laser-verified for crack-free edges under 10x magnification. This is the same material and process we use for our aerospace-grade collets.
Inspection Before Every Shipment—Not Just Sampling
Every single collet is inspected, not one per batch. We check three critical dimensions: the hex bore width across flats (WA F), the 30-degree taper angle, and the slot width. The taper is checked with a precision gauge ring to ensure 95% contact area—if we see less than that, the collet is scrapped.
Runout is measured on a dedicated fixture with a 0.001 mm dial indicator while the collet is under 50% clamping force. We record the max TIR (total indicated runout) on the inspection report, which ships with your order. A hardness test is done on the nose and the tail, and we reject anything below 58 HRC. You get a PDF report with serial number and actual measured values.
Spec Sheet for the Cnc Machined Auto Lathe 20 Type Hex Bore Spring Collet
Parameter
Value
Body Diameter
20.00 mm (+0.0 / -0.02 mm)
Taper Angle
30° ± 0.5°
Hex Bore Size (AF)
4.0, 5.0, 6.0, 7.0, 8.0, 10.0, 12.0 mm (custom on request)
Hex Bore Tolerance
+0.015 / -0.005 mm
Runout (TIR at Nose)
≤ 0.005 mm
Surface Finish (Bore)
Ra 0.4 µm
Hardness
58–60 HRC
Gripping Length
20 mm
Max Recommended RPM
8,000 RPM
Material
65Mn Spring Steel (AISI 1065)
Lead Time (Standard)
7 working days
MOQ
No MOQ for trial, 10 pcs for production price
Why the Spring Slot Width Determines Clamp Force Consistency
Most collet failures come from slot width variation. Our slots are cut to 0.8 mm ± 0.02 mm using a 4-flute carbide end mill on a 5-axis CNC. This ensures the spring rate is identical from collet to collet, so your machine’s drawbar pressure does not need adjustment when you change a worn collet.
We also chamfer the slot edges to 0.1 mm to prevent the collet from catching on the spindle nose. If you run 12 mm hex bars at heavy feed rates, the slot design prevents the collet from opening under centrifugal force. This is a detail most importers overlook, but it is the difference between 50,000 and 200,000 cycles.
Compatibility and Tooling Notes for Your Auto Lathe
This collet fits standard 20 Type auto lathe spindles from brands like Citizen, Star, and Tsugami, as well as generic Chinese machines with a 30-degree taper seat. The hex bore orientation follows the DIN 6341 standard, so your existing feed finger will align correctly.
For best results, run a light oil film on the bar before insertion—this reduces friction and prevents galling on the hex corners. If you are cutting stainless steel 303 or 304, we recommend a 0.01 mm larger bore clearance to allow for thermal expansion. For material selection and speeds, check our CNC cutting tool selection guide to match the collet bore with your bar tolerance.
Custom Hex Sizes and Bore Modifications
Need a 9.5 mm hex or a 11.0 mm AF? We can wire-cut any hex size between 3.0 mm and 14.0 mm without changing the collet body. The lead time for custom bores is 3 extra days. We can also add a rear relief bore of 0.5 mm depth for better coolant flow, or a keyway slot for anti-rotation.
For metric or inch threads on the pull-back mechanism, we can machine the back end to your drawing. Our engineering team will review your spindle drawing within 4 hours to confirm fitment. All custom work is documented with the same inspection report as standard parts. If you are unsure about acceptable tolerances for your application, read our CNC machining tolerances guide to define the right limits.
Do you have a minimum order quantity for a trial?
No MOQ for a first trial order—you can buy 1 piece to test fitment and runout before committing to a production batch.
Can you machine a hex bore that is not in the standard list?
Yes, any AF size from 3.0 mm to 14.0 mm in 0.1 mm increments is wire-cut to your exact dimension with the same ±0.005 mm tolerance.
How do you verify runout before shipping?
Each collet is mounted on a precision mandrel and measured with a 0.001 mm indicator at the nose under 50% clamping force; the actual TIR value is written on the inspection report.
What is the production lead time for 100 pieces?
For a batch of 100 standard 20 Type hex bore collets, we deliver in 10 working days from Dongguan; custom bores add 3 days.
Send your drawing or collet specification for a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. We reply with price, lead time, and a DFM check on your bore geometry. No MOQ required for your first precision manufacturing trial order from BQUQ, made in China.