What These Titanium Fasteners Are and Why They Hold Tight at 300C These are CNC machined titanium fasteners built for aerospace mounting, bracket, and housing assemblies where wei
BQUQ Cnc Machined Titanium Fasteners Aerospace Grade, Precision Made in China
What These Titanium Fasteners Are and Why They Hold Tight at 300°C These are CNC machined titanium fasteners built for aerospace mounting, bracket, and housing assemblies where weight and fatigue life
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What These Titanium Fasteners Are and Why They Hold Tight at 300°C
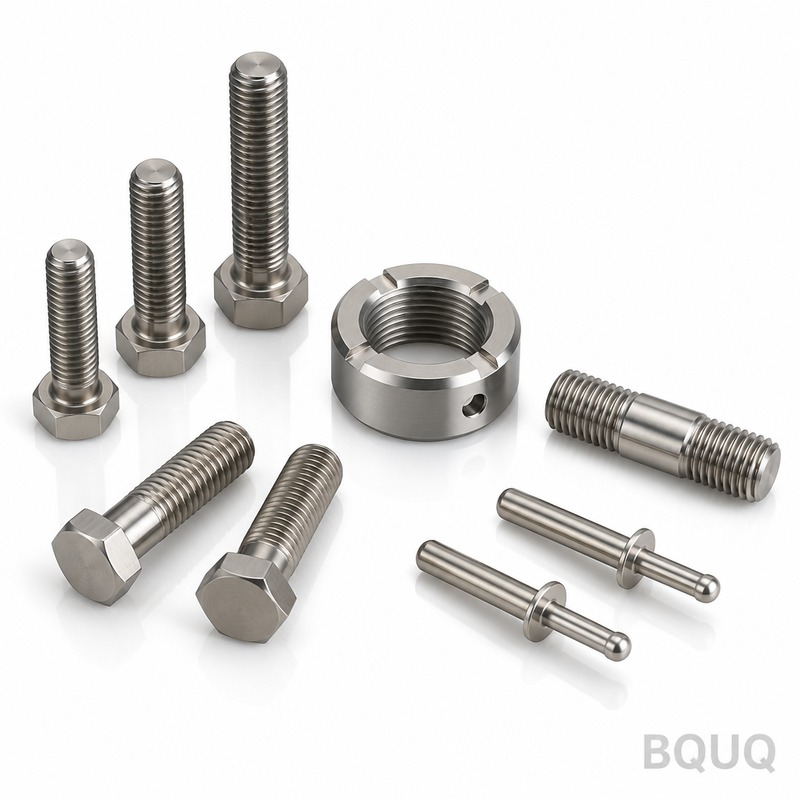
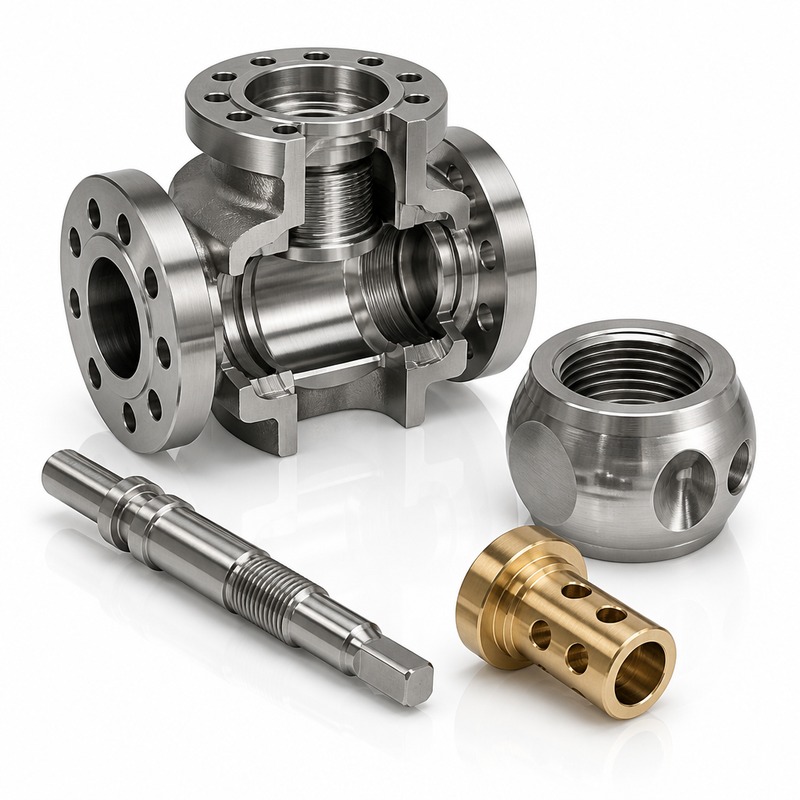
These are CNC machined titanium fasteners built for aerospace mounting, bracket, and housing assemblies where weight and fatigue life decide the design. We machine them from forged Ti-6Al-4V (Grade 5) bar stock to a consistent ±0.005 mm tolerance, with a guaranteed runout of 0.01 mm or less on the shank-to-head axis. Hardness lands at 32-36 HRC after solution treatment and aging, which gives you the strength of steel at roughly 56% of the weight. Lead time for standard diameters is 10 working days, and we ship from our Dongguan factory with full material traceability.
This is not a catalog item. Every batch is a precision manufacturing run tailored to your thread pitch, head style, and surface treatment. You send a drawing or a sample, and we return a firm quote within 12 hours. Because we keep a stock of pre-certified titanium bar in six common diameters, we can start cutting the same day you approve the order.
How We Control Thread Profile and Runout on a 5-Axis Mill
Threads on aerospace fasteners are not decorative. A loose fit under vibration fractures the lug. We cut all threads on a 5-axis mill using single-point thread milling, not taps. This gives us a thread profile that matches the pitch diameter tolerance class 3A (external) with zero tear-out on the crest. We hold runout under 0.01 mm by machining the head and shank in the same clamping operation. That means the driving socket, the bearing face, and the threaded axis are all true to each other. You will not need to shim or ream a hole to make the fastener seat flush.
For internal threads on nuts or inserts, we use a custom carbide thread mill with a 0.2 mm corner radius. This avoids the stress riser that a sharp V-thread creates at the root. Every fastener gets a 100% thread gauge check before it leaves the machine. We do not sample. We gauge every single piece.
Materials and Heat Treatment We Use for High-Cycle Fatigue
We machine three titanium grades, but aerospace fasteners almost always run on Ti-6Al-4V (Grade 5). This alloy gives you a tensile strength of 950 MPa minimum and a fatigue endurance limit of 500 MPa at 10^7 cycles. For higher temperature zones near the engine, we switch to Ti-6Al-2Sn-4Zr-2Mo (Grade 19), which holds its strength up to 400°C. For non-structural, corrosion-critical clips, we use commercially pure Grade 2.
Heat treatment is a solution anneal at 920°C, water quench, then aging at 540°C for 4 hours. This yields the 32-36 HRC hardness range. We never machine titanium in the fully hardened state because it work-hardens and tears. Instead, we rough in the annealed condition, then perform the final passes after heat treatment to maintain the ±0.005 mm tolerance. Each heat lot gets a hardness test on a Rockwell C scale, and the report goes with the shipment.
Surface Finish and Coatings That Stop Galling
Raw titanium fasteners gall when torqued. The threads seize against the mating part. We fix this in two ways. First, we run a final pass with a wiper insert to achieve Ra 0.4 µm on the bearing face and thread flanks. Second, we apply a dry film lubricant (MIL-PRF-46010) that reduces the coefficient of friction to 0.1. This coating is 8-12 µm thick and will not flake off under repeated assembly cycles.
If your application needs electrical bonding or extra corrosion resistance, we offer an anodize (Type II) in clear or yellow. That adds a 2-3 µm oxide layer. We do not recommend hard anodize on threads because it changes the pitch diameter. For most aerospace jobs, the dry film lube is the right call.
Inspection Before Every Shipment: CMM, Thread Gauges, and Hardness Reports
You get a full inspection report with every box. We run a coordinate measuring machine (CMM) check on critical diameters, head height, and thread concentricity. We use a calibrated GO/NO-GO thread gauge on 100% of the parts. Hardness is verified on two samples per heat treat batch. Surface finish is measured with a profilometer on the bearing face. If a part fails any check, it is scrapped, not reworked. We would rather lose a piece of titanium than ship a fastener that fails on your line.
All inspection equipment is calibrated to ISO 9001:2015 standards every 90 days. The calibration certificates are available on request. Material certificates (EN 10204 3.1) list the mill origin, heat number, and chemical composition for each bar.
Why No MOQ Means You Can Prototype Without a Factory Minimum
Most aerospace fastener suppliers demand a 500-piece minimum per size. That kills your prototype budget. At BQUQ, we run a no MOQ policy. You can order 10 pieces for a test jig or 10,000 for a production line. The per-piece price drops with quantity, but the setup cost is the same, so small orders are priced transparently. This is a precision manufacturing service, not a commodity parts bin. You pay for the engineering setup once, then the part price scales.
We keep pre-cut blanks for the six most common thread sizes (M3, M4, M5, M6, M8, M10) in Grade 5 titanium. That shortens lead time for prototype orders to 5 working days. For custom diameters, add 3 days for material cutting.
Pricing and Lead Time for Custom Aerospace Fasteners
Pricing depends on three variables: material grade, thread length, and coating. A standard M6 x 1.0 x 25 mm Grade 5 fastener with dry film lube costs about $2.80 per piece at 100 pieces. At 1,000 pieces, it drops to $1.90. For Grade 19 or custom head styles, add 20-30% for material and tooling. We provide a firm quote within 12 hours of receiving your drawing. The quote includes a lead time, not just a price. Standard lead time is 10 working days. For rush orders, we can compress to 5 days at a 15% surcharge.
What You Need to Send for an Accurate Quote
Send a STEP or IGES file, or a PDF drawing with dimensions. Include the thread size and pitch, head style (hex, socket cap, countersunk, or custom), and the coating requirement. If you have a torque spec, include it. That helps us choose the right dry film lubricant thickness. If you do not have a drawing, send a physical sample. We will reverse-engineer it and confirm the dimensions before cutting. Email sc@bquq.com or WhatsApp +86 13713157787. We respond within one business hour.
Common Mistakes We See in Aerospace Fastener Drawings
Three errors appear on most drawings we receive. First, the thread tolerance is too loose. A class 2A thread is standard for general use, but aerospace needs class 3A. Second, the fillet radius under the head is missing. Without a 0.3-0.5 mm radius, the part will crack at the head-shank junction under cyclic load. Third, the surface finish callout is on the shank but not on the thread flanks. Thread flanks need Ra 0.8 or better to prevent galling. We flag these issues in your quote and suggest corrections. This saves you a failed test cycle.
Dry film lubricant MIL-PRF-46010 (8-12 µm) or Type II anodize
Lead Time
10 working days standard, 5 days rush
MOQ
No MOQ (prototype orders accepted)
What is your minimum order quantity for these titanium fasteners?
No MOQ. We machine 10 pieces for a prototype or 10,000 for production at the same setup quality.
Can you customize the head shape, thread length, or coating?
Yes, we machine any head style (hex, socket, countersunk, torx, custom) and adjust thread length, coating, and material grade to your drawing.
How do you guarantee quality control on a small batch?
We inspect 100% of parts with CMM and thread gauges, plus hardness and surface finish checks per heat lot, and ship a full report.
What is your lead time for a custom fastener order?
Standard is 10 working days from drawing approval; rush orders at 5 days with a 15% surcharge.
Get a Firm Quote Within 12 Hours
Send your drawing or sample to sc@bquq.com or WhatsApp +86 13713157787. We reply within one business hour with a firm price and lead time. No generic estimates. No hidden tooling costs. Just a precise quote for your Cnc Machined Titanium Fasteners Aerospace application. Made in China, but with the same quality discipline you expect from a German or US shop. Start your order today.