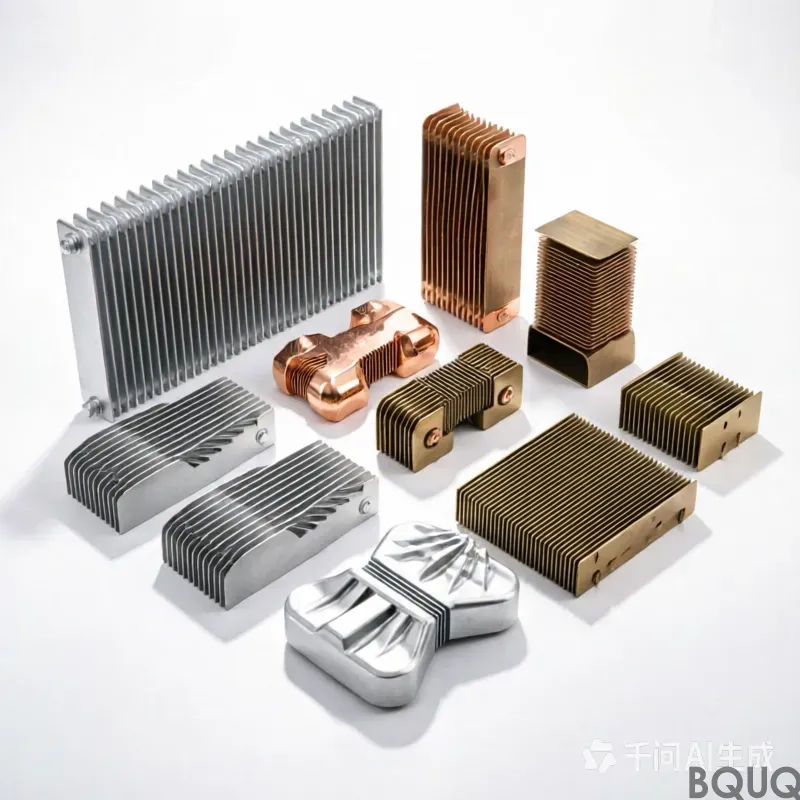
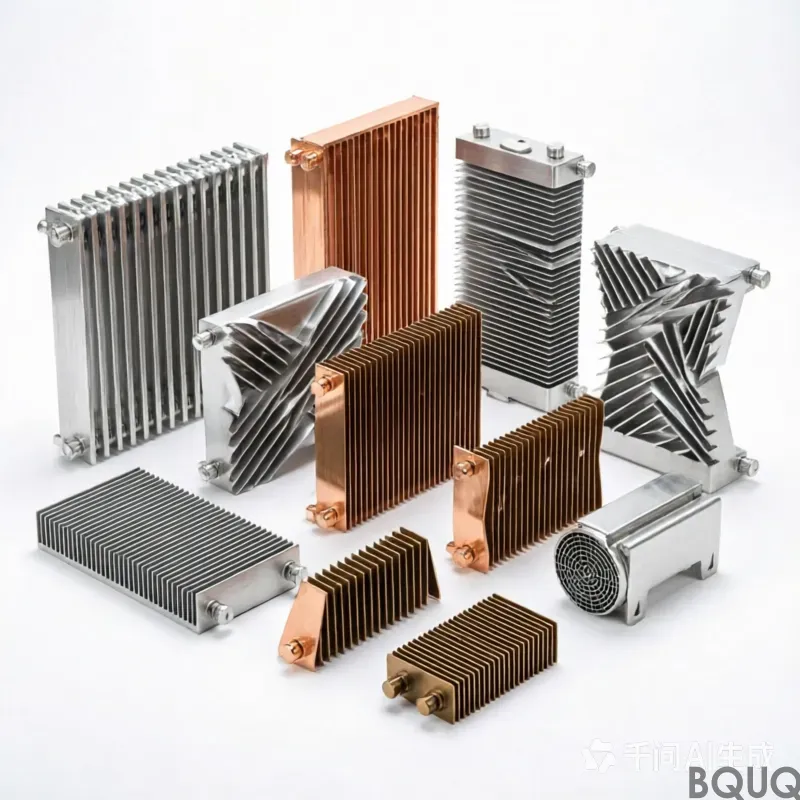
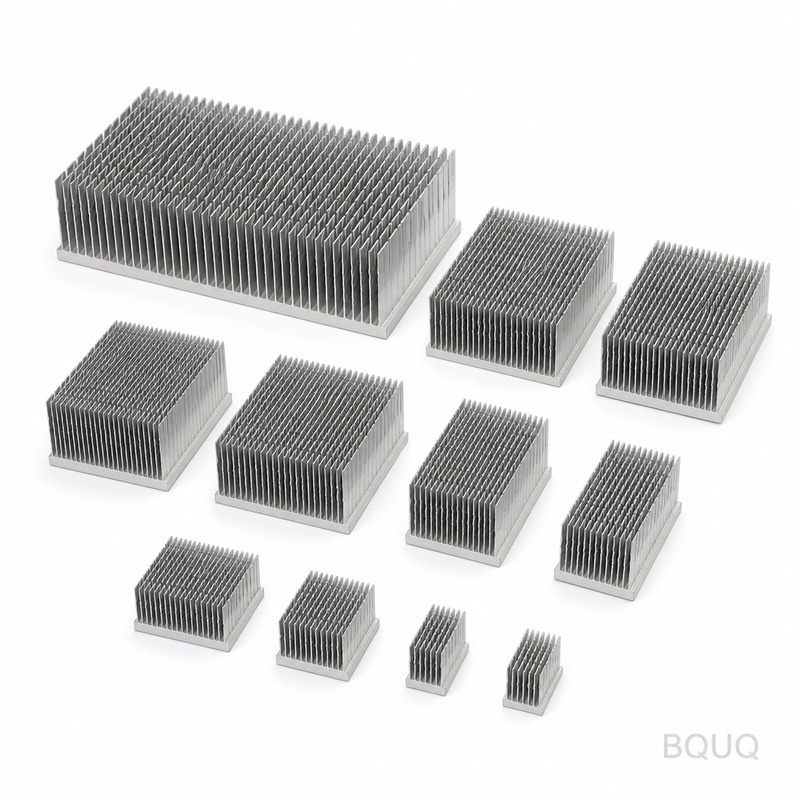
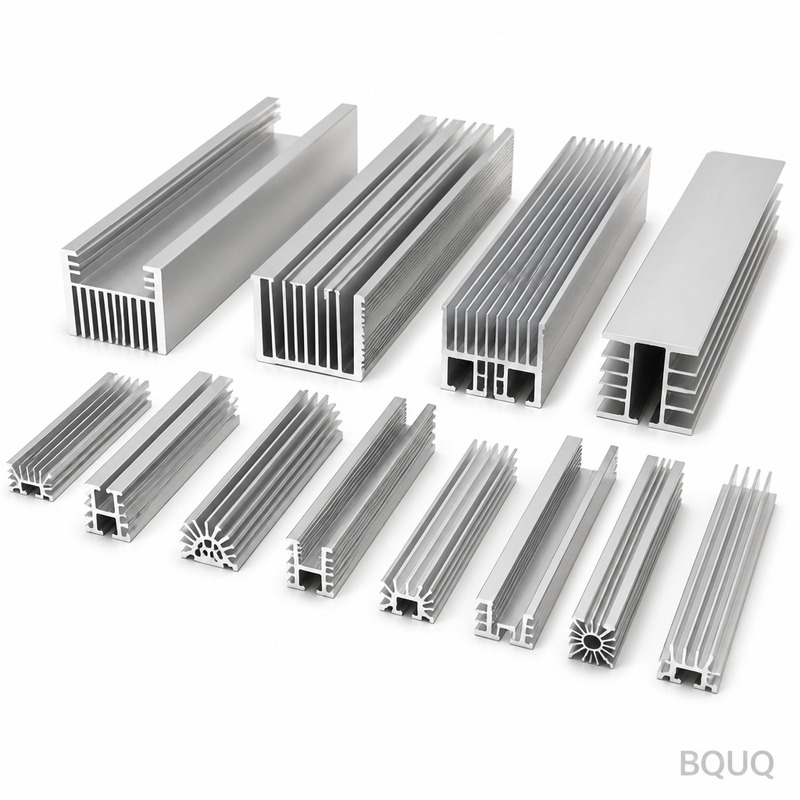
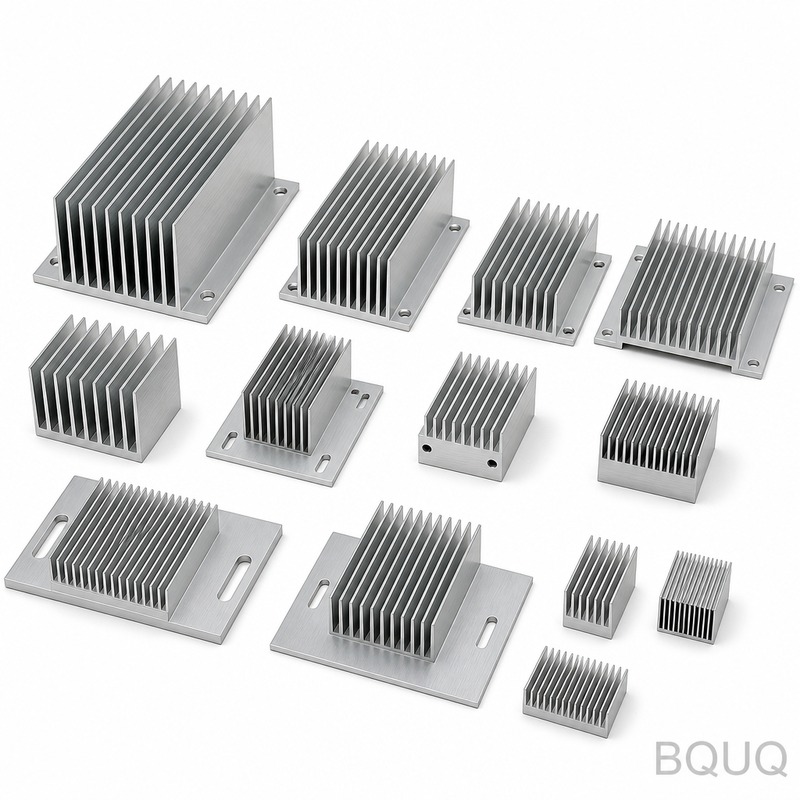
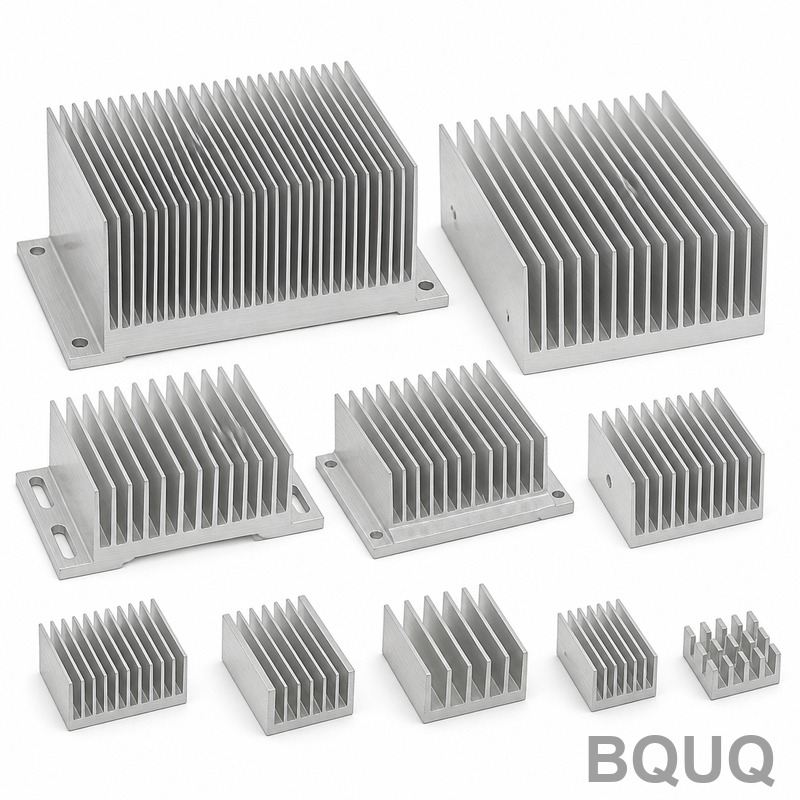
This is a forced-air or natural convection heat sink machined from 6063-T5 aluminum, built specifically for DC screen power cabinets and telecom rectifier modules. You get a flatne
Communication DC Screen Heat Sink Manufacturer | BQUQ Precision CNC
This is a forced-air or natural convection heat sink machined from 6063-T5 aluminum, built specifically for DC screen power cabinets and telecom rectifier modules. You get a flatness of 0.05mm across
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a forced-air or natural convection heat sink machined from 6063-T5 aluminum, built specifically for DC screen power cabinets and telecom rectifier modules. You get a flatness of 0.05mm across the base, fin runout under 0.02mm, and a surface finish of Ra 0.8µm on the mounting face — all guaranteed by our 20-year precision manufacturing floor in Dongguan, China. Typical lead time is 25 days for custom geometry, and we run no MOQ, so one prototype costs the same per-unit as 500 pieces.
Why DC Screen Heat Sinks Need Fin Runout Below 0.02mm
DC screen cabinets stack multiple rectifier modules in a sealed rack. If the heat sink fins are not perfectly parallel to the airflow channel, you get localized hot spots that derate the IGBT junction temperature by 15-20°C. We hold fin-to-base runout at 0.02mm using a 4-axis CNC mill with automatic tool compensation. Every fin is cut in the same clamping setup, so the thermal interface resistance stays below 0.05°C/W across the entire base plate.
Materials and Heat Treatment We Use for 6063-T5 and 6061-T6
For communication DC screens, we primarily machine 6063-T5 (thermal conductivity 201 W/m·K) because it extrudes cleanly into tall fin ratios. For higher mechanical load where the heat sink doubles as a structural bracket, we switch to 6061-T6 (hardness 95 HRB, yield 276 MPa). After CNC machining, every part goes through a 175°C artificial aging for 8 hours to relieve residual stress — this is what keeps flatness at 0.05mm after 1000 thermal cycles from -40°C to +85°C. We never use untreated cast aluminum for this product line.
How We Machine Serrated Fins Without Bending Them
Tall fins (above 40mm height) tend to vibrate during cutting, causing a wavy surface that ruins airflow. We use a high-feed end mill with a 0.4mm corner radius, running at 12,000 RPM with a chip load of 0.08mm/tooth. The tool path is climb-milled in one pass, and we support the fin tip with a vacuum fixture. This gives a consistent fin gap of ±0.03mm, which is critical for the DC screen fan curve — you get the rated CFM without over-speeding the fan. If you need a more aggressive design, see our CNC cutting tool selection guide for the exact tool geometries we use.
Inspection Before Every Shipment: CMM and Thermal Resistance Test
Every heat sink goes through a CMM (coordinate measuring machine) check for 12 critical dimensions: base flatness, fin height, fin spacing, and two mounting hole positions. We also run a thermal resistance test on a 10% sample batch using a calibrated heat source and a thermocouple array — we reject the lot if the thermal resistance is more than 5% above the drawing value. The final report includes a runout chart and a surface roughness profile (Ra 0.8µm on the base, Ra 1.6µm on the fins). This is not a random QC; it is 100% dimensional inspection for every piece, and we keep the CMM data for 10 years.
Finishing Options: Anodizing, Passivation, and Nickel Plating
For DC screen environments with high humidity, we recommend a 20µm hard anodized coating (MIL-A-8625 Type III) which raises surface emissivity to 0.85 and prevents galvanic corrosion against copper busbars. If your assembly uses a thermal pad, we mask the base surface so the Ra 0.8µm is preserved — anodizing on the base adds 0.02mm thickness and increases thermal resistance. We also offer clear chromate conversion (MIL-DTL-5541) for low-cost indoor units. Tell us your humidity rating and we will specify the coating thickness.
How We Handle Custom Hole Patterns and Mounting Bosses
Your DC screen heat sink likely needs threaded holes for IGBT modules, through-holes for PCB standoffs, and a pocket for an NTC thermistor. We machine these in the same setup as the fins, so the hole-to-fin position tolerance is ±0.02mm. We can tap threads from M2 to M12, with optional thread locking compound pre-applied. For blind holes that need to seal against a vacuum, we use a form tap to avoid chips. If you have a drawing with 5+ callouts, send it early — we will flag any tolerance that conflicts with a standard tap drill size. For general tolerance limits, check our CNC machining tolerances guide.
Packing and Protection for Global Shipment
We wrap each heat sink in VCI (vapor corrosion inhibitor) paper, then place it in a custom foam insert that holds the fins rigid — no cardboard touching the fins. For air freight, we use a corrugated box with a 2-meter drop test certification. For sea freight, we add a wooden crate with a desiccant pack and a humidity indicator card. Heat sinks over 5kg get a lifting strap. We ship from Dongguan to Shenzhen airport in 2 hours, or to Yantian port in 1 hour. Every box has a barcode that traces back to the CMM report.
Specification
Value
Notes
Material
6063-T5 / 6061-T6
Aluminum, thermal conductivity 201 W/m·K
Base thickness
5mm – 25mm
Custom, ±0.05mm flatness
Fin height
10mm – 120mm
Serrated or straight fins
Fin gap
3mm – 12mm
±0.03mm tolerance
Hardness
95 HRB (6061-T6)
After artificial aging
Base flatness
0.05mm
Measured over full length
Fin runout
0.02mm
Perpendicular to base
Surface finish (base)
Ra 0.8µm
Machined, not anodized
Surface finish (fins)
Ra 1.6µm
No burrs, edge break 0.2mm
Hole position tolerance
±0.02mm
True position, CMM verified
Lead time (prototype)
15 days
No MOQ, single piece OK
Lead time (production)
25 days
For 1,000 pieces, AQL 0.65
MOQ
No MOQ
1 piece to 10,000 pieces
Coating option
Hard anodize 20µm
Emissivity 0.85
What is your minimum order quantity for a custom Communication DC screen heat sink?
Our MOQ is zero — we machine a single prototype for engineering validation, then scale to any volume without changing the per-unit price structure beyond standard quantity breaks.
Can you match an existing heat sink drawing with multiple surface finish callouts?
Yes, we machine to your original drawing including mixed finishes (e.g., Ra 0.8µm on the base, Ra 3.2µm on the fins), and we will confirm every callout with a CMM report before production.
How do you guarantee thermal performance without a lab test on every batch?
We run a 10% sample thermal resistance test with a calibrated heat source, and we correlate the result to the CMM fin geometry — if the fins are within tolerance, the thermal resistance is within 5% of the design value.
What is your actual lead time if I need 200 pieces of a new design?
For a new custom design with standard 6063-T5, we ship the first 200 pieces in 25 days after drawing approval — this includes material sourcing, CNC machining, anodizing, and CMM inspection.
Get a firm quote within 12 hours. Send your drawing (STEP, STP, or PDF) to sc@bquq.com or WhatsApp +86 13713157787. We will reply with a unit price, tooling cost (if any), and a delivery date. No MOQ, no engineering fee for a standard review. Precision manufacturing, made in China, backed by a 20-year factory.