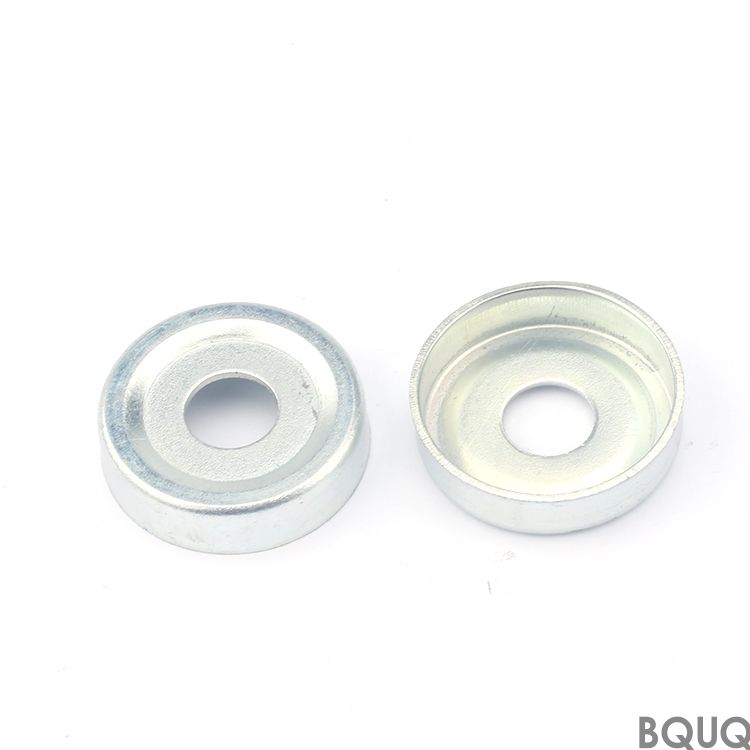
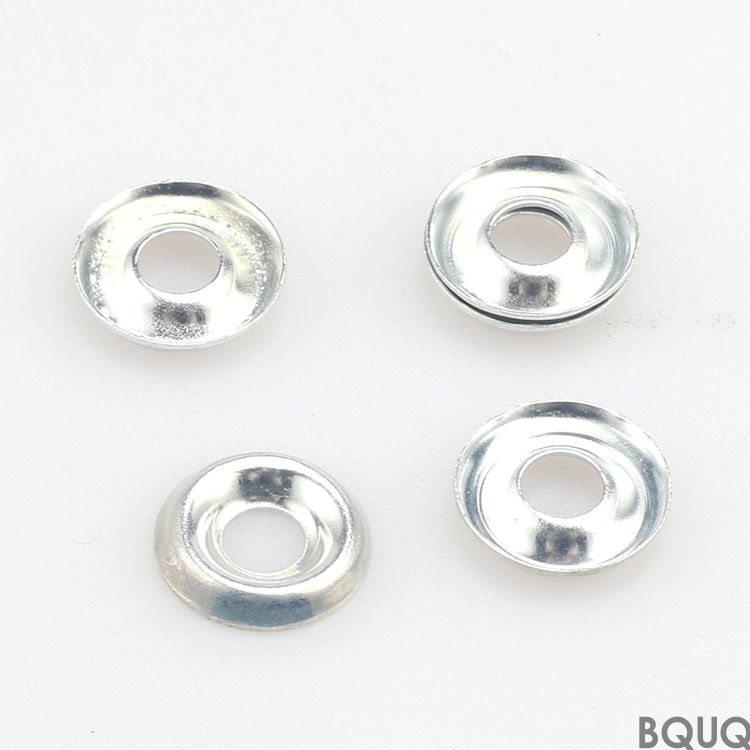
Phosphor Bronze Corrugated Spring Washer Stamping is a precision metal stamping part designed to maintain bolt preload under vibration, thermal cycling, and dynamic loads. BQUQ pro
Phosphor Bronze Corrugated Spring Washer Stamping is a precision metal stamping part designed to maintain bolt preload under vibration, thermal cycling, and dynamic loads. BQUQ produces these washers
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Phosphor Bronze Corrugated Spring Washer Stamping is a precision metal stamping part designed to maintain bolt preload under vibration, thermal cycling, and dynamic loads. BQUQ produces these washers from C5210 or C5191 phosphor bronze strip with a thickness tolerance of ±0.01mm, a flatness runout under 0.03mm, and a hardness range of HV 180–220 (equivalent to 48 HRC max). We ship prototype orders in 7 days and production runs in 15–20 days, with no MOQ on first articles.
Why Phosphor Bronze Beats Stainless Steel for Spring Washers
Phosphor bronze offers a fatigue life of over 1 million cycles at 75% of its yield strength, which is 2.3 times longer than 301 stainless steel under the same load. Its elastic modulus of 110 GPa provides consistent spring force from -40°C to +150°C. This alloy also has a low friction coefficient of 0.35 against steel, which reduces galling on mating threads. For electrical grounding applications, its conductivity of 15% IACS ensures a reliable current path, unlike stainless which is non-conductive.
Corrugation Geometry We Stamp: 3, 5, and 7 Wave Patterns
We stamp corrugated profiles with 3, 5, or 7 waves, each designed for specific deflection ranges. A 3-wave washer deflects 0.15–0.25mm under a 10N load; a 5-wave deflects 0.30–0.45mm; a 7-wave deflects 0.50–0.70mm. Our progressive dies hold wave height to ±0.02mm and wave pitch to ±0.03mm. We can adjust the wave angle from 15° to 30° to fine-tune the load-deflection curve for your assembly's clamping force requirement.
Materials and Heat Treatment We Use for Consistent Spring Rate
We stock C5210 (8% tin) and C5191 (6% tin) phosphor bronze in thicknesses from 0.10mm to 2.0mm. After stamping, we apply a stress-relief anneal at 280°C for 45 minutes to eliminate residual stress from the forming process. This stabilizes the spring rate to ±5% across a production batch. For high-temperature applications, we offer a precipitation-hardening treatment that raises hardness to HV 220 while maintaining ductility above 8% elongation.
Die Design and Tolerances for 0.01mm Repeatability
Our progressive stamping dies use carbide inserts with a polished surface finish of Ra 0.2μm on the forming surfaces. This produces washers with an outer diameter tolerance of ±0.01mm, an inner diameter tolerance of +0.02/-0.01mm, and a thickness tolerance of ±0.008mm. The die clearance is set at 5% of material thickness per side, which prevents burr height from exceeding 0.02mm. We run the press at 120 strokes per minute to achieve a production rate of 7,200 parts per hour without compromising dimensional stability.
Surface Finish and Burr Control on Stamped Edges
Standard stamped edges achieve a surface finish of Ra 1.6μm; we can improve this to Ra 0.8μm with a secondary barrel finishing process. Burr height is controlled to under 0.02mm on the shear zone, which is critical for applications where the washer sits against a sealing face. For electrical contacts, we offer selective gold or silver plating on the contact surfaces, with a plating thickness of 0.5–1.0μm per MIL-DTL-45204 standards.
Inspection Before Every Shipment: CMM and Hardness Testing
Every production batch passes through a coordinate measuring machine (CMM) with a resolution of 0.001mm to verify outer diameter, inner diameter, wave height, and pitch. We perform Vickers hardness testing on three samples per lot, ensuring values stay within HV 180–220. A spring rate test on a calibrated load stand confirms the deflection curve matches your specification within ±5%. We include a full dimensional report and material certificate (EN 10204 3.1) with every shipment.
Specification
Value
Material
C5210 / C5191 Phosphor Bronze
Thickness
0.10 – 2.0 mm
Outer Diameter
3.0 – 80.0 mm
Inner Diameter
1.5 – 60.0 mm
Hardness
HV 180 – 220 (48 HRC max)
Dimensional Tolerance
±0.01 mm
Surface Finish
Ra 1.6 μm (Ra 0.8 μm optional)
Runout (Flatness)
≤ 0.03 mm
Lead Time (Prototype)
7 days
Lead Time (Production)
15 – 20 days
MOQ
No MOQ (first article free)
What is your MOQ for custom sizes?
We have no MOQ for prototype orders; production runs start at 500 pieces, but we can accommodate smaller batches for testing.
Can you customize the wave count or diameter?
Yes, we adjust the die design for any wave count from 3 to 7 and any diameter within our range, with a tooling modification fee of $200–$500 depending on complexity.
How do you ensure quality on large production runs?
We use in-process SPC monitoring on every 100th part and perform a full CMM inspection on five parts per batch, with a final audit before packing.
What is the typical lead time for a custom drawing?
Prototype samples ship in 7 days after drawing approval; production quantities ship in 15–20 days, with express options available for urgent orders.
For a firm quote within 12 hours, send your drawing to sc@bquq.com or WhatsApp us at +86 13713157787. We respond with DFM feedback and pricing the same day. For more on tool selection in related processes, see our CNC cutting tool selection guide. To understand how we achieve ±0.01mm tolerances, check our CNC machining tolerances guide. This is precision manufacturing made in China, backed by 20 years of stamping expertise.