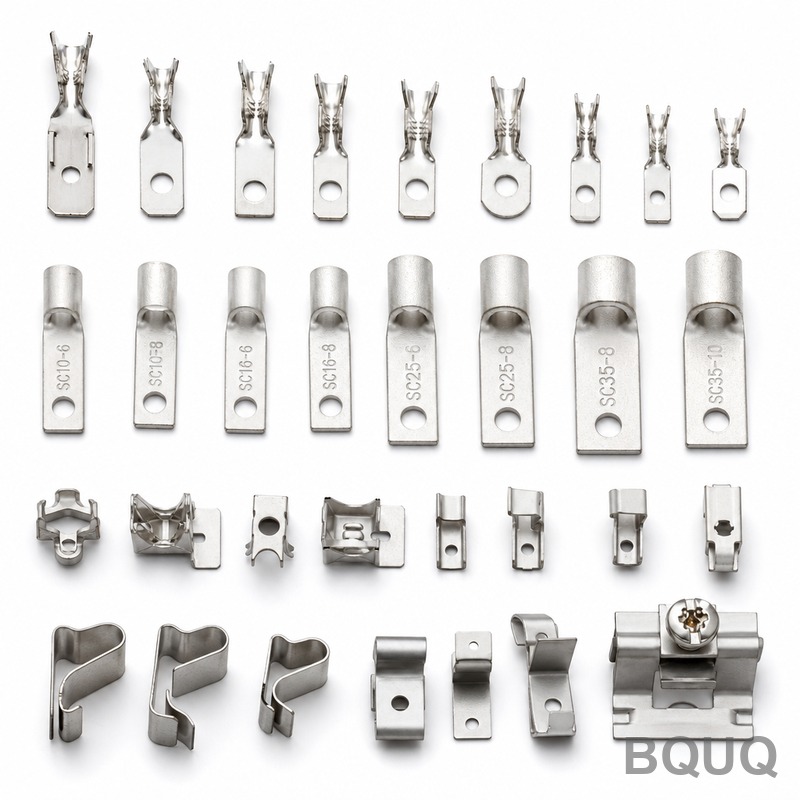
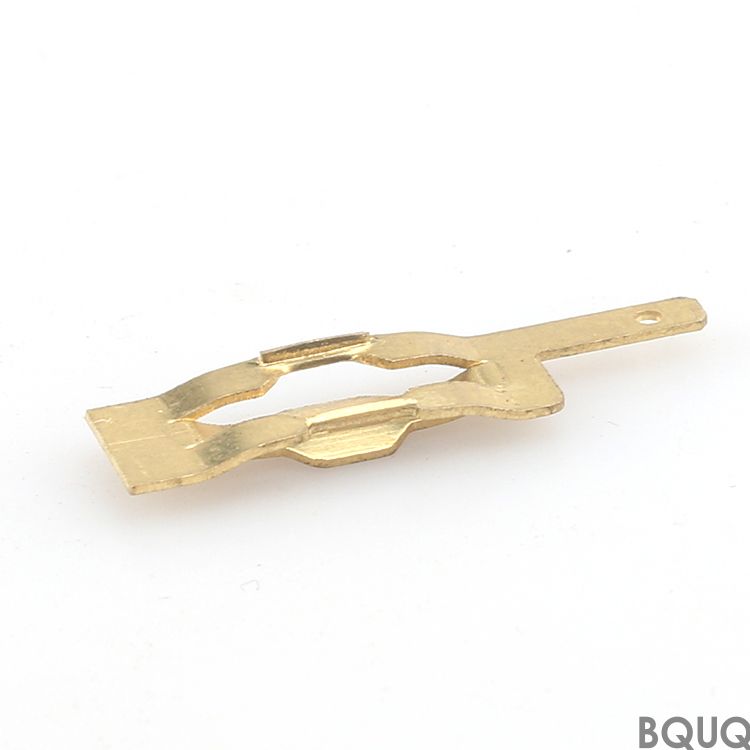
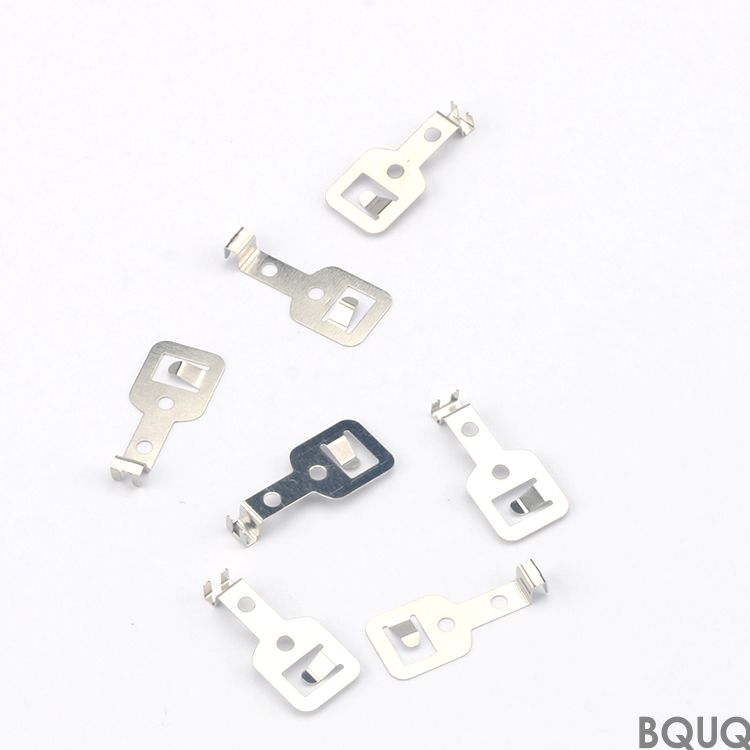
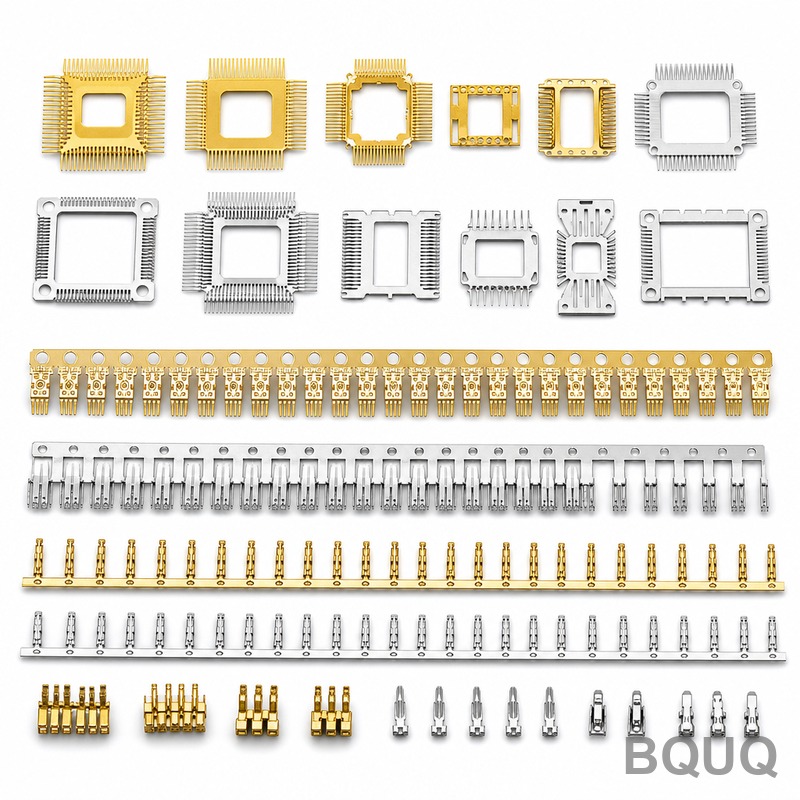
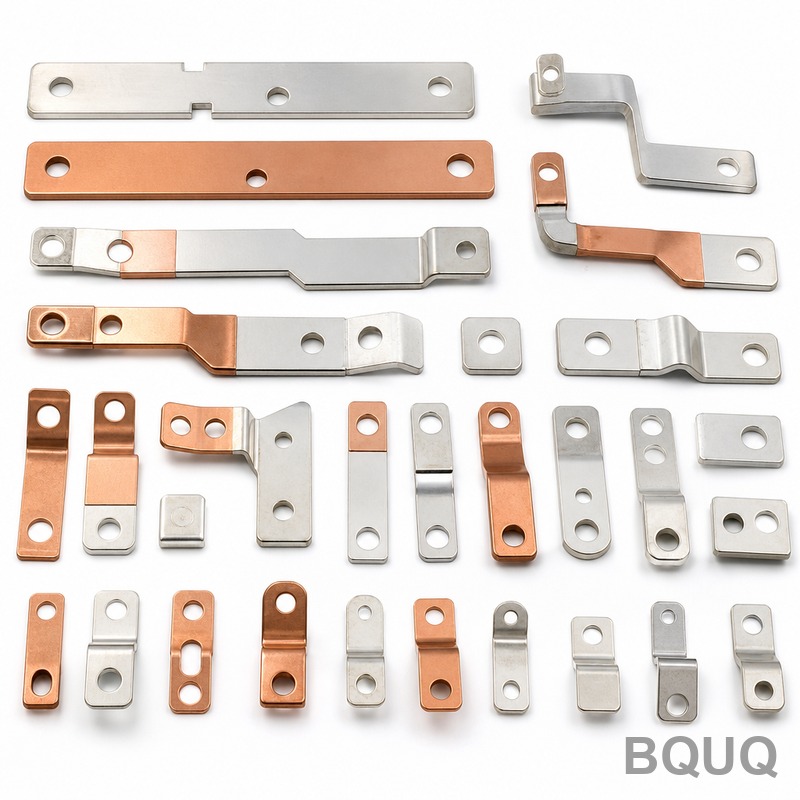
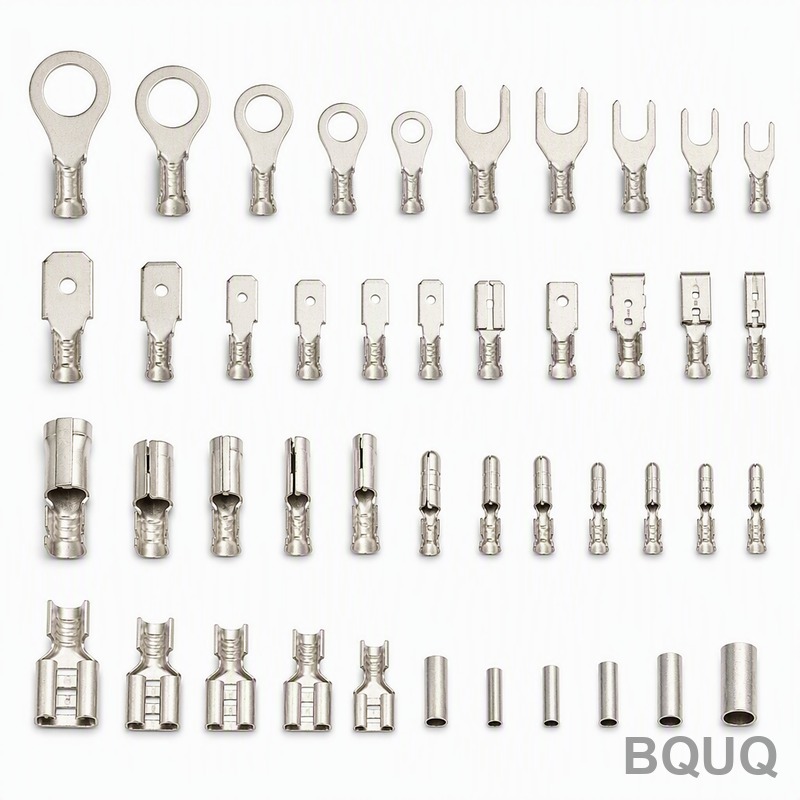
This is a complete line of solar junction box terminals and clips — stamped metal contacts that lock PV wires into place and carry current from the panel to the cable. Each part is
Solar Junction Box Terminals Clips Collection | BQUQ Precision Stamping
This is a complete line of solar junction box terminals and clips — stamped metal contacts that lock PV wires into place and carry current from the panel to the cable. Each part is formed on high-spee
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a complete line of solar junction box terminals and clips — stamped metal contacts that lock PV wires into place and carry current from the panel to the cable. Each part is formed on high-speed Bruderer presses with tolerances held to ±0.02 mm, surface finish at Ra 0.8, and hardness up to HV 450 for spring clips that survive 10,000 insertion cycles without losing grip force.
Why Our Stamped Contacts Hold 30A Without Overheating
The terminals are made from C1100 copper or C5191 phosphor bronze, depending on your current load. For 30A+ systems, we specify 0.6 mm thick C1100 with a selective silver plating (2–3 µm) on the contact zone. This drops contact resistance below 0.5 mΩ and keeps temperature rise under 30 K at rated current. For spring clips, we use C5191-H which gives a yield strength of 500 MPa — the clip keeps pressing against the PV wire even after 10,000 mating cycles. We also offer tin-plated versions for salt-spray environments (tested 96 hours per ASTM B117).
Tooling Die Design That Cuts Burr Height to 0.03 mm
Burrs are the number one cause of arcing in junction boxes. Our toolroom builds progressive dies with a clearance of 5–7% of material thickness on the punch and die. That clearance, combined with a micro-ground punch tip (Ra 0.2), holds burr height under 0.03 mm on the cut edge. We also add a secondary coined step for the contact spring fingers — this work-hardens the radius and removes any micro-cracks that could propagate under vibration. Every new die is validated with 50,000 test strokes before production begins.
Materials and Heat Treatment We Use for PV-Rated Parts
We stock four material grades specifically for solar junction box components: C1100 ETP copper (conductivity 101% IACS), C5191 phosphor bronze (spring temper), C7521 nickel silver (for corrosion resistance), and SUS301 stainless steel (for high-temperature bypass diode clips). Spring clips made from C5191 are age-hardened at 300°C for 2 hours to reach HV 350–450, while stainless clips get a 480°C bright annealing to restore elasticity. We do not use recycled copper — every coil comes with a mill certificate showing chemical composition and conductivity.
Inspection Before Every Shipment: CMM and Pull-Force Testing
We measure three critical dimensions on every batch: terminal width (to ±0.02 mm), clip gap (to ±0.03 mm), and solder pad flatness (to 0.05 mm total). A CMM (Zeiss Contura) checks the first article from each die set; for production lots, we pull 5 pieces per hour from the press and verify with a digital micrometer and a 50 N pull-force gauge. The pull test simulates a PV wire being yanked out — we require a minimum of 80 N retention force for a 2.5 mm² wire. Test reports are included with each shipment, showing measured values against your drawing callouts.
Packing and Delivery for Solar Junction Box Terminals Clips Collection
Parts are cleaned in an ultrasonic bath to remove stamping oil, then packed in anti-static bags with desiccant. We ship in telescopic cartons with 5-layer corrugation, each box holding 10,000–50,000 pieces depending on part size. For reels, we use 330 mm plastic reels with 4,000–8,000 pieces per reel, taped every 20 positions for easy SMT feeding. Standard lead time is 15 days for stamped parts without plating, 20 days with silver or tin plating. Air freight from Dongguan to LAX takes 3 days; sea freight to Rotterdam takes 25 days. We can also hold stock in our Hong Kong warehouse for JIT delivery.
How Our Stamping Process Differs from CNC Cutting for This Product
Stamping is the right process for high-volume terminals because it produces the part in one stroke — no material waste, no secondary machining. Our presses run at 200–400 strokes per minute, so a 100,000-piece order finishes in 2 days. CNC machining would take 10 times longer and cost 4–5 times more per piece. However, if your design has complex 3D bends or requires tight tolerances below ±0.01 mm, we will recommend a hybrid approach: stamp the flat blank, then CNC-machine the critical contact surface. See our CNC cutting tool selection guide for when cutting is the better choice.
Design Checks We Flag Before You Send the Final Drawing
We review every drawing for three common issues: (1) bend radius smaller than 1× material thickness — this cracks the grain structure; we suggest a minimum of 1.5× thickness for copper and 2× for stainless. (2) Tolerances tighter than ±0.02 mm on stamped features — we can hold these but the die cost goes up by 30%. (3) Plating specified on the entire part — we recommend selective plating only on the contact zone to save cost. If you are unsure about your tolerance stack-up, read our CNC machining tolerances guide for a general reference on what is achievable in precision manufacturing.
Selective silver (2–3 µm), tin (3–5 µm), nickel (2–3 µm)
Lead time
15 days (stamped), 20 days (plated)
MOQ
No MOQ — we run pilot lots from 1,000 pieces
What is the MOQ for a custom terminal design?
There is no MOQ — we will stamp 1,000 pieces for a pilot run and scale up to 1 million per month as your project grows.
Can you match an existing terminal from another supplier?
Yes, send us the drawing or a physical sample; we reverse-engineer the dimensions and material within 2 days, then quote tooling and piece price.
How do you guarantee quality for a high-volume order?
We run SPC on every press — control charts track width and gap every hour, and a final AQL 1.0 sampling inspection is done before packing.
What is the fastest lead time for a prototype?
We can ship soft-tooled prototypes in 7 days; hard tooling takes 20 days, and production parts follow 15 days after approval.
Send your drawing for a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. We reply with a full cost breakdown — tooling, unit price at 10k/50k/100k quantities, and delivery date. No MOQ, made in China, precision manufacturing guaranteed.