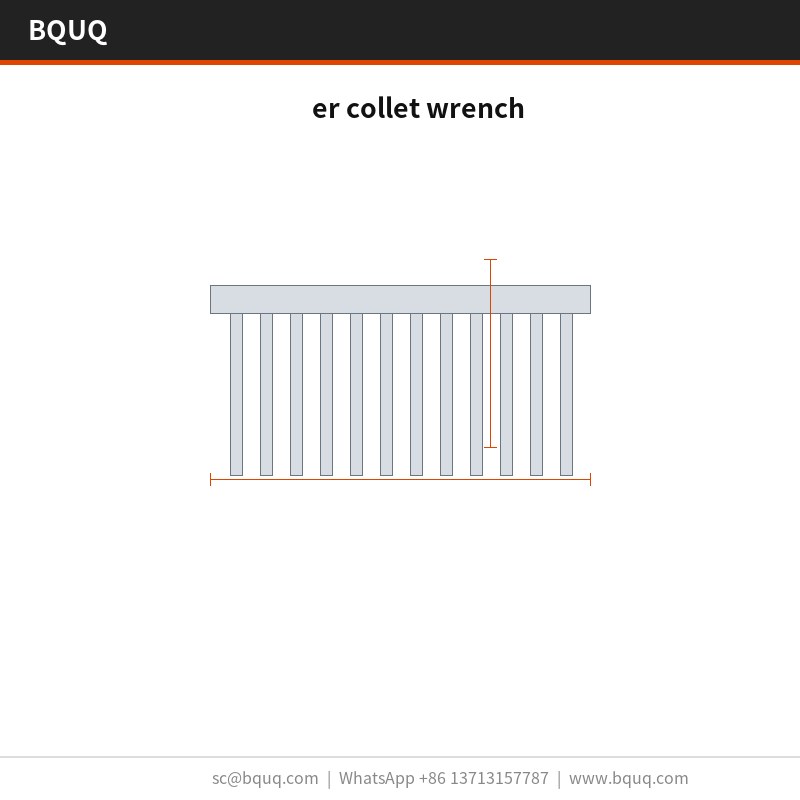
The ER collet wrench is a stamped one-piece tool with a base and fins, pressed from a single die in one stroke. Fin pitch stays within tolerance across a run, flatness on the mounting face is held directly from the tool, and the finish is applied after forming. Monthly output runs at capacity, and a single stroke forms the whole wrench so part cost stops scaling with complexity.
Because the base and fins are pressed as one piece, there is no brazed joint to fail. flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
A single stroke forms the whole er collet wrench, so part cost stops scaling with complexity. Tooling runs , and the cycle feeds a line.
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
The finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is , supplied with . For applications where drilling and tapping exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Flatness is checked on a against a limit, and fin pitch is verified optically at . Reports go out with each lot.
Incoming is checked for thickness and hardness before it enters the press. After forming, confirms and against the drawing.
Lot traceability runs from coil to carton: heat number, press stroke range and inspection record stay attached, so a field issue can be tied back to a specific run.
Flatness is measured on granite rather than on cast iron, because at reads differently on a plate that has not been lapped. Records keep both readings.
Where This Part Is Used
For drilling and tapping builds, the mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Where a er collet wrench runs at drilling and tapping volumes, part-to-part consistency decides field returns. on a run keeps the thermal curve inside one band.
In drilling and tapping, the base usually doubles as the mounting interface. with flat gives a stable surface for the drilling and tapping thermal pad.
For drilling and tapping prototypes, 10 working days covers drawing review and first article. Production lots move to 20 working days once the capability is signed off.
Specifications
Parameter
Value / Range
MOQ (prototype)
50 sets
MOQ (production)
1000 sets
Lead time (prototype)
10 working days
Lead time (production)
20 working days
FAQ: Your Questions Before Ordering
Which materials do you recommend?
is the standard choice. For drilling and tapping in a corrosive environment we specify 6063-T5 with ; for the highest conductivity we move to copper C110, which raises cost and weight but drops thermal resistance by roughly half at the same envelope.
How does this compare to an extruded er collet wrench?
Extrusion is cheaper above roughly 500,000 pieces per year and gives a smoother profile. Stamping wins below that and wherever fin gauge drops below 0.5 mm, because extrusion cannot hold consistently. For drilling and tapping prototypes, tooling cost usually decides it.
Can the er collet wrench be powder coated or plated?
Yes. Standard is . Powder coating to RAL 9005 adds about 0.1 mm to the base; zinc-nickel is better for grounding. Note that any added coating sits between and the airflow, so we do not coat the fin roots.
We supply a 2D drawing with the CMM report, and 3D STEP on request. Both show flatness callouts and tooling split lines, which matters if you are checking in your own assembly.
What quality certifications do you hold?
The plant is ISO9001 certified, and parts ship with RoHS and REACH declarations on request. Third-party SGS inspection can be arranged before the container is sealed, which is what most drilling and tapping buyers specify.
Standard steel; optional passivated route; copper C110 for conductivity
Tolerance
Fin pitch held within tolerance across a run; flatness held directly from tool
Lead time
Tooling runs; cycle feeds a line
MOQ
Monthly output runs at capacity
Capacity
Monthly output runs at capacity
Selection / comparison
Option
Best for
Trade-off
Stamped one-piece
Repeatable fin profile and no brazed joint
Low fin gauge limits thick-section strength
Extruded profile
Simple constant cross-sections
Cannot hold fin pitch as stamping does
Machined alternative
Complex features and tight details
Higher cost per part and finish cut at fin roots
Passivated route
Drilling and tapping exposure concerns
Adds a process step after forming
Copper C110
Conductivity matters more than weight
Higher material cost and weight
Process / inspection
Stage
Control
Record
Stamping
Die forms every fin in one stroke; pitch within tolerance
Tool setup and stroke record
Forming
Base and fins pressed as one piece; no brazed joint
One-piece verification
Flatness
Mounting face flatness held directly from tool
Flatness check record
Finish
Applied after forming; corrosion protection not cut at fin roots
Finish application record
Inspection
Inspection before every shipment
Shipment inspection record
Frequently Asked Questions
What is the fin pitch tolerance on the ER collet wrench?
The die forms every fin in one stroke, so pitch stays within tolerance across a run. This repeatable fin profile is what extrusion cannot hold. The flatness on the mounting face is also held directly from the tool, keeping thermal interface contact uniform.
Can the ER collet wrench be supplied in copper C110?
Yes. Where conductivity matters more than weight, copper C110 raises thermal performance. The standard material is supplied with a standard finish. For drilling and tapping exposure concerns, we recommend the passivated route. The finish is applied after forming.
How does stamping compare to extrusion for fin profile?
Stamping gives a repeatable fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within tolerance across a run. Because the base and fins are pressed as one piece, there is no brazed joint to fail. A single stroke forms the whole wrench.
What is the monthly output capacity for this part?
Monthly output runs at capacity. Tooling runs, and the cycle feeds a line. A single stroke forms the whole ER collet wrench, so part cost stops scaling with complexity. Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile.
Is the finish applied before or after forming?
The finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives. For applications where drilling and tapping exposure is a concern, we recommend the passivated route. Where conductivity matters more than weight, copper C110 raises thermal performance.
What inspection is done before shipment?
Inspection before every shipment. The die forms every fin in one stroke, so pitch stays within tolerance across a run. Flatness on the mounting face is held directly from the tool. The finish is applied after forming, so corrosion protection does not get cut through at the fin roots.
Why choose a stamped ER collet wrench over a machined one?
Stamping gives a repeatable fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within tolerance across a run. Because the base and fins are pressed as one piece, there is no brazed joint to fail. A single stroke forms the whole wrench, so part cost stops scaling with complexity.