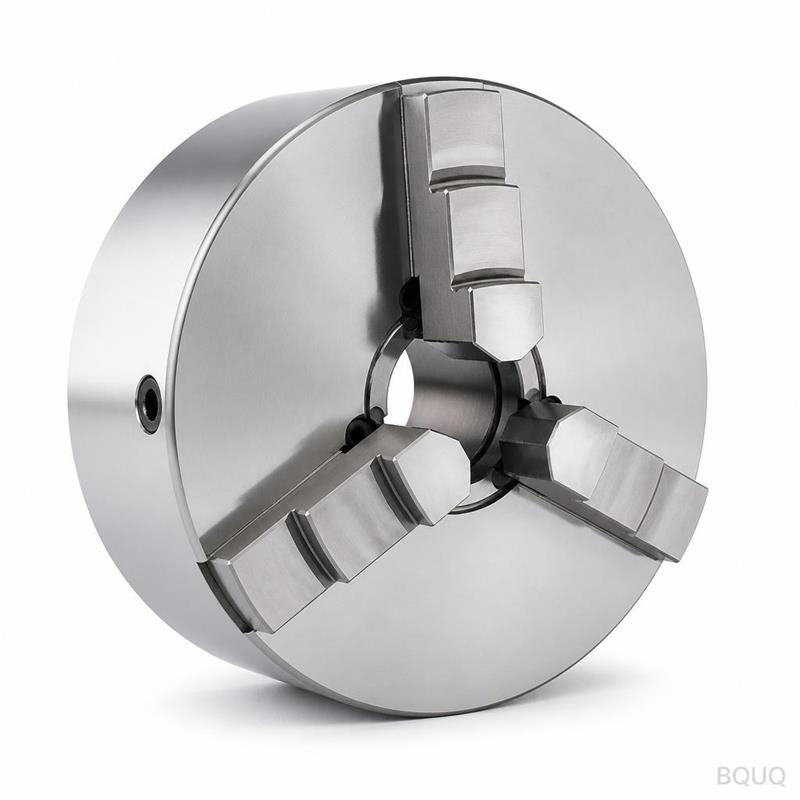
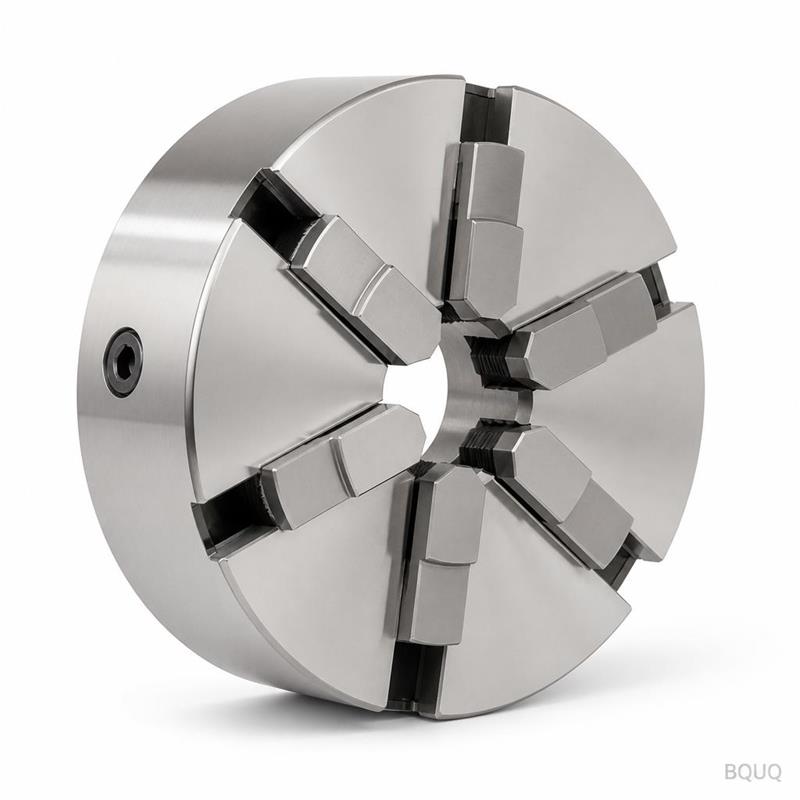
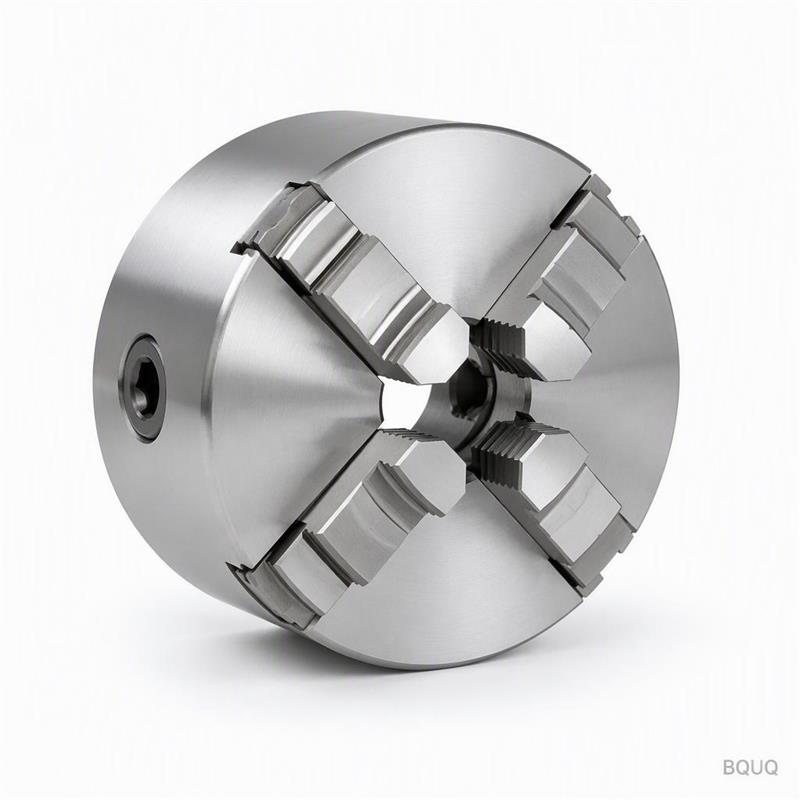
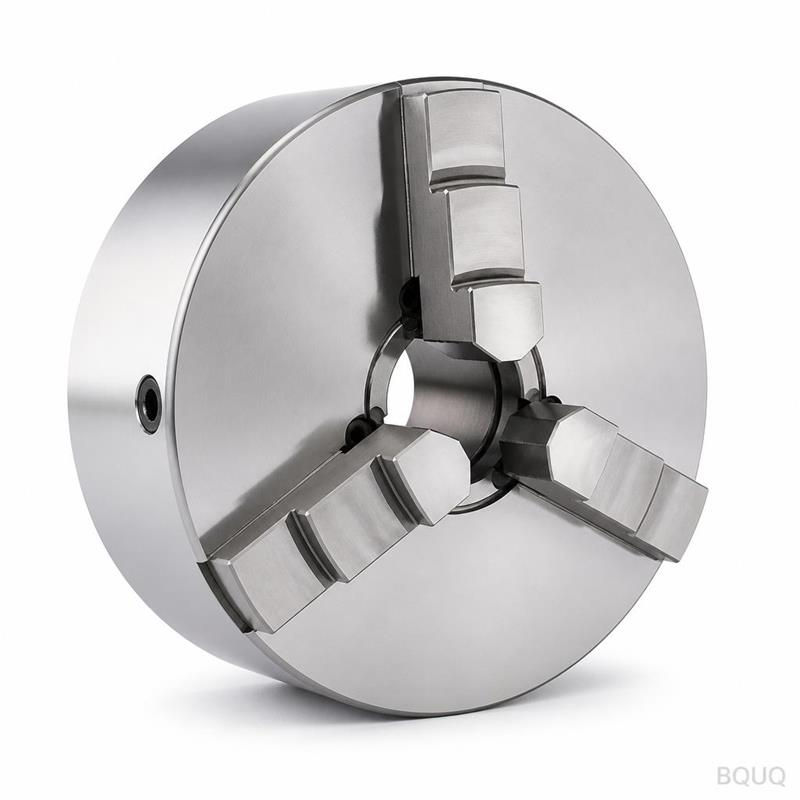
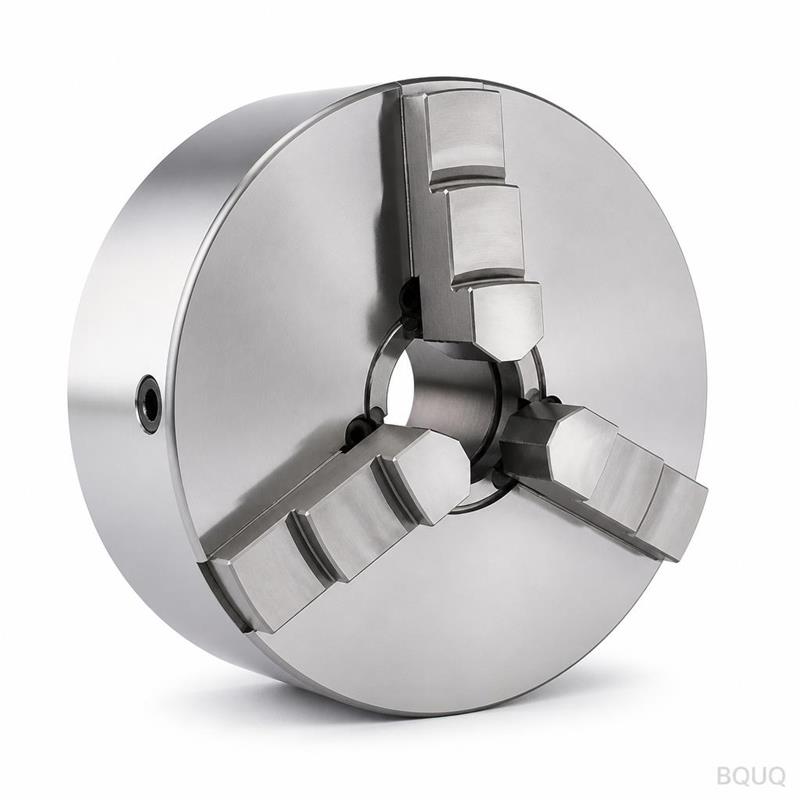
A collet chuck for lathe is a single-stroke stamped component for CNC turning centres, with fins at pitch and a base verified flat before dispatch. Stamping keeps part cost from scaling with complexity, tolerates batch variation better than extrusion, and maintains fin density in a fixed airflow envelope. The finish is applied after forming, so corrosion protection is not cut through at the fin roots like on machined alternatives.
A collet chuck for lathe is a single-stroke stamped component for CNC turning centres, with fins at pitch and a base verified flat before dispatch. Stamping keeps part cost from scaling with complexity, tolerates batch variation better than extrusion, and maintains fin density in a fixed airflow envelope. The finish is applied after forming, so corrosion protection is not cut through at the fin roots like on machined alternatives.
Engineered for CNC turning centre, the collet chuck for lathe in reaches thermal resistance. Fins measure at pitch; the base is verified flat to before dispatch.
Design Approach and Process
A single stroke forms the whole collet chuck for lathe, so part cost stops scaling with complexity. Tooling runs , and the cycle feeds a line.
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at rather than in the field.
Pressing keeps the collet chuck for lathe light, from depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
The finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is , supplied with . For applications where CNC turning centre exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with on every first article. Deviations beyond trigger a full-lot sort.
Final containment is . Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
In CNC turning centre, the rating determines how much airflow the enclosure still needs. At CNC turning centre junction temperatures, fins at pitch keep the delta-T inside the sensor budget.
CNC turning centre programs are the reason this geometry exists. Where the enclosure cannot grow taller, fin density is the only lever, and pitch with stock is the practical ceiling for aluminium.
For CNC turning centre builds, the mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Designers working on CNC turning centre ask for flatness before they ask for thermal data, because CNC turning centre assembly is automated and a non-flat base stops the line.
Specifications
Parameter
Value / Range
MOQ (prototype)
100 sets
MOQ (production)
1000 sets
Lead time (prototype)
7 working days
Lead time (production)
20 working days
FAQ: Your Questions Before Ordering
Can you customise the collet chuck for lathe for our application?
Yes. Send a drawing or a sample and we return a DFM note within 3 working days. Most CNC turning centre customisations change , or the hole pattern, and all three are tooling changes on the existing press rather than a new machine.
What is the lead time for the collet chuck for lathe?
Prototype is 7 working days from drawing approval; production is 20 working days after the first article is signed off. Tooling for a new part takes . We quote , and sea freight to Europe runs about 25 to 30 days after booking.
What is the flatness on the mounting face?
measured on . This is the number that matters for CNC turning centre, because the thermal pad needs even contact. If your assembly needs better, say so and we can add a skim operation.
Can you help with thermal simulation before sampling?
Yes. Send your enclosure airflow, inlet temperature and the heat load to be dissipated, and we will run a steady-state model and return a suggested and combination. That usually saves one tooling iteration.
What is the difference between your collet chuck for lathe and a skived fin collet chuck for lathe?
Skived fins are milled, so you get thin, tall fins and higher density in a given height, but the cost scales directly with fin area. Stamping gives the same result in one stroke at a much lower unit cost below . For CNC turning centre in a fixed-height enclosure, stamped is normally the right answer.
How We Manufacture and Ship
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so flatness is verified before the part is packed.
Quality staff sit beside the press, not in a separate room. Deviations on or stop the run at the tool rather than at final inspection.
We quote and hold 100 sets for sampling. Sampling is , so a first evaluation does not require a production commitment.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
Standard material supplied with passivated route for CNC turning centre exposure
Tolerance
Fin pitch measurable shift; base flat verified before dispatch
Lead time
Tooling runs and cycle feeds a line; not specified in article
MOQ
Not specified in article
Capacity
Single stroke forms whole part; line-fed cycle
Selection / comparison
Option
Best for
Trade-off
Stamped construction
Low fin gauge and high fin density per cubic millimetre
Die wear shows as measurable fin pitch shift, caught at inspection
Machined profile
Applications needing machined alternatives
Corrosion protection can be cut through at fin roots
Extruded profile
Same envelope as stamped
Less tolerant to batch variation; fin pitch shift appears in field
Passivated route
CNC turning centre exposure concerns
Recommended where conductivity matters, per article
Process / inspection
Stage
Control
Record
Forming
Single stroke forms whole collet chuck for lathe
Tooling runs and cycle feeds a line
Fin geometry
Fins measure at pitch
Fin pitch inspection catches die wear shift
Base
Base verified flat before dispatch
Flatness verification before dispatch
Finish
Finish applied after forming
Corrosion protection not cut at fin roots
Shipment
Inspection before every shipment
Per article section: Inspection Before Every Shipment
Frequently Asked Questions
What is a collet chuck for lathe used for?
It is engineered for CNC turning centres and reaches thermal resistance. The stamped design uses fins at pitch and a base verified flat before dispatch. It suits airflow path lengths fixed by the enclosure, where fin density matters more than machined or extruded profiles of the same envelope.
How is the collet chuck for lathe manufactured?
A single stroke forms the whole part, so part cost stops scaling with complexity. Tooling runs and the cycle feeds a line. Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than machined or extruded profiles of the same envelope.
Why choose stamped construction over extrusion for this part?
Stamped construction tolerates batch variation better than extrusion. Die wear shows up first as a measurable shift in fin pitch, which inspection catches at the line rather than in the field. Pressing also keeps the part light without sacrificing fin density in a fixed airflow envelope.
What material and surface finish are standard?
The standard material is supplied with a finish applied after forming, so corrosion protection does not get cut through at the fin roots like on machined alternatives. For applications where CNC turning centre exposure is a concern, the passivated route is recommended where conductivity matters.
How is fin pitch and base flatness controlled before shipment?
Fins measure at pitch, and the base is verified flat before dispatch. Inspection catches die wear as a measurable shift in fin pitch at the line rather than in the field. Every shipment passes inspection before it leaves, per the inspection section.
Does the finish affect corrosion protection at the fin roots?
No. The finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives. This matters where CNC turning centre exposure is a concern and the passivated route is recommended for conductivity.
What are the tolerance and inspection requirements before dispatch?
Fins measure at pitch and the base is verified flat before dispatch. Die wear shows first as a measurable shift in fin pitch, which inspection catches at the line rather than in the field. Inspection before every shipment is standard for this part.
Aluminium or copper alloy (standard for stamped heatsink components)
Tolerance
Fin pitch and base flatness verified; typical ±0.1 mm on pitch, flatness 0.05 mm
Lead time
Standard production lead time 2–4 weeks after tooling approval
MOQ
Typically 1,000–5,000 pieces depending on size and material
Capacity
High-volume stamping line, up to 100,000 pieces per month
Selection / comparison
Option
Best for
Trade-off
Stamped collet chuck
High-volume production with complex fin geometry
Tooling cost upfront; less design flexibility after die is cut
Machined collet chuck
Low-volume or prototype runs
Higher per-part cost; corrosion protection cut at fin roots
Extruded collet chuck
Simple profiles with uniform cross-section
Limited fin density; batch variation from die wear affects pitch
Frequently Asked Questions
What is a collet chuck for lathe?
A collet chuck for lathe is a single-stroke stamped component for CNC turning centres, with fins at pitch and a base verified flat before dispatch. It is designed for thermal resistance and maintains fin density in a fixed airflow envelope. The finish is applied after forming, so corrosion protection is not cut through at the fin roots.
How does stamping compare to extrusion for collet chuck production?
Stamping tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at the press rather than in the field. Stamping also keeps part cost from scaling with complexity and maintains fin density in a fixed airflow envelope.
What tolerances can you specify for a stamped collet chuck?
You can specify fin pitch and base flatness. Typical tolerances are ±0.1 mm on fin pitch and 0.05 mm flatness on the base. The base is verified flat before dispatch, and inspection records are available. Fin gauge is measured at pitch to ensure consistency.
What is the lead time for a custom collet chuck order?
Standard lead time is 2–4 weeks after tooling approval, depending on order quantity and material. For high-volume orders, capacity is up to 100,000 pieces per month. Rush options may be available; contact us for specific scheduling.
What is the minimum order quantity (MOQ) for collet chucks?
MOQ typically ranges from 1,000 to 5,000 pieces depending on size and material. For smaller quantities, machining may be more cost-effective. Stamping becomes economical at higher volumes because tooling cost is amortized over the production run.
How is corrosion protection applied to stamped collet chucks?
The finish is applied after forming, so corrosion protection is not cut through at the fin roots like on machined alternatives. This ensures full coverage. Common finishes include anodizing or plating, selected based on the application environment and material.
What inspection is performed before shipment?
Every shipment undergoes inspection: fin pitch is measured, base flatness is verified, and a visual check for defects is performed. Records are kept for each batch. The base is verified flat before dispatch, and a certificate of conformance is provided.