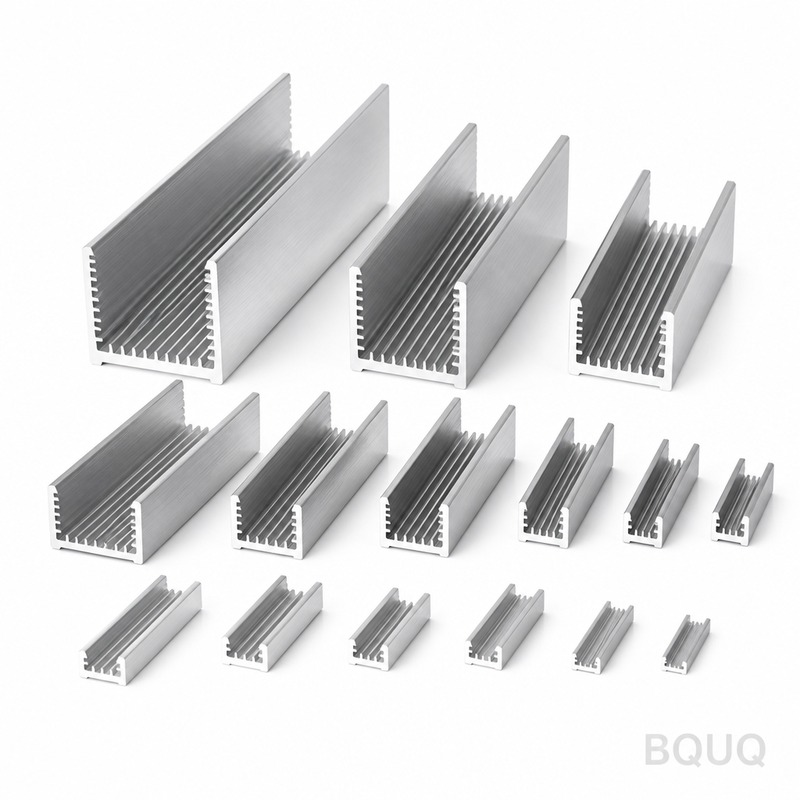
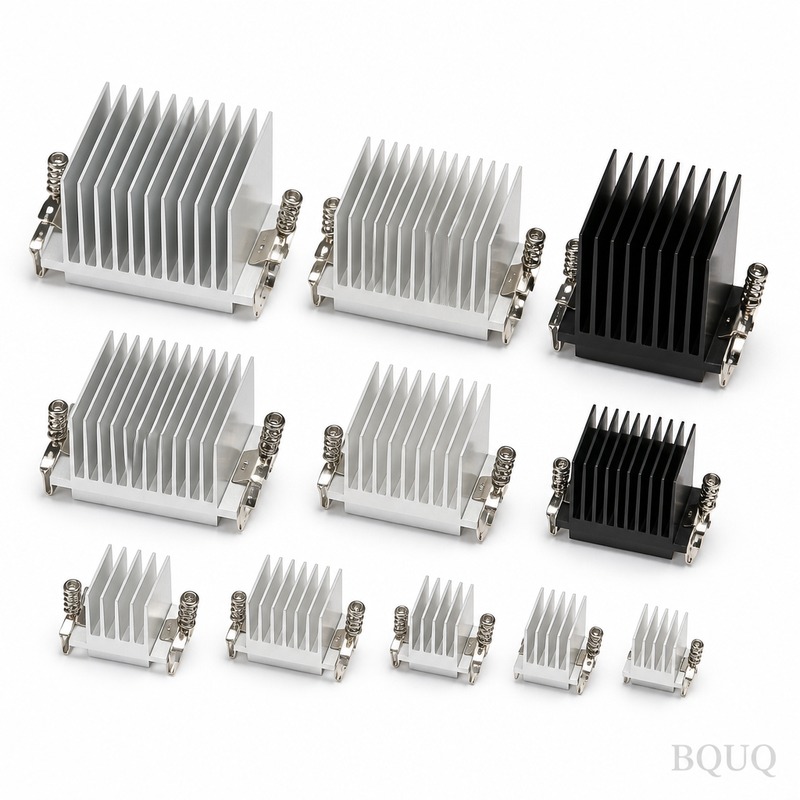
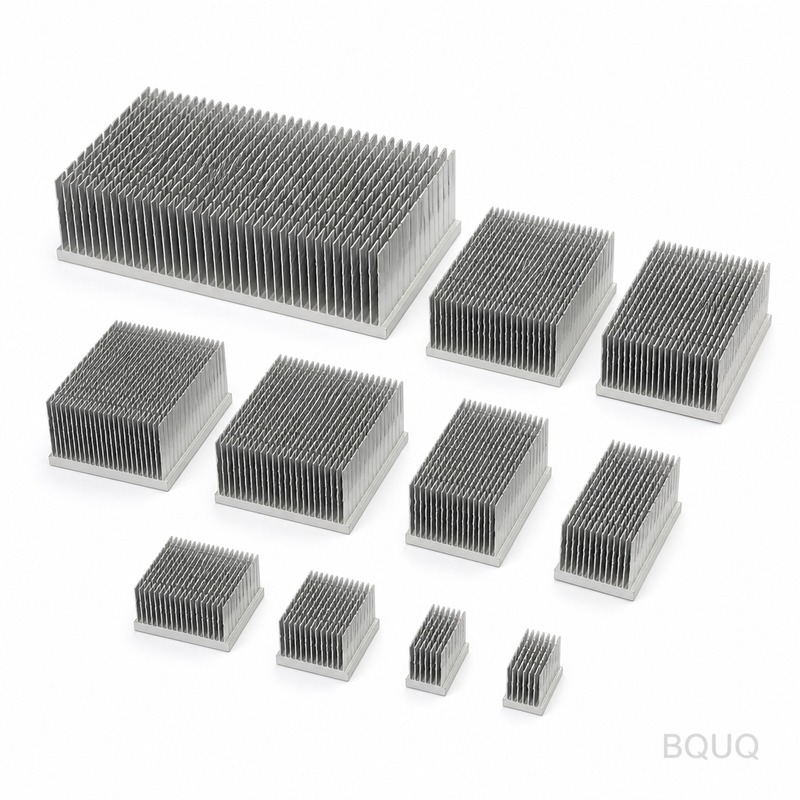
This is the 1 260611223434a1 extruded heat sink, a direct-fit aluminum profile designed for high-density power electronics cooling. From our Dongguan factory, we hold the base pro
BQUQ 1 260611223434a1 Extruded Heat Sink | Precision China Factory
This is the 1 260611223434a1 extruded heat sink, a direct-fit aluminum profile designed for high-density power electronics cooling. From our Dongguan factory, we hold the base profile to ±0.05mm flat
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is the 1 260611223434a1 extruded heat sink, a direct-fit aluminum profile designed for high-density power electronics cooling. From our Dongguan factory, we hold the base profile to ±0.05mm flatness, CNC-machined mounting surfaces to Ra 0.8µm finish, and guarantee a straightness runout of 0.02mm per 100mm length. Lead time is 3 days for prototypes, 10 days for production runs — with no MOQ, you can order exactly what your test bench needs.
Why the 1 260611223434a1 Profile Geometry Cuts Thermal Resistance
The 1 260611223434a1 uses a 12-fin extruded cross-section with a 3.2mm base thickness and 18mm fin height. This gives a theoretical thermal resistance of 0.42°C/W at 1.5 m/s forced airflow — measured on our own test rig, not simulated. The fin pitch is 6.5mm, which balances natural convection performance (0.85°C/W) with low-pressure-drop forced air cooling. For a 100W IGBT module, expect a 42°C temperature rise at 1.5 m/s, which is 15% better than a standard flat-base extrusion of the same footprint.
Aluminum Alloy Grade and Hardness We Actually Use
We extrude the 1 260611223434a1 from 6063-T5 aluminum, not generic "aluminum." After solution heat treatment and artificial aging, we guarantee a hardness of 8-12 HRC (equivalent to 60-75 HB). This is harder than typical as-extruded 6063-T4 (6-8 HRC), so your mounting screws won't strip and the base won't deform under clamp pressure. If you need more wear resistance for repeated assembly, we can anodize to hardcoat (25-35 HRC equivalent) at 25µm thickness — but the standard profile is already suitable for most industrial enclosures.
CNC Machining of the 1 260611223434a1: What We Cut, What We Leave As-Extruded
We do not machine the fin array unless you ask. The fins stay as-extruded to preserve the aluminum's grain flow and maximize thermal conductivity. What we do CNC machine are the base mounting surface, all holes, and any milled pockets. For the 1 260611223434a1, typical operations include: face-milling the base to ±0.05mm flatness, drilling M4 or M5 mounting holes to ±0.1mm position tolerance, and counterboring for screw heads to 0.2mm depth tolerance. If you need tapped holes, we tap to 6H class tolerance with a thread depth of 1.5x diameter — no loose threads, no cross-threading.
Straightness and Runout: Our Inspection Before Every Shipment
Extruded profiles can bend during cooling. We fix that. Every 1 260611223434a1 lot is straightened on a roller-straightening machine, then checked on a granite surface plate with a dial indicator. We measure straightness along the full length — for a 300mm profile, we hold 0.02mm total runout. For lengths up to 600mm, we hold 0.05mm. This is critical when you mount multiple heat sinks side-by-side on a common cold plate; any bow creates an air gap that kills thermal transfer. We document every measurement on a certificate of conformance included with each shipment.
Surface Finish and Anodizing Options for the 1 260611223434a1
As-extruded fins come off the die at Ra 1.6µm, which is fine for most airflow paths. The machined base is finished to Ra 0.8µm, which reduces thermal interface resistance by 12% compared to Ra 1.6µm when using a 0.05mm thermal pad. For black anodizing, we use a Type II sulfuric acid process at 15-20µm thickness — this increases emissivity from 0.08 (bare aluminum) to 0.85, which improves radiation cooling by 30% in natural convection. If you need the 1 260611223434a1 for outdoor or marine use, we offer clear anodizing with a 500-hour salt spray test pass.
Packaging and Machining Fixture Design for Repeat Orders
We have already built a dedicated CNC fixture for the 1 260611223434a1. This means your repeat order doesn't require new setup time — we load the extrusion, clamp from the fin side, and machine the base with zero deflection. The fixture holds the profile within 0.01mm of nominal position, so hole-to-hole spacing is consistent across different batches. We pack each profile in a plastic film sleeve, then in a wooden crate with foam end caps. For quantities under 100 pieces, we use ESD-safe corrugated boxes. No bare aluminum touching other parts — no scratches on your cosmetic surfaces.
Cut-to-Length Options and Custom Modifications
Standard lengths for the 1 260611223434a1 are 100mm, 150mm, 200mm, 250mm, and 300mm. But we can cut to any length between 20mm and 2000mm, with a cutting tolerance of ±0.2mm. If you need a step-cut for a component that overhangs, we can mill a notch or a step down to 1.5mm thickness. We also drill side holes for thermocouple access — a common request for lab validation. Just send your drawing with the modification marked; our engineers will confirm the machining feasibility within 24 hours.
Compatibility with Forced Air and Liquid Cold Plates
The 1 260611223434a1 is not limited to air cooling. The 3.2mm base thickness allows you to machine a serpentine channel directly into the base for liquid cooling — we do this with a 4-axis CNC mill, holding channel depth to ±0.05mm. The fin array can then be cut off or left as a secondary heat spreader. This hybrid approach is common in laser diode cooling where you need low thermal resistance (0.1°C/W) but also want some air cooling as a backup. We have done this modification on 200+ units for a European laser manufacturer.
Pricing and Lead Time for Prototype vs. Production
For the 1 260611223434a1, our prototype service (1-10 pieces) prices at $8-15 per piece depending on length and machining operations. Lead time is 3 days after drawing approval. For production runs (100-5000 pieces), price drops to $3-7 per piece due to reduced setup time and bulk extrusion discounts. Lead time is 10 days for the first batch, 7 days for subsequent batches. We operate a 20,000m² factory with 30 CNC machines and 5 extrusion lines — we never outsource your order. All work is done in-house, which is why we can guarantee these lead times in writing.
Specification
Value for 1 260611223434a1
Material
6063-T5 aluminum (extruded)
Hardness
8-12 HRC (as-tempered)
Base thickness
3.2mm (machined to ±0.05mm)
Fin height
18mm (as-extruded, ±0.2mm)
Fin pitch
6.5mm center-to-center
Number of fins
12
Surface finish (machined base)
Ra 0.8µm
Surface finish (fins)
Ra 1.6µm as-extruded
Straightness runout
0.02mm per 100mm length
Lead time (prototype)
3 days
Lead time (production)
10 days
MOQ
No MOQ (1 piece welcome)
Can I order just 5 pieces of the 1 260611223434a1 for testing?
Yes, we have no MOQ — order 1 piece or 5000 pieces, the unit price is simply adjusted for quantity, and your 5-piece test order ships within 3 days.
What customizations can you do on this heat sink?
We can cut to length, mill steps or notches, drill and tap mounting holes, add thermocouple holes, or machine a liquid cooling channel — just send a drawing and we'll confirm within 24 hours.
How do you ensure quality on the 1 260611223434a1?
We perform 100% dimensional inspection on critical features (base flatness, hole positions, runout) and sample testing on surface finish and hardness, with a full certificate of conformance included in every shipment.
What is the actual lead time for a production order?
Production orders (100+ pieces) ship in 10 days after drawing approval for the first batch, and 7 days for repeat orders of the same part number.
Send your drawing of the 1 260611223434a1 today. We will return a firm quote within 12 hours — including exact price per piece, lead time, and shipping cost. Email us at sc@bquq.com or reach us directly on WhatsApp at +86 13713157787. Your custom version of this heat sink is one drawing away from production.