Cnc Machined Power Tool Parts Machinery | BQUQ Precision Manufacturing
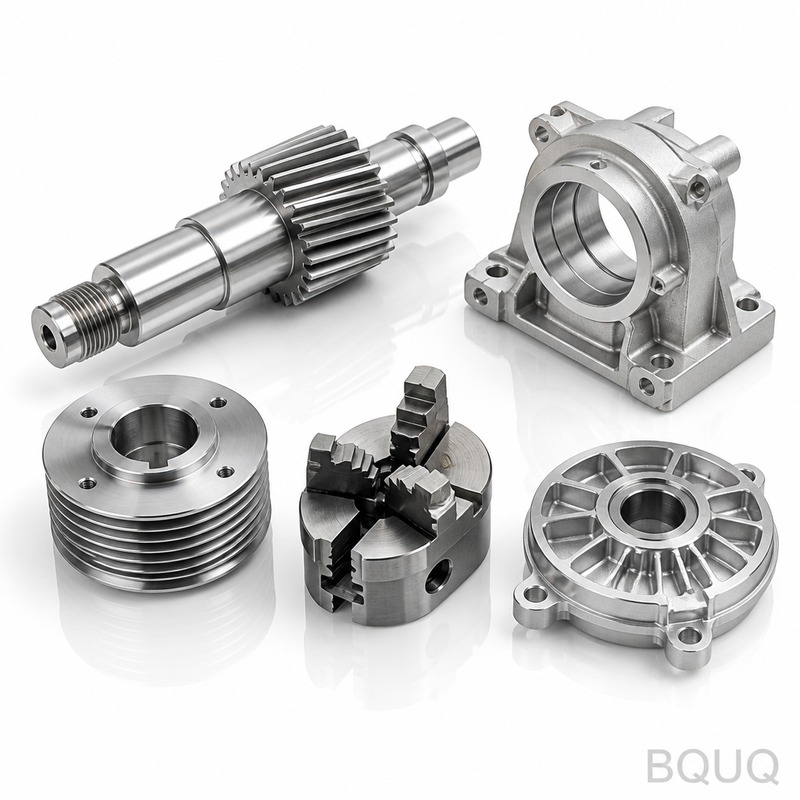
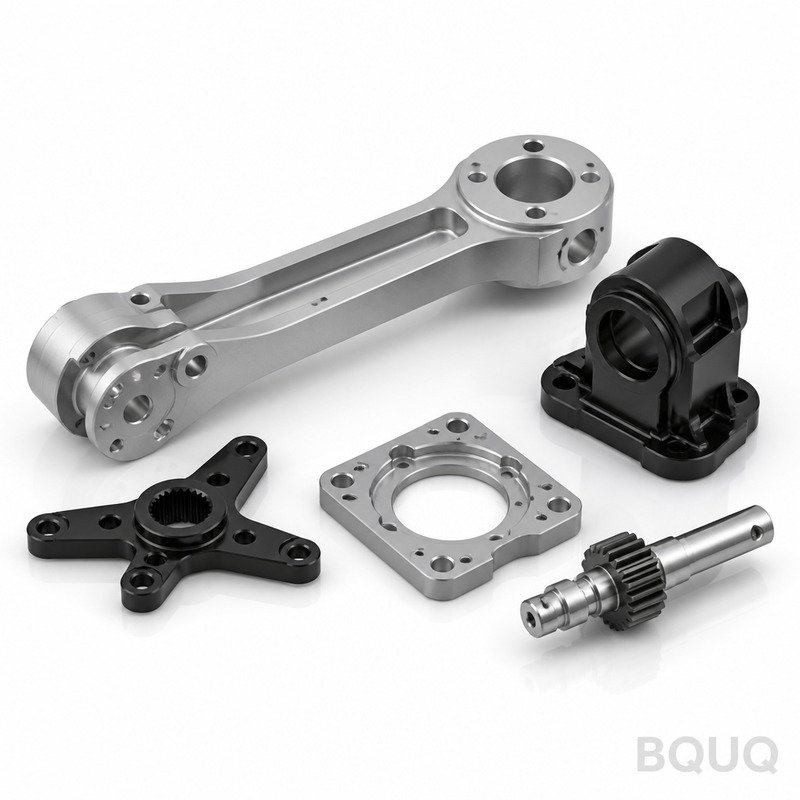
This product line covers CNC machined components for power tools—gear housings, armature shafts, bearing seats, and chuck bodies—produced on 5-axis Mazak and Fanuc machines in our Dongguan factory. Yo
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This product line covers CNC machined components for power tools—gear housings, armature shafts, bearing seats, and chuck bodies—produced on 5-axis Mazak and Fanuc machines in our Dongguan factory. You get ±0.005 mm positioning tolerance, 0.008 mm TIR runout on critical diameters, and 48 HRC surface hardness after heat treatment, with a standard 15-day lead time for prototypes. If your drill, grinder, or impact wrench needs a part that survives 10,000+ cycles without wear, this is the spec sheet to read.
How We Hold 0.008 mm Runout on Armature Shafts
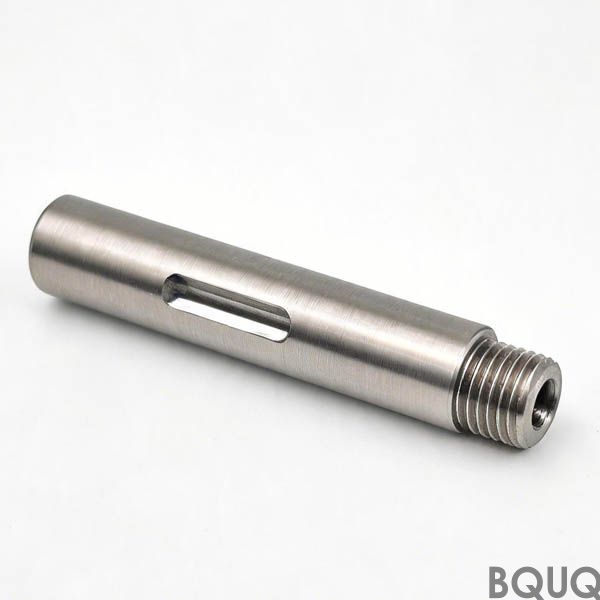
Runout kills bearing life and causes vibration in rotary tools. We grind armature shafts between centers after CNC turning, using a cylindrical grinder with a 0.5 µm resolution. Then we check every shaft on a Talyrond roundness tester. The process: rough turn, heat treat, grind OD to 0.008 mm TIR, then finish hone the bearing journal to Ra 0.4 µm. For splined shafts, we use form grinding to keep tooth spacing within ±0.01 mm—this prevents gear chatter at 20,000 RPM.
Materials and Heat Treatment for Impact Loads
Power tool parts see shock loads, not just steady torque. We machine from 8620 alloy steel for carburized gears (58-62 HRC case depth 0.8-1.2 mm), 4140 for chuck bodies (28-32 HRC core, induction hardened to 52 HRC on the gripping face), and 6061-T6 aluminum for lightweight housings. For high-temperature environments like circular saw arbors, we use 440C stainless hardened to 56 HRC. Every batch gets a hardness test report—we do not skip this even for one-off samples.
If you need a specific grade, we source it domestically within 3 days. But stick to these three base materials unless you have a fatigue test requirement. Our heat treater is ISO 9001 certified and runs vacuum furnaces for minimal distortion—critical for thin-walled sleeves.
Inspection Before Every Shipment: CMM and Surface Profilometer
We do not trust the machine alone. Each Cnc Machined Power Tool Parts Machinery order goes through a 3-step check: (1) in-process probing every 10 parts for critical bore diameters, (2) final CMM inspection on a Zeiss machine for GD&T—true position, parallelism, and concentricity, (3) surface finish verification with a Mitutoyo profilometer on sealing faces. For runout-critical parts, we add a 100% functional test: spinning the part at rated speed with a dial indicator. You get a digital PDF report with all measured values, not just a "pass" stamp.
Spec Item
Value / Range
Materials
8620, 4140, 440C, 6061-T6, 7075-T6, brass C360
Diameter range
3 mm to 300 mm
Length range
2 mm to 600 mm
Hardness (through)
28-32 HRC (4140 core), 56-60 HRC (440C)
Case hardness
58-62 HRC on carburized 8620
Machining tolerance
±0.005 mm on bores, ±0.01 mm on external threads
Surface finish (Ra)
0.4 µm ground, 0.8 µm turned, 1.6 µm milled
Runout (TIR)
0.008 mm on ground journals, 0.02 mm on turned surfaces
Lead time
15 days for prototypes, 25 days for production
MOQ
No MOQ — single piece accepted
Threads and Splines: Cutting Tool Selection That Prevents Tapping Breakage
Power tool housings often use M4-M8 threads in aluminum and hardened steel. We use spiral-flute taps for blind holes and roll taps for through holes in aluminum to avoid chip packing. For spline shafts, we use hobbing cutters with TiAlN coating—this extends tool life to 800 parts per regrind. If you are designing a new spline profile, check our CNC cutting tool selection guide—it covers the exact feeds and speeds for these geometries.
Surface Finish Options: From Machined to Black Oxide
Bare machined surfaces are standard, with Ra 1.6 µm on non-critical faces. But for corrosion resistance on steel parts, we offer black oxide (MIL-DTL-13924) which adds 0.5 µm thickness—no dimension change. For aluminum housings, we do Type II anodizing (18-22 µm) in black or clear, which increases surface hardness to 60 HRC equivalent. If you need a low-friction surface for sliding parts, we apply a PTFE impregnated anodize that cuts friction coefficient to 0.1. All finishes are RoHS compliant.
Batching and Lead Time: No MOQ, Fixed 15-Day Prototype
We run a dedicated line for power tool parts with preset tooling for common diameters. This is why we can offer no MOQ—a single piece costs the same per-part as a 500-piece run, only the setup fee is higher. Prototype lead time is 15 days from drawing approval, production runs ship in 25 days. If you need 48-hour rush, we charge a 30% expedite fee and run a night shift. For repeat orders, we keep your tooling and CAM files for 2 years, so reordering takes just 10 days.
Before you send a drawing, read our CNC machining tolerances guide—it explains which features should be ±0.005 mm and which can be ±0.05 mm to save cost. Over-tolerancing is the #1 reason for quote delays.
How We Handle Long-Shaft Warpage After Grinding
Shafts over 200 mm long can bow during heat treatment. We straighten them with a hydraulic press to within 0.02 mm before grinding, then stress-relieve at 150°C for 2 hours. After grinding, we re-check straightness on a granite table with a height gauge. For shafts over 400 mm, we use centerless grinding to maintain 0.01 mm roundness. This is the difference between a part that hums at 15,000 RPM and one that vibrates the whole tool.
What is the minimum order quantity?
We have no MOQ—order one prototype or 10,000 units, the unit price only changes by setup amortization.
Can you machine parts from our 3D model without a 2D drawing?
Yes, we accept STEP or IGES files, but we will generate a GD&T drawing for your approval, especially for runout and concentricity callouts.
How do you guarantee the 0.008 mm runout spec?
Every shaft is measured on a Talyrond tester after grinding, and we include the raw roundness trace in the inspection report.
What is your actual lead time for a 100-piece production order?
25 days from drawing approval, but we can compress to 18 days if you accept a partial shipment of the first 50 parts.
Get a firm quote within 12 hours. Send your drawing or 3D file to sc@bquq.com or WhatsApp +86 13713157787. We will reply with unit price, tooling cost (if any), and a confirmed delivery date—no guessing. BQUQ, precision manufacturing made in China since 2005.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.