BQUQ CNC Machined Watch Bezels Crowns | Precision Made in China
What You Get When You Order Bezels and Crowns from BQUQ We machine watch bezels and crowns that hold ±0.005 mm on critical diameters and 0.01 mm total runout on the thread-to-seat interface. Our 20-ye
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What You Get When You Order Bezels and Crowns from BQUQ
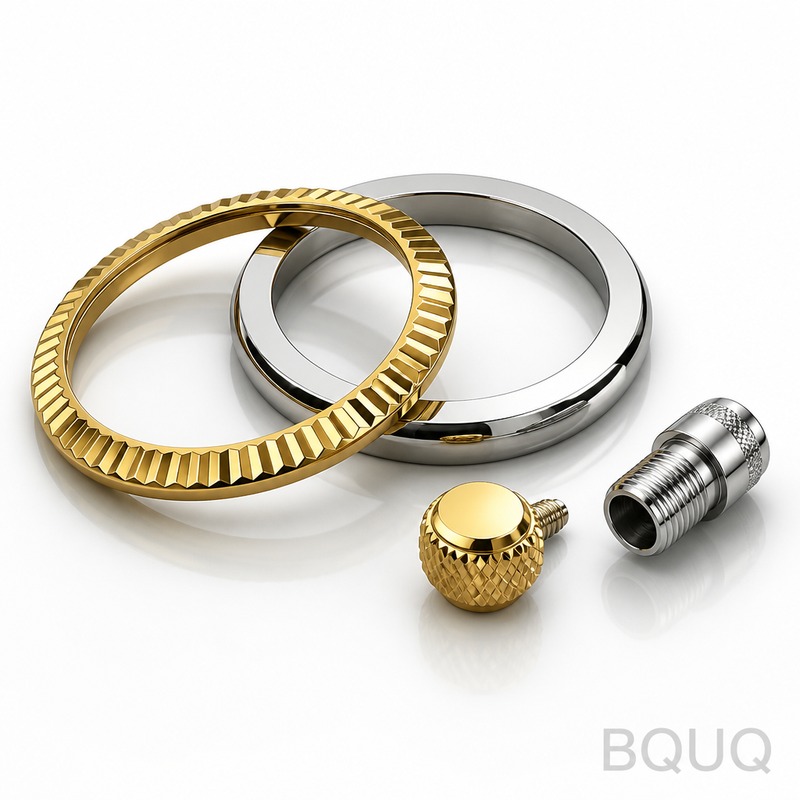
We machine watch bezels and crowns that hold ±0.005 mm on critical diameters and 0.01 mm total runout on the thread-to-seat interface. Our 20-year factory in Dongguan delivers these parts in 10 days for prototypes and 18 days for production runs, with hardness up to 42 HRC on 316L and 48 HRC on 904L. This is precision manufacturing for watches that must survive daily wear, pressure testing, and repeated crown operation without binding.
How We Hold 0.01 mm Runout on a Rotating Bezel Seat
Runout on a bezel seat causes a wobbly rotating ring and uneven gasket compression. We eliminate this by machining the inner bore and the outer seat in the same clamping operation on our Citizen L20 and Star SR-32 Swiss lathes. We use a live tool with a C-axis index that locks the spindle at 0.0001 degrees, then we cut the thread and the bearing race without releasing the part. This single-setup method keeps the geometric relationship tight, and we verify every 10th piece on a Zeiss Contura CMM with a 0.5 µm probe.
Materials and Heat Treatment We Use for Bezel and Crown Parts
We stock 316L stainless steel (1.4404), 904L (1.4539), and Grade 5 Titanium (6Al-4V) for bezels and crowns. For hardened steel crowns, we use 17-4PH in H900 condition, which gives 40-44 HRC with good corrosion resistance. We also handle 6061-T6 aluminum for lightweight bezels and 304 stainless for budget production runs. Heat treatment is done in-house in a vacuum furnace, so we do not lose time or tolerance to an outside vendor. We control case depth on nitrided crowns to 0.05 mm, which prevents surface brittleness on the knurled edges.
Surface Finish and Edge Quality on Visible Watch Parts
Bezels and crowns are visible parts, so we finish them to Ra 0.4 µm on flat surfaces and Ra 0.2 µm on sealing faces. We use a 3-step polishing process: first a 320-grit belt, then a 600-grit abrasive, and finally a cotton wheel with 1 µm diamond paste for a mirror finish. For brushed finishes, we use a satin wheel with a 240-grit aluminum oxide that leaves a uniform 0.5 µm Ra across the entire circumference. We break every sharp edge to 0.1 mm radius, because a sharp edge on a crown catches on shirt cuffs and wears out quickly. Laser engraving for logos or depth marks is done after finishing, so the mark depth is consistent at 0.02 mm.
Threading and Knurling Details That Matter for Crowns
Crowns have small threads (M1.6 to M3.5) that must engage smoothly with the stem. We use a thread whirling attachment on the Swiss lathe, which produces a rolled-like surface finish of Ra 0.4 µm on the thread flanks. This reduces the risk of galling when the crown is screwed onto a steel stem. For knurling, we use a 45° diamond pattern with a 0.3 mm pitch, and we control the knurl depth to 0.15 mm so the gripping surface is tactile but not fragile. We measure the knurl outer diameter with a laser micrometer, because a deformed knurl will not seat properly against the case middle.
Inspection Before Every Shipment of Bezel and Crown Orders
Every batch of bezels and crowns goes through a 3-stage inspection. First, we check dimensions on a Zeiss CMM with a 0.5 µm repeat accuracy, covering all critical diameters, thread pitch diameters, and runout values. Second, we do a visual inspection under a 10x stereo microscope for edge breaks, scratches, or tool marks. Third, we do a functional test on a sample crown: we thread it onto a test stem and cycle it 500 times to ensure smooth engagement. We save the CMM report in PDF format and attach it to your shipment email. You get the data, not just a claim of quality.
We sign an NDA before you send any drawings, and we never share your files with third parties. Our factory is ISO 9001:2015 certified, and we have a separate secure server for customer CAD files. We do not use your design in any other order, and we delete the file from our public server after completion (we keep a backup on an encrypted drive for 1 year in case you need a reorder). If you want, we can watermark the files with your company name. The quote you receive includes a full breakdown of material cost, machining time, and finishing cost, so you know exactly what you are paying for.
Do you have a minimum order quantity for machined bezels and crowns?
No MOQ. We accept a single prototype piece for testing, and you pay only the machining rate plus material cost for that one piece.
Can you match a specific finish or design from a competitor's sample?
Yes. Send us a physical sample or detailed photos, and we reverse-engineer the dimensions and finish to match or improve on it, including custom engraving or logo marks.
How do you ensure quality control for small batches of 50–200 pieces?
We run 100% dimensional inspection on the first article, then check every 5th piece for critical dimensions and every 10th for visual finish, with a full CMM report included with the shipment.
What is the fastest lead time for an urgent crown order?
For a standard 316L crown with a simple knurled finish, we can ship in 7 days if you approve the drawing within 24 hours and use our standard material stock.
Shipping and Packaging for Delicate Watch Parts
We pack bezels and crowns in anti-static foam trays with individual slots for each part, then seal the tray in a vacuum bag with desiccant. For orders over 500 pieces, we use a rigid plastic box with a foam insert that prevents any metal-to-metal contact during shipping. We ship via DHL Express or FedEx International Priority, with a typical transit time of 3–5 days to the USA, EU, or Japan. The package value is declared correctly for customs, but we mark the goods as "precision metal components" to avoid unnecessary delays. We insure every shipment at full value at no extra cost to you.
If you are still deciding on tooling or tolerances for your next run, read our CNC cutting tool selection guide to pick the right inserts for hardened steel, and check our CNC machining tolerances guide to understand how we hold ±0.005 mm on your specific features. Both guides are written by our shop floor engineers, not by marketing staff.
Send your drawing (STEP, IGES, or PDF) to sc@bquq.com, or message us on WhatsApp at +86 13713157787. We reply with a firm quote within 12 hours, including unit price, tooling cost (if any), and a confirmed lead time. Your parts are machined in our Dongguan factory, and we ship worldwide. No MOQ, no hidden fees, and the CMM report is free with every order.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.