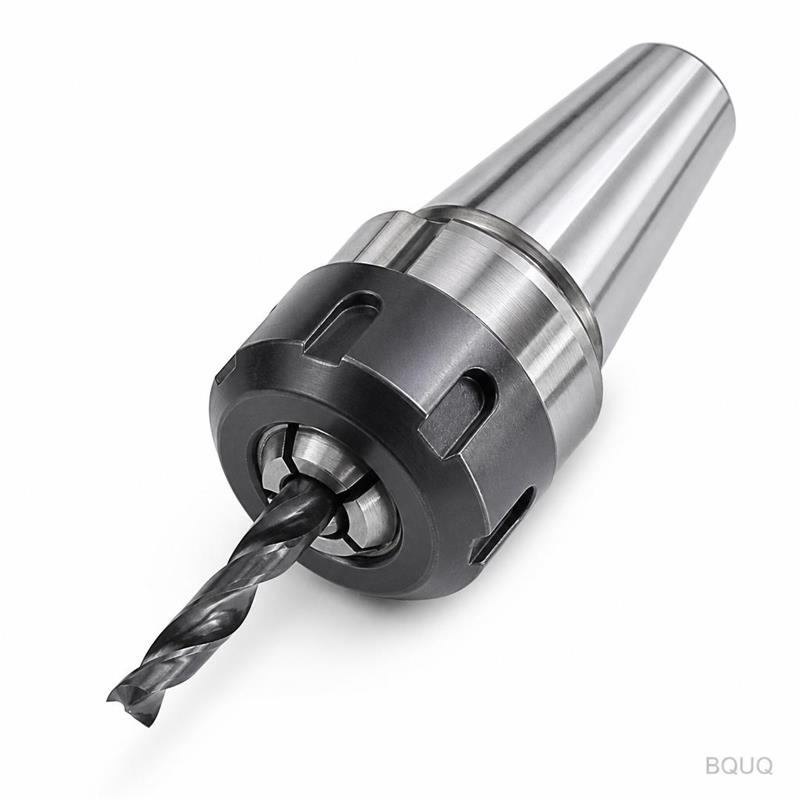
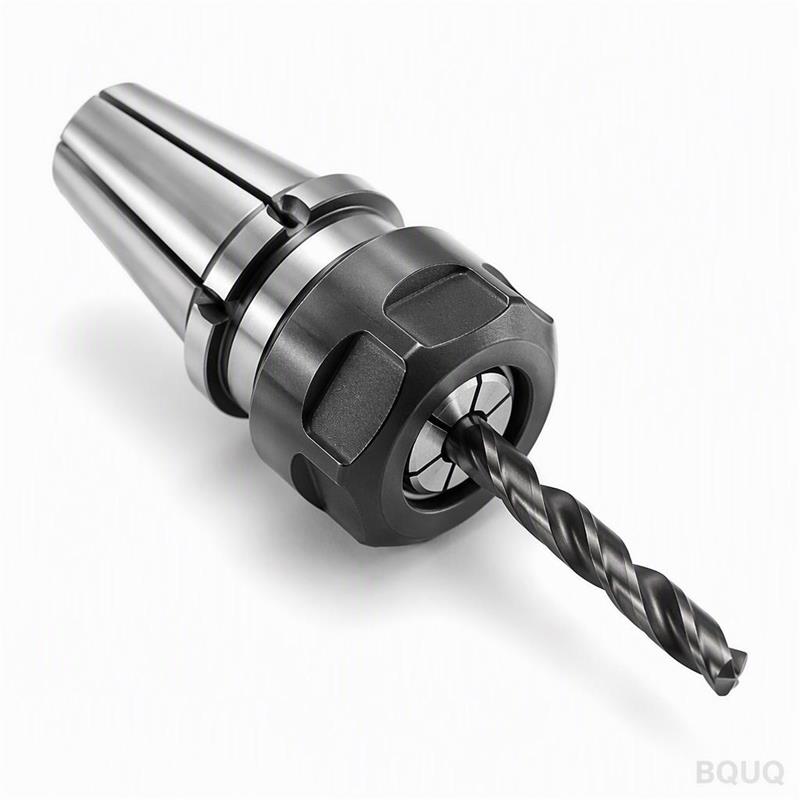
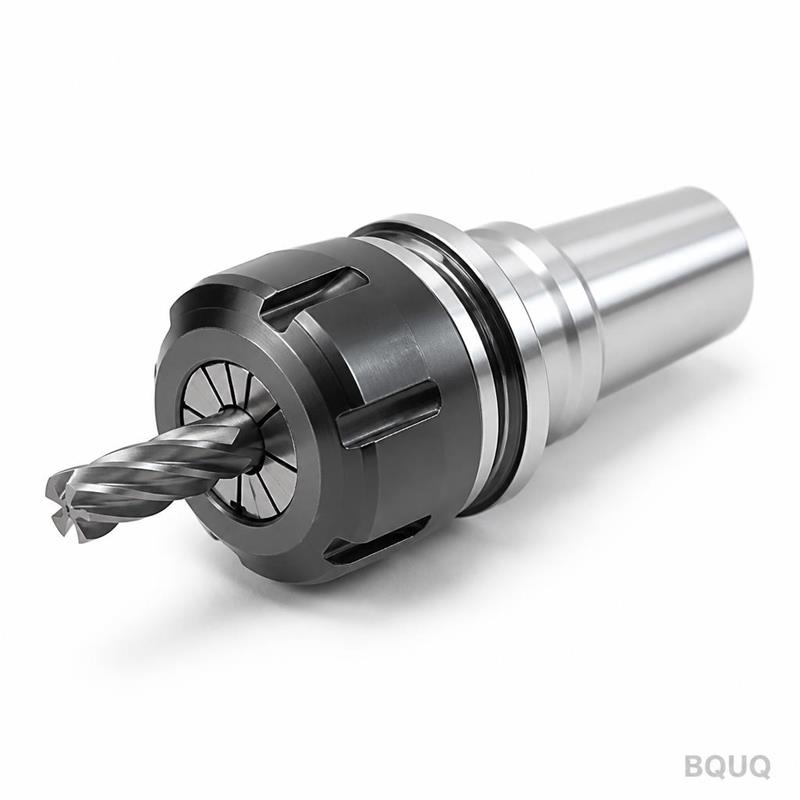
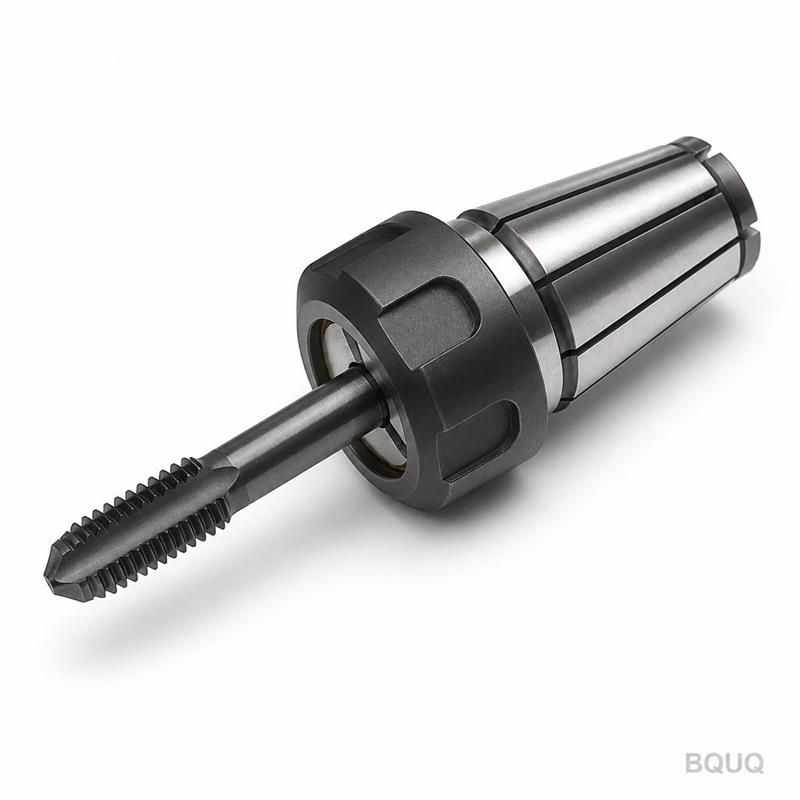
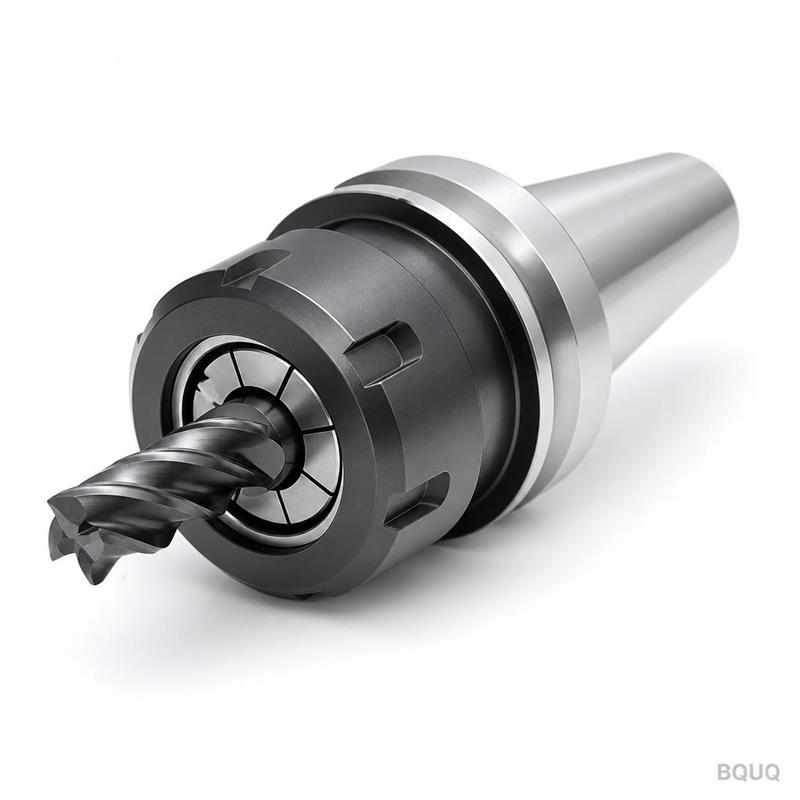
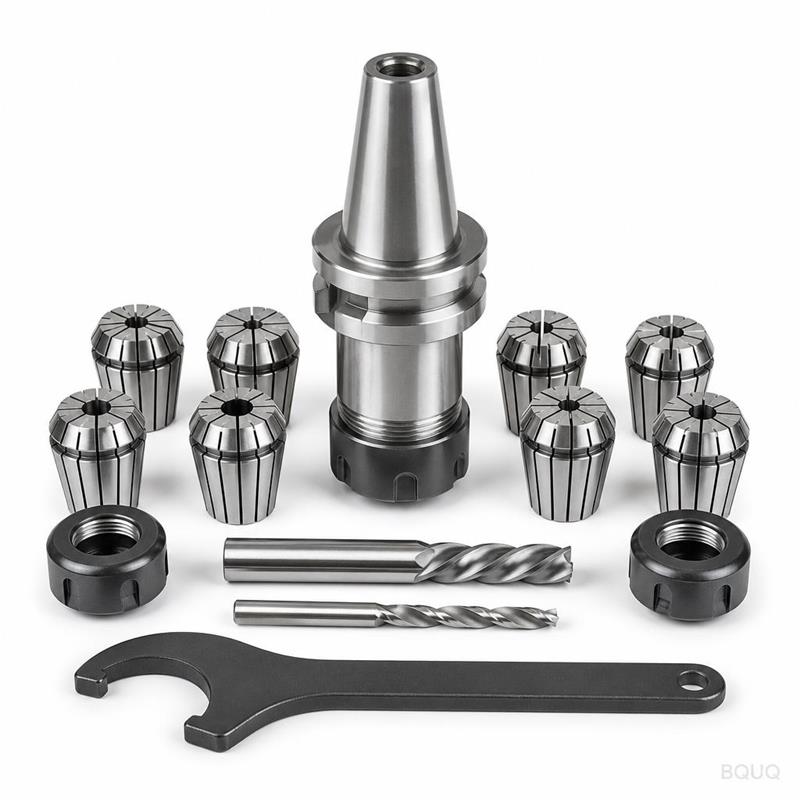
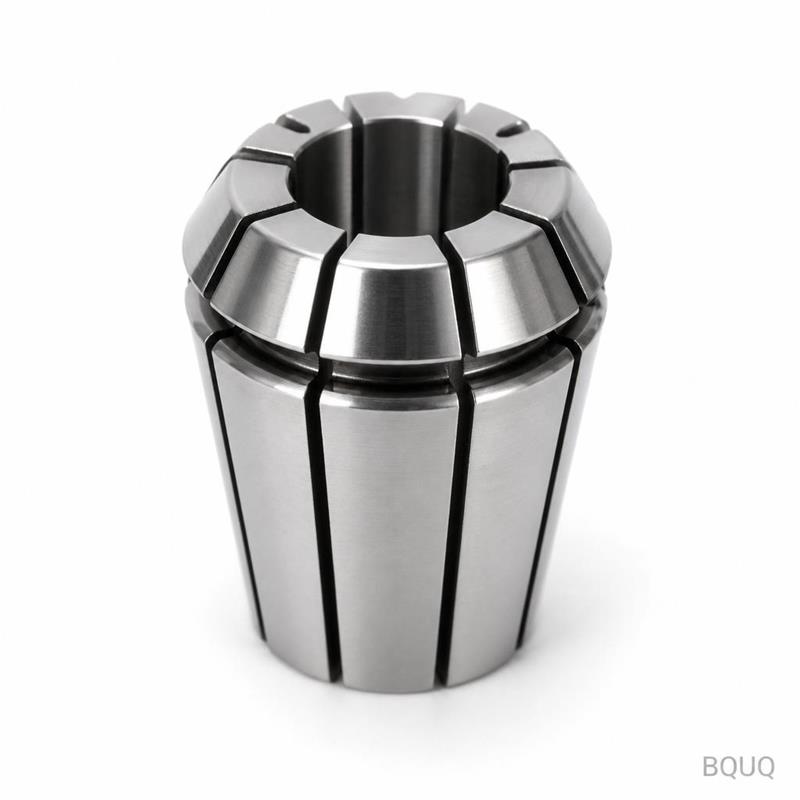
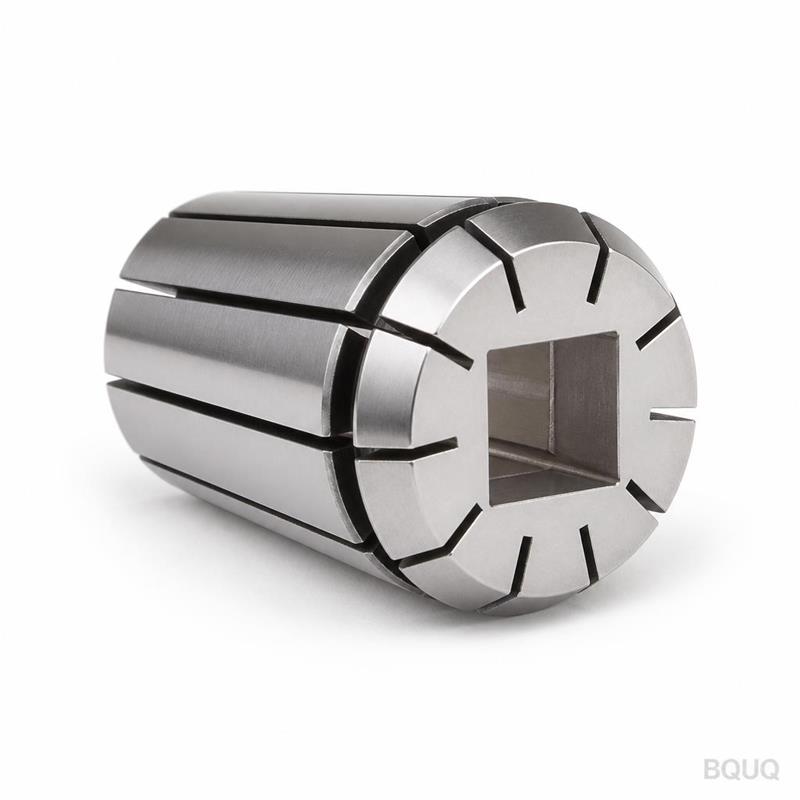
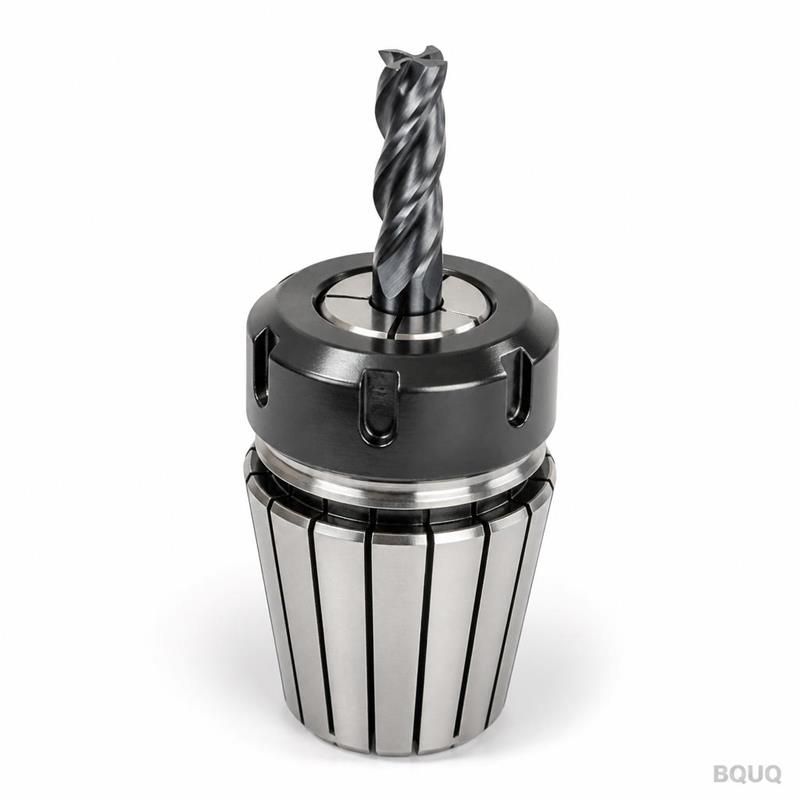
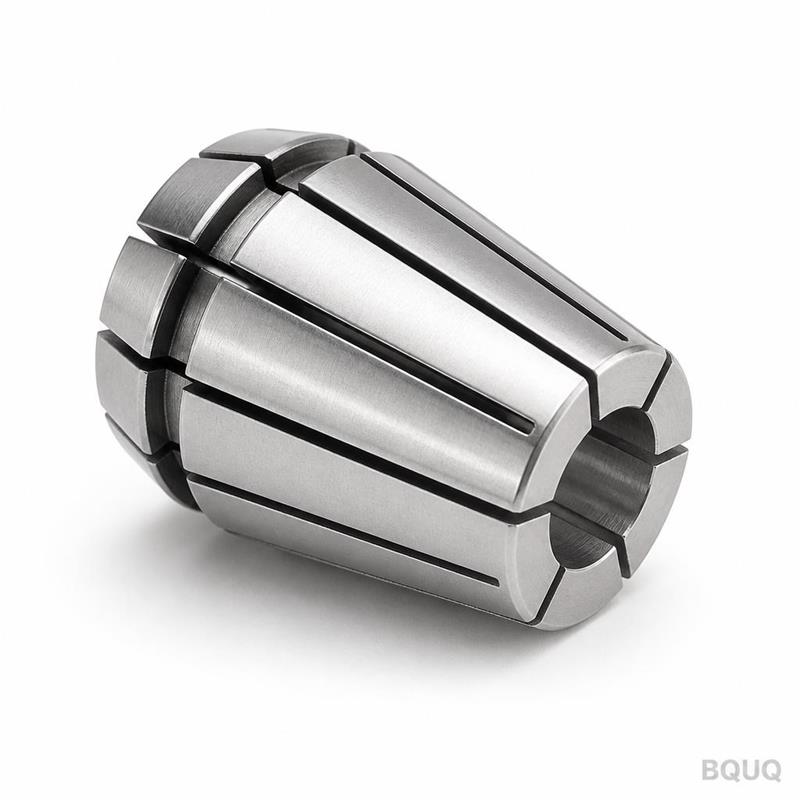
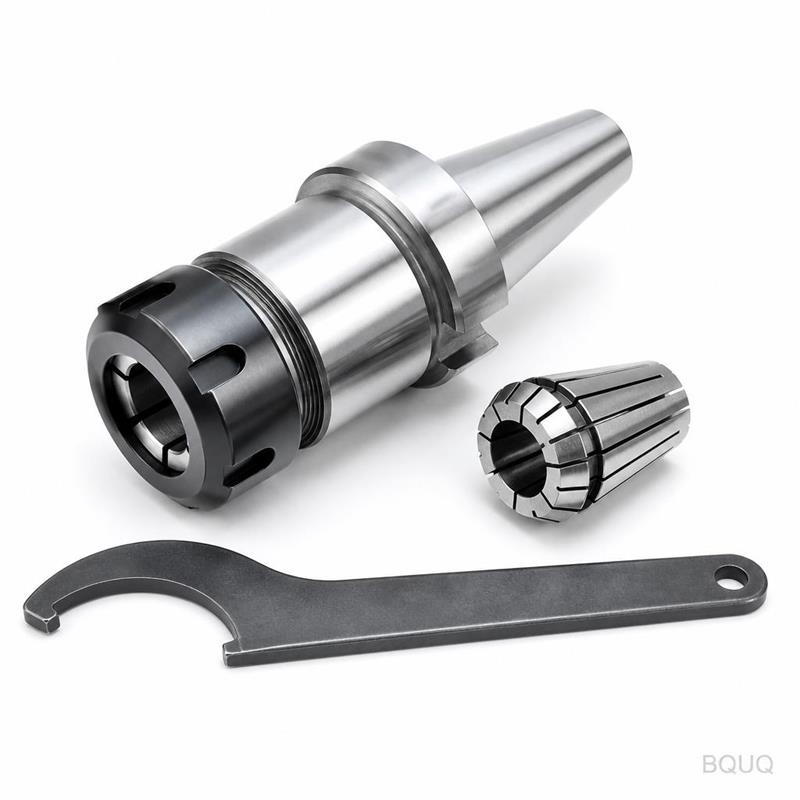
BQUQ CNC Machined ER11 Spring Collet Chuck with Drill Bit Set
What This ER11 Collet Chuck Does for Your Drilling Cycle This is a CNC machined ER11 spring collet chuck with drill bit, ready for direct mounting on your spindle or holder. It holds round-shank drill
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This ER11 Collet Chuck Does for Your Drilling Cycle
This is a CNC machined ER11 spring collet chuck with drill bit, ready for direct mounting on your spindle or holder. It holds round-shank drill bits from 1.0 mm to 7.0 mm with a guaranteed runout of 0.005 mm TIR at the nose, measured after assembly. The body is hardened to 58-60 HRC, and we ship standard sizes in 48 hours from our Dongguan factory. You get a rigid, repeatable grip that eliminates drill wandering and extends tool life by up to 30% compared to set-screw holders.
How the ER11 Collet Grips Tooling Without Runout
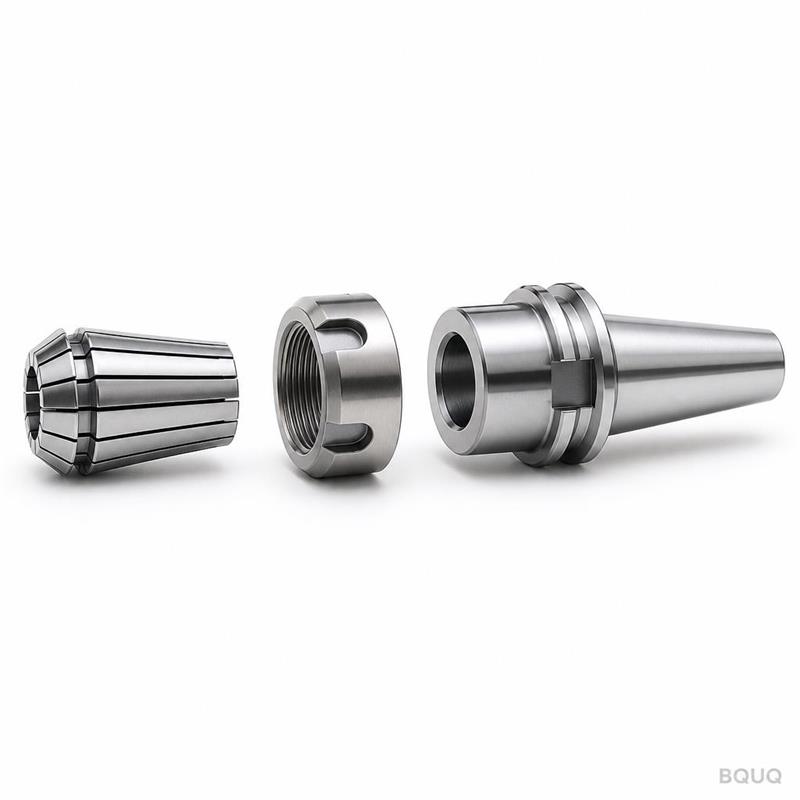
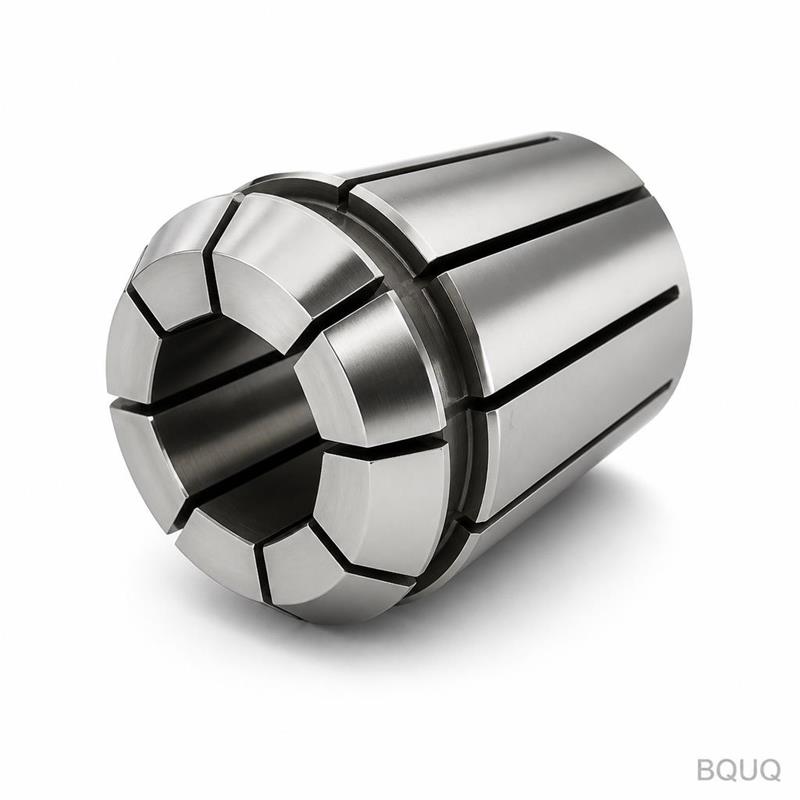
The ER11 collet uses a tapered outer surface that compresses evenly around the drill shank when you tighten the lock nut. Our chuck body is machined from a single billet of 42CrMo alloy steel, not welded or assembled from parts. The taper angle is ground to 8 degrees with a tolerance of ±0.002 mm. This precision manufacturing ensures the collet seats fully and concentrically, so your drill bit spins true at 20,000 RPM or higher. We test every chuck with a dial indicator before shipping.
Materials and Heat Treatment We Use for the Chuck Body
We start with 42CrMo steel, which gives high toughness and wear resistance. After CNC turning and milling, we carburize the surface to a case depth of 0.8-1.2 mm, then harden to 58-60 HRC. The bore is honed to a surface finish of Ra 0.4 µm. The lock nut is made from 20CrMnTi, case-hardened to 60-62 HRC, and its threads are rolled, not cut, for smoother tightening and longer life. No coatings, no plating—just clean, hard steel that holds up in coolant-heavy drilling applications.
ER11 Chuck Sizes, Runout, and Hardness Specifications
Parameter
Value
Collet type
ER11 spring collet
Clamping range
1.0 mm – 7.0 mm (metric), 1/16" – 1/4" (inch)
Chuck body material
42CrMo alloy steel, carburized
Hardness (body)
58-60 HRC
Hardness (lock nut)
60-62 HRC
Runout (TIR at nose)
0.005 mm
Surface finish (bore)
Ra 0.4 µm
Taper angle accuracy
±0.002 mm
Max RPM
20,000 RPM
Lead time (standard sizes)
48 hours
MOQ
No MOQ – order 1 piece
Why a Single-Piece Billet Beats a Fabricated Chuck
Many low-cost chucks are made from free-cutting steel or even cold-drawn bars, which deform under heat. We machine the ER11 chuck body from a solid 42CrMo billet on a 5-axis CNC lathe, then grind the taper on a dedicated internal grinder. This process removes residual stress and gives you a chuck that holds its geometry after thousands of clamping cycles. If you compare our chuck to a cast or forged competitor, you will see the difference in the first 100 parts you drill.
Inspection Before Every Shipment
Each chuck is 100% inspected, not sample-checked. We use a CMM (coordinate measuring machine) to verify the taper angle, bore diameter, and concentricity. Then we assemble the chuck with a standard ER11 collet and a 5.0 mm drill bit, spin it on a test spindle, and measure runout with a laser sensor. We record the actual runout value on the QC report, which you receive with the shipping documents. If the runout exceeds 0.005 mm, the chuck is scrapped—not reworked.
Adapting This Chuck for Your Spindle or Tool Holder
The standard shank is straight, 10 mm diameter by 30 mm long, but we can machine any shank configuration you need: threaded, tapered, or with a flat for set screws. Send us your spindle drawing or the holder part number, and we will match the geometry exactly. We also offer the chuck with a pre-mounted ER11 collet of your chosen size, so you do not have to buy collets separately. For drilling deep holes, we can add internal coolant holes through the Chuck body.
What is the minimum order quantity?
No MOQ – you can order a single piece to test with your machine, and we offer quantity discounts starting at 10 pieces.
Can you customize the shank or clamping range?
Yes, we machine custom shanks, extended lengths, and special clamping ranges up to 7.0 mm, with your drawing or a sample part.
How do you control quality for large orders?
We use SPC (statistical process control) on every batch, and each chuck comes with a CMM inspection report and a runout certificate.
What is your standard lead time for custom ER11 chucks?
Standard sizes ship in 48 hours; custom shanks or materials take 5-7 working days, and we can rush orders for an additional fee.
Before you buy, check our CNC cutting tool selection guide to see how this chuck fits into your overall tooling strategy. For tighter tolerances on the chuck itself, review our CNC machining tolerances guide to understand what we can hold on your custom part.
This CNC machined ER11 spring collet chuck with drill bit is made in China, and it is built for production environments where downtime costs money. Every chuck is inspected, tested, and shipped with a report. We are a precision manufacturing factory with 20 years of experience, and we stand behind our work.
Send your drawing or the spindle interface details to get a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. No MOQ, no minimum call-out—just a precision chuck that works.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.