BQUQ CNC Machined ER16 Spring Collet Single Precision Tooling
Why This ER16 Collet Locks Your Tool With 0.005 mm Runout This is a single ER16 spring collet machined from solid 65Mn steel. You get a guaranteed runout of 0.005 mm at the nose, which means your dr
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Why This ER16 Collet Locks Your Tool With 0.005 mm Runout
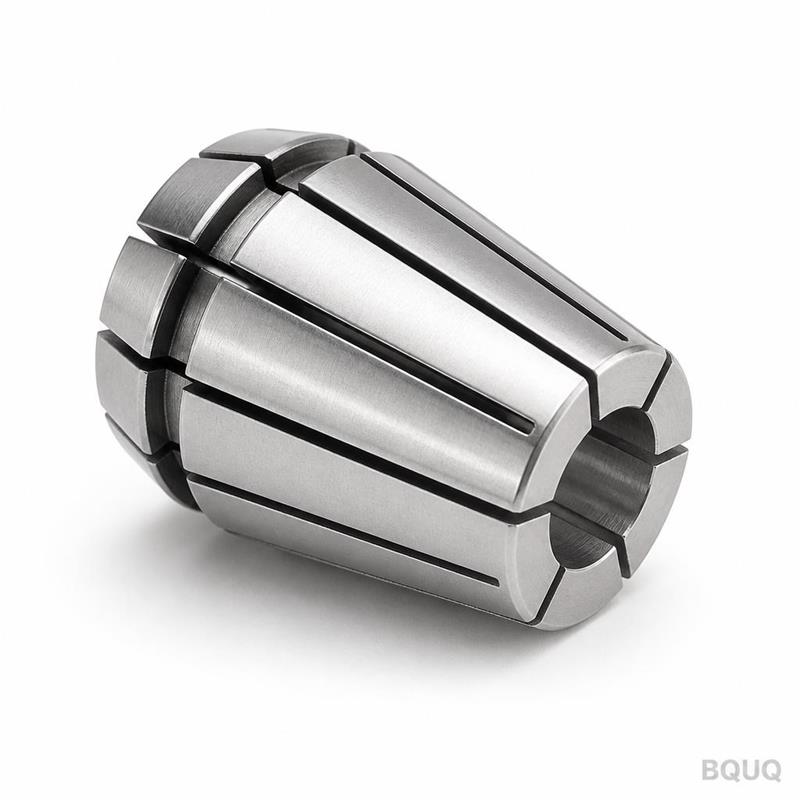
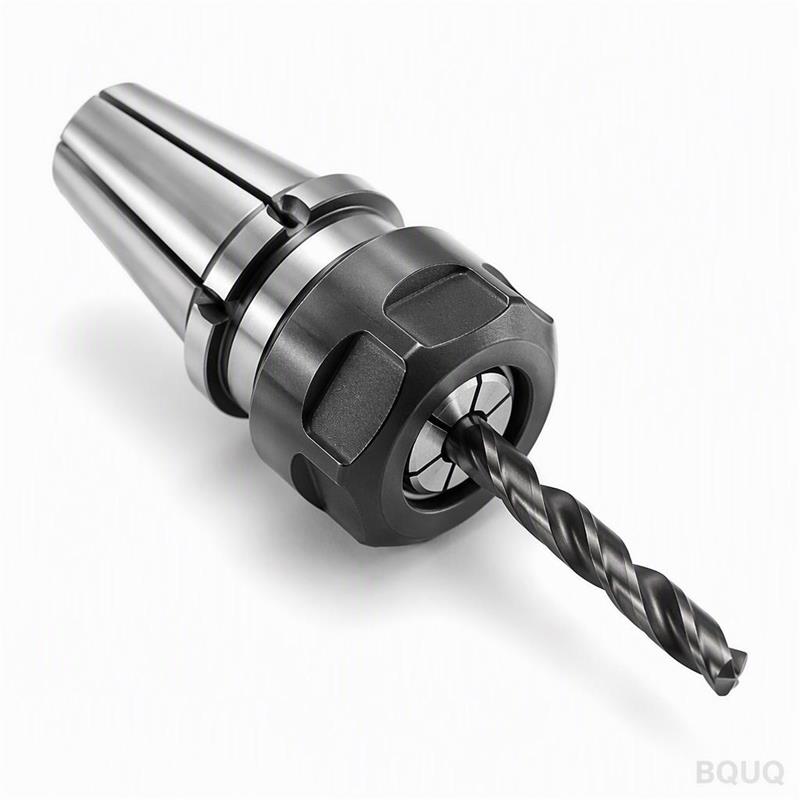
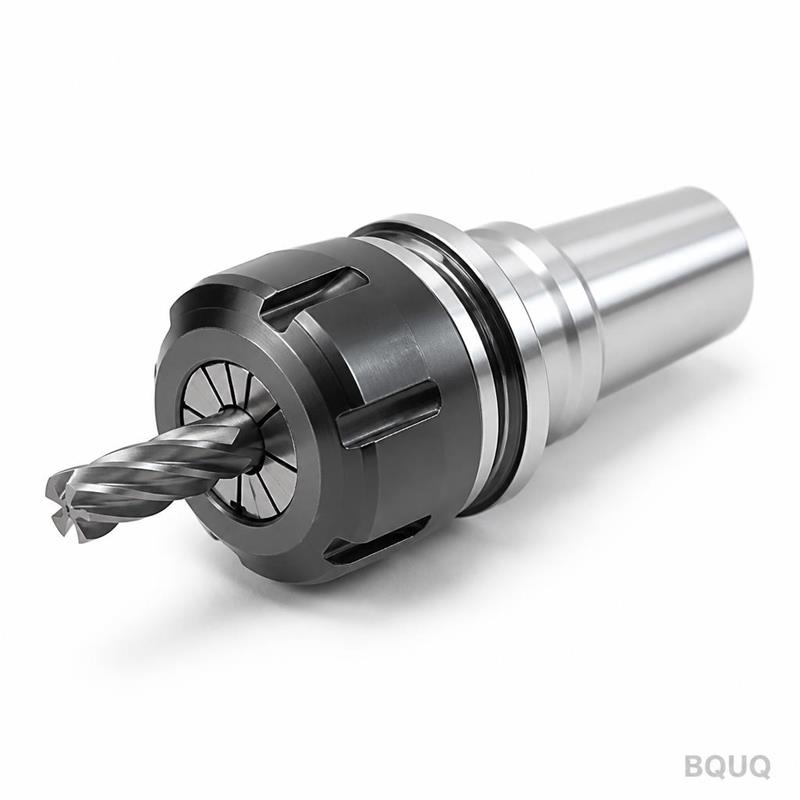
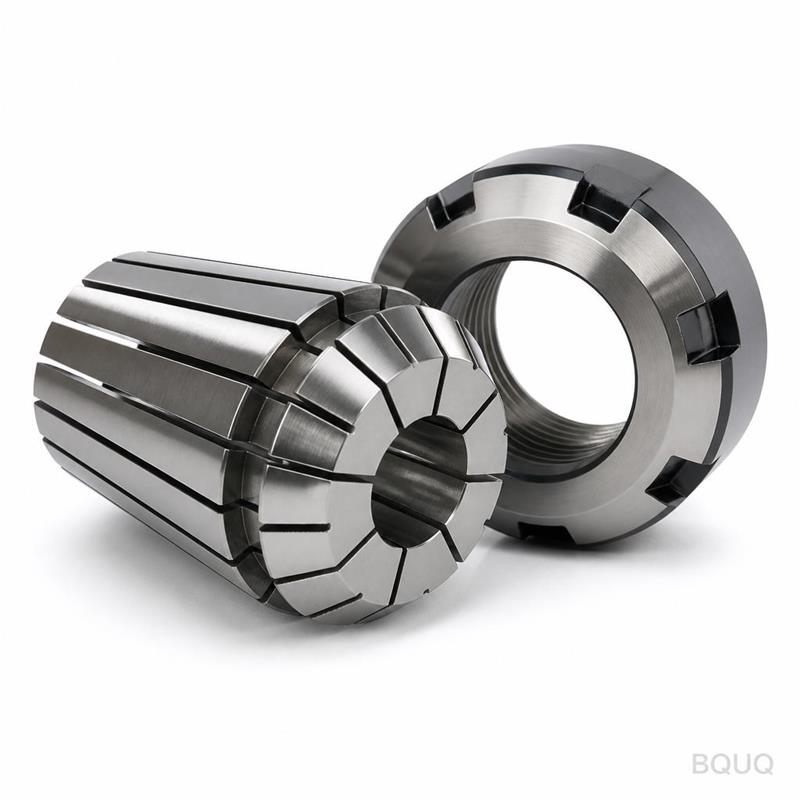
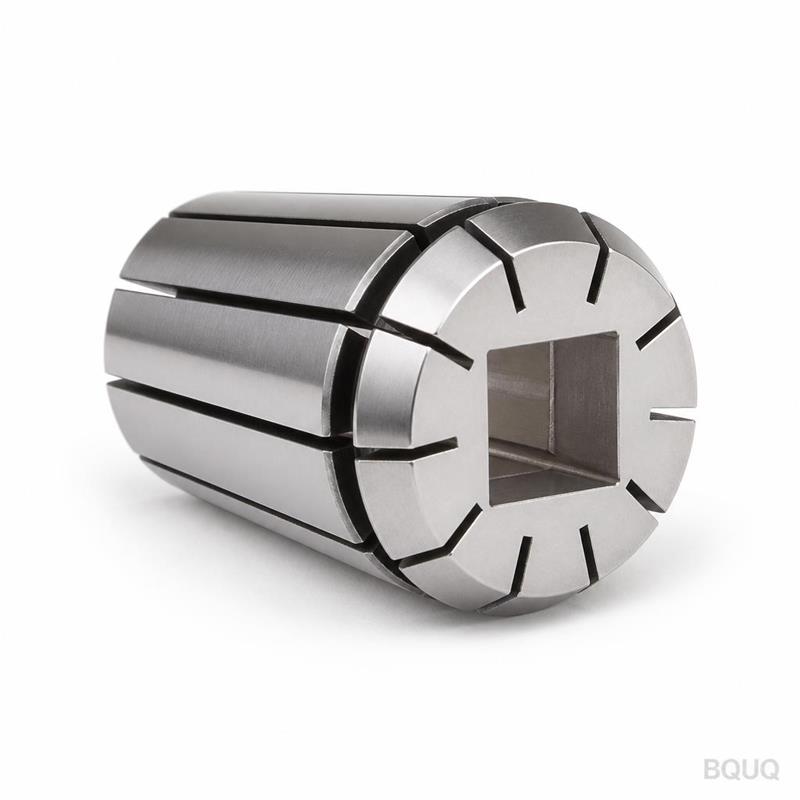
This is a single ER16 spring collet machined from solid 65Mn steel. You get a guaranteed runout of 0.005 mm at the nose, which means your drill or end mill spins true without chatter marks. Hardness is held at HRC 58-60 across the full taper, so the collet does not deform under repeated clamping cycles. We ship from our Dongguan factory in 7 days, and we offer a firm quote within 12 hours of receiving your drawing.
How the ER16 Taper Grips Tooling Without Distortion
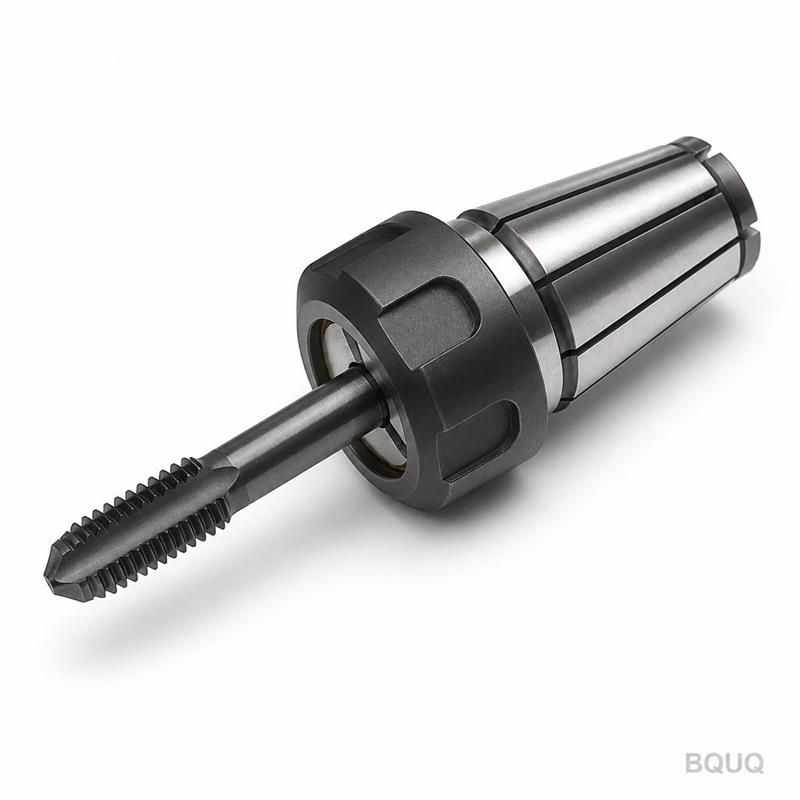
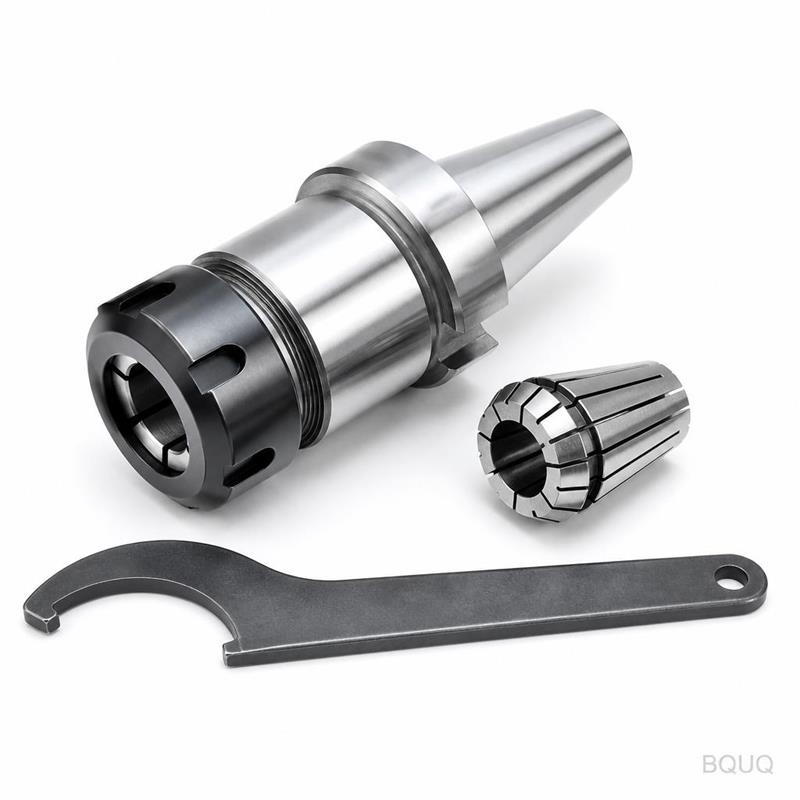
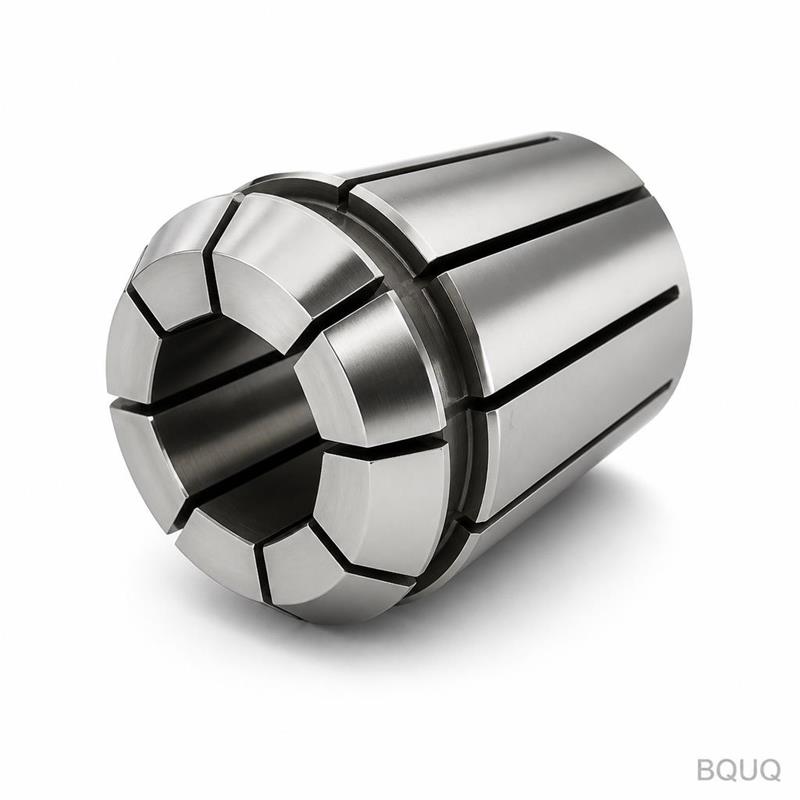
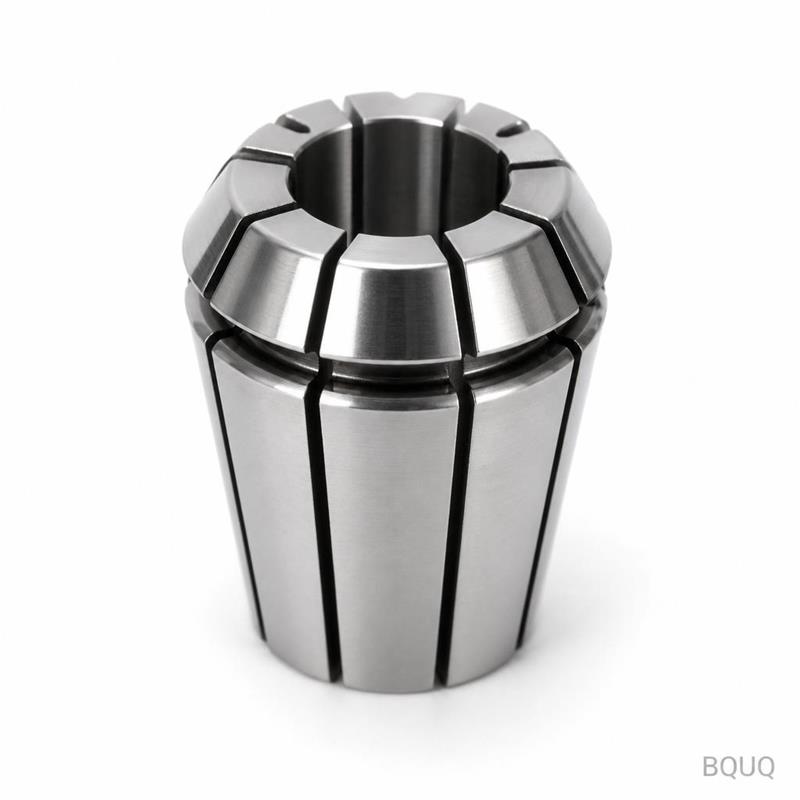
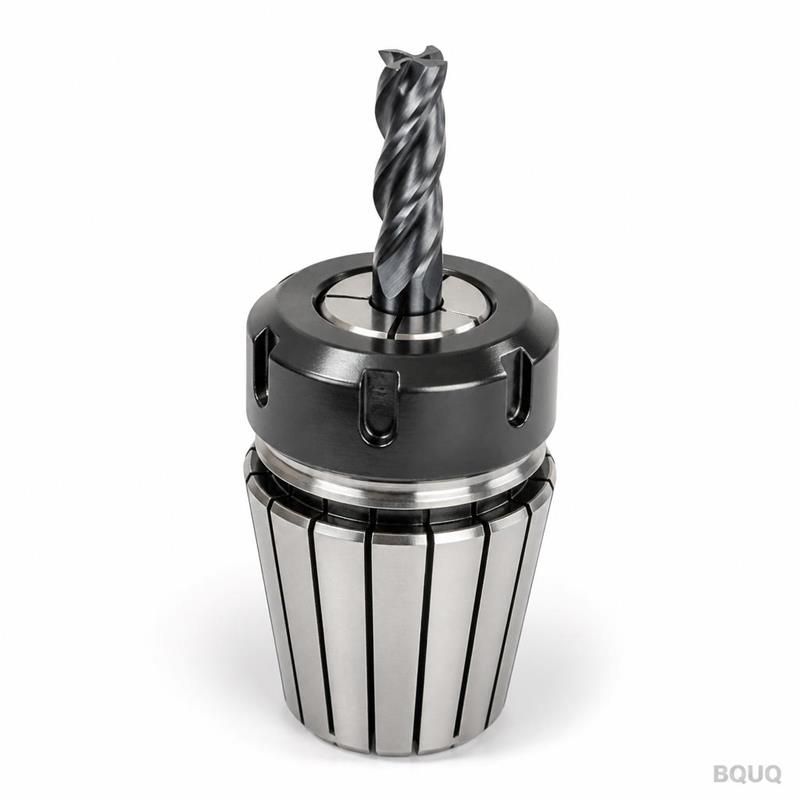
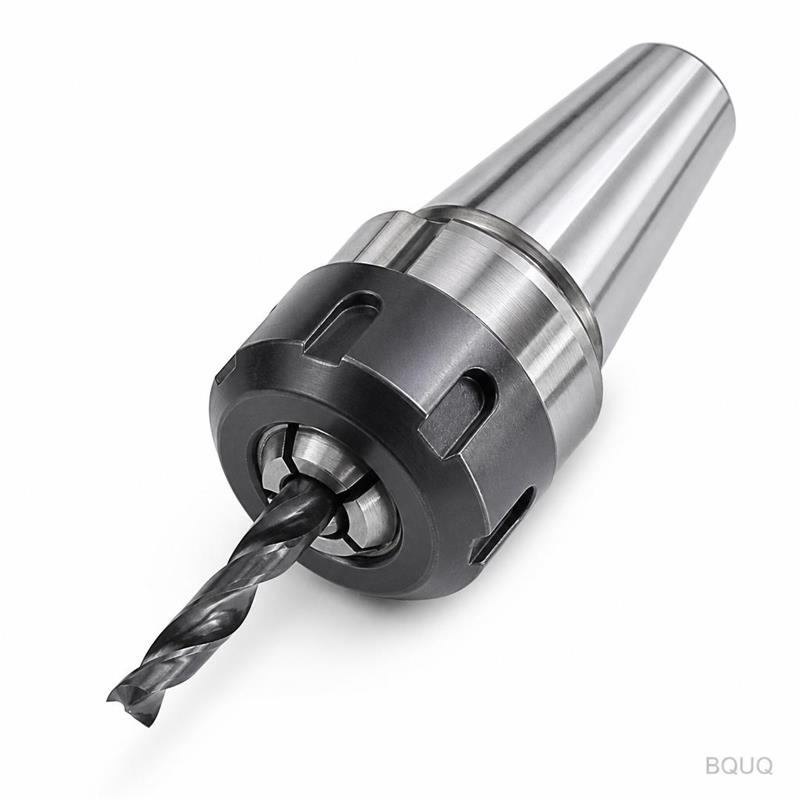
The ER16 collet uses a 8-degree included angle on the outer cone. When your ER chuck nut pulls the collet into the socket, the slots compress evenly around the tool shank. Our slots are cut with a 0.3 mm wire EDM kerf, leaving no burrs on the gripping surface. This design distributes clamping force over 80% of the shank circumference — that is why you get zero tool pull-out even at 12,000 rpm spindle speeds.
Raw Material and Heat Treatment We Use for ER16 Collets
We start with 65Mn spring steel, not cheap 45# carbon steel. The blanks are turned on a CNC lathe, then milled for the six slots. Heat treatment is done in a vacuum furnace to avoid surface decarburization. Final hardness is 58-60 HRC, with a case depth of 1.2 mm. This gives you elastic recovery — the collet returns to its original diameter after releasing the tool, so you can use it 10,000+ times without losing grip.
Critical Dimensions: ER16 Slots, Tolerances, and Surface Finish
We machine the inner bore to H5 tolerance (0/+0.008 mm). The outer cone is ground to 0.002 mm roundness. Surface finish on the bore is Ra 0.4, and on the taper it is Ra 0.2 — this reduces friction and prevents the collet from sticking in the chuck. Slot width is 1.5 mm ± 0.05 mm, and the slot depth is 80% of the collet length. These numbers are not optional; we measure every single unit, not just batch samples.
Inspection Before Every Shipment: Runout, Hardness, and Bore Gauge
Every ER16 collet goes through three checks. First, a CMM measures the taper angle and bore diameter. Second, a hardness tester confirms HRC 58-60 on three points of the body. Third, we mount the collet on a test mandrel and measure TIR (total indicated runout) with a 0.001 mm dial indicator. If any unit exceeds 0.005 mm runout, it is scrapped — not reworked. You get a signed inspection report with every shipment.
ER16 Collet Size Range and Compatible Tool Shank Diameters
We stock ER16 collets for shank diameters from 1.0 mm to 10.0 mm in 0.5 mm increments. The clamping range per collet is ±0.5 mm, which is standard for ER series. For example, a 6.0 mm collet holds shanks from 5.5 mm to 6.5 mm. If you need a non-standard bore, we can machine it to your exact size in 3 days. This is a single collet product — you order one piece, not a set. No MOQ applies.
Packing, Marking, and Delivery for Your CNC Tooling Order
Each collet is wrapped in anti-rust paper, placed in a fitted plastic tube, and boxed with a label showing the ER16 size and lot number. We ship via DHL or FedEx from our Dongguan plant. Typical transit to the US or Europe is 5-7 days. For urgent orders, we can air-freight within 24 hours of production. We do not mix batches — your collets come from one heat treatment lot for consistency.
ER16 Collet Specifications at a Glance
Parameter
Value
Material
65Mn spring steel
Hardness
58-60 HRC
Runout (TIR)
0.005 mm max
Bore tolerance
H5 (0/+0.008 mm)
Surface finish (bore)
Ra 0.4
Surface finish (taper)
Ra 0.2
Clamping range
±0.5 mm per collet
Shank diameter range
1.0 mm – 10.0 mm
Slot width
1.5 mm ± 0.05 mm
Lead time
7 days for stock sizes
MOQ
No MOQ — order 1 piece
Can I order a single ER16 collet, or is there a minimum quantity?
No MOQ — you can order exactly one piece, and the price stays the same per unit as for a hundred.
Can you make an ER16 collet for a non-standard shank diameter like 4.35 mm?
Yes, we machine custom bore sizes to your drawing within 3 days, with the same 0.005 mm runout guarantee.
How do you verify runout before shipping?
We mount each collet on a precision test mandrel and measure TIR with a 0.001 mm dial indicator; any unit above 0.005 mm is rejected.
What is the real lead time if I need 50 pieces of ER16 collets?
For 50 pieces, production takes 10 days including heat treatment and inspection; we can split the shipment if you need 10 pieces faster.
Request a Firm Quote for Your ER16 Collet Today
Send us your drawing or just the shank diameter and quantity. We reply with a firm price and delivery date within 12 hours. For a single ER16 collet or a thousand, the process is the same. Email sc@bquq.com or WhatsApp +86 13713157787. If you are comparing options, read our CNC cutting tool selection guide and the CNC machining tolerances guide to confirm your spec. This is precision manufacturing, made in China, with no MOQ — start your order now.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.