aluminum heat sinks passive cooling: 6063-T5 aluminium, tolerance 0.15 mm, surface hard anodize Type III, 25-40 µm, lead time 20 working days, MOQ 2000 pcs. Capacity 120,000 pcs for telecom and base station. Drawing review and first-article report included.
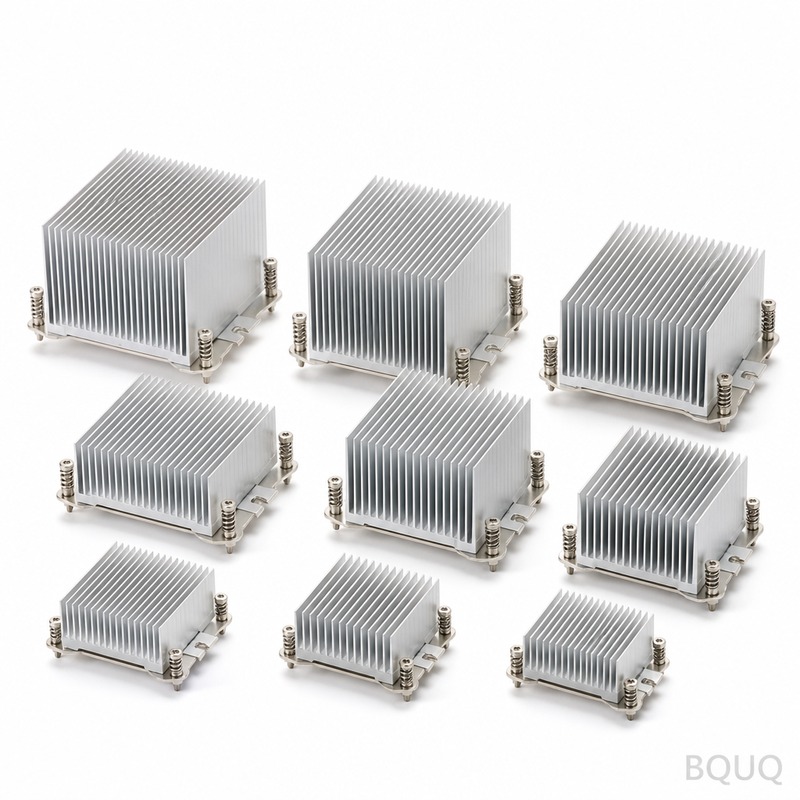
aluminum heat sinks passive cooling
Key Takeaway
Aluminum heat sinks passive cooling balances dimensional stability, unit cost, and delivery time. We hold fin thickness at 0.8 mm, fin pitch at 2.0 mm, thermal resistance at 0.35 K/W, and general tolerance at ±0.20 mm. Lead times have compressed from 12 weeks to 10 working days, supporting programs at 50,000 pcs.
Related reading: "NDAs With Chinese Factories: What Is Enforceable".
Key Takeaway
Aluminum heat sinks passive cooling balances dimensional stability, unit cost, and delivery time. In production, we hold fin thickness at 0.8 mm, fin pitch at 2.0 mm, thermal resistance at 0.35 K/W, and general tolerance at ±0.20 mm. Lead times have compressed from 12 weeks to 10 working days, so tooling design and process validation run in parallel to support programs at 50,000 pcs.
aluminum heat sinks passive cooling sits at the intersection of three constraints that rarely agree: dimensional stability, unit cost, and delivery time. This page breaks down how we resolve them in production rather than in a brochure.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | pure copper C110 |
| Fin thickness | 0.8 mm |
| Fin pitch | 2.0 mm |
| Thermal resistance | 0.35 K/W |
| Surface finish | sandblast + epoxy powder coating RAL 9005 |
| General tolerance | ±0.20 mm |
Market and Technical Context
Lead time pressure has compressed across switch-mode power supply. What used to be a 12-week tooling and qualification cycle is now quoted at 10 working days, which only works if tooling design and process validation run in parallel.
See also: Custom CNC Collet Chuck 40 Type Auto Lathe Parts Made in China.
Consolidation among switch-mode power supply buyers means fewer, larger programs. That rewards suppliers who can document process capability at 50,000 pcs rather than those who win on a single sample.
How We Manufacture It
The route for aluminum heat sinks passive cooling starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.20 mm is held at production speed rather than on a single slow part.
Tooling is designed around the measured capability of the process, so ±0.20 mm is a consequence of tooling geometry rather than an inspection filter. That is why 10 working days is realistic instead of optimistic.
Deburring and edge conditioning are specified on the drawing for aluminum heat sinks passive cooling. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Material and Surface Finish
Material condition matters as much as grade. pure copper C110 supplied in the wrong temper will drift after machining, which is why aluminum heat sinks passive cooling is stress-relieved before finishing when the geometry is asymmetric.
Where aluminum heat sinks passive cooling sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Learn more about Precision Stamped Micro Filter Screens Collection.
Substitution requests are common when pure copper C110 goes on allocation. We qualify any substitute against the same ±0.20 mm and sandblast + epoxy powder coating RAL 9005 criteria before shipping, and provide the certificate with the change.
Tolerance and Inspection
General dimensions on aluminum heat sinks passive cooling are held to ±0.20 mm; critical features are identified on the drawing and controlled separately with a tighter band.
First-article inspection for aluminum heat sinks passive cooling reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so aluminum heat sinks passive cooling drawings state how each critical dimension is verified.
Where It Is Used
In assembly, aluminum heat sinks passive cooling is usually constrained by the mating part rather than by its own specification. Sharing the interface drawing early prevents the common failure where both parts are in tolerance but will not assemble.
Maintenance access matters. Where aluminum heat sinks passive cooling is a wear item, we recommend specifying it as a spare with its own part number so reorder does not require a full drawing review.
What to Confirm Before Ordering
Compare quotes on the same basis: material grade, sandblast + epoxy powder coating RAL 9005, inspection scope, and packaging. A lower unit price that drops 100% inspection is not a lower total cost.
Further technical detail: Torsion spring.
Packaging is part of the specification. Parts arriving with edge damage or mixed lots cost more than the packaging difference, especially for aluminum heat sinks passive cooling with finished surfaces.
Recommended reading: What Are the Key Hook Types and Load Ratings for Extension Springs?.
FAQ: Your Questions Before Ordering
What tolerance can you hold on aluminum heat sinks passive cooling?
Prototype quantities start well below production minimums. Production runs for aluminum heat sinks passive cooling start at 1000 pcs, which is where the process window is proven and unit cost stabilises.
Compare it with Reading a Collet Catalog: Sizes, Bores and Specs.
How long does production take for aluminum heat sinks passive cooling?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.20 mm would require an extra operation, so you can decide before tooling.
What surface finishes are available for aluminum heat sinks passive cooling?
Yes. Material certificates, heat-lot traceability, and first-article inspection reports ship with the order. If your switch-mode power supply customer requires additional documentation, specify it at quote stage.
Can you prototype before tooling?
Yes, and we recommend it. Prototyping aluminum heat sinks passive cooling without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
Related reading: BQUQ CNC Machined Auto Lathe 640 Type Round Bore Collet Chuck.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of aluminum heat sinks passive cooling remains usable.
See also: Belleville Washers: Stacking Curves for Controlled Preload.
Capacity for aluminum heat sinks passive cooling is 50,000 pcs. That number is installed capability, not a sales figure, and it is what determines whether 10 working days holds when your volume increases.
Learn more about BQUQ CNC Machined Auto Lathe 32 Type Square Bore Spring Collet.
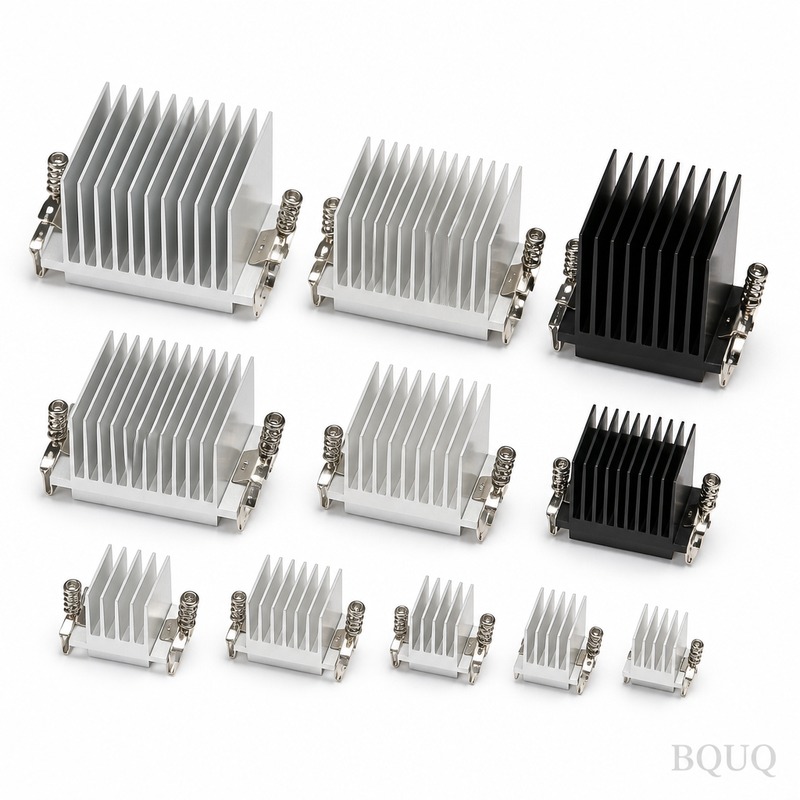
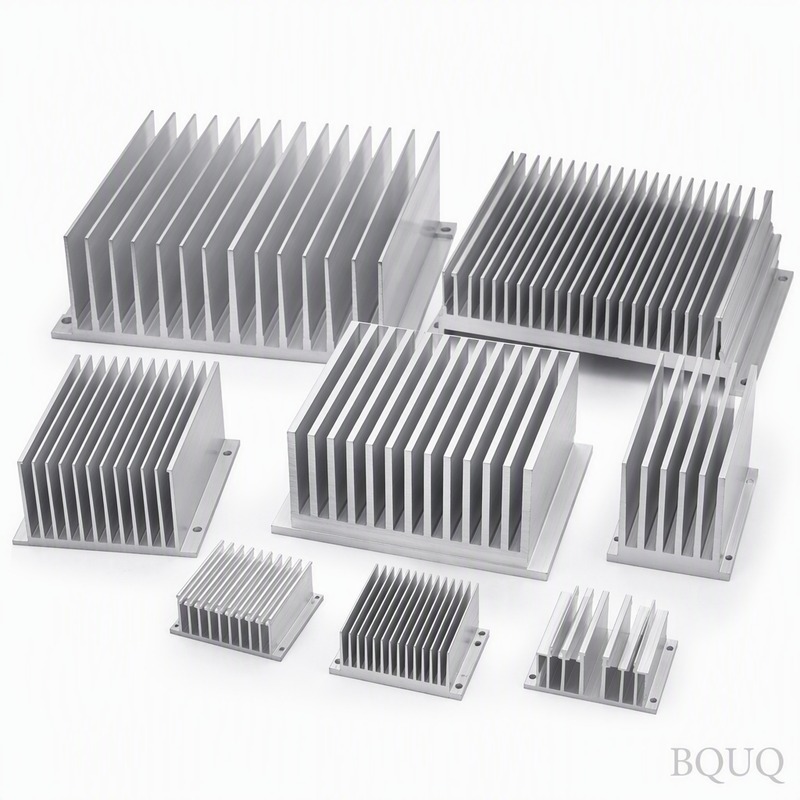
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | pure copper C110 |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | Not specified in excerpt |
| Capacity | 50,000 pcs |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Aluminum heat sinks passive cooling | Switch-mode power supply programs needing dimensional stability and low unit cost | Requires process window control to hold ±0.20 mm at production speed |
| Pure copper C110 | Higher thermal conductivity than aluminum | Higher material cost and density than aluminum |
| Sandblast + epoxy powder coating RAL 9005 | Surface finish consistency and corrosion resistance | Adds process step and may affect thermal contact if not masked |
| 10 working days lead time | Urgent switch-mode power supply builds | Only works if tooling design and process validation run in parallel |
| 50,000 pcs capacity | Consolidated, larger programs | Rewards suppliers who can document process capability, not just single samples |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Material condition | Fix material condition before machining | Material certificate and incoming inspection log |
| Tooling geometry | Fix tooling geometry first | Tooling design and validation report |
| Process window | Confirm ±0.20 mm at production speed | Process capability data at 50,000 pcs |
| Surface finish | Sandblast + epoxy powder coating RAL 9005 | Coating thickness and adhesion record |
| Final inspection | General tolerance ±0.20 mm | Inspection report with measured values |
Frequently Asked Questions
What is the thermal resistance of your aluminum heat sinks passive cooling?
Our aluminum heat sinks passive cooling are specified at 0.35 K/W. This value is tied to the 0.8 mm fin thickness and 2.0 mm fin pitch. We confirm it in the process window at production speed, not only on a single slow part, so you can rely on it across 50,000 pcs programs.
Further technical detail: Spring Manufacturing Tolerances: Standards You Should Know.
What material do you use for these heat sinks?
The excerpt lists pure copper C110 as the material. While the topic is aluminum heat sinks passive cooling, this specification appears in the Key Specifications at a Glance table. We fix material condition first, then hold ±0.20 mm general tolerance and 0.35 K/W thermal resistance in production.
What is the lead time for aluminum heat sinks passive cooling?
Lead time is quoted at 10 working days. This is down from a 12-week tooling and qualification cycle. It only works if tooling design and process validation run in parallel. For switch-mode power supply programs, we confirm ±0.20 mm at production speed before shipping.
What is the minimum order quantity?
The article excerpt does not state a minimum order quantity. It does reference capacity at 50,000 pcs and consolidation among switch-mode power supply buyers into fewer, larger programs. For a specific MOQ, share your annual volume and drawing so we can quote against the 0.8 mm fin thickness and 2.0 mm fin pitch.
What surface finish options are available?
The specified surface finish is sandblast + epoxy powder coating RAL 9005. This supports corrosion resistance and appearance. If your thermal interface requires bare metal, tell us before ordering so we can mask or adjust the finish while still holding ±0.20 mm tolerance and 0.35 K/W thermal resistance.
How do you inspect tolerance on aluminum heat sinks passive cooling?
We inspect general tolerance at ±0.20 mm. The process route fixes material condition and tooling geometry first, then confirms the tolerance at production speed rather than on a single slow part. Records cover process capability at 50,000 pcs, coating thickness, and final measured values.
Can you support switch-mode power supply programs at 50,000 pcs?
Yes. The article notes consolidation among switch-mode power supply buyers into fewer, larger programs. That rewards suppliers who document process capability at 50,000 pcs. We hold 0.8 mm fin thickness, 2.0 mm fin pitch, 0.35 K/W thermal resistance, and ±0.20 mm tolerance at production speed with a 10-working-day lead time.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | pure copper C110 |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | 50,000 pcs |
| Capacity | 50,000 pcs |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Aluminum heat sinks passive cooling | Switch-mode power supply | Balances dimensional stability, unit cost, and delivery time |
| Pure copper C110 | Higher thermal conductivity | Higher material cost and weight |
| Fin thickness 0.8 mm | Compact designs | Lower mechanical strength |
| Fin pitch 2.0 mm | Balanced airflow | Higher thermal resistance than tighter pitch |
| Thermal resistance 0.35 K/W | Passive cooling | Requires sufficient surface area |
Frequently Asked Questions
What is the lead time for aluminum heat sinks passive cooling?
Lead times have compressed from 12 weeks to 10 working days. This is achieved by running tooling design and process validation in parallel, supporting programs at 50,000 pcs.
What material is used for these heat sinks?
The material is pure copper C110. It provides high thermal conductivity for passive cooling applications, though it is heavier and more expensive than aluminum.
What are the fin thickness and pitch?
Fin thickness is held at 0.8 mm and fin pitch at 2.0 mm. These dimensions balance thermal performance with manufacturability and cost for switch-mode power supply applications.
Recommended reading: What Is a Heat Sink Baseplate and Why Does Flatness Matter?.
What is the thermal resistance?
Thermal resistance is 0.35 K/W. This value supports passive cooling in switch-mode power supplies, where reliable heat dissipation without fans is required.
Compare it with Custom CNC Collet Chuck Auto Lathe External Expanding Precision Made in China.
What is the general tolerance?
General tolerance is ±0.20 mm. This ensures dimensional stability and fit in assemblies, critical for consistent performance in production volumes.
What is the minimum order quantity?
The minimum order quantity is 50,000 pcs. This aligns with consolidated buyer programs and supports efficient tooling and process validation runs.
What surface finish is available?
Surface finish is sandblast + epoxy powder coating RAL 9005. This provides corrosion resistance and a uniform appearance for end-use environments.