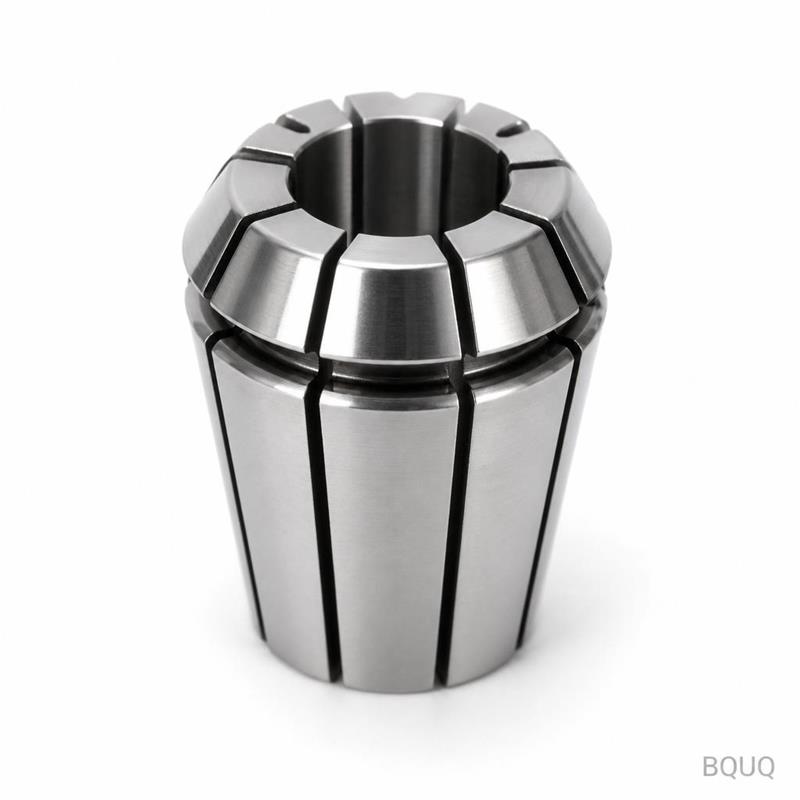
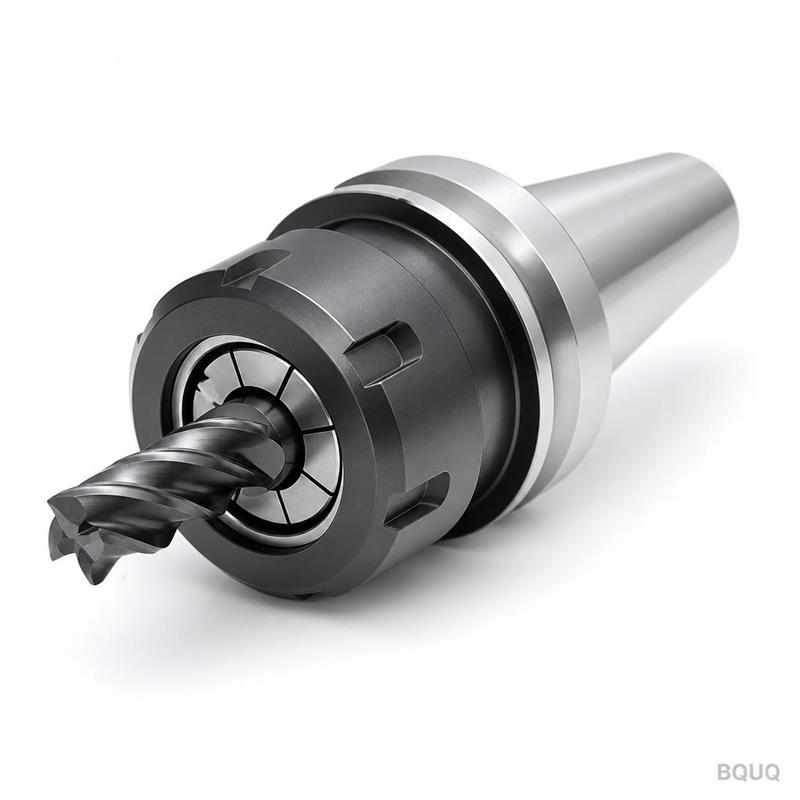
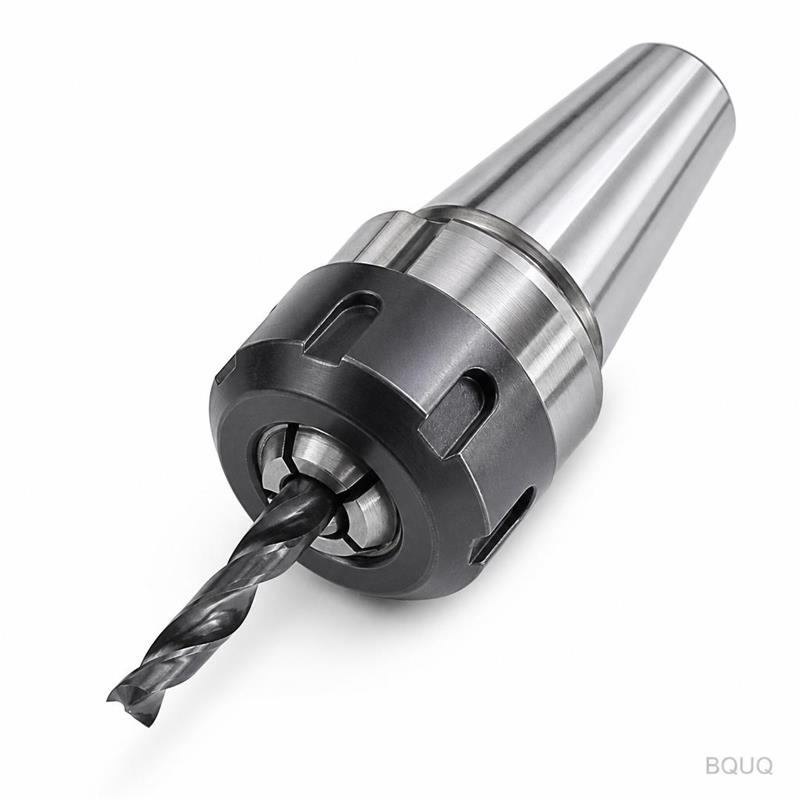
OpeningYour drawing defines the part. We make it exactly to that drawing—no interpretation, no shortcuts. Every custom CNC collet chuck body is machined, heat-treated, and inspecte
Custom CNC Collet Chuck Holder | Precision Manufacturing Made in China
OpeningYour drawing defines the part. We make it exactly to that drawing—no interpretation, no shortcuts. Every custom CNC collet chuck body is machined, heat-treated, and inspected before shipment. W
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
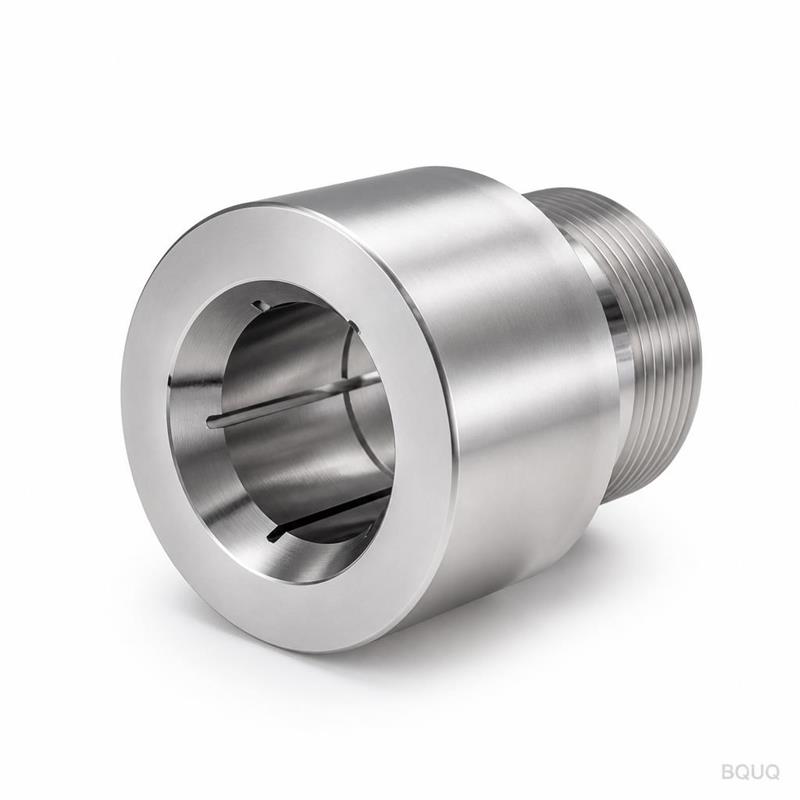
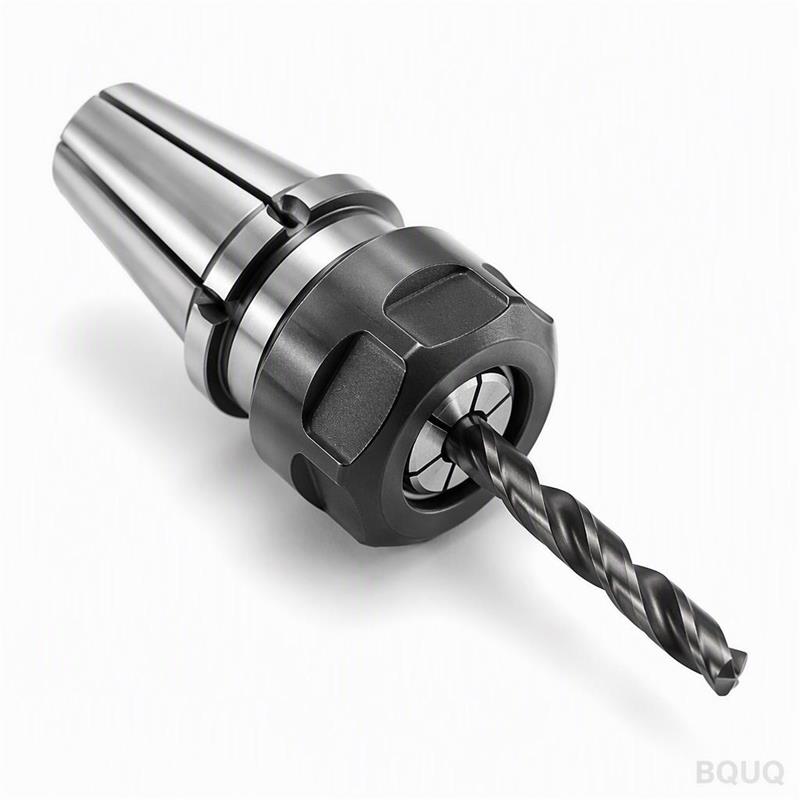
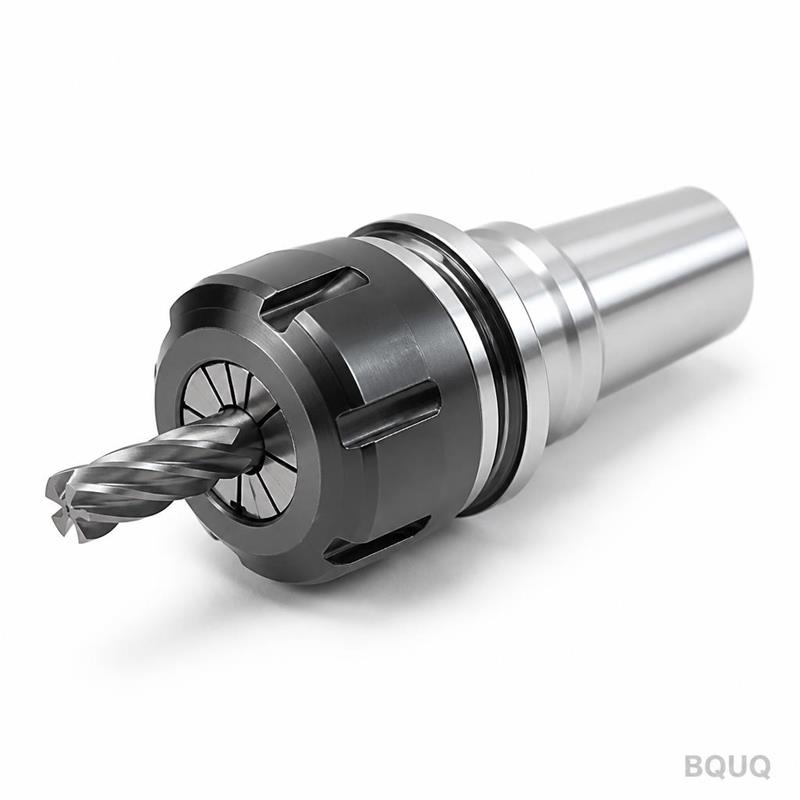
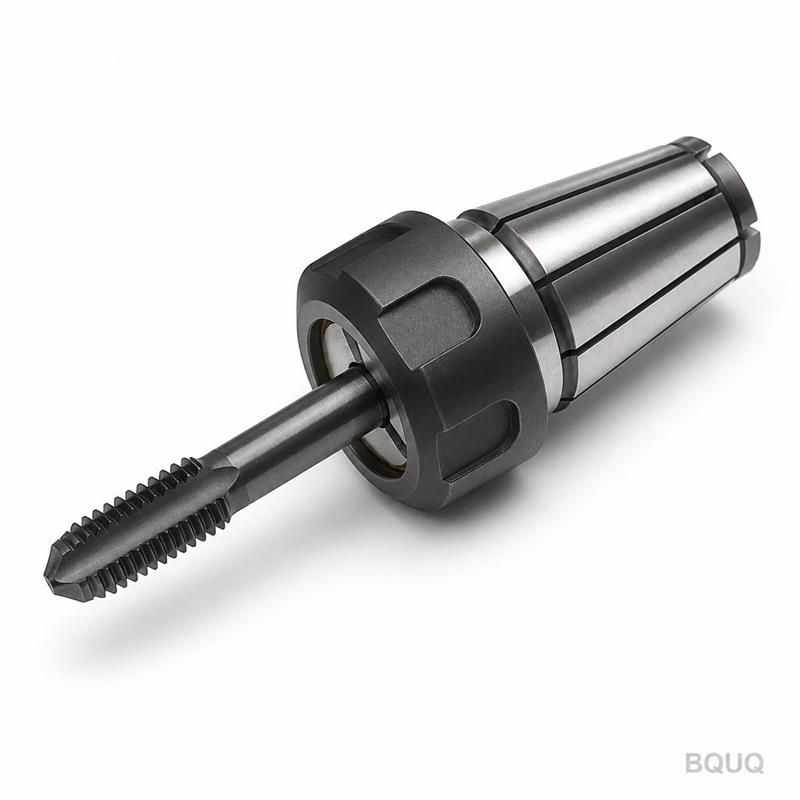
Your drawing defines the part. We make it exactly to that drawing—no interpretation, no shortcuts. Every custom CNC collet chuck body is machined, heat-treated, and inspected before shipment. We verify concentricity, taper angle, and pull-back dimensions on every unit.
Tolerance: ±0.005 mm on critical diameters
Runout: ≤0.005 mm TIR at nose
Lead time: 7–12 working days for prototypes
No MOQ—order one piece or one thousand
Material certs and full inspection report included
CMM, air gauge, optical comparator, hardness tester
Surface treatment
Black oxide, hard anodize, electroless nickel, or as-drawn
Three reasons buyers send us their drawings
1. Batch-traceable quality.
Every heat lot gets a unique code. We record material cert, heat treatment parameters, and final gauge readings. If a problem appears in your spindle, we trace it to the exact batch and shift. No guesswork.
2. Inspection report per batch.
You get a dimensional report with actual measured values—not just a pass/fail stamp. We include runout plots, taper angle deviations, and hardness readings. Your QC team can file it without re-checking.
3. One factory for CNC + stamping + spring + heatsink.
Your collet chuck is not the only part you need. We also make stamped retainers, compression springs for the chuck mechanism, and aluminum heatsinks for the spindle motor. One purchase order, one logistics point, one quality standard. Fewer suppliers, fewer delays.
Where these parts are used
Custom CNC collet chucks are not limited to standard ER collets. We machine bodies for:
High-speed spindles (30,000–60,000 RPM) for PCB drilling and routing—balancing is critical here.
Swiss-type lathes where the chuck body must fit a narrow guide bushing envelope.
Automatic tool changers in machining centers, requiring precise pull-stud geometry and repeatable seating.
Grinding spindles for internal grinding, where runout below 0.003 mm is mandatory.
Special collet systems (DIN 6499, TG, RDO, or custom tapers) for aerospace and medical part clamping.
Rotary transfer machines where the chuck body must survive coolant and chip impact without corrosion.
If your application needs a non-standard taper angle, a longer nose, or a custom flange, we machine it from solid. No off-the-shelf compromise.
Q: What is your MOQ?
A: No MOQ. We run one prototype for your validation, then scale to your production quantity. Tooling and setup costs are quoted separately for small batches.
Q: How do you guarantee tolerance and runout?
A: We grind the taper and bore in the same setup after heat treatment. Final runout is measured on a precision air spindle with a 0.0001 mm resolution gauge. The inspection report shows the actual numbers.
Q: What is your lead time?
A: Standard 7–12 working days for prototypes. Production batches of 100–500 pieces take 15–20 working days. If you need faster, we can expedite for a small surcharge—just ask.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. We supply mill certificates for raw material and a heat treatment report with hardness curves and case depth. All documents are traceable to your batch number.
Send your drawing
We quote firm in 12 hours. Send your 2D or 3D file, specify material and quantity, and we will reply with unit price, tooling cost (if any), and delivery date. No hidden charges.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing, made in China, with no MOQ. Your drawing is the only requirement.