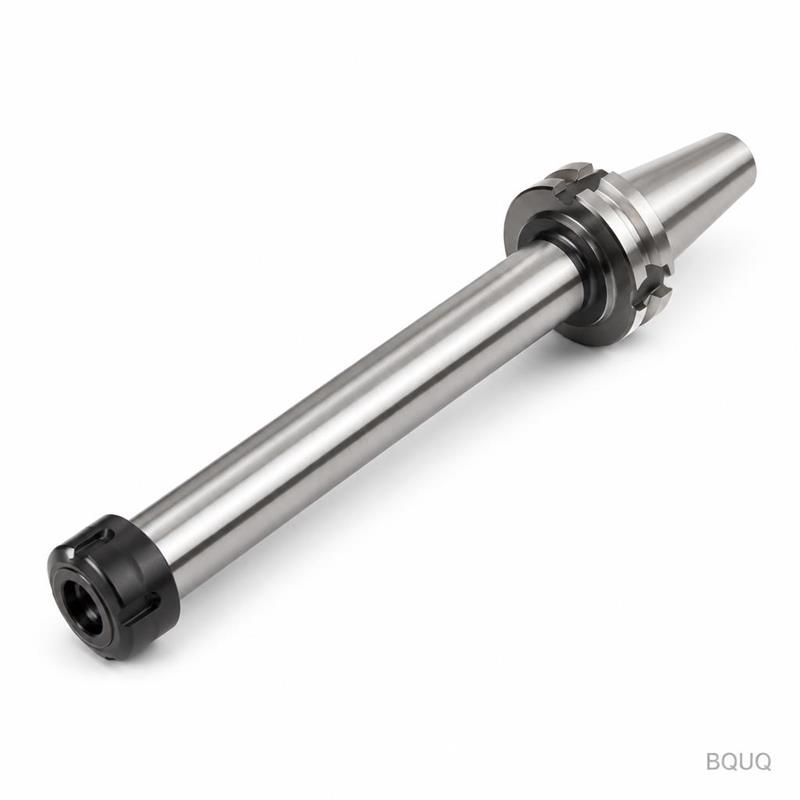
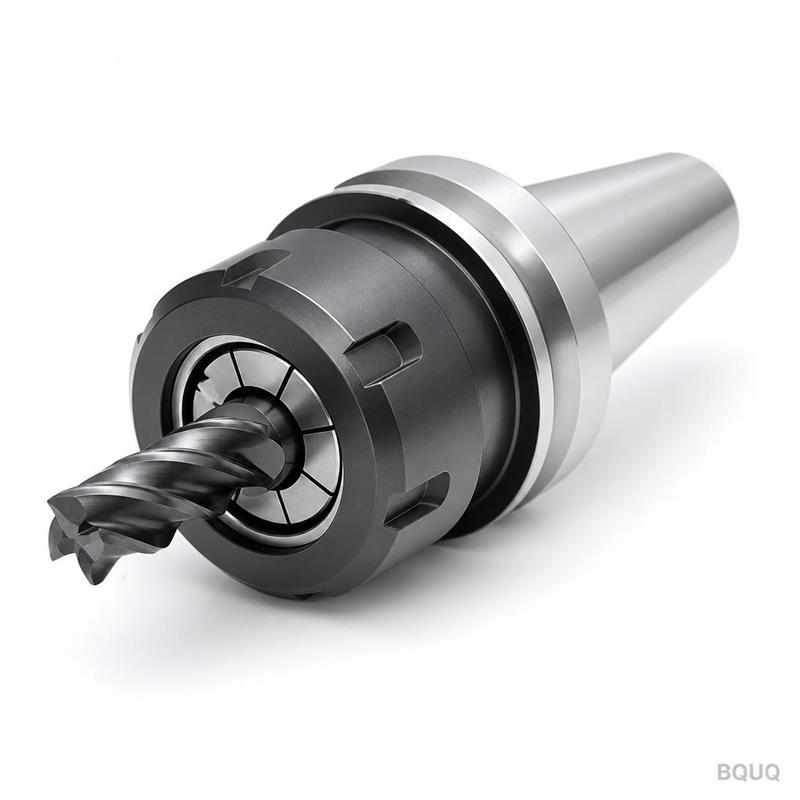
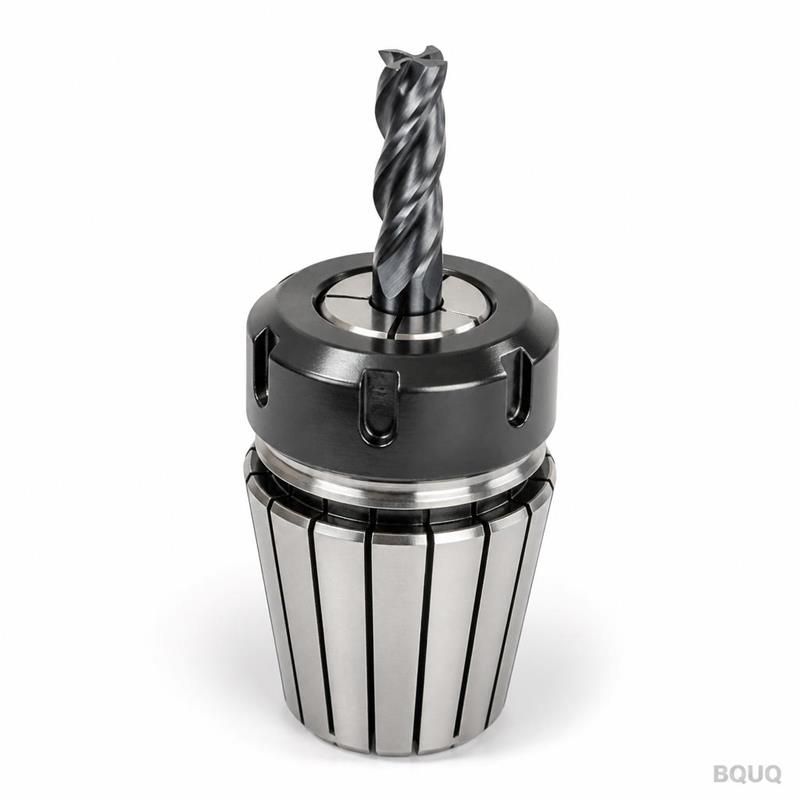
OpeningWe machine ER20 spring collets to your exact drawing. Not from stock blanks. Not modified from standard sizes. We start from bar stock and cut every profile, slot, and taper
Custom CNC Machined ER20 Spring Collet Chuck Precision Tooling No MOQ
OpeningWe machine ER20 spring collets to your exact drawing. Not from stock blanks. Not modified from standard sizes. We start from bar stock and cut every profile, slot, and taper to your specified d
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
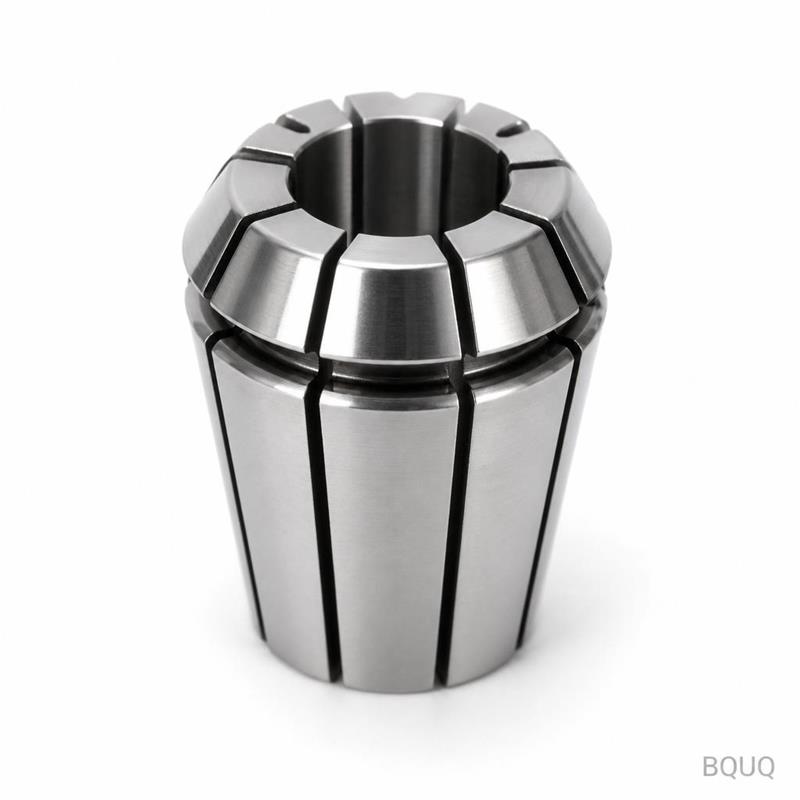
We machine ER20 spring collets to your exact drawing. Not from stock blanks. Not modified from standard sizes. We start from bar stock and cut every profile, slot, and taper to your specified dimensions.
Each collet is verified before shipment. We check the critical taper angle, slot width, and concentricity on a CMM. You get the numbers, not just a "passed" stamp.
At a glance: Tolerance ±0.005 mm on the bore, surface finish Ra 0.4, lead time 7–12 days, no MOQ. One collet or one thousand, same process.
Specifications
Parameter
Value
Material options
65Mn spring steel, 60Si2MnA, 9Cr18 stainless, or per drawing
Hardness
HRC 45–52 (through-hardened, not case-hardened)
Taper angle
8° per side, verified with air gauge
Bore tolerance
H5 (+0.008 / 0) or tighter per drawing
Concentricity
≤ 0.005 mm TIR at nose
Surface finish
Ra 0.4 on taper, Ra 0.8 on slots
Slot width
±0.02 mm, burr-free edges
Process
CNC turning, CNC milling, wire EDM for slots, heat treatment
Heat treatment
Vacuum hardening, no decarb layer
Batch size
1 to 10,000 pieces
Inspection
100% taper check, 30% full dimension report per batch
Lead time
7 days for prototypes, 12 days for production
We use 5-axis CNC turning centers for the taper and bore. Slots are cut with wire EDM to avoid tool deflection. Heat treatment is done in-house in a vacuum furnace, so we control the hardness curve, not a subcontractor.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Every collet gets a heat treatment lot number. We record the furnace cycle, the material heat number, and the final hardness reading. If you have a problem at tool #47, we can pull the exact batch record and tell you the hardness, the taper measurement, and the operator. No guesswork.
2. Inspection report per batch. You do not have to ask for it. Each shipment includes a dimensional report with actual measured values for taper angle, bore diameter, slot width, and concentricity. We use a Zeiss CMM and a calibrated air gauge. The report is signed by QC, not generated by software.
3. One factory for CNC, stamping, springs, and heat sinks. This is precision manufacturing with no middlemen. Your collet chuck assembly might need a spring, a stamped retainer, or a heat sink for the spindle drive. We make all of them under one roof. You send one drawing package, get one quote, one set of QC reports, and one shipment. Fewer vendors, fewer tolerance stack-ups, fewer arguments.
Where these parts are used
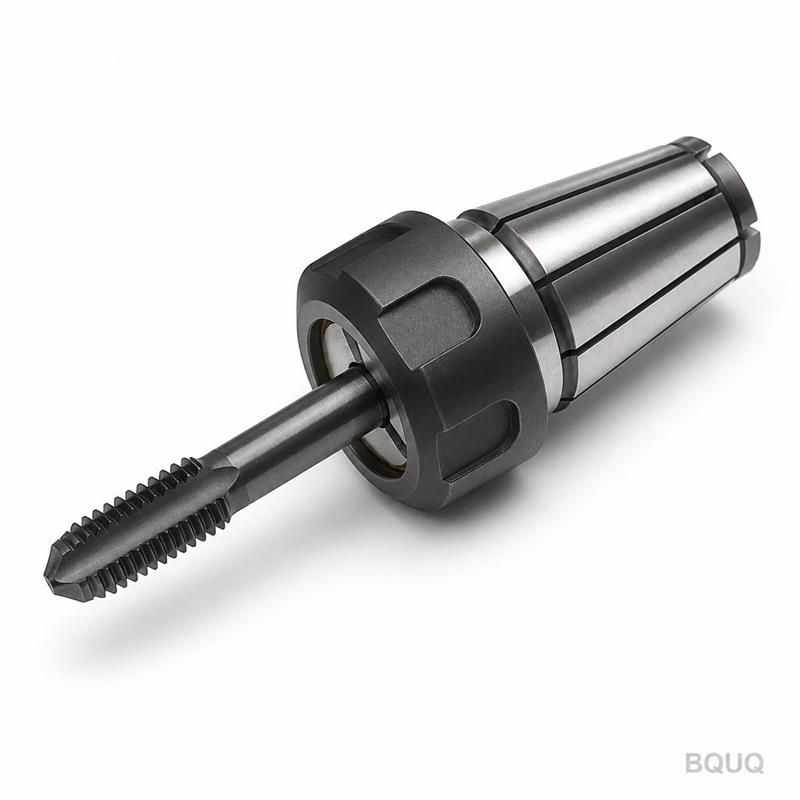
ER20 collets are the workhorse of high-speed machining centers and CNC lathes. Typical applications:
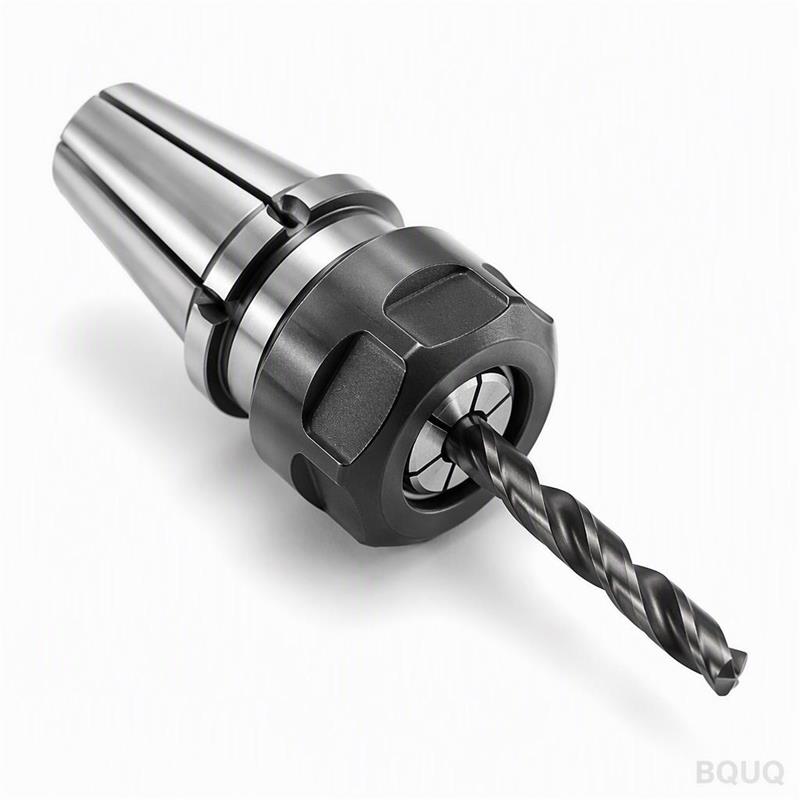
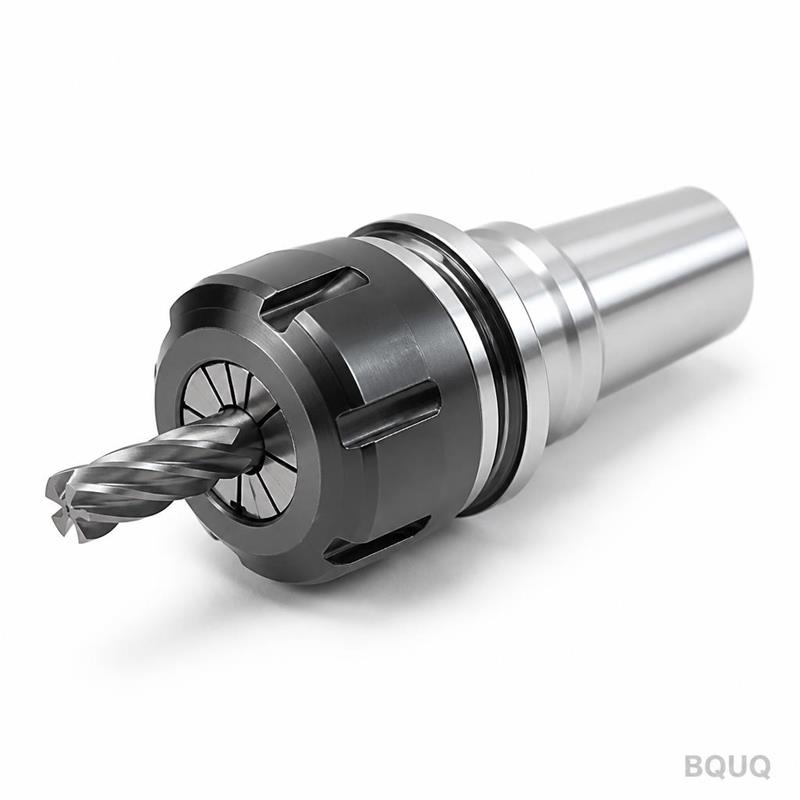
Tool holding on milling spindles – 1–13 mm shank tools, runout-sensitive finishing operations.
Drilling and reaming – where a hydraulic chuck is overkill but a standard drill chuck cannot hold concentricity.
Swiss-type lathes – guide bushings and main spindle collets for bar stock up to 20 mm diameter.
Automotive valve seat machining – production lines that run 24/7 and need repeatable tool change without re-setting offsets.
Aerospace aluminum and titanium – where tool pull-out under heavy radial load is not acceptable.
We also make custom ER20 variants: longer noses for deep reach, slotted versions for coolant-through, and hardened steel versions for high-clamping-force applications. If your drawing says "ER20 but different," we can make it.
Q: What is the MOQ?
A: No MOQ. We quote and make one piece. The per-piece price for a single collet is higher than for 100 pieces, but the process is identical. We do not batch small orders with other customers' work.
Q: How do you guarantee tolerance and quality?
A: The taper angle is measured with an air gauge, not a comparator. The bore is measured with a bore gauge calibrated to NIST standards. Each batch gets a written inspection report. If any dimension is out of spec, we scrap the part, not ship it.
Q: What is the lead time for a custom CNC collet chuck?
A: Prototype (1–5 pieces) is 7 days. Production (50+ pieces) is 10–12 days. Heat treatment adds 2 days, but it is included in those numbers. We do not quote "up to 4 weeks" to be safe. We quote what we can deliver.
Q: Can you provide material certificates?
A: Yes. We supply mill certificates for the raw material, heat treatment reports with actual hardness curves, and a certificate of conformity. All documents are in English. We can also provide third-party inspection (SGS or BV) at your cost.
Send your drawing
Email your PDF or STEP file to sc@bquq.com. Include the material, hardness, and quantity if you know them. If you do not, we will recommend based on your application.
We reply with a firm quote in 12 hours. Not a "budget range." A fixed price per piece, tooling cost (if any), and delivery date.
For urgent projects, WhatsApp us at +86 13713157787. We answer 7 days a week, 8:00–22:00 Beijing time.
Custom CNC collet chuck, made in China, with no MOQ and no surprises. Send the drawing. Get the quote.