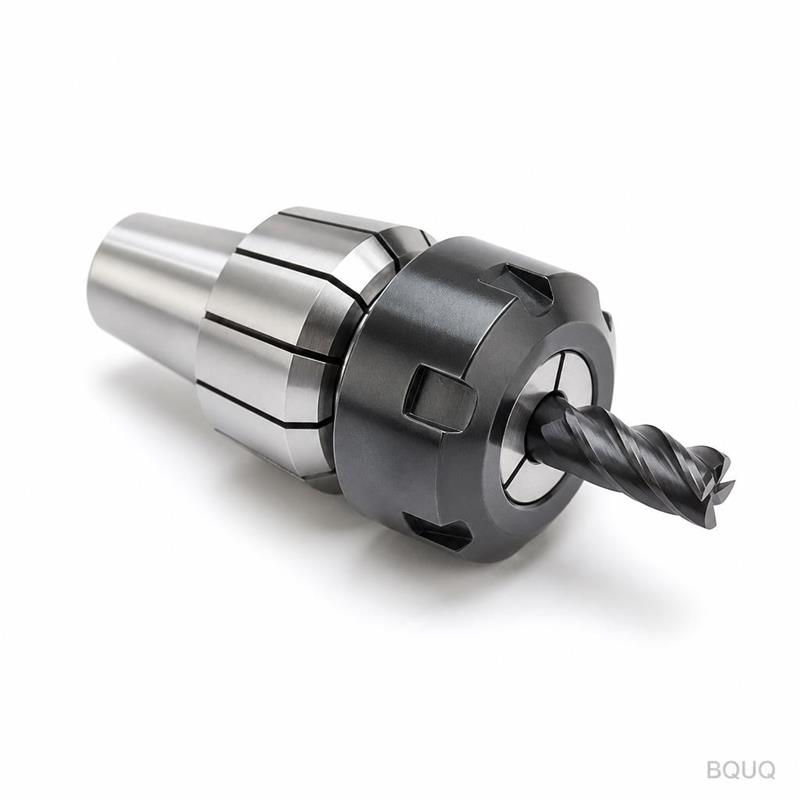
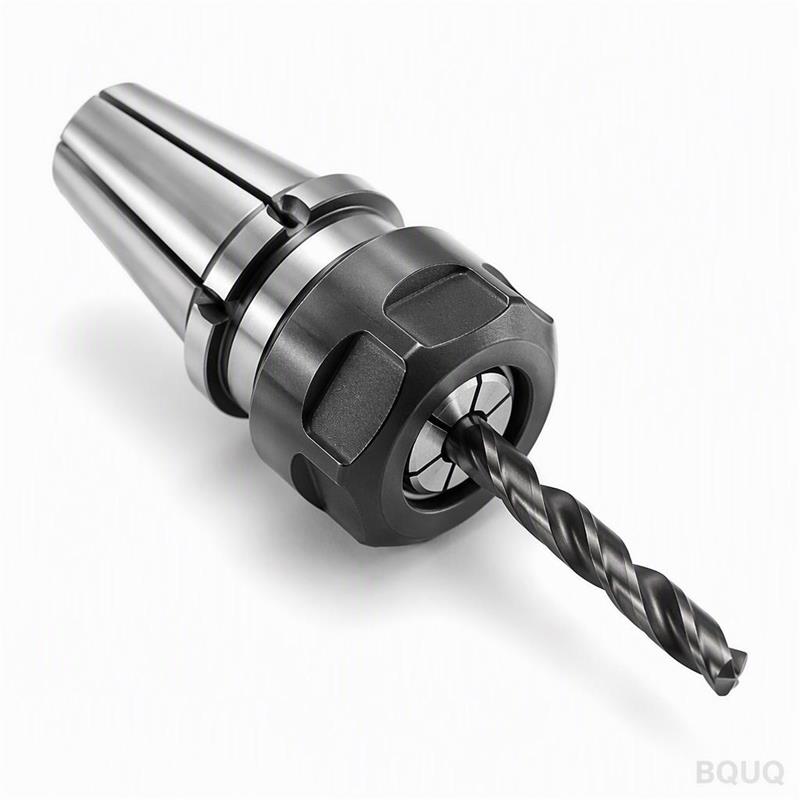
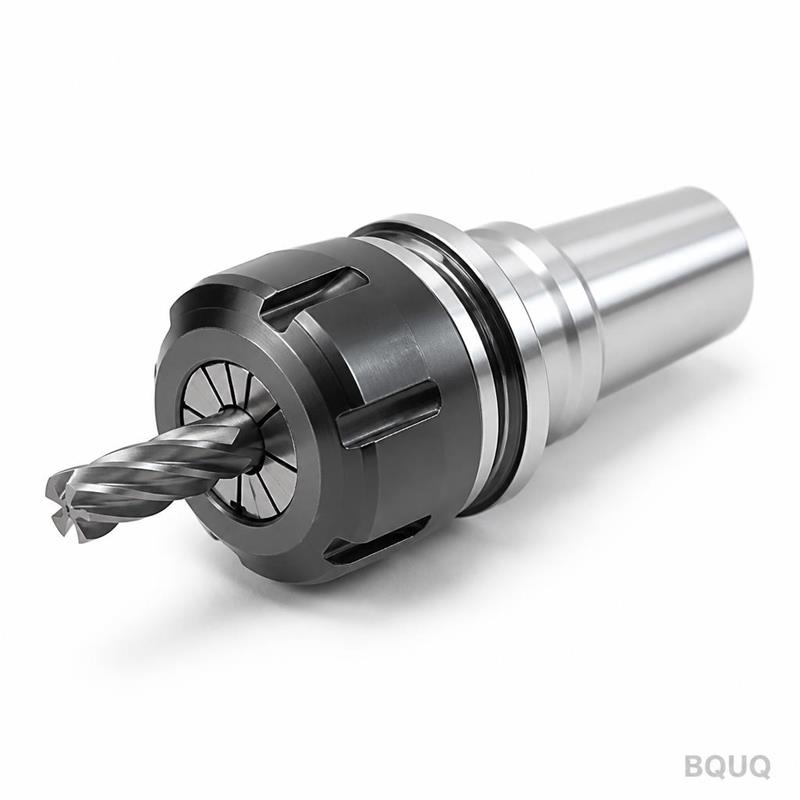
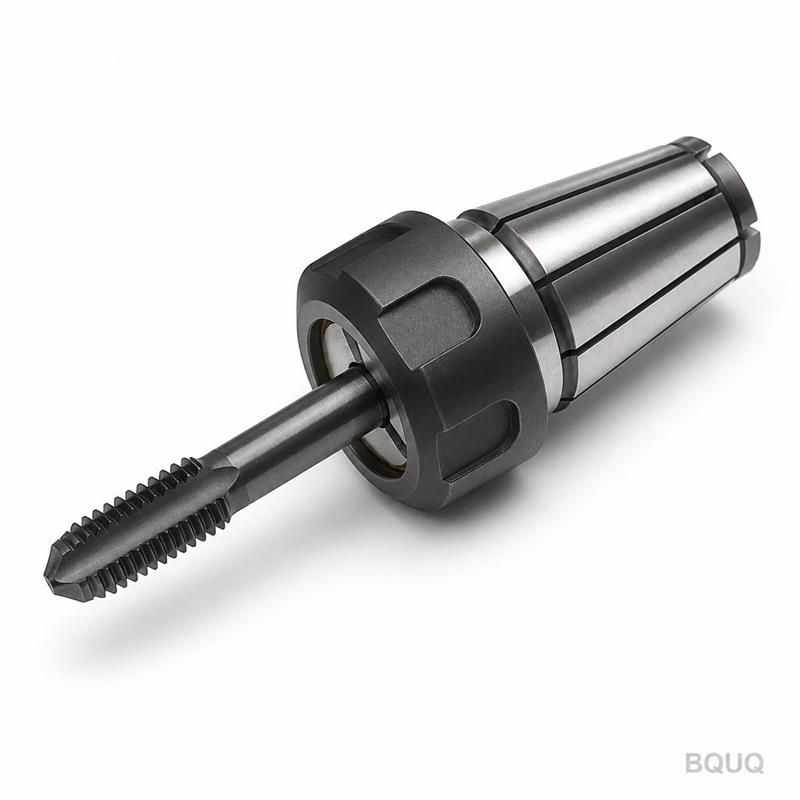
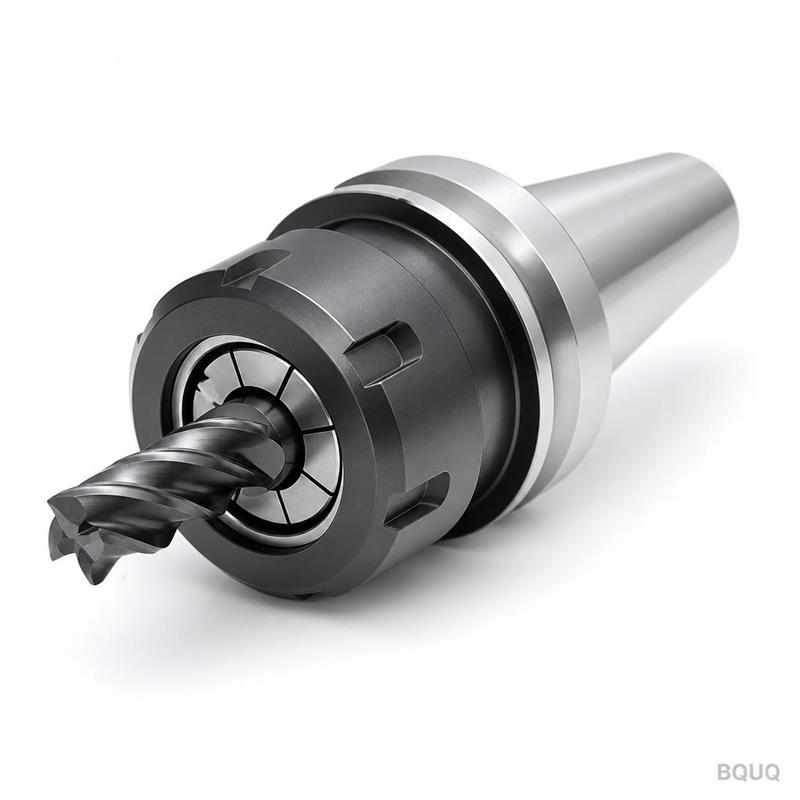
What This ER20 Collet Chuck Does for Your Spindle This is a CNC machined ER20 spring collet chuck built to clamp carbide end mills with a guaranteed runout of 0.005 mm TIR (teste
BQUQ CNC Machined ER20 Spring Collet Chuck With Carbide End Mill Milling
What This ER20 Collet Chuck Does for Your Spindle This is a CNC machined ER20 spring collet chuck built to clamp carbide end mills with a guaranteed runout of 0.005 mm TIR (tested at 3×D from the no
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined ER20 spring collet chuck built to clamp carbide end mills with a guaranteed runout of 0.005 mm TIR (tested at 3×D from the nose). The chuck body is hardened to 58 HRC, ground on the taper and bore, and ships from our Dongguan factory in 15 days. You get repeatable tool clamping for finishing passes, not just roughing.
How the ER20 Taper Locks Tooling Without Flex
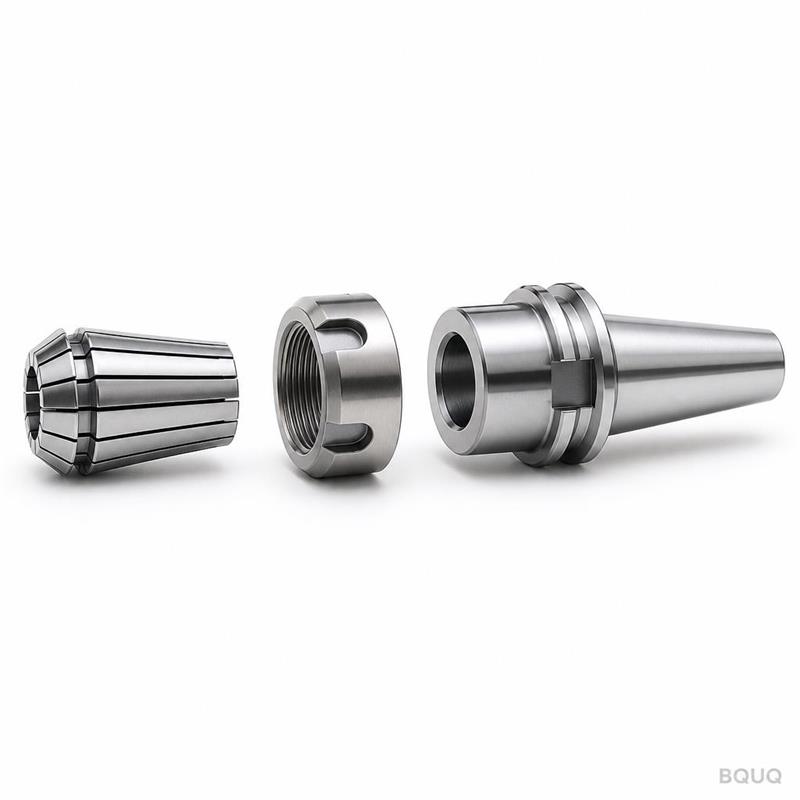
The ER20 collet chuck uses a 8° cone angle. When you tighten the nut, the collet compresses radially, not axially. That radial squeeze grips the carbide end mill shank with even force across the full 20 mm clamping length. No set screws, no side pressure, no tool push-out under heavy chip loads. The result is a rigid connection that keeps tool deflection below 0.01 mm at 12,000 RPM.
Materials and Heat Treatment We Use for the Chuck Body
We machine the chuck body from AISI 4140 alloy steel, not cheap 45# carbon steel. After CNC turning and milling, we through-harden to 58–60 HRC, then temper to relieve stress. The taper is ground on a Junker grinder to a surface finish of Ra 0.4 μm. The collet slot and thread are cut with a wire EDM to avoid burrs that can cause runout drift.
Why We Match This Chuck with Carbide End Mills for Testing
Every ER20 chuck we ship is test-fitted with a 6 mm carbide end mill (two-flute, AlTiN coated) before packaging. We measure runout at the shank and at the cutting edge. If the reading exceeds 0.005 mm, we reject it. This is not a random sample. It is 100% inspection on every unit, and we include the runout report in the box.
Inspection Before Every Shipment – What We Measure
Our QC room runs a Zeiss CMM for taper angle (8° ± 5′), a Marposs gauge for bore ID, and a TIR indicator for runout. We also check thread pitch with a go/no-go gauge. Each chuck gets a laser-etched serial number. You can trace the heat treatment batch and grinding operator from that number. We do not ship parts without this paperwork.
Sizes and Ordering – No MOQ, Mix Your Batch
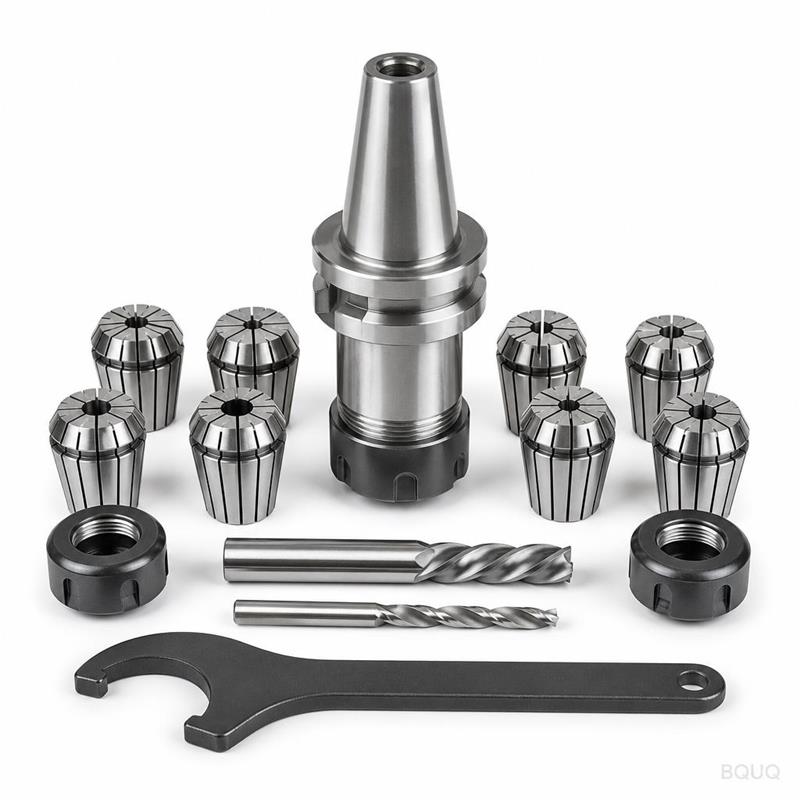
We stock ER20 chucks in shank diameters of 16 mm, 19.05 mm (3/4″), 20 mm, and 25.4 mm (1″). Straight shank, CAT40, BT30, and BT40 are available. You can order one piece for prototype work or 500 pieces for production. There is no minimum order quantity. Mix sizes in one order – the price per unit stays the same.
Specification
Value
Collet type
ER20 (clamping range 1–13 mm)
Shank diameter
16 / 19.05 / 20 / 25.4 mm
Body material
AISI 4140 alloy steel
Hardness
58–60 HRC (through-hardened)
Taper angle
8° ± 5′ (ground)
Surface finish
Ra 0.4 μm on taper, Ra 0.8 μm on bore
Runout (TIR)
0.005 mm at shank, 0.008 mm at 3×D
Max RPM
20,000 RPM (balanced G2.5 option)
Lead time
15 days for standard sizes
MOQ
No minimum – order 1 piece or more
How to Avoid Common Collet Chuck Failures
Most runout problems come from dirty tapers or over-tightening the nut. Clean the chuck bore and collet with solvent before every tool change. Use a torque wrench – ER20 standard is 60–70 Nm, not 100 Nm. If you see wear marks on the collet slots, replace the collet, not the chuck. Our chuck body is designed for 10,000+ clamping cycles if you follow this.
What is the minimum order quantity for this ER20 collet chuck?
No MOQ – you can order a single piece for a prototype run, and the price remains the same as a bulk order.
Can you customize the shank length or balance grade?
Yes, we offer custom shank lengths, through-coolant holes, and G2.5 balancing for high-speed spindles, with a 3-day engineering lead time for drawings.
How do you control quality on a small batch order?
Every chuck, regardless of order size, goes through the same 100% inspection with CMM and TIR gauge, and we email you the inspection report before shipping.
What is the actual lead time if I need 100 pieces?
For 100 standard ER20 chucks (same size), lead time is 12 days from drawing approval; for mixed sizes, it is 15 days.
Why Precision Manufacturing in China Matters for This Part
Our factory in Dongguan has been making CNC tool holders since 2004. We run 30 CNC lathes and 5 grinders in-house, so we control the entire process – turning, hardening, grinding, and inspection. You are not buying from a trader. This is a precision manufacturing operation, made in China, with the same QC discipline as German or Japanese shops but at a lower cost. Before you order, read our CNC cutting tool selection guide to match the chuck to your spindle. And check our CNC machining tolerances guide to understand what 0.005 mm means for your application.
Request a Firm Quote and Get a Drawing Review in 12 Hours
Send us your spindle model, shank size, and collet range. Our engineers will confirm the exact ER20 chuck configuration and email you a firm quote with a technical drawing within 12 hours. We accept prototype orders and production runs. No MOQ, no hidden tooling costs. Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. The Cnc Machined Er20 Spring Collet Chuck With Carbide End Mill Cnc Milling is ready for your spindle.