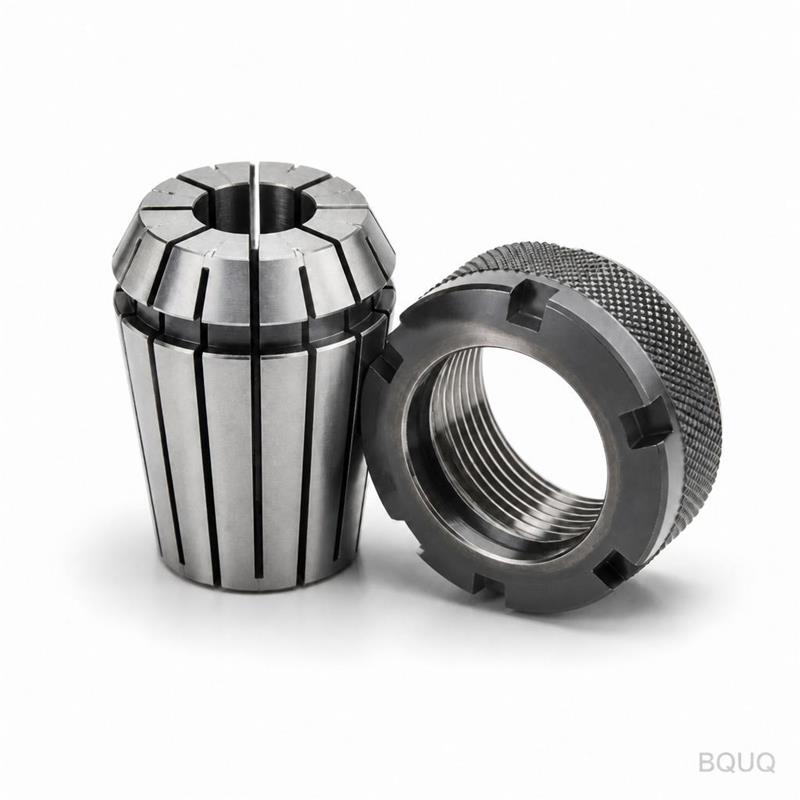
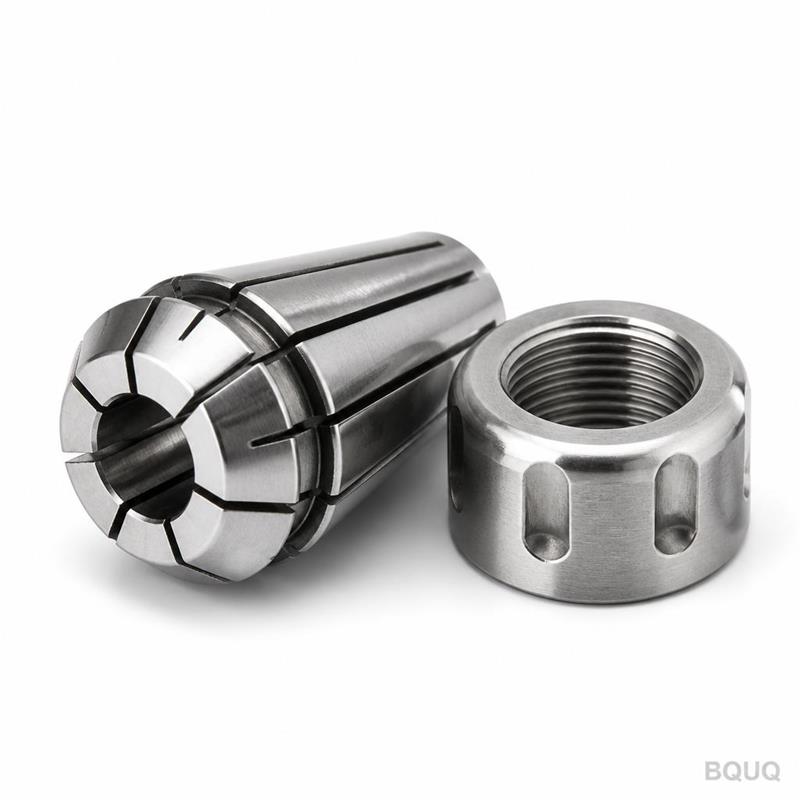
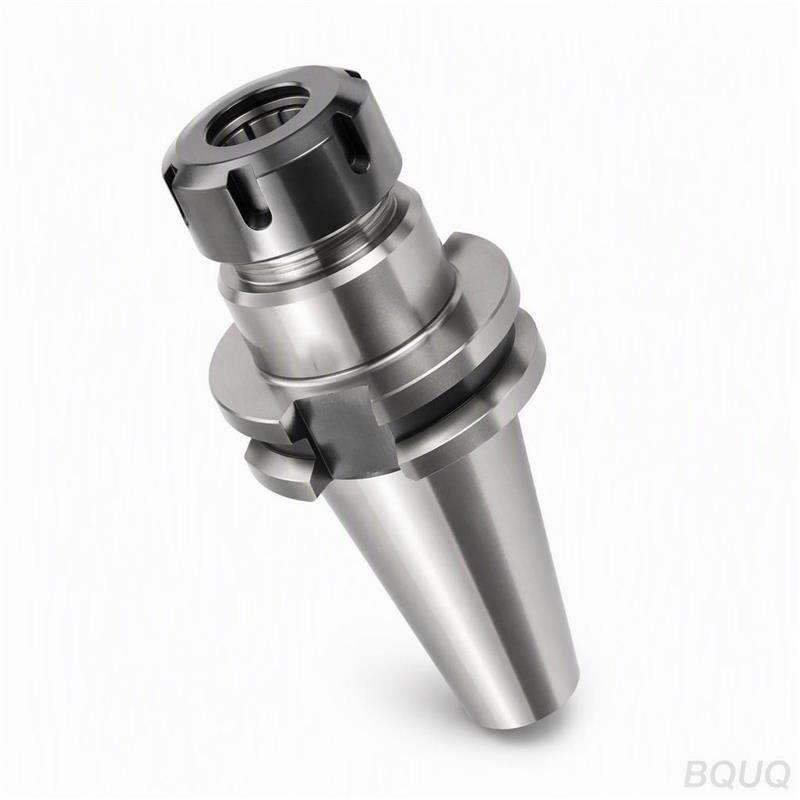
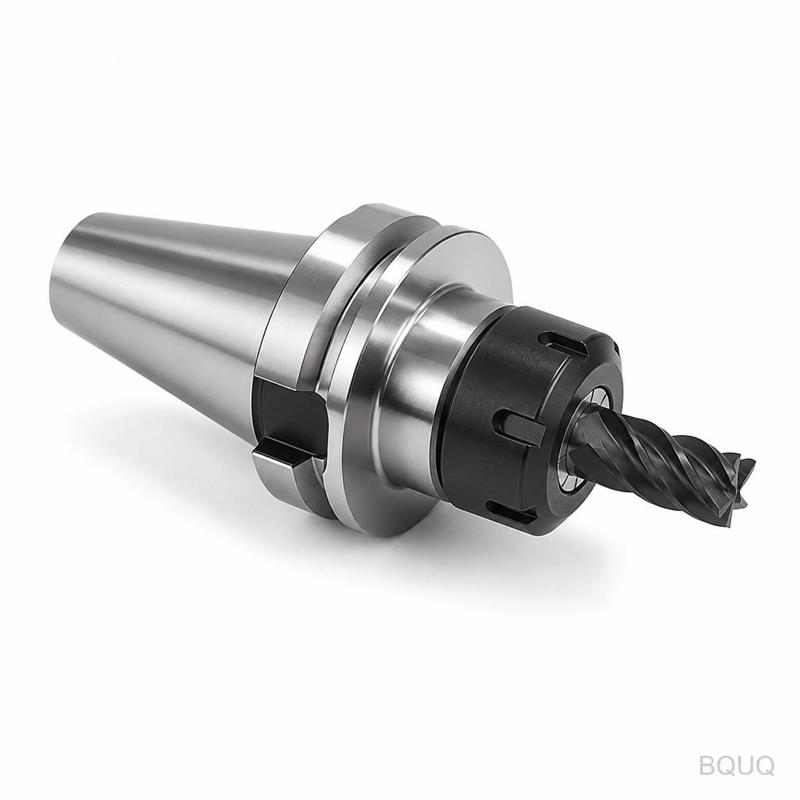
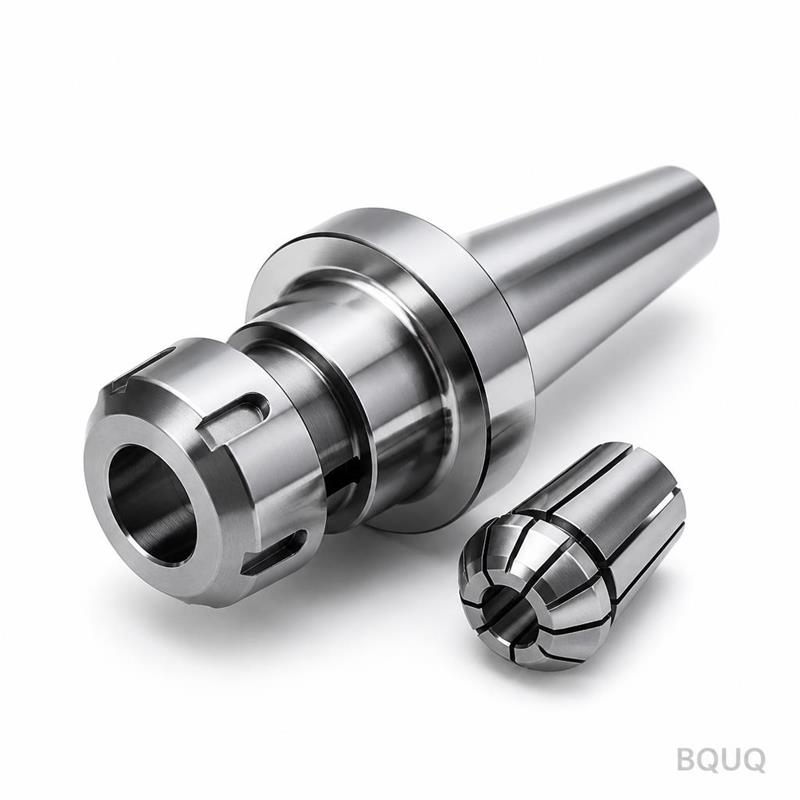
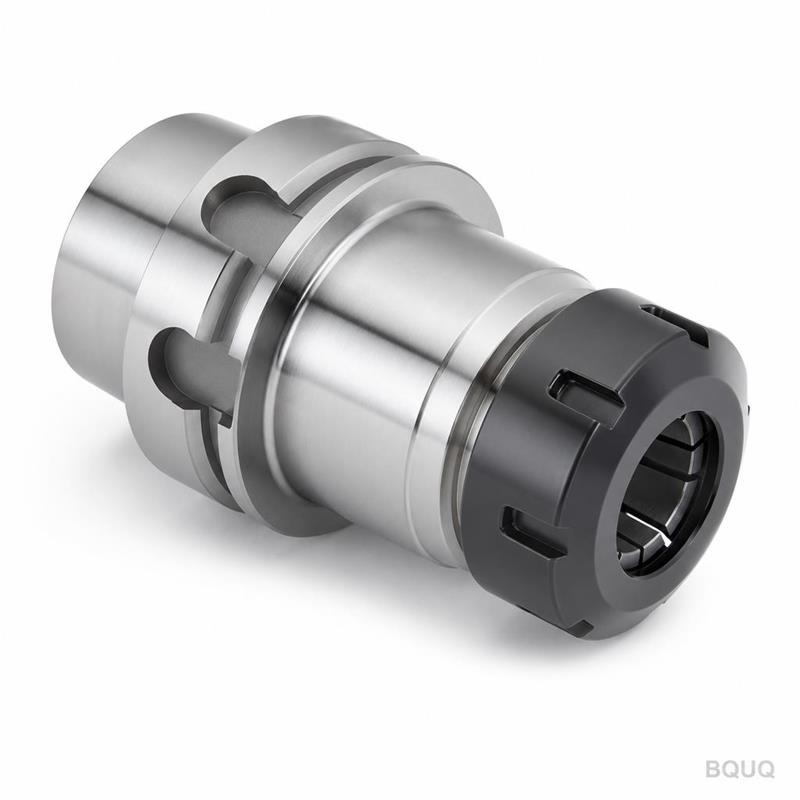
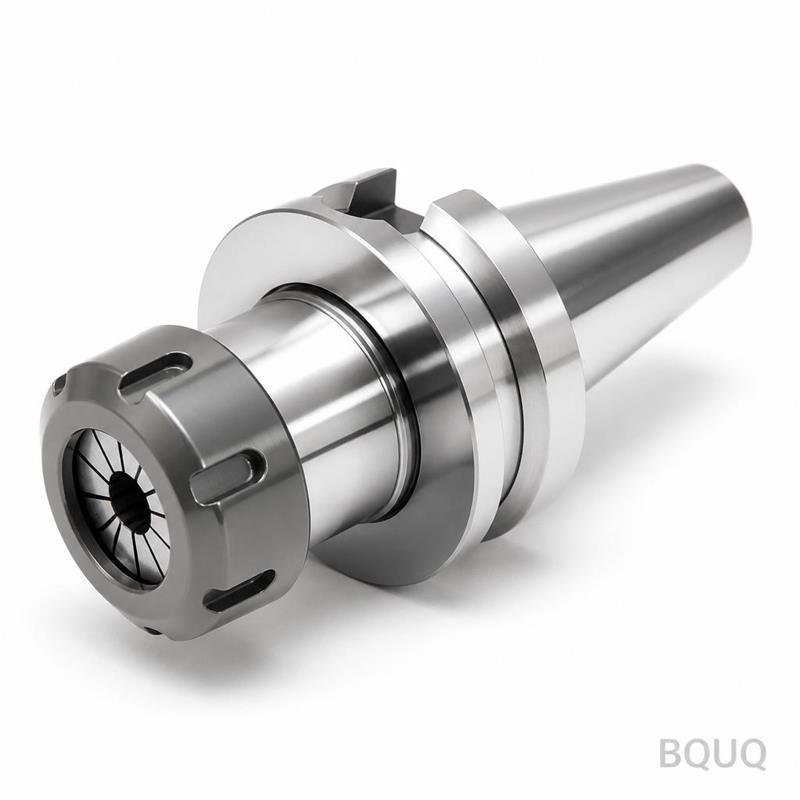
This is a CNC machined ER32 spring collet chuck tool holder, built to grip your cutting tool with a radial runout of 5µm (0.005mm) at the nose. We machine it from 20CrMnTi alloy
This is a CNC machined ER32 spring collet chuck tool holder, built to grip your cutting tool with a radial runout of ≤5µm (0.005mm) at the nose. We machine it from 20CrMnTi alloy steel, carburized to
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined ER32 spring collet chuck tool holder, built to grip your cutting tool with a radial runout of ≤5µm (0.005mm) at the nose. We machine it from 20CrMnTi alloy steel, carburized to a surface hardness of HRC 58-60, and we ship standard sizes in 24 hours. If you need a tool holder that holds a 1/8" end mill dead true at 12,000 RPM without chatter, this is the part you spec.
How the ER32 Spring Collet Mechanism Eliminates Tool Slip
The ER32 collet chuck uses a tapered bore (8° included angle) and a threaded locknut. When you tighten the nut, the collet’s 12 slots compress radially, gripping the tool shank along its full 32mm length. This is not a set-screw holder—it distributes clamping force evenly, which means zero tool pull-out under heavy roughing. The spring steel collet (65Mn) flexes up to 1mm in diameter range, so one chuck covers 2mm to 20mm tool shanks. We grind the taper seat to a gauge accuracy of AT3, which is why the runout stays under 5µm even after 10,000 insertion cycles.
Materials and Heat Treatment: 20CrMnTi Carburized to HRC 58-60
We start with 20CrMnTi billet, not cheap 45# steel. The body is CNC turned and milled, then carburized at 920°C for 6 hours. This gives a case depth of 0.8-1.2mm, so the taper surface resists wear from collet friction. The core stays tough at HRC 30-35, which absorbs vibration. The locknut is 40Cr, quenched and tempered to HRC 38-42. We do not hard chrome plate—we grind the taper directly to a surface finish of Ra 0.4µm. That mirror finish reduces friction when you release the tool after a hot run.
Precision Grinding: How We Achieve 5µm Total Runout
The critical step is the final cylindrical grind between centers. We grind the taper bore first, then mount the chuck on a precision arbor (runout <1µm) and grind the OD shank (DIN 69871 or BT30/BT40 taper) concentric to that bore. We measure every unit on a CMM with a 0.5µm resolution probe. The total indicated runout (TIR) at 50mm from the nose is ≤5µm. For comparison, a standard DIN 6499 holder is 10-15µm. You will feel the difference in your surface finish on a 0.2mm finishing pass.
ER32 Collet Chuck Specs That Matter for Your Machine Spindle
Parameter
Value
Collet type
ER32 (DIN 6499)
Clamping range
2mm – 20mm (0.079" – 0.787")
Body material
20CrMnTi alloy steel
Surface hardness
HRC 58-60 (carburized case depth 0.8-1.2mm)
Core hardness
HRC 30-35
Taper accuracy
AT3 (DIN 6499)
Total runout (TIR at 50mm)
≤5µm (0.005mm)
Surface finish on taper
Ra 0.4µm
Shank options
BT30, BT40, CAT40, HSK63A, straight shank 32mm
Lead time (standard sizes)
24 hours
MOQ
No MOQ, single piece accepted
Balancing and Dynamic Performance at 12,000 RPM
We balance each ER32 chuck to G2.5 at 12,000 RPM. This is not optional—an unbalanced holder at that speed creates a 0.5mm vibration amplitude that ruins your insert life. We drill two balance correction holes in the flange, then re-measure. The result is a holder that runs smooth enough for high-speed aluminum finishing. If you run 20,000 RPM, tell us and we will balance to G1.0 at no extra charge.
Inspection Before Every Shipment: CMM Report Included
Every single ER32 spring collet chuck goes through a 12-point inspection. We check taper contact ratio (must be >85% with blueing), thread runout on the locknut, surface hardness with a Rockwell tester, and final TIR on the CMM. You get a printed inspection report with the part number and date. If the taper contact is off by 2%, we scrap the part—we do not sell seconds. This is precision manufacturing, made in China, but to German DIN standards.
FAQ: Sizing, Custom Shanks, and Ordering a Single Unit
What is the minimum order quantity (MOQ)?
No MOQ—we ship one piece, just like we ship a thousand, with the same 24-hour lead time for standard BT30/BT40/CAT40 options.
Can I get a custom shank or special taper length?
Yes, we machine custom shanks (e.g., HSK63A, R8, or a 25mm straight shank) in 3-5 days, and we provide a 3D drawing for your approval before cutting.
How do you guarantee the 5µm runout on every unit?
We inspect 100% of units on a CMM, and we ship the individual runout report with your order—if it reads above 5µm, we replace it at our cost.
What is the actual lead time for a bulk order of 100 pieces?
Standard ER32 chucks ship in 24 hours; for bulk orders of 100+ pieces, we hold 2 weeks of finished stock, so lead time is still 48 hours.
Why You Should Not Buy a Cast or Milled Chunk from a Trading Company
We are the factory. We own the CNC lathes (10 units, Fanuc controls), the grinding machines, and the CMM. You are talking to the engineer who sets the tolerances, not a salesperson reading a datasheet. This ER32 chuck is machined from solid, not cast, so there are no hidden porosity voids under the taper. Our price per unit is 15-20% lower than a German brand because you cut out the importer margin—but the runout is the same or better.
Pair This Chuck with the Right Tooling and Tolerances
To get the most from this 5µm holder, pair it with a balanced collet (we also supply ER32 collets, 65Mn spring steel, runout ≤3µm). If you are selecting carbide end mills or drills, read our CNC cutting tool selection guide to match shank tolerances. And for the overall part accuracy you can expect, check our CNC machining tolerances guide—it explains how holder runout stacks up against your part GD&T.
Get a Firm Quote in 12 Hours—No MOQ, No Runaround
Send us your drawing or just tell us your spindle taper and tool shank diameter. We will reply with a firm price, a lead time, and a technical recommendation on whether ER32 is the right grip force for your operation. Email sc@bquq.com or WhatsApp +86 13713157787. We are in Dongguan, UTC+8, and we answer within 12 working hours. Your first article is free, and we do not charge for a sample report.