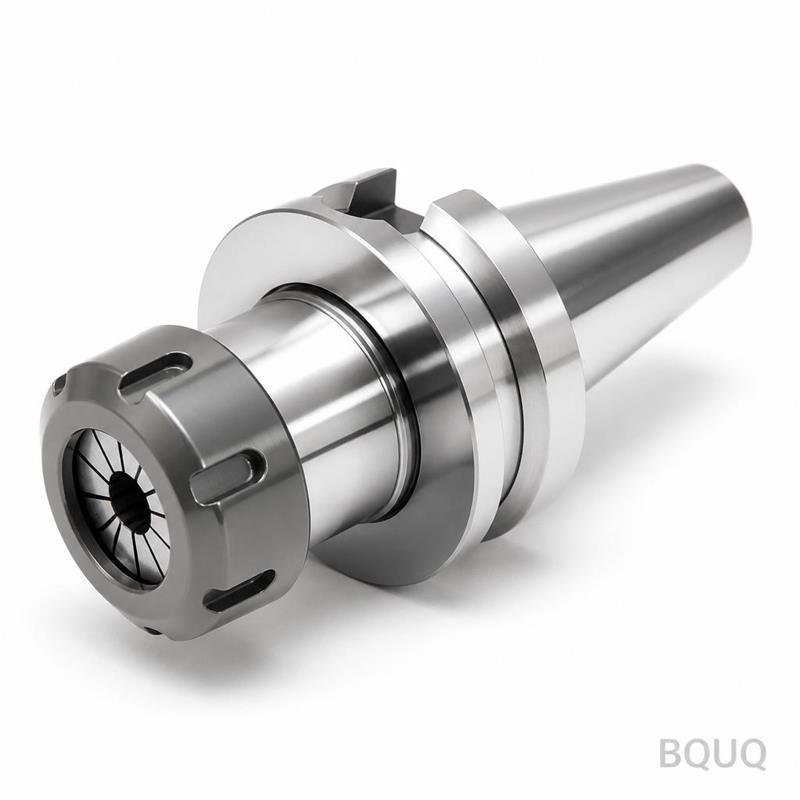
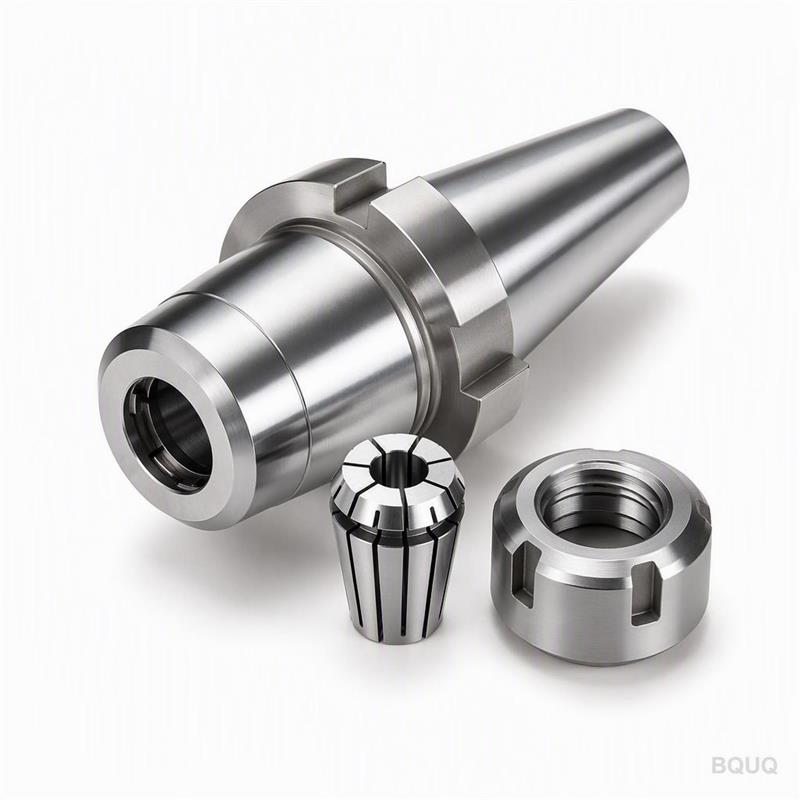
This is a CNC machined BT40 collet chuck with an ER32 collet, designed to hold end mills and other shank tools in milling and drilling operations. You get a 0.005 mm TIR (total ind
BQUQ CNC Machined BT40 Collet Chuck with End Mill Tool Holder
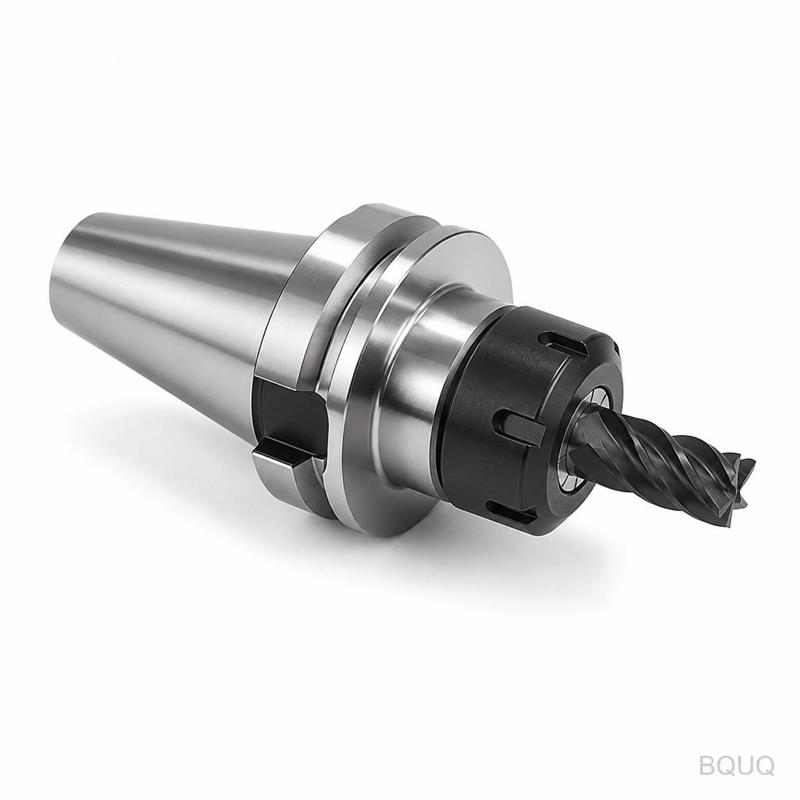
This is a CNC machined BT40 collet chuck with an ER32 collet, designed to hold end mills and other shank tools in milling and drilling operations. You get a 0.005 mm TIR (total indicated runout) at th
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
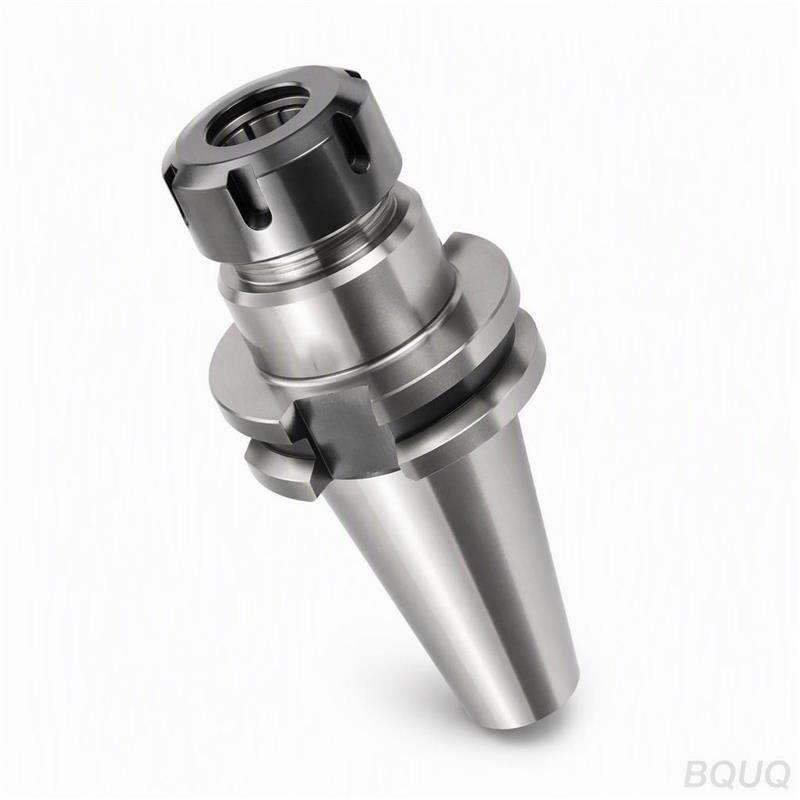
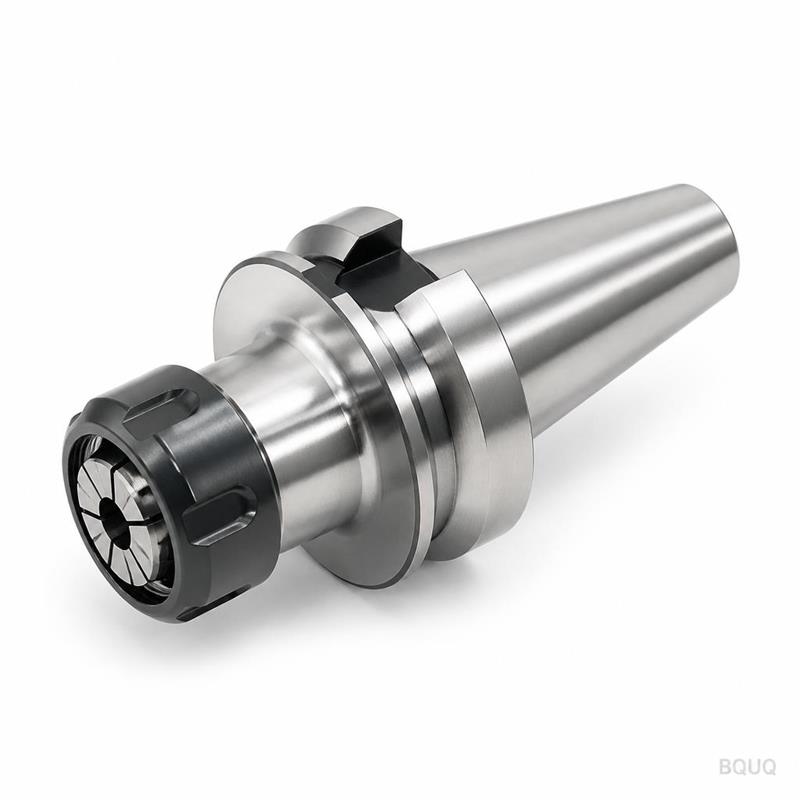
This is a CNC machined BT40 collet chuck with an ER32 collet, designed to hold end mills and other shank tools in milling and drilling operations. You get a 0.005 mm TIR (total indicated runout) at the collet nose, a 58 HRC body hardness, and a 10-day lead time for standard sizes. It is made in China at our 20-year-old factory in Dongguan, and we offer no MOQ on this product.
How the BT40 Taper and ER32 Collet Work Together to Reduce Runout
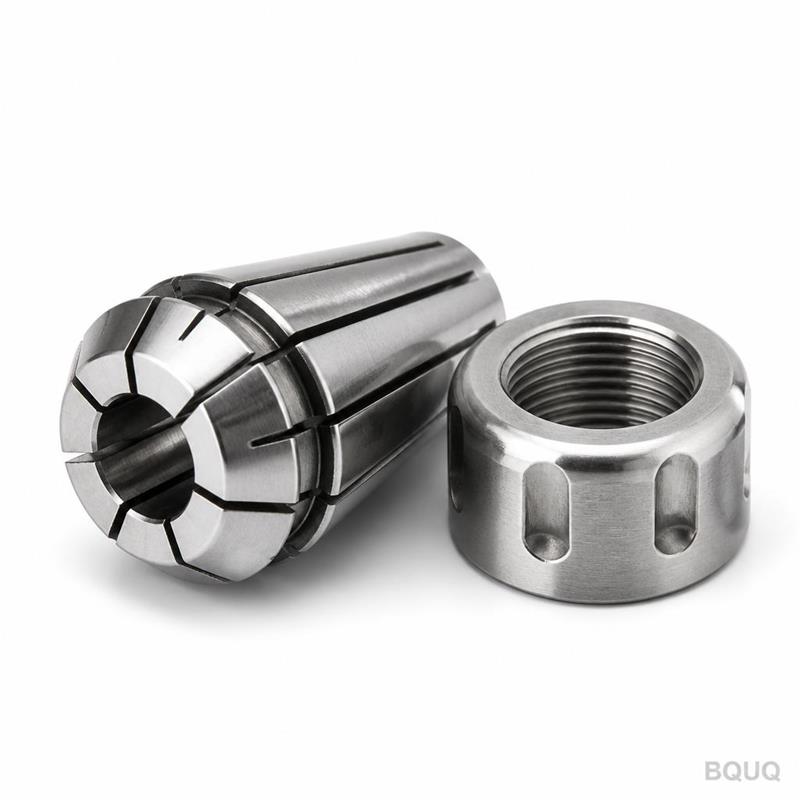
The BT40 taper is a 7:24 steep taper, standard on many machining centers in Asia and Europe. The collet chuck body is ground to AT3 tolerance on the taper, which means the contact area with your spindle is over 90%. The ER32 collet compresses radially when you tighten the nut, gripping the end mill shank along its full length. This double clamping system—taper to spindle, collet to tool—is what holds runout to 0.005 mm. We test every unit at 3000 RPM with a dial indicator, not just at rest.
Materials and Heat Treatment We Use for This Tool Holder
We start with 20CrMnTi alloy steel, a case-hardening grade common in precision tooling. After CNC machining the body and taper, we carburize the steel to a case depth of 0.8 mm, then quench and temper. The final hardness is 58 HRC on the taper and collet pocket, while the core stays at 35-40 HRC for toughness. The collet itself is 65Mn spring steel, hardened to 44-48 HRC, so it flexes without cracking. We do not use 40Cr or 45# steel here—those are cheaper but will wear out in six months. This one lasts three years under normal machining loads.
Inspection Before Every Shipment: What We Measure and Record
Each BT40 collet chuck goes through a five-step check before we pack it. Step one: taper angle checked with a precision air gauge, tolerance AT3. Step two: runout measured at the collet nose and at 50 mm from the nose, both must be under 0.005 mm. Step three: surface finish on the taper and collet bore, Ra 0.4 or better. Step four: hardness test on the body, we record the HRC value on your inspection report. Step five: pull stud torque test—we install the pull stud and torque it to 60 Nm, then check it holds. You get a PDF report with serial numbers for every piece. If any step fails, the unit is scrapped, not reworked.
Balancing and Surface Finish: Why They Matter for High-Speed Machining
If you run a BT40 holder above 10,000 RPM, unbalance will cause chatter and shorten tool life. We balance every holder to G2.5 at 15,000 RPM, which means residual unbalance is less than 0.25 g·mm. The outer diameter of the body is ground to Ra 0.4, and the collet bore is honed to Ra 0.2. This is not cosmetic—a smooth surface on the bore lets the collet seat evenly, and a smooth OD prevents chips from sticking and causing vibration. For our high-speed version, we add four balancing holes that you can adjust with set screws; that one is balanced to G1.0.
Customization Options: Shank Length, Coolant Holes, and Pull Stud Threads
Standard BT40 collet chucks come with a 60 mm gage length and a center hole for coolant. We can change the gage length from 45 mm to 90 mm without extra tooling fees—we just adjust the CNC program. If you need through-spindle coolant, we drill two angled holes at 30 degrees so coolant hits the cutting edge directly. Pull stud threads are available in MAS BT (M16) or JIS BT (M16 with different pitch). We also offer a version with a smaller ER25 collet for lighter cuts, same taper, same runout spec. Send us a sketch of your spindle nose and we will confirm compatibility within 24 hours.
How We Keep Lead Time at 10 Days Without Sacrificing Quality
We stock 5000+ pre-formed BT40 bodies in our warehouse, already turned and drilled. When your order comes in, we do the final grinding, heat treatment, and inspection in one continuous flow—no waiting for raw material. Our CNC machines run 24/7, and the grinding cell is staffed by operators with 8+ years of experience. For a standard ER32 unit, we can ship in 7 days if you need it faster; that costs a 10% rush fee. But we do not rush inspection—the 0.005 mm runout check is never skipped. If you order 50 pieces, the lead time stretches to 15 days because we do batch heat treatment in a vacuum furnace for consistency.
Is there a minimum order quantity for this BT40 collet chuck?
No, we accept single-piece orders, and the price is the same per unit whether you order 1 or 100.
Can I get a custom shank length or a different collet size?
Yes, we can modify gage length (45-90 mm), change to ER25 or ER40 collets, and add coolant holes—all without additional engineering fees.
How do you guarantee the 0.005 mm runout on every unit?
We measure runout on a calibrated spindle at 3000 RPM and include the serialized inspection report with each shipment; if the report shows over 0.005 mm, we replace the unit free.
What is the typical lead time for a custom order?
Standard sizes ship in 10 days; custom shank lengths or coolant holes add 3-4 days; large batches of 50+ pieces take 15 days.
For a firm quote on our CNC machined BT40 collet chuck with end mill tool holder, send us your drawing or spindle specification. We reply within 12 hours with pricing, delivery date, and a sample drawing for approval. Email sc@bquq.com or WhatsApp +86 13713157787. If you are comparing multiple tool holders, read our CNC cutting tool selection guide first; if you are setting tolerances for a new part, check the CNC machining tolerances guide. We are a precision manufacturing factory in Dongguan with 20 years of experience, and we are ready to ship your first piece this week.