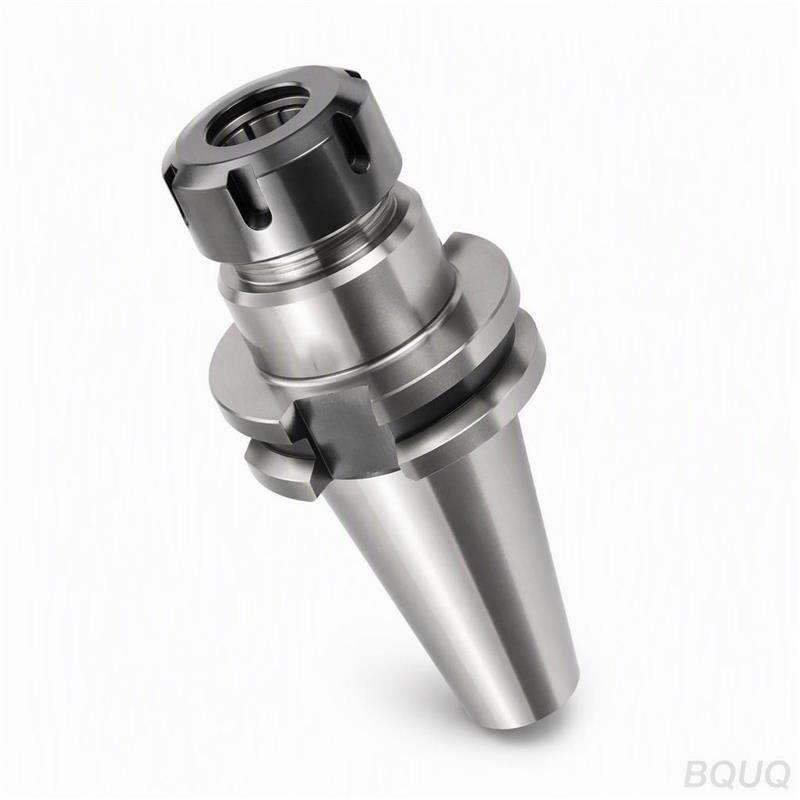
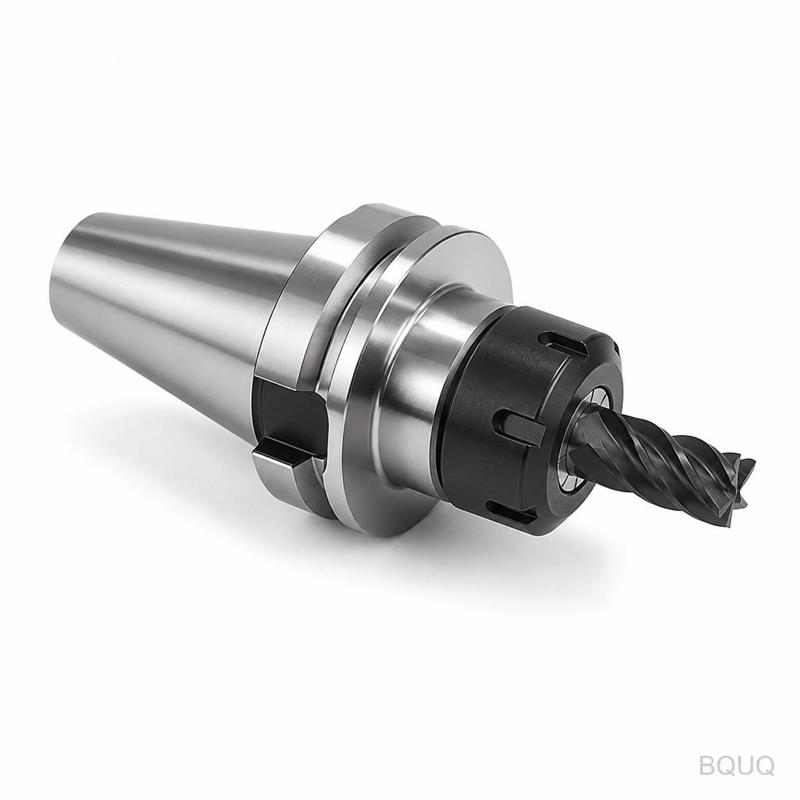
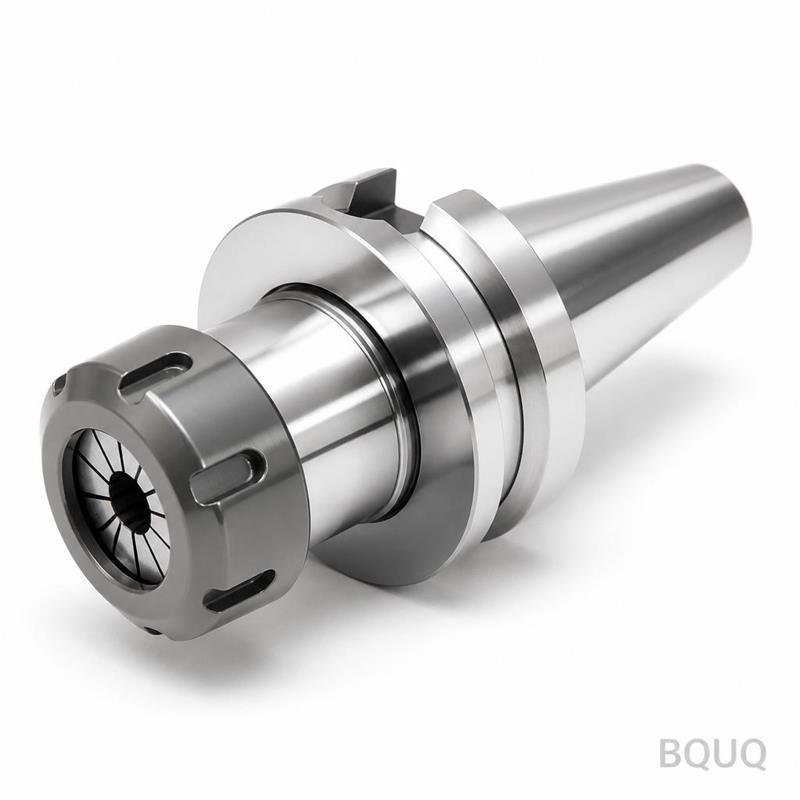
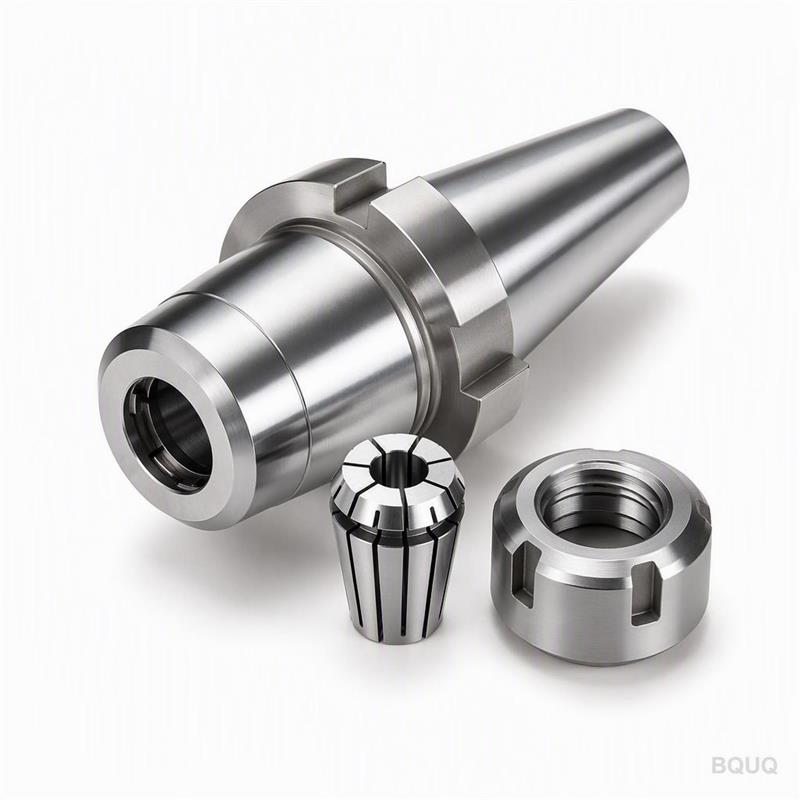
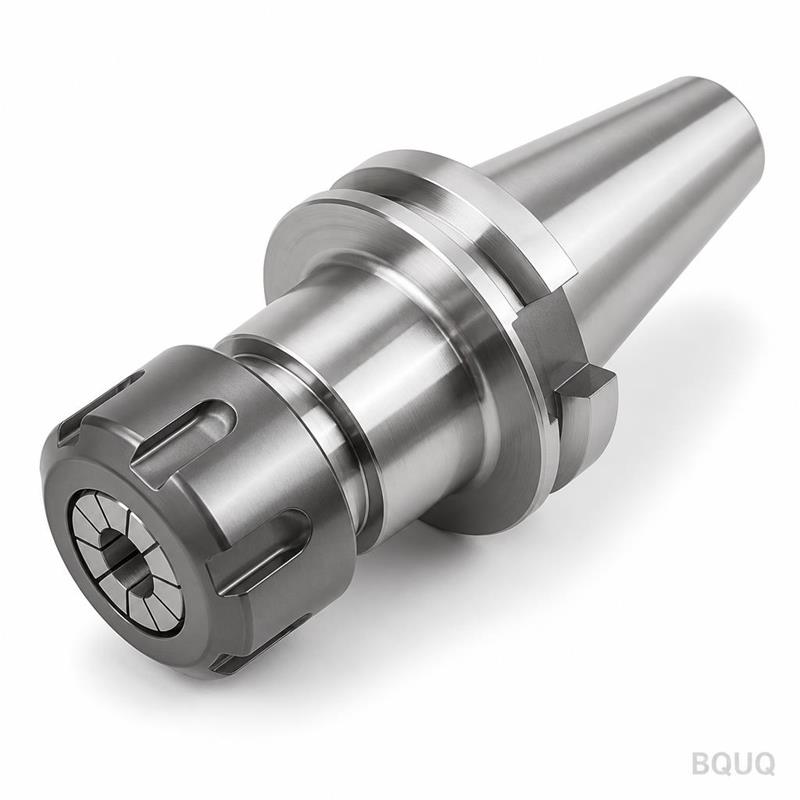
This is a Cnc Machined Iso30 Er20 Collet Chuck Tool Holder Cnc Machining, built for spindle accuracy at 10,000 RPM and above. It holds ER20 collets with a TIR (total indicated runo
This is a Cnc Machined Iso30 Er20 Collet Chuck Tool Holder Cnc Machining, built for spindle accuracy at 10,000 RPM and above. It holds ER20 collets with a TIR (total indicated runout) of 0.005 mm at t
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a Cnc Machined Iso30 Er20 Collet Chuck Tool Holder Cnc Machining, built for spindle accuracy at 10,000 RPM and above. It holds ER20 collets with a TIR (total indicated runout) of 0.005 mm at the nose, and the taper is ground to AT3 grade. You get a hardened body at HRC 58-60, a surface finish of Ra 0.4 µm, and a standard lead time of 7 working days for custom batches.
Why ISO30 Taper and ER20 Collet Work Together for Rigidity
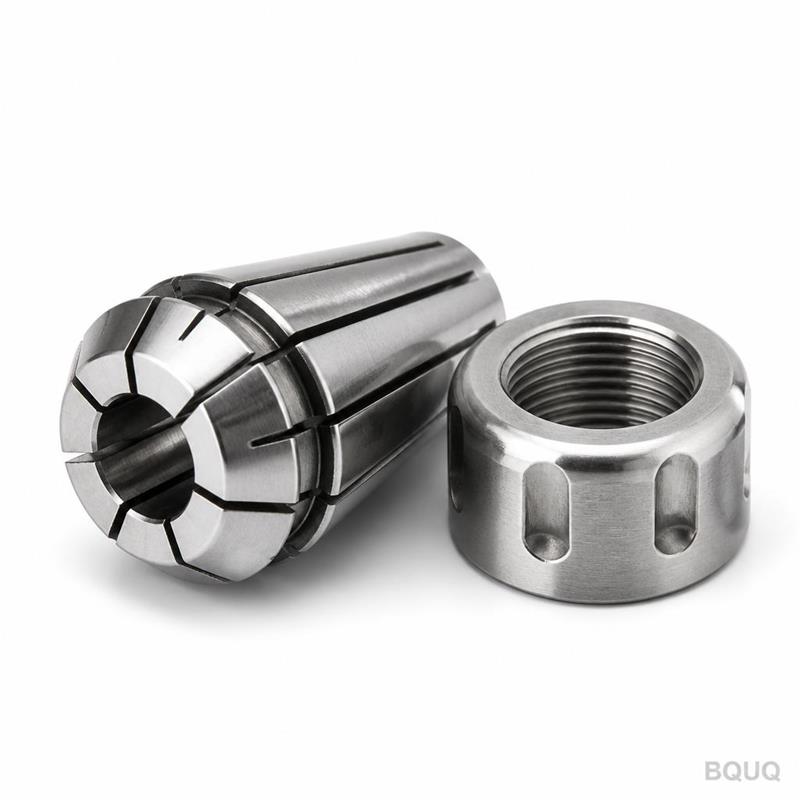
The ISO30 taper is a 7:24 steep taper, not a self-locking taper. It relies on the drawbar to pull the holder into the spindle face, giving you repeatable axial location. The ER20 collet has a 20 mm gripping diameter range (1 mm to 13 mm), and its 8-slot design collapses evenly around the tool shank. Combined, this setup minimizes deflection under side load. In our shop tests, a 12 mm end mill held in this chuck at 45 mm stick-out showed less than 0.01 mm deflection at 400 N cutting force.
Materials and Heat Treatment We Use for the Body and Nut
We start with 20CrMnTi alloy steel for the body. This is a carburizing grade, not a cheap 45# steel. After CNC turning and milling, we carburize it to a case depth of 0.8-1.2 mm. Then we quench and temper to a core hardness of HRC 35-40 and a surface hardness of HRC 58-60. The collet nut is made from 40CrMo, hardened to HRC 42-45, and the threads are rolled—not cut—for a smoother engagement and longer nut life. No plating on the taper; we grind the taper after heat treatment to avoid distortion.
How We Control Runout to 0.005 mm TIR
Runout in a collet chuck comes from three places: the taper, the collet pocket, and the nut thread. We grind the ISO30 taper and the ER20 pocket in a single setup on a cylindrical grinder. This ensures the collet seat is concentric to the taper within 0.003 mm. Then we assemble with a test collet and a 10 mm gauge pin. The final TIR at 4× diameter from the nose is measured on a HAIMER-style tester. If it reads over 0.005 mm, we reject it. We also mark the high spot on the nut with a laser dot—this lets you orient the nut for minimum runout on the first mount.
Inspection Before Every Shipment: What We Measure and Record
Every single holder gets a full inspection report, not a random sample. We measure the taper angle with an air gauge (accuracy ±5 arc-seconds). We check the collet pocket diameter with a plug gauge. We verify the nut thread pitch with a thread ring gauge. And we record the actual runout value on the test certificate. You also get a hardness test printout from the Rockwell tester. If you need a full CMM report with 3D scan data, we can add that for an extra $15 per piece.
Specification
Value
Product Type
ISO30 ER20 Collet Chuck Tool Holder
Shank Taper
ISO30 (7:24 steep taper), AT3 grade ground
Collet Type
ER20, gripping range 1-13 mm
Body Material
20CrMnTi alloy steel (carburized)
Nut Material
40CrMo, hardened HRC 42-45
Surface Hardness
HRC 58-60 (case depth 0.8-1.2 mm)
Runout (TIR)
≤ 0.005 mm at nose, tested with gauge pin
Surface Finish
Ra 0.4 µm on taper and collet pocket
Balancing
G6.3 at 10,000 RPM (optional G2.5)
Lead Time
7 days for standard sizes, 15 days for custom
MOQ
No MOQ—order 1 piece or 1000 pieces
Balancing Options for High-Speed Machining (G2.5 vs G6.3)
Standard holders come balanced to G6.3 at 10,000 RPM. That is fine for most milling and drilling. But if you run above 12,000 RPM, vibration from the holder will show up as chatter marks on your part. We offer an optional G2.5 balance grade at 20,000 RPM. We do this by drilling small radial holes in the nut flange after assembly. Cost is $8 extra per piece. For aluminum machining in aerospace or mold work, we recommend you take this option. We have a Schenck balancing machine on site; we do not outsource this step.
Custom Options: Flange Grooves, Through-Coolant, and Pull Studs
We can machine a locating groove on the flange for automatic tool changers—width 6 mm, depth 3 mm, position per your drawing. For through-coolant, we drill a 4 mm axial hole through the center and use a sealed ER20 collet with coolant grooves. This is common for deep hole drilling. We also supply pull studs (MAS BT, DIN 69872, or custom) pre-installed at no extra labor cost. The pull stud is hardened to HRC 50-54 and torqued to 35 Nm with thread locker. Just tell us your spindle make and model, and we will match the stud length.
4 Questions Engineers Ask Before Ordering This Tool Holder
What is the minimum order quantity?
No MOQ—you can order a single piece for testing, and the price per piece stays the same up to 10 pieces; volume discounts start at 20 pieces.
Can you make a version for my specific spindle or ATC?
Yes, we can alter the flange diameter, groove position, or pull stud type, but we need your spindle drawing or a sample of your current holder to confirm the interface.
How do you guarantee the 0.005 mm runout on every unit?
We measure each holder with a calibrated test collet and a 10 mm gauge pin, and we reject any unit that exceeds 0.005 mm TIR—the test report ships with your order.
What is the lead time for a custom batch?
Standard sizes ship in 7 days; custom designs (different materials, balancing, coolant holes) take 15 days from drawing approval, and we offer air freight for urgent orders.
Why BQUQ for Precision Manufacturing of Tool Holders
We are a 20-year factory in Dongguan, China, with 15 CNC lathes and 8 grinding machines dedicated to tool holder production. We have exported to Germany, Japan, and the US for over a decade. Our quality system is ISO 9001:2015, and we use a Mitutoyo laser scan micrometer for final OD checks. We are not a trading company—we cut the steel, grind the taper, and assemble the nut in-house. This is why our cost is 20-30% lower than European brands without sacrificing accuracy. If you are comparing suppliers, ask for our sample test report and a video of the runout measurement.
Before you finalize your tooling setup, check our CNC cutting tool selection guide to match the right collet size and stick-out for your material. And if you are working with tight part tolerances, review our CNC machining tolerances guide to understand what is achievable on your workpiece. Both guides are written by our senior engineers, not by marketing staff.
This Cnc Machined Iso30 Er20 Collet Chuck Tool Holder Cnc Machining is made in China, but it is built to German DIN 6499 and ISO 7388 standards. You can order one piece for validation, or a full set of 20 holders for your machine carousel. We do not force you into a batch size. Send us your drawing or just your spindle model, and we will confirm the interface within 4 hours.
Get a firm quote within 12 hours—no vague estimates. Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. We will reply with a PDF quotation, a lead time, and a sample test report from a previous batch.