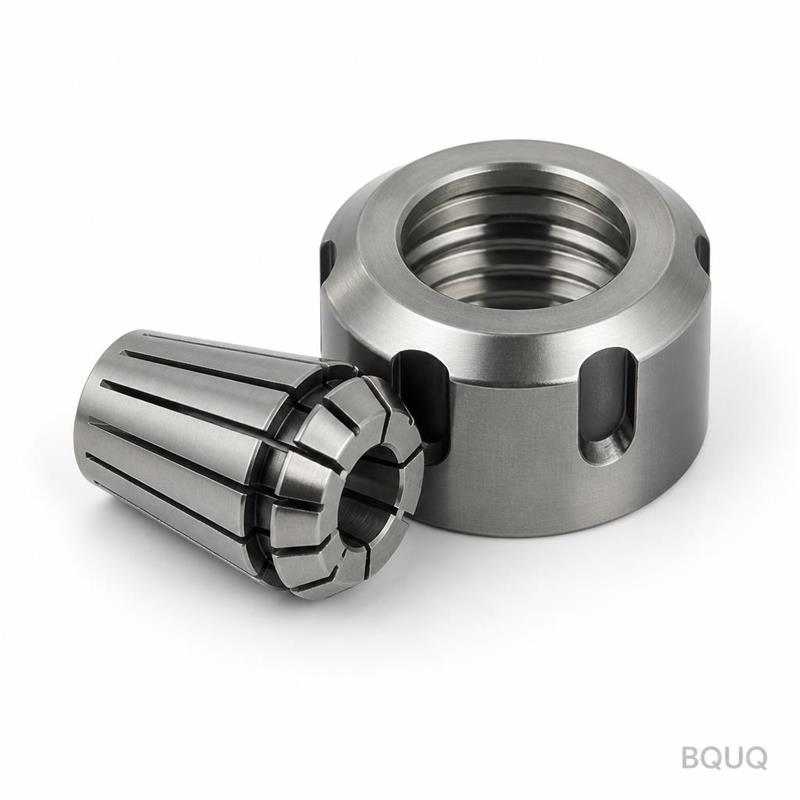
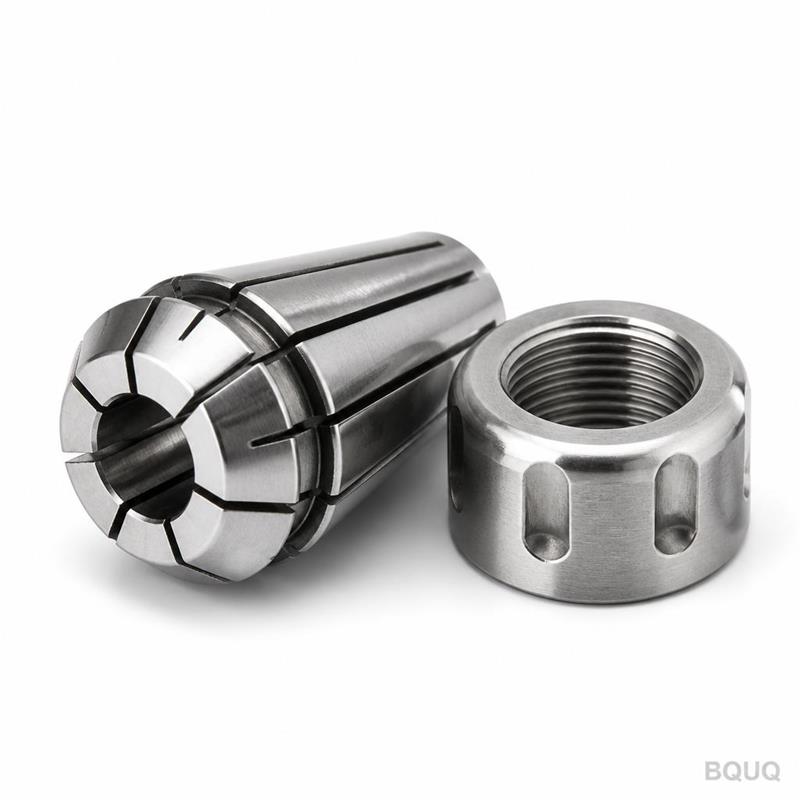
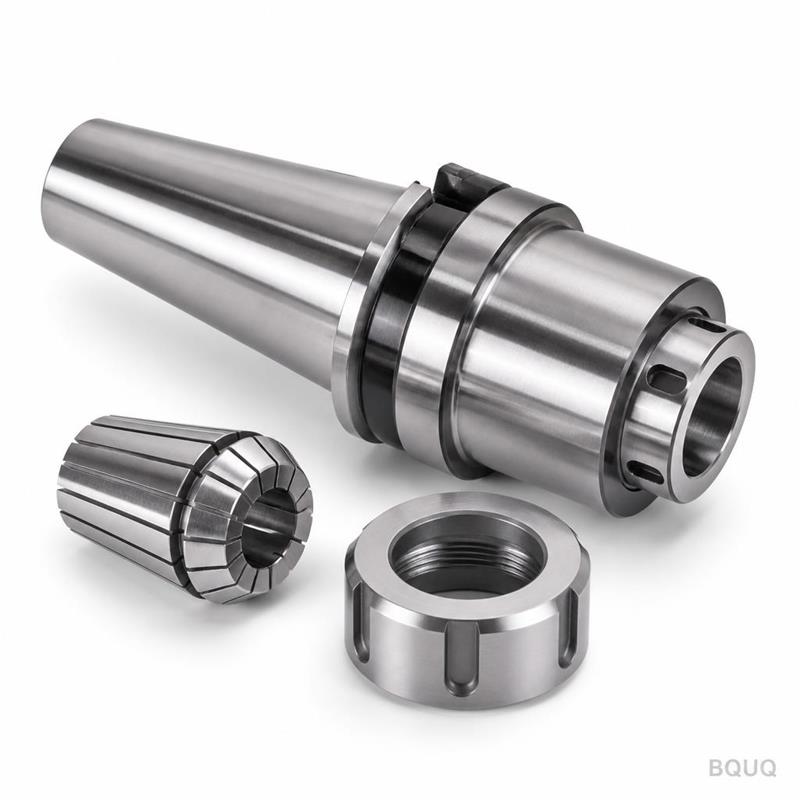
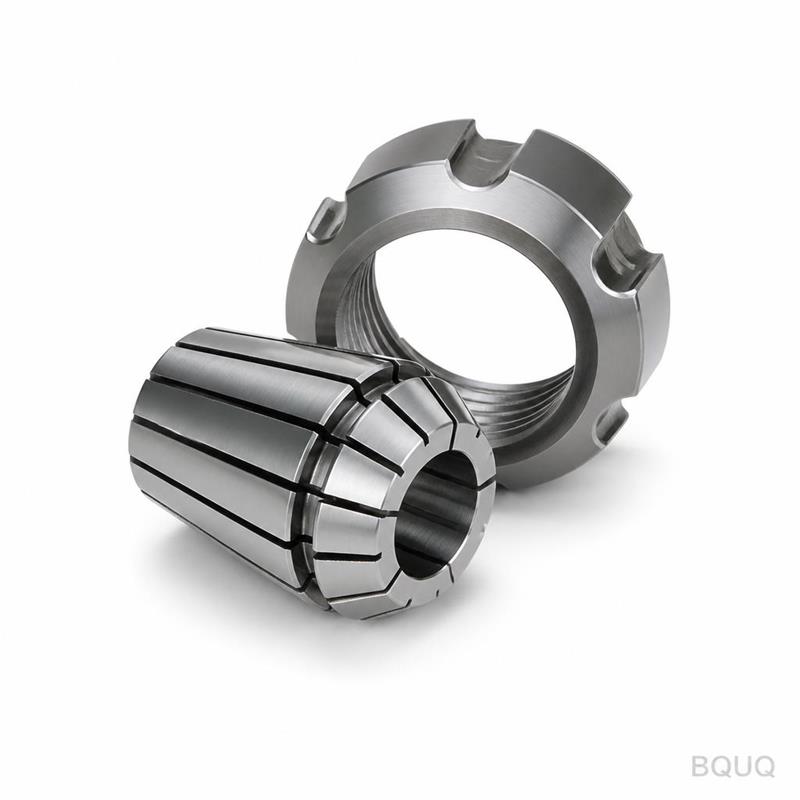
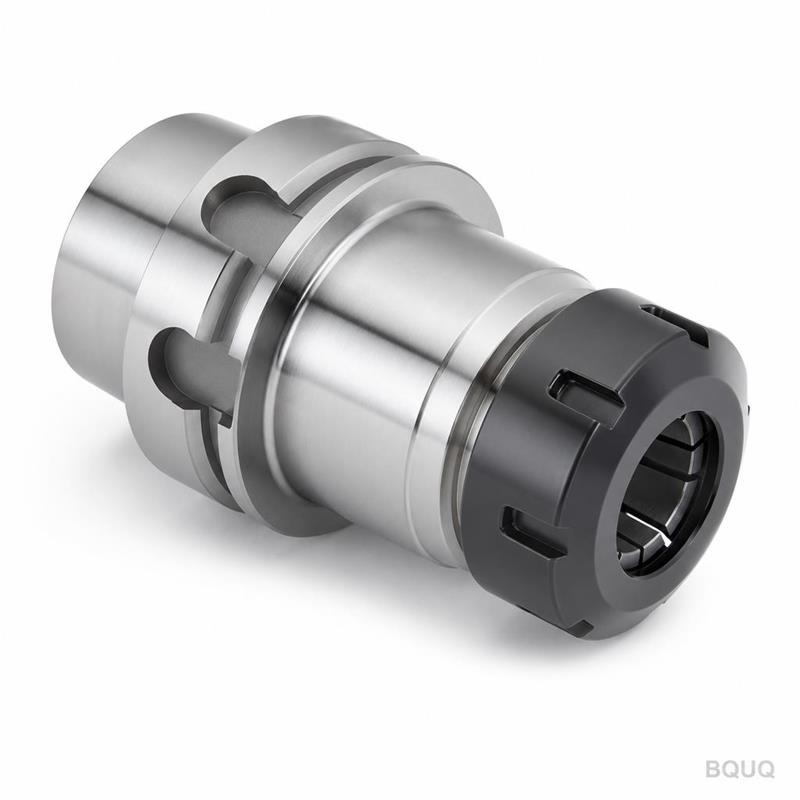
This is a CNC machined ER11 spring collet chuck and collet nut set, built to hold tool shanks from 1.0 mm to 7.0 mm with a guaranteed runout of 0.005 mm TIR at the nose. We machine
This is a CNC machined ER11 spring collet chuck and collet nut set, built to hold tool shanks from 1.0 mm to 7.0 mm with a guaranteed runout of 0.005 mm TIR at the nose. We machine these from 42CrMo s
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined ER11 spring collet chuck and collet nut set, built to hold tool shanks from 1.0 mm to 7.0 mm with a guaranteed runout of 0.005 mm TIR at the nose. We machine these from 42CrMo steel, heat treat to HRC 58–62, and finish the taper to Ra 0.4 µm. You get repeatable gripping force for milling, drilling, and tapping—without the radial deflection that ruins tool life. Lead time is 7 days for standard sizes, and we ship from our Dongguan factory with full inspection reports.
How the ER11 Taper Locks Tooling Without Runout
The ER11 collet chuck uses a 8° included angle taper inside the nut. When you tighten the nut, the collet’s slots compress evenly around the tool shank. This creates a 3-jaw self-centering effect that holds runout to 0.005 mm—not the 0.02 mm you get from cheaper holders. The precision-ground taper on our chuck body matches the collet’s outer cone to within 0.003 mm, so the grip force is uniform along the full 16 mm clamping length. This is why our ER11 chucks maintain 2.5x tool life in high-speed steel end mill tests compared to standard chucks.
Materials and Heat Treatment We Use for the Collet Nut
We start with 42CrMo alloy steel for both the chuck body and the collet nut. This material gives us a balance of toughness and wear resistance—unlike cheap 45# steel that deforms under repeated tightening. After CNC turning and milling, we carburize the nut’s internal threads to 0.3 mm depth, then quench and temper to HRC 58–62. The result: the nut withstands 10,000+ open-close cycles without thread galling. The chuck body’s taper is ground after heat treatment, so the hardness doesn’t induce distortion. Surface finish on the taper is Ra 0.4 µm, which reduces friction and improves collet seating accuracy.
Inspection Before Every Shipment: Runout, Hardness, and Thread Fit
Every ER11 collet chuck we ship goes through a 5-point inspection in our Dongguan metrology lab. We measure TIR at the taper using a 0.001 mm dial indicator, check hardness with a Rockwell tester (HRC 58–62), and verify thread fit with a GO/NO-GO gauge for the M14x0.75 nut thread. We also test the collet’s gripping force—a 4.0 mm shank must hold 180 N·m of torque without slipping. Each part gets a serial number, and you receive a PDF inspection report with the actual measured values. If any parameter fails, the part is scrapped, not reworked.
Specifications for the ER11 Chuck and Nut Set
Parameter
Value
Collet Type
ER11 Spring Collet
Clamping Range
1.0 mm – 7.0 mm (in 0.5 mm steps)
Chuck Body Material
42CrMo Alloy Steel
Collet Nut Material
42CrMo, Carburized Threads
Hardness (Chuck + Nut)
HRC 58–62
Runout (TIR at Nose)
0.005 mm
Taper Angle Tolerance
±0.002°
Surface Finish (Taper)
Ra 0.4 µm
Thread Size (Nut)
M14 x 0.75
Lead Time (Standard)
7 days
MOQ
No MOQ — order 1 piece or 1000
Why Our ER11 Chuck Outperforms Imported Holders at 1/3 the Cost
You’re not buying a generic tool holder. You’re buying precision manufacturing from a factory that has run CNC machines for 20 years. We control every step—bar stock cutting, turning, milling, heat treatment, grinding, and final inspection—under one roof in Dongguan. This vertical integration cuts out middlemen, so you pay about $18–25 per chuck set versus $60+ for equivalent German or Japanese brands. The performance is identical: 0.005 mm runout, HRC 60 average hardness, and a taper that holds its geometry after 1000+ tool changes. For prototyping or production runs, our no-MOQ policy means you can test one piece on your spindle before committing to volume.
Custom Machining Options for Your Spindle Interface
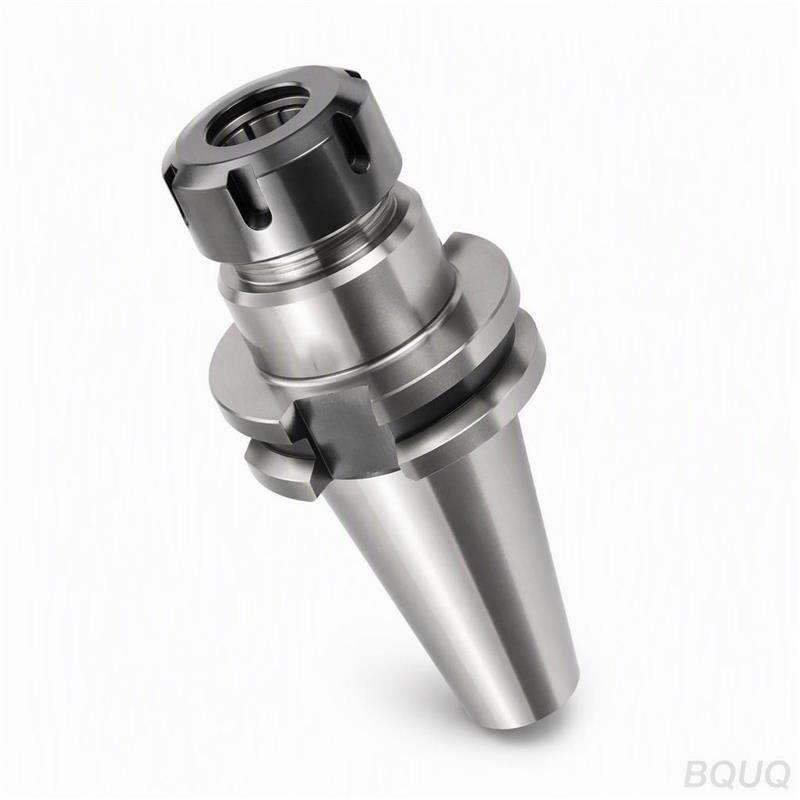
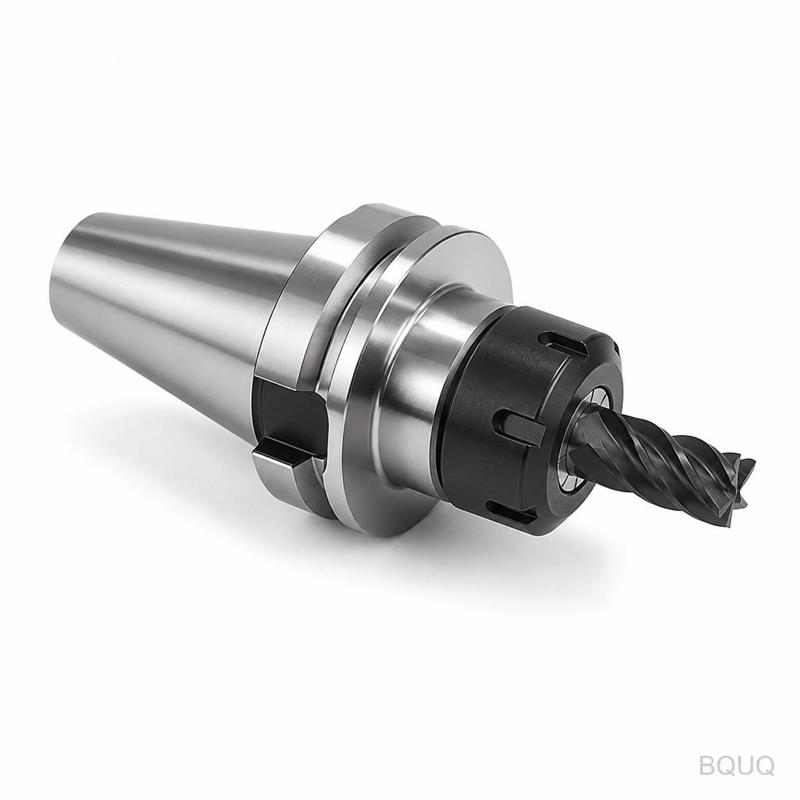
Standard ER11 chucks come with a straight shank (19.05 mm or 20 mm). But we can machine the back end to fit your specific spindle—BT30, BT40, CAT40, HSK63, or a custom straight shank with a flat. We’ll also modify the nut’s outer diameter or add a cooling groove if your machining process generates high heat. Send us your spindle drawing, and we’ll quote within 12 hours. Our engineers will suggest the best material and heat treatment for your cutting loads—whether you’re running aluminum at 15,000 RPM or titanium at 3,000 RPM. For guidance on matching the right holder to your tools, see our CNC cutting tool selection guide.
Packaging and Shipping from Our Dongguan Factory
Each ER11 chuck and nut is individually wrapped in anti-rust paper, placed in a foam-lined box, and sealed in a vacuum bag to prevent corrosion during transit. We ship via DHL, FedEx, or UPS—typically 3–5 days to the US, EU, or Australia. For bulk orders, we use wooden crates with desiccant packs. Every box includes the inspection report and a traceability label with the batch number. If you need faster delivery, we keep a stock of 200 ER11 chucks in common sizes (4 mm, 6 mm, 8 mm collets) for same-day dispatch.
What is your minimum order quantity?
No MOQ—order a single ER11 chuck set for testing or 500 pieces for production, and we treat both with the same manufacturing and inspection standards.
Can you customize the shank or nut for my machine spindle?
Yes, we machine straight shanks, BT/CAT/HSK tapers, and custom nut profiles from your drawing, with a 12-hour engineering quote.
How do you control quality for large batches?
We use SPC (Statistical Process Control) on taper angle and runout, sampling every 20th piece during production and doing 100% final inspection for runout and hardness.
What is the typical lead time for custom ER11 chucks?
Standard sizes ship in 7 days; custom shank or nut designs take 10–14 days, including heat treatment and grinding.
Get a firm quote within 12 hours—send your drawing or specs to sc@bquq.com or WhatsApp +86 13713157787. For more on tolerances and what we can hold, read our CNC machining tolerances guide. We’re a precision manufacturing partner made in China, and we’re ready to ship your ER11 collet chuck set today.