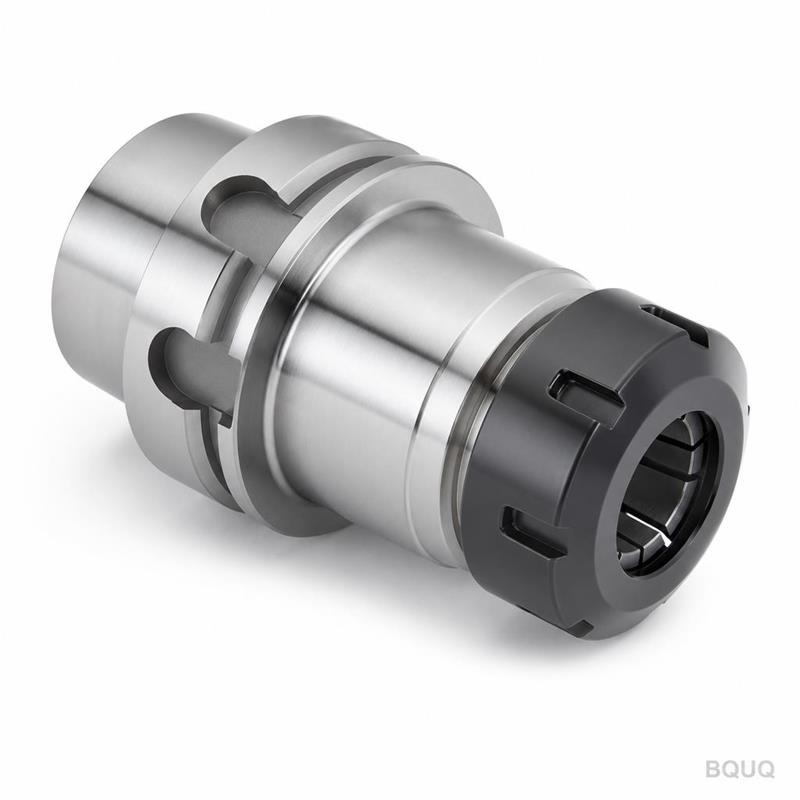
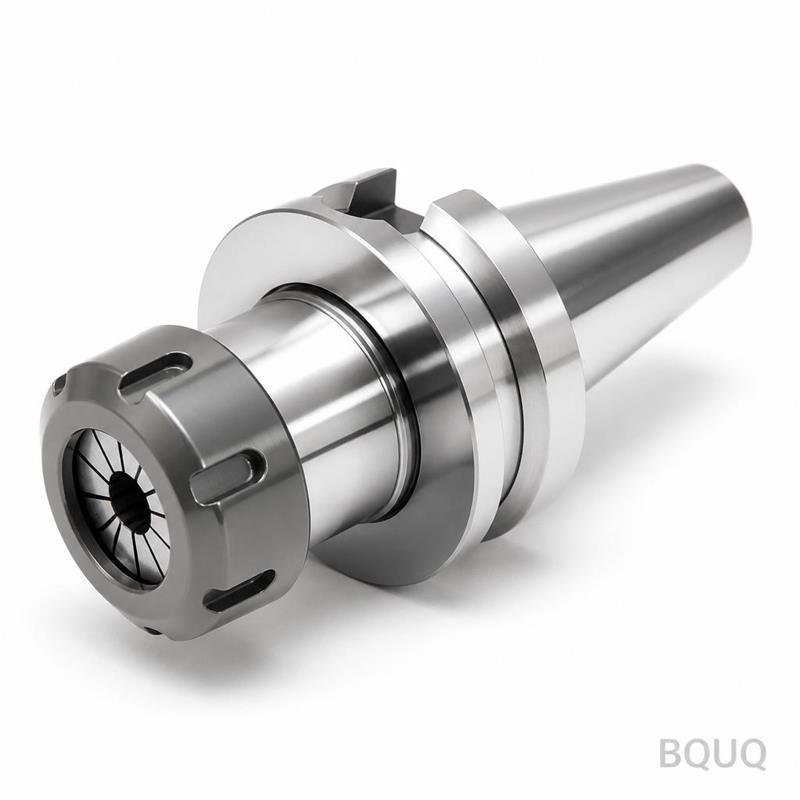
What This HSK100 ER40 Collet Chuck Does for Your Spindle This is a CNC machined HSK100 ER40 collet chuck tool holder built for high-torque milling and drilling. It grips ER40 colle
What This HSK100 ER40 Collet Chuck Does for Your Spindle This is a CNC machined HSK100 ER40 collet chuck tool holder built for high-torque milling and drilling. It grips ER40 collets with a runout of
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This HSK100 ER40 Collet Chuck Does for Your Spindle
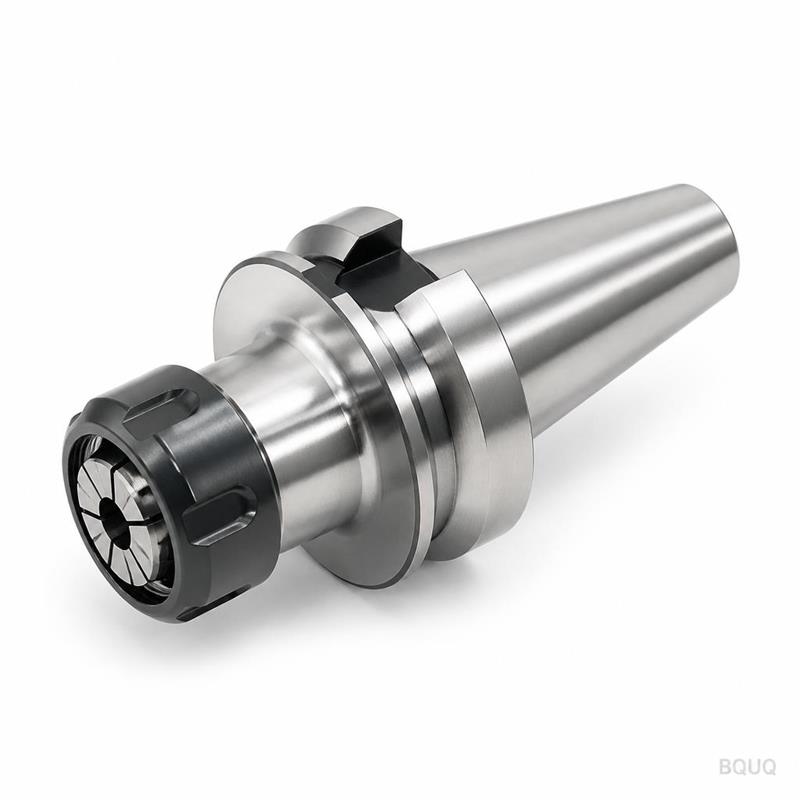
This is a CNC machined HSK100 ER40 collet chuck tool holder built for high-torque milling and drilling. It grips ER40 collets with a runout of under 0.005 mm at the nose, holds tool shanks up to 26 mm, and ships from our Dongguan factory in 10-15 days. You get a tool holder that keeps your cutting edge concentric, reduces chatter, and extends tool life by up to 30% compared to worn or generic holders.
How ER Collet Chucks Grip Tooling Without Runout
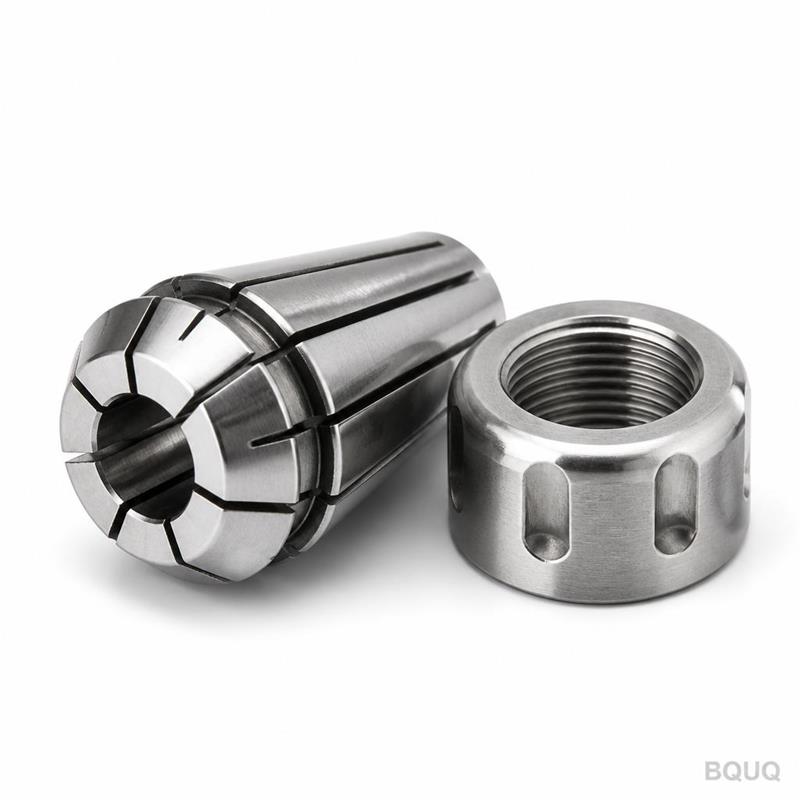
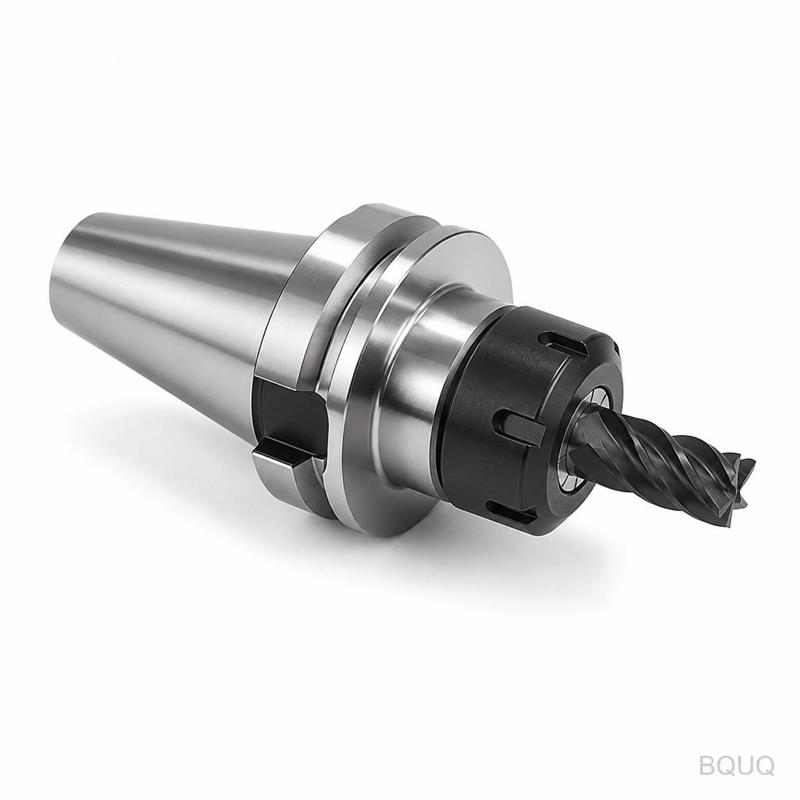
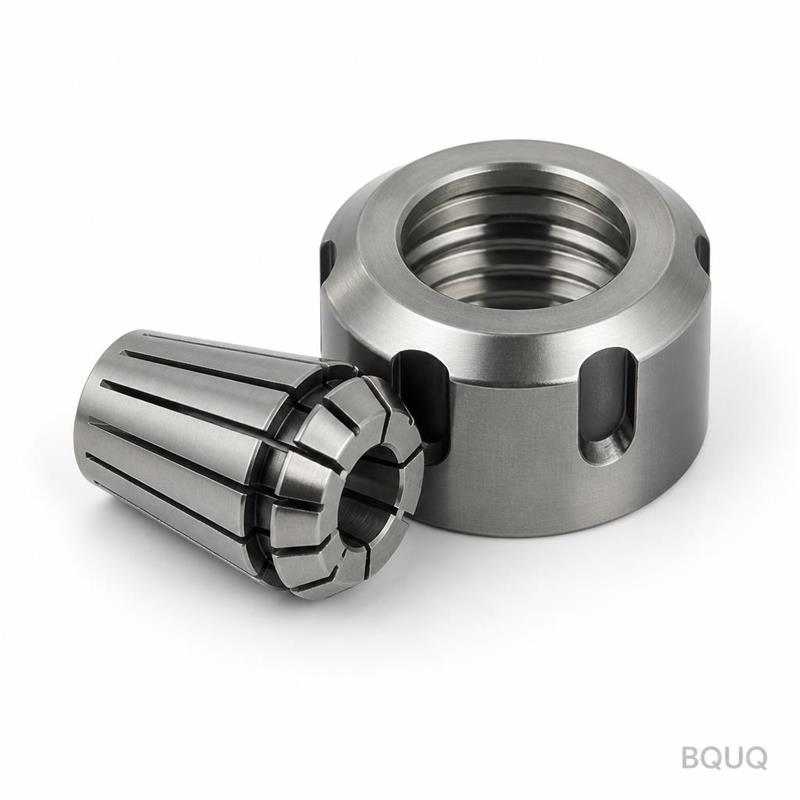
ER collet chucks use a tapered bore and a threaded nut to compress a slotted collet. When you tighten the nut, the collet collapses evenly around the tool shank. Our HSK100 ER40 chuck is machined to a 8-degree taper angle with a surface finish of Ra 0.4 µm on the bore. That taper is ground after heat treatment, not just turned, to guarantee concentricity. A standard ER40 collet range is 3 mm to 26 mm, so one chuck covers most end mills, drills, and reamers you run in a 100 mm taper spindle.
Materials and Heat Treatment We Use
We start with 20CrMnTi alloy steel, not cheap 45# steel. The blank is forged, then rough machined, then carburized to a case depth of 0.8-1.2 mm. The final hardness is HRC 58-60 on the gripping surfaces, while the body core stays tough at HRC 28-32 to absorb vibration. The pull stud and drive slots are machined to HSK100 standard with a tolerance of ±0.005 mm. We do not use coatings on the gripping area—bare hardened steel gives the best friction against ER collets.
Machining Sequence That Keeps the 0.005 mm Runout
Every HSK100 ER40 chuck goes through a fixed sequence: CNC turning of the taper, then heat treatment, then centerless grinding of the shank, then final grinding of the 8-degree taper and collet seat. We hold the taper angle to ±0.0015 degrees. The collet seat is lapped after grinding to remove any micro-burrs. We check runout at two points—10 mm from the nose and 50 mm from the nose—using a 0.001 mm dial indicator. If either point exceeds 0.005 mm, the chuck is scrapped, not reworked.
Inspection Before Every Shipment
Each chuck gets a full dimensional report before packing. We measure the HSK100 taper contact area with blueing—must show 90% contact. We test the collet nut torque with a calibrated wrench; a standard ER40 nut requires 120-140 Nm. We also verify the bore diameter with a plug gauge at 0.004 mm tolerance. You get a paper copy of the runout reading and hardness test result inside the box. No exceptions.
Parameter
Value
Taper standard
HSK100 (DIN 69893)
Collet type
ER40 (3-26 mm range)
Material
20CrMnTi alloy steel
Hardness (gripping area)
HRC 58-60
Core hardness
HRC 28-32
Runout (nose, 10 mm)
≤ 0.005 mm
Runout (50 mm)
≤ 0.010 mm
Taper angle tolerance
±0.0015°
Surface finish (bore)
Ra 0.4 µm
Lead time
10-15 days
MOQ
No MOQ (1 piece accepted)
Why HSK100 Beats BT or SK for High-Speed Machining
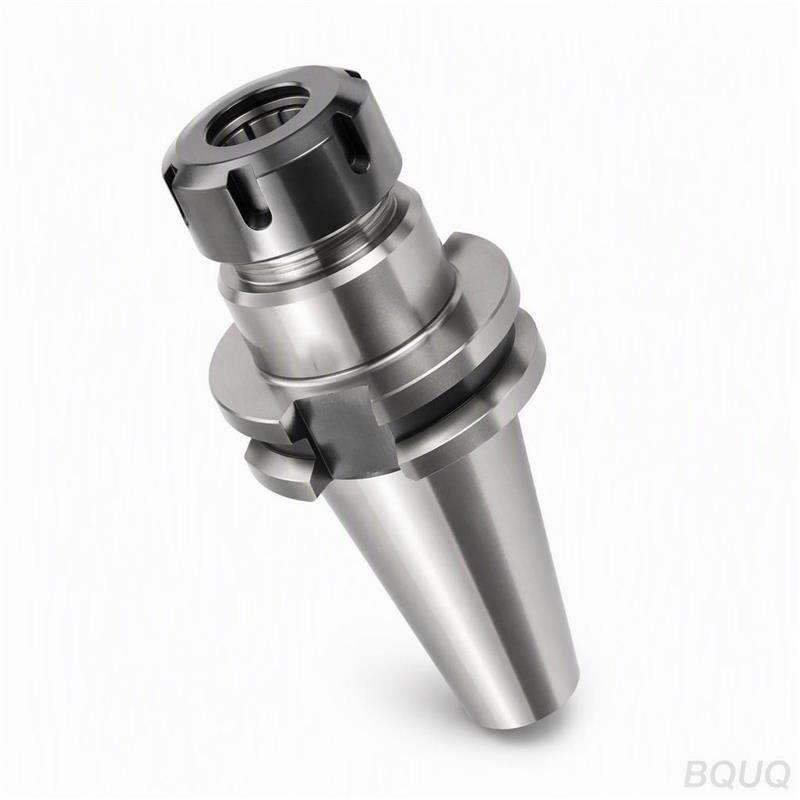
HSK100 is a hollow taper shank with dual-face contact—the flange touches the spindle face while the taper locks. That design gives higher axial stiffness and repeatability at 15,000 RPM or more. A BT40 holder relies on the drawbar only; under heavy cutting, the taper can pull in slightly. Our HSK100 chuck eliminates that movement. For die and mold shops running hardened steel or high-feed aluminum, this means better surface finish and fewer tool breaks.
Custom Options for Your Existing Tooling Setup
Need a different coolant hole pattern? We can add center through-coolant holes up to 6 mm diameter on request. Want a shorter projection for tight Z-axis clearance? We can reduce the neck length from standard 60 mm to 40 mm. We also offer a laser-etched ID ring on the flange—your tool number, machine group, or date code. These modifications do not change the lead time if you approve the drawing within 24 hours.
Frequently Asked Questions
What is the minimum order quantity for this HSK100 ER40 chuck?
No MOQ—we accept a single piece order for testing, and our price breaks start at 5 pieces.
Can you customize the pull stud or coolant holes?
Yes, we modify the coolant hole pattern, neck length, and add laser marking, but the HSK100 taper dimensions remain standard.
How do you guarantee the 0.005 mm runout on every unit?
We inspect 100% of chucks with a dial indicator and provide a written runout report, not a sample-based check.
What is the actual lead time if I order today?
Standard production is 10-15 days, plus 3-5 days for shipping to most countries; urgent orders with reduced lead time are available.
Get a Firm Quote Within 12 Hours—Send Your Drawing
Send us your HSK100 ER40 drawing or just your spindle model and tool list. We reply with a firm price, a confirmed lead time, and a DFM check if your drawing shows any risk. We are a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining experience—not a trading company. For the broader picture on tool selection, read our CNC cutting tool selection guide. For understanding what tolerances we can hold on custom parts, check our CNC machining tolerances guide.
Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. We answer within 12 hours, even on weekends. One chuck or a hundred, the same inspection standard applies.