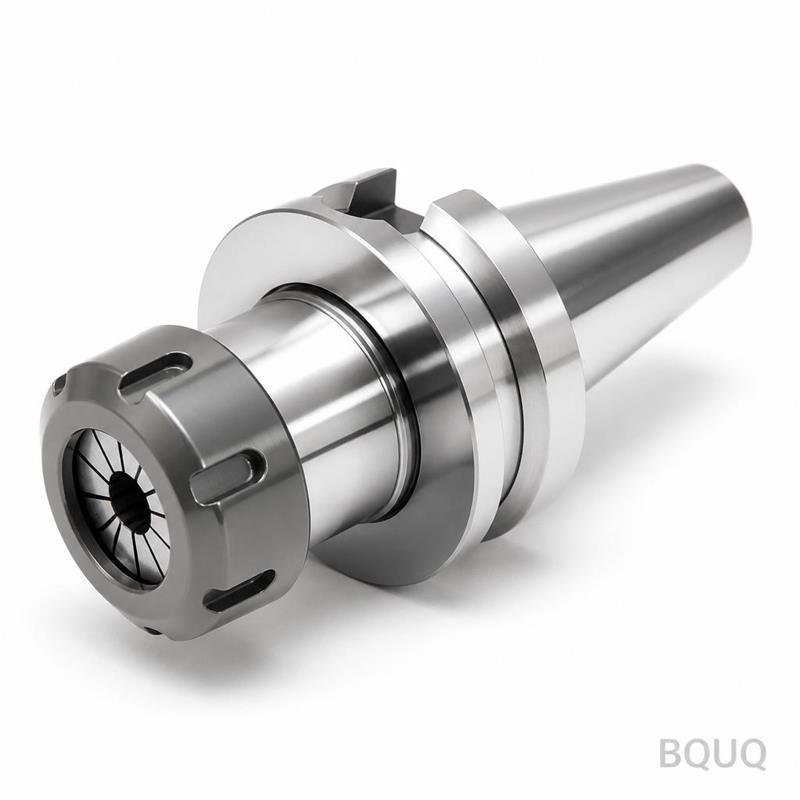
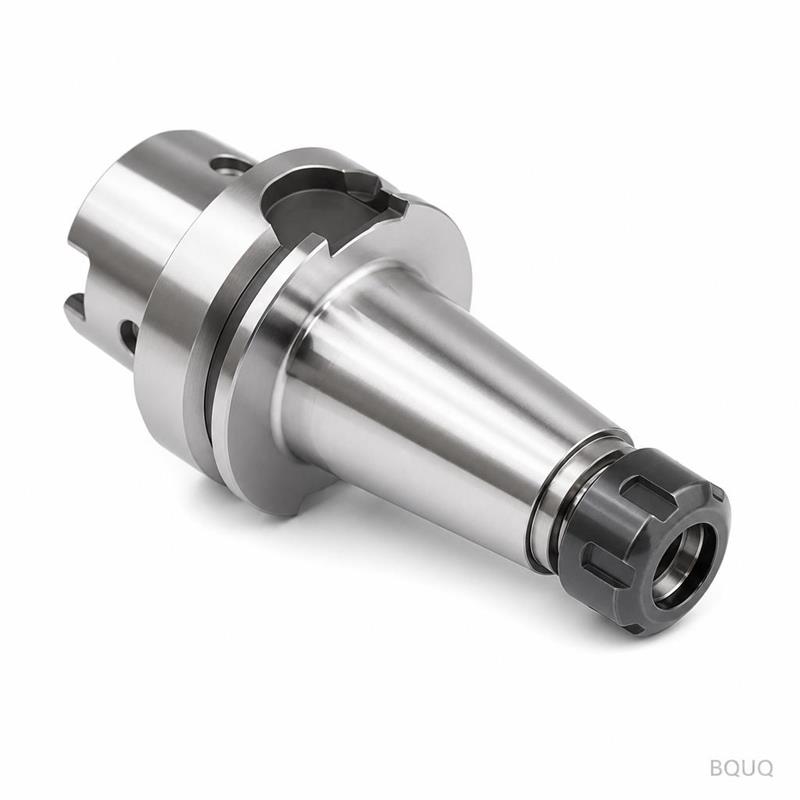
This is a CNC machined ER16 spring collet chuck with a matching collet nut, built for holding tool shanks from 1.0 mm to 10.0 mm in milling, drilling, and tapping operations. Runou
This is a CNC machined ER16 spring collet chuck with a matching collet nut, built for holding tool shanks from 1.0 mm to 10.0 mm in milling, drilling, and tapping operations. Runout is held to 0.005 m
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
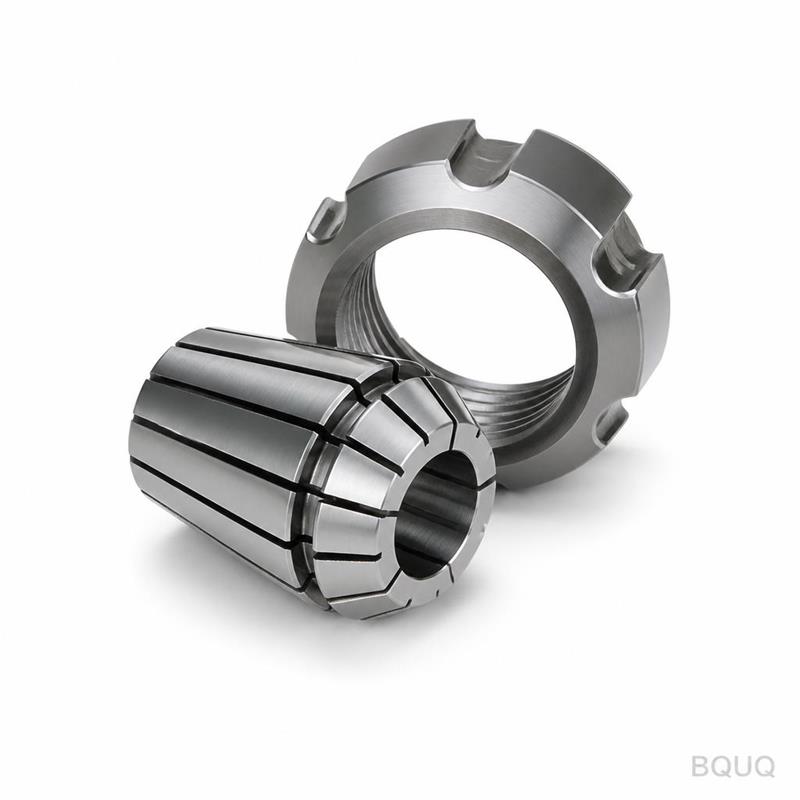
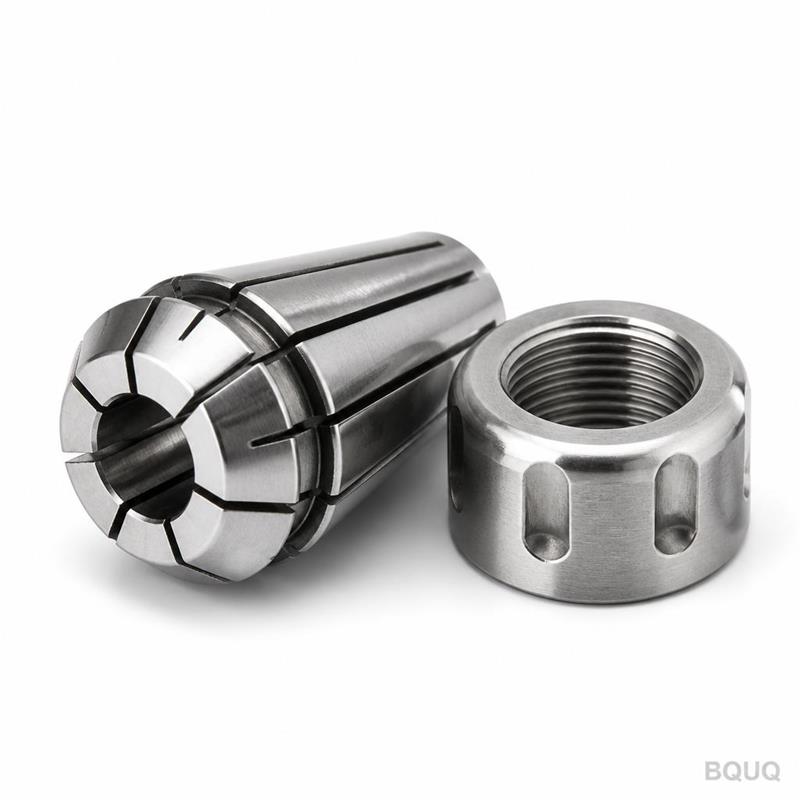
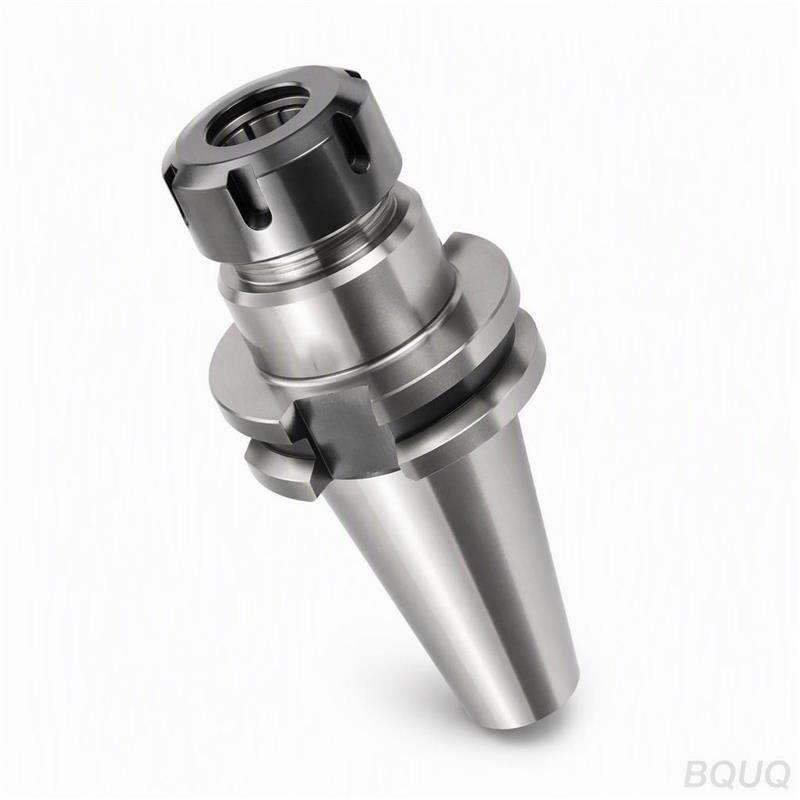
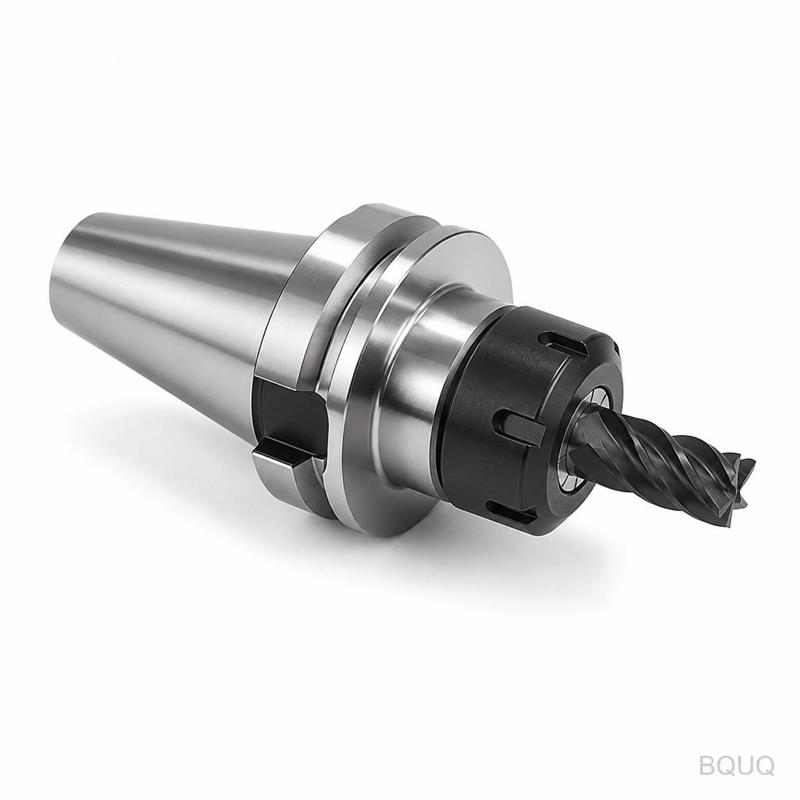
This is a CNC machined ER16 spring collet chuck with a matching collet nut, built for holding tool shanks from 1.0 mm to 10.0 mm in milling, drilling, and tapping operations. Runout is held to 0.005 mm TIR at the nose, hardness is HRC 58-62, and surface finish is Ra 0.4 µm. Lead time is 7 days for standard sizes, 15 days for custom thread forms, and we ship from Dongguan, China with no MOQ.
How the ER16 Collet System Grips Tooling Without Runout
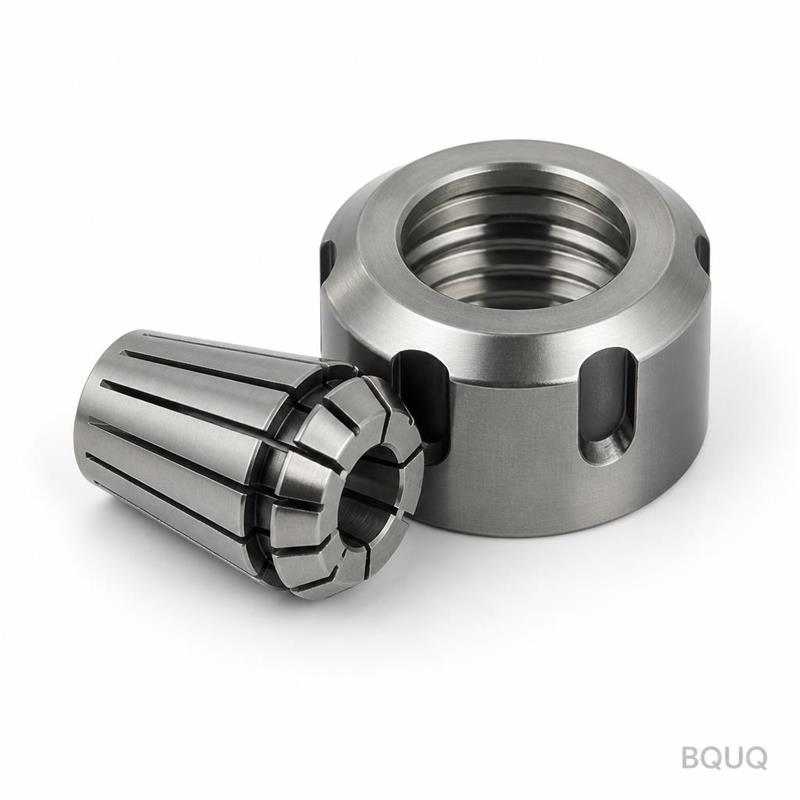
The ER16 collet chuck uses a tapered collet that compresses radially when the collet nut is tightened. The 8-slot design of the ER16 collet allows uniform elastic deformation, clamping the tool shank along its full length. This distributes gripping force evenly, which keeps runout below 0.005 mm even at 20,000 RPM. The collet nut has a precision-ground 30-degree internal taper that matches the chuck face, so the clamping force vector points directly into the spindle, not sideways.
Unlike hydraulic or shrink-fit holders, the ER16 spring collet chuck allows quick tool changes with a single wrench. You can swap an end mill from 6 mm to 8 mm in under 10 seconds. The collet nut is machined with two flat sides for a standard 27 mm open-end wrench, and the thread is ground to ISO 15488-B class, which means the nut seats without wobble.
Materials and Heat Treatment We Use for the Chuck Body and Nut
The chuck body is made from AISI 4140 chromium-molybdenum steel, which we pre-hardened to HRC 28-32 before machining. After CNC turning and milling, we induction harden the taper and thread zones to HRC 58-62. This gives a wear-resistant surface where the collet seats, while the body retains toughness to absorb vibration during heavy cuts. The collet nut is made from 20CrMnTi case-hardened steel, carburized to a depth of 0.8-1.2 mm and hardened to HRC 58-62. The case depth prevents the thread from stripping under repeated tightening torque of 70-80 N·m.
The collets themselves are made from 65Mn spring steel, tempered to HRC 44-48 for elastic recovery. We grind the collet slots with wire EDM, which leaves a burr-free edge and a slot width of 0.5 mm ±0.05 mm. This ensures the collet closes evenly without cracking after 50,000+ cycles. All raw material certificates are traceable to the heat number, and we can provide them with every shipment.
Critical Dimensions and Tolerance Control on the ER16 Taper
The ER16 collet chuck nose taper is ground to a 30-degree included angle with a tolerance of ±0°5'. The taper surface is cylindrical ground to a roundness of 0.002 mm, and the concentricity between the taper and the shank is held to 0.005 mm. The collet nut thread is M27x1.5, class 6H, with a pitch diameter tolerance of 0.032 mm. We measure these with a CMM (coordinate measuring machine) and a Talyrond roundness tester on every batch.
The shank diameter is 16 mm h6, which fits standard ER16 collet chucks in most spindles. The overall length of the standard chuck is 60 mm, but we can customize to any length from 40 mm to 120 mm. The back face is flat ground to 0.002 mm flatness, so it seats squarely against the spindle face. If you need a different shank diameter, like 20 mm or 1/2 inch, we can machine that too—just send your drawing.
Inspection Before Every Shipment: Runout, Hardness, and Surface Finish
Every ER16 collet chuck we ship goes through a 5-step inspection. First, we check the taper angle with a digital protractor. Second, we mount a precision test bar in the collet and measure runout at the nose and at 50 mm from the nose using a 0.001 mm dial indicator. Third, we test hardness on the taper and thread with a Rockwell tester. Fourth, we measure surface finish on the taper with a portable profilometer, target Ra 0.4 µm. Fifth, we torque the collet nut to 75 N·m and re-check runout to confirm the assembly is stable.
We keep a copy of the inspection report for every batch, and we send it with the shipment. If you need a full material certificate or a dimensional report with CMM data, we can include that at no extra cost. Our QC team rejects any part that exceeds 0.006 mm runout—we do not ship borderline parts. This is why our customers in Germany, Japan, and the US reorder without inspecting incoming parts.
Lead Time, MOQ, and Custom Thread Options for Your Spindle
Standard ER16 collet chucks with a 16 mm shank and M27x1.5 nut thread ship in 7 days. If you need a custom thread on the nut, like M25x1.5 or a left-hand thread, lead time extends to 15 days because we cut the thread with a single-point CNC lathe and then grind it. There is no MOQ on standard sizes—you can order 1 piece for a prototype or 500 pieces for production. For custom designs, the MOQ is 10 pieces, but tooling cost is zero because we use existing CNC programs.
We also offer a nickel-plated version of the chuck body for corrosion resistance, which adds 2 days to lead time. If you need a through-coolant version, we can drill a 3 mm coolant hole through the center of the chuck and collet, but this requires a custom collet design. The standard ER16 collet does not support through-coolant; you would need an ER16 with a coolant hole, which we can source or machine.
Specification
Value
Collet type
ER16 spring collet
Clamping range
1.0 mm – 10.0 mm
Shank diameter
16 mm h6 (custom 20 mm, 1/2 in)
Chuck body material
AISI 4140 (pre-hardened)
Nut material
20CrMnTi, carburized
Hardness (taper & thread)
HRC 58-62
Runout (TIR at nose)
0.005 mm
Taper angle
30° ±0°5'
Surface finish (taper)
Ra 0.4 µm
Nut thread
M27x1.5, class 6H
Lead time (standard)
7 days
MOQ
1 piece (standard), 10 pcs (custom)
What is the minimum order quantity for ER16 collet chucks?
No MOQ for standard ER16 collet chucks with 16 mm shank—order 1 piece for testing, we ship it in 7 days.
Can you make a custom thread on the collet nut for my spindle?
Yes, we machine custom nut threads like M25x1.5 or M20x1.0, with a 15-day lead time and a 10-piece MOQ for custom thread forms.
How do you guarantee 0.005 mm runout on every chuck?
We measure runout with a 0.001 mm dial indicator on a test bar after torquing the nut to 75 N·m, and we reject any part above 0.006 mm.
What is your lead time for a rush order of 50 pieces?
For 50 standard ER16 chucks, we can deliver in 5 days if you confirm by Tuesday, because we run this part every week.
This ER16 collet chuck is one component in a broader tooling system. To match it with the right cutting tools, read our CNC cutting tool selection guide. If you are specifying tolerances for a custom holder, check our CNC machining tolerances guide to avoid over-specifying.
We are BQUQ, a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining experience. We also produce stamping parts, springs, and heat sinks. Every ER16 collet chuck is made in China on our own CNC lathes, and we control the full process from raw bar stock to final inspection. No MOQ means you can test our quality with a single piece.
Get a firm quote within 12 hours. Email your drawing or your standard part number to sc@bquq.com. For urgent questions, WhatsApp +86 13713157787. Send your drawing today, and we will reply with a price and lead time before you finish your coffee.