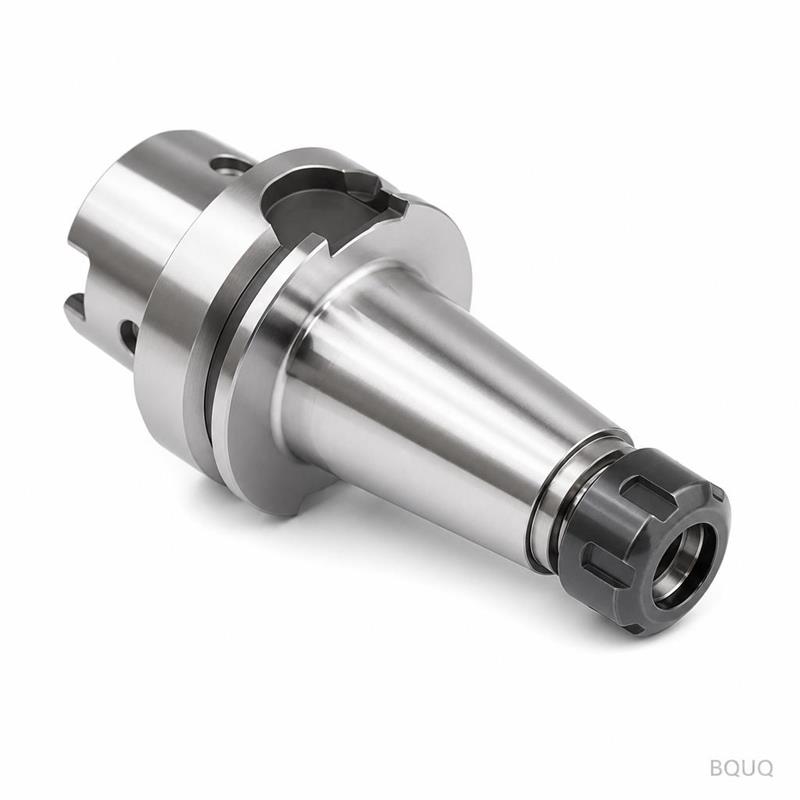
What This HSK50 ER20 Collet Chuck Actually Does for Your Spindle This is a precision-machined HSK50 ER20 collet chuck tool holder built for high-speed CNC machining centers. It g
What This HSK50 ER20 Collet Chuck Actually Does for Your Spindle This is a precision-machined HSK50 ER20 collet chuck tool holder built for high-speed CNC machining centers. It grips ER20 collets (u
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This HSK50 ER20 Collet Chuck Actually Does for Your Spindle
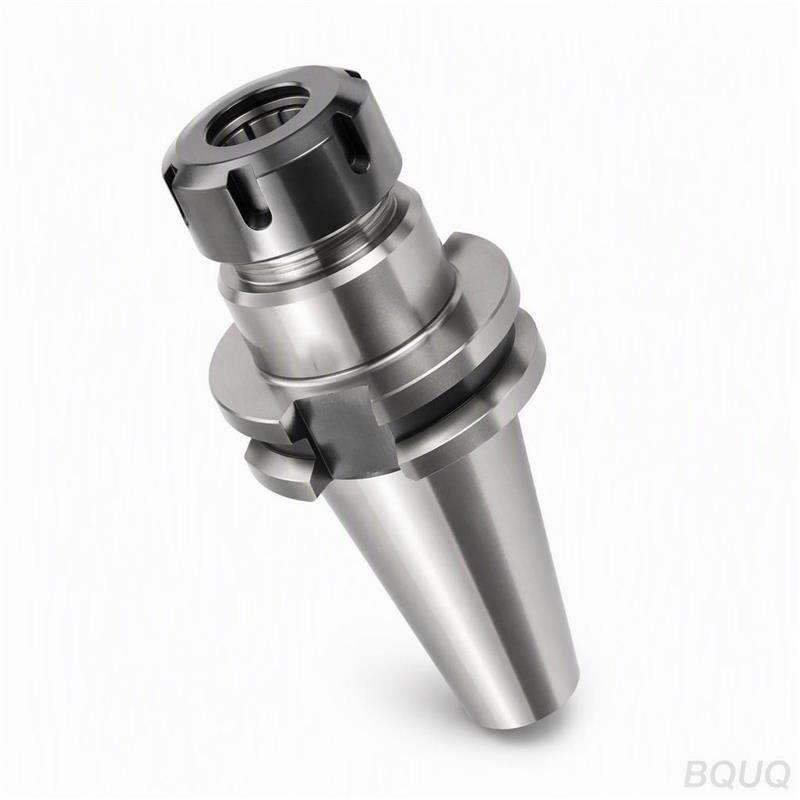
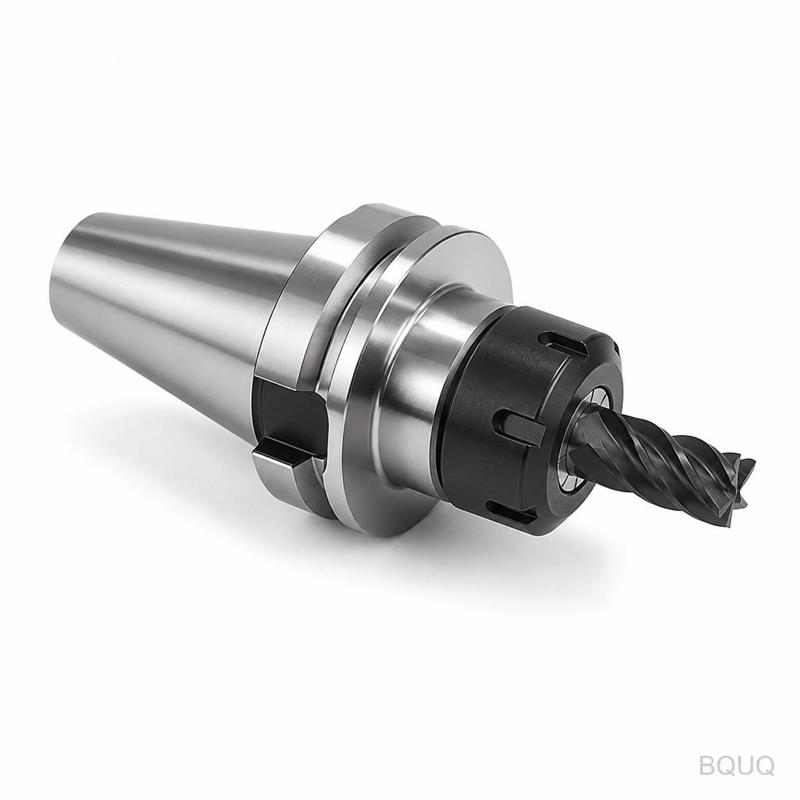
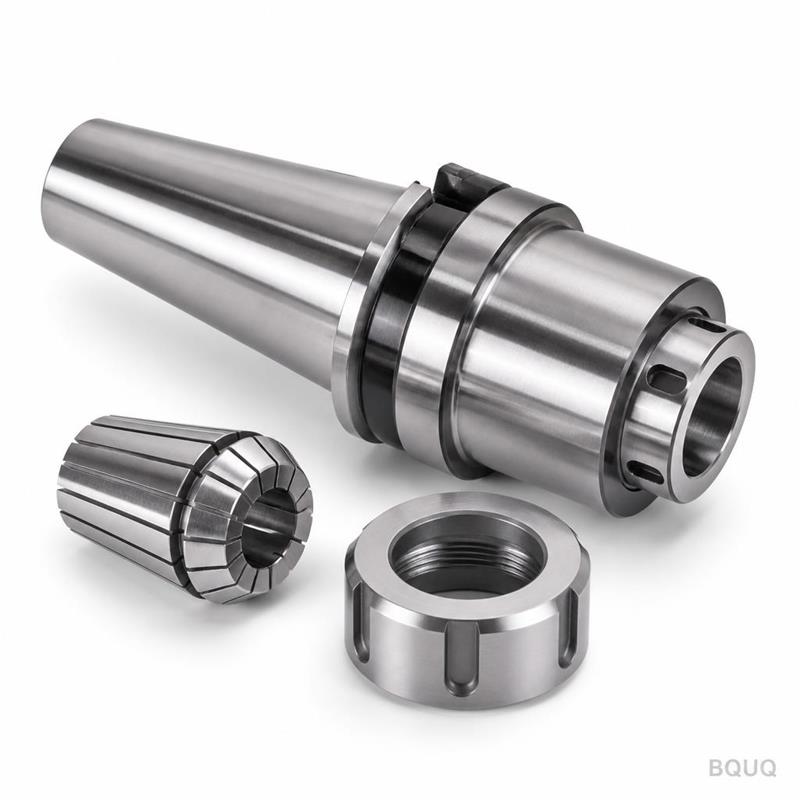
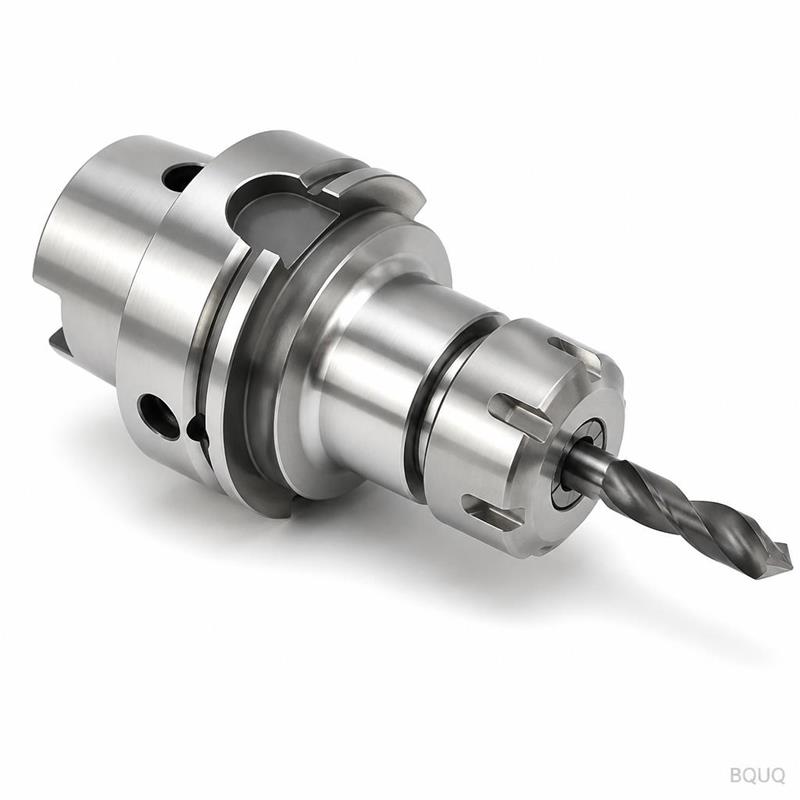
This is a precision-machined HSK50 ER20 collet chuck tool holder built for high-speed CNC machining centers. It grips ER20 collets (up to 13 mm shank diameter) with a radial runout of ≤0.005 mm at the nose—measured after assembly, not just on paper. That runout number translates directly to longer tool life and better surface finish on your parts, especially at 15,000 RPM and above. We ship from our Dongguan factory in 12 working days, with no MOQ.
Why HSK50 Beats BT40 or SK40 for High-Speed Work
HSK50 uses a hollow taper (1:10) that pulls the holder tighter into the spindle as RPM increases. Unlike BT40’s 7:24 taper, HSK50 maintains axial and radial contact under centrifugal force. For high-speed machining—10,000 to 30,000 RPM—this means less vibration and no tool pullout. The ER20 collet system adds clamping force up to 23 Nm, so your end mills stay put during interrupted cuts.
Materials and Heat Treatment We Use
We start with 20CrMnTi (case-hardening steel) for the body and 65Mn for the collet nut. The body is carburized to a depth of 0.8–1.2 mm, then hardened to 58±2 HRC. The taper and collet seat are ground after heat treatment, not before—this eliminates distortion and keeps the taper concentric. Surface finish on the taper is Ra 0.2 μm; the gripping bore is Ra 0.4 μm. We do not use chrome plating or nickel coatings; they flake off and contaminate coolant.
How ER Collet Chucks Grip Tooling Without Runout
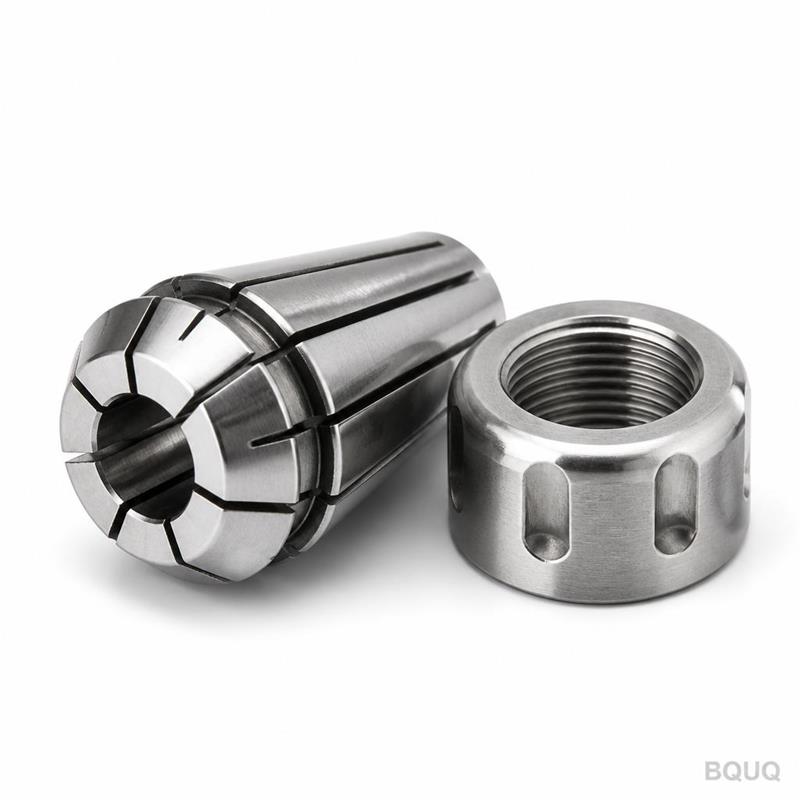
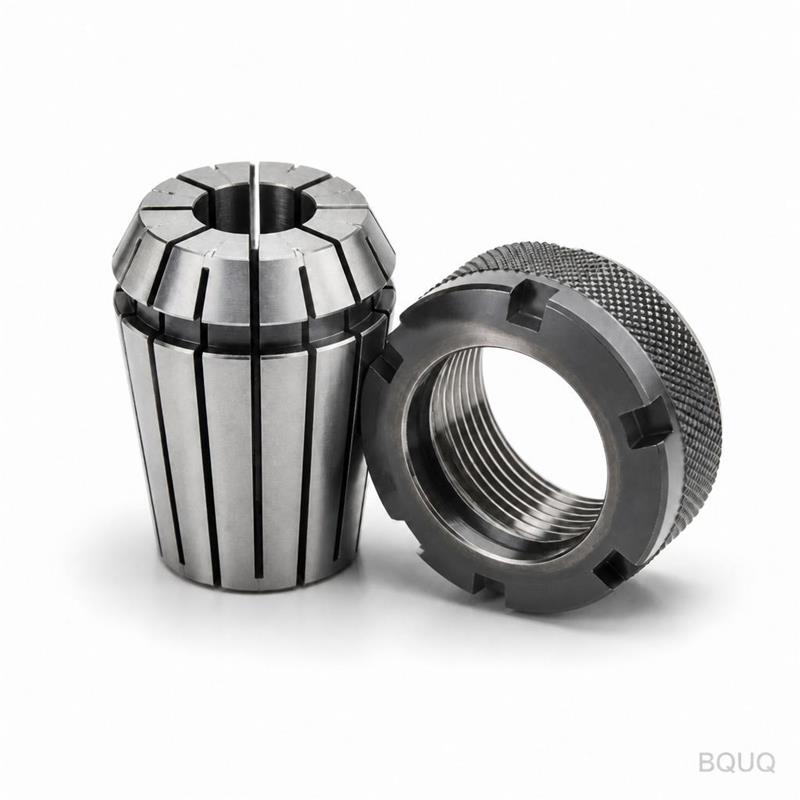
The ER20 collet is a split sleeve with 8 slots. When you tighten the nut, the collet collapses evenly around the tool shank. The key is the internal geometry of the chuck body: the collet seat is ground to a 8° included angle, and the nut thread is ground to class 6H. That combination pushes the collet axially and radially at the same time, centering the tool within 0.005 mm. We test each unit with a 10 mm test bar—not a master collet—so you know the real number.
Inspection Before Every Shipment
Every HSK50 ER20 chuck gets a full inspection, not a sampling. We check: taper contact area (≥90% with blueing), runout at the nose (≤0.005 mm), pull-back force (≥12 kN), and thread fit. We also balance each holder to G2.5 at 20,000 RPM—if it fails, we re-machine the relief grooves until it passes. A written inspection report ships with your order, referencing the exact serial number on the holder.
Specs That Matter for Your Toolholder Selection
Here are the numbers we quote for every batch. If you need a different grip range or balance grade, tell us—we adjust the process, not the price.
Parameter
Value
Interface
HSK50 (DIN 69893-1)
Collet type
ER20 (ISO 15488)
Grip range
1.0 – 13.0 mm
Body material
20CrMnTi, case-hardened
Hardness (body)
58±2 HRC
Hardness (nut)
48±2 HRC
Runout at nose
≤0.005 mm (with test bar)
Surface finish (taper)
Ra 0.2 μm
Balance grade
G2.5 @ 20,000 RPM
Lead time
12 working days (stock to order)
MOQ
1 piece (no MOQ)
Balancing and Runout Limits for High-Speed CNC
At 20,000 RPM, a 1-gram imbalance on a 60 mm diameter creates about 13 N of centrifugal force. That force pushes the tool off-center and leaves chatter marks on your part. We balance every holder individually to G2.5, which means residual imbalance is below 0.6 g·mm for this size. The runout we measure is total indicated reading (TIR) at the nose, including collet seat error—not just the taper. That is the number that affects your hole tolerance and tool wear.
Can I get a custom grip length or through-coolant holes?
Yes—we can machine the overall length from 60 mm to 120 mm, and add two 4 mm coolant holes through the body, but this adds 3–4 days to lead time and changes the balance grade to G6.3 unless you request re-balancing.
Do you really have no MOQ?
Correct—we ship one piece for prototyping, and the per-unit price drops about 18% at 10 pieces and 32% at 50 pieces, but the inspection and material cost stay the same.
How do you control quality on a batch of 100 pieces?
We use a CMM to check the taper angle and concentricity on the first article, then every 5th piece gets a full runout test on a precision mandrel; the rest get a taper contact check with a master gauge.
What is your actual lead time for a custom HSK50 ER20 holder?
Standard holders ship in 12 working days; custom length or coolant holes take 15–16 working days. If you need faster, we can rush a standard holder in 7 days for a 15% surcharge.
Why Precision Manufacturing in China Works for This Part
We have been making toolholders for 20 years in Dongguan—not as a low-cost alternative, but because our grinding department runs 24/7 on dedicated machines for HSK tapers. That means we hold the 1:10 taper within ±0.002 mm on every piece, not just when a customer is watching. You get consistent quality batch after batch, because we control the entire process from steel cutting to final inspection. This is precision manufacturing, made in China, with export-grade documentation.
Before you select a holder for your next job, check our CNC cutting tool selection guide to confirm your collet size and grip length. If you are tightening tolerances on existing parts, our CNC machining tolerances guide explains how runout and taper contact affect your final hole positions.
Get a Firm Quote in 12 Hours
Send your drawing—even a rough sketch with target runout and RPM—to sc@bquq.com. We reply with a firm price, lead time, and balance specification within 12 working hours. For urgent questions, WhatsApp +86 13713157787. No MOQ, no negotiation games—just a straight quote for a Cnc Machined Hsk50 Er20 Collet Chuck Tool Holder High Speed Cnc that works on your machine.