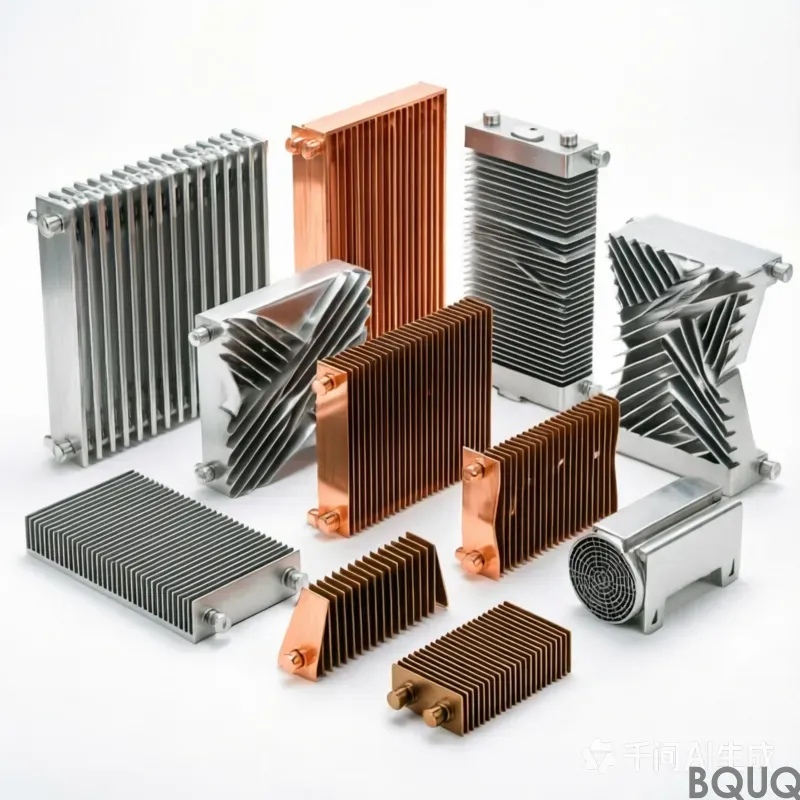
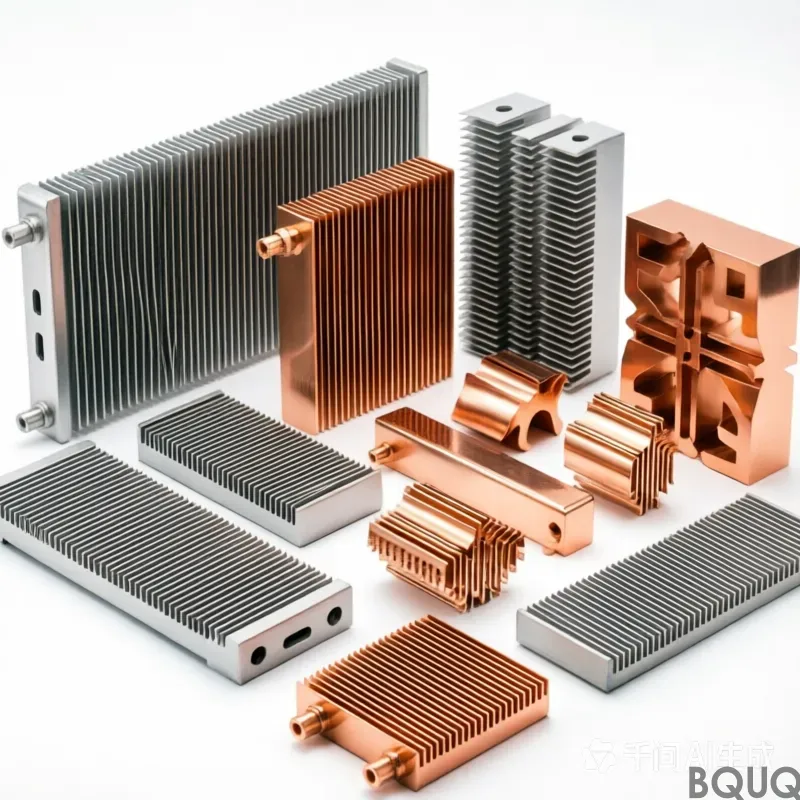
What This Heat Sink Does and Why the Numbers Matter This is a CNC-machined or stamped Heat Sink built to pull heat off your component at a predictable rate, not a decorative block
Precision Heat Sink Manufacturing | BQUQ CNC Machining, Made in China
What This Heat Sink Does and Why the Numbers Matter This is a CNC-machined or stamped Heat Sink built to pull heat off your component at a predictable rate, not a decorative block of aluminum. You get
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Heat Sink Does and Why the Numbers Matter
This is a CNC-machined or stamped Heat Sink built to pull heat off your component at a predictable rate, not a decorative block of aluminum. You get a flatness of 0.05mm across the base, a surface finish of Ra 0.8, and a hardness of HB 90 on 6061-T6, so your thermal interface material spreads evenly and your device runs cooler for longer.
We ship these parts from our Dongguan factory in 10 days for prototypes and 18 days for production runs. The tolerance on fin pitch is ±0.02mm, and the runout on the base-to-fin axis is 0.03mm, which means no warping under load and no rework on your assembly line.
This is precision manufacturing, made in China, with a 20-year track record behind it. You are not gambling on a cheap extrusion house; you are buying repeatable geometry that survives your thermal cycling tests.
Fin Geometry and Airflow Direction: How We Cut the Channels
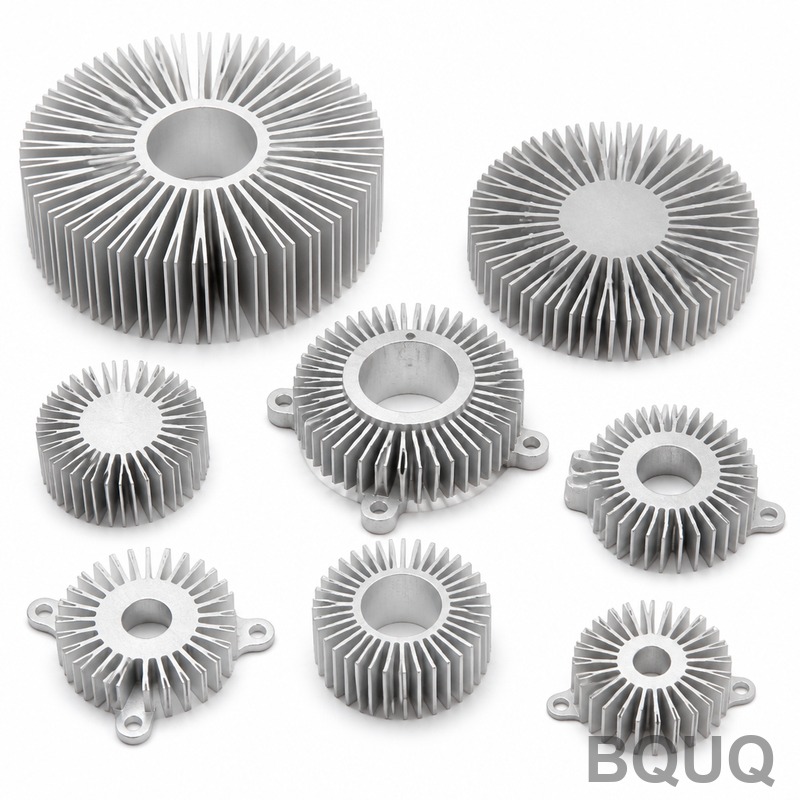
Straight fins are for forced convection. Pin fins are for natural convection. We cut both, plus offset strip fins for high-pressure drop applications.
For a standard 100x100mm base, we machine fin thickness down to 1.5mm with a height-to-width ratio of 8:1. That is a 12mm tall fin with a 1.5mm wall, held at ±0.02mm. Below 1.5mm, we switch to stamping to avoid tool deflection and burr formation.
Every fin channel is deburred manually under a 10x loupe. A burr on the fin edge acts as a hot spot and a particle source. We remove it before anodizing, not after.
Materials and Heat Treatment We Use for Thermal Conductivity
We stock three materials for Heat Sinks: 6061-T6 aluminum (conductivity 167 W/mK), 6063-T5 (conductivity 201 W/mK), and C1100 copper (conductivity 398 W/mK).
Aluminum parts are solution heat-treated and artificially aged to T6 condition, giving a hardness of HB 95. Copper parts are annealed to half-hard, not full hard, so they bend rather than crack during stamping.
If you need a nickel-plated copper base for solderability, we do that in-house with a 5-micron layer. The plating thickness is held to ±1 micron, and we test adhesion with a tape pull test on every batch.
Surface Finish and Anodizing: Ra 0.8 Is Only the Start
A raw machined Heat Sink has a finish of Ra 1.6. We polish the base to Ra 0.8 to reduce contact resistance with your IGBT or CPU.
For the fins, we leave a machined finish at Ra 1.6, because a rougher surface increases the effective surface area for convection. We do not polish the fins unless you specifically ask for a cosmetic finish.
Black anodizing is available at 18 microns thickness (MIL-A-8625 Type II). The coating adds emissivity of 0.85, which helps radiate heat in sealed enclosures. We mask the base if you need a bare aluminum contact surface.
Inspection Before Every Shipment: CMM and Air Gauge Data
Every Heat Sink goes through a coordinate measuring machine (CMM) check for base flatness and fin parallelism. We also use an air gauge for bore diameters if you have mounting holes.
We provide a full dimensional report with each lot, including fin pitch, fin height, base thickness, and surface roughness traces. You get a PDF with actual measured values, not a certificate of compliance.
For high-volume orders, we use a go/no-go fixture that checks all critical dimensions in 30 seconds per part. This catches any drift in tool wear before it becomes a scrap batch.
Lead Time and MOQ: No Minimum Order for Prototypes
There is no MOQ. You can order one prototype Heat Sink or 10,000 pieces. The price per piece drops significantly at 500 units, but we do not penalize you for testing first.
Prototype lead time is 10 days from drawing approval. Production lead time is 18 days for quantities up to 5,000 pieces. For stamped Heat Sinks, tooling takes 15 days, then parts ship 7 days after tool approval.
If you are in a rush, we can expedite a single prototype in 5 days with a 30% surcharge. This includes CNC machining, deburring, and DHL shipping to your door.
Mounting Options: Through Holes, Tapped Holes, and Spring Clips
We machine through holes for screw mounting, tapped holes for standoffs, or we can install spring clips for tool-free assembly.
Through holes are drilled to H7 tolerance, which is +0.012mm / -0.000mm for a 4mm hole. Tapped holes are cut with form taps, giving a stronger thread than cut taps because the metal is compressed, not removed.
For spring clips, we use our in-house stamping press to make stainless steel clips that snap into the Heat Sink base. This eliminates screws entirely and speeds up your assembly time by about 40%.
Parameter
Value
Available Materials
6061-T6, 6063-T5, C1100 Copper
Base Flatness
0.05mm
Fin Thickness
1.5mm minimum (CNC), 0.8mm minimum (stamped)
Fin Pitch Tolerance
±0.02mm
Surface Finish (Base)
Ra 0.8
Surface Finish (Fins)
Ra 1.6
Hardness (Aluminum)
HB 90-95
Hardness (Copper)
Half-hard, HV 80-100
Anodizing Thickness
18 microns, Type II
Runout (Base to Fin Axis)
0.03mm
Prototype Lead Time
10 days
Production Lead Time
18 days
MOQ
No MOQ
Max Part Size
600mm x 400mm x 150mm
FAQ: Heat Sink Ordering and Engineering Questions
Is there really no MOQ for a custom Heat Sink?
Yes, we accept single-piece orders for prototypes, and we do not charge a separate setup fee for the first article.
Can you match an existing Heat Sink design from a competitor?
Yes, send us the part or a drawing, and we will reverse-engineer the geometry and suggest a cheaper manufacturing method if possible.
What quality control data do you send with each shipment?
You receive a CMM report, surface finish traces, a material certificate, and photos of the first article before we ship.
How fast can I get a quote and then the parts?
A firm quote comes within 12 hours, prototypes ship in 10 days, and production parts ship in 18 days after your approval.
Cost Reduction Ideas: Stamping vs. CNC Machining
If your Heat Sink volume exceeds 2,000 pieces per month, we can often switch from CNC machining to stamping and cut cost per piece by 40-50%.
Stamped Heat Sinks use a progressive die that forms fins from a flat sheet. The die cost is $3,000-$8,000, but the piece price drops to $0.50-$2.00 depending on size.
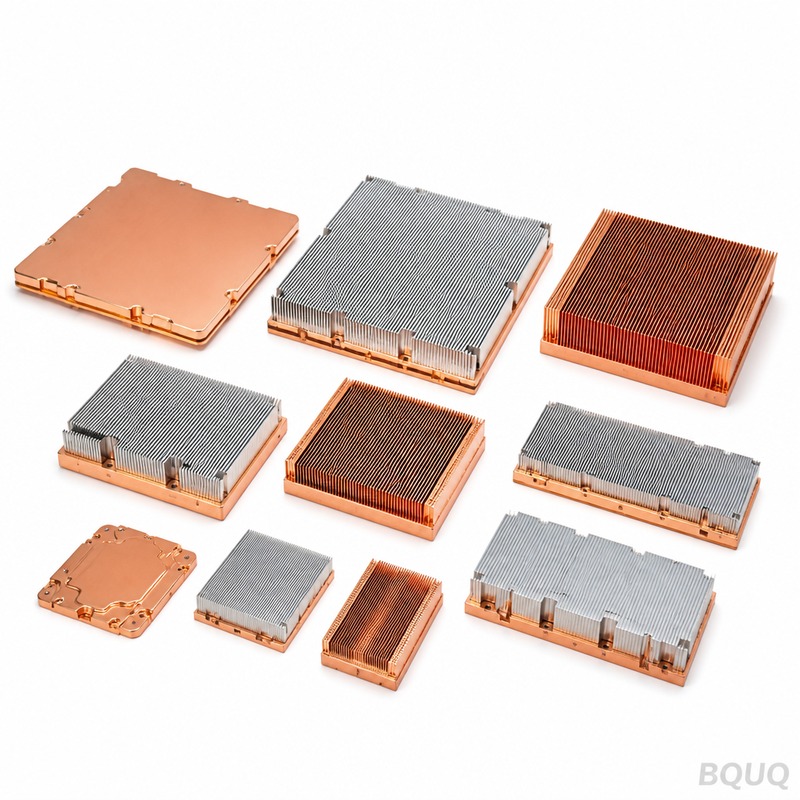
We can also combine a stamped base with CNC-machined fins for a hybrid design that gives you the precision of machining where it matters and the low cost of stamping elsewhere.
Before you finalize your design, check our CNC cutting tool selection guide to understand how tool geometry affects your fin surface finish. Also review our CNC machining tolerances guide to see which dimensions you actually need to hold tightly and which ones you can loosen to save money.
Send your drawing today for a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. We will review your thermal budget, suggest a material, and confirm the lead time before you pay anything.