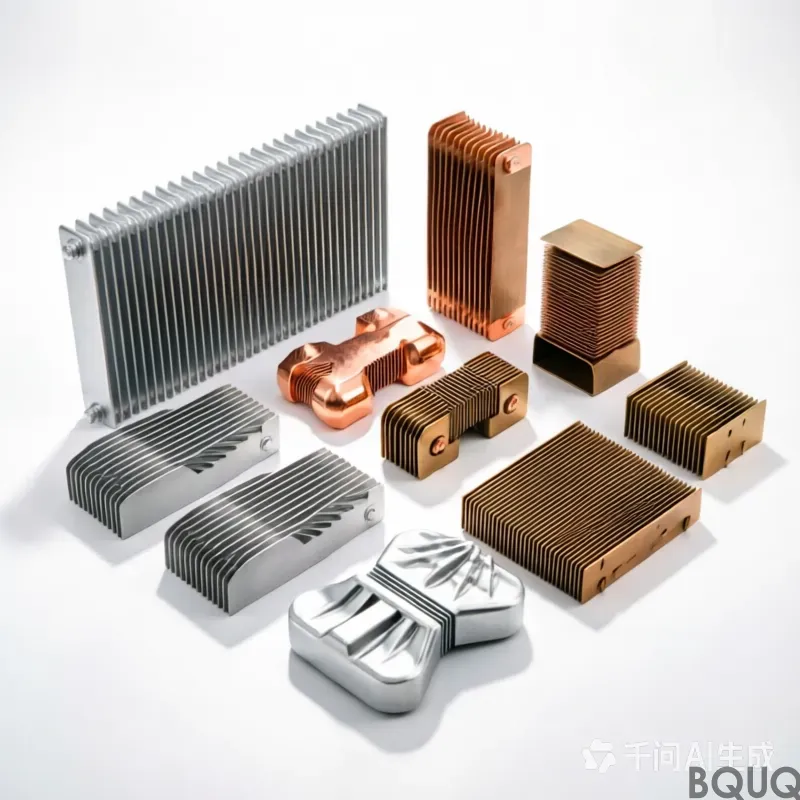
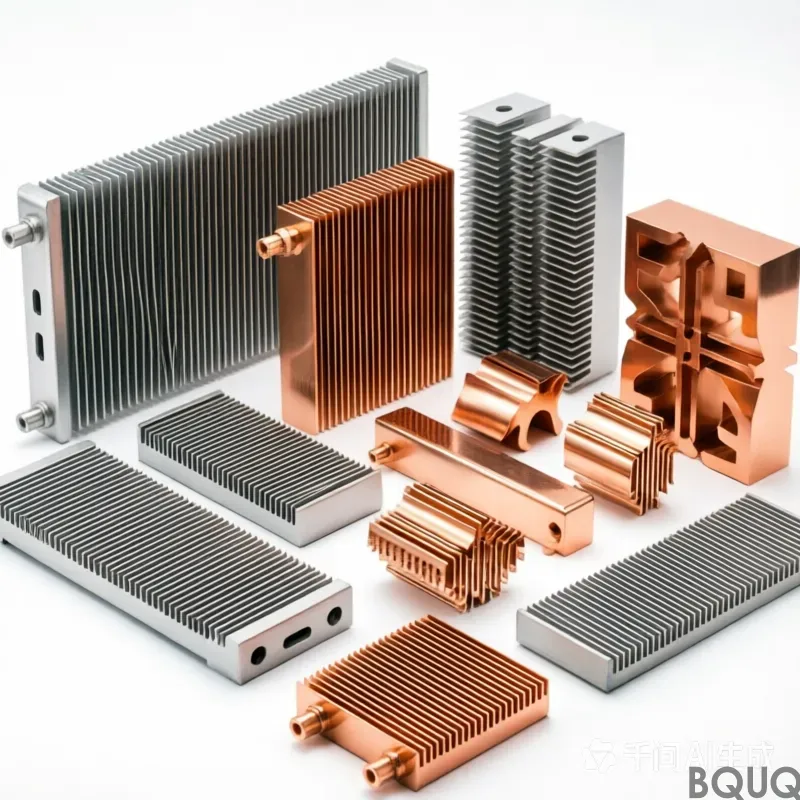
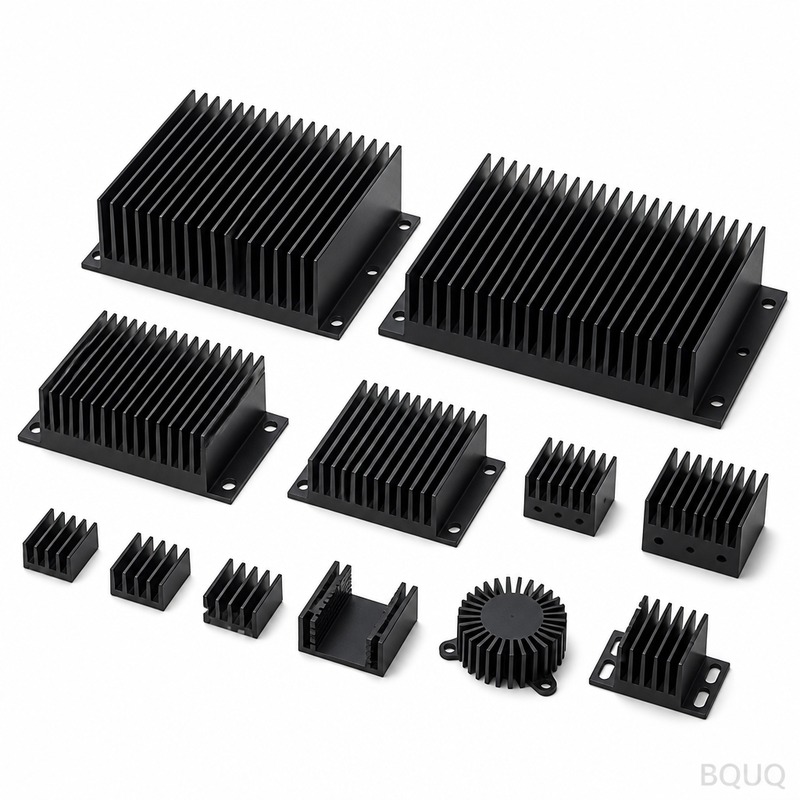
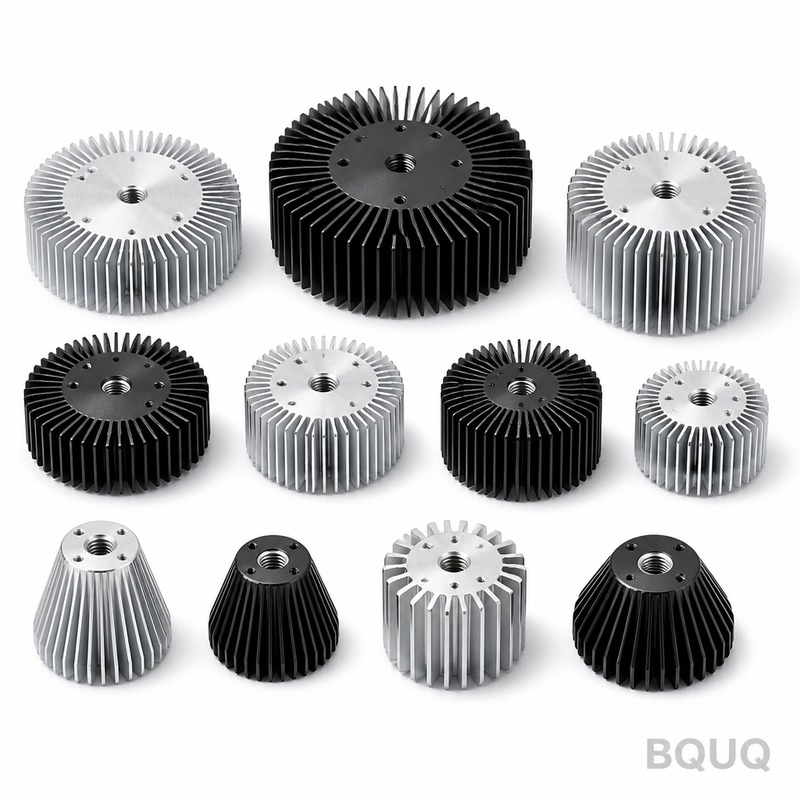
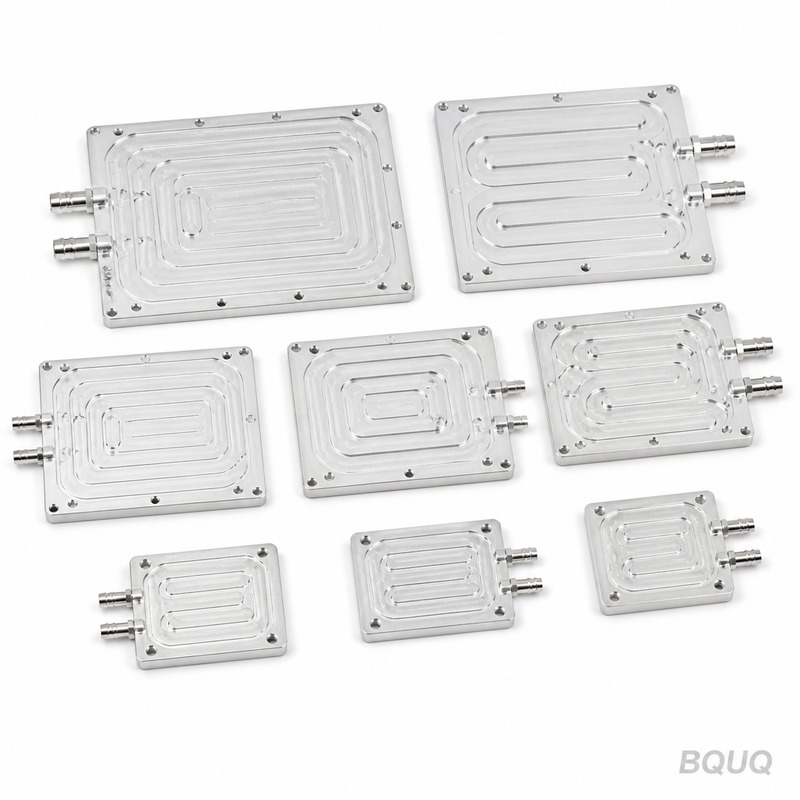
This is a CNC-machined Metal Heat Sink built for active and passive cooling of high-power electronics, power modules, and laser diodes. You get a flatness of 0.02mm across the moun
Precision Metal Heat Sink by BQUQ | CNC Machined, Made in China
This is a CNC-machined Metal Heat Sink built for active and passive cooling of high-power electronics, power modules, and laser diodes. You get a flatness of 0.02mm across the mounting surface, a surf
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC-machined Metal Heat Sink built for active and passive cooling of high-power electronics, power modules, and laser diodes. You get a flatness of 0.02mm across the mounting surface, a surface finish of Ra 0.8µm, and a straightness tolerance of ±0.01mm per 100mm—all verified before shipment. Lead time is 15 days for standard aluminum alloys, and we hold a hardness of 63 HRC on steel-based sinks where structural rigidity matters.
Why Flatness and Surface Finish Determine Your Thermal Junction Temperature
Every 0.05mm of air gap between your IGBT and the sink adds roughly 0.5°C/W of thermal resistance. Our CNC milling and fly-cutting process holds the base flatness to 0.02mm, so you do not need thermal paste thicker than 0.05mm. We measure each surface with a coordinate measuring machine (CMM) and a profilometer. The result: a predictable thermal path for your 200W to 2kW heat loads.
Aluminum 6061-T6, 5052, or Copper C1100—What We Machine Daily
We stock 6061-T6 with a yield strength of 276 MPa and thermal conductivity of 167 W/m·K. For higher conductivity, we use C1100 copper at 391 W/m·K, but we recommend anodized aluminum for weight-sensitive designs. All raw material comes with mill certificates. We reject any plate that shows internal voids or inconsistent grain structure before cutting.
Fins, Pins, and Skived Geometry—How We Machine Without Burrs
We use a 3-axis and 5-axis CNC milling center to produce straight fins, pin fins, or dovetail slots. For fin pitches below 2.5mm, we switch to a custom saw-blade cutter that reduces burr formation. After machining, we tumble every part for 30 minutes to remove micro-burrs that your assembly line would otherwise catch. We also offer a skiving process for fins as thin as 0.8mm, which gives you 30% more surface area than extrusion.
Inspection Before Every Shipment—CMM, Air Gauge, and Leak Test
Every batch goes through a 3-point check. First, a CMM measures critical mounting holes and base flatness. Second, an air gauge verifies hole diameters to ±0.01mm. Third, for liquid-cooled versions, we perform a 0.6 MPa air leak test under water. We send you a PDF inspection report with each shipment. If a part fails, we scrap it on the floor—not in your incoming quality check.
Anodizing, Ni-Plating, or Passivation—Your Corrosion and Insulation Options
We offer Class 2 black anodizing (18–20 µm thickness) for aluminum, which adds dielectric strength of up to 800V. For copper, we provide electroless nickel plating to prevent oxidation at high humidity. If you need a bare surface for maximum thermal conductivity, we ship it with a VCI anti-corrosion paper and sealed poly bags. We do not apply any coating without your written approval.
How We Handle Your Prototype—From One Piece to 5,000 with No MOQ
Send a STEP or IGES file, and we generate a DFM report within 24 hours. For a single prototype, we use the same CNC program as production, so you get identical geometry. We do not charge tooling fees for standard shapes. Only if you require a new skiving blade or custom fixture, we quote a one-time cost of $200–$800, which is waived once you order over 500 pieces.
What is the minimum order quantity?
We operate with no MOQ—you can order one piece for testing, and the unit price is only 15% higher than at 1,000 pieces.
Can you customize the fin pattern for my specific airflow direction?
Yes, we machine any fin pattern—straight, pin, or offset—based on your CFD data, and we will suggest a fin pitch based on your fan curve.
How do you guarantee the flatness of the mounting surface?
We measure flatness on a granite table with a dial indicator at 9 points, and we provide the CMM report before shipping.
What is the lead time for a copper heat sink prototype?
Copper prototypes take 20 days because of longer machining time and additional deburring steps, but we can rush it to 12 days for an extra 10% fee.
Material Selection Guide—Read Before You Send Your Drawing
If you are unsure whether to use 6061-T6 or copper, check our CNC cutting tool selection guide for tips on machinability and tool wear. For tolerance decisions, read our CNC machining tolerances guide to see what is achievable without driving up cost. Both guides are written by our shop floor engineers, not marketing staff.
We are a precision manufacturing factory in Dongguan, China, with 20 years of experience in CNC machining, stamping, and springs. Our heat sinks have shipped to 14 countries for use in EV chargers, medical lasers, and industrial inverters. We keep our process simple: you send a drawing, we quote in 12 hours, and we ship with full inspection data.
Send your drawing for a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. Mention "Metal Heat Sink" in the subject line, and we will prioritize your DFM review.