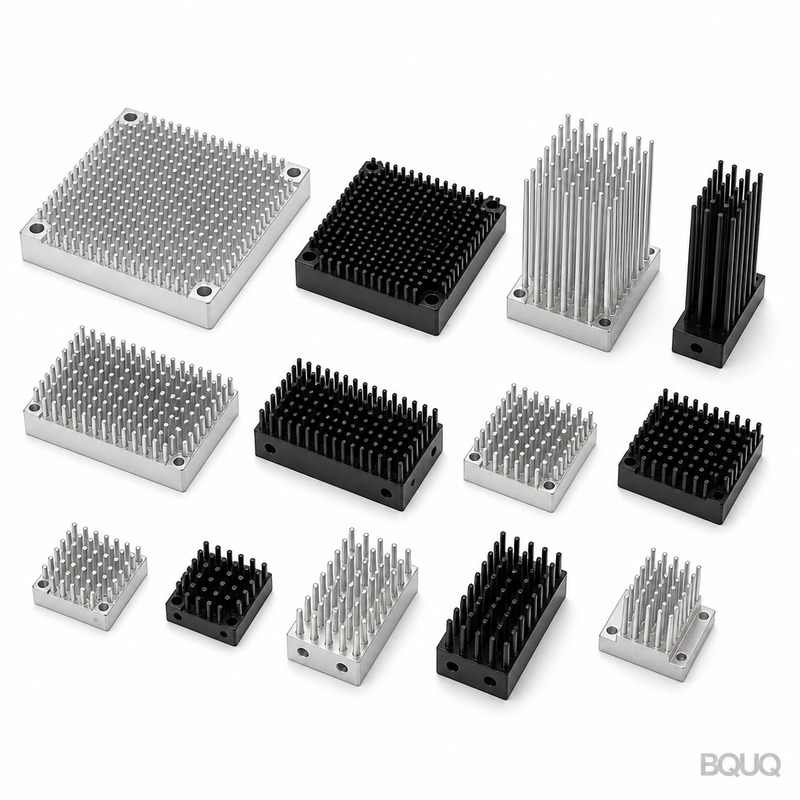
high precision heat sink: 6063-T5 aluminium, 0.5 mm fins at 1.5 mm pitch, 0.05 mm over 100 mm flatness, 0.48 K/W thermal resistance. MOQ 500 pcs, ships in 5 ...
high precision heat sink
high precision heat sink: 6063-T5 aluminium, 0.5 mm fins at 1.5 mm pitch, 0.05 mm over 100 mm flatness, 0.48 K/W thermal resistance. MOQ 500 pcs, ships in 5 ...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
High precision heat sinks are pressed from 6063-T5 aluminium on 250 T tooling, holding 0.05 mm over 100 mm flatness and 0.5 mm fin pitch within ±0.03 mm. They deliver 0.48 K/W at ΔT = 60 K in natural convection, with a 25 s cycle and 800,000 pcs monthly output. Black anodize Type II, 10-15 µm, protects fin roots after forming.
Key Takeaway
High precision heat sinks are pressed from 6063-T5 aluminium on 250 T tooling, holding 0.05 mm over 100 mm flatness and 0.5 mm fin pitch within ±0.03 mm. They deliver 0.48 K/W at ΔT = 60 K in natural convection, with a 25 s cycle and 800,000 pcs monthly output. Black anodize Type II, 10-15 µm, protects fin roots after forming.
A 2.0 mm base and 0.5 mm fins define this high precision heat sink. Pressed from 6063-T5 aluminium on 250 T tooling, it holds 0.05 mm over 100 mm and returns 0.48 K/W at ΔT = 60 K, natural convection. Monthly output runs at 800,000 pcs.
Design Approach and Process
Stamping gives a repeatable 0.5 mm fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within ±0.03 mm across a 800,000 pcs run.
Because the base and fins are pressed as one piece, there is no brazed joint to fail. 0.05 mm over 100 mm flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
A single 250 T stroke forms the whole high precision heat sink, so part cost stops scaling with complexity. Tooling runs ±0.03 mm, and the 25 s cycle feeds a 800,000 pcs line.
Every stroke is dimensionally identical, so ±0.15 mm hole position carries across the batch. That is what makes switch-mode power supply volume programs repeatable.
The black anodize Type II, 10-15 µm finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is 6063-T5 aluminium, supplied with black anodize Type II, 10-15 µm. For applications where switch-mode power supply exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
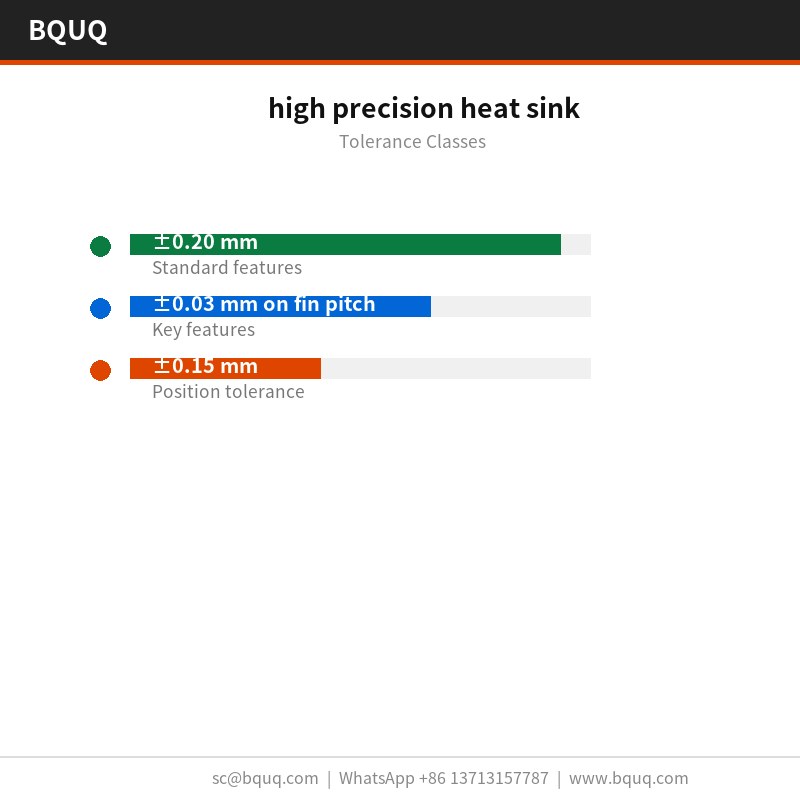
General dimensions run to ±0.20 mm, with critical features such as ±0.03 mm on fin pitch held separately. Formed geometry inherits tooling repeatability of ±0.03 mm, and hole position is held to ±0.15 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Flatness is checked on a granite surface plate, 25 °C against a 0.05 mm over 100 mm limit, and fin pitch is verified optically at ±0.03 mm. Reports go out with each lot.
Each batch carries a CMM report from CMM plus granite flatness plate. We record flatness, pitch, base thickness and hole position, and flag anything outside ±0.20 mm before it leaves the line.
Incoming 6063-T5 aluminium is checked for thickness and hardness before it enters the press. After forming, CMM plus granite flatness plate confirms 0.05 mm over 100 mm and 1.5 mm against the drawing.
Flatness is measured on granite rather than on cast iron, because 0.05 mm over 100 mm at 40 x 40 x 22 mm reads differently on a plate that has not been lapped. Records keep both readings.
Where This Part Is Used
In switch-mode power supply, the 0.48 K/W rating determines how much airflow the enclosure still needs. At switch-mode power supply junction temperatures, 0.5 mm fins at 1.5 mm pitch keep the delta-T inside the sensor budget.
Where a high precision heat sink runs at switch-mode power supply volumes, part-to-part consistency decides field returns. ±0.03 mm on a 800,000 pcs run keeps the thermal curve inside one band.
In switch-mode power supply, the base usually doubles as the mounting interface. 2.0 mm with 0.05 mm over 100 mm flat gives a stable surface for the switch-mode power supply thermal pad.
switch-mode power supply designs often run a 2.0 m/s forced-air path. 0.48 K/W at ΔT = 60 K, natural convection means switch-mode power supply can hold its target with fan power below the acoustic limit.
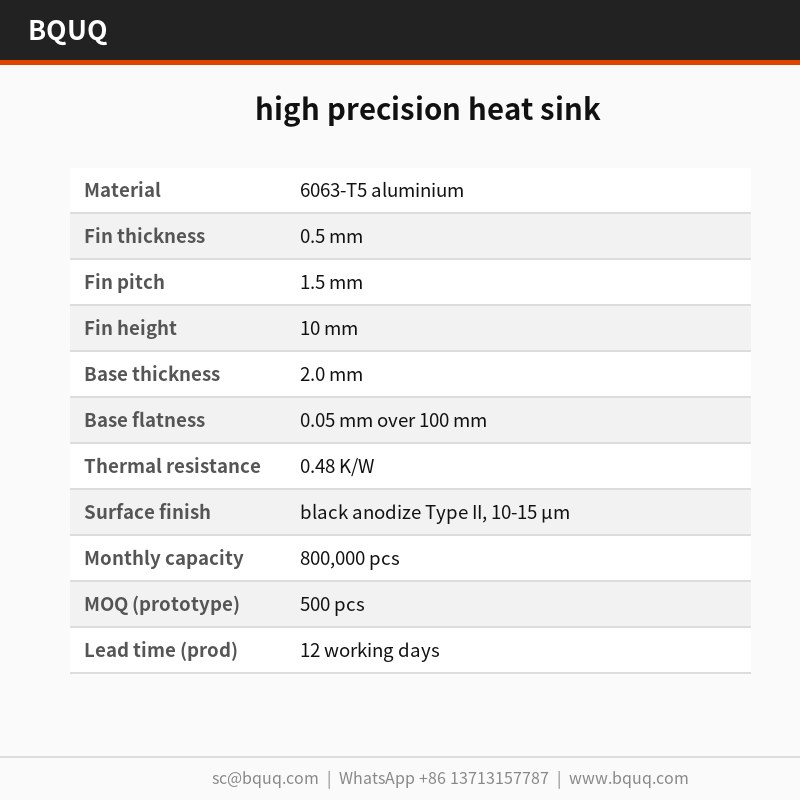
Specifications
Parameter
Value / Range
Material
6063-T5 aluminium
Fin thickness
0.5 mm
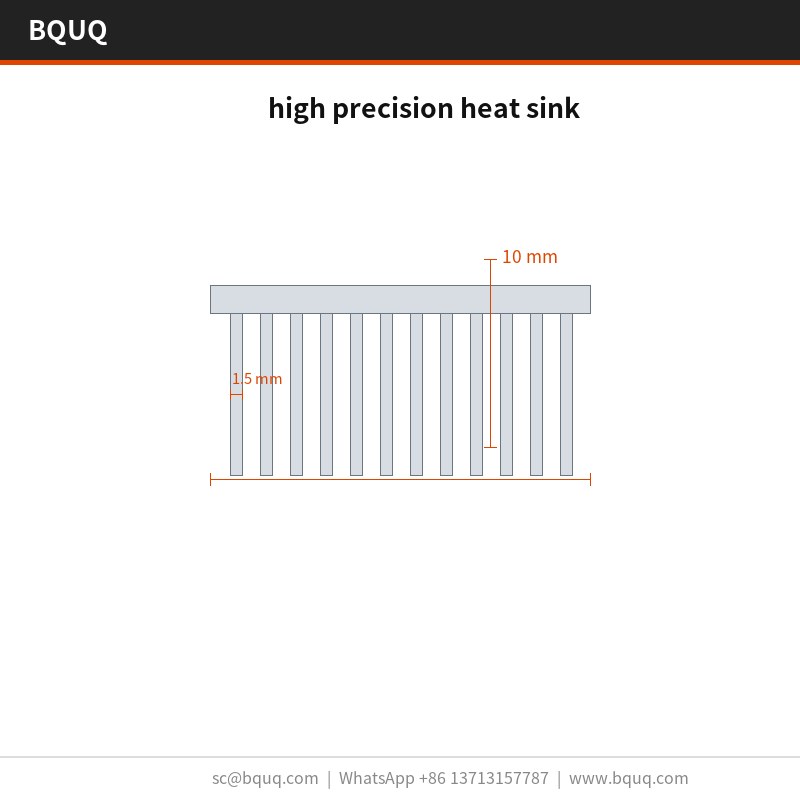
Fin pitch
1.5 mm
Fin height
10 mm
Base thickness
2.0 mm
Base flatness
0.05 mm over 100 mm
Thermal resistance
0.48 K/W
Thermal test condition
ΔT = 60 K, natural convection
Surface finish
black anodize Type II, 10-15 µm
Size range
40 x 40 x 22 mm
FAQ: Your Questions Before Ordering
What is the lead time for the high precision heat sink?
Prototype is 5 working days from drawing approval; production is 12 working days after the first article is signed off. Tooling for a new part takes . We quote CIF Rotterdam, and sea freight to Europe runs about 25 to 30 days after booking.
Can the high precision heat sink be powder coated or plated?
Yes. Standard is black anodize Type II, 10-15 µm. Powder coating to RAL 9005 adds about 0.1 mm to the base; zinc-nickel is better for grounding. Note that any added coating sits between 6063-T5 aluminium and the airflow, so we do not coat the fin roots.
Do you test for thermal resistance?
We test at ΔT = 60 K, natural convection and report 0.48 K/W. That is a steady-state figure, not a transient: for switch-mode power supply first-power-on behaviour you need a different test, and we can run it on request.
Yes, we ship as-pressed for customers who do their own finishing. The risk is handling marks on 0.5 mm fins, so we pack those parts with interleaving sheets inside Anti-static bag + wooden crate over 50 kg.
Can you supply the high precision heat sink pre-assembled?
Yes. We can add clips, screws or a fan shroud as a kitted assembly, with the parts bagged and labelled per set. This is common in switch-mode power supply programs and adds about 3 working days.
The line sits in Dongguan in a single ISO9001 plant. 250 T presses cover the high precision heat sink family, and 800,000 pcs per month is current committed output.
Tooling is built in-house, which is how ±0.03 mm is held across a 800,000 pcs programme rather than drifting part by part.
We quote CIF Rotterdam and hold 500 pcs for sampling. Sampling is paid sample refundable with order, so a first evaluation does not require a production commitment.
0.05 mm over 100 mm; ±0.03 mm fin pitch; ±0.15 mm hole position
Lead time
Not specified in article
MOQ
Not specified in article
Capacity
800,000 pcs per month; 25 s cycle
Selection / comparison
Option
Best for
Trade-off
Stamped 6063-T5 heat sink
High-volume switch-mode power supply programs
Requires 250 T tooling; limited to 0.5 mm fin profile
Extruded heat sink
Lower-volume or simpler fin geometries
Cannot hold 0.5 mm fin profile; pitch varies more than ±0.03 mm
Machined heat sink
Prototype or low-volume complex shapes
Higher part cost; anodize can be cut through at fin roots
Brazed fin heat sink
Applications needing mixed materials
Brazed joint can fail; no one-piece construction
Process / inspection
Stage
Control
Record
Stamping
250 T stroke forms base and fins in one piece; 25 s cycle
±0.03 mm fin pitch; ±0.15 mm hole position
Flatness
Mounting face held directly from tool
0.05 mm over 100 mm
Surface finish
Black anodize Type II applied after forming
10-15 µm thickness
Inspection
Before every shipment
Dimensional and visual checks per batch
Thermal performance
Natural convection at ΔT = 60 K
0.48 K/W
Frequently Asked Questions
What is the thermal resistance of this high precision heat sink?
It returns 0.48 K/W at ΔT = 60 K under natural convection. This is achieved with a 2.0 mm base and 0.5 mm fins pressed from 6063-T5 aluminium on 250 T tooling, holding 0.05 mm over 100 mm flatness for uniform thermal interface contact.
How tight is the fin pitch tolerance on your stamped heat sink?
Fin pitch stays within ±0.03 mm across an 800,000 pcs run. The 250 T die forms every fin in one stroke, so pitch is repeatable. This is tighter than extrusion can hold for a 0.5 mm fin profile, ensuring consistent airflow and thermal performance.
Can you hold 0.05 mm flatness on the mounting face?
Yes. The 0.05 mm over 100 mm flatness is held directly from the tool on the mounting face. Because the base and fins are pressed as one piece, there is no brazed joint to distort. This keeps thermal interface contact uniform and repeatable.
What is the monthly production capacity for this heat sink?
Monthly output runs at 800,000 pcs. The 25 s cycle on a 250 T line feeds this volume. Every stroke is dimensionally identical, so ±0.15 mm hole position carries across the batch. This makes switch-mode power supply volume programs repeatable.
We apply black anodize Type II, 10-15 µm, after forming. This protects corrosion resistance without cutting through at the fin roots, unlike machined alternatives. The finish is uniform because the part is pressed as one piece, with no brazed joints to mask or degrade.
Is the heat sink made from one piece or assembled?
It is pressed as one piece from 6063-T5 aluminium. The base and fins are formed in a single 250 T stroke, so there is no brazed joint to fail. This one-piece construction also eliminates joint thermal resistance and maintains 0.5 mm fin profile repeatability.
What is the cycle time and how does it affect lead time?
The cycle time is 25 s per stroke on a 250 T line. This feeds an 800,000 pcs monthly output. Lead time depends on order quantity and tooling availability, but the high-speed stamping process supports volume programs with repeatable ±0.03 mm fin pitch and ±0.15 mm hole position.
0.05 mm over 100 mm flatness; 0.5 mm fin pitch within ±0.03 mm
Lead time
Not specified in article
MOQ
Not specified in article
Capacity
800,000 pcs monthly output; 25 s cycle
Selection / comparison
Option
Best for
Trade-off
Stamping
Repeatable 0.5 mm fin profile with ±0.03 mm pitch across 800,000 pcs run
Requires 250 T tooling; limited to sheet thicknesses formable in one stroke
Extrusion
Longer parts with uniform cross-section
Cannot hold 0.5 mm fin profile as repeatably; pitch variation higher
Brazed assembly
Complex geometries with separate base and fins
Brazed joint can fail; additional process steps and cost
Frequently Asked Questions
What is the flatness tolerance of the mounting face?
The mounting face holds 0.05 mm over 100 mm flatness directly from the 250 T tool. This ensures uniform thermal interface contact. Inspection before every shipment verifies this tolerance.
What is the fin pitch and its tolerance?
The fin pitch is 0.5 mm with a tolerance of ±0.03 mm. Stamping forms every fin in one stroke, so pitch stays within ±0.03 mm across an 800,000 pcs run.
What is the thermal performance of this heat sink?
It delivers 0.48 K/W at ΔT = 60 K in natural convection. This performance is achieved with 6063-T5 aluminium and a 2.0 mm base and 0.5 mm fins.
What material and surface finish are used?
The heat sink is pressed from 6063-T5 aluminium. It receives black anodize Type II, 10-15 µm, which protects fin roots after forming.
What is the production capacity and cycle time?
Monthly output runs at 800,000 pcs. The 25 s cycle on 250 T tooling feeds this 800,000 pcs line, ensuring consistent production.
Why is stamping preferred over extrusion for this heat sink?
Stamping gives a repeatable 0.5 mm fin profile that extrusion cannot hold. The die forms every fin in one stroke, so pitch stays within ±0.03 mm across an 800,000 pcs run, and there is no brazed joint to fail.
Inspection before every shipment verifies flatness, fin pitch, and surface finish. The 0.05 mm over 100 mm flatness and ±0.03 mm fin pitch are checked to ensure they meet specifications.