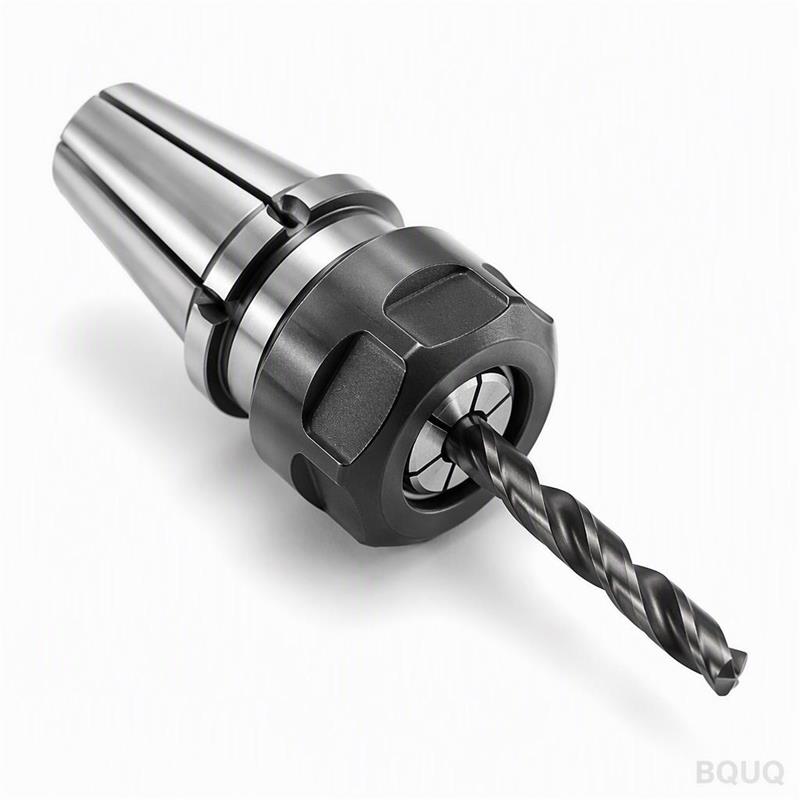
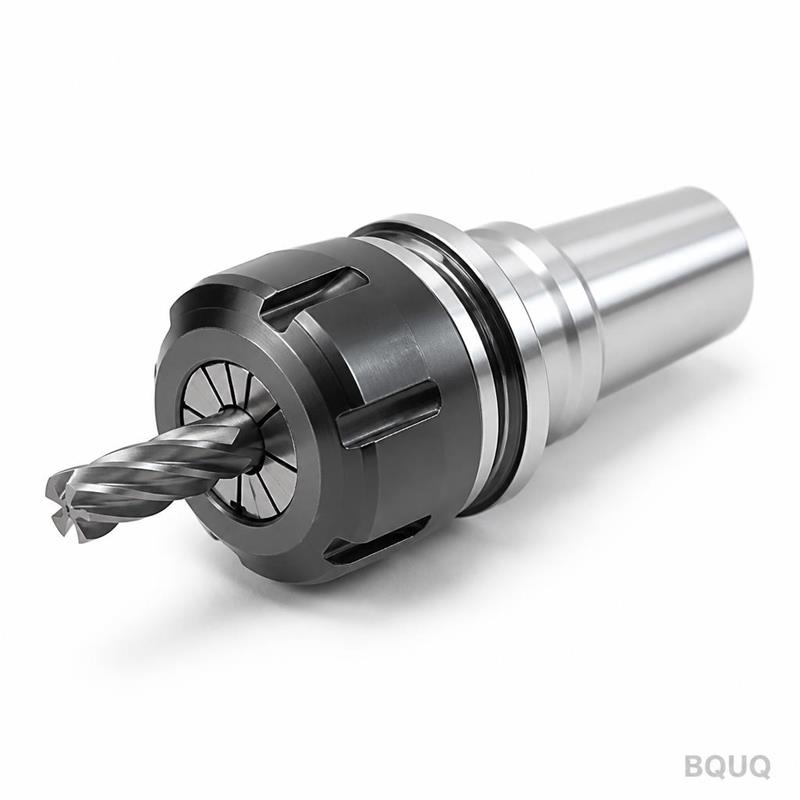
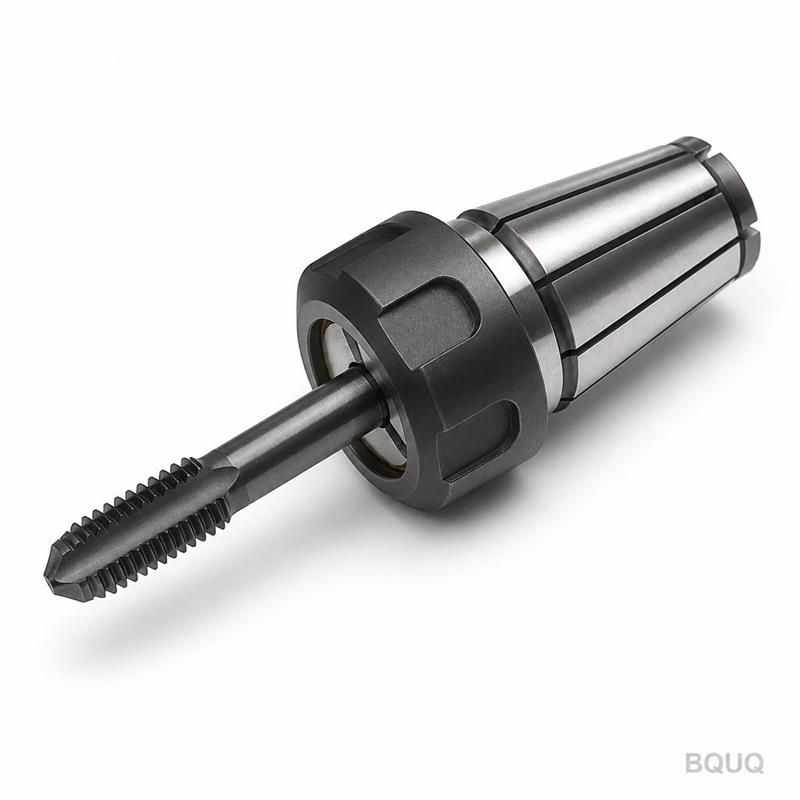
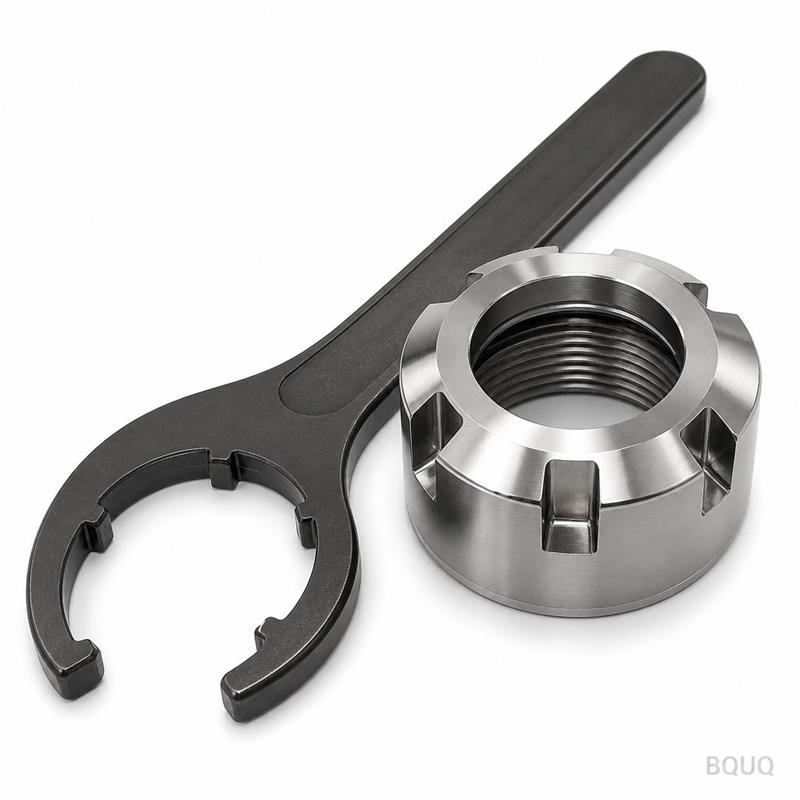
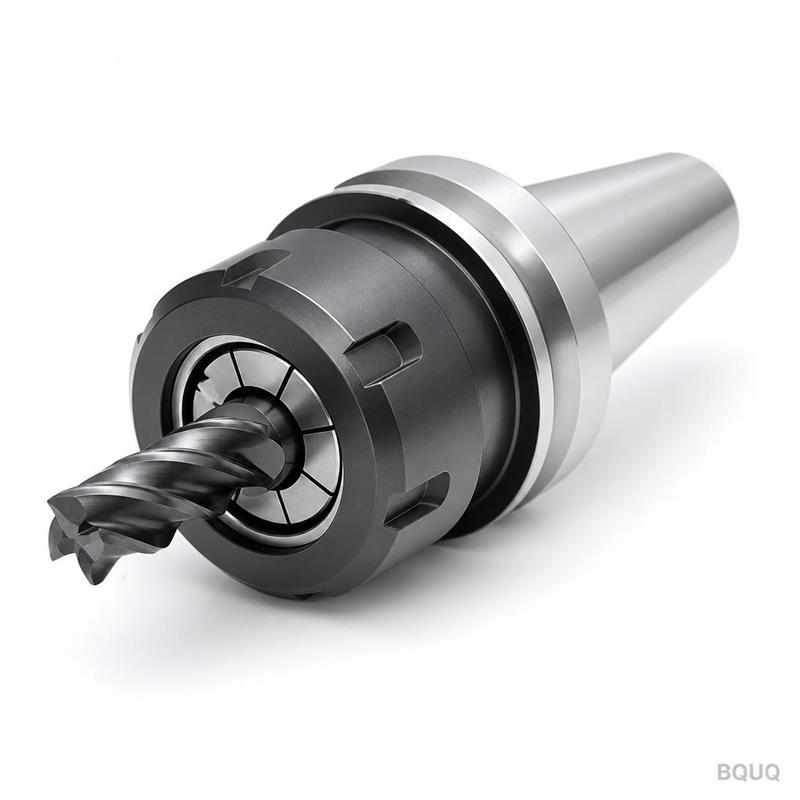
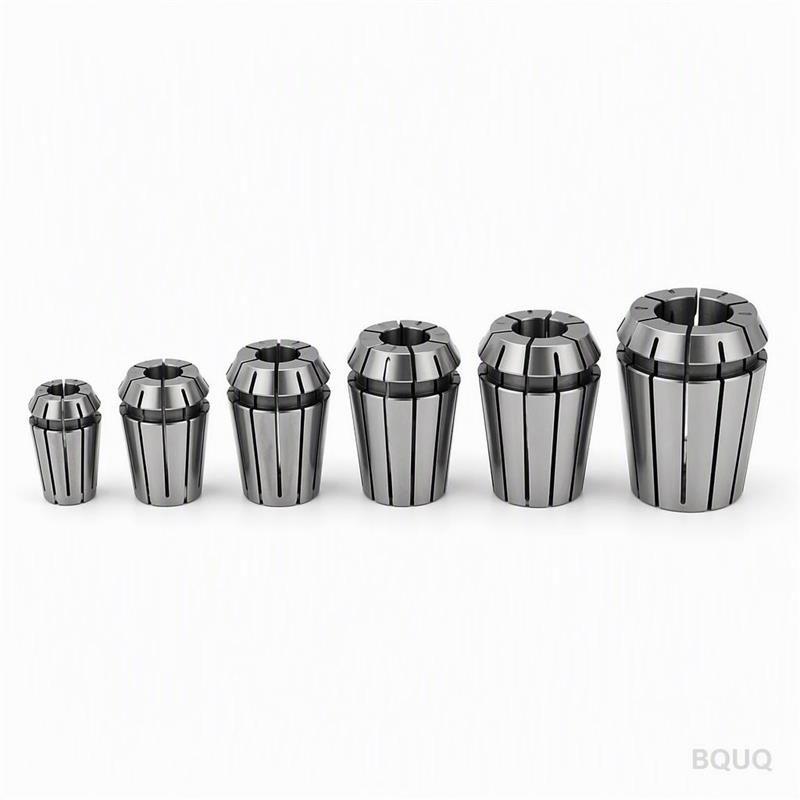
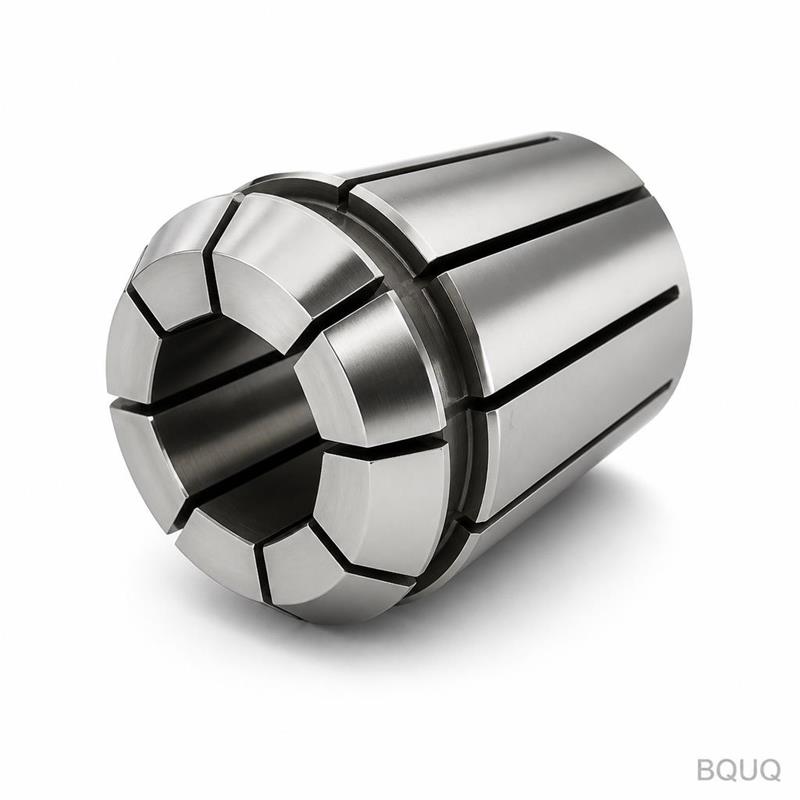
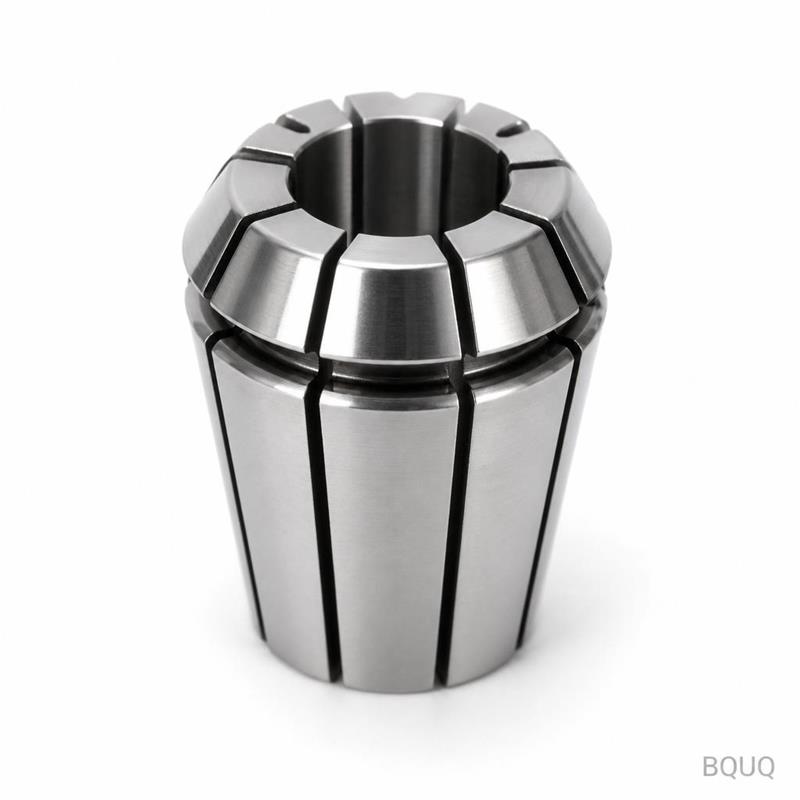
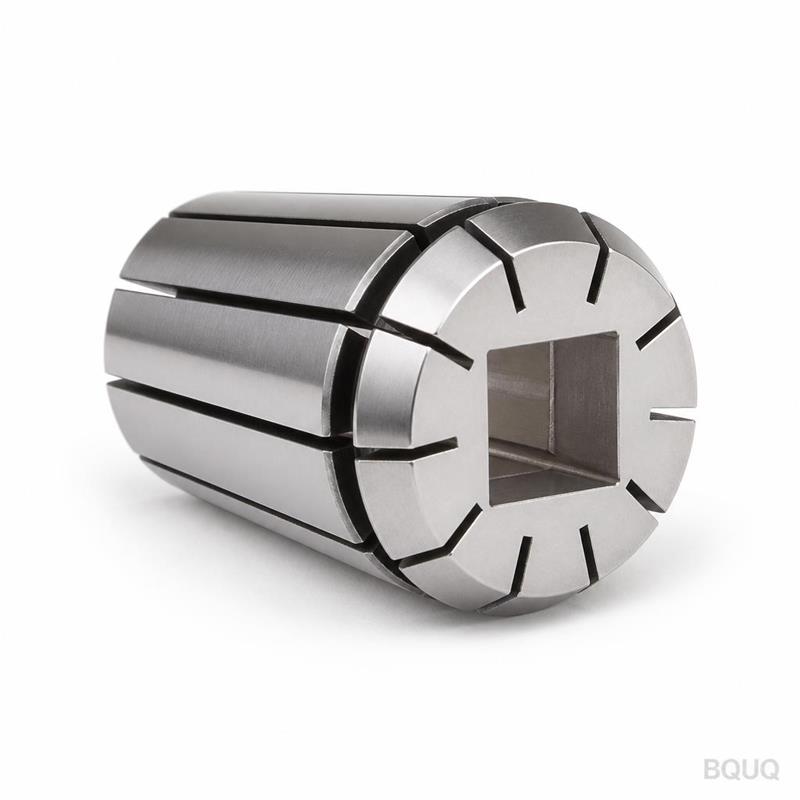
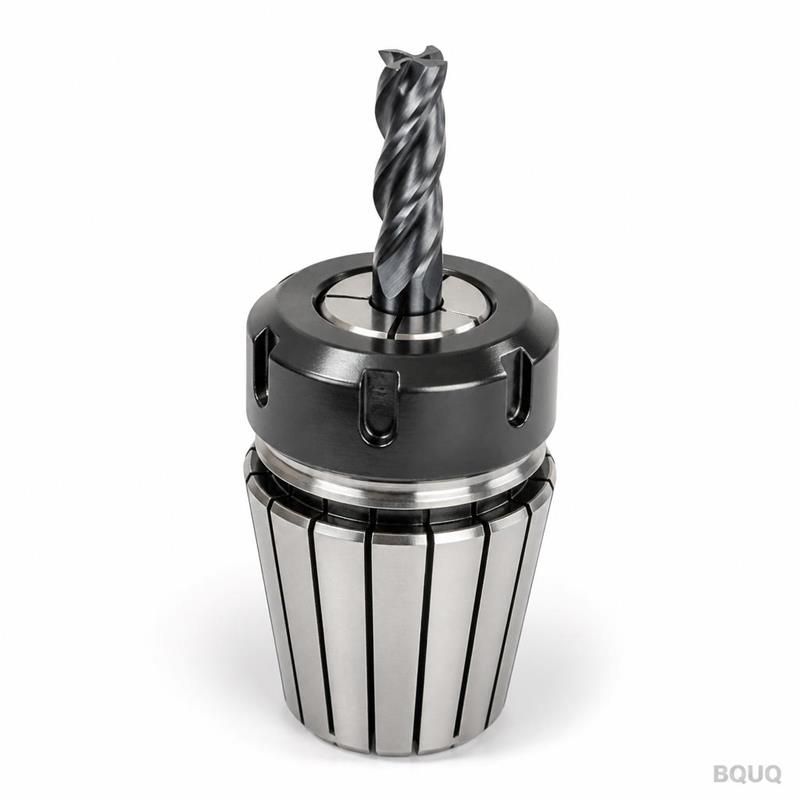
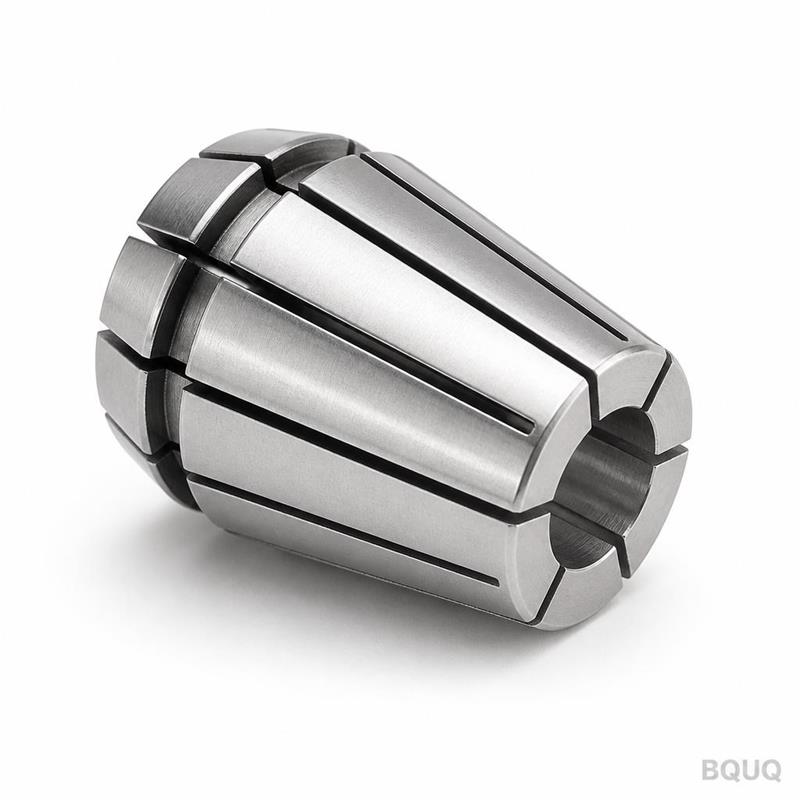
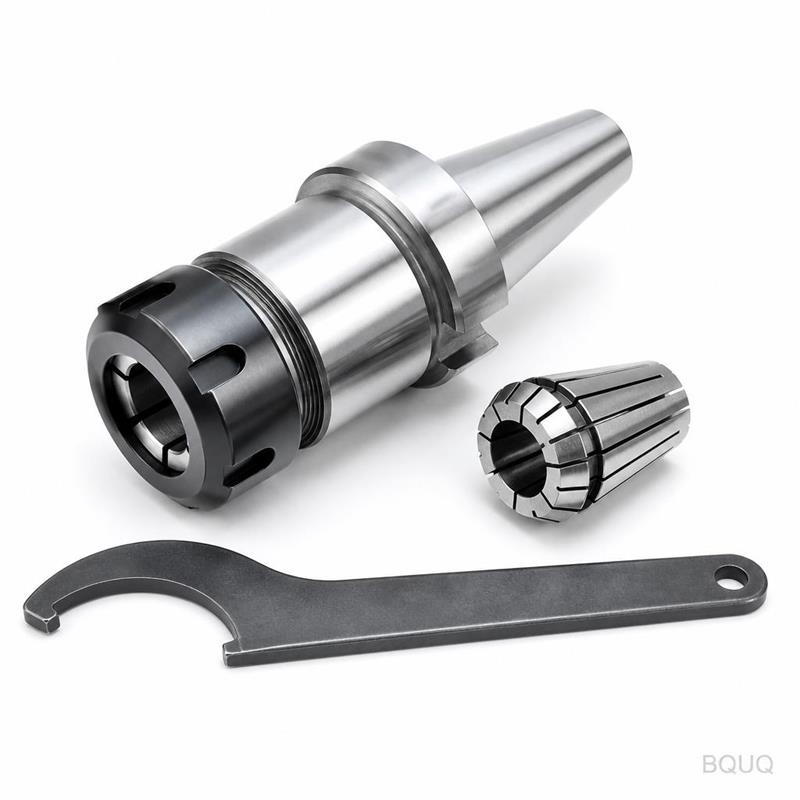
Custom CNC Collet Chuck ER16 with Drill Bit, Made in China
OpeningYour drawing defines the part. We machine it exactly to that geometry. Every ER16 collet chuck is inspected before shipment. We do not ship guesswork.Tolerance: ±0.005 mm on critical diametersR
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your drawing defines the part. We machine it exactly to that geometry. Every ER16 collet chuck is inspected before shipment. We do not ship guesswork.
Tolerance: ±0.005 mm on critical diameters
Runout: ≤0.005 mm TIR at nose
Material: 20CrMnTi or 42CrMo, case-hardened to 58–62 HRC
Lead time: 7–12 days for standard batches
No MOQ – order one piece or one thousand
Made in China, Dongguan factory, 20 years in precision manufacturing
Specifications
Parameter
Value
Notes
Standard
ER16 collet taper, 1:10 angle
Matches ER16 collet spec
Shank diameter
19.05 mm or custom
Per your drawing
Shank tolerance
h6
Ground finish
Concentricity
≤0.005 mm TIR
Between taper and shank
Surface finish
Ra 0.4 µm on taper
Ground, not turned
Hardness
58–62 HRC
Case-hardened
Case depth
0.8–1.2 mm
Consistent, no soft spots
Material
20CrMnTi, 42CrMo, or 65Mn
Your choice
Threads
M12, M16, or custom
Tapped after hardening
Key slots
Per drawing
Broached or wire-cut
Batch size
1–10,000 pcs
No MOQ
Inspection
100% dimension check on criticals
Report included
Process: CNC turning of the blank, heat treatment, then cylindrical grinding for the taper and shank. We use Mazak and Okuma CNC lathes. Grinding is done on Studer or Jones & Shipman machines. This is not a milled-only part. The taper is always ground.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Each heat number and batch is logged. If a problem appears in your assembly, we trace it back to the exact material lot and machine operator. No ambiguity. This matters when you run a production line and need answers fast.
2. Inspection report per batch. You get a dimensional report with every shipment. Not a generic certificate – actual measured values for taper angle, runout, hardness, and surface finish. We use CMM and optical comparators. The report is signed by our QC lead, not a computer.
3. One factory for CNC + stamping + spring + heatsink. Your collet chuck is not the only part in your tool holder. If you also need a spring for the collet retention, a stamped washer, or a heatsink for a spindle motor, we make those in the same building. Fewer vendors, shorter lead times, one point of contact. You send a full assembly drawing, we quote the whole kit.
Where these parts are used
These collet chucks are not for hobby routers. They go into production drilling and milling spindles.
Automotive transfer lines: Drilling holes in engine blocks and cylinder heads. The ER16 chuck holds a twist drill at high RPM. Runout must be low to avoid oversize holes.
CNC machining centers: Used for through-coolant drilling. The collet chuck has internal coolant channels per your drawing. We machine the channels before hardening.
PCB drilling machines: High-speed spindles at 80,000 RPM. The ER16 taper is ground to tight concentricity to prevent drill breakage.
Aerospace fixture drilling: Manual drilling of aircraft skins. The chuck must be lightweight and repeatable. We use 7075 aluminum bodies with a hardened steel insert if you specify that.
Robotic end-of-arm tooling: Automated drilling cells. The chuck is mounted on a robot wrist. Our shank tolerance ensures no vibration at high feed rates.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototype validation. The price per piece is higher for a single unit, but the quality is identical to a batch of 500. Many buyers start with one, test it, then order 200.
Q: How do you guarantee tolerance and runout?
A: We grind the taper and shank in the same setup on a cylindrical grinder. This eliminates setup error. Then we measure runout on a precision V-block with a 0.001 mm indicator. The inspection report shows the actual value. If it exceeds 0.005 mm TIR, we reject it.
Q: What is your lead time?
A: 7 days for standard ER16 chucks in 42CrMo. 12 days if you need case-hardened 20CrMnTi with a specific case depth. For urgent orders, we can do 5 days with a 20% rush fee. We do not quote faster than we can actually deliver.
Q: Can you provide material certificates?
A: Yes. We supply EN 10204 3.1 mill certificates for the raw material. For aerospace or medical applications, we can also provide full traceability to the heat number and batch. Just specify the standard you need in your RFQ.
Send your drawing
Email your PDF or STEP file to sc@bquq.com. We reply with a firm quote in 12 hours. Not a ballpark – a fixed price with tolerance, surface finish, and lead time. You can also reach us on WhatsApp at +86 13713157787 for a quick technical discussion.
We are a 20-year-old precision manufacturing factory in Dongguan, China. We do not outsource. We machine, grind, heat-treat, and inspect in-house. Send your drawing. Get a quote. Get a part that fits.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.