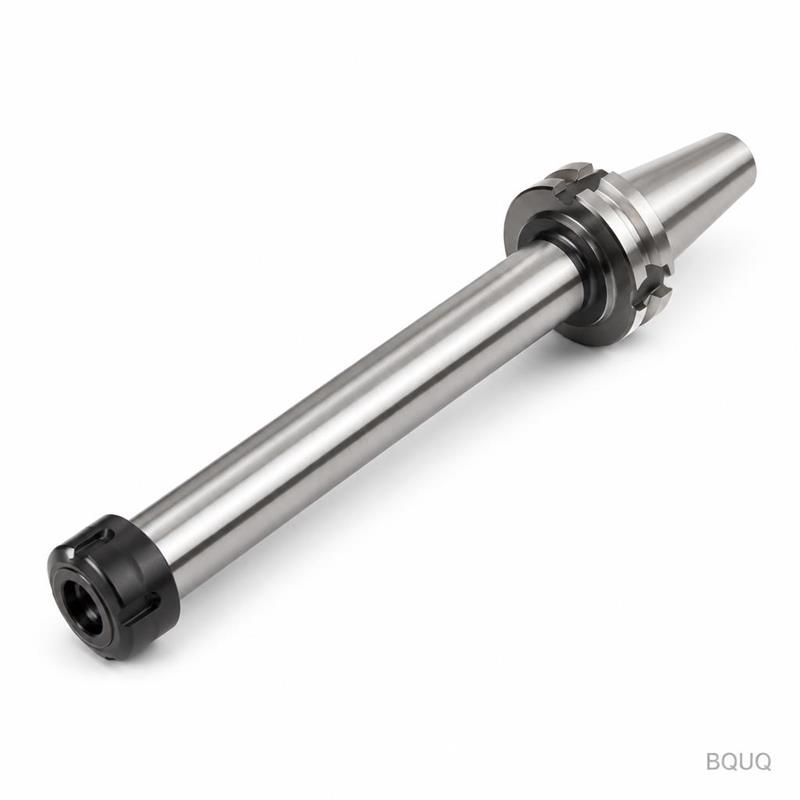
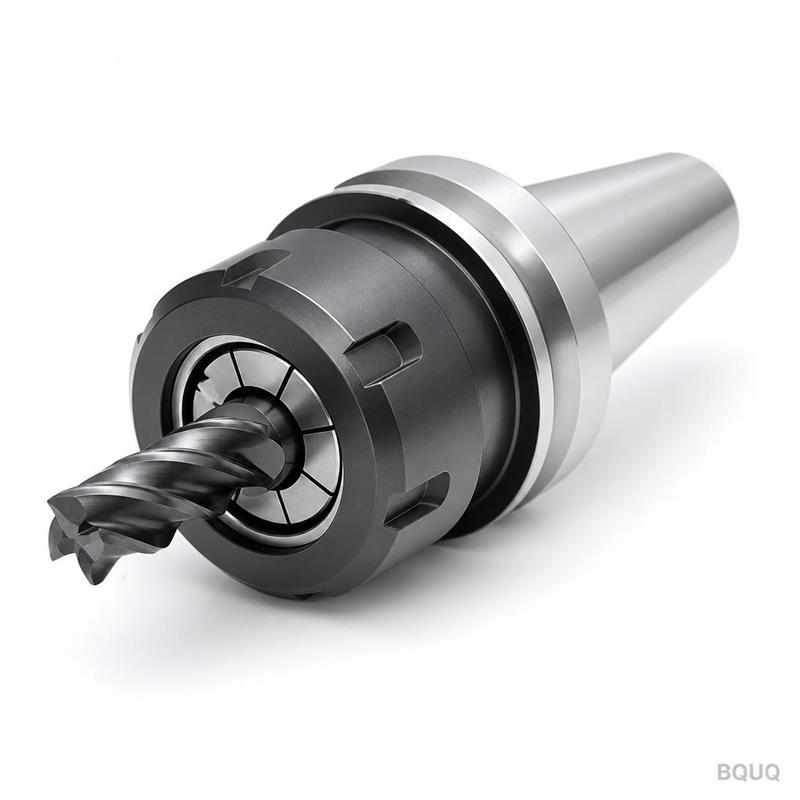
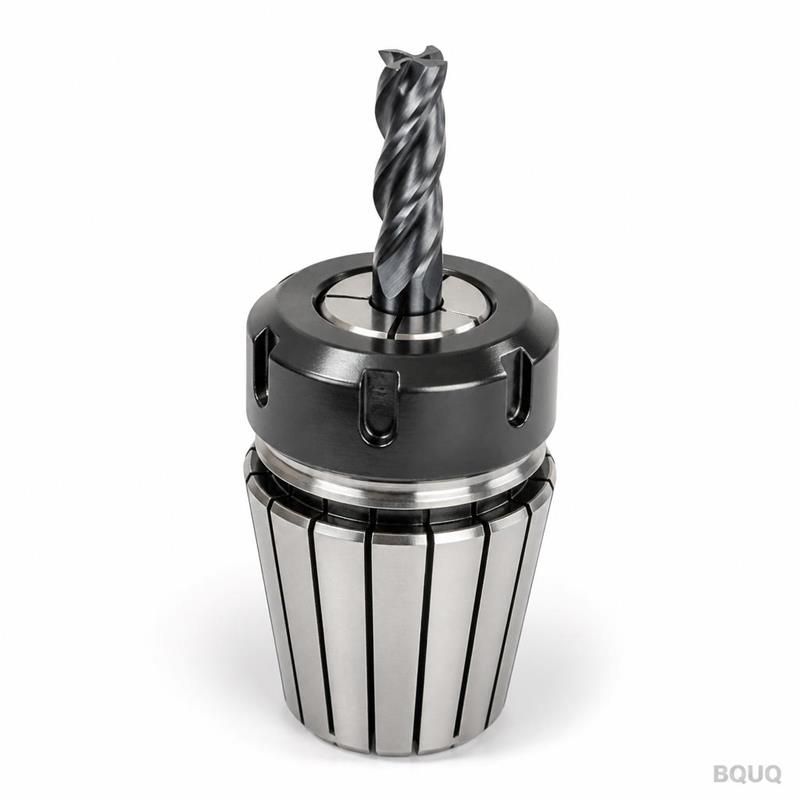
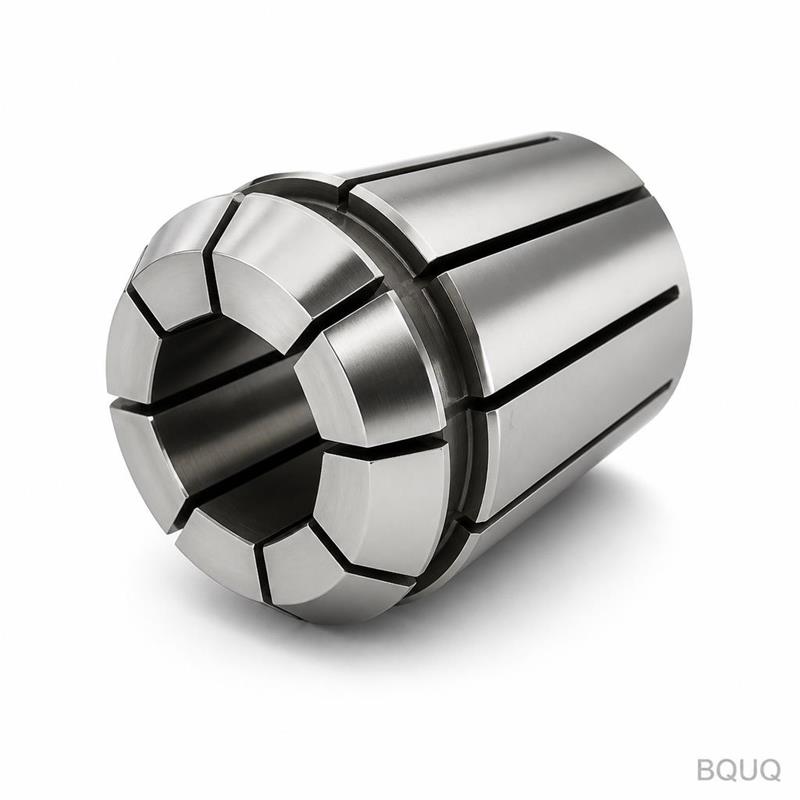
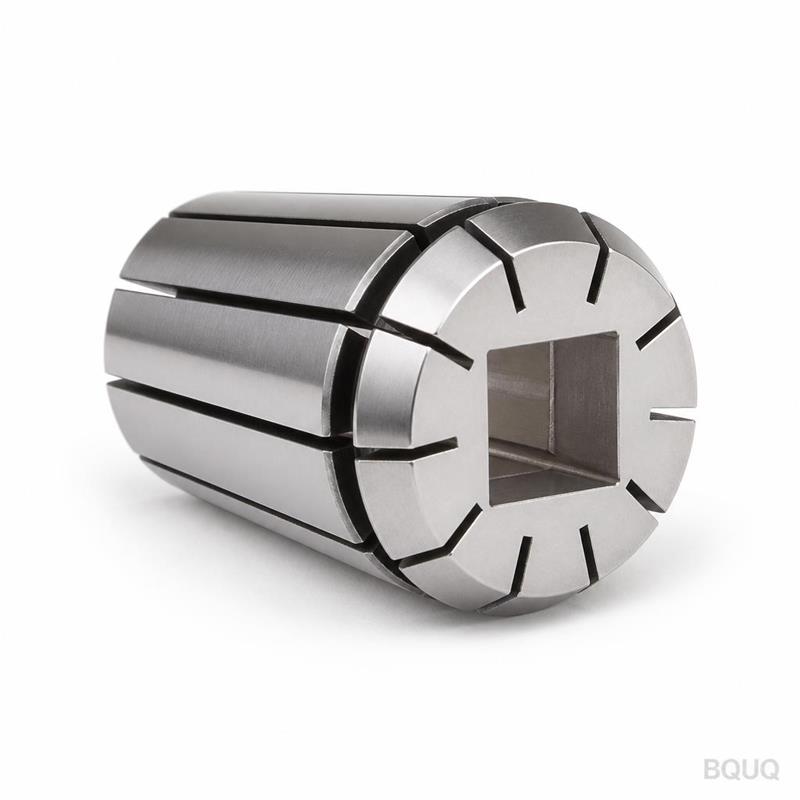
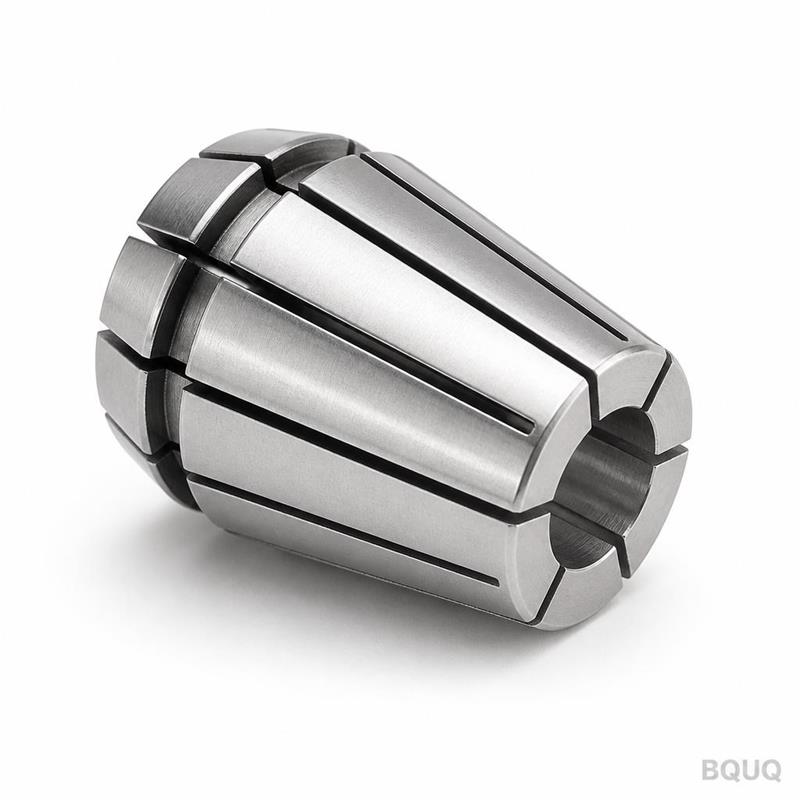
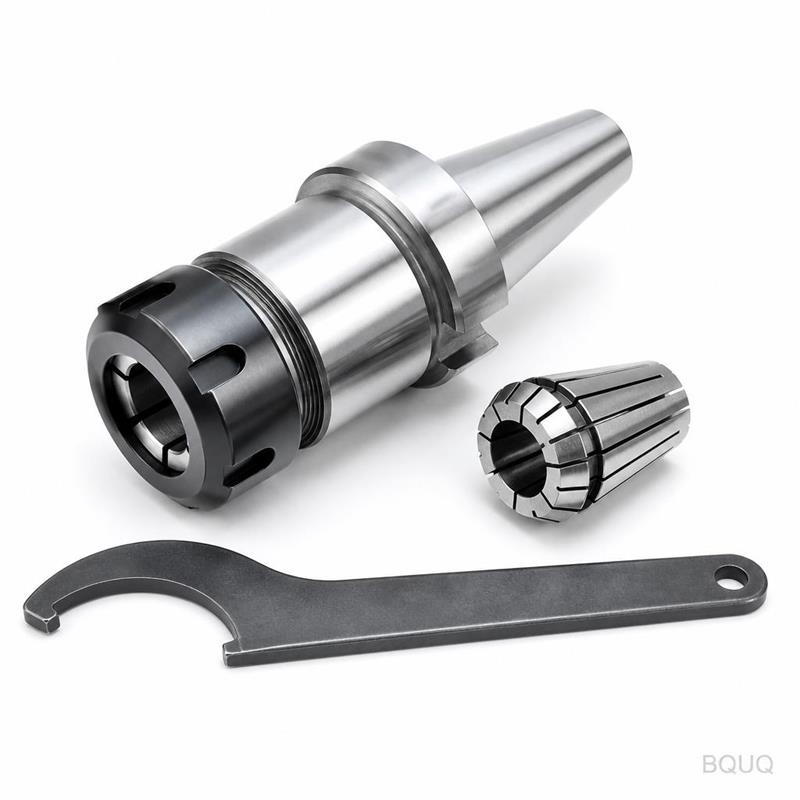
Custom CNC Machined ER20 Spring Collet Chuck Precision Tooling No MOQ
OpeningWe machine ER20 spring collets to your exact drawing. Not from stock blanks. Not modified from standard sizes. We start from bar stock and cut every profile, slot, and taper to your specified d
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
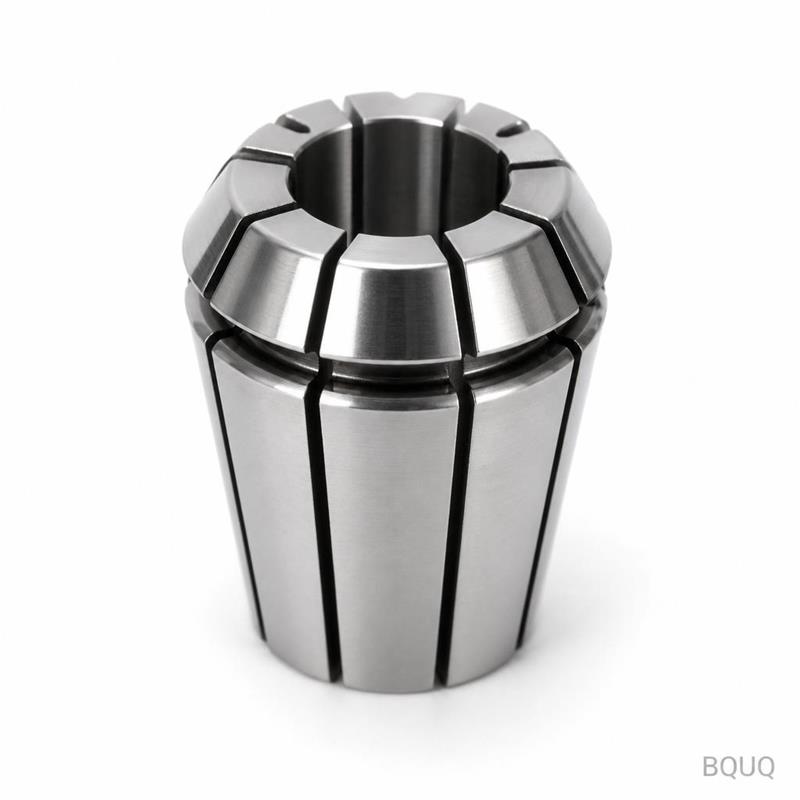
We machine ER20 spring collets to your exact drawing. Not from stock blanks. Not modified from standard sizes. We start from bar stock and cut every profile, slot, and taper to your specified dimensions.
Each collet is verified before shipment. We check the critical taper angle, slot width, and concentricity on a CMM. You get the numbers, not just a "passed" stamp.
At a glance: Tolerance ±0.005 mm on the bore, surface finish Ra 0.4, lead time 7–12 days, no MOQ. One collet or one thousand, same process.
Specifications
Parameter
Value
Material options
65Mn spring steel, 60Si2MnA, 9Cr18 stainless, or per drawing
Hardness
HRC 45–52 (through-hardened, not case-hardened)
Taper angle
8° per side, verified with air gauge
Bore tolerance
H5 (+0.008 / 0) or tighter per drawing
Concentricity
≤ 0.005 mm TIR at nose
Surface finish
Ra 0.4 on taper, Ra 0.8 on slots
Slot width
±0.02 mm, burr-free edges
Process
CNC turning, CNC milling, wire EDM for slots, heat treatment
Heat treatment
Vacuum hardening, no decarb layer
Batch size
1 to 10,000 pieces
Inspection
100% taper check, 30% full dimension report per batch
Lead time
7 days for prototypes, 12 days for production
We use 5-axis CNC turning centers for the taper and bore. Slots are cut with wire EDM to avoid tool deflection. Heat treatment is done in-house in a vacuum furnace, so we control the hardness curve, not a subcontractor.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Every collet gets a heat treatment lot number. We record the furnace cycle, the material heat number, and the final hardness reading. If you have a problem at tool #47, we can pull the exact batch record and tell you the hardness, the taper measurement, and the operator. No guesswork.
2. Inspection report per batch. You do not have to ask for it. Each shipment includes a dimensional report with actual measured values for taper angle, bore diameter, slot width, and concentricity. We use a Zeiss CMM and a calibrated air gauge. The report is signed by QC, not generated by software.
3. One factory for CNC, stamping, springs, and heat sinks. This is precision manufacturing with no middlemen. Your collet chuck assembly might need a spring, a stamped retainer, or a heat sink for the spindle drive. We make all of them under one roof. You send one drawing package, get one quote, one set of QC reports, and one shipment. Fewer vendors, fewer tolerance stack-ups, fewer arguments.
Where these parts are used
ER20 collets are the workhorse of high-speed machining centers and CNC lathes. Typical applications:
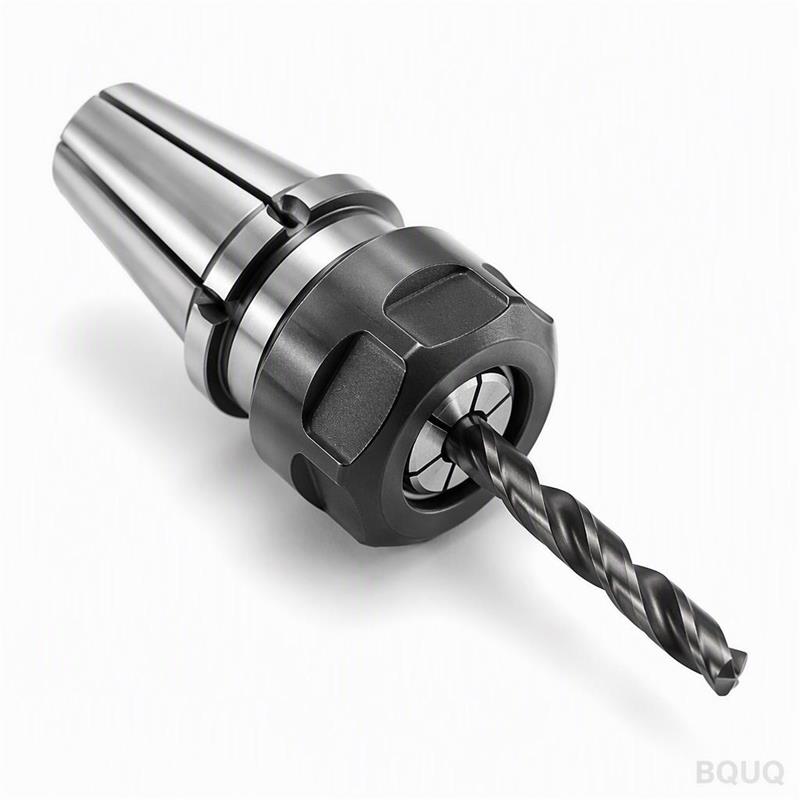
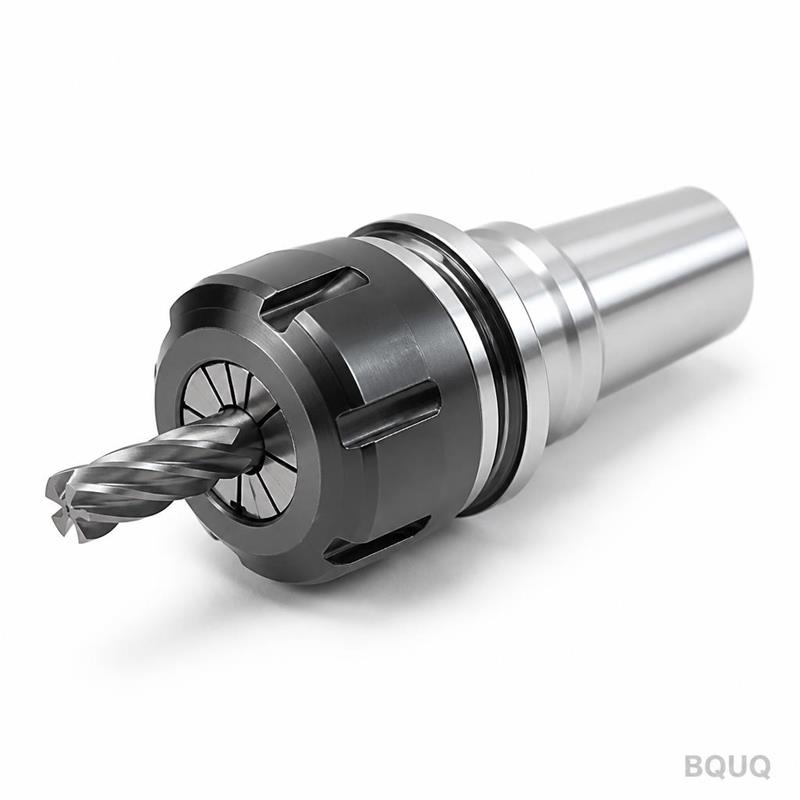
Tool holding on milling spindles – 1–13 mm shank tools, runout-sensitive finishing operations.
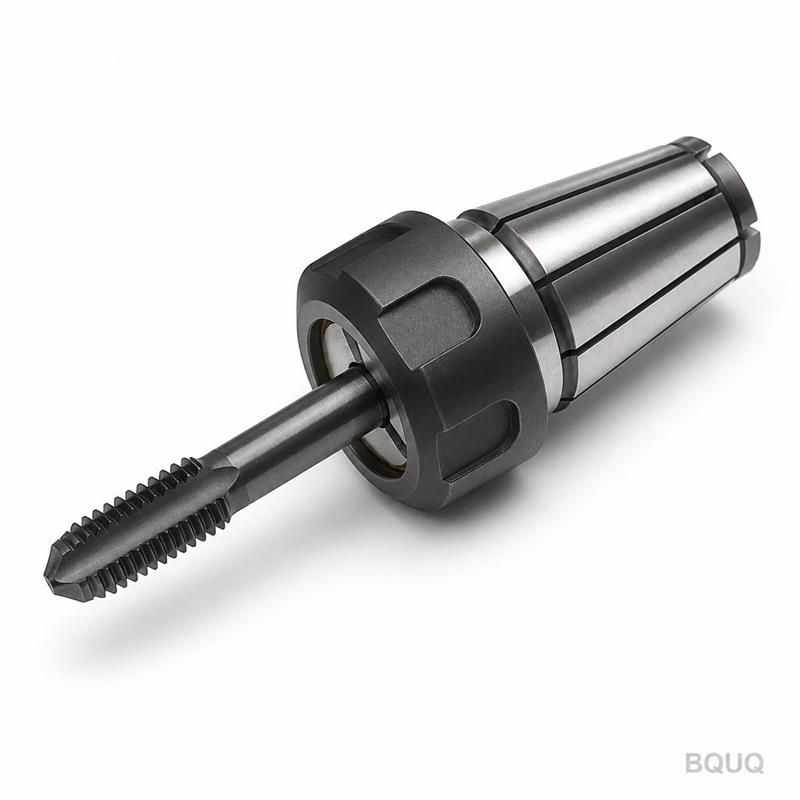
Drilling and reaming – where a hydraulic chuck is overkill but a standard drill chuck cannot hold concentricity.
Swiss-type lathes – guide bushings and main spindle collets for bar stock up to 20 mm diameter.
Automotive valve seat machining – production lines that run 24/7 and need repeatable tool change without re-setting offsets.
Aerospace aluminum and titanium – where tool pull-out under heavy radial load is not acceptable.
We also make custom ER20 variants: longer noses for deep reach, slotted versions for coolant-through, and hardened steel versions for high-clamping-force applications. If your drawing says "ER20 but different," we can make it.
Q: What is the MOQ?
A: No MOQ. We quote and make one piece. The per-piece price for a single collet is higher than for 100 pieces, but the process is identical. We do not batch small orders with other customers' work.
Q: How do you guarantee tolerance and quality?
A: The taper angle is measured with an air gauge, not a comparator. The bore is measured with a bore gauge calibrated to NIST standards. Each batch gets a written inspection report. If any dimension is out of spec, we scrap the part, not ship it.
Q: What is the lead time for a custom CNC collet chuck?
A: Prototype (1–5 pieces) is 7 days. Production (50+ pieces) is 10–12 days. Heat treatment adds 2 days, but it is included in those numbers. We do not quote "up to 4 weeks" to be safe. We quote what we can deliver.
Q: Can you provide material certificates?
A: Yes. We supply mill certificates for the raw material, heat treatment reports with actual hardness curves, and a certificate of conformity. All documents are in English. We can also provide third-party inspection (SGS or BV) at your cost.
Send your drawing
Email your PDF or STEP file to sc@bquq.com. Include the material, hardness, and quantity if you know them. If you do not, we will recommend based on your application.
We reply with a firm quote in 12 hours. Not a "budget range." A fixed price per piece, tooling cost (if any), and delivery date.
For urgent projects, WhatsApp us at +86 13713157787. We answer 7 days a week, 8:00–22:00 Beijing time.
Custom CNC collet chuck, made in China, with no MOQ and no surprises. Send the drawing. Get the quote.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.