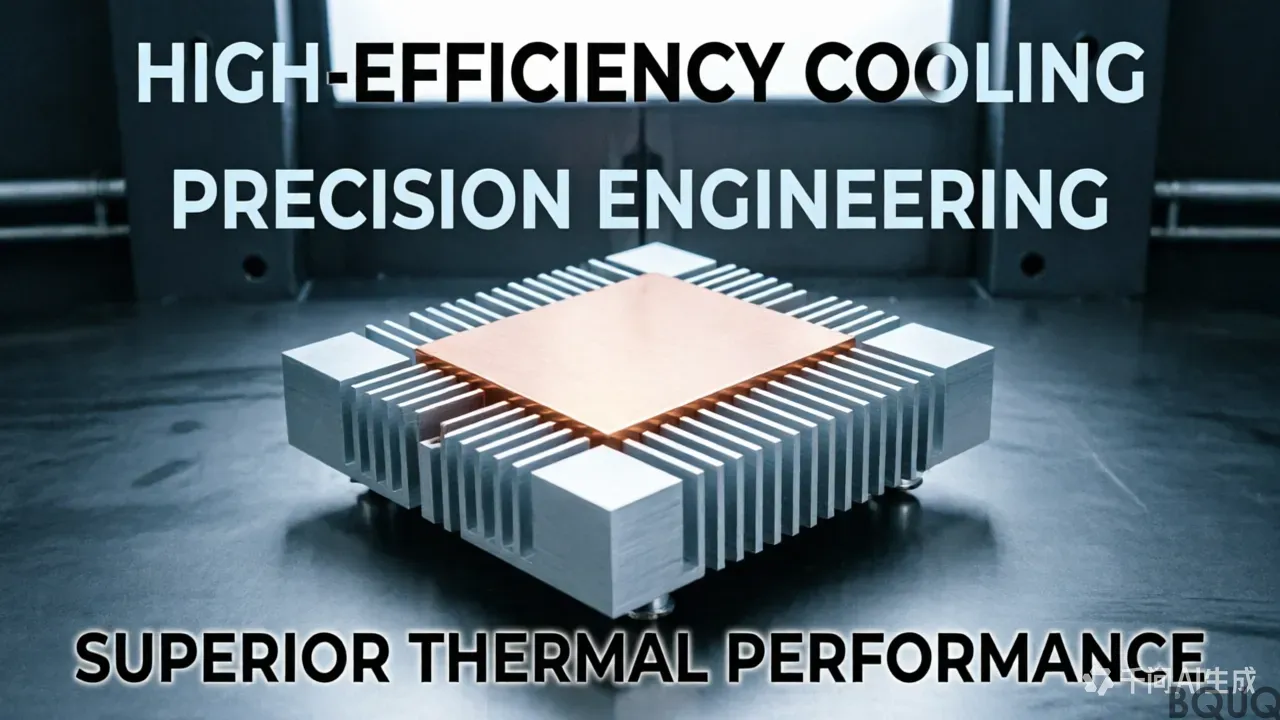
heat sink compound: pure copper C110, tolerance 0.20 mm, surface black anodize Type II, 10-15 µm, lead time 20 working days, MOQ 1000 pcs. Capacity 300,000 pcs for 1U server and AI accelerator. Drawing review and first-article report included.
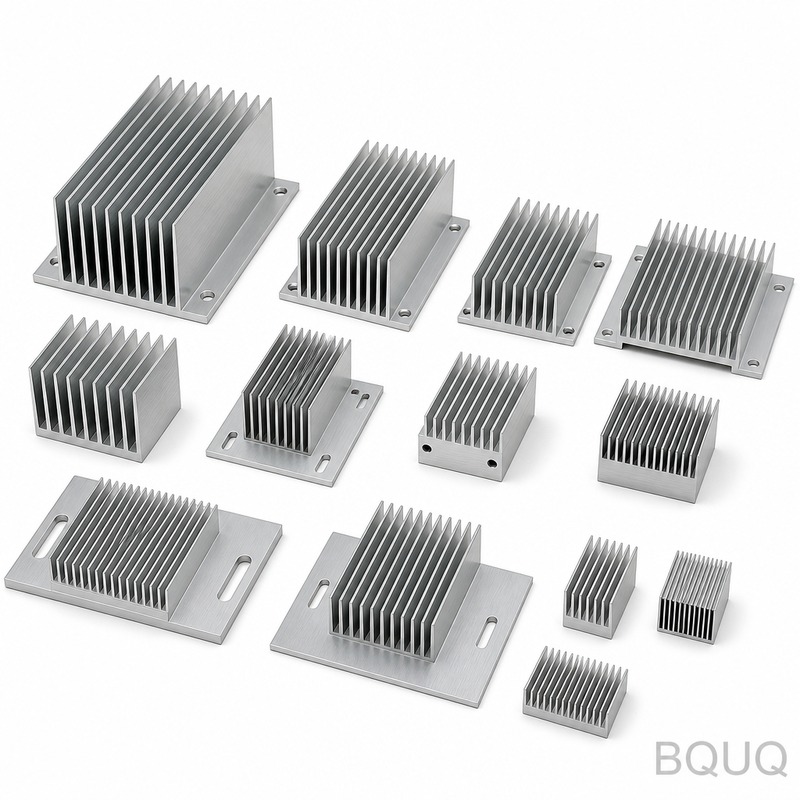
heat sink compound
Key Takeaway
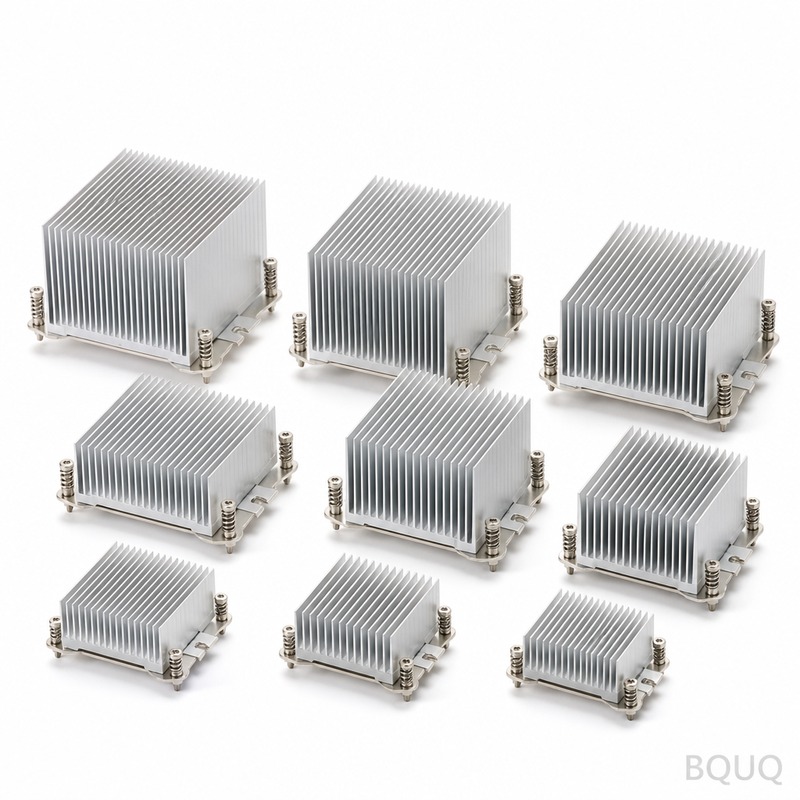
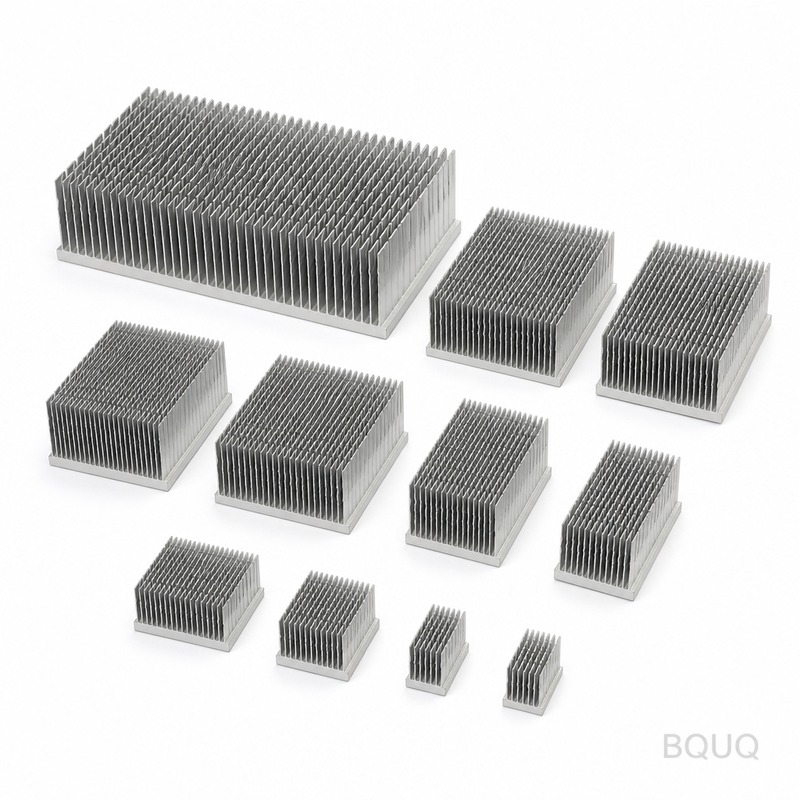
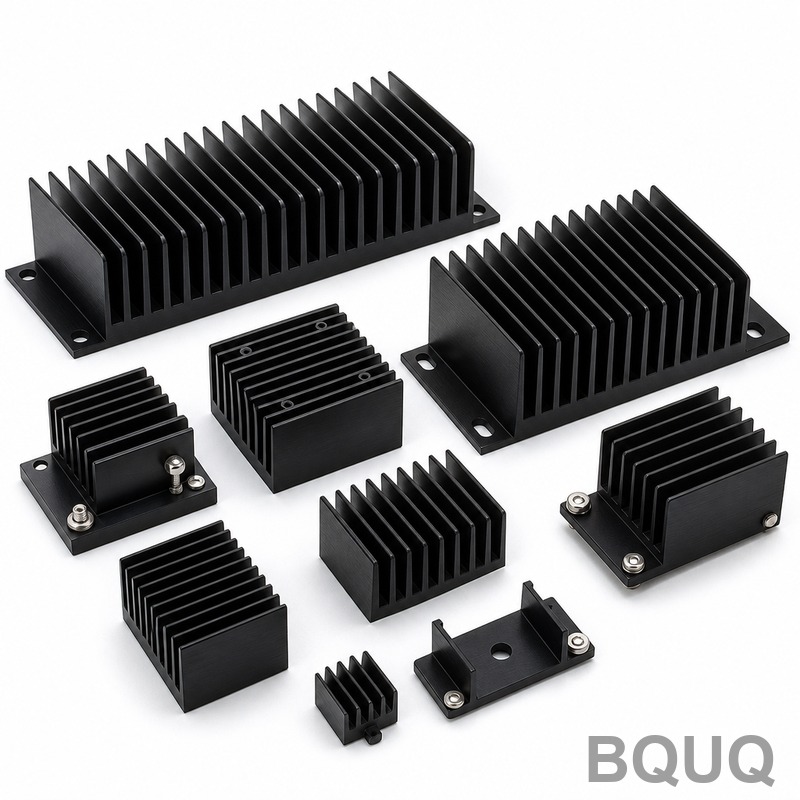
Heat sink compound is a 1050A aluminium heatsink with 0.8 mm fin thickness, 1.5 mm fin pitch, and 0.85 K/W thermal resistance. It uses hard anodize Type III, 25-40 µm, and holds ±0.20 mm general tolerance. Lead time can be 10 working days for 50 to 50,000 pieces, with cost driven by deburring, plating, and inspection.
Whether you need 50 pieces for validation or 50,000 for a production line, heat sink compound follows the same physics. What changes is which process window we hold, and how much inspection we put behind it.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | 1050A aluminium |
| Fin thickness | 0.8 mm |
| Fin pitch | 1.5 mm |
| Thermal resistance | 0.85 K/W |
| Surface finish | hard anodize Type III, 25-40 µm |
| General tolerance | ±0.20 mm |
Market and Technical Context
Lead time pressure has compressed across VFD and inverter. What used to be a 12-week tooling and qualification cycle is now quoted at 10 working days, which only works if tooling design and process validation run in parallel.
Cost pressure in VFD and inverter rarely comes from the raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
Related reading: Presetting and Scragging Springs: Settling Load Before Delivery.
How We Manufacture It
The route for heat sink compound starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.20 mm is held at production speed rather than on a single slow part.
Tooling is designed around the measured capability of the process, so ±0.20 mm is a consequence of tooling geometry rather than an inspection filter. That is why 10 working days is realistic instead of optimistic.
Deburring and edge conditioning are specified on the drawing for heat sink compound. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Material and Surface Finish
Material condition matters as much as grade. 1050A aluminium supplied in the wrong temper will drift after machining, which is why heat sink compound is stress-relieved before finishing when the geometry is asymmetric.
Surface specification for heat sink compound is hard anodize Type III, 25-40 µm, chosen for the service environment in VFD and inverter. Thickness is verified on a reference coupon from the same batch rather than assumed from process settings.
Where heat sink compound sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Tolerance and Inspection
General dimensions on heat sink compound are held to ±0.20 mm; critical features are identified on the drawing and controlled separately with a tighter band.
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so heat sink compound drawings state how each critical dimension is verified.
See also: heat sink for ssd.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on heat sink compound, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Where It Is Used
VFD and inverter is the largest application area for heat sink compound, where the part typically sees continuous load and a wide temperature range rather than laboratory conditions.
Retrofit requests are common: an existing assembly needs heat sink compound in a slightly different size. Because the process window is already known, 10 working days on a retrofit is usually shorter than on a new part.
What to Confirm Before Ordering
Define critical features at quote stage. Moving a feature from general ±0.20 mm to critical after tooling adds cost and extends 10 working days, which is the most avoidable delay in custom sourcing.
Learn more about Stamped Heat Sinks vs Extruded: When Does Metal Stamping Make Sense for Cooling?.
Compare quotes on the same basis: material grade, hard anodize Type III, 25-40 µm, inspection scope, and packaging. A lower unit price that drops 100% inspection is not a lower total cost.
Further technical detail: What Are the Standard Heat Sink Mounting Hole Patterns and Best Practices?.
FAQ: Your Questions Before Ordering
What tolerance can you hold on heat sink compound?
Standard lead time for heat sink compound is 10 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Recommended reading: Precision CPU Heat Sink Manufacturing.
What is the minimum order quantity for heat sink compound?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.20 mm would require an extra operation, so you can decide before tooling.
How long does production take for heat sink compound?
hard anodize Type III, 25-40 µm is standard for heat sink compound. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
Compare it with Custom CNC Collet Chuck Auto Lathe Double Ended Precision Made in China.
Do you provide material and inspection certificates?
Yes, and we recommend it. Prototyping heat sink compound without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of heat sink compound remains usable.
If heat sink compound is already in production elsewhere, send a sample and the current drawing. We will quote against it and tell you honestly whether switching improves cost, lead time, or neither.
Related reading: BQUQ Round Radial Aluminum Heatsink Collection.
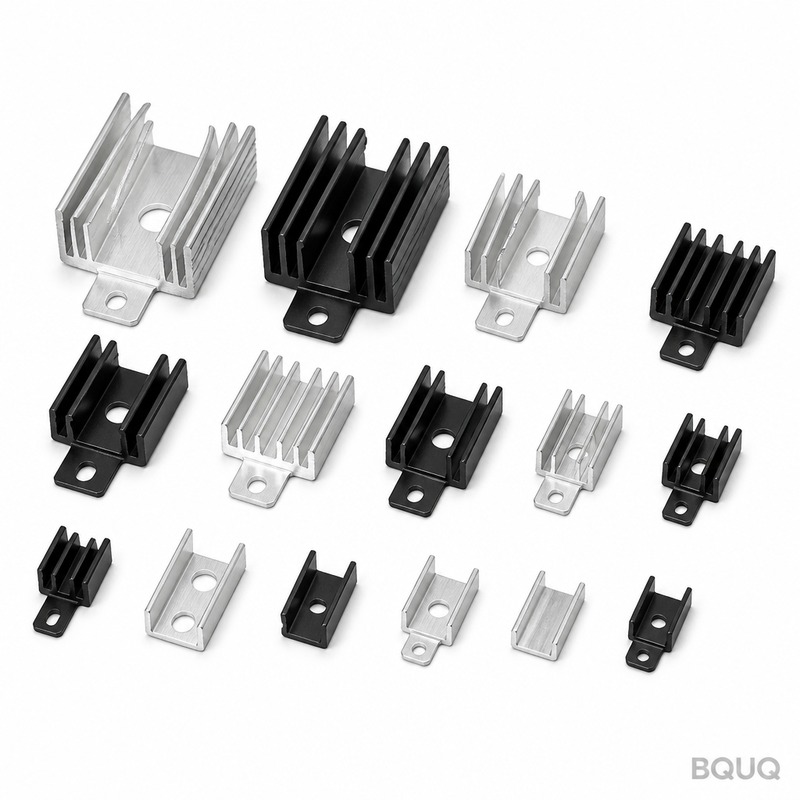
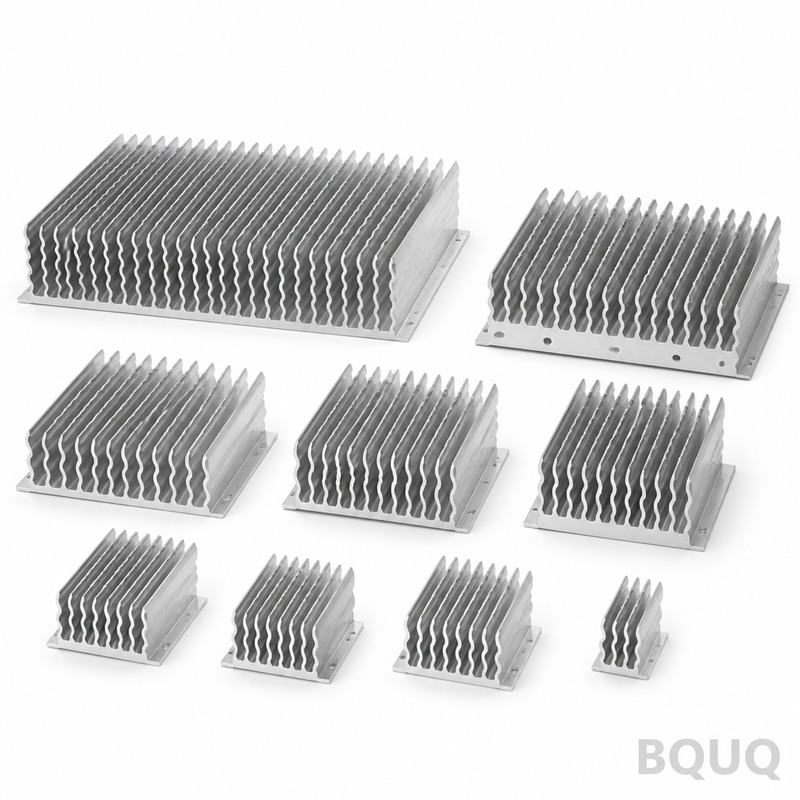
See also: Custom Decorative Craft Springs.
Learn more about Why Does LED Heat Sink Design Matter for Lifespan and Performance?.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 1050A aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | 50 pieces |
| Capacity | 50,000 pieces |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard hard anodize Type III | VFD and inverter thermal management | 25-40 µm coating adds cost versus bare aluminium |
| 0.8 mm fin thickness | Balancing thermal performance and weight | Thinner fins reduce stiffness and may need extra deburring |
| 1.5 mm fin pitch | High surface area in compact envelopes | Tighter pitch increases tooling wear and inspection time |
| ±0.20 mm general tolerance | Production speed with standard CNC and stamping | Tighter tolerances require 100% inspection and higher unit cost |
| 50-piece validation run | Design verification before mass production | Higher per-unit cost than 50,000-piece production |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Tooling design | Fix material condition and tooling geometry before machining | Tooling design and process validation run in parallel |
| Machining | Hold ±0.20 mm at production speed, not on a single slow part | Measured capability recorded for the process window |
| Deburring | Remove burrs from fins and edges | Deburring step logged as a secondary operation |
| Anodizing | Hard anodize Type III, 25-40 µm | Coating thickness and surface finish recorded |
| Final inspection | 100% inspection when required by tolerance or customer | Inspection data retained for traceability |
Frequently Asked Questions
What is the thermal resistance of this heat sink compound?
The thermal resistance is 0.85 K/W. This value is tied to the 1050A aluminium base, 0.8 mm fin thickness, and 1.5 mm fin pitch. It is a key number for comparing against other VFD and inverter cooling solutions before you commit to a 50-piece or 50,000-piece order.
Further technical detail: Extruded vs Skived vs Stamped Heat Sinks: Cost and Performance Compared.
What material and surface finish do you use?
We use 1050A aluminium with hard anodize Type III at 25-40 µm. This finish supports thermal management in VFD and inverter applications. The general tolerance is ±0.20 mm. If your design needs a different coating or thickness, confirm it before ordering because it changes cost and lead time.
Recommended reading: 5052 vs 6061 Aluminum: Machining and Finishing Differences.
What is the lead time for 50 to 50,000 pieces?
Lead time can be 10 working days when tooling design and process validation run in parallel. This applies from 50 pieces for validation up to 50,000 for production. The compressed cycle replaces what used to be a 12-week tooling and qualification cycle, so confirm your drawing and inspection requirements early.
What tolerance can you hold at production speed?
We hold ±0.20 mm general tolerance at production speed, not just on a single slow part. We fix material condition and tooling geometry first, then confirm capability across the run. If your application needs tighter than ±0.20 mm, expect added inspection and higher unit cost.
Compare it with LED Heat Sink Selection: Sizing for Lumen Output and Lifetime.
What drives the unit cost of heat sink compound?
Cost pressure in VFD and inverter rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution. Confirm which secondary operations are truly required before you request a quote.
Can you support both validation runs and mass production?
Yes. Whether you need 50 pieces for validation or 50,000 for a production line, the same physics apply. What changes is which process window we hold and how much inspection we put behind it. Tooling design and process validation run in parallel to support the 10-working-day lead time.
What should I confirm before ordering heat sink compound?
Confirm material 1050A aluminium, fin thickness 0.8 mm, fin pitch 1.5 mm, thermal resistance 0.85 K/W, hard anodize Type III at 25-40 µm, and general tolerance ±0.20 mm. Also confirm quantity from 50 to 50,000 pieces, lead time of 10 working days, and which secondary operations like deburring, plating, or 100% inspection are required.